Stage 01
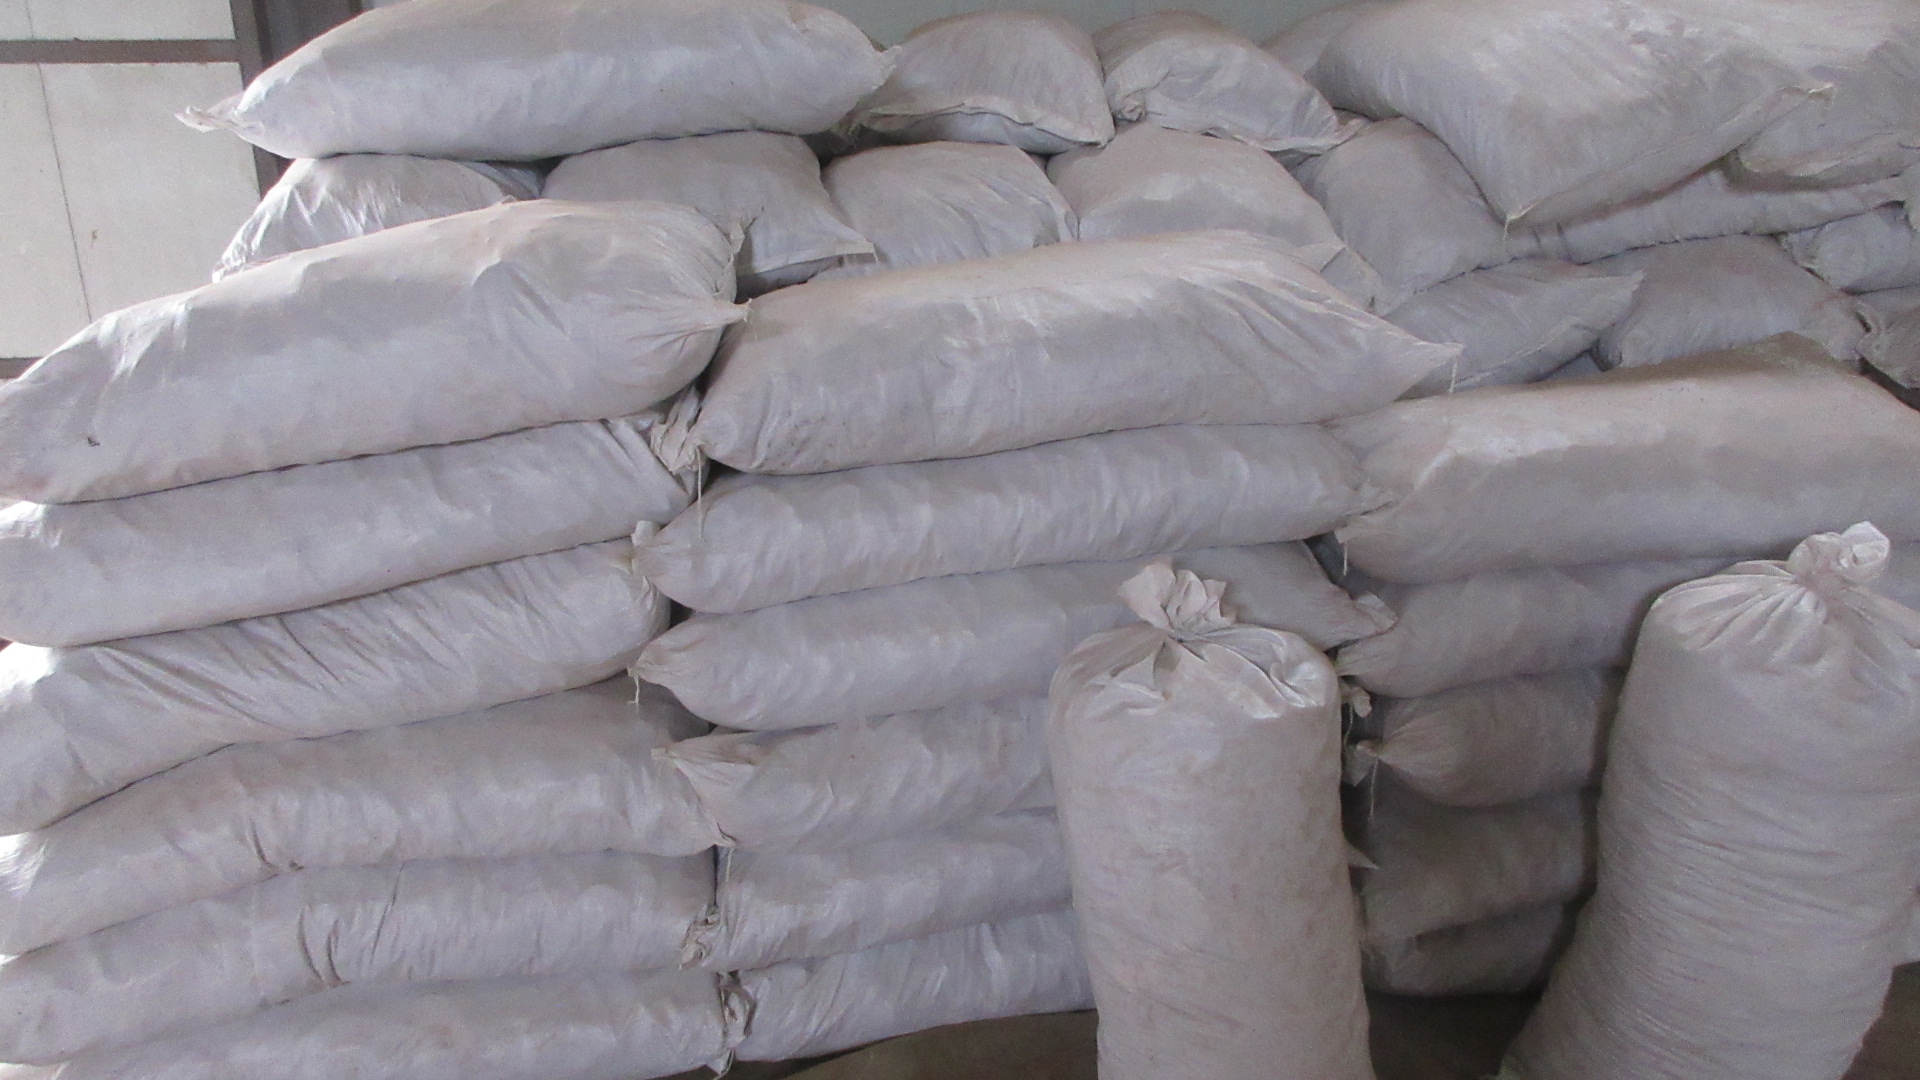
Raw Materials
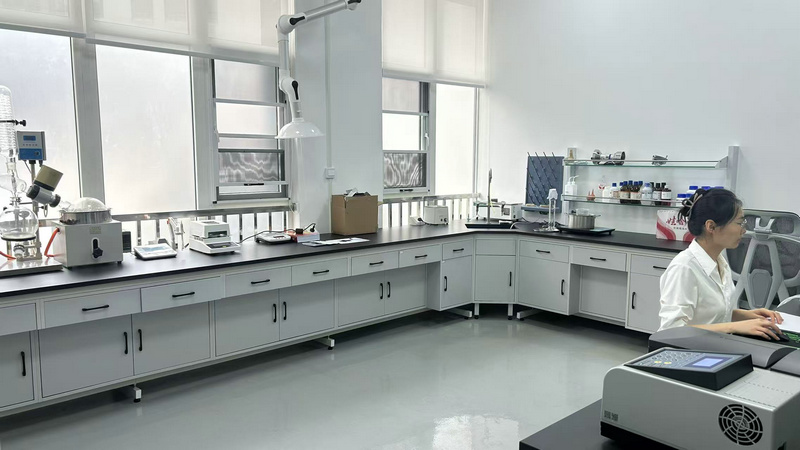
Direct farm-sourced botanicals undergo physical sorting, botanical identity verification (TLC/microscopic), moisture testing, and pre-screening for contaminants.
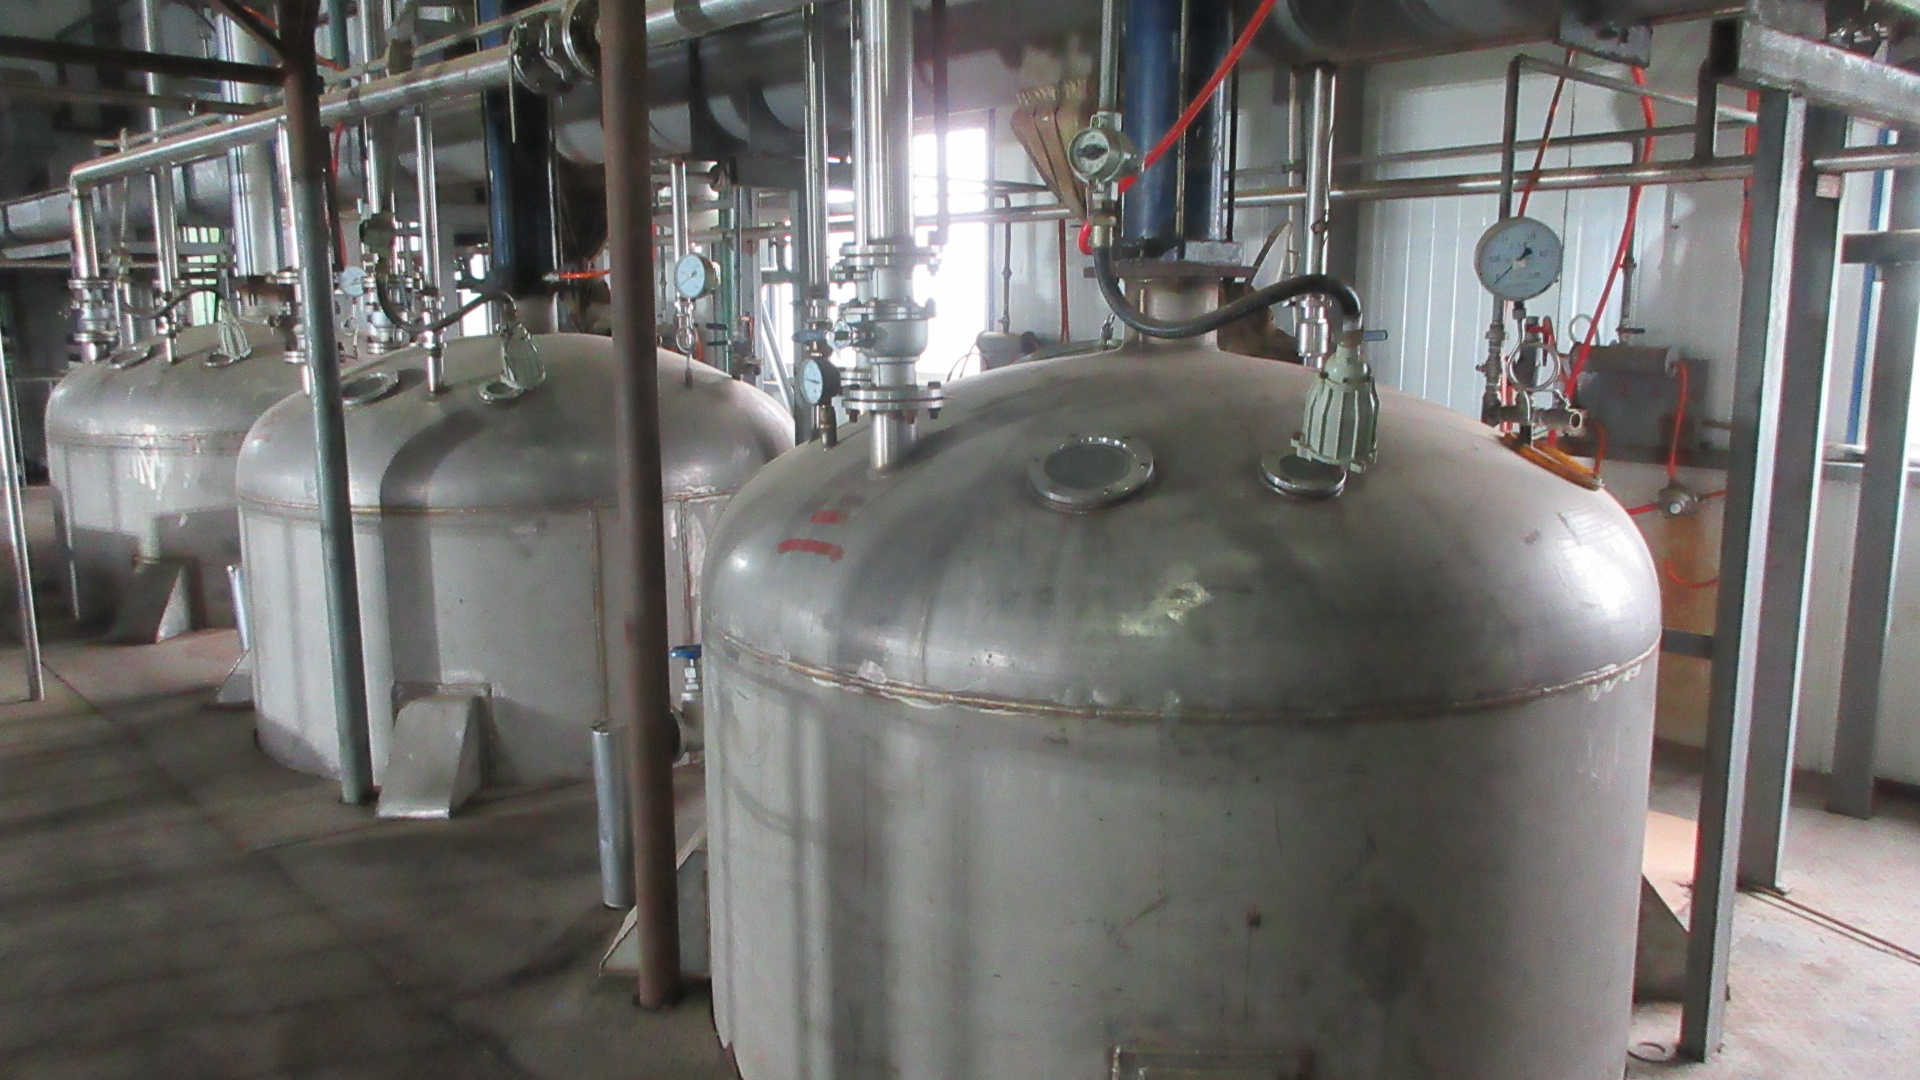
Xi'an Vexli Bio-Tech Co., Ltd. integrates origin-direct botanical sourcing with modern industrial extraction technology and strict analytical validation. Situated in Shaanxi Province—a traditional hub for herbal resources and botanical processing—our facility features high-standard cleanrooms, sealed stainless-steel extraction systems, low-temperature vacuum concentrators, and closed powder-handling workshops.
From raw herb incoming inspection to multi-stage crystallization, purification, spray drying, and clean packaging, every unit operation is systematically controlled to ensure strict batch-to-batch uniformity, international regulatory compliance, and total traceability.
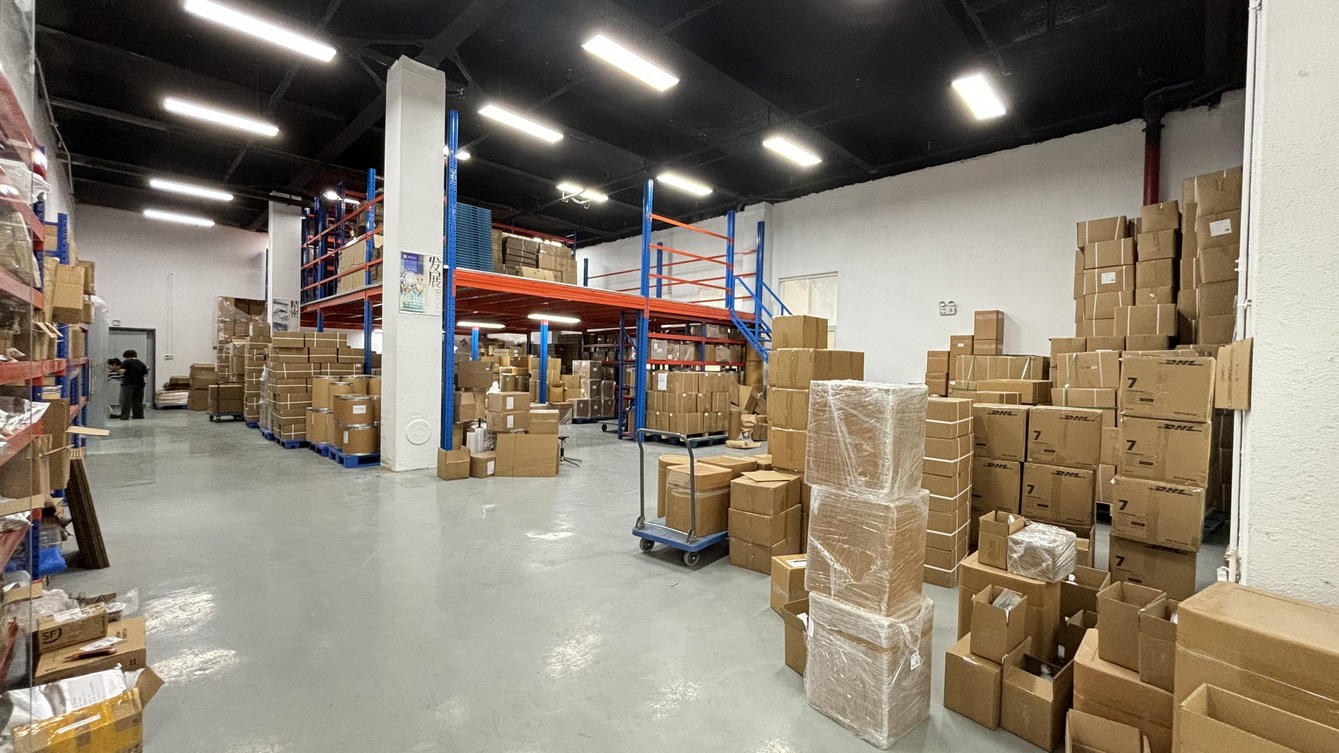
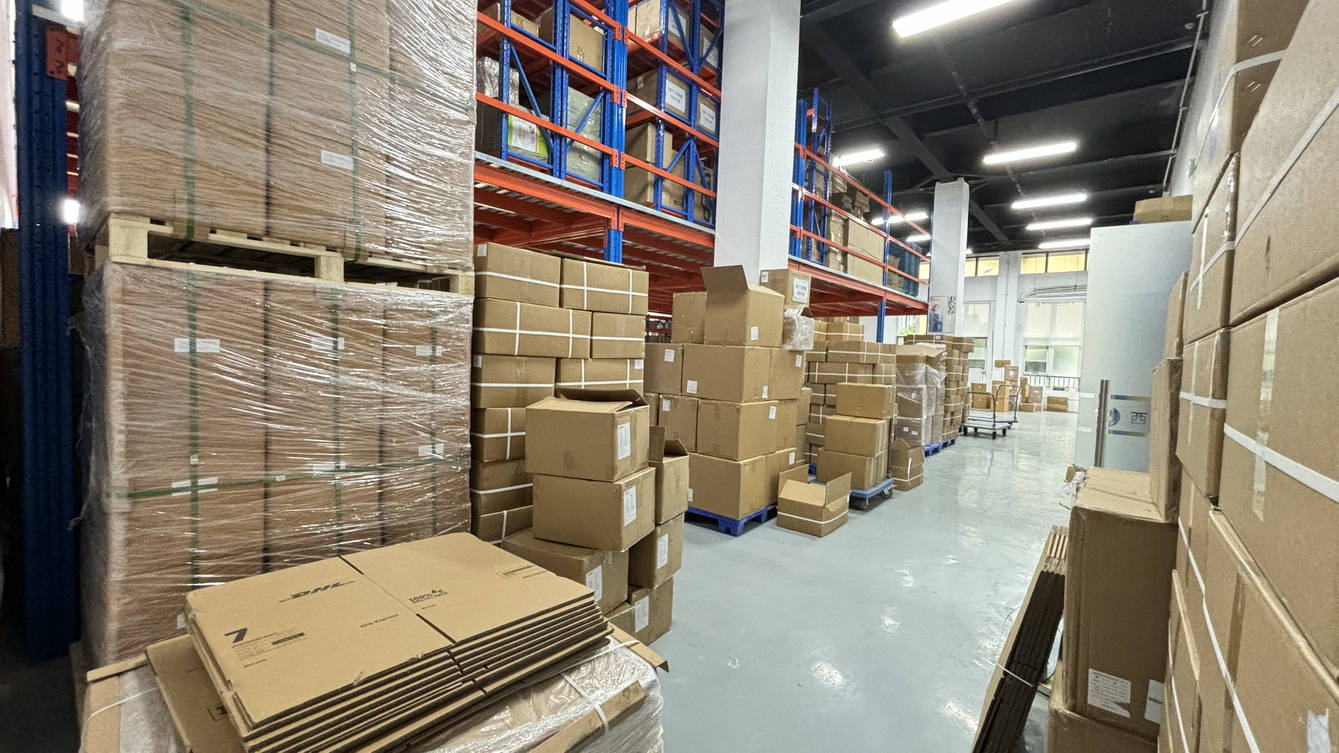
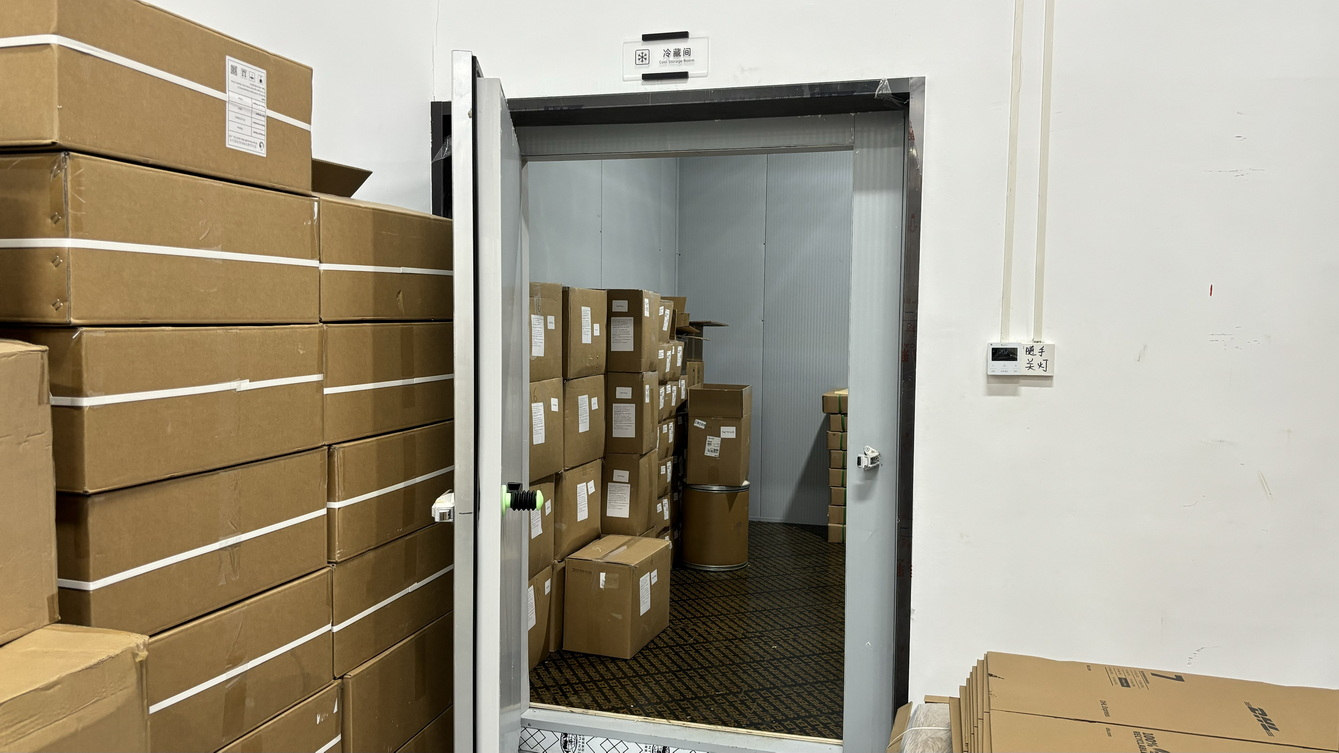
Every active ingredient and superfood powder produced by Xi'an Vexli Bio-Tech Co., Ltd. adheres to an audited, reproducible manufacturing protocol designed to protect functional bioactives and maintain purity.
Direct farm-sourced botanicals undergo physical sorting, botanical identity verification (TLC/microscopic), moisture testing, and pre-screening for contaminants.
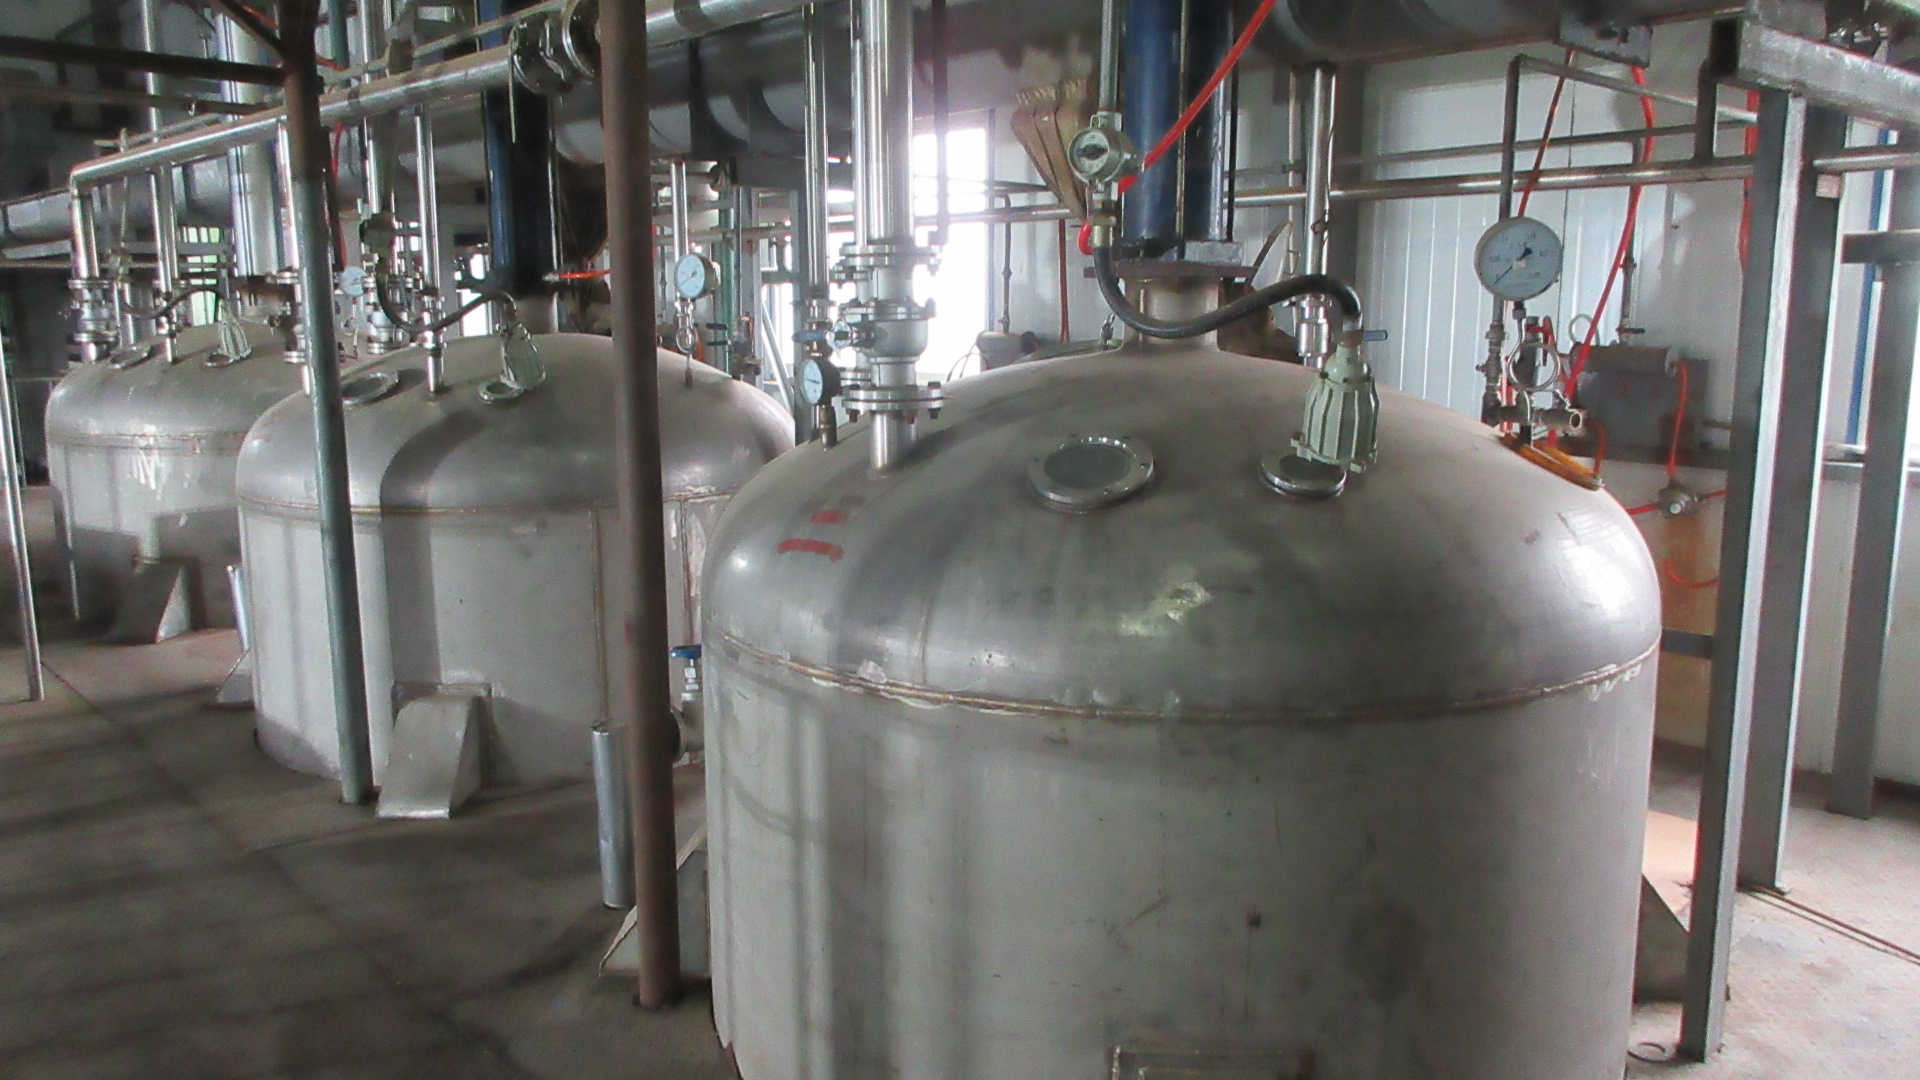
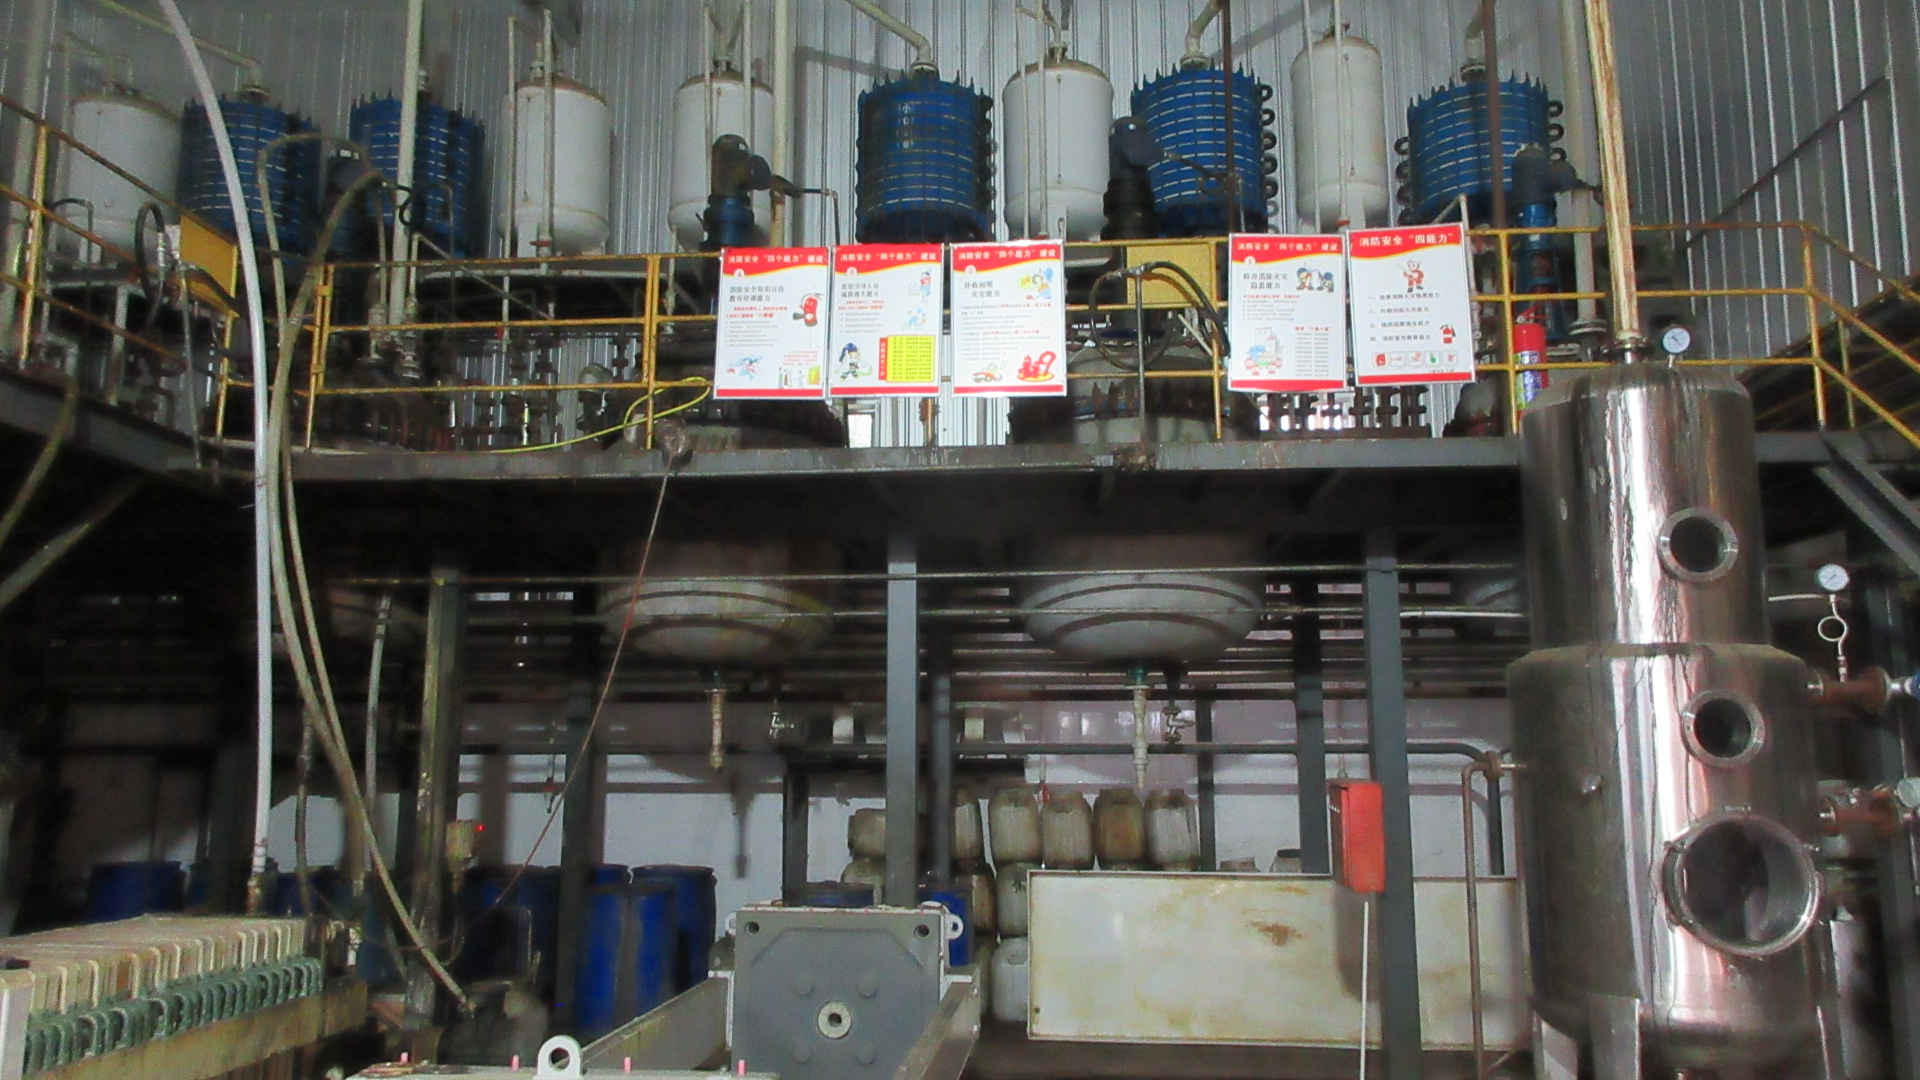
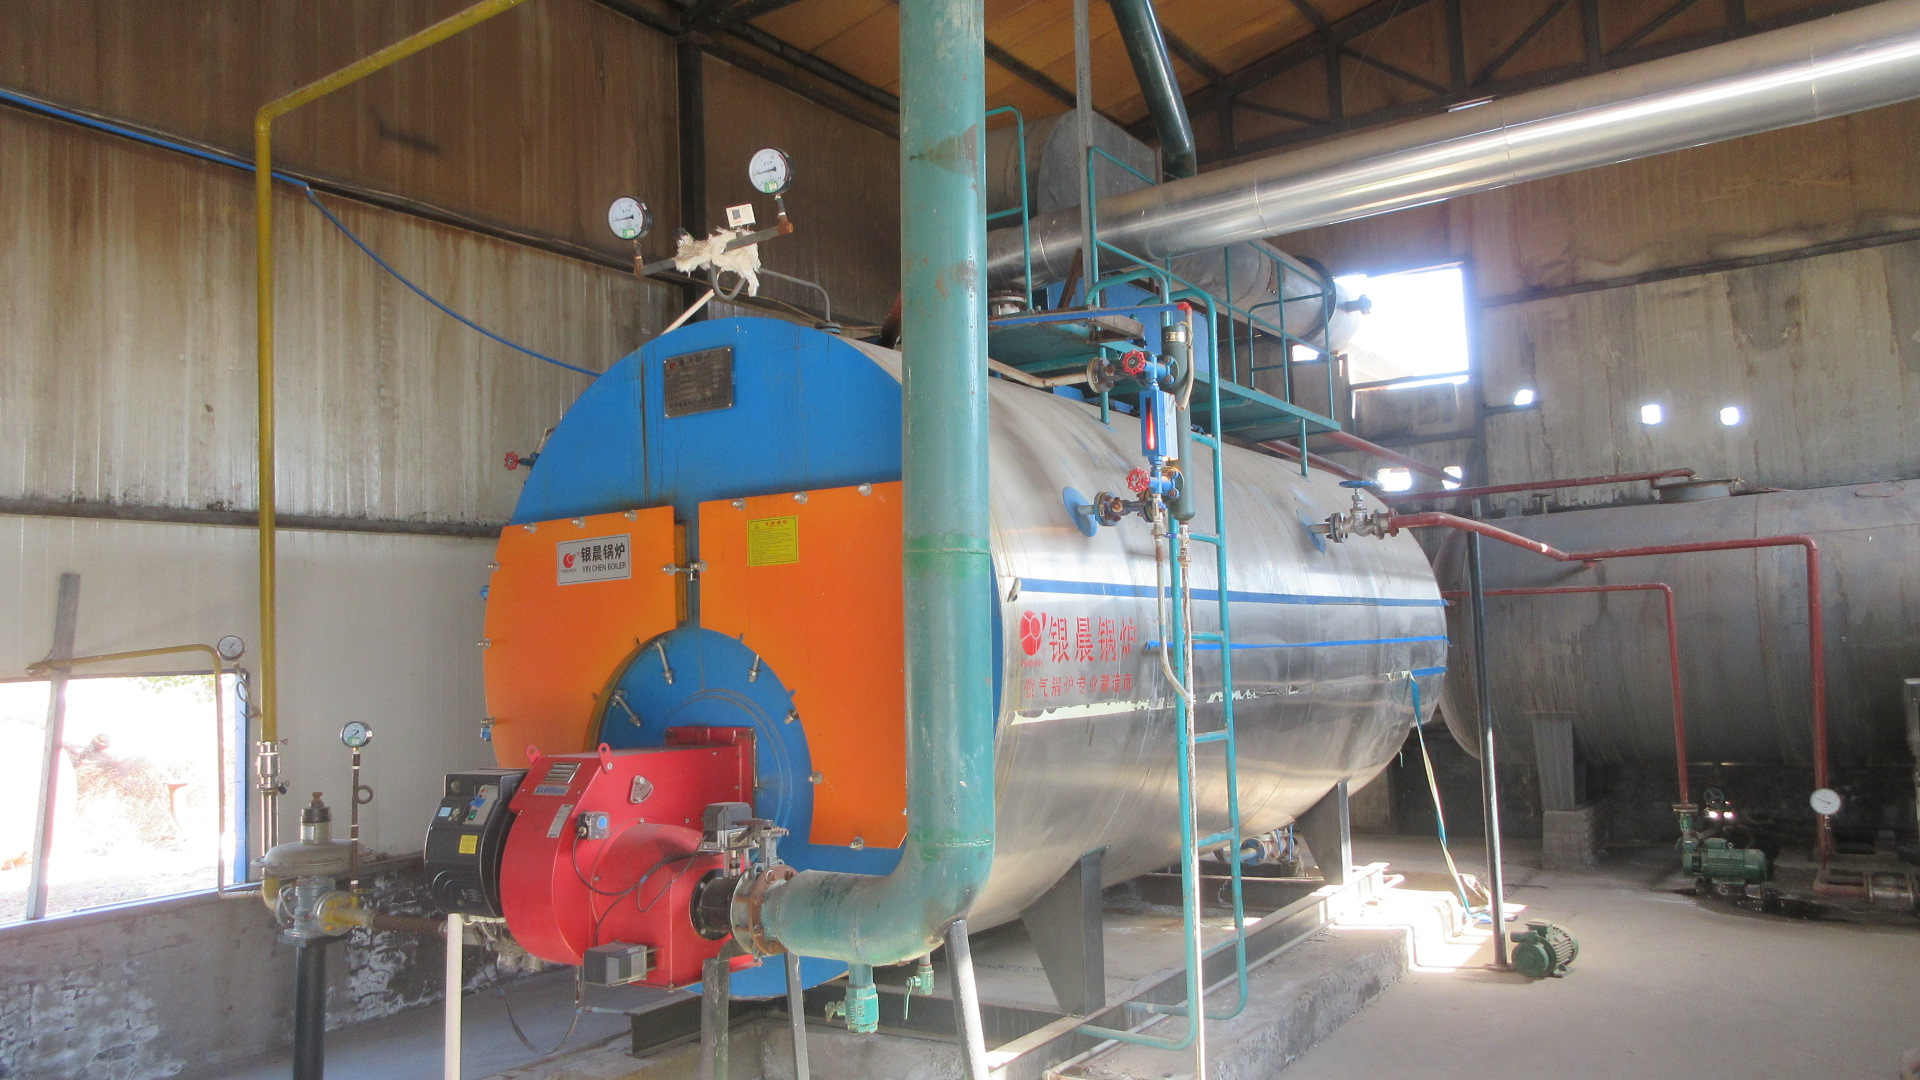
Dynamic multi-functional solid-liquid extraction with deionized water or food-grade ethanol under strictly calibrated temperature, pressure, and time curves.
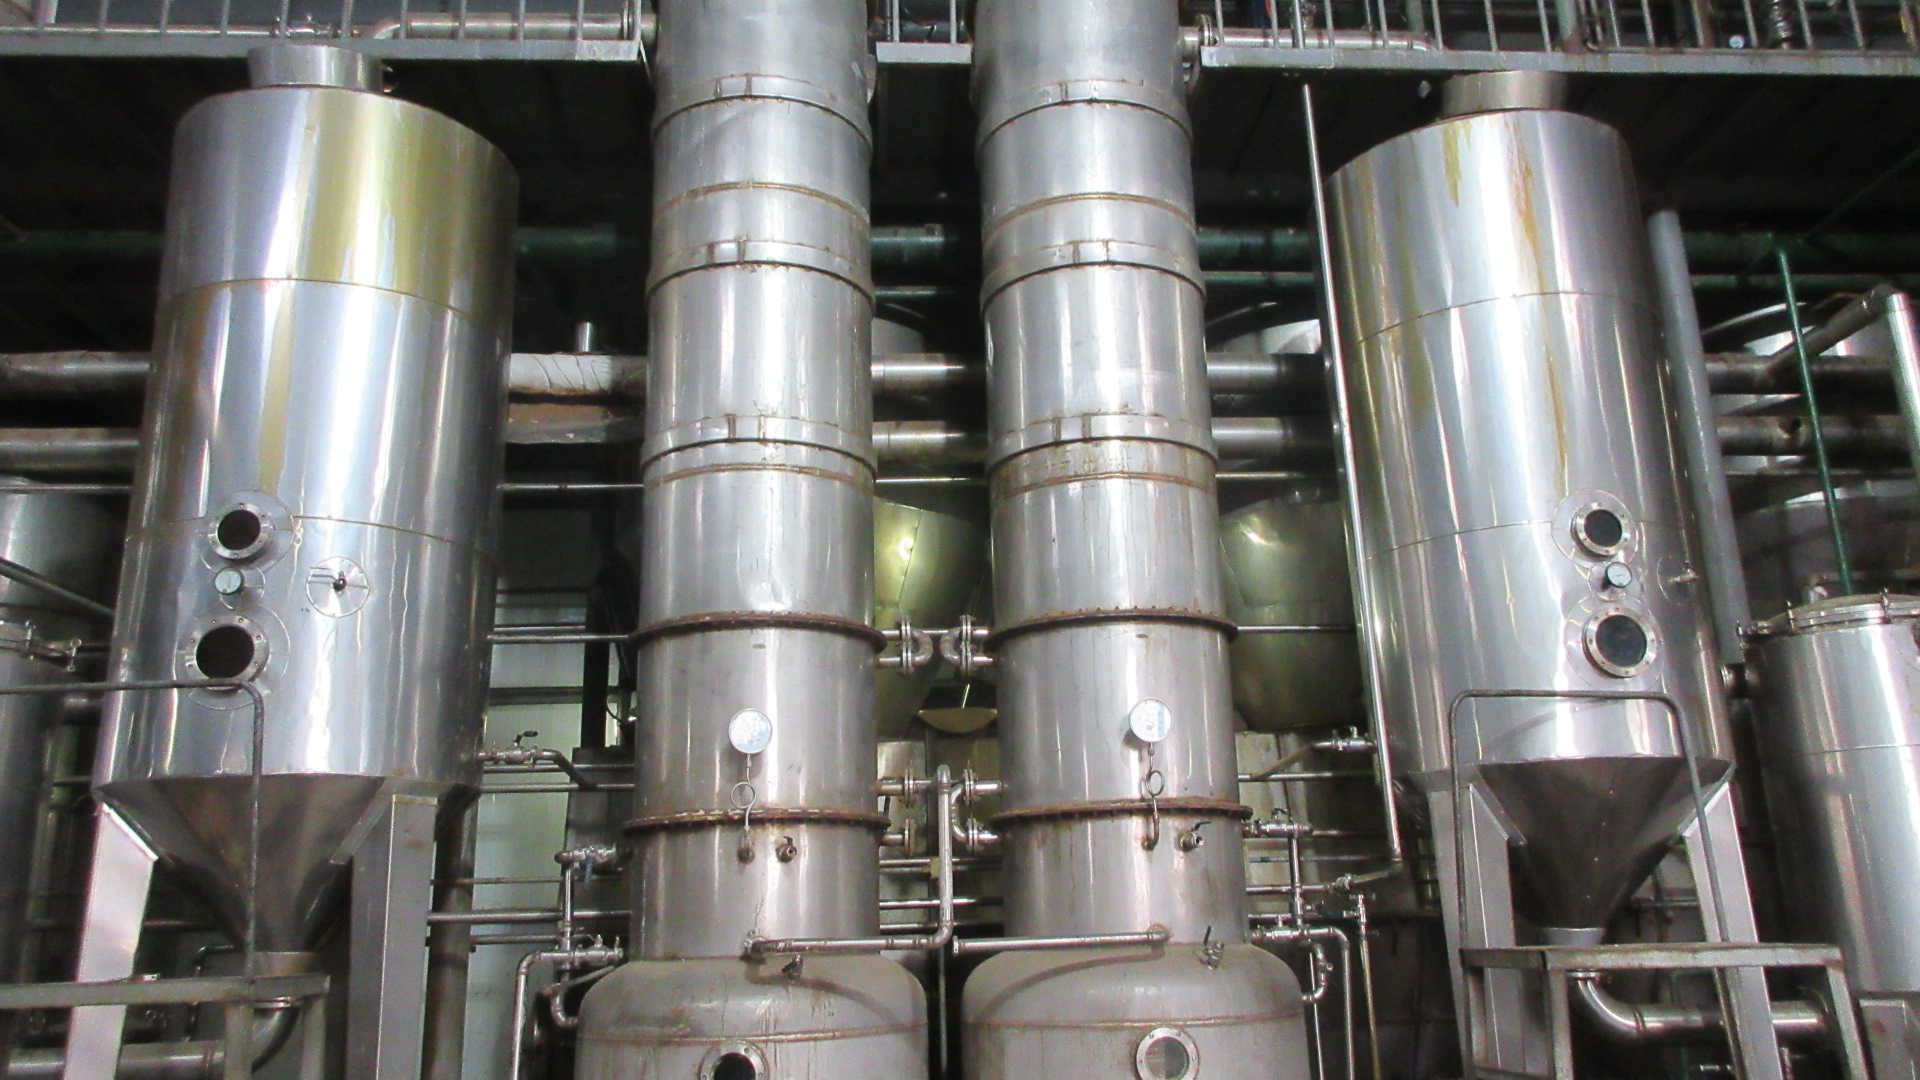
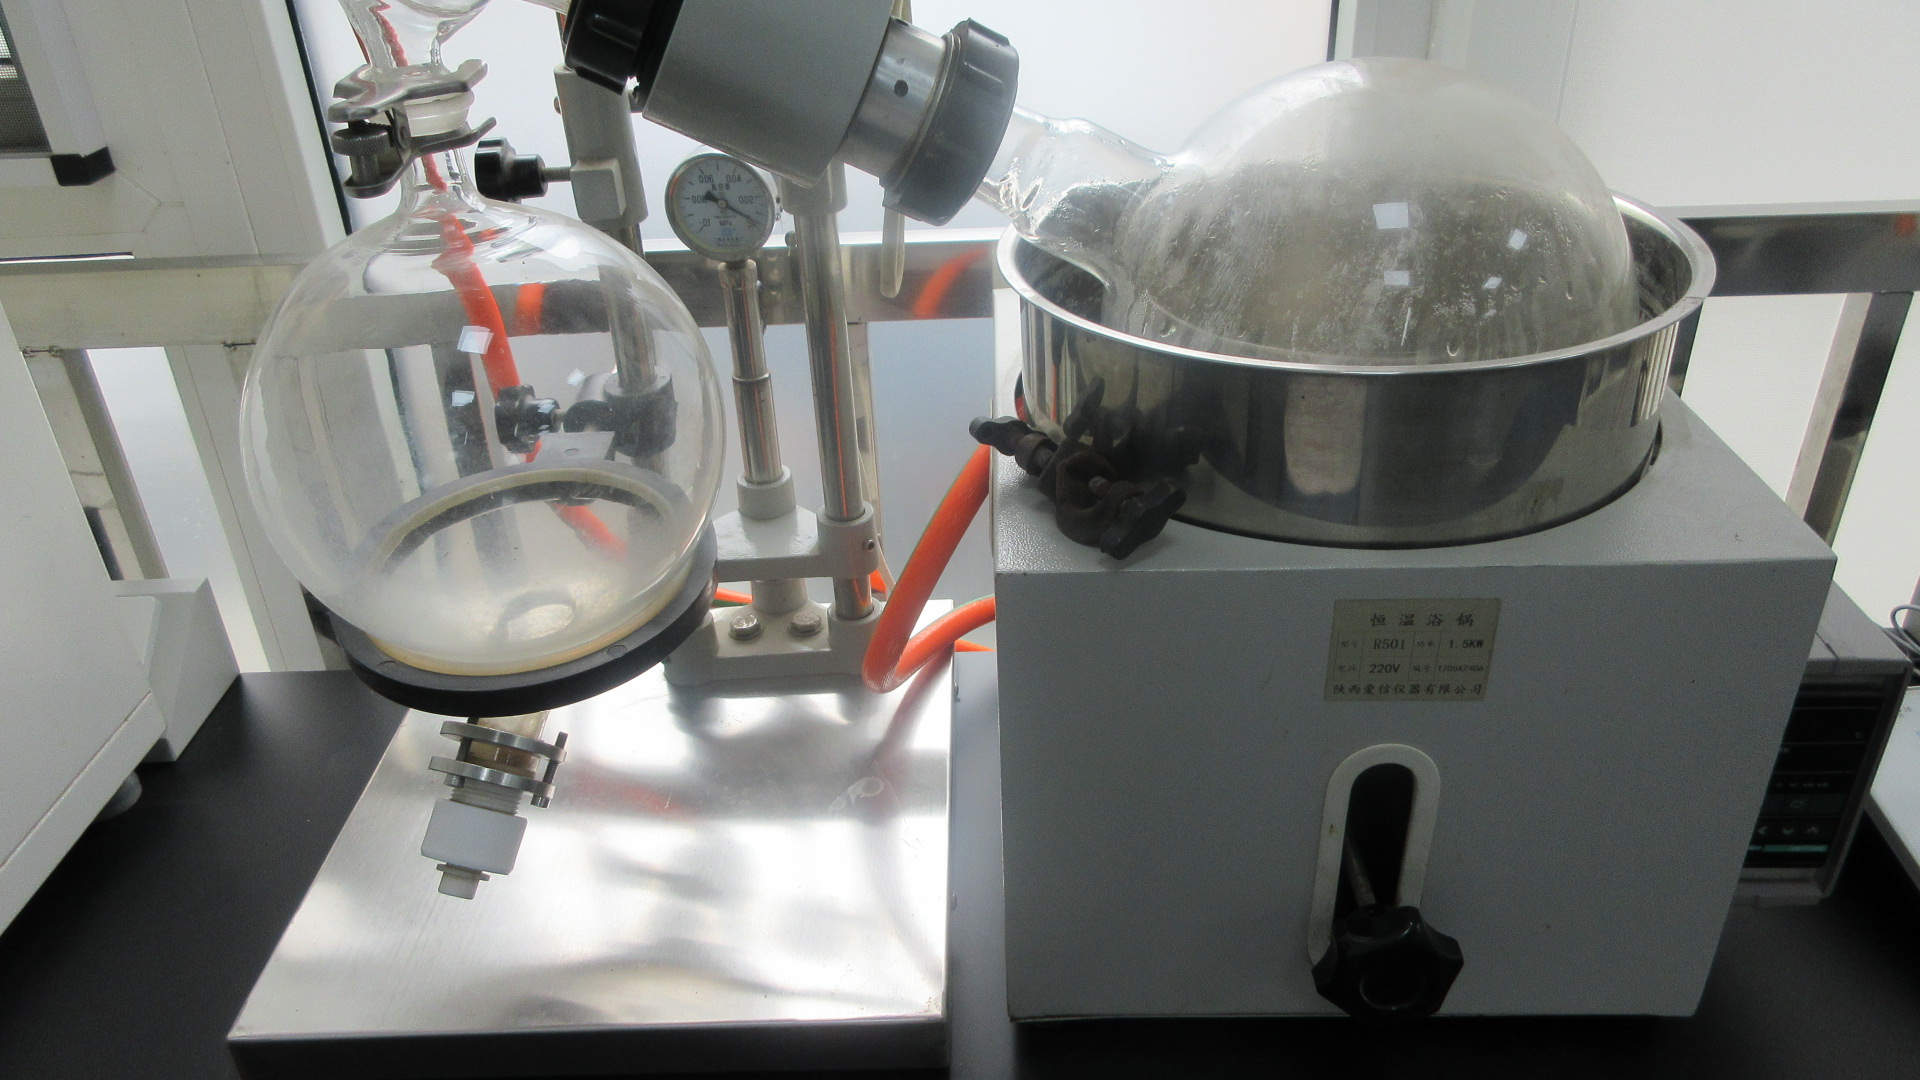
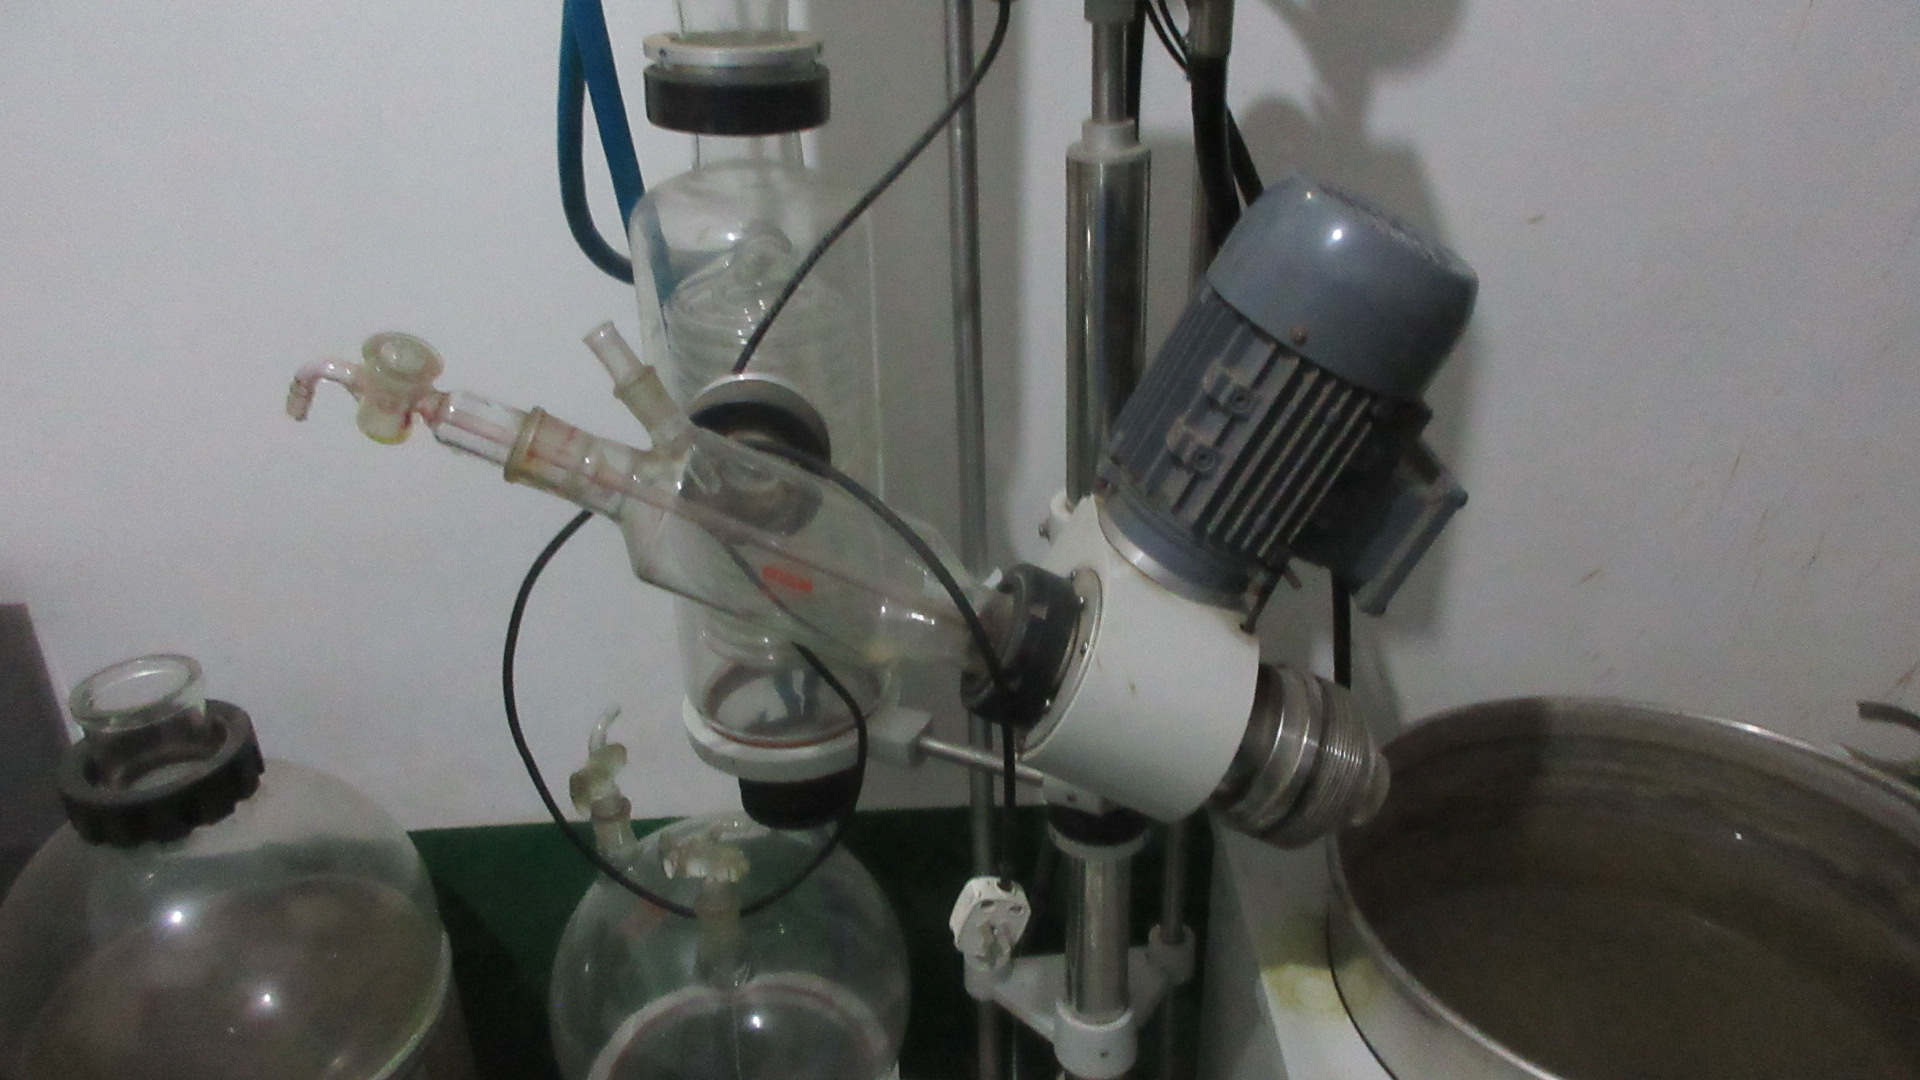
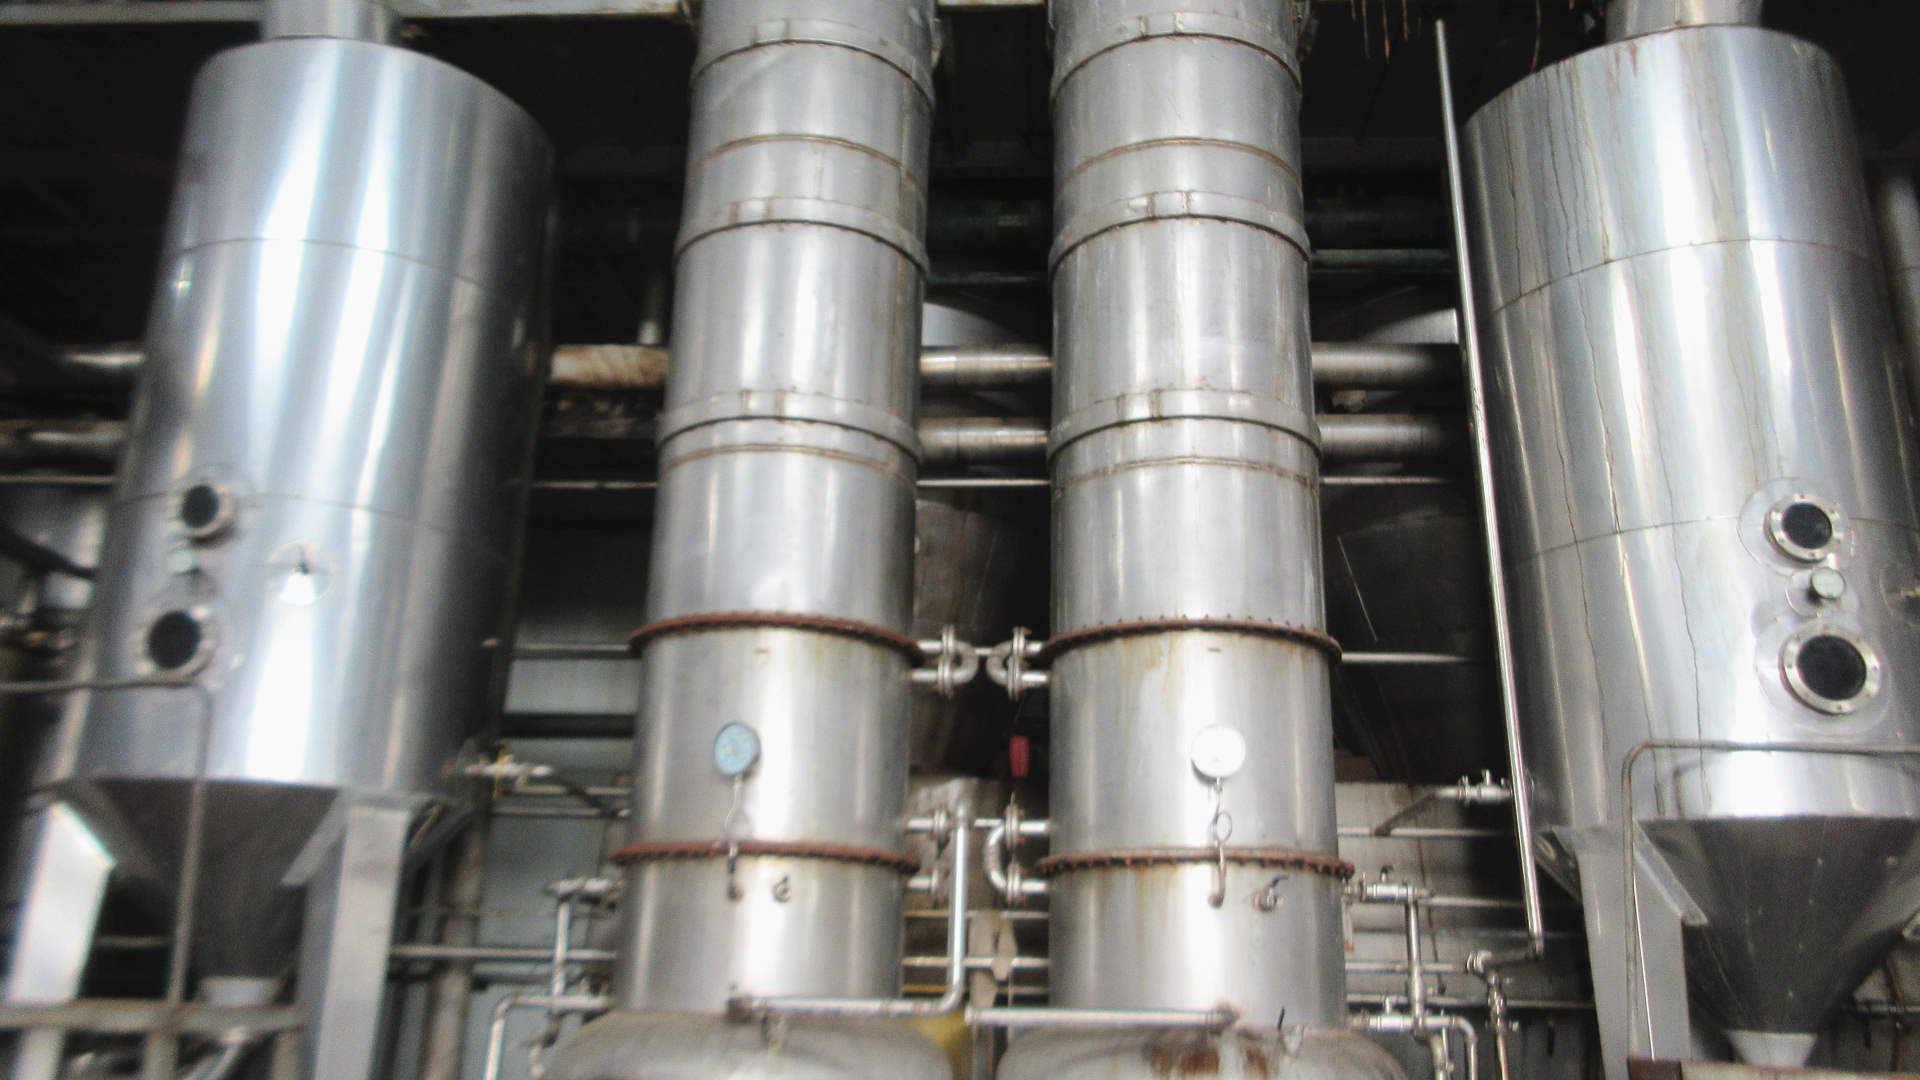
Falling-film and vacuum external circulation concentrators reduce moisture at low operating temperatures to preserve thermosensitive phytochemicals.
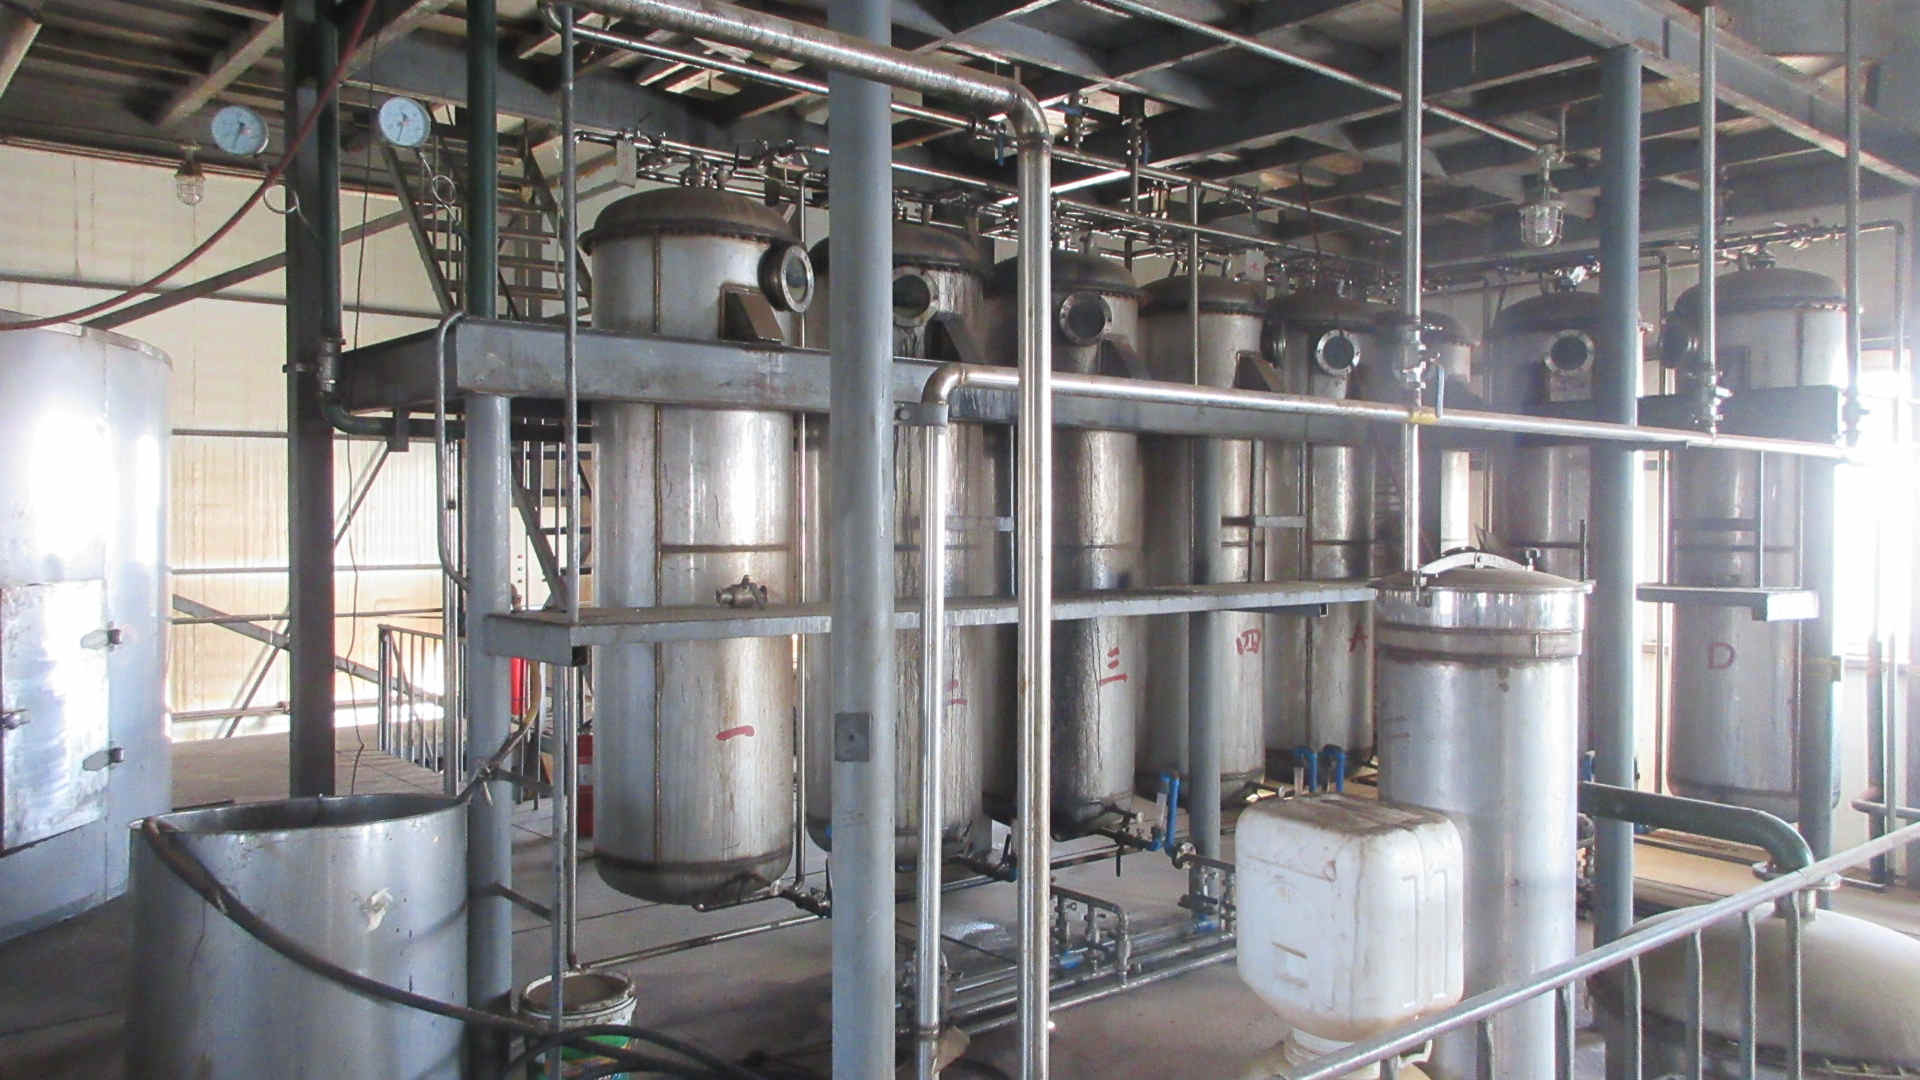
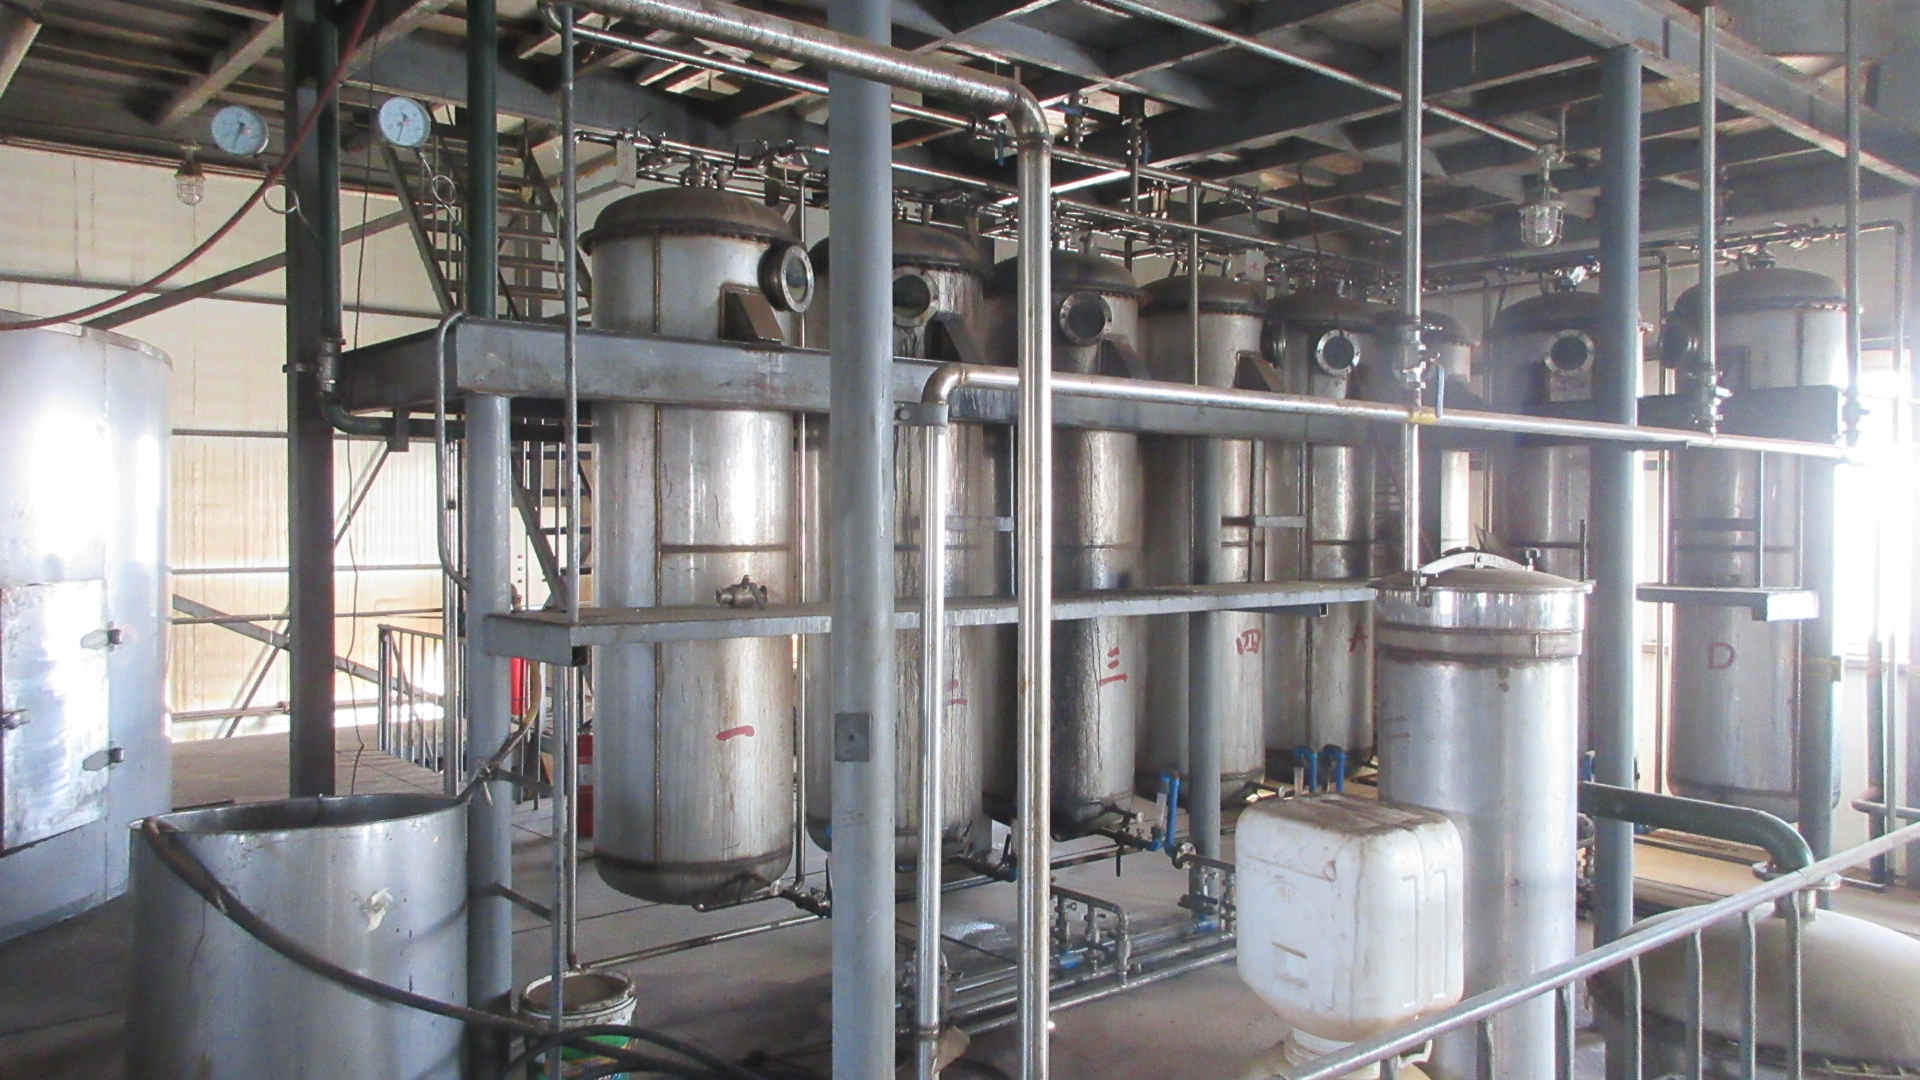
Macroporous adsorption resins and nanofiltration separation remove inactive impurities, isolating target markers such as polyphenols, polysaccharides, or alkaloids.
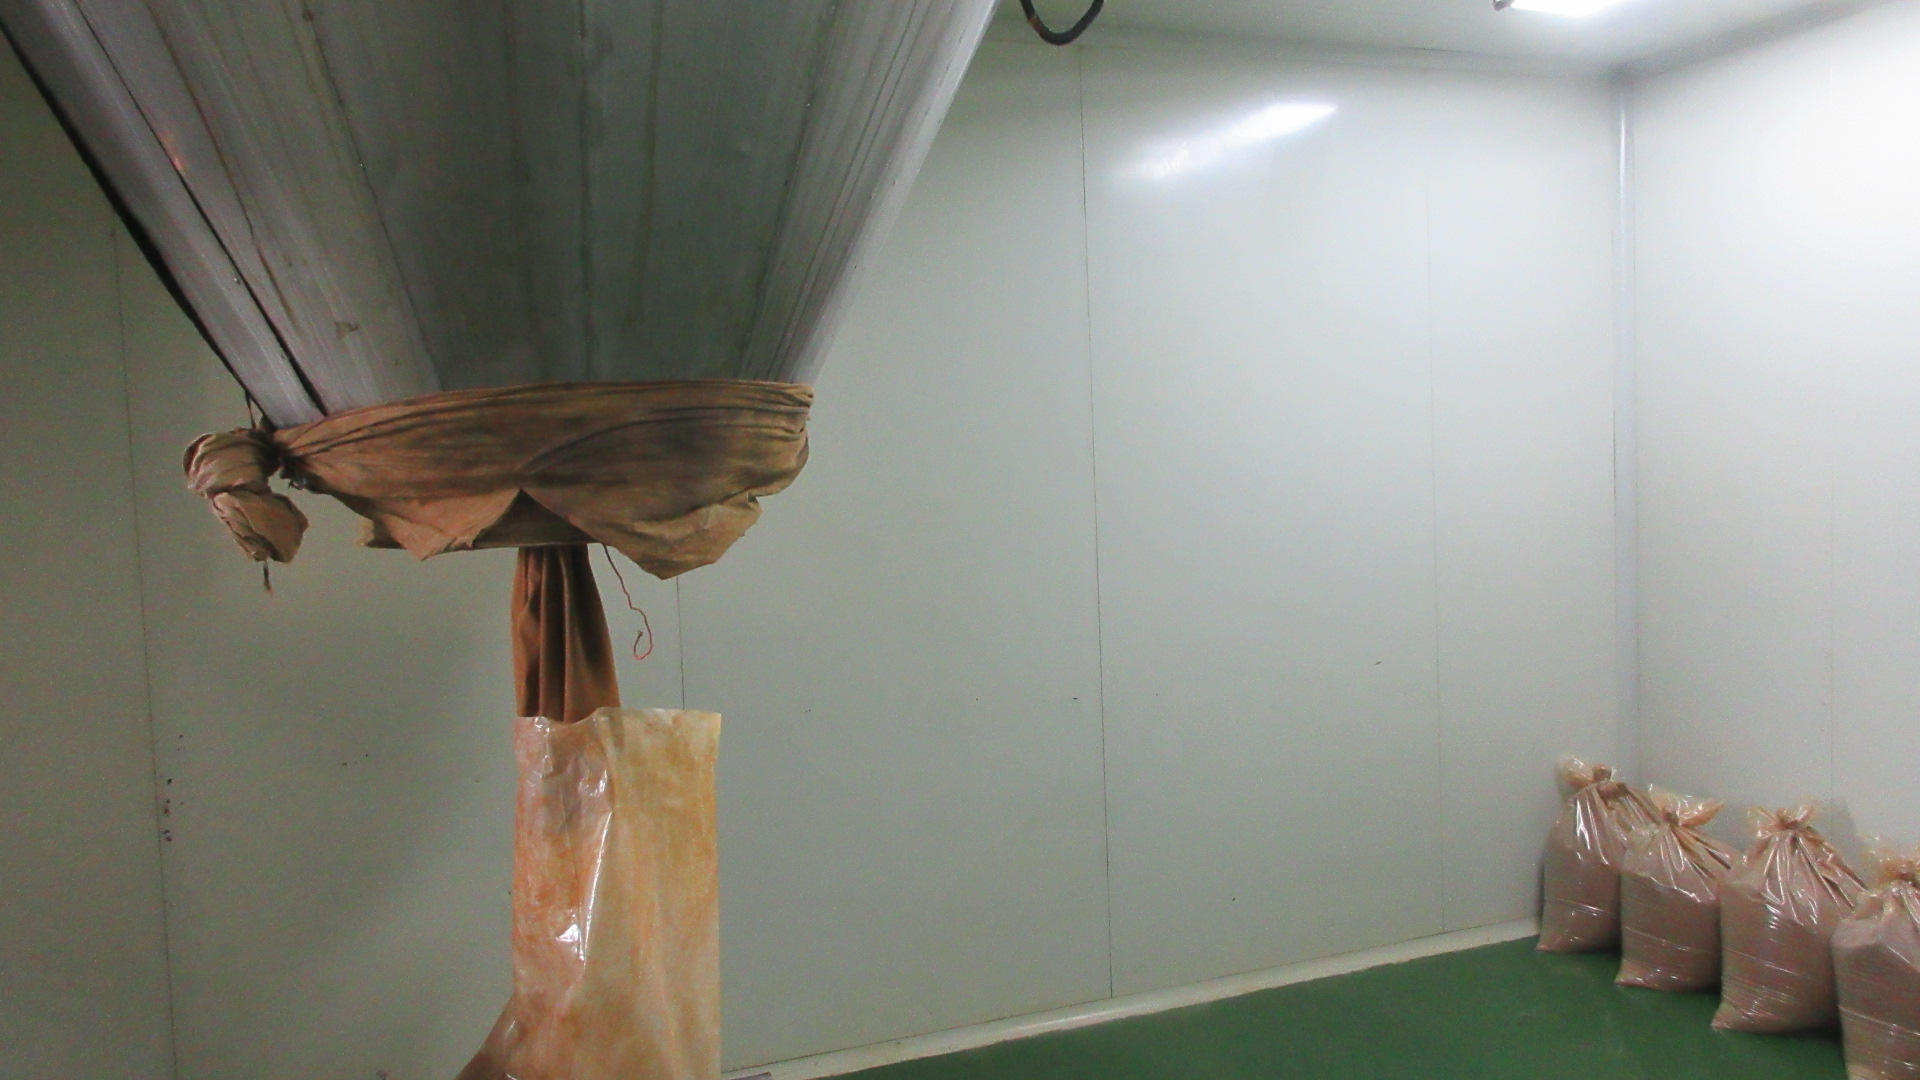
High-speed centrifugal spray drying and vacuum drying towers instantly convert purified concentrates into uniform, instantly soluble micro-powders.
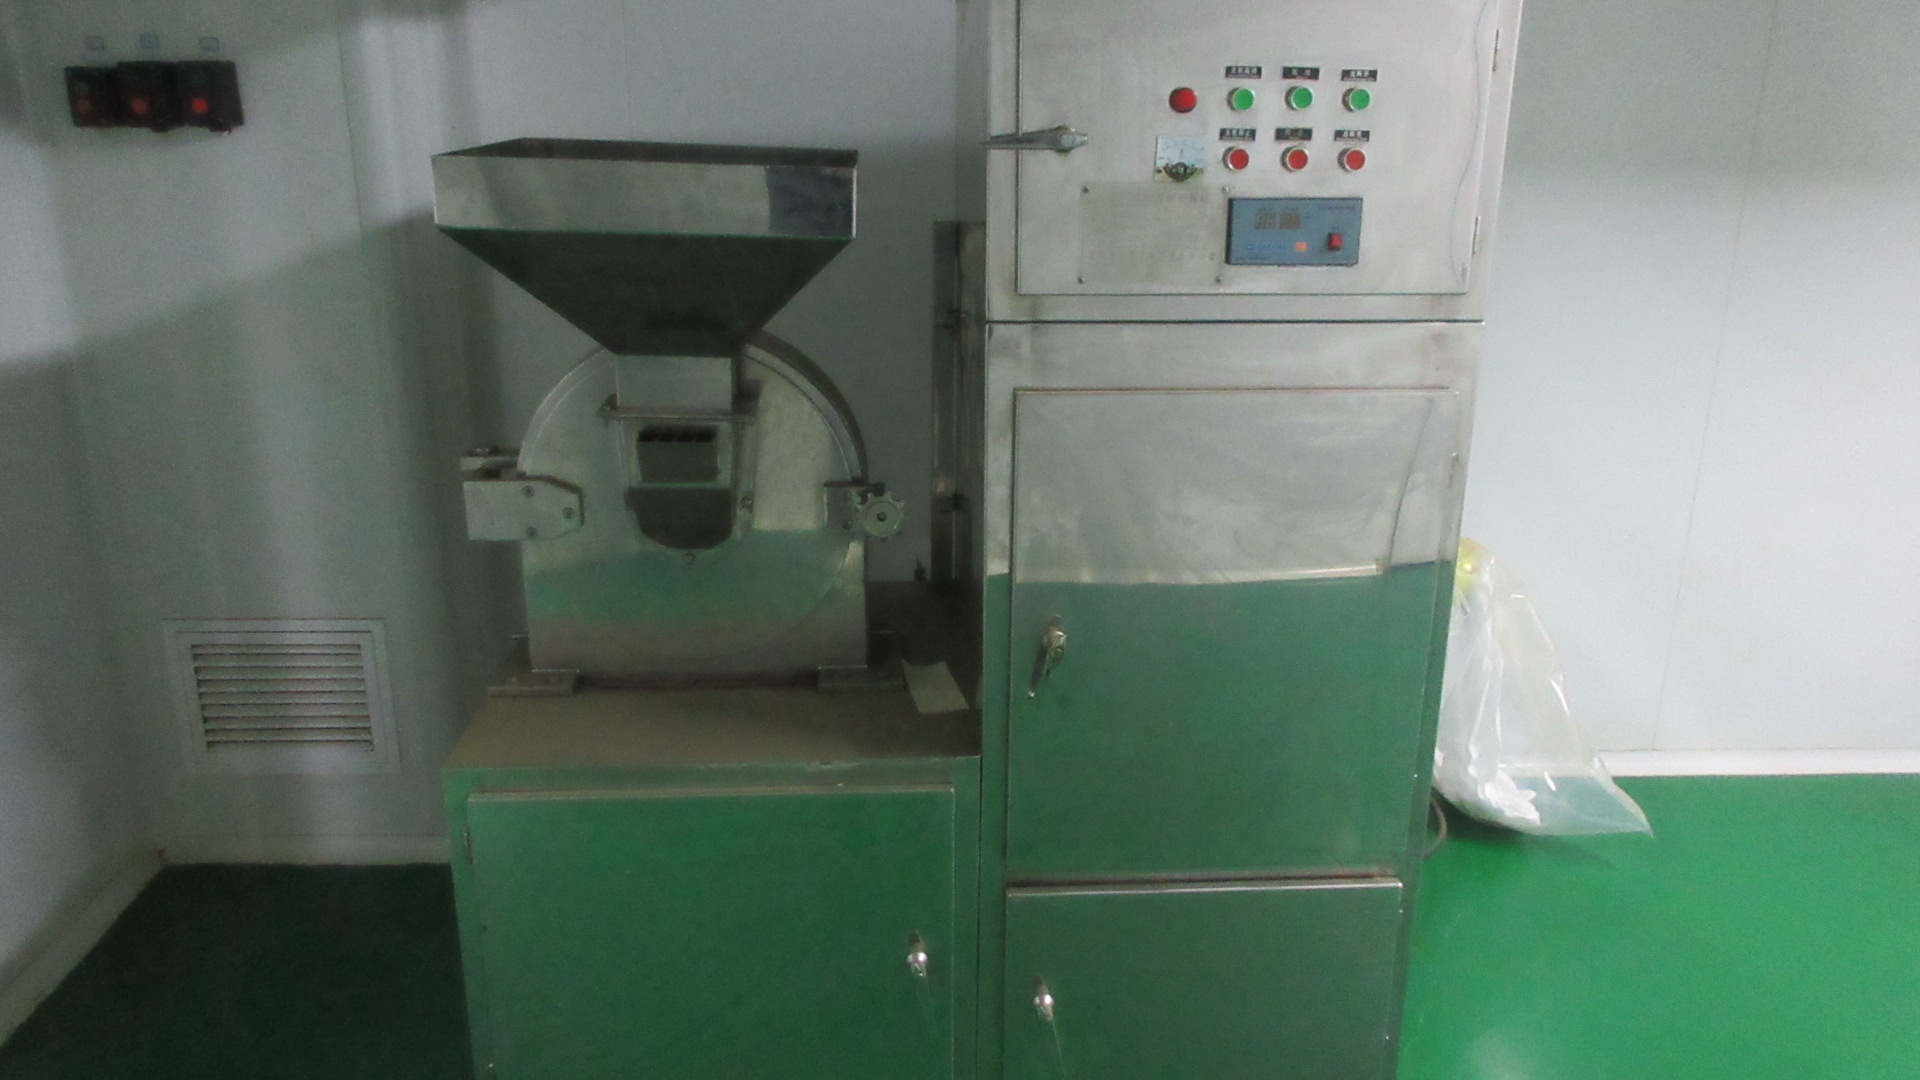
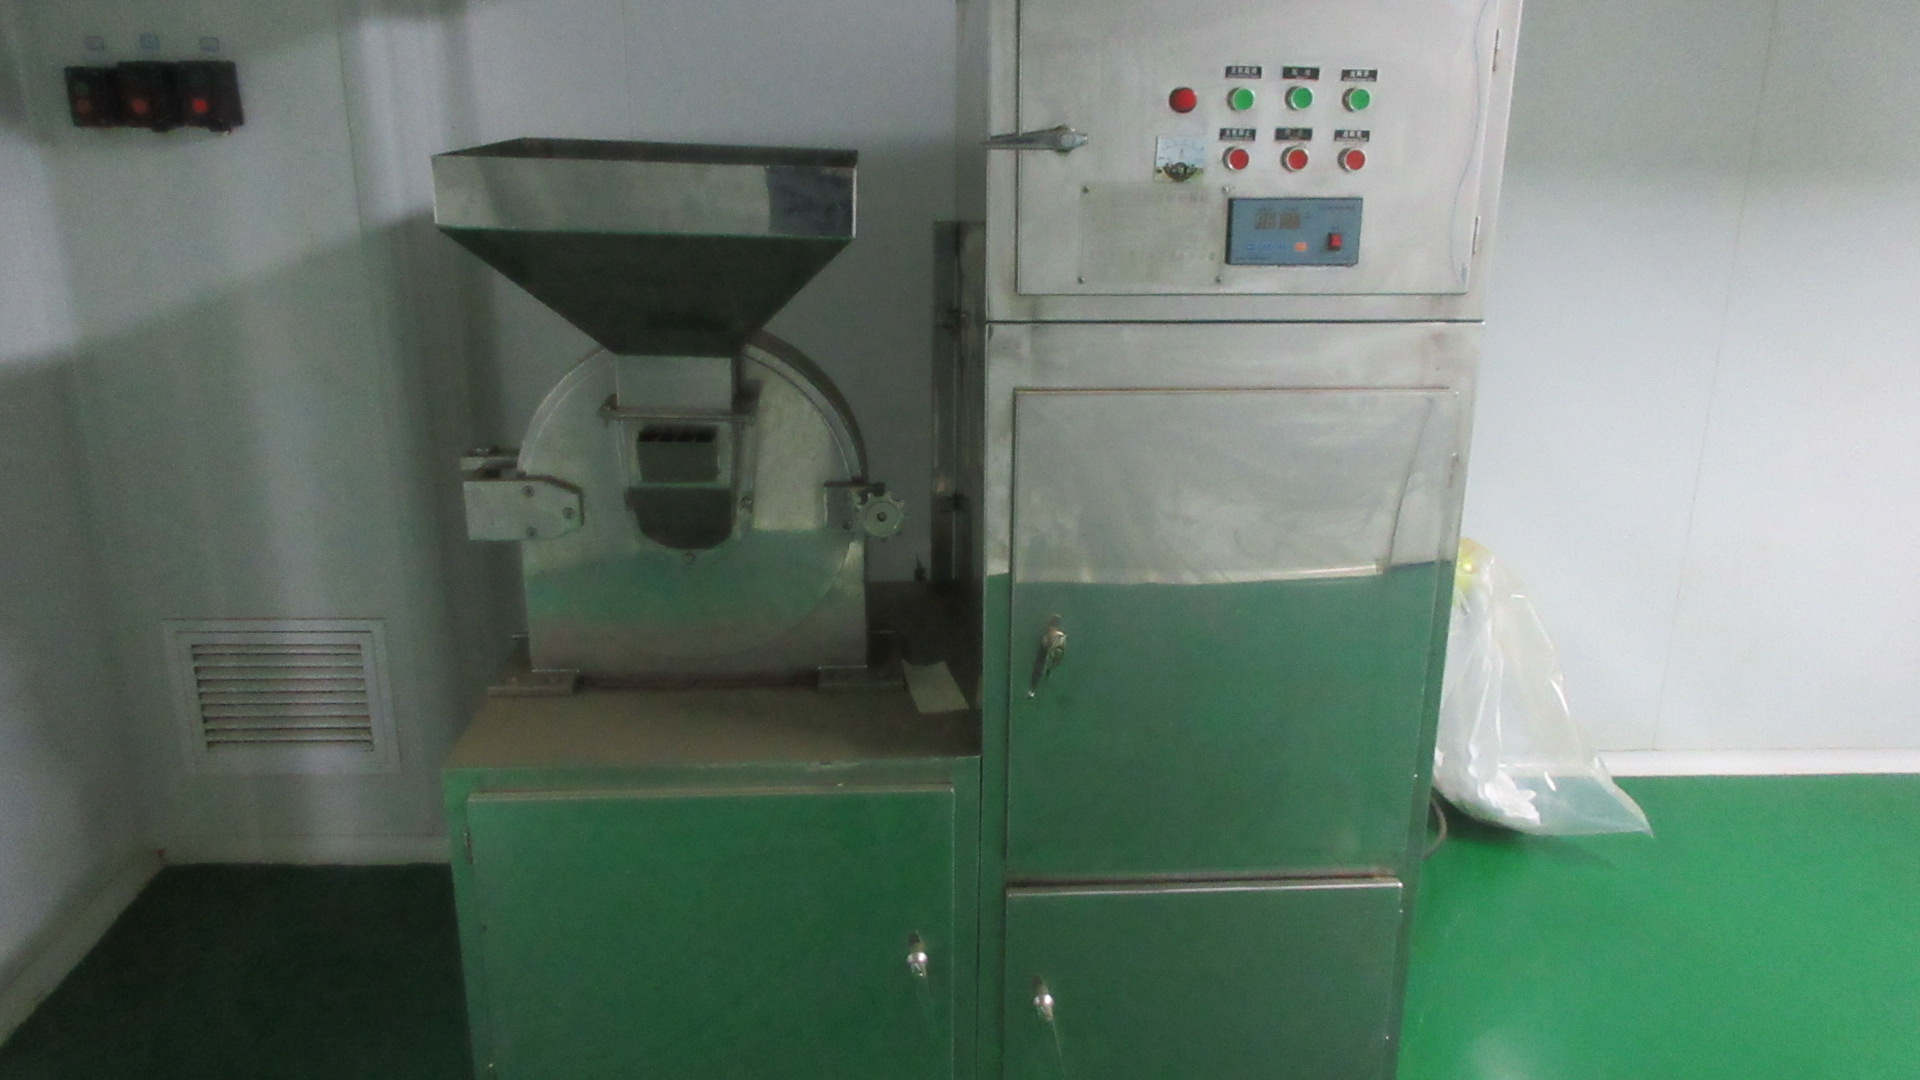
Ultra-fine airflow micronizers and mechanical pin mills crush dried solids into controlled particle sizes required for capsules, tablets, or liquid formulations.
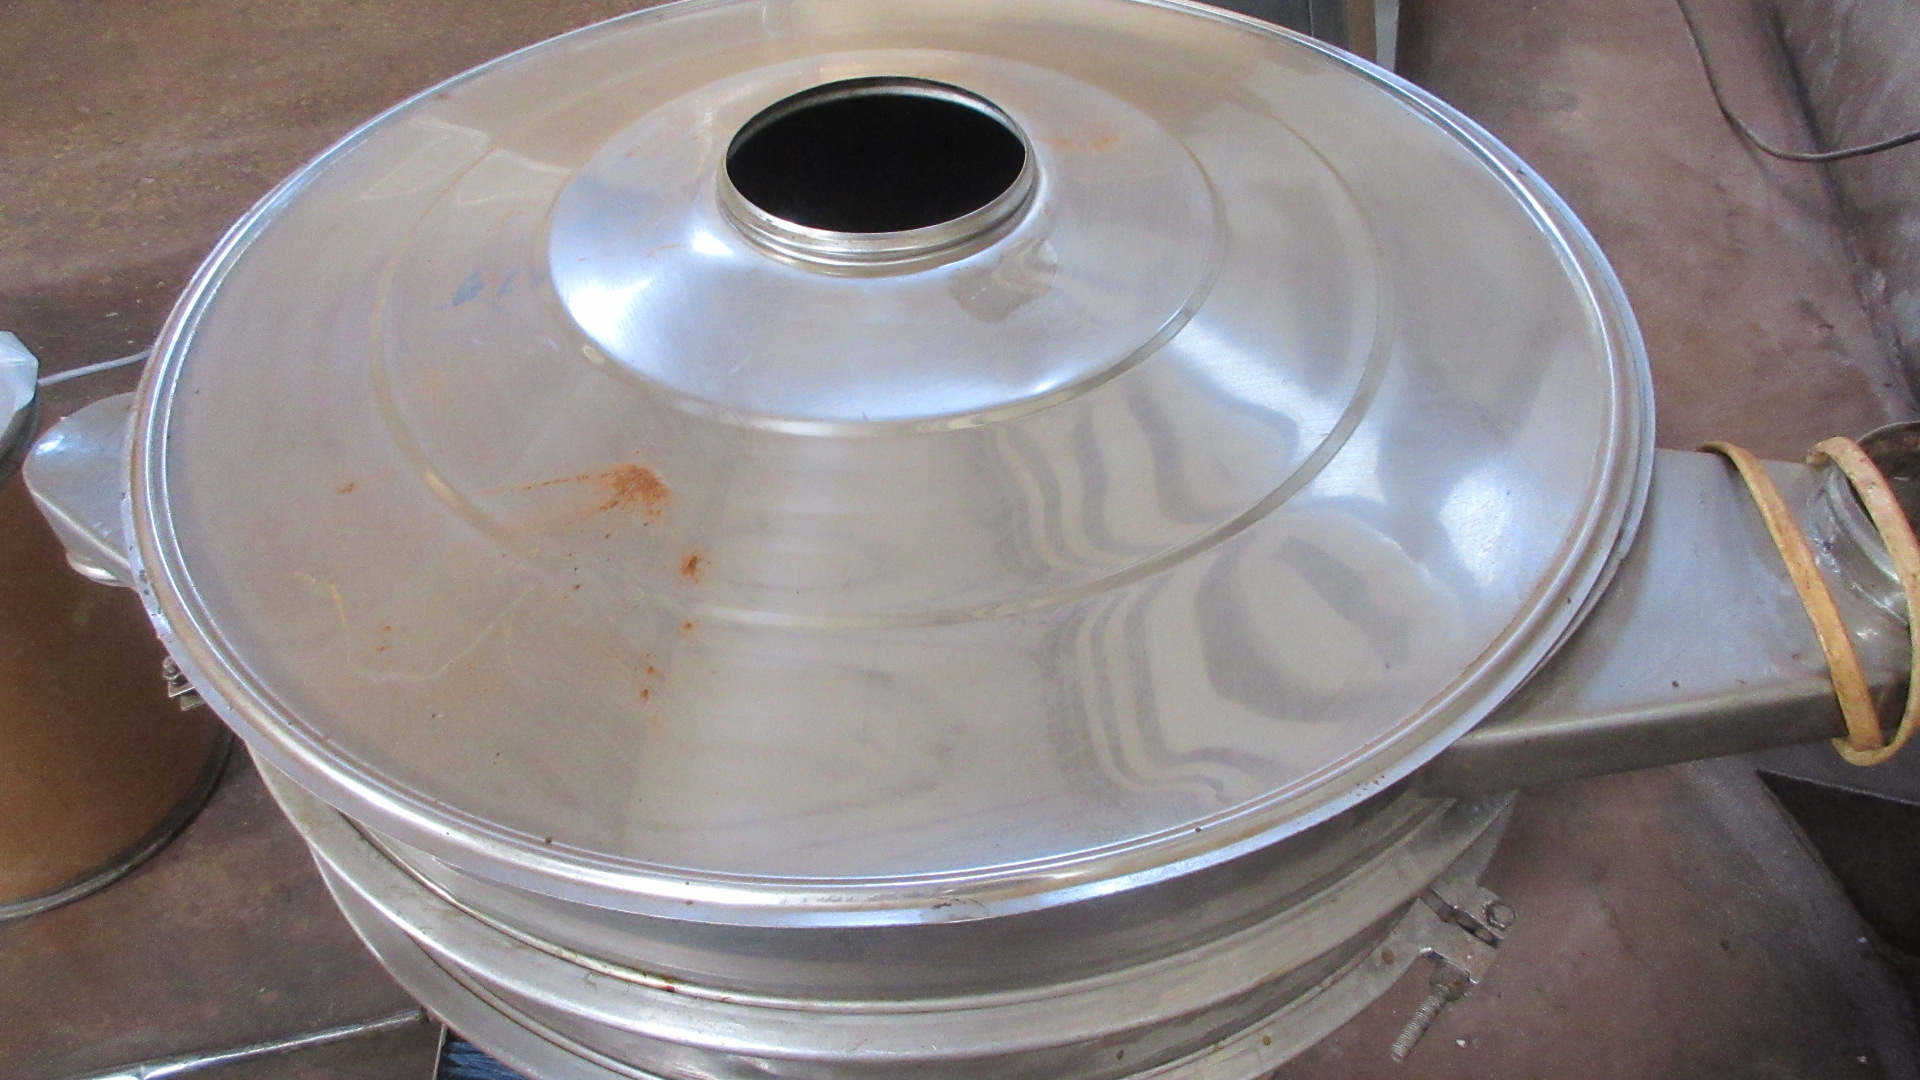
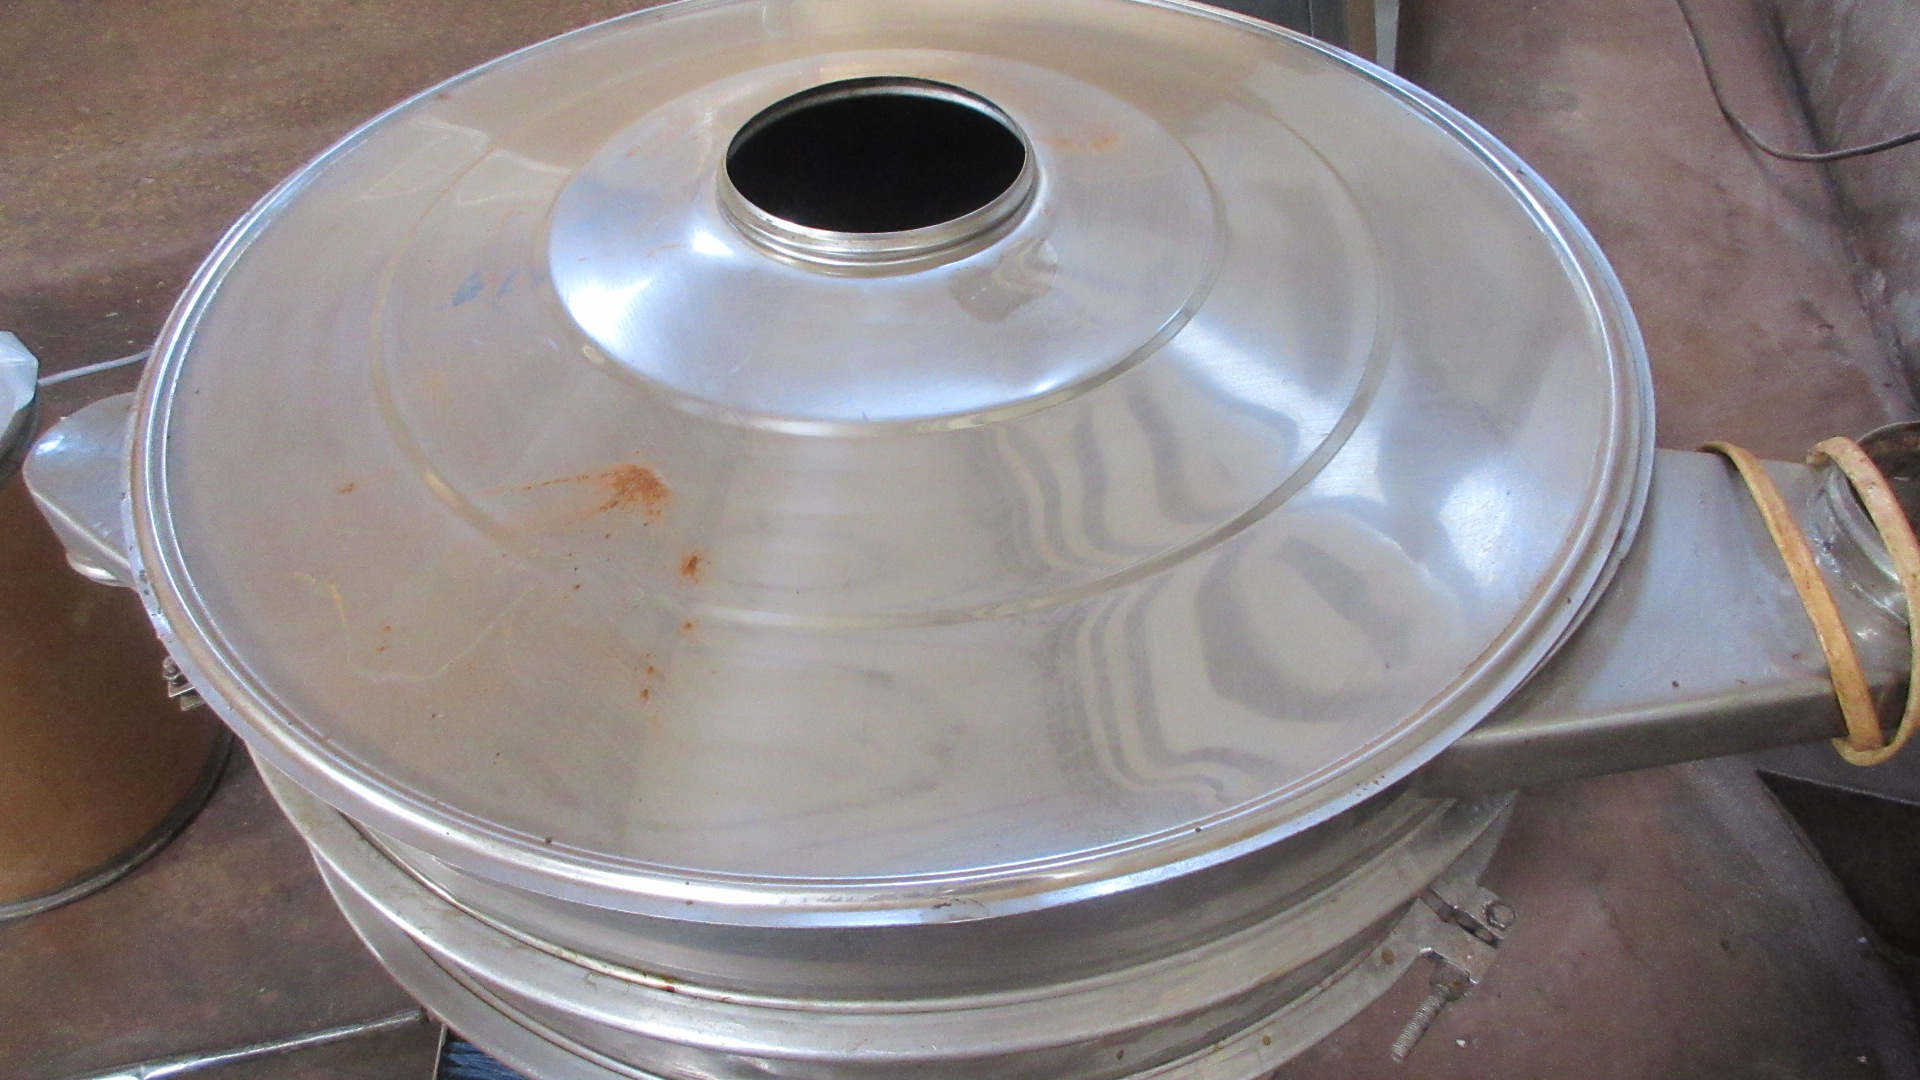
Vibratory grading screens separate powders from 80 up to 450 mesh, integrated with high-sensitivity rare-earth magnetic traps and inline metal detectors.
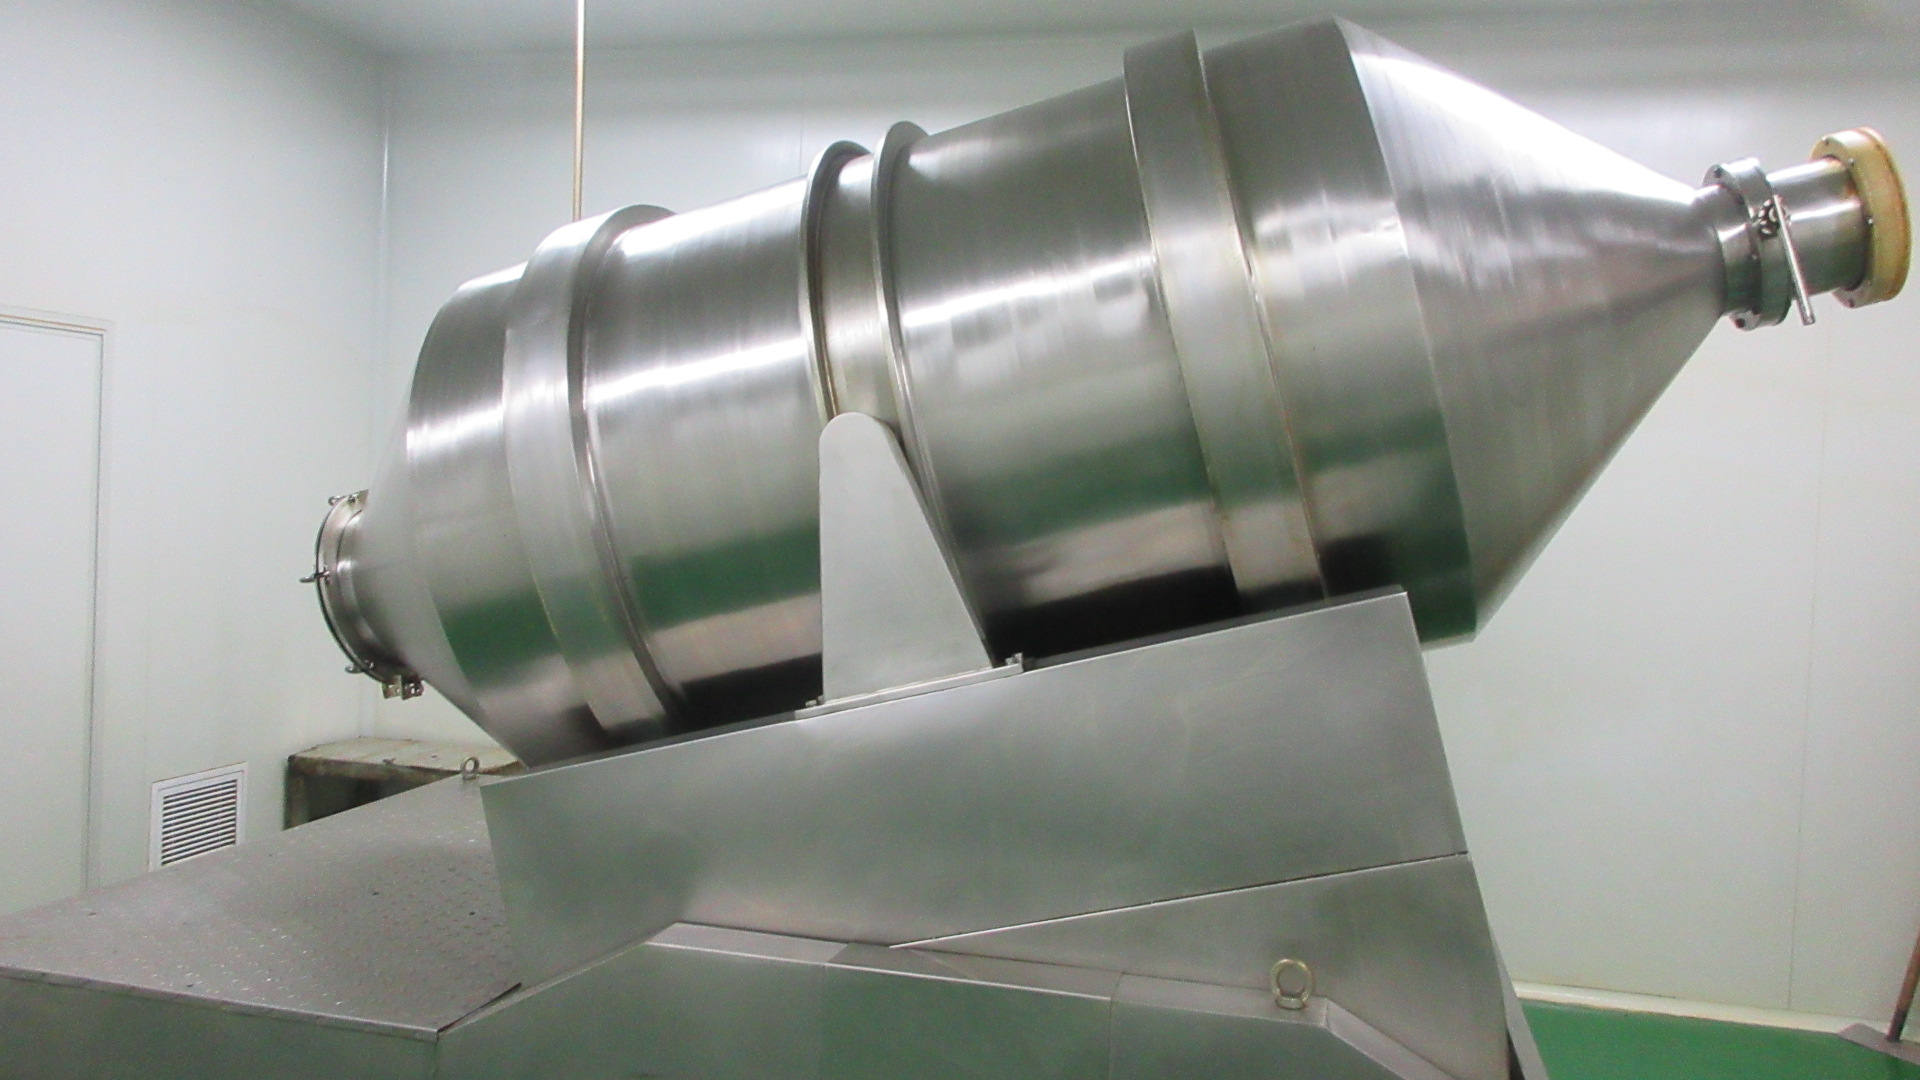
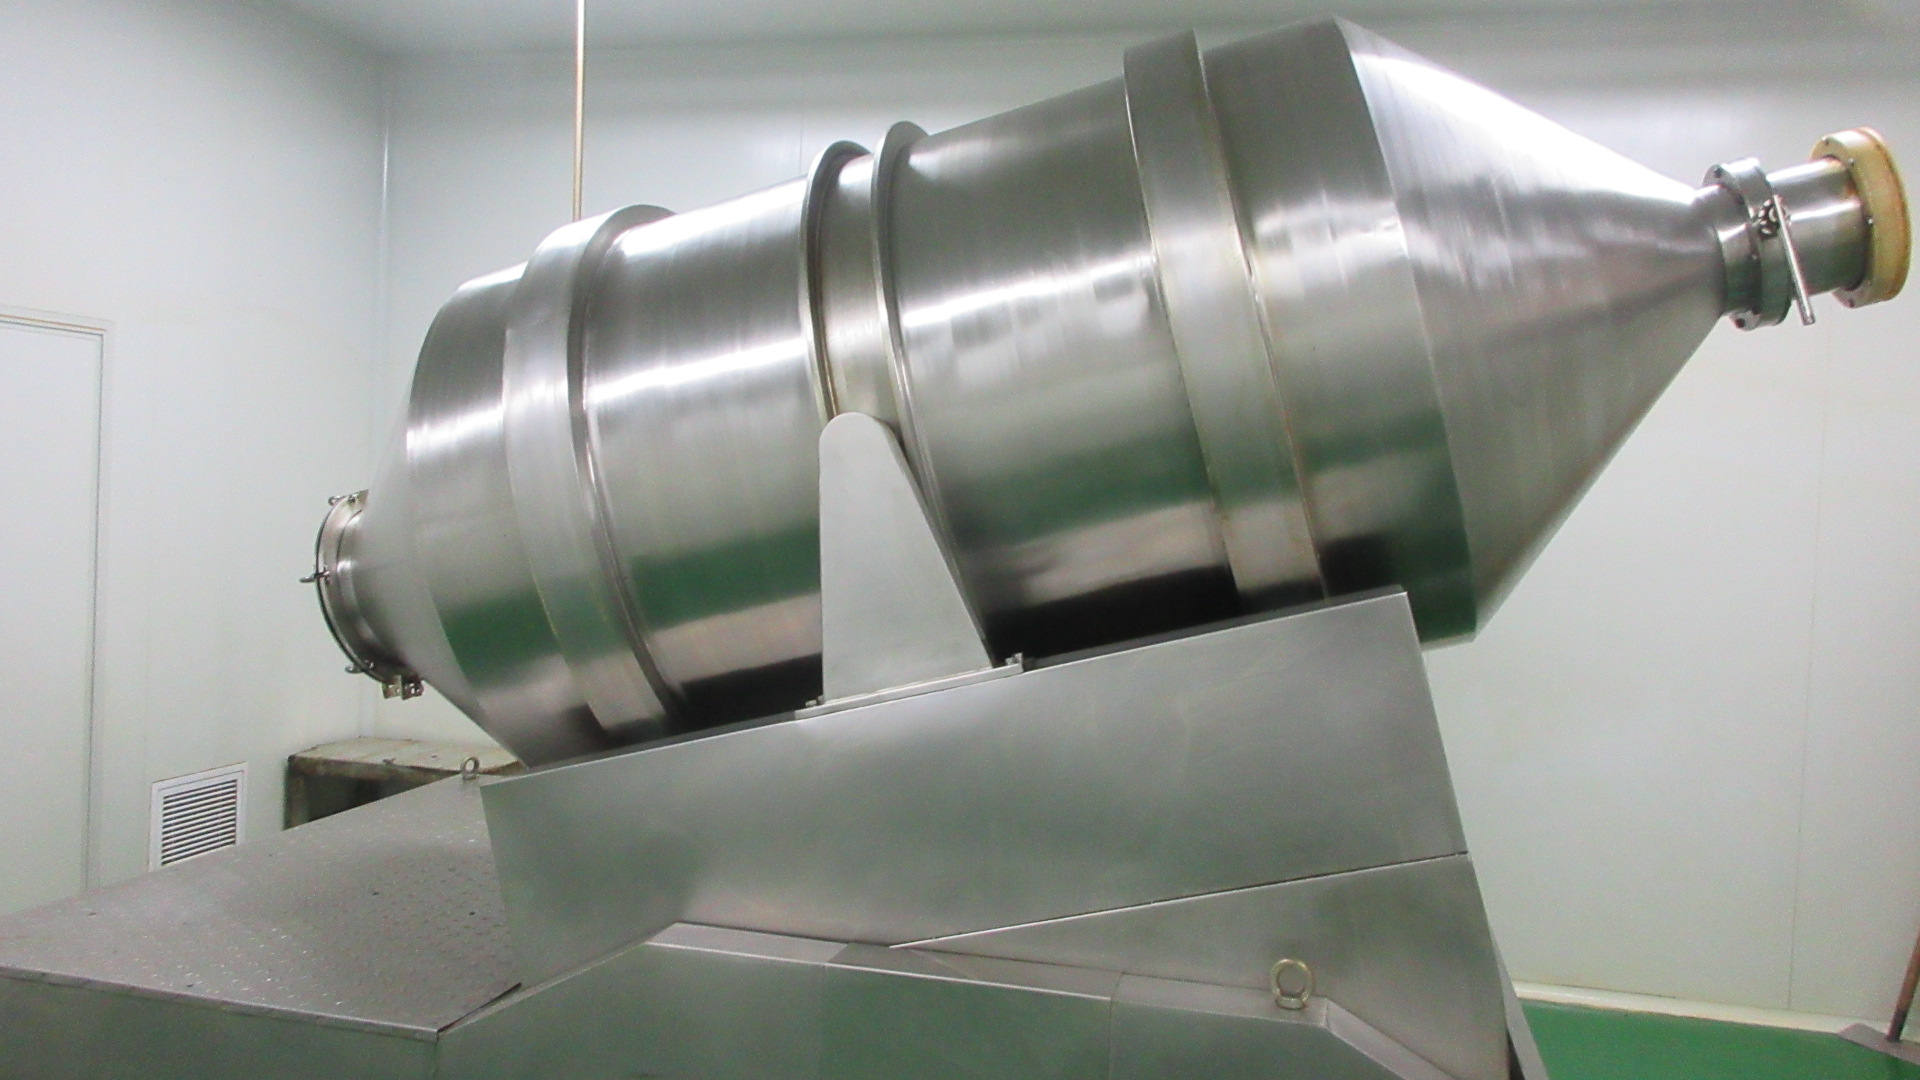
Three-dimensional cone blenders ensure thorough homogeneity for custom active blends, carrier balances, and batch-to-batch color stabilization.
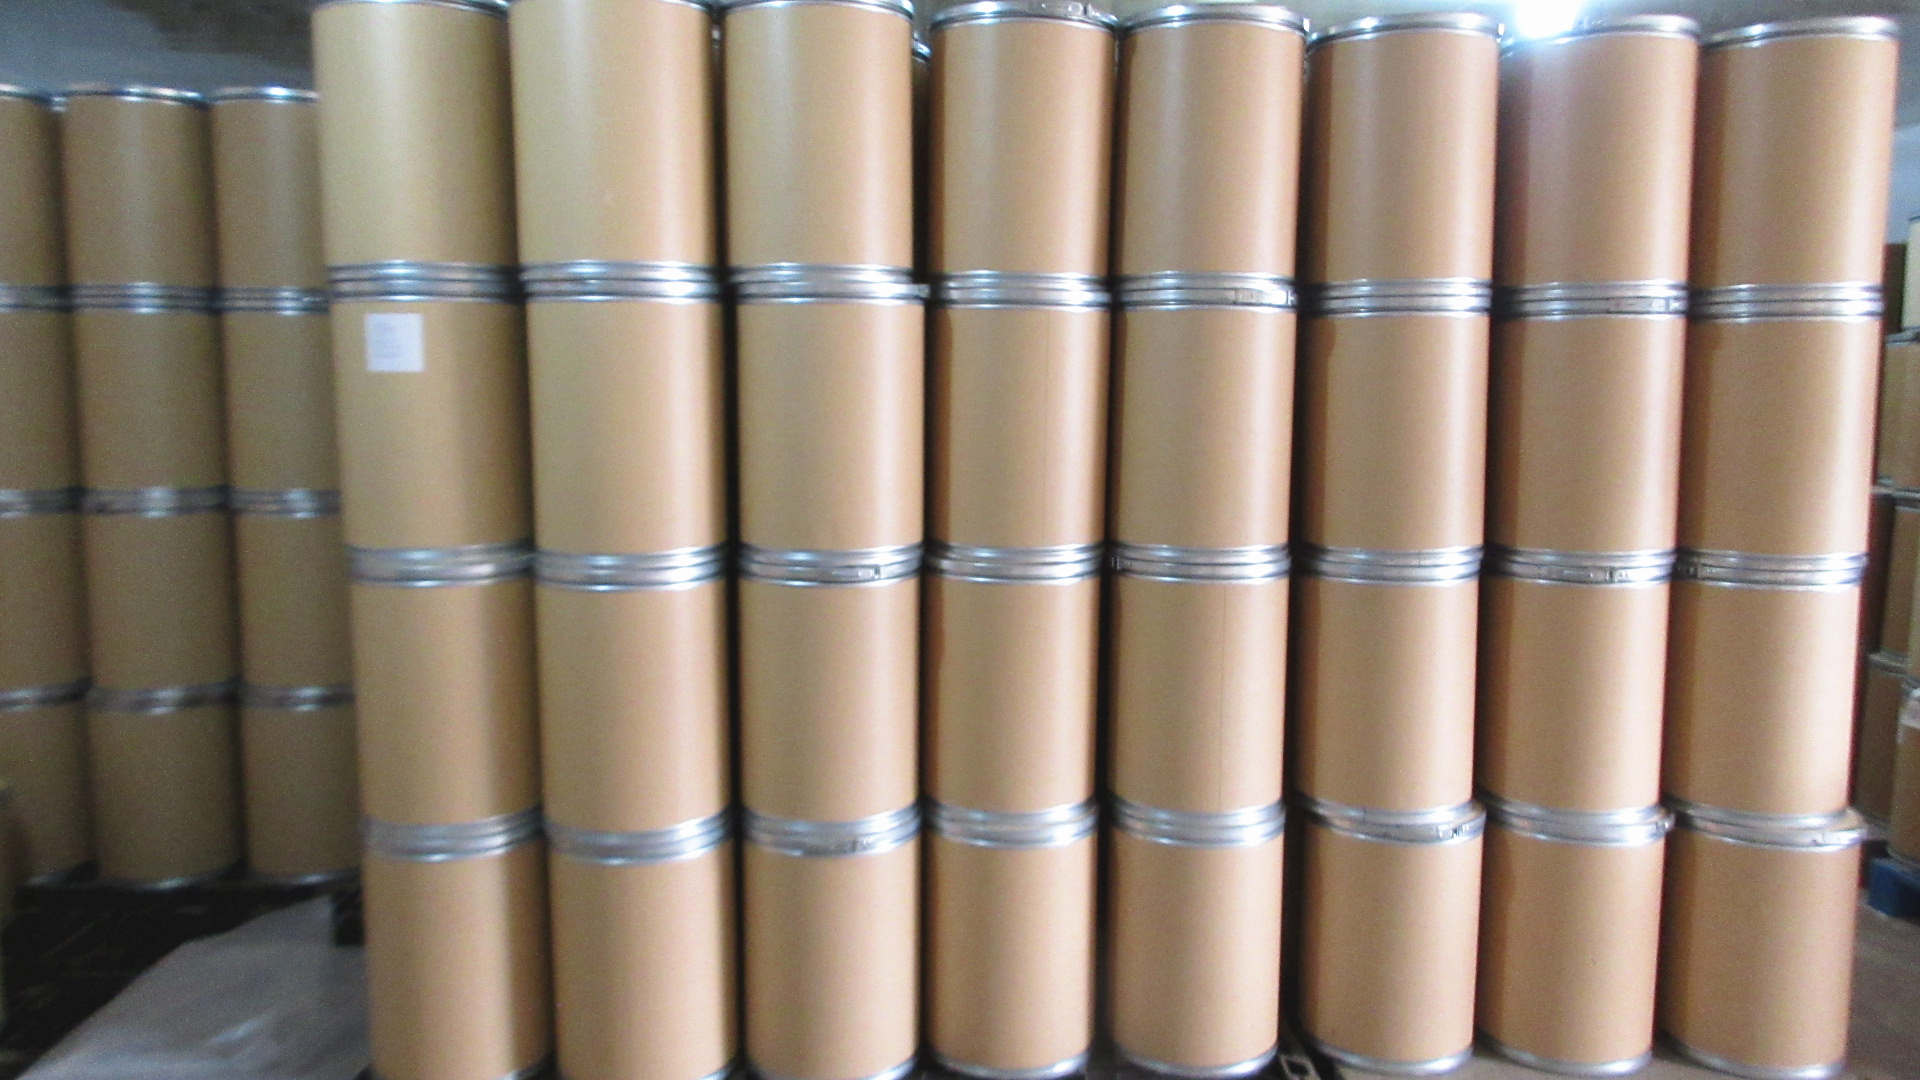
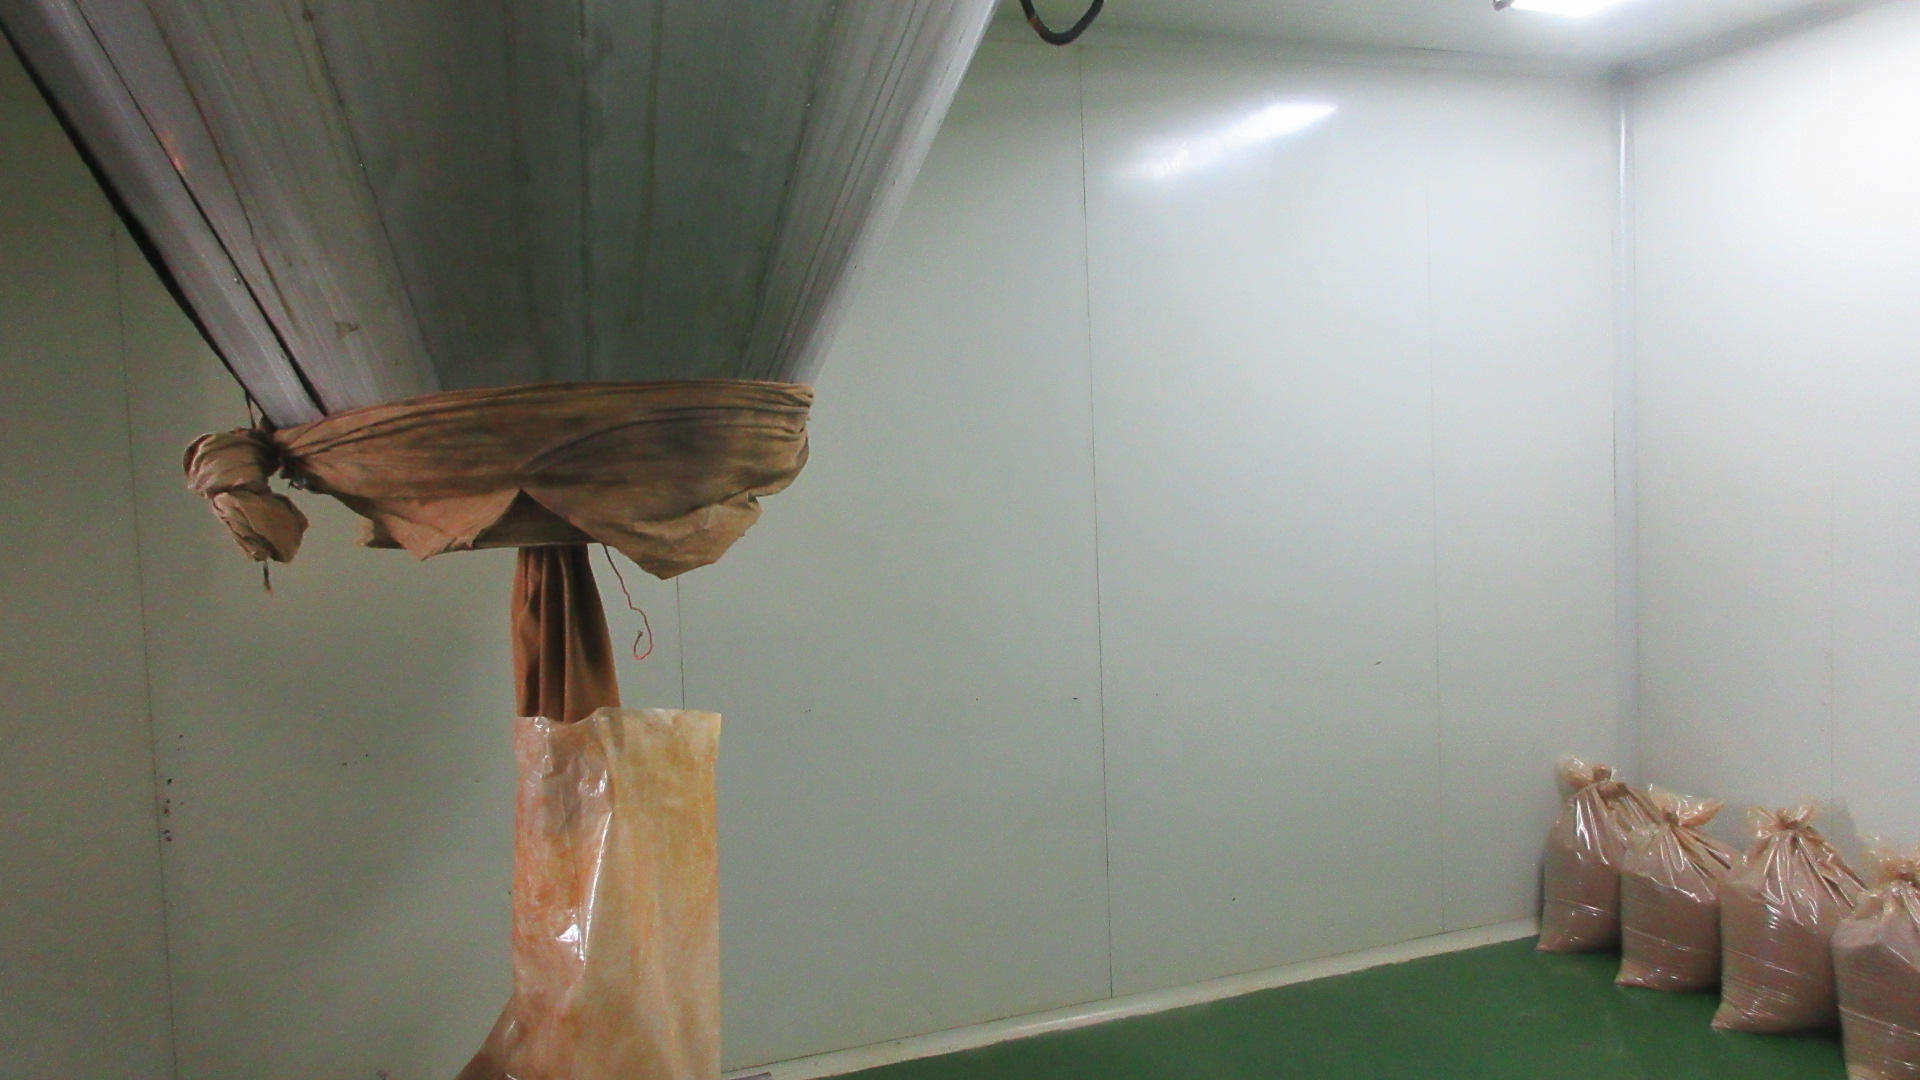
Sealed inside pharmaceutical-grade aseptic cleanrooms into food-grade polyethylene bags within tamper-evident drums, accompanied by a batch-specific COA.
Built with 304/316L stainless steel, automated CIP (clean-in-place) loops, and digital telemetry to guarantee clean-label integrity.
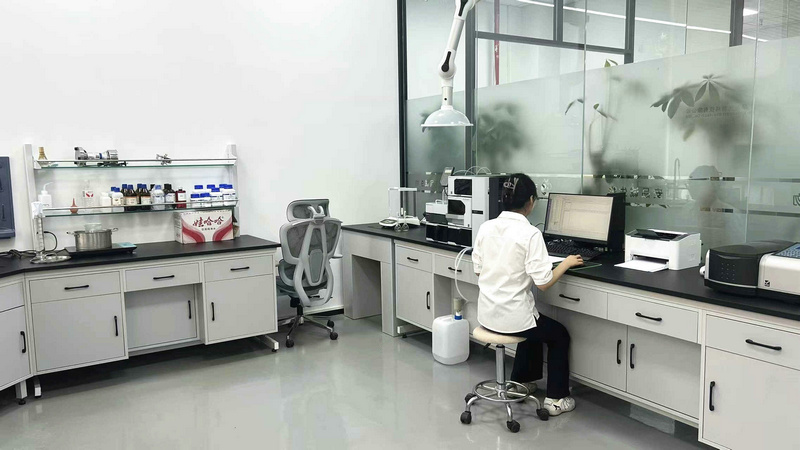
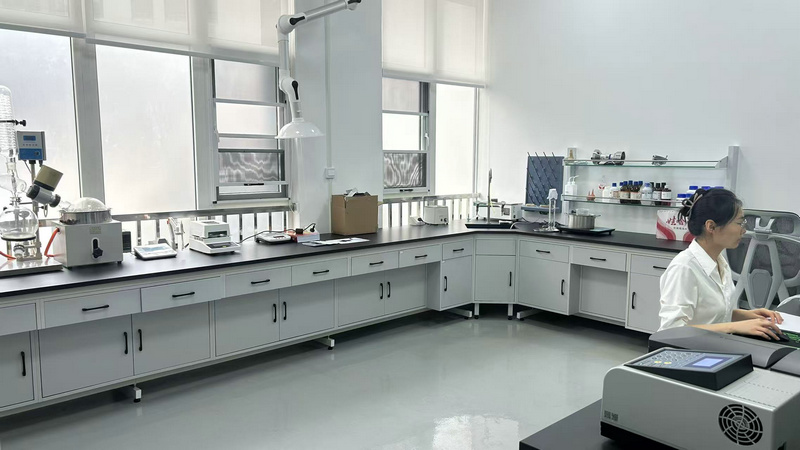
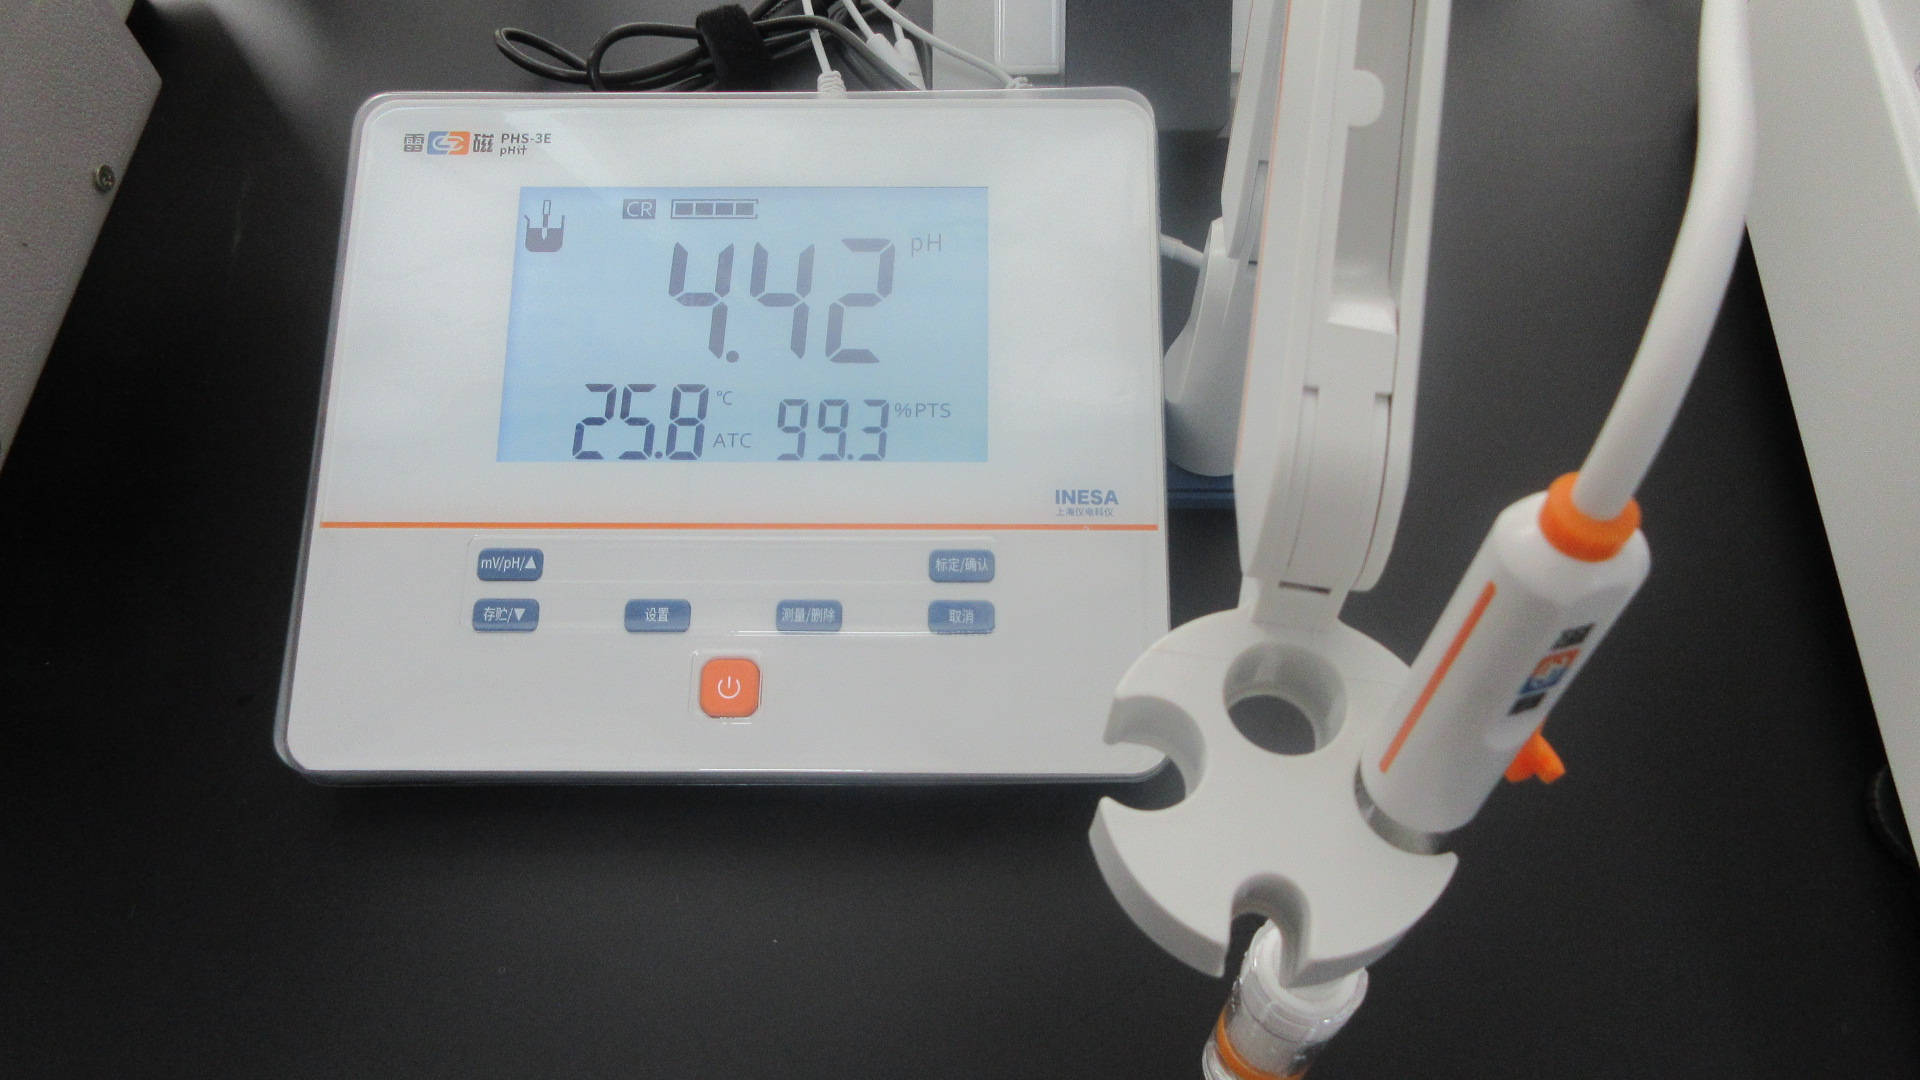
At Xi'an Vexli Bio-Tech Co., Ltd., full chemical assay and microbial safety validation occur on-site before third-party SGS or Eurofins audits, ensuring complete regulatory compliance in destination markets.
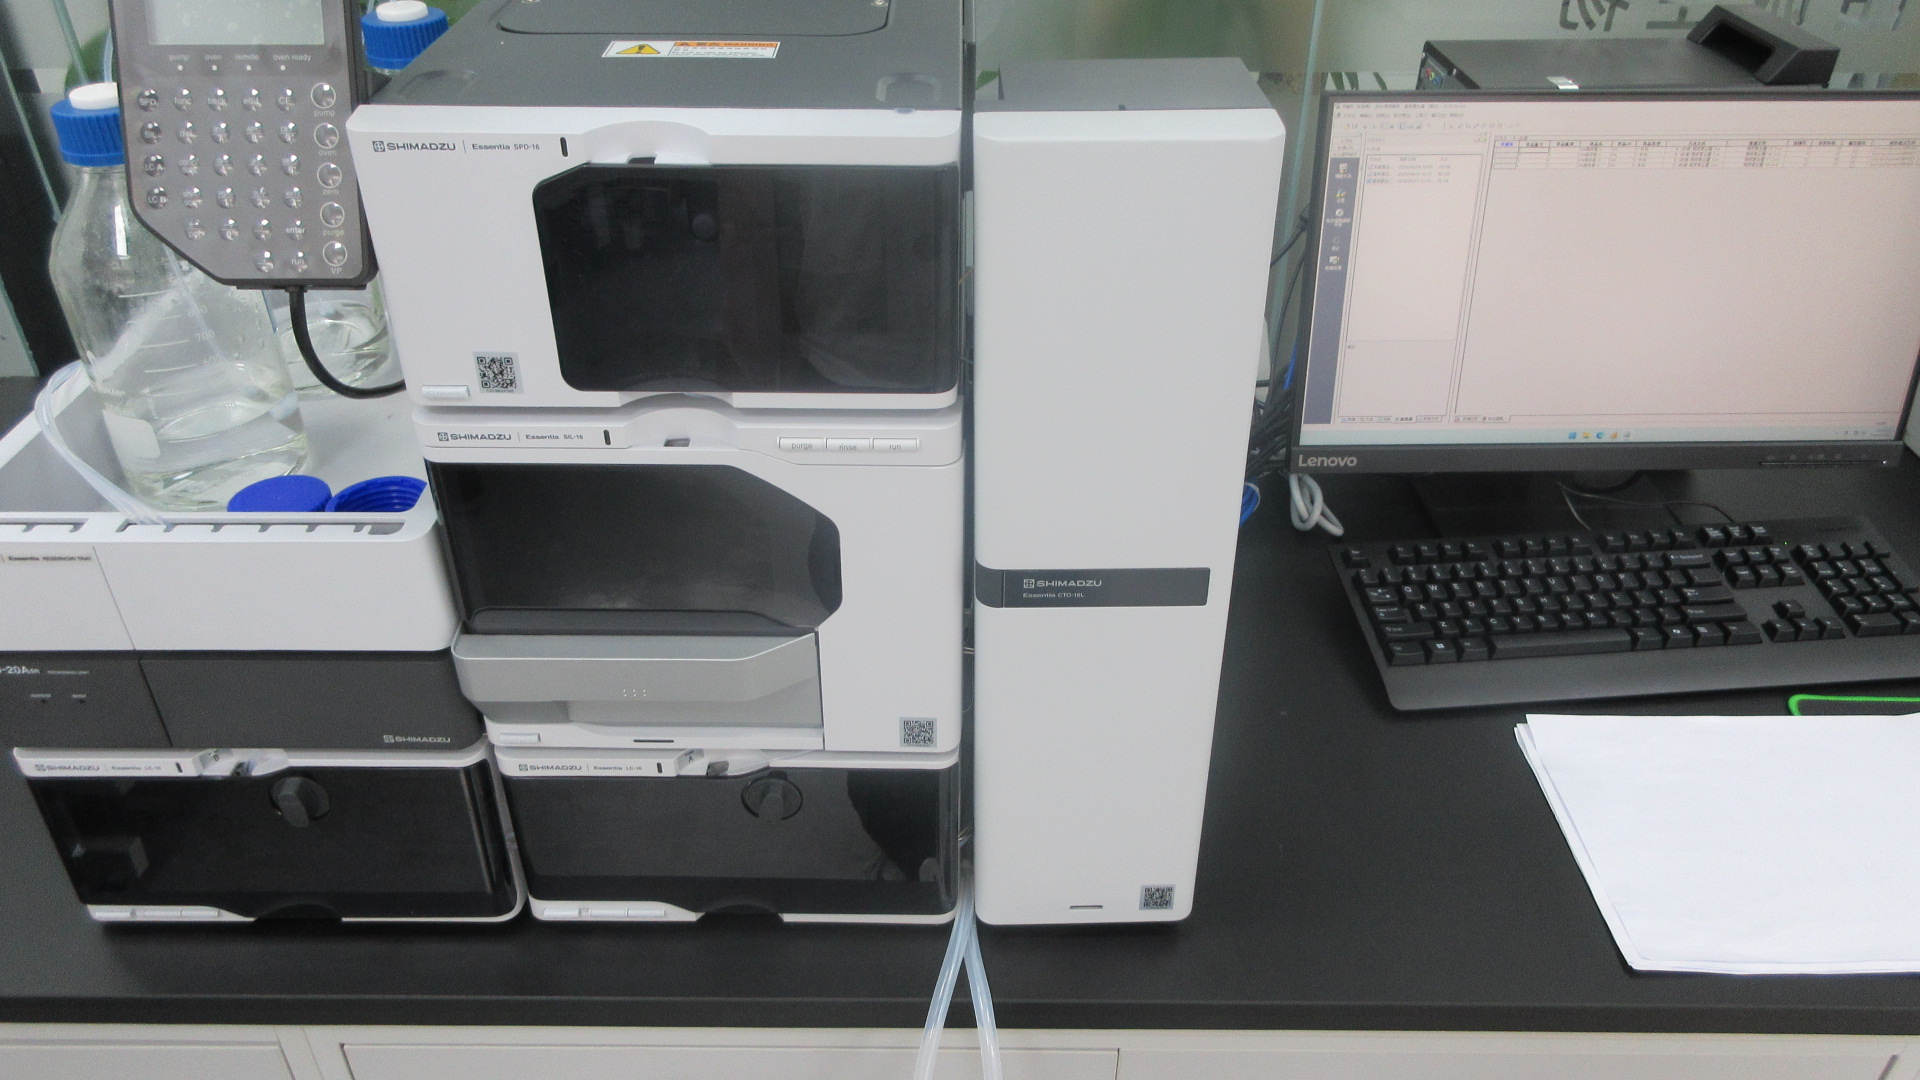
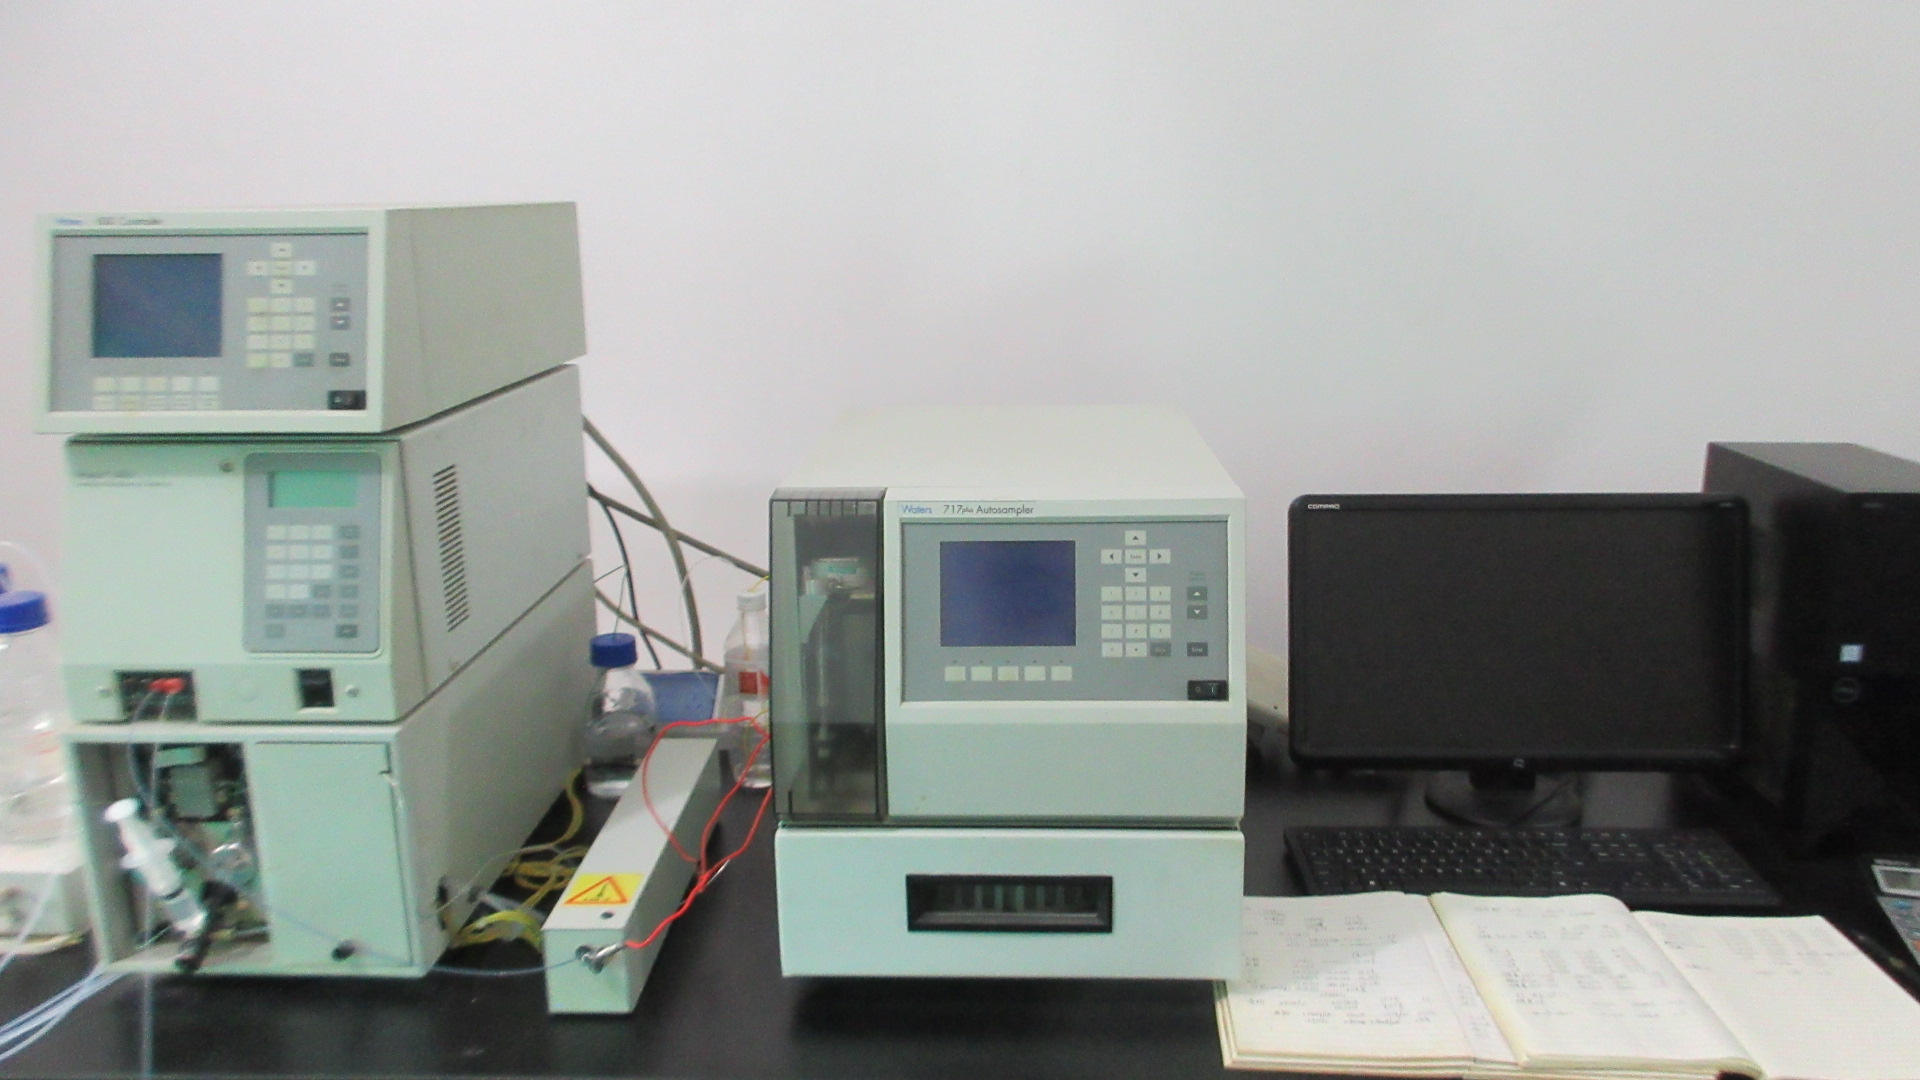
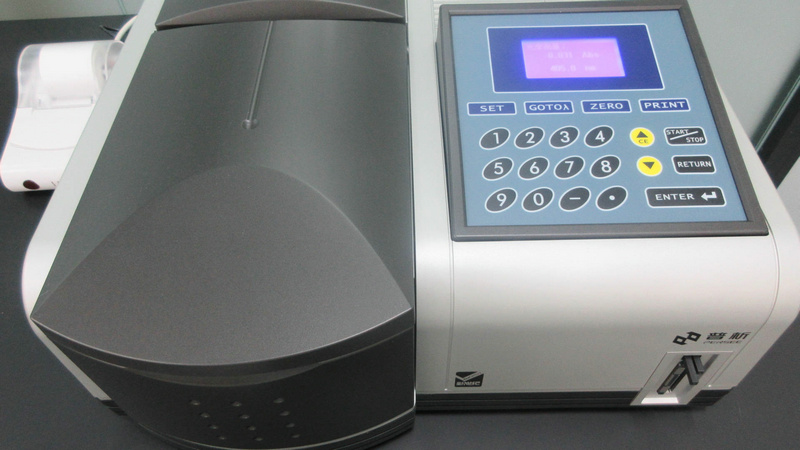
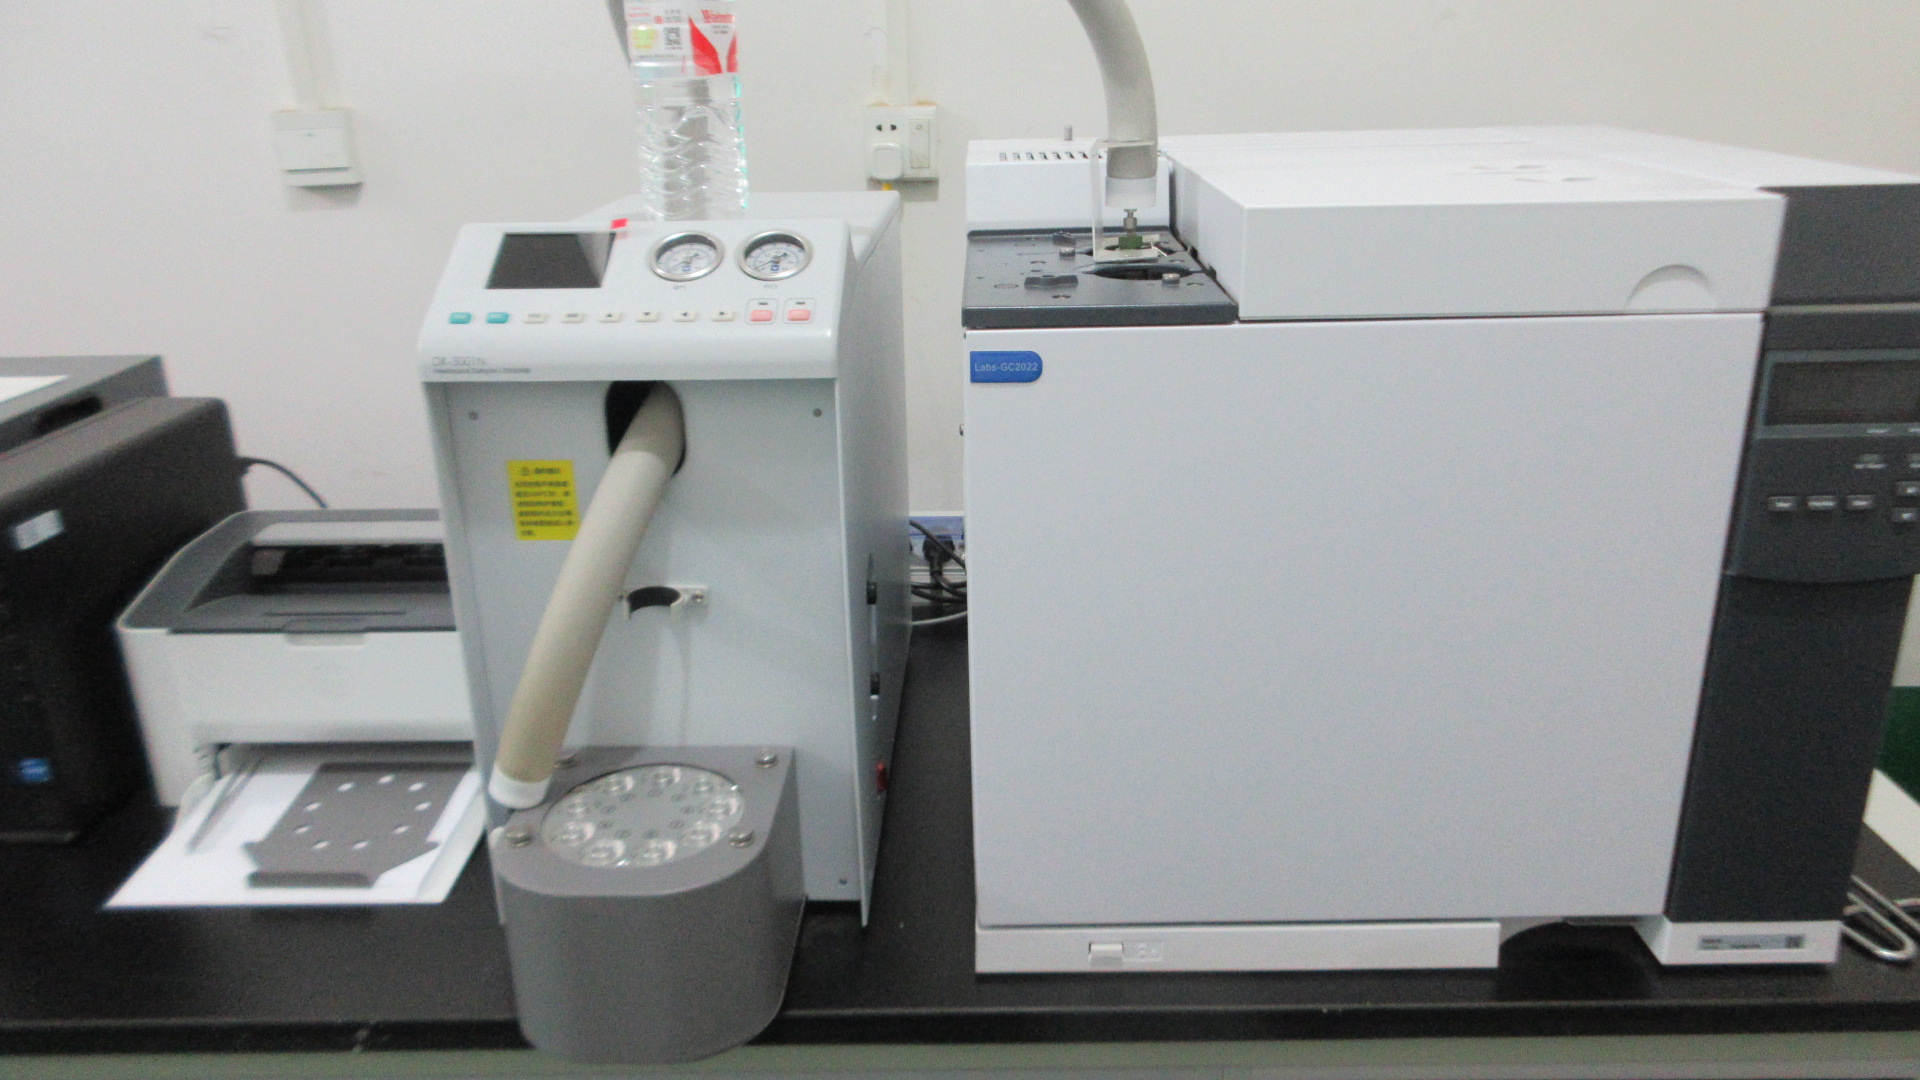
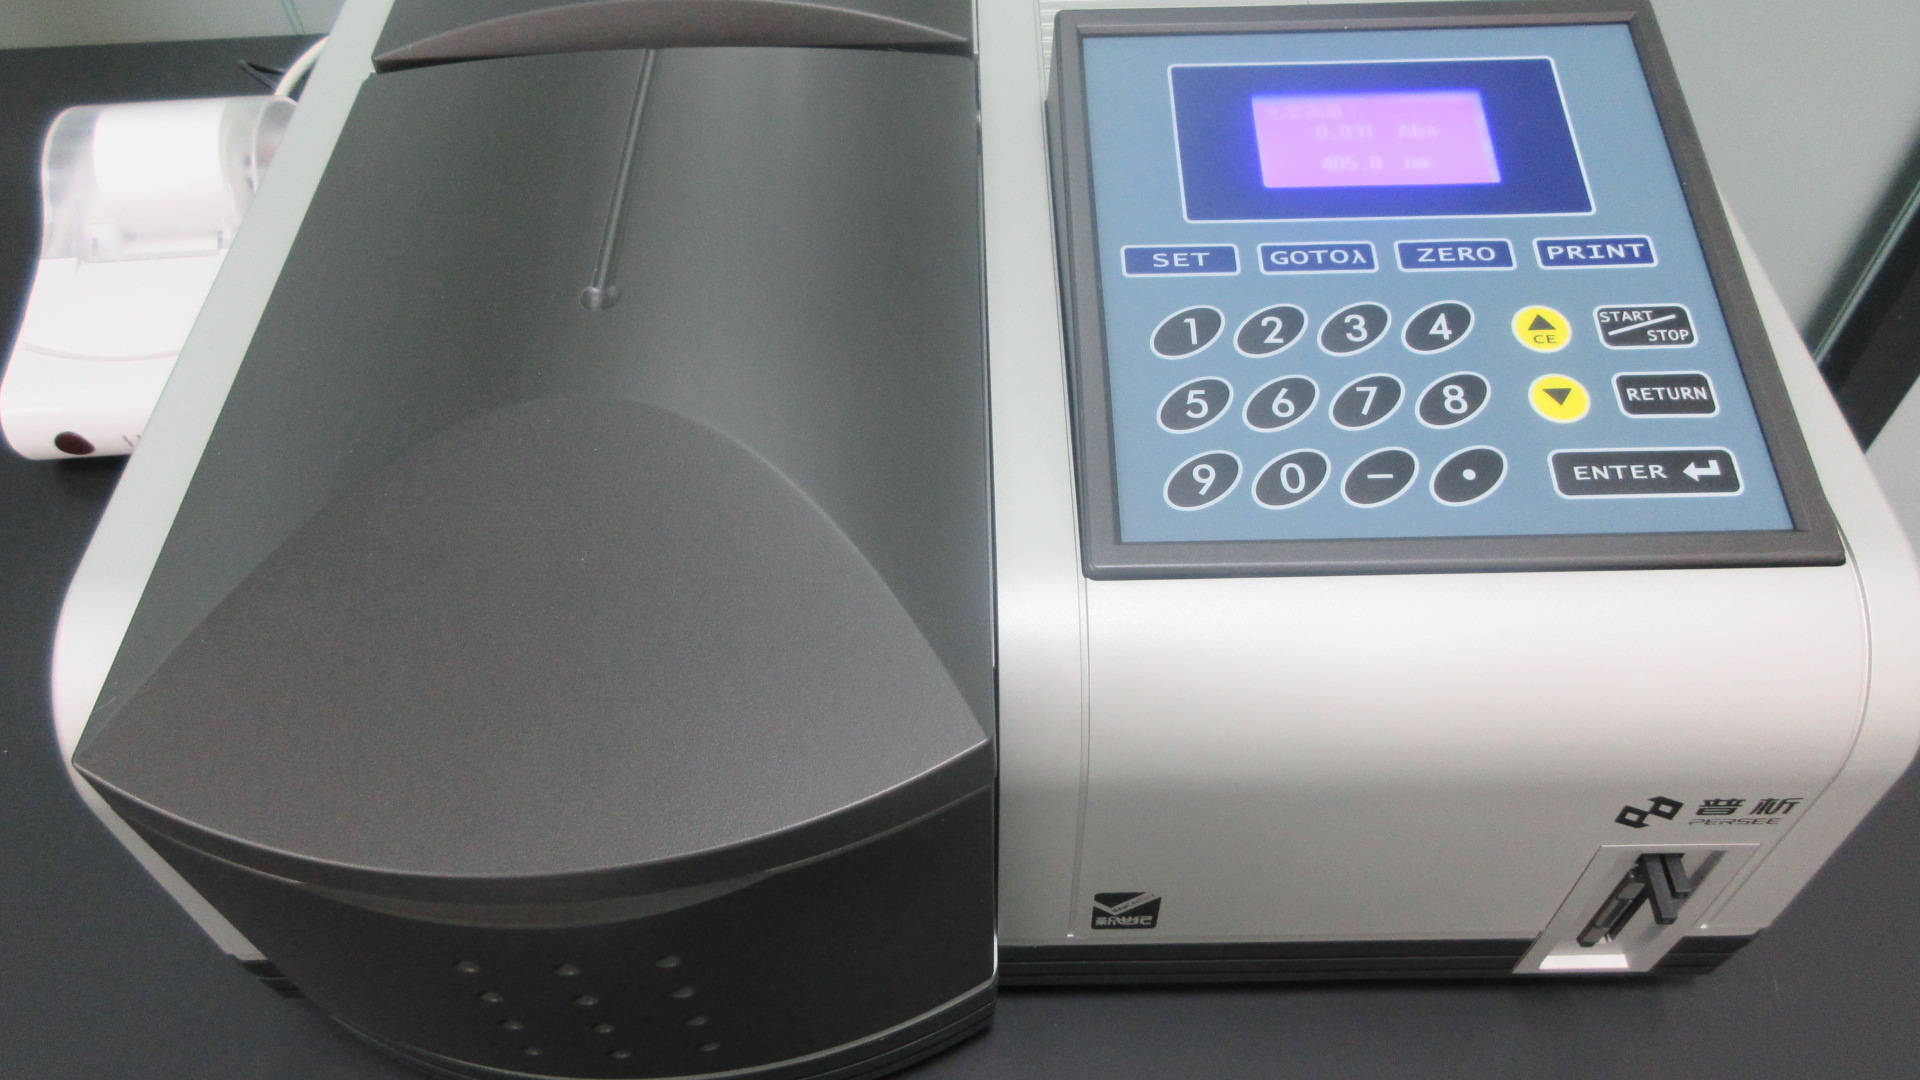
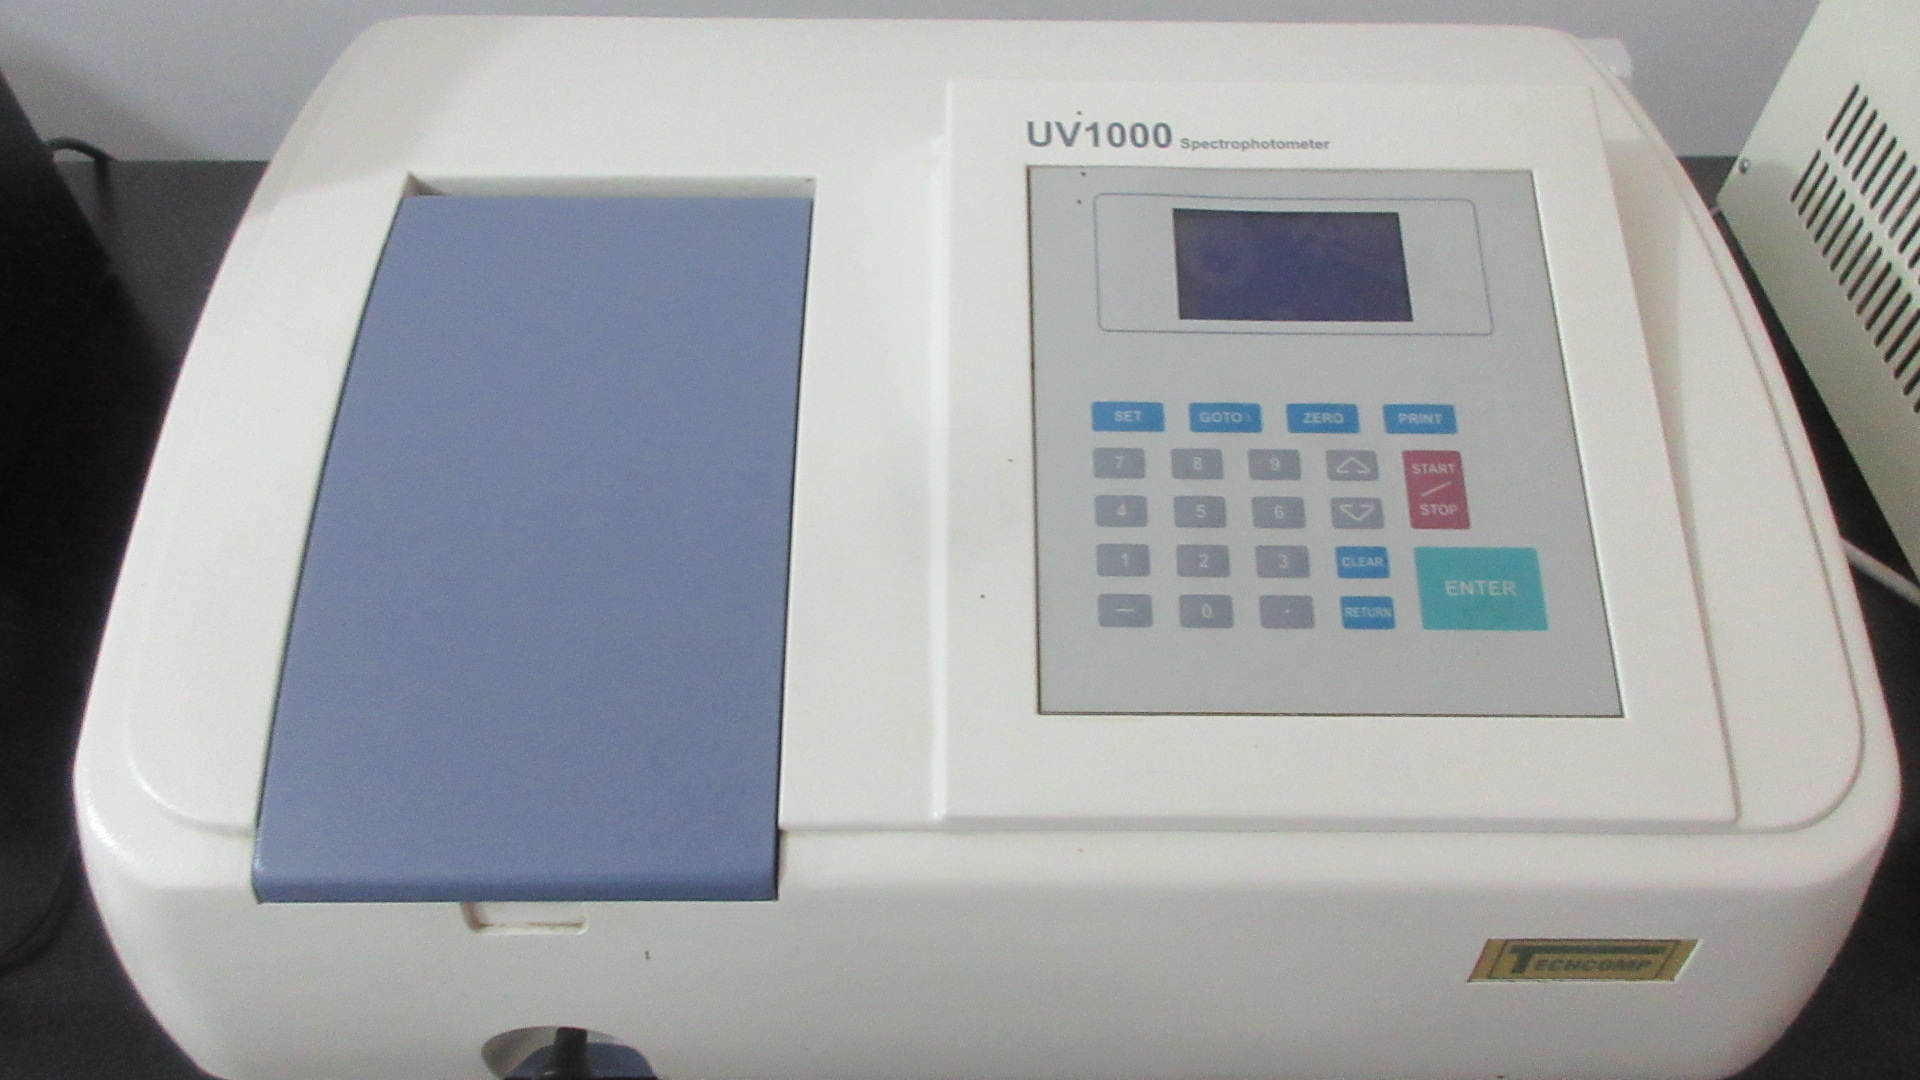
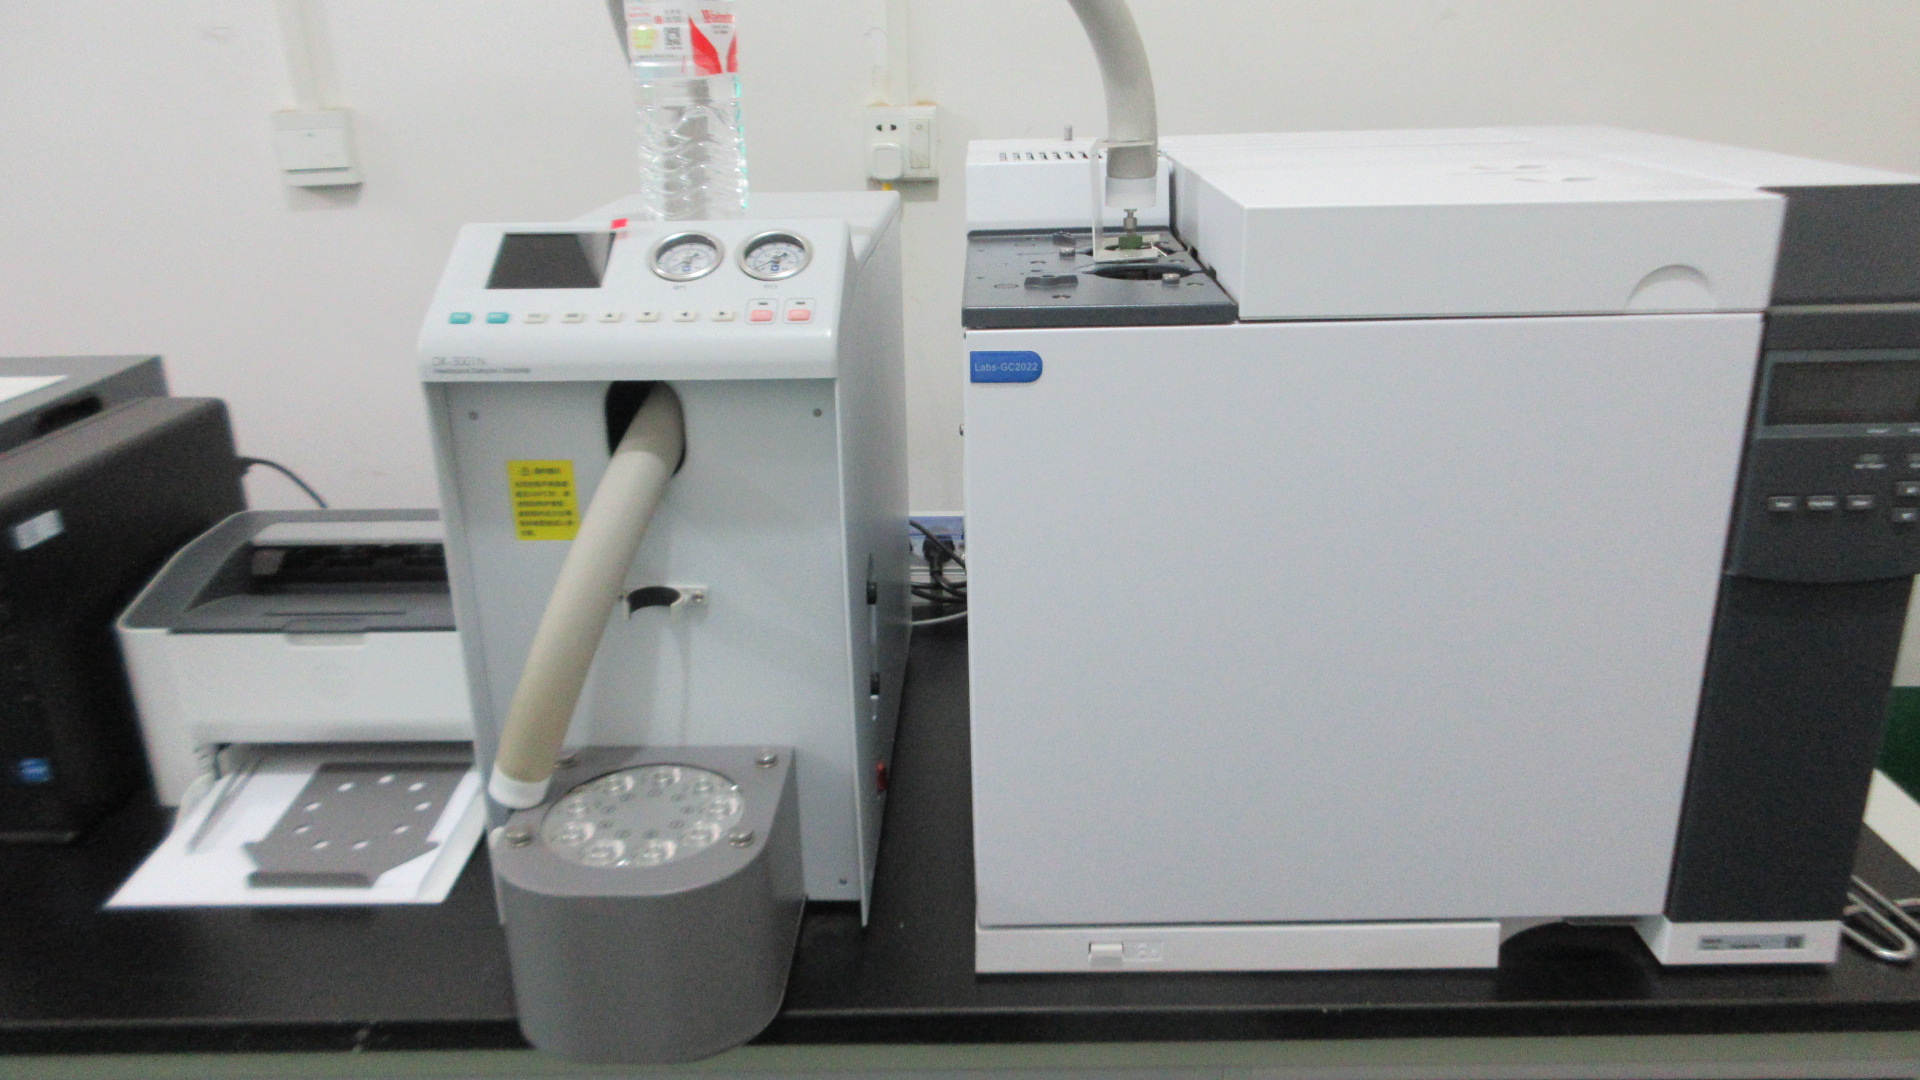
Quantitative chromatography (HPLC, GC) and spectrophotometry (UV-Vis) verify purity, active compound concentrations (e.g. NMN, NAD+, Mogroside V, Polysaccharides), and absence of synthetic adulteration.
Rigid monitoring for residual solvents via Gas Chromatography, elemental heavy metals (Pb, As, Cd, Hg) via atomic absorption, and BS EN 15662 pesticide multi-residue compliance for EU & North American entry.
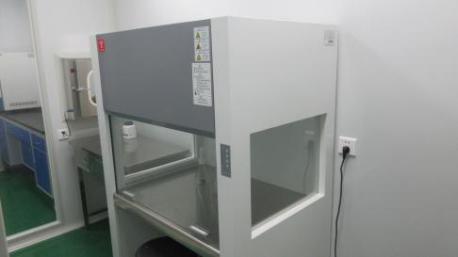
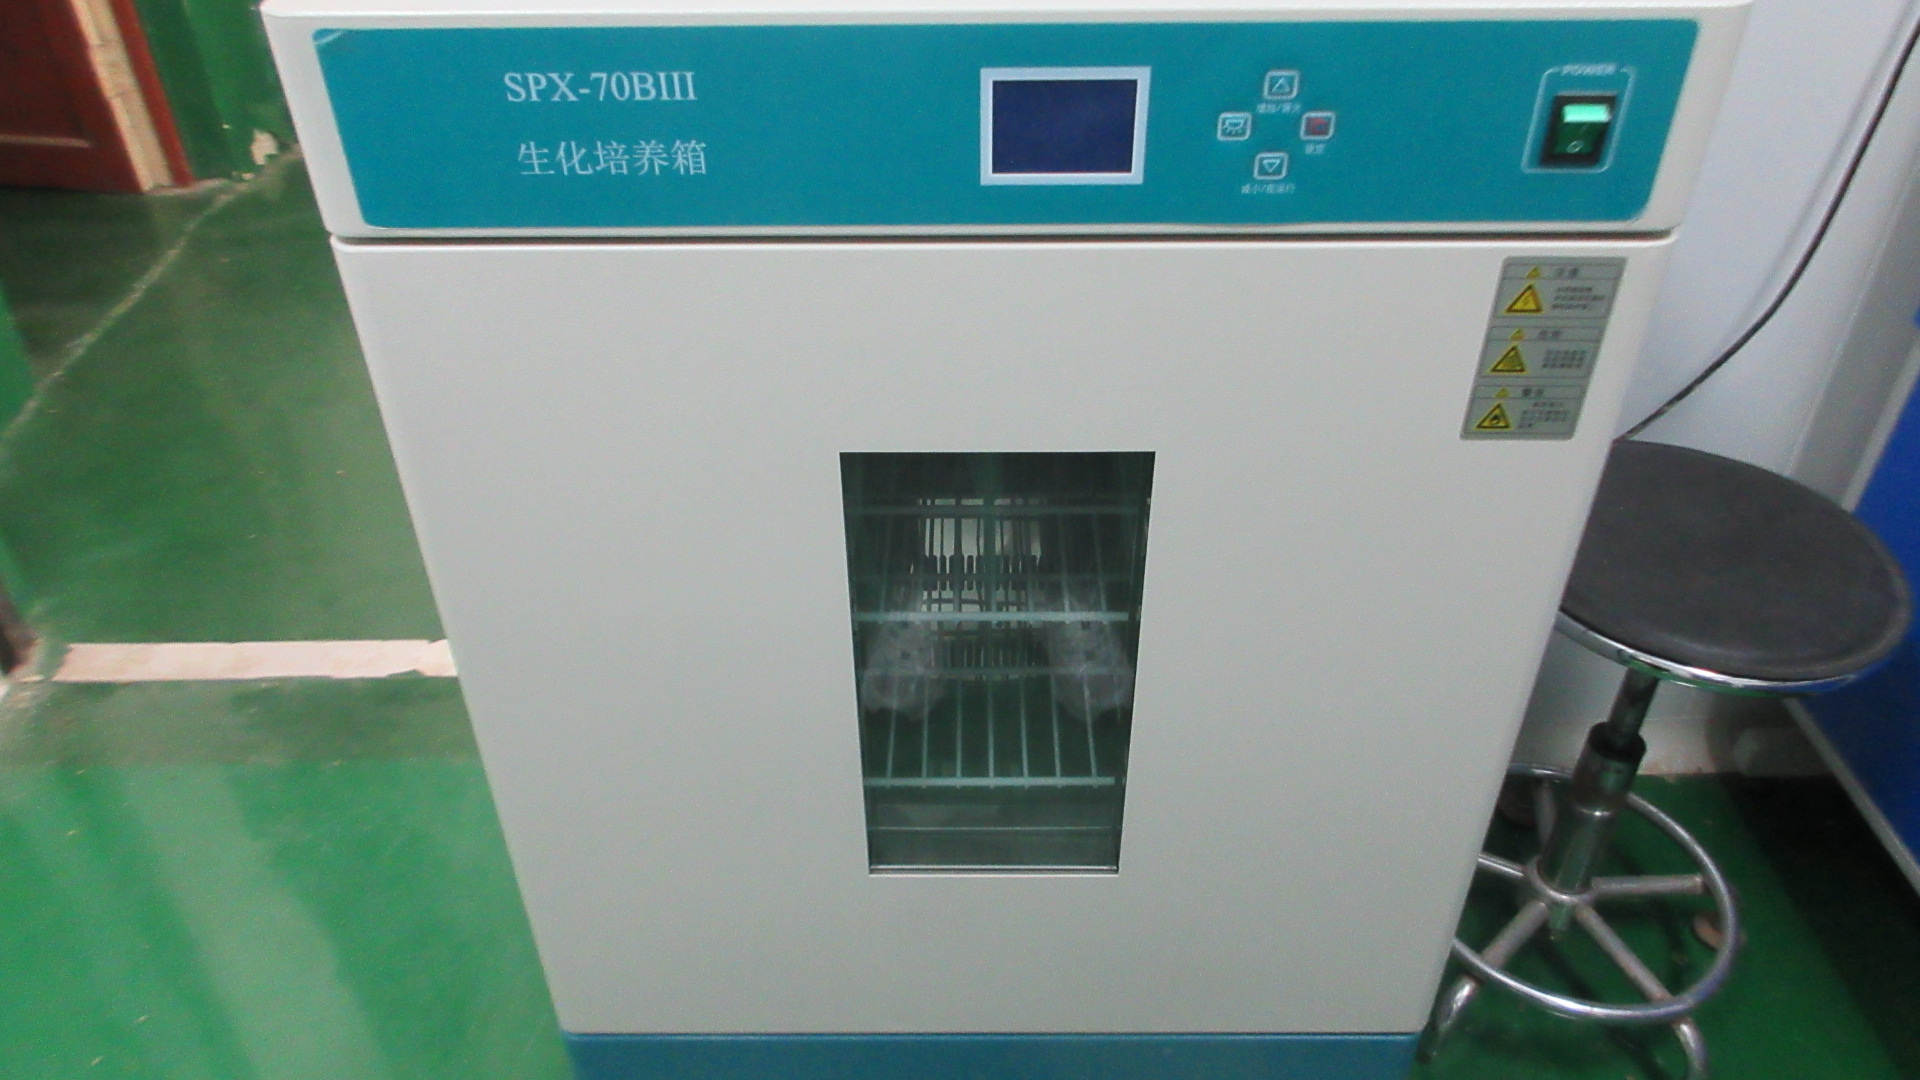
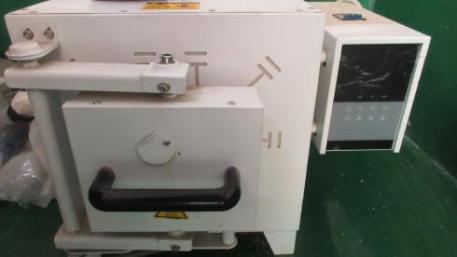
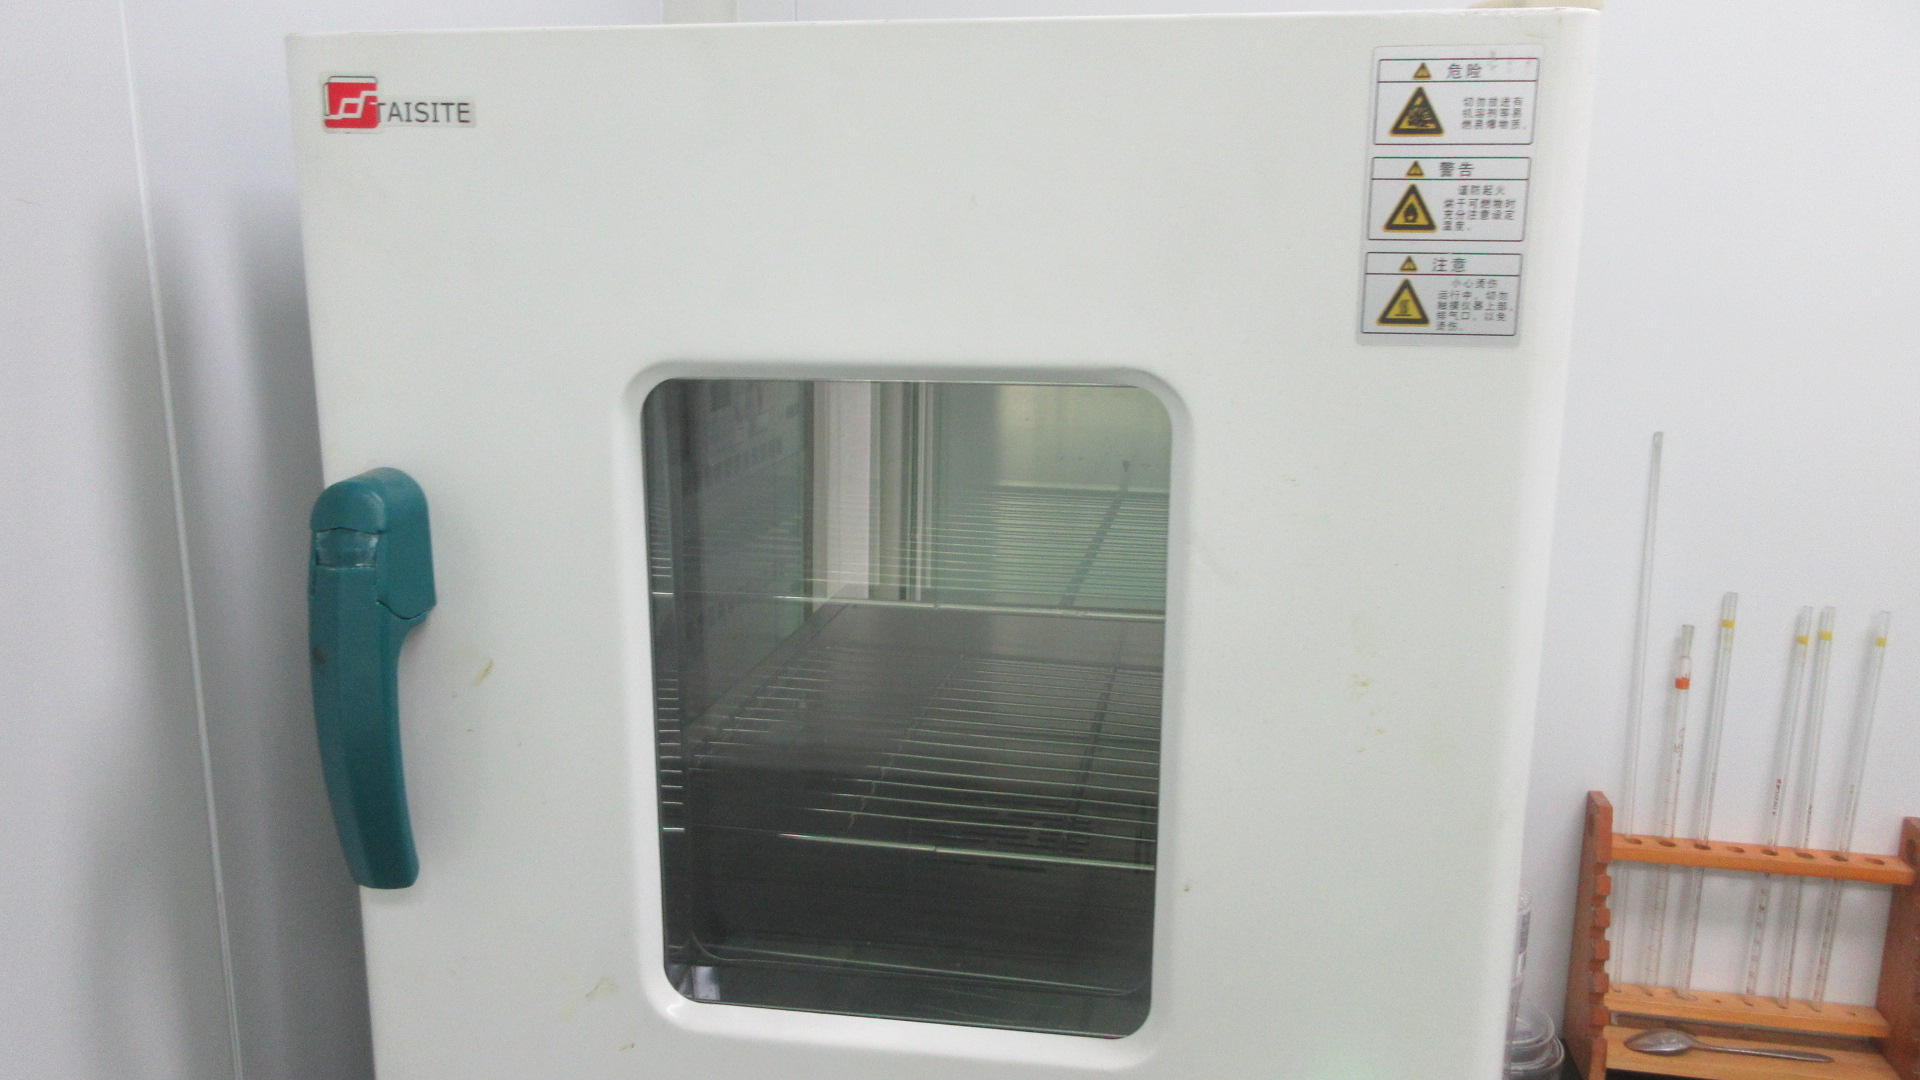
Class-100 clean benches and precision incubators rigorously test Total Plate Count (TPC), Yeast & Mold, and test pathogen-free status for E. coli and Salmonella on every manufactured lot.
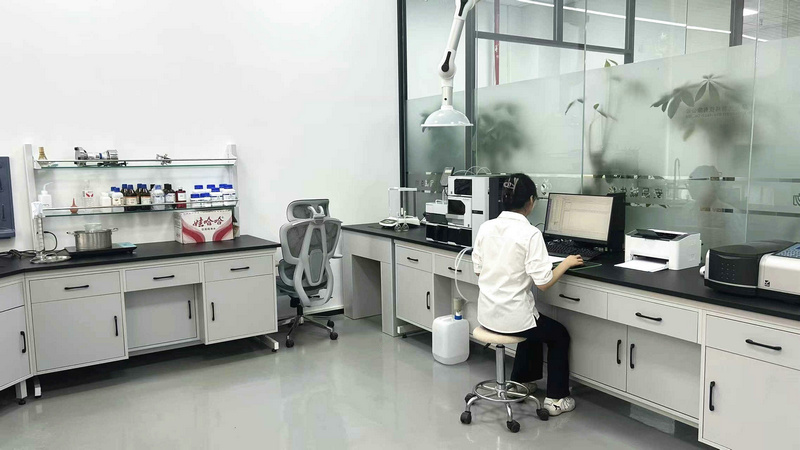
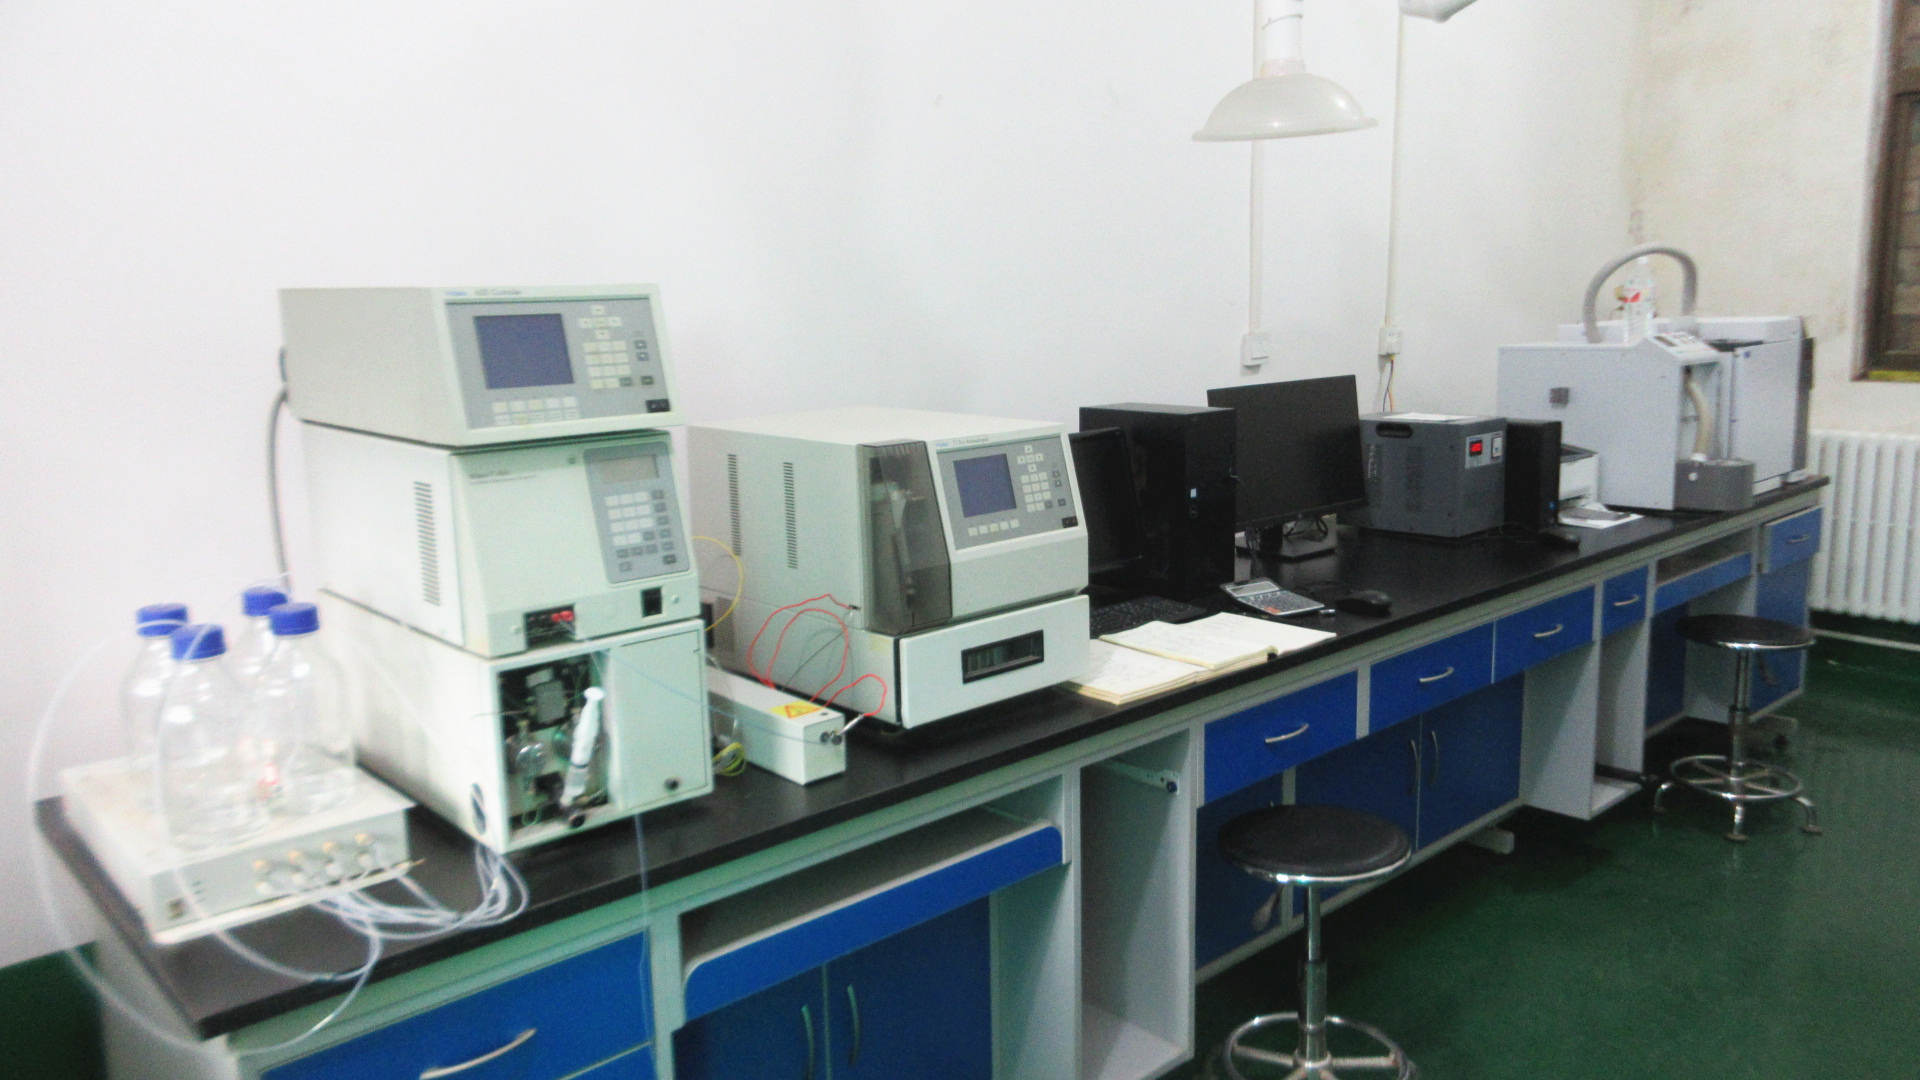
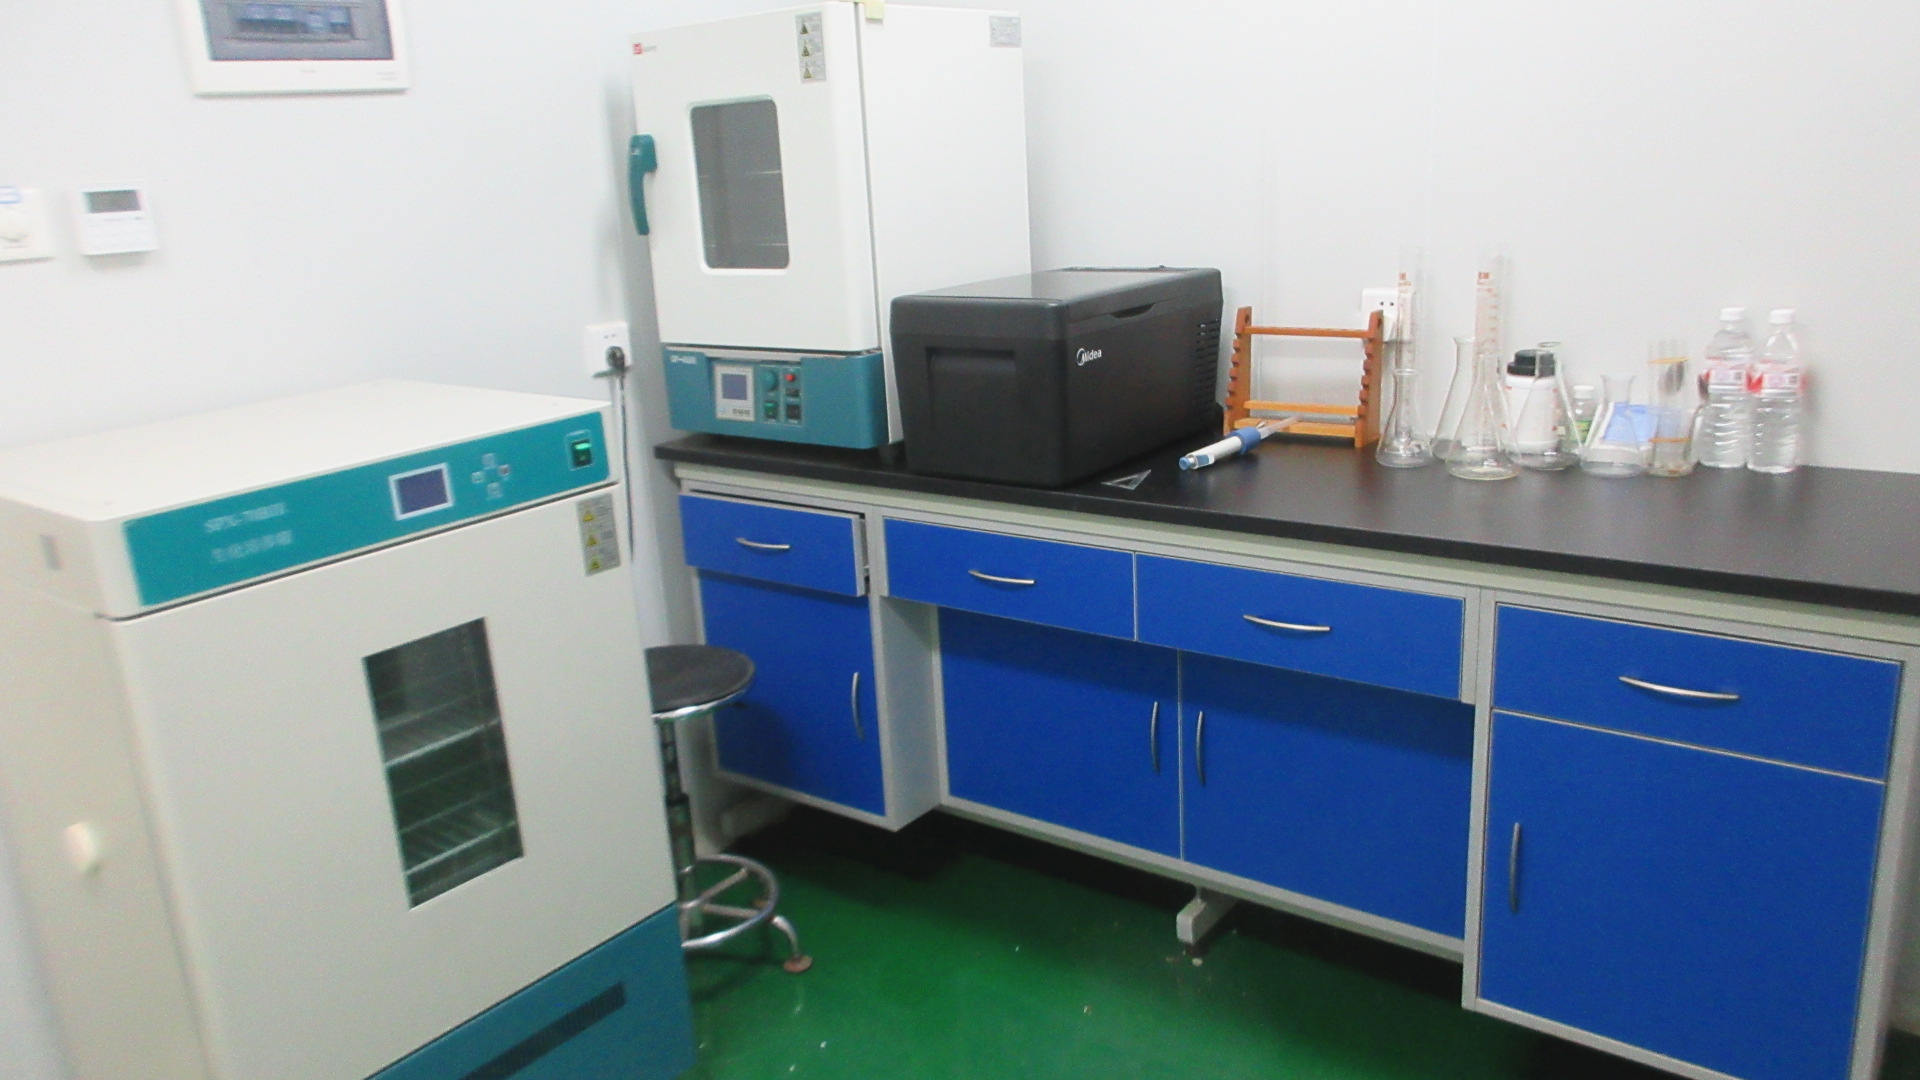
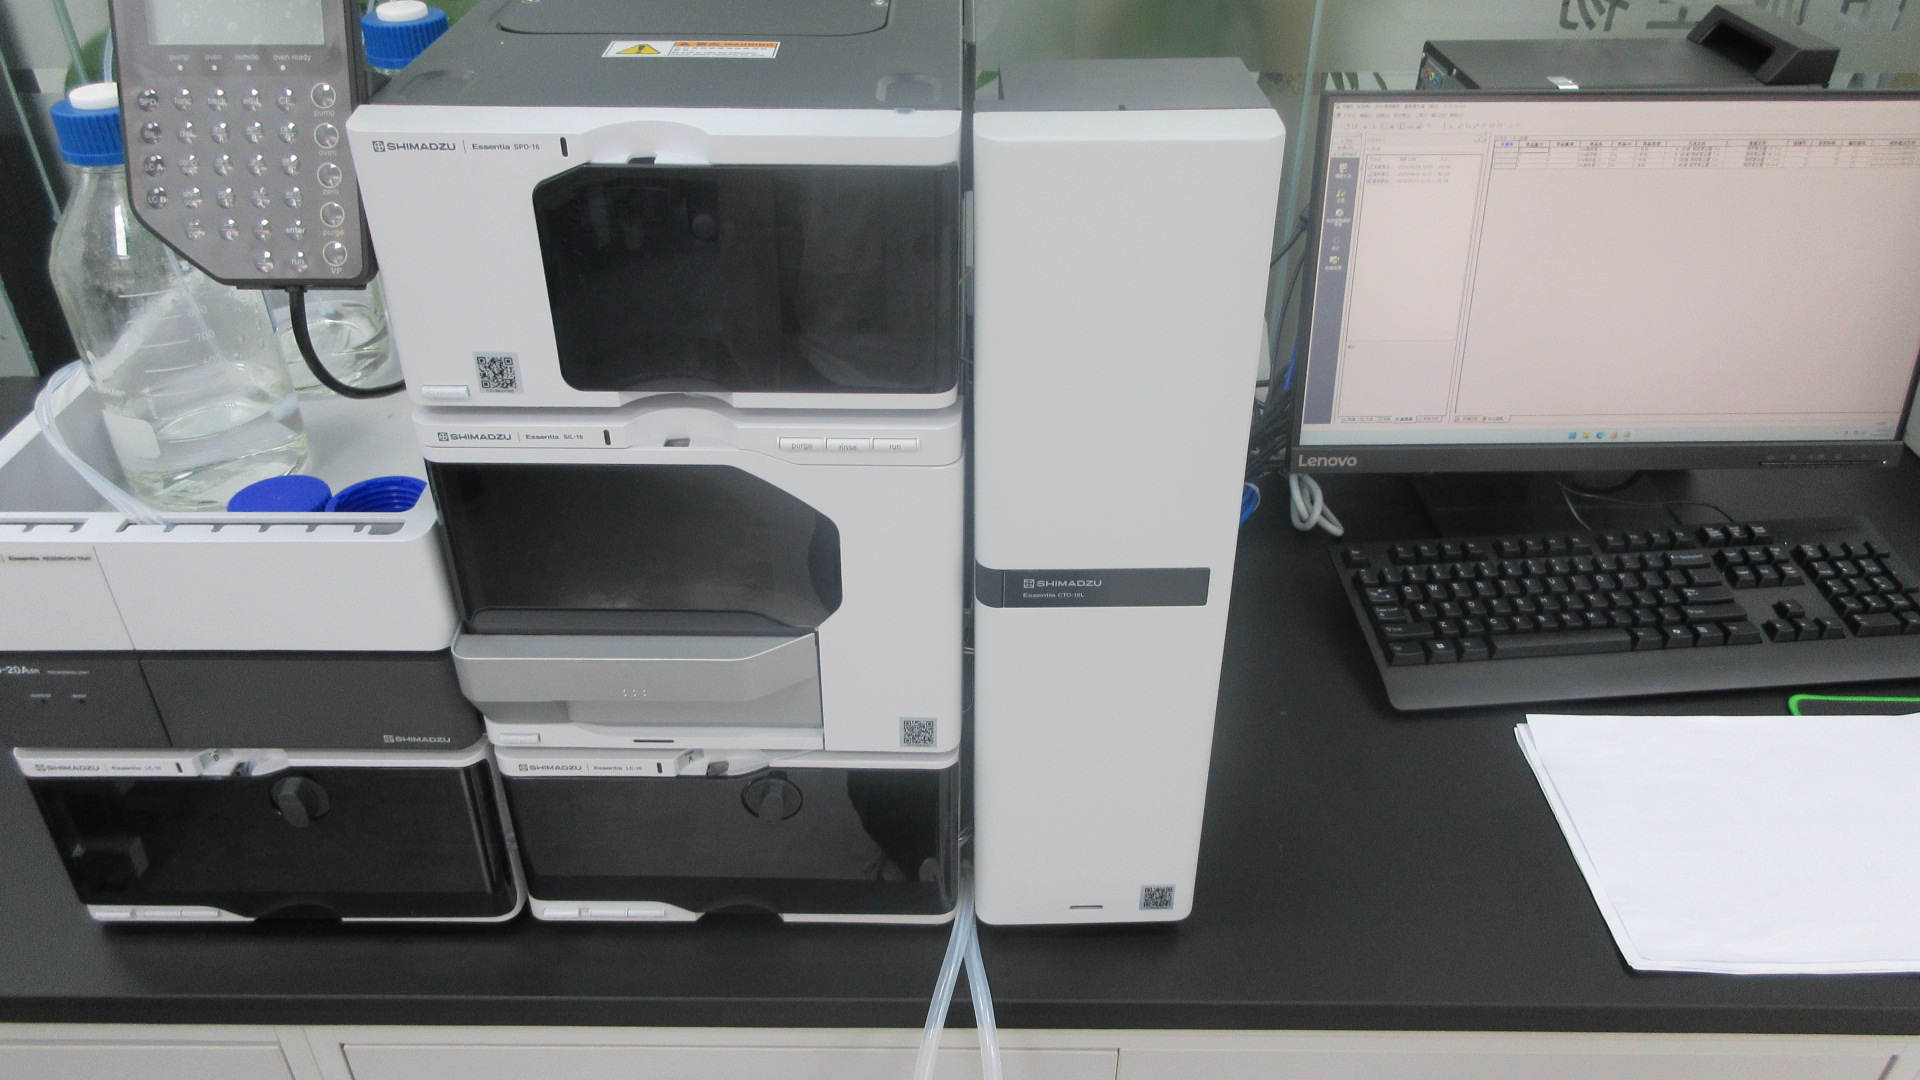
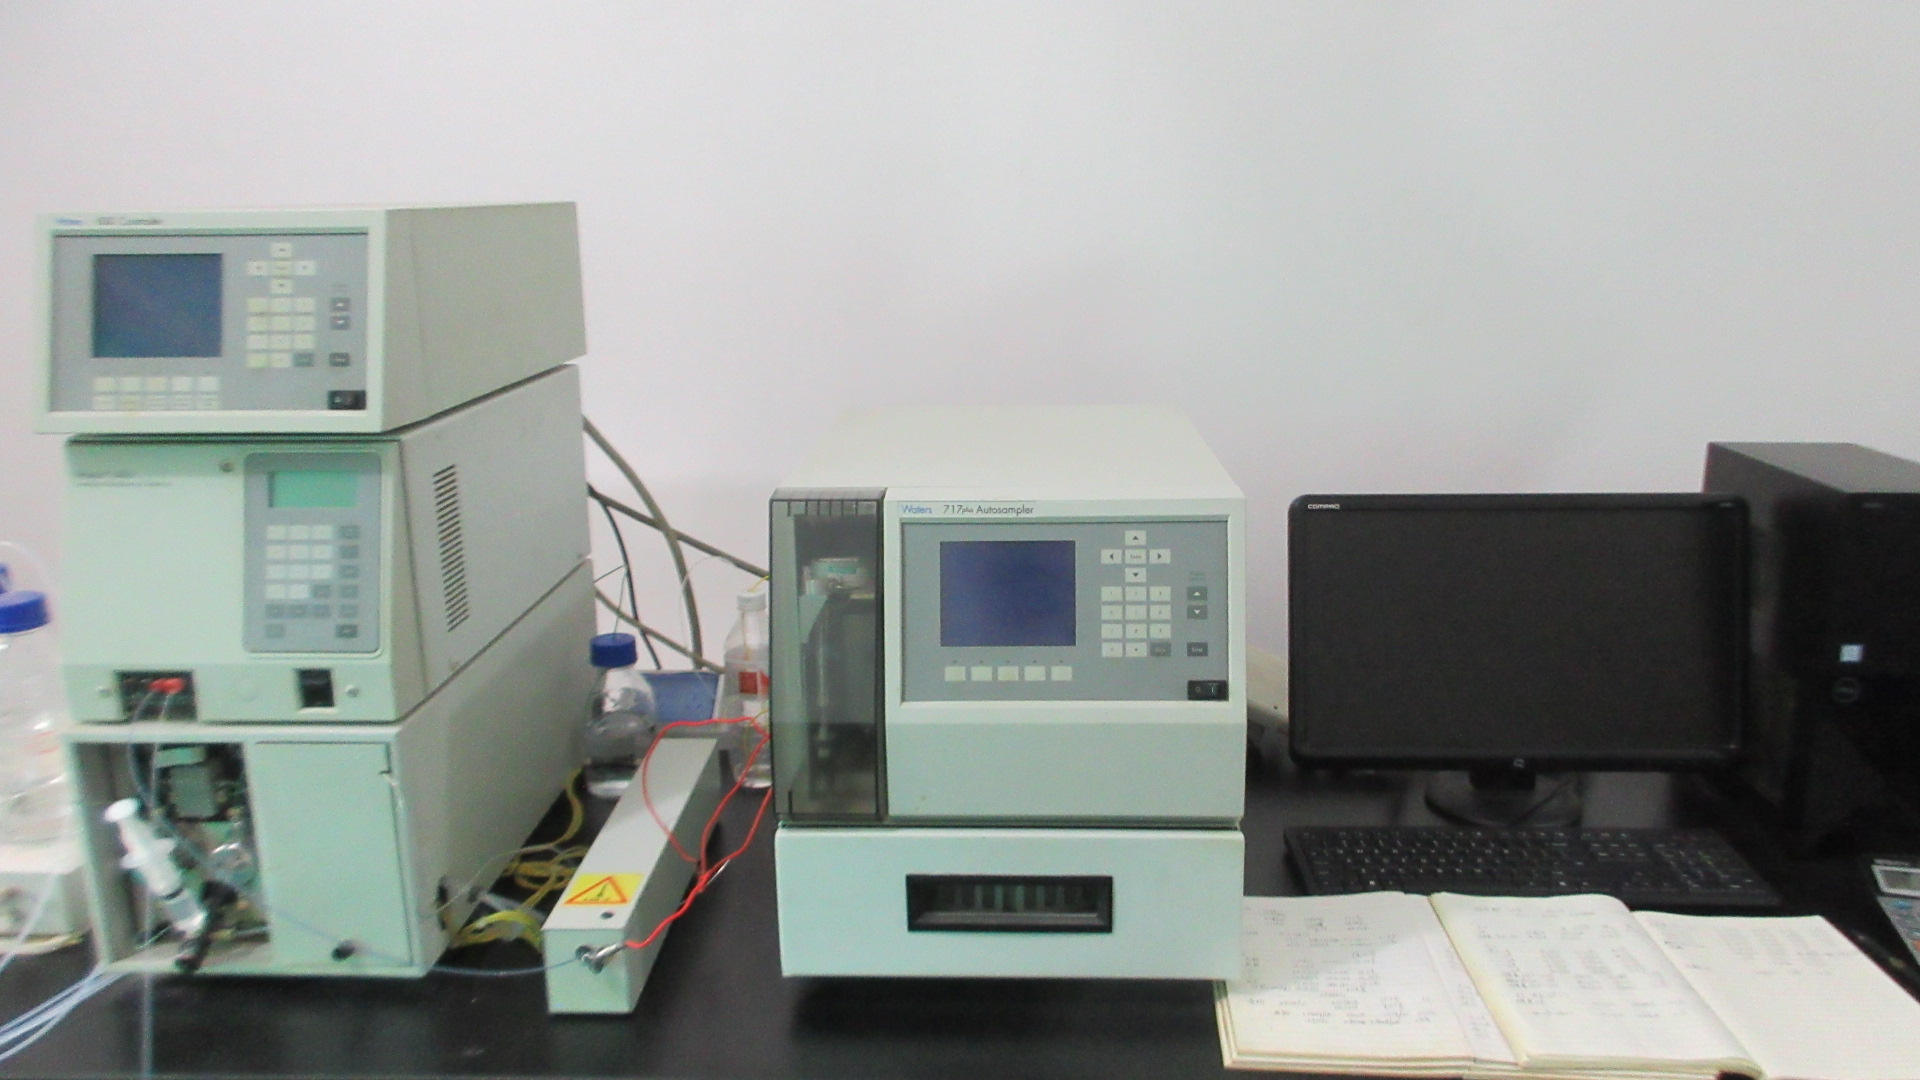
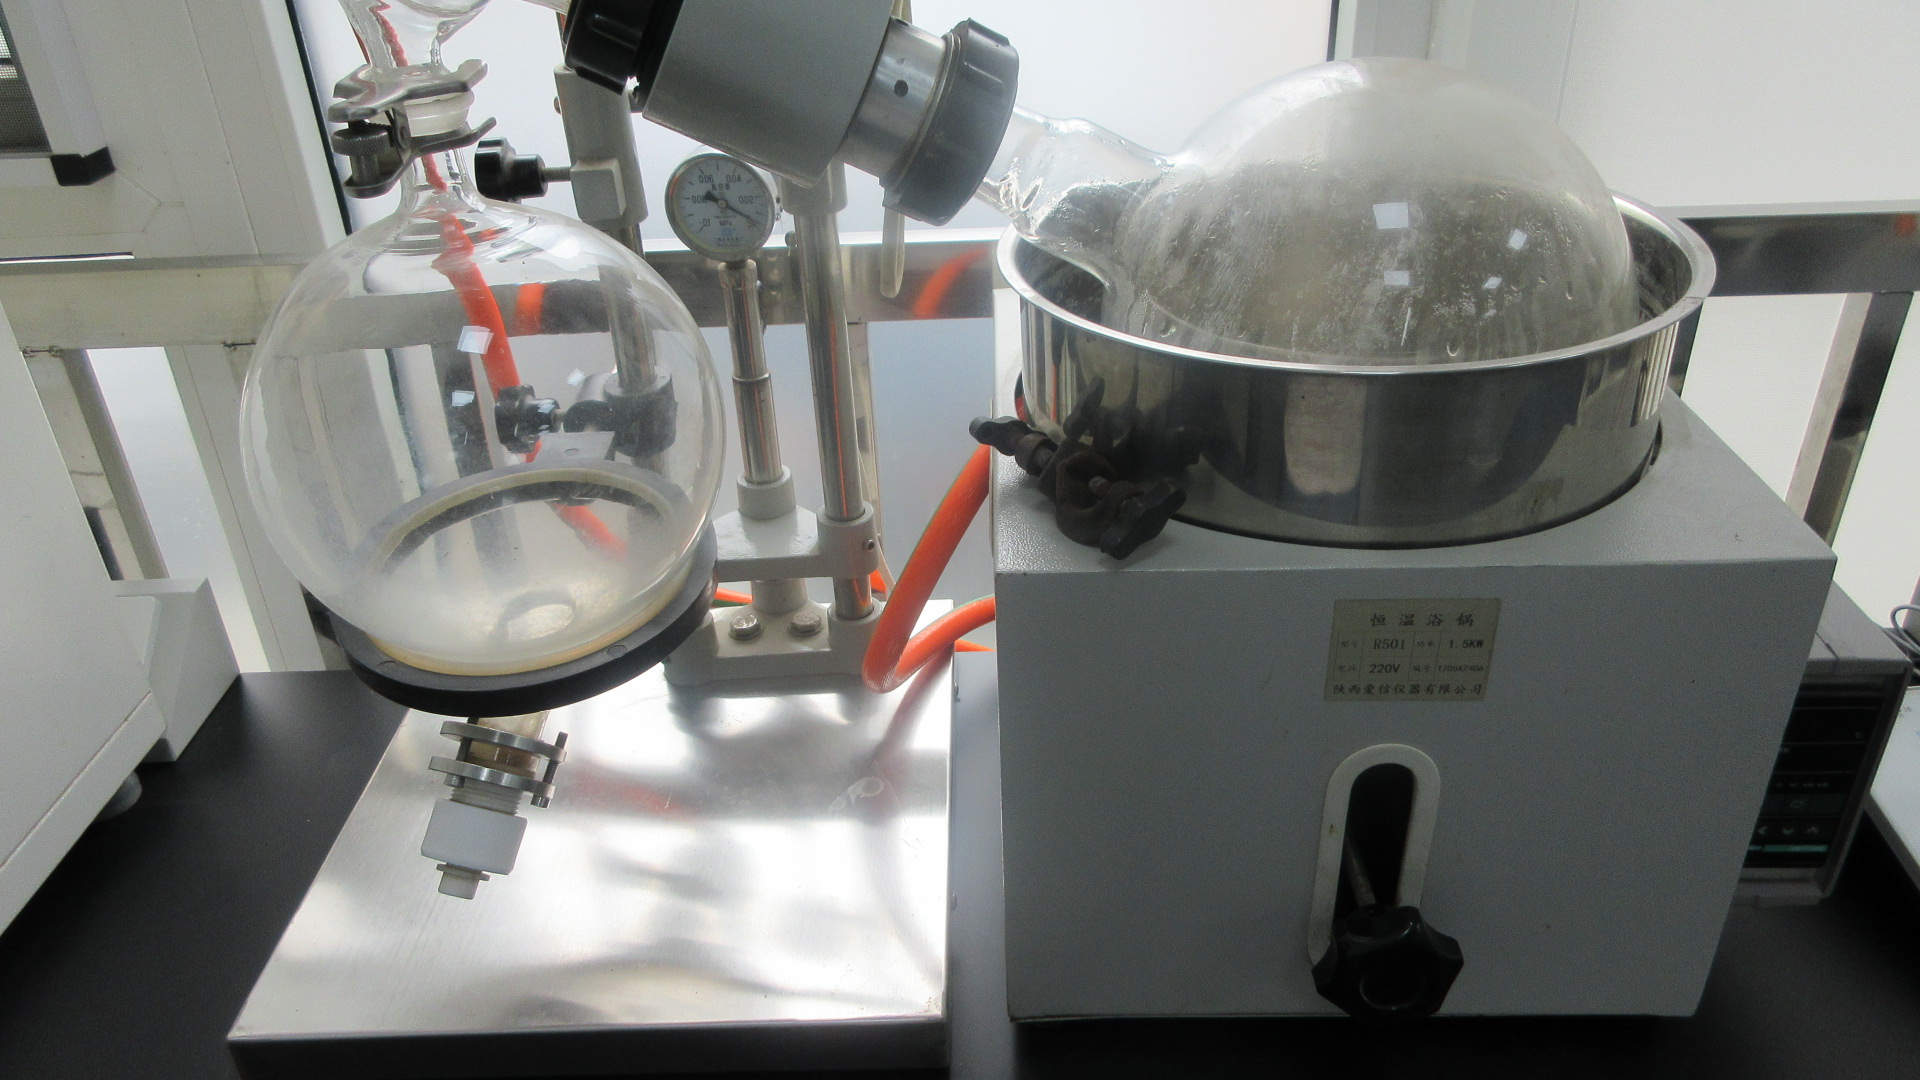
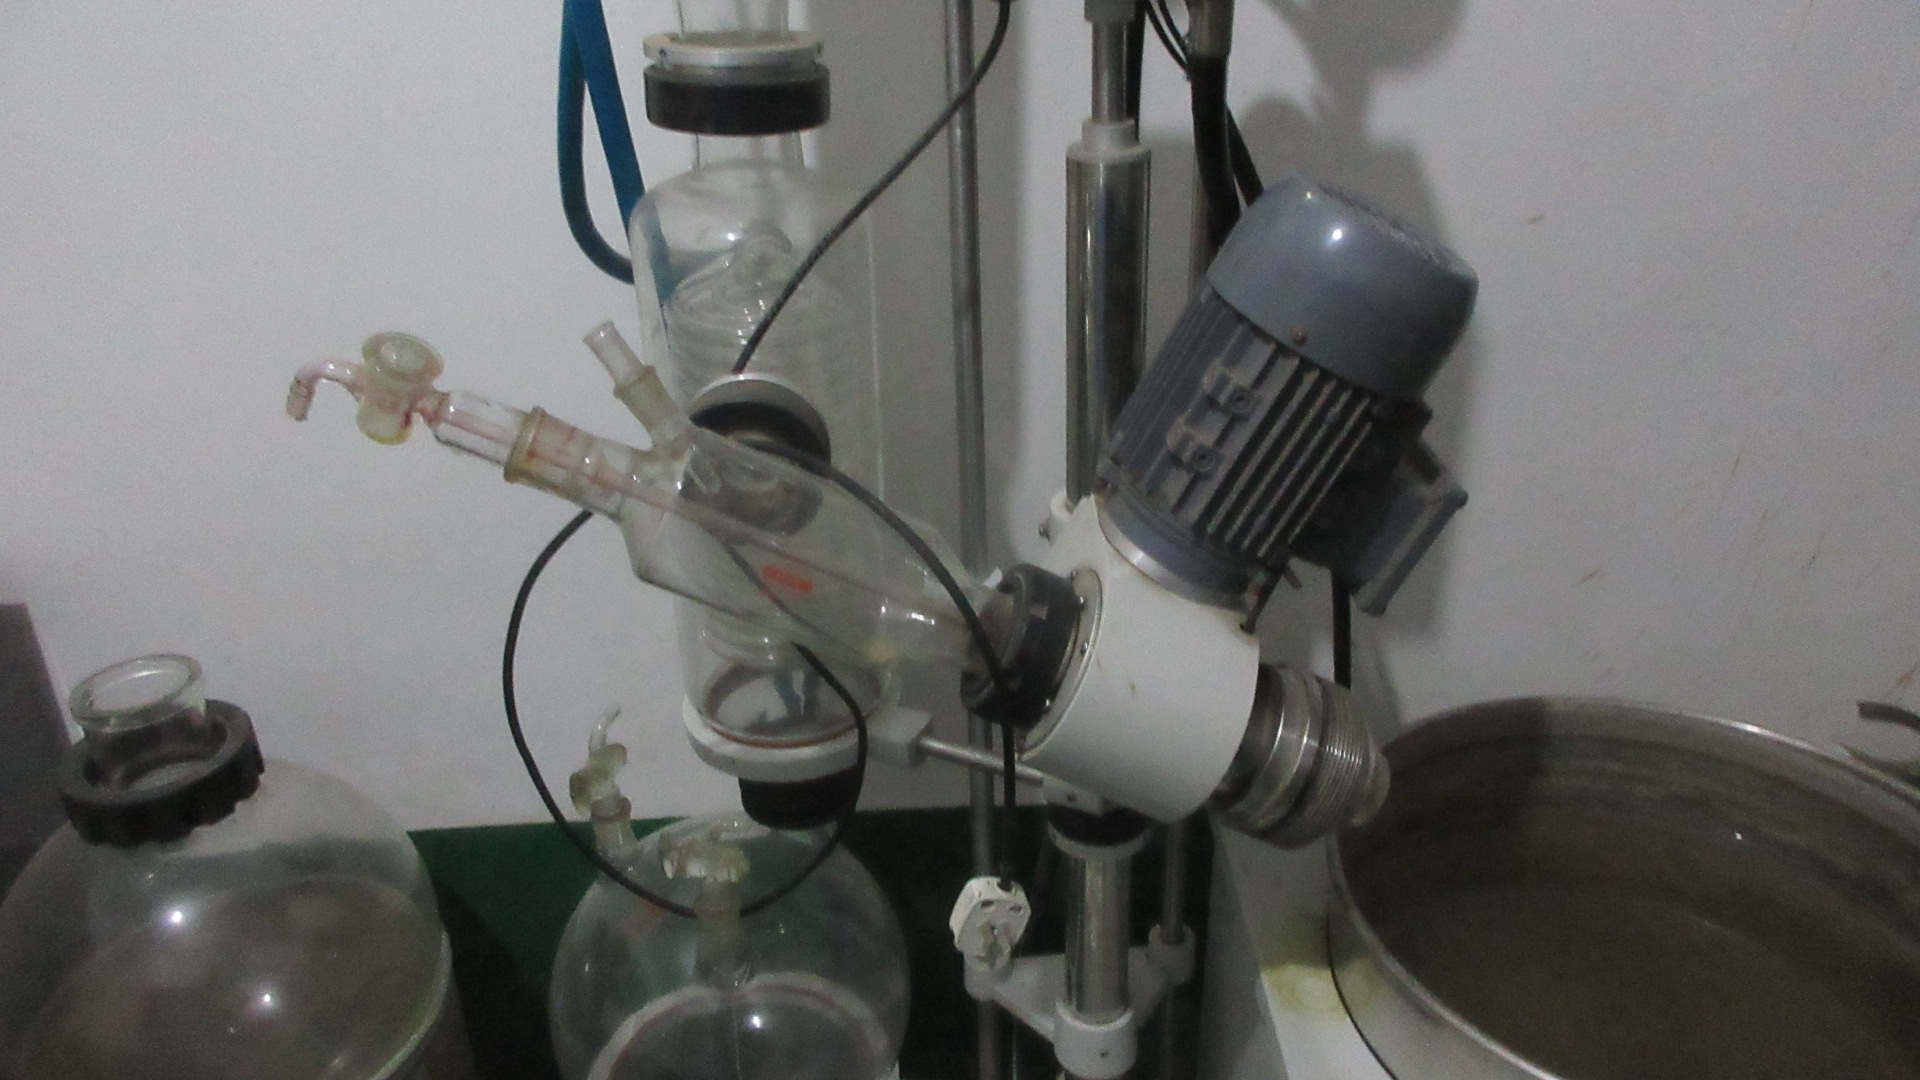
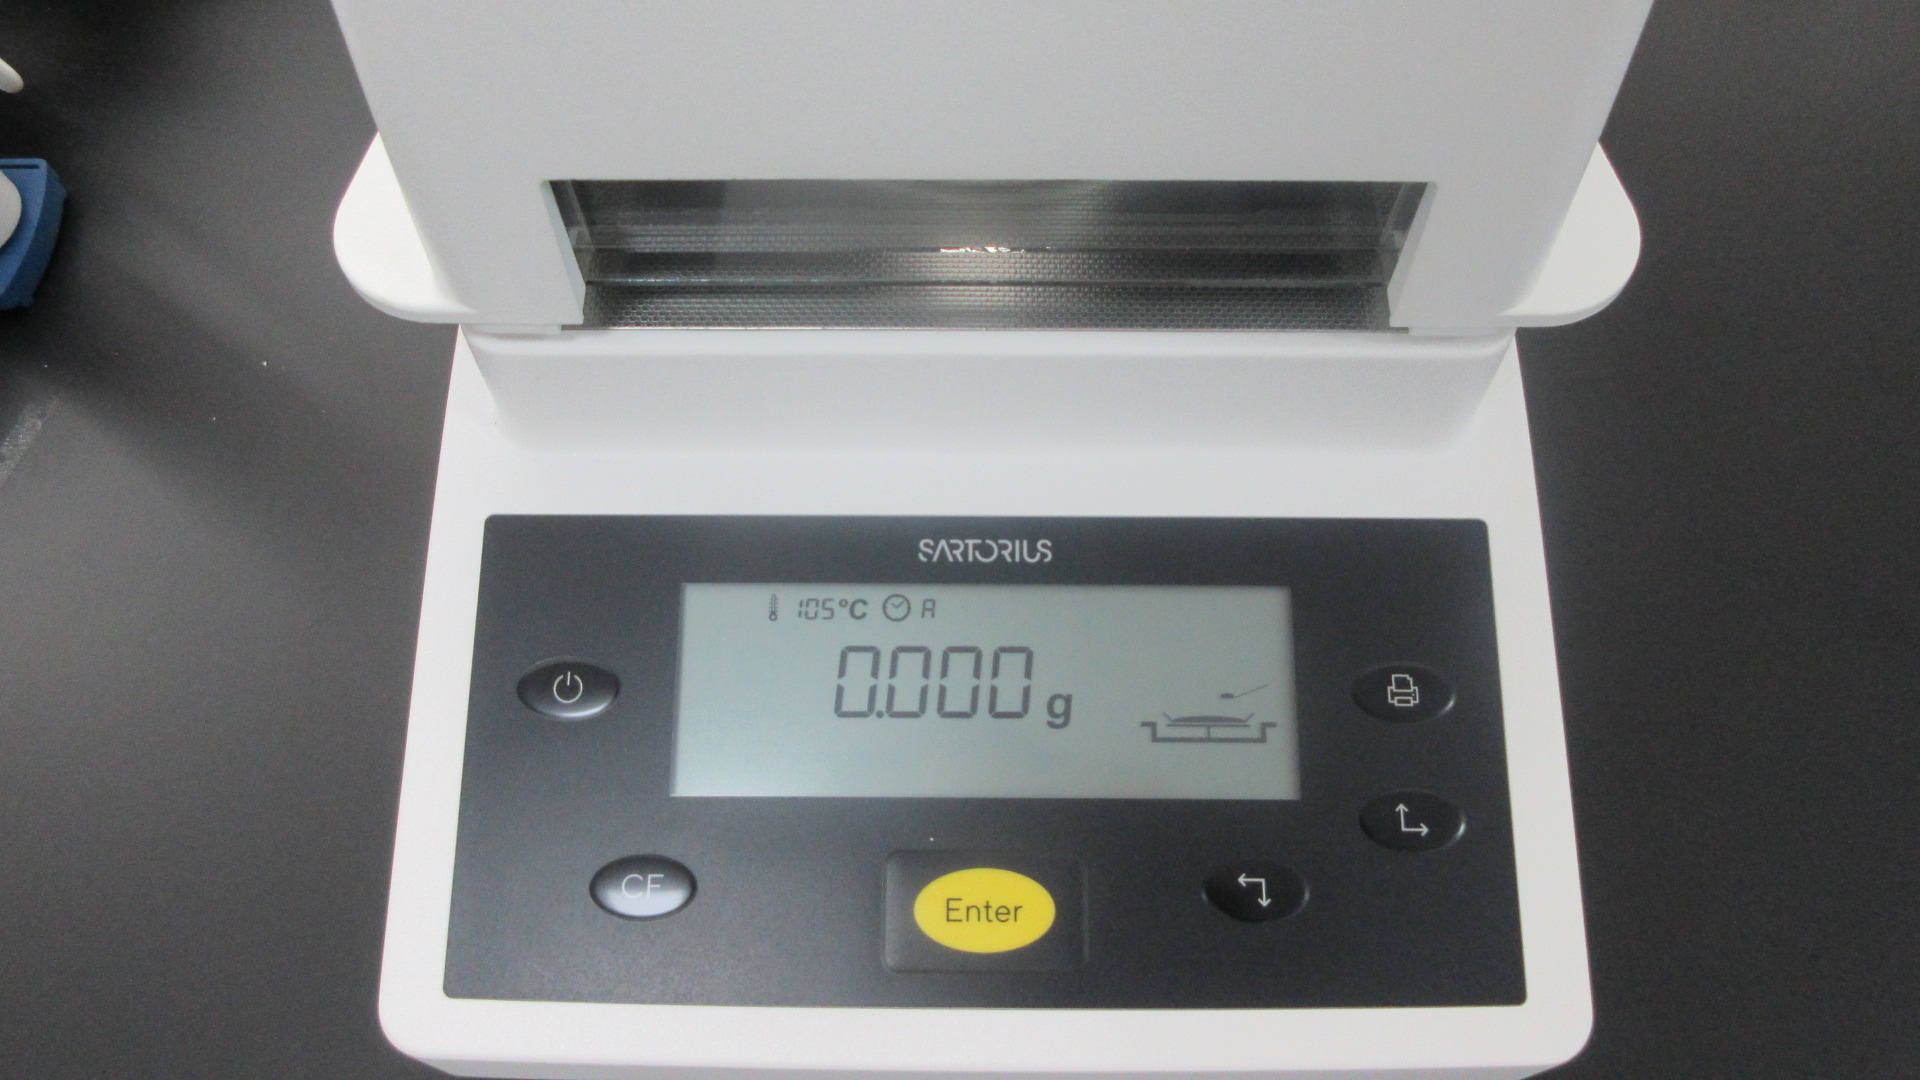
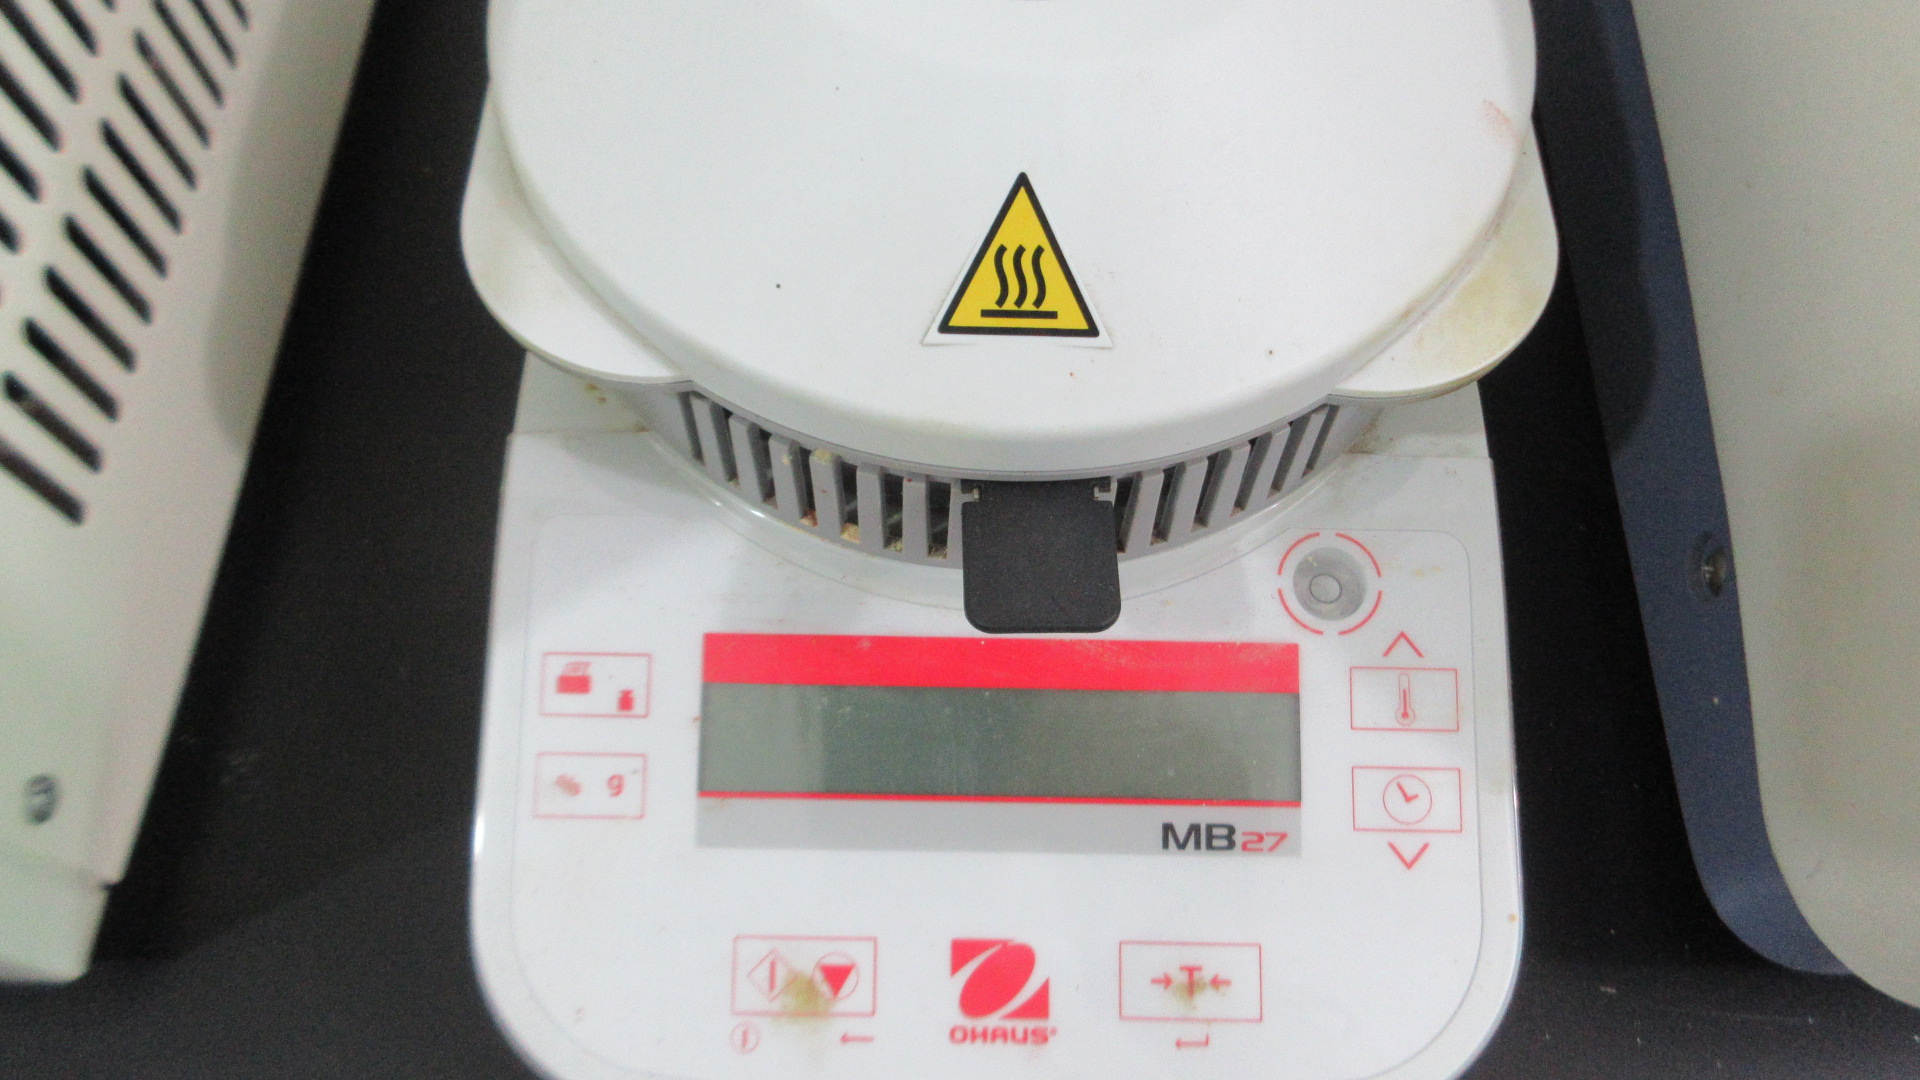
From small-scale pilot extractions to developing unique analytical HPLC marker methods, our in-house engineering and R&D team works closely with global brand owners and formulators.