Company Profile
A trusted global manufacturer of natural plant extracts, zero-calorie sweeteners, and active supplement ingredients.

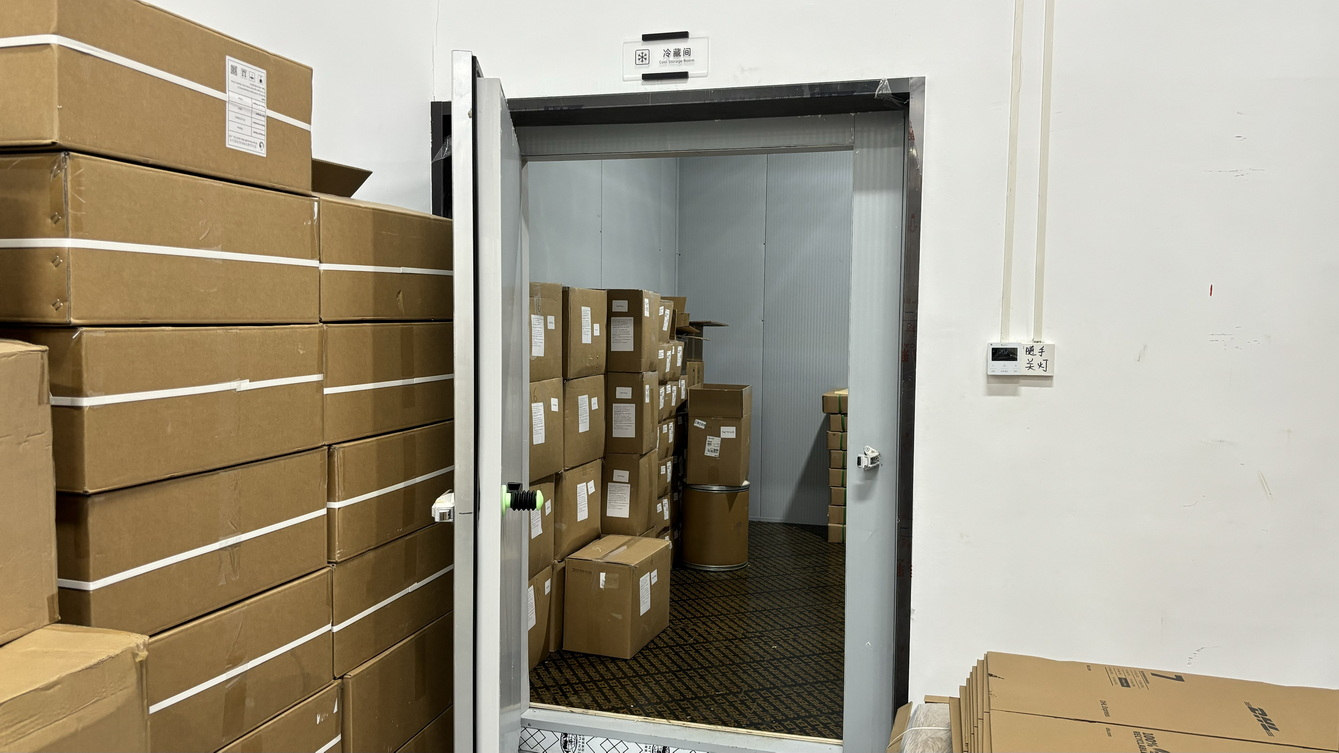
extraction industry
Precision Extraction & Global Botanical Ingredient Supply
Xi'an Vexli Bio-Tech Co., Ltd. is a specialized enterprise based in Xi'an, Shaanxi, China, engaged in the research, production, and international trade of premium natural ingredients. Our product portfolio spans natural plant extracts, natural colorants, zero-calorie sweeteners, natural preservatives, and anti-aging supplement actives (NMN, NAD+, Glutathione) for food, beverage, nutraceutical, and cosmetic industries.
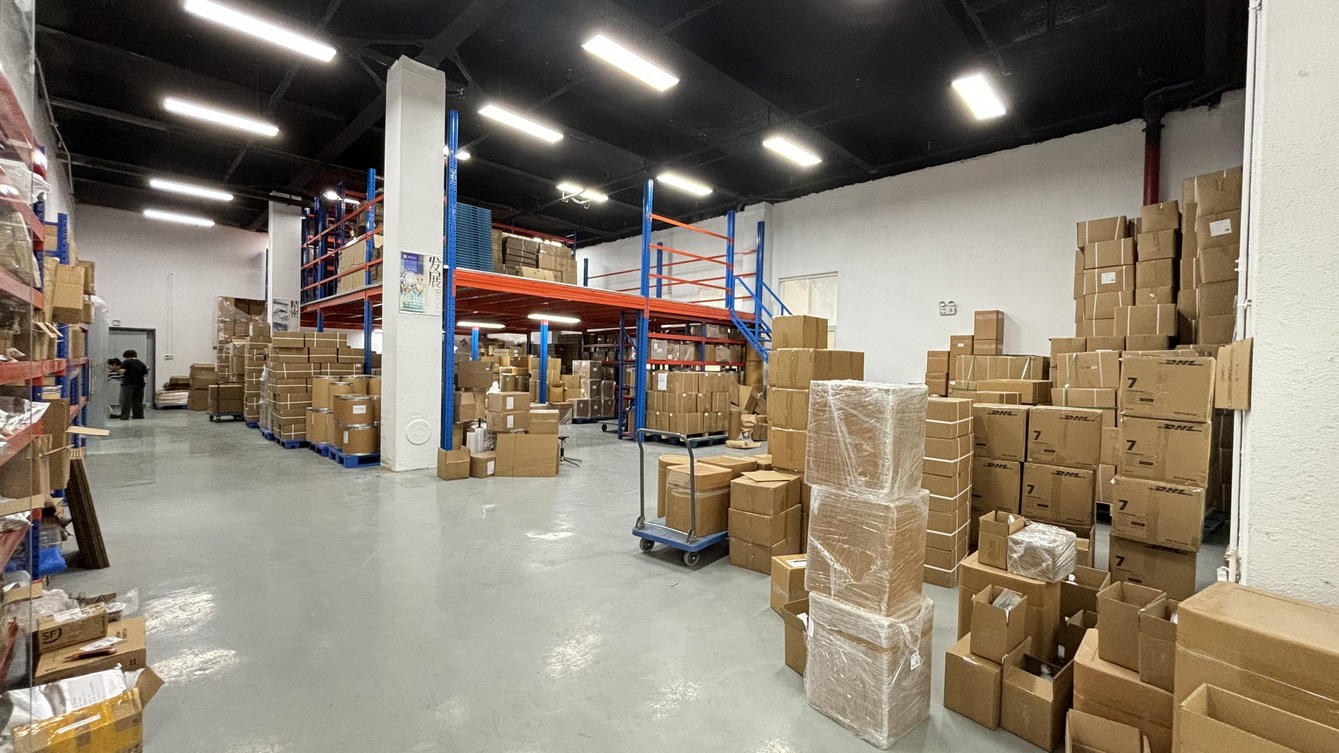
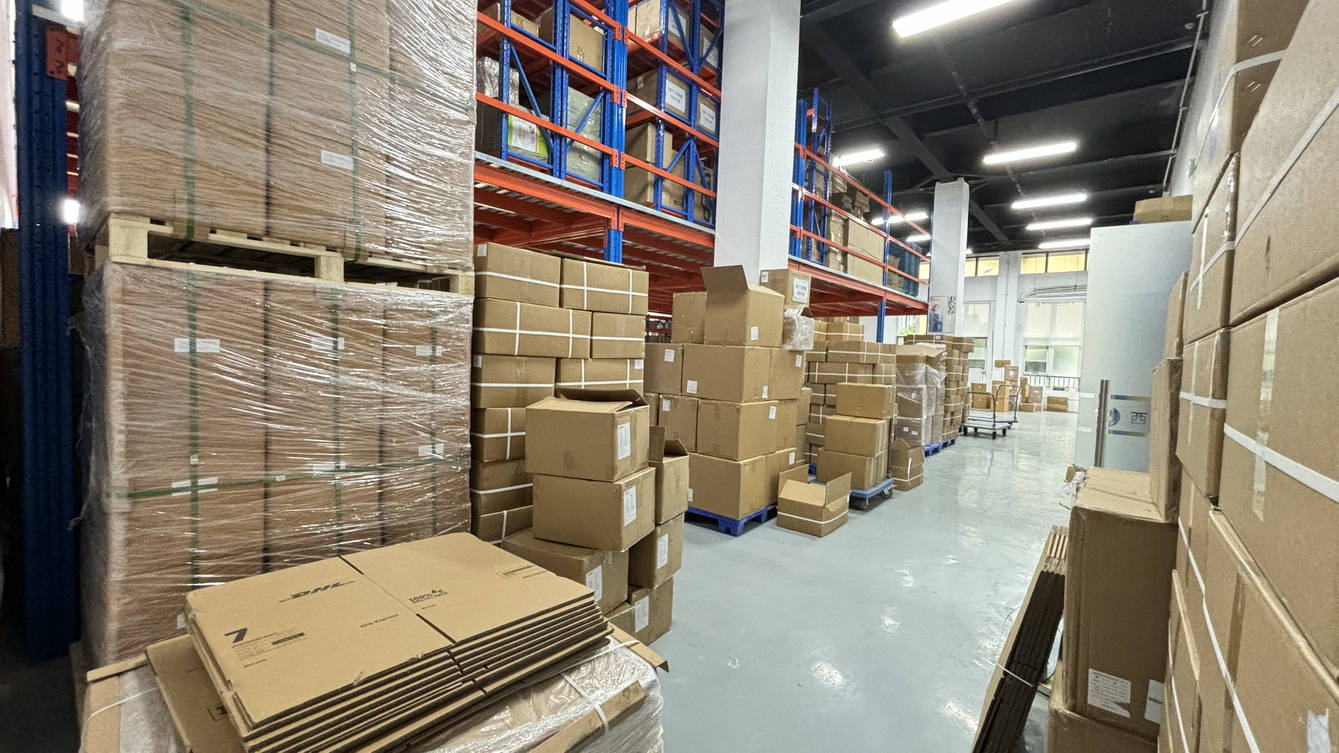
By establishing direct origin-sourcing for raw herbs and operating a modern 1,250 m² processing center alongside 25 audited partner facilities, Xi'an Vexli Bio-Tech Co., Ltd. delivers consistent, specification-controlled powders with low MOQs and comprehensive documentation to buyers across 30+ countries.
- SGS Group On-Site Assessed
- Contracted Fortune 500 Supplier
- Invention & Utility Model Patents
- ISO 22000 & HACCP Food Safety
- Full Customization & Private Label
- Batch-Level COA & SGS Reports
Commercial Capability & Track Record
Independent audit data reflecting our trade stability, quality control, and customer satisfaction.
Operational Performance Benchmarks
How Xi'an Vexli Bio-Tech Co., Ltd. compares against industry standards across key procurement metrics.
Customer Rating
Based on verified buyer reviews. 4.0% higher than category average.
Average Response Time
Fast inquiry handling and active technical customer support.
Dispatch Speed
Average order dispatch speed, beating the 9.7-day industry standard.
Trade Dispute Rate
Significantly lower than the 4.8% industry average, demonstrating strict compliance.
Quality Assurance Team
Dedicated QA/QC specialists covering incoming, in-process, and finished goods.
R&D Engineering
Active development of novel specs, particle milling, and customized blends.
Our 9-Step Plant Extraction Process
Every botanical batch undergoes controlled extraction, purification, and particle standardization.
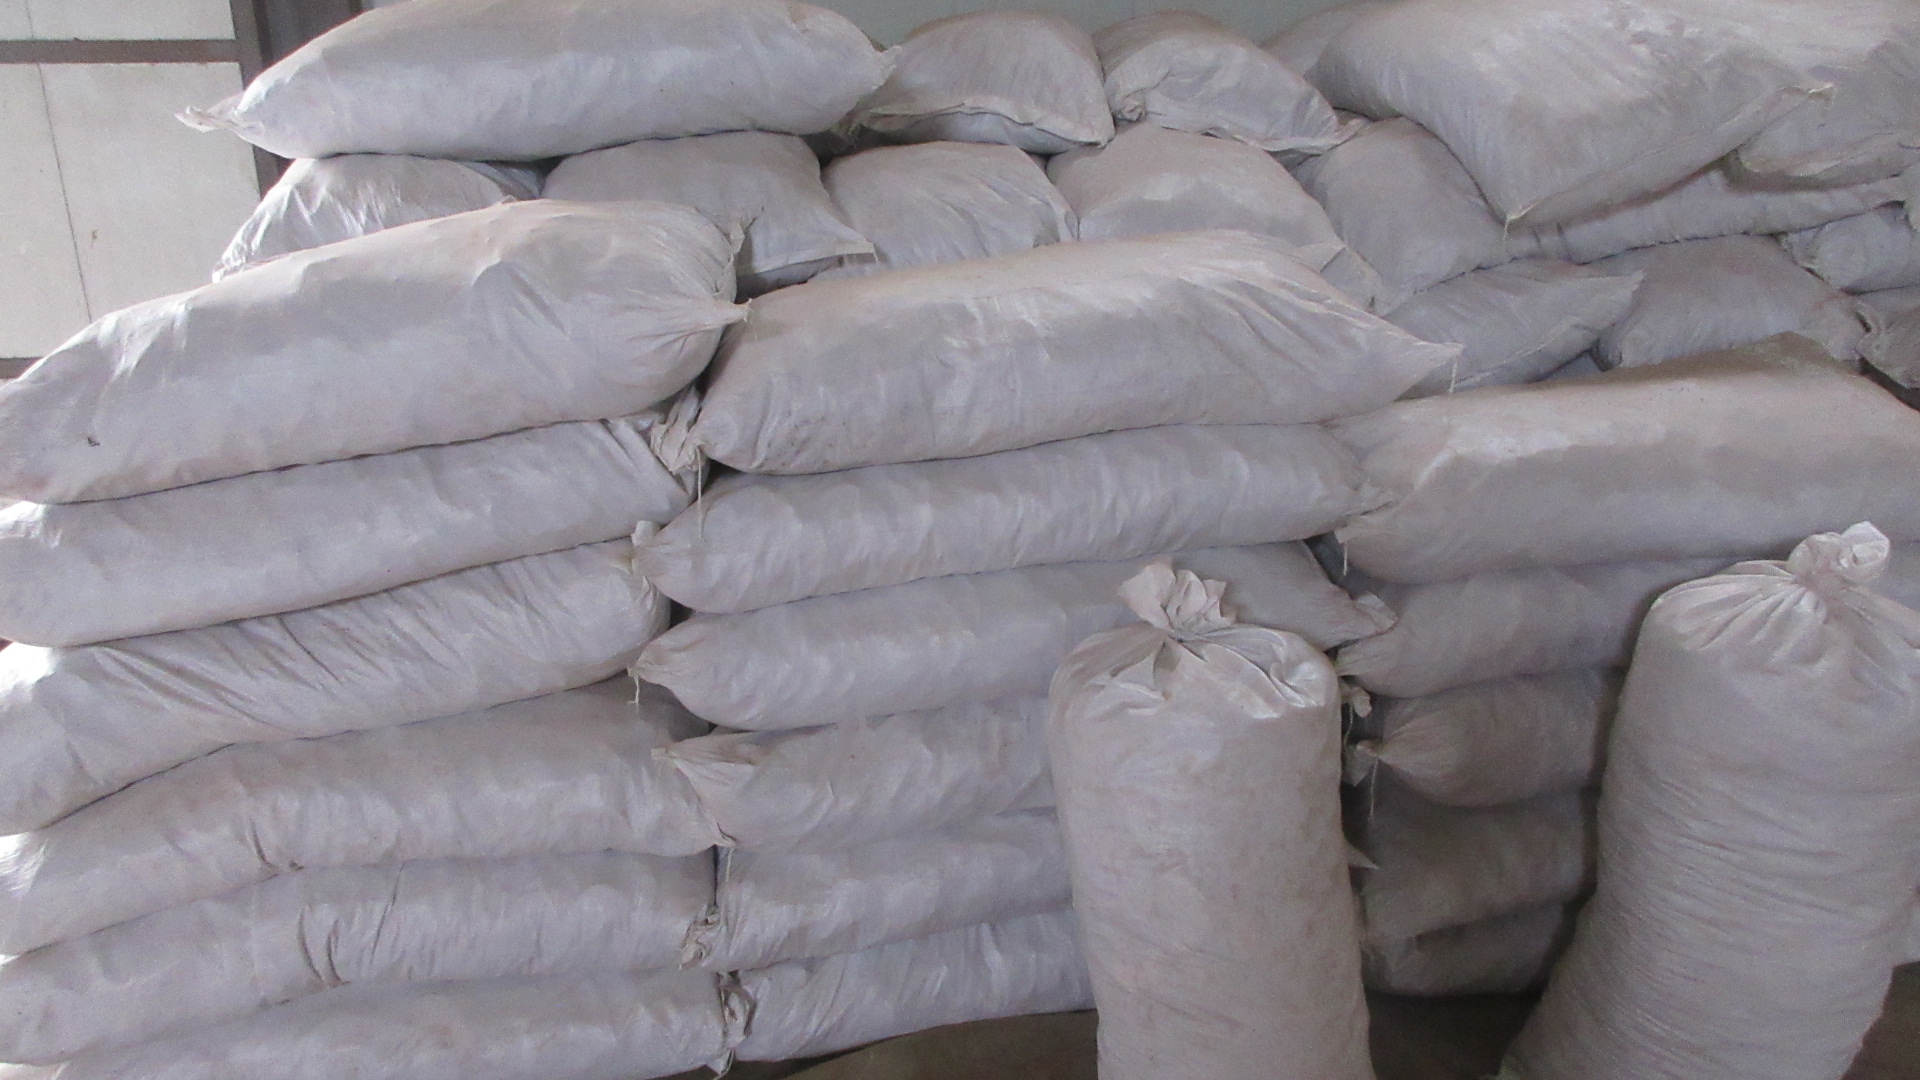
1. Raw Materials
Botanicals sourced directly from origin, checked for species identity, moisture, and active marker content.
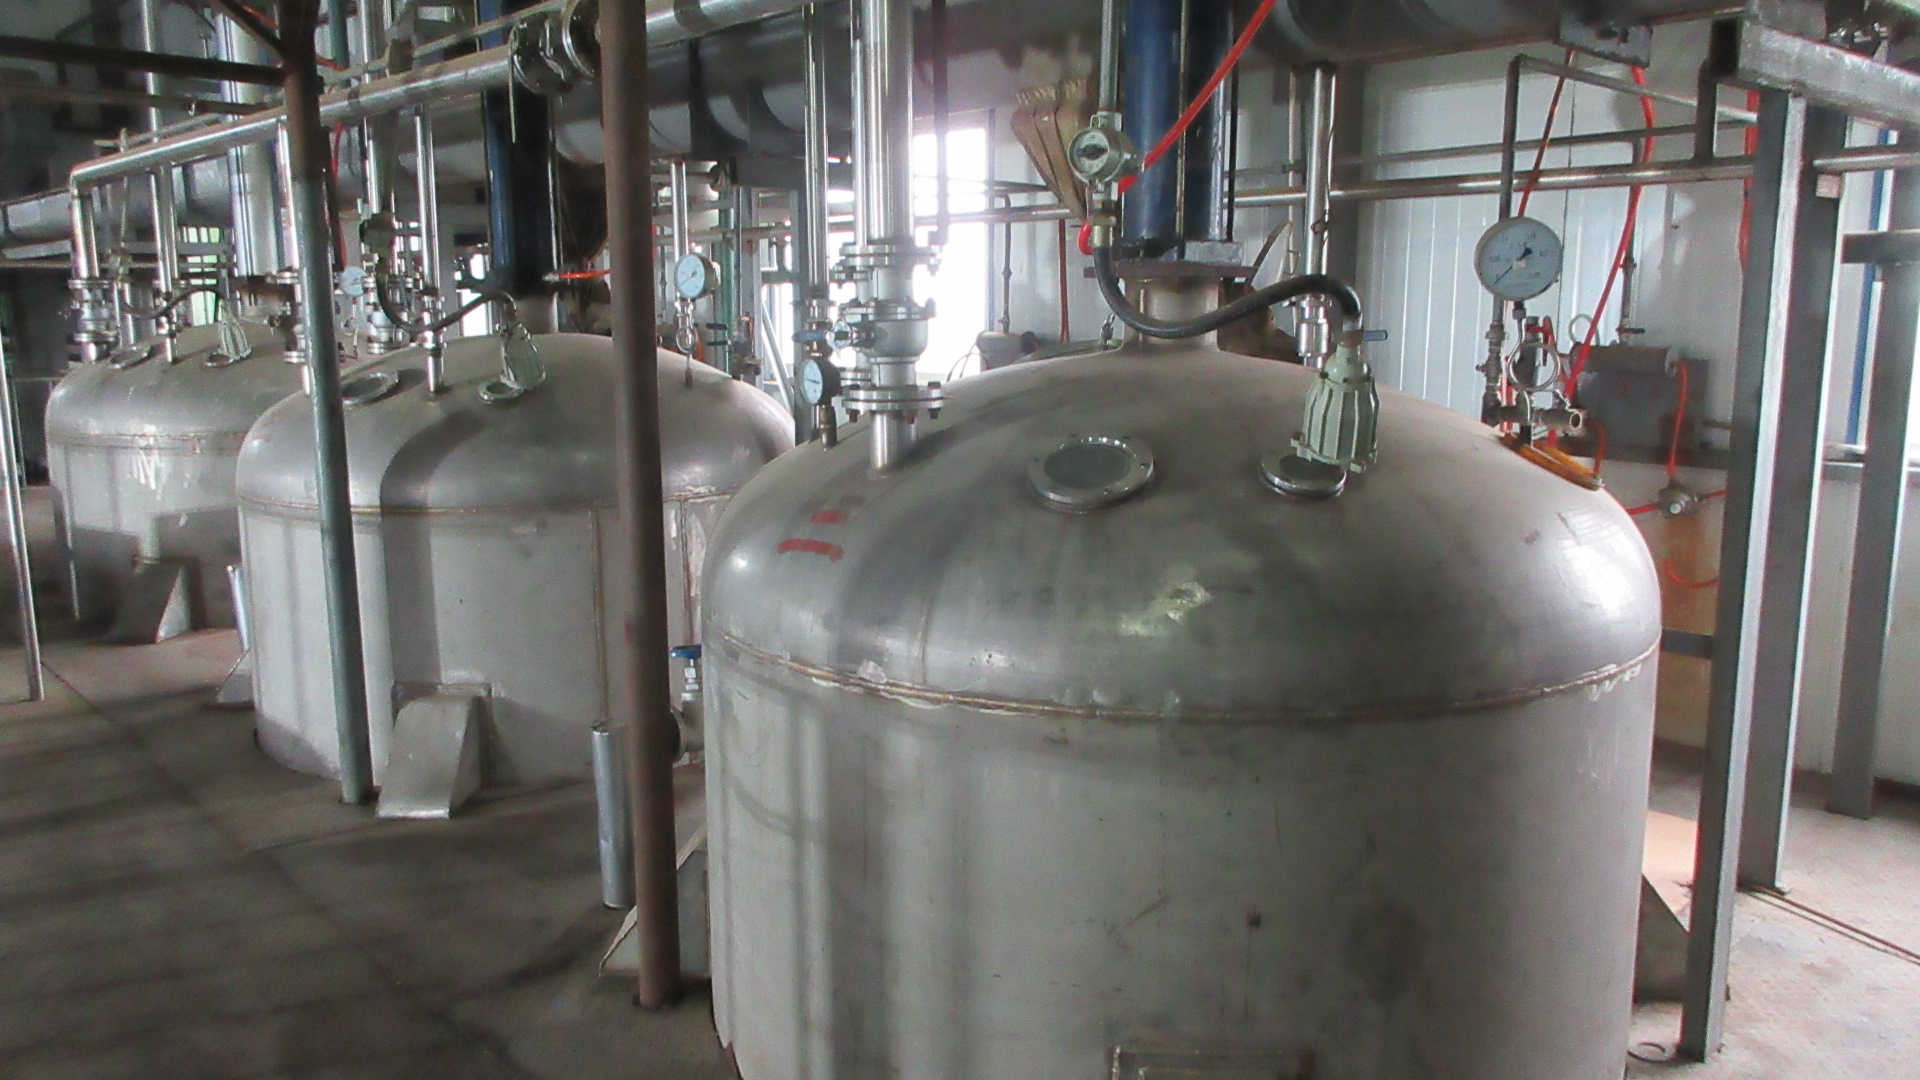
2. Extracting
Multi-stage water or ethanol extraction under controlled temperature and duration.
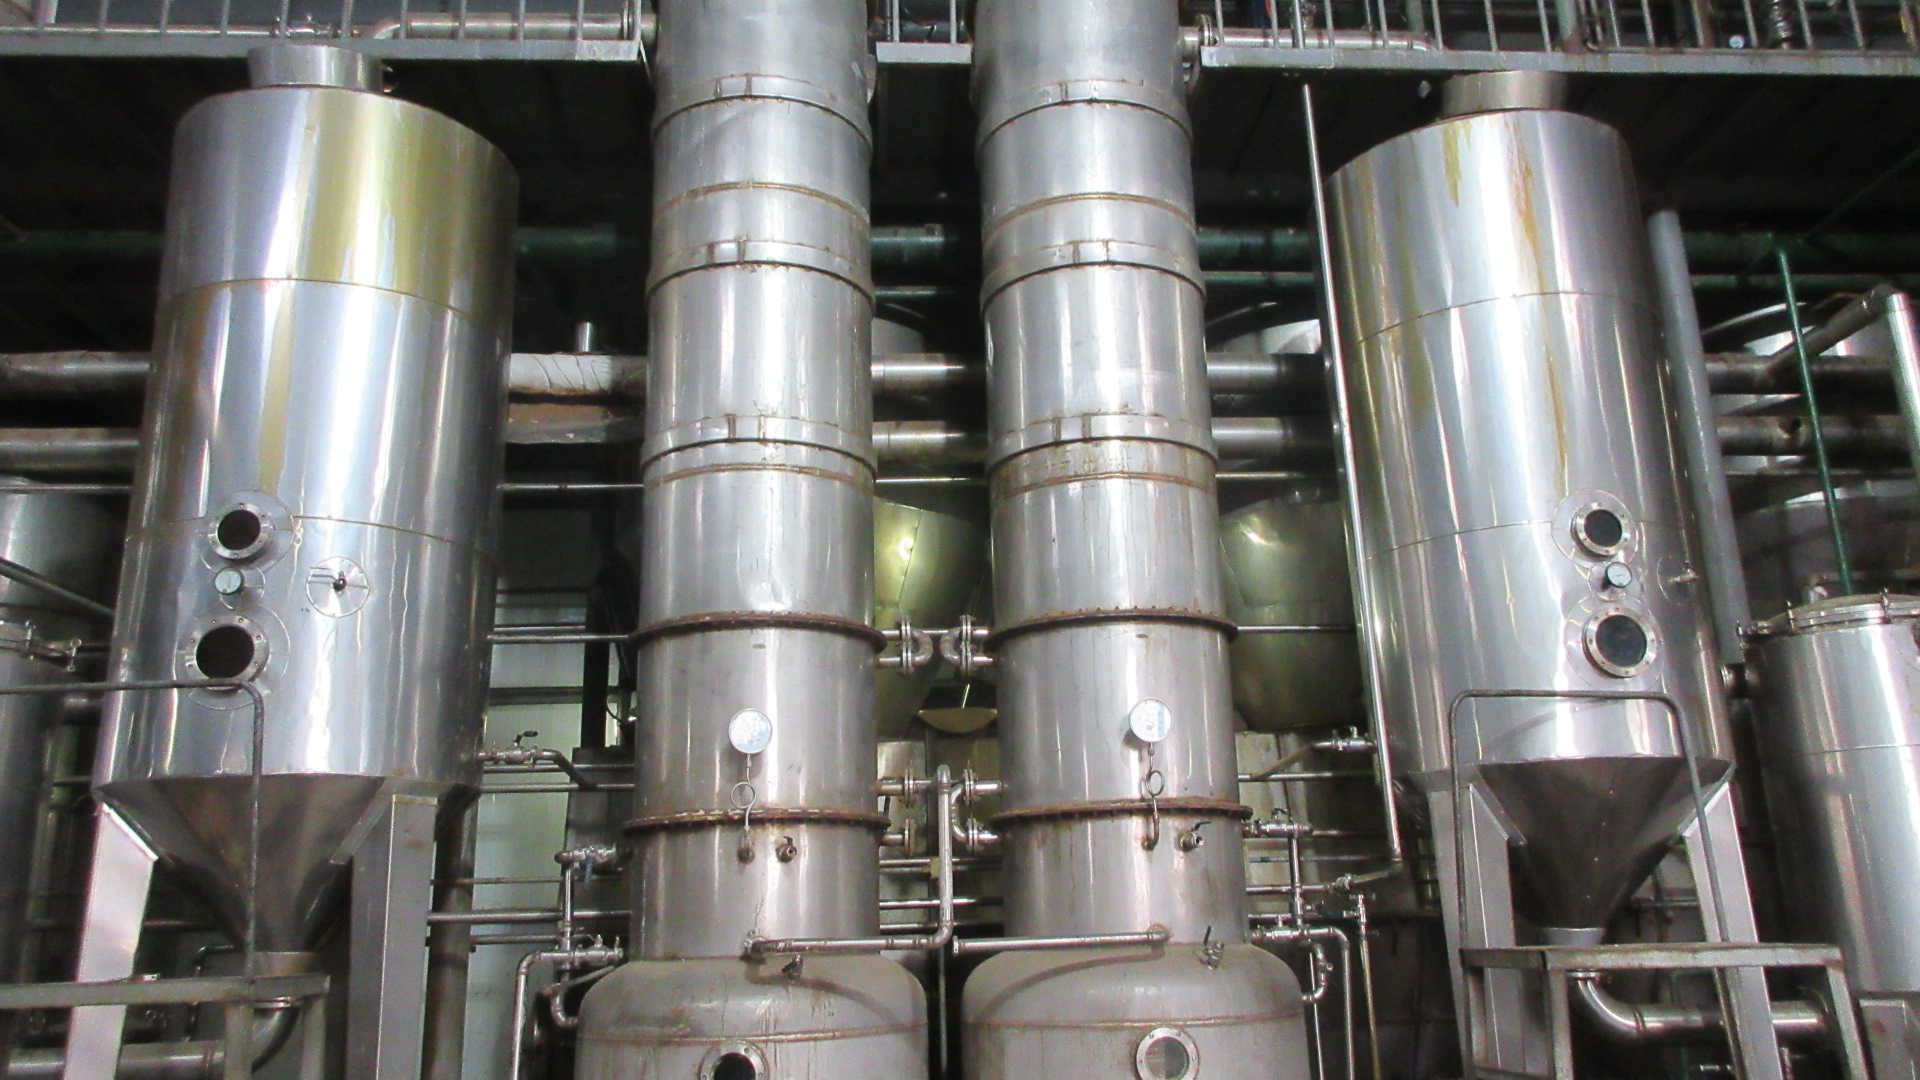
3. Concentration
Low-temperature vacuum evaporation to concentrate actives while preserving heat-sensitive bio-compounds.
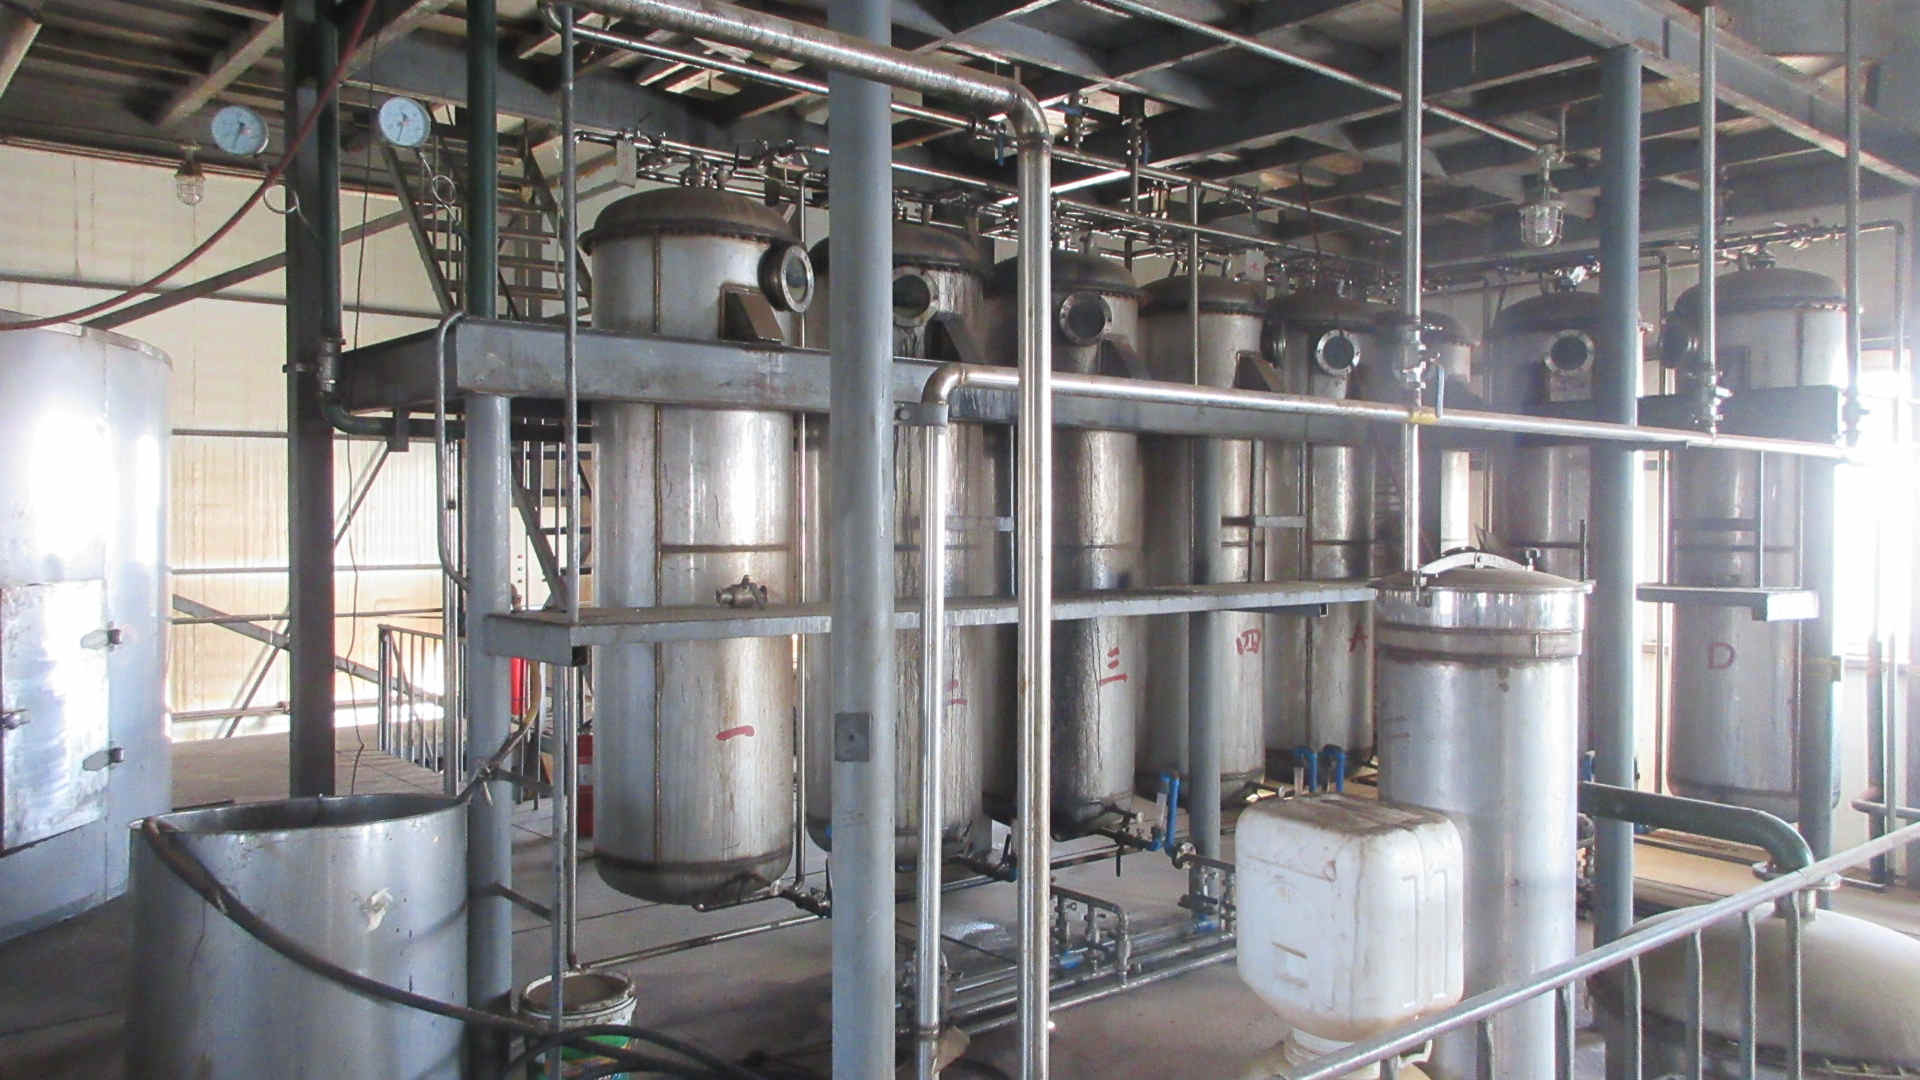
4. Purification
Macroporous resin column chromatography and filtration to achieve targeted assay purity.
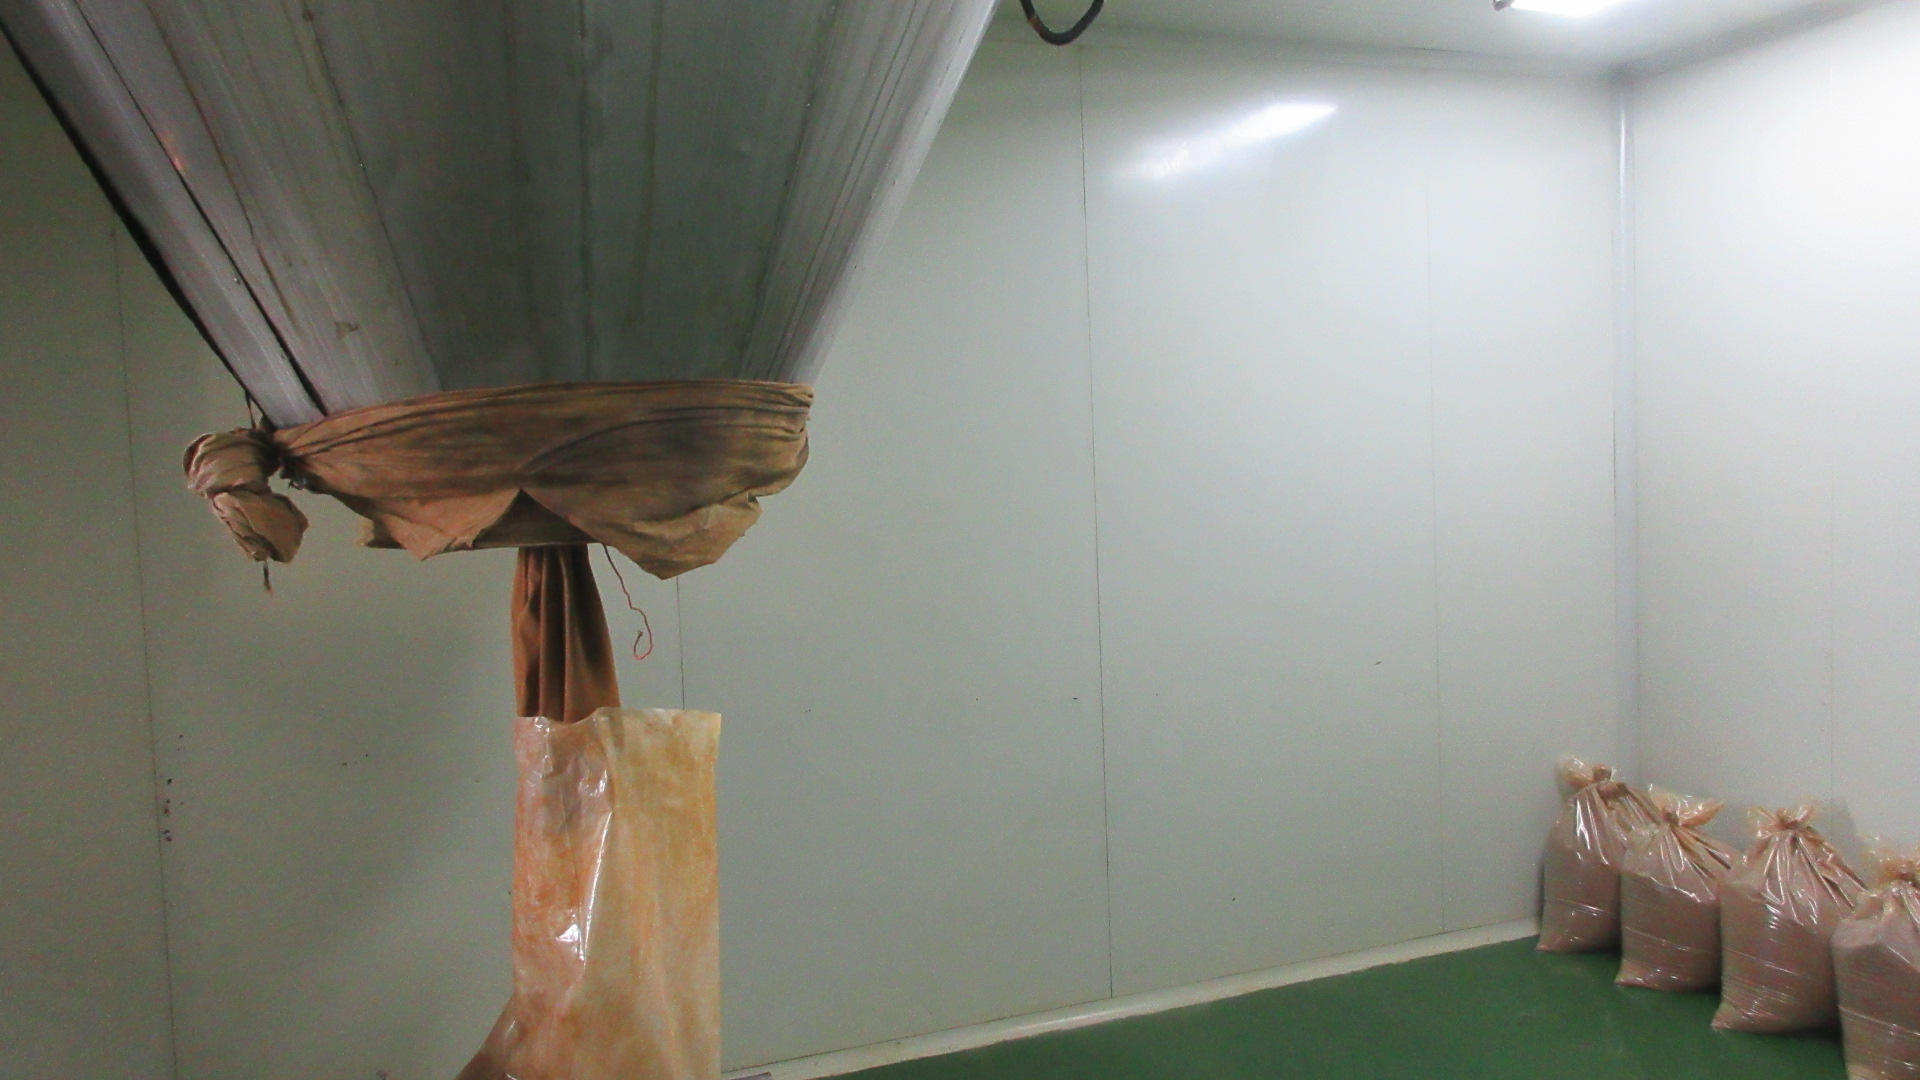
5. Drying & Spraying
Advanced spray-drying tower or vacuum drying for optimal moisture control and solubility.
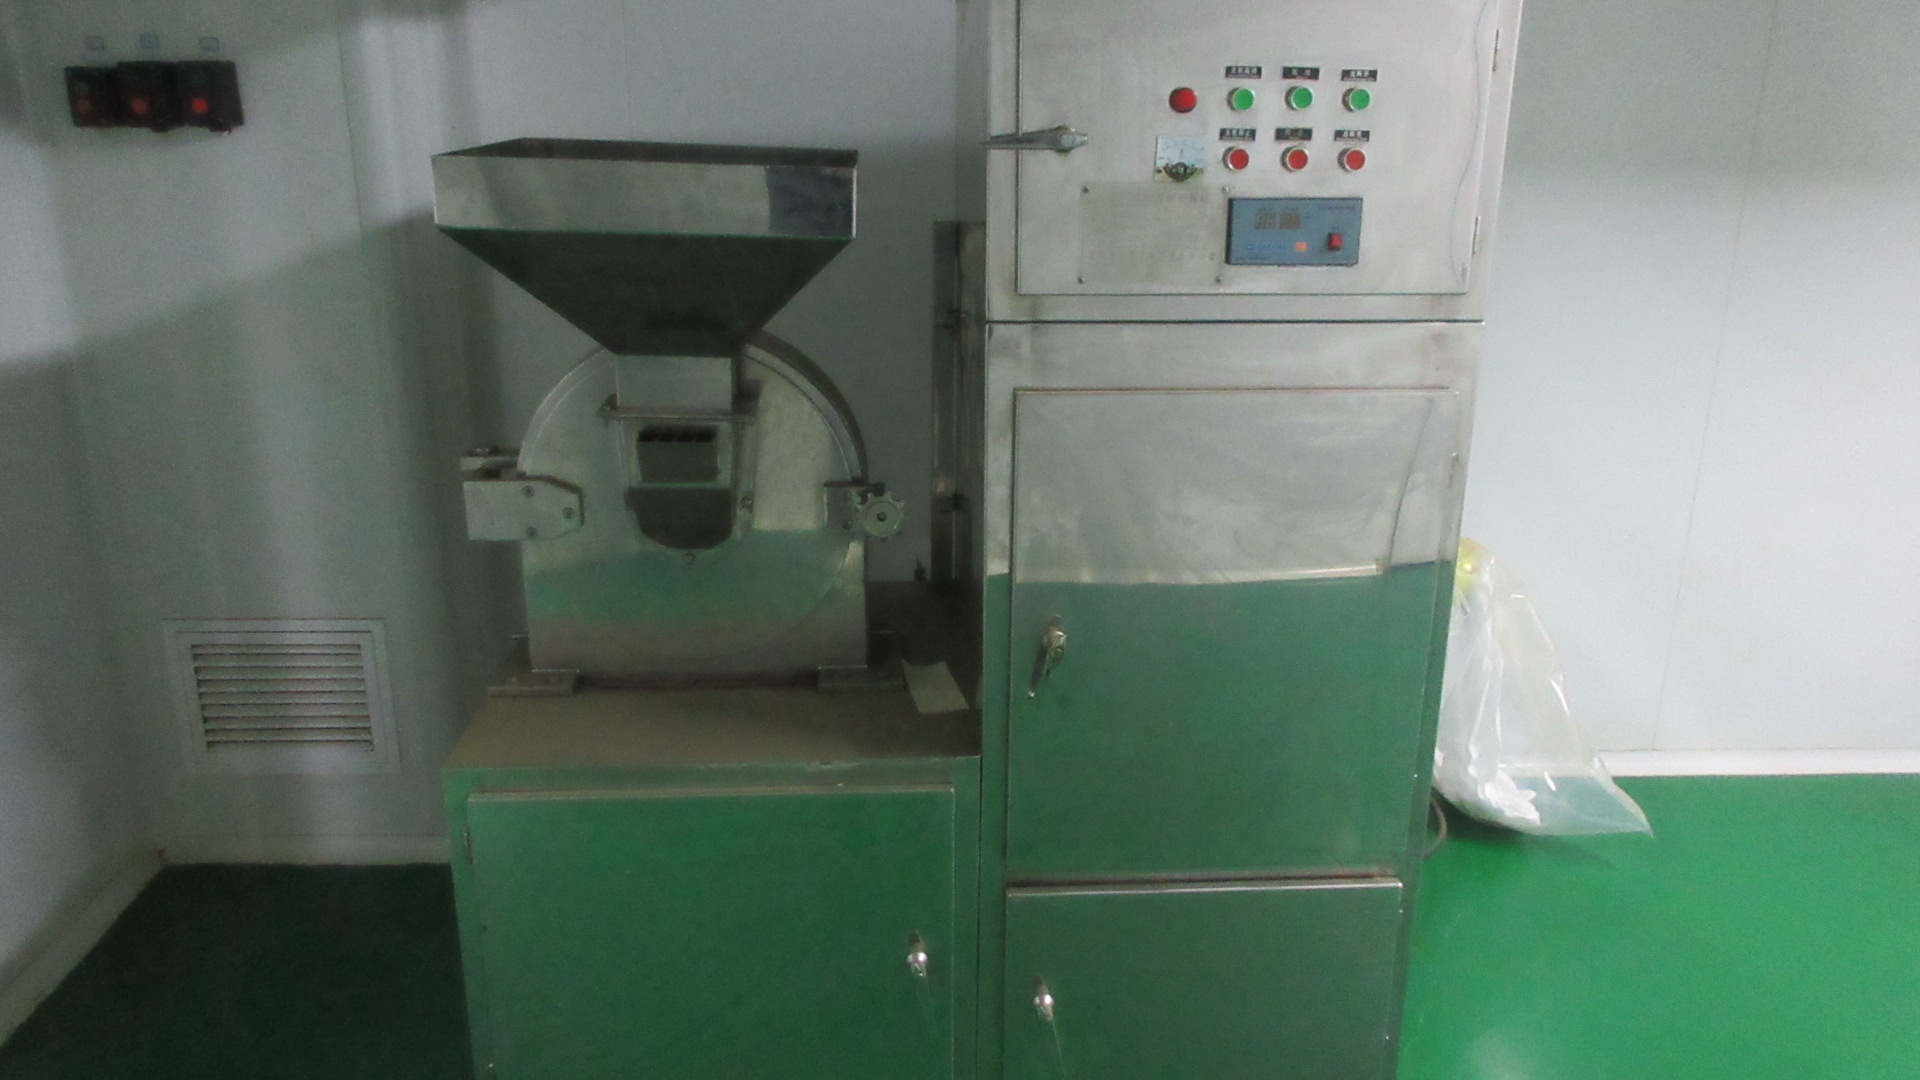
6. Pulverizing
Precision milling to achieve smooth flowability and customer-defined particle sizes.
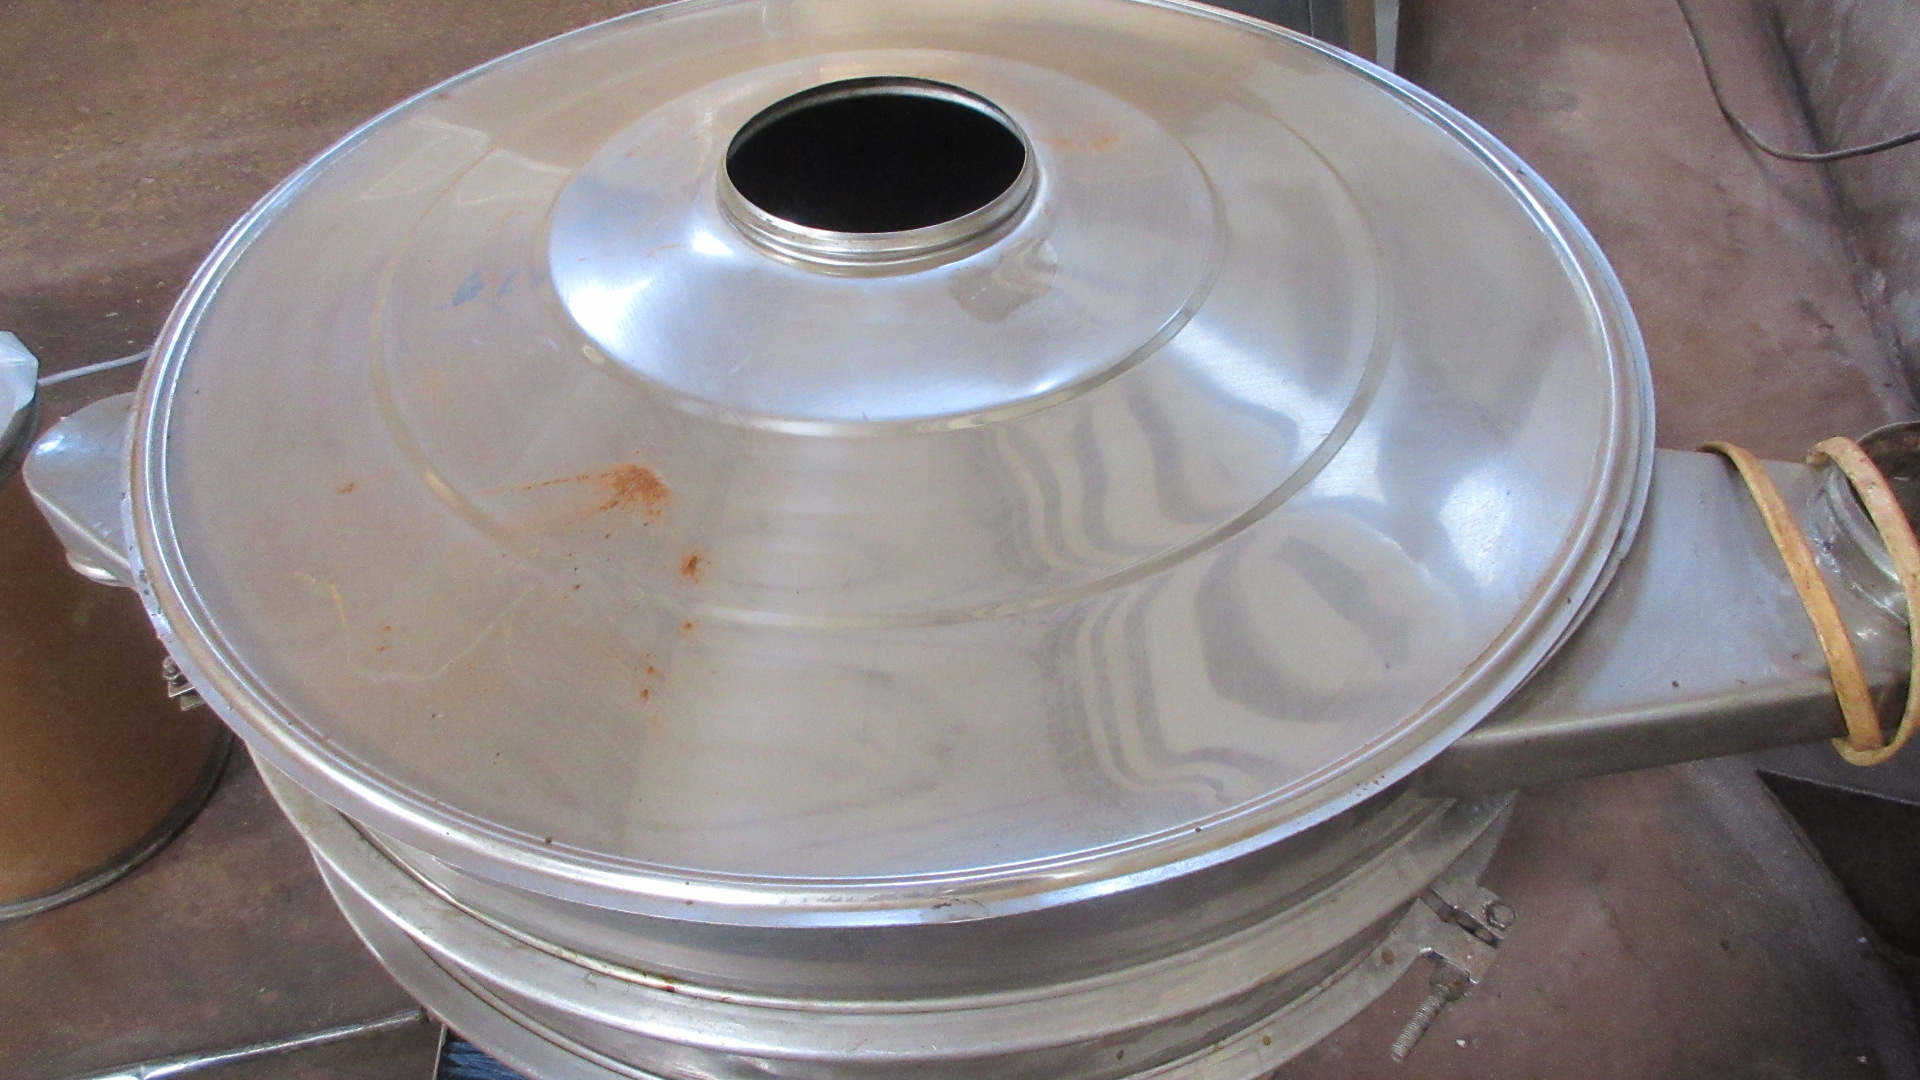
7. Sieving
Screening from 80 mesh up to 450 mesh superfine powder, with integrated metal detection.
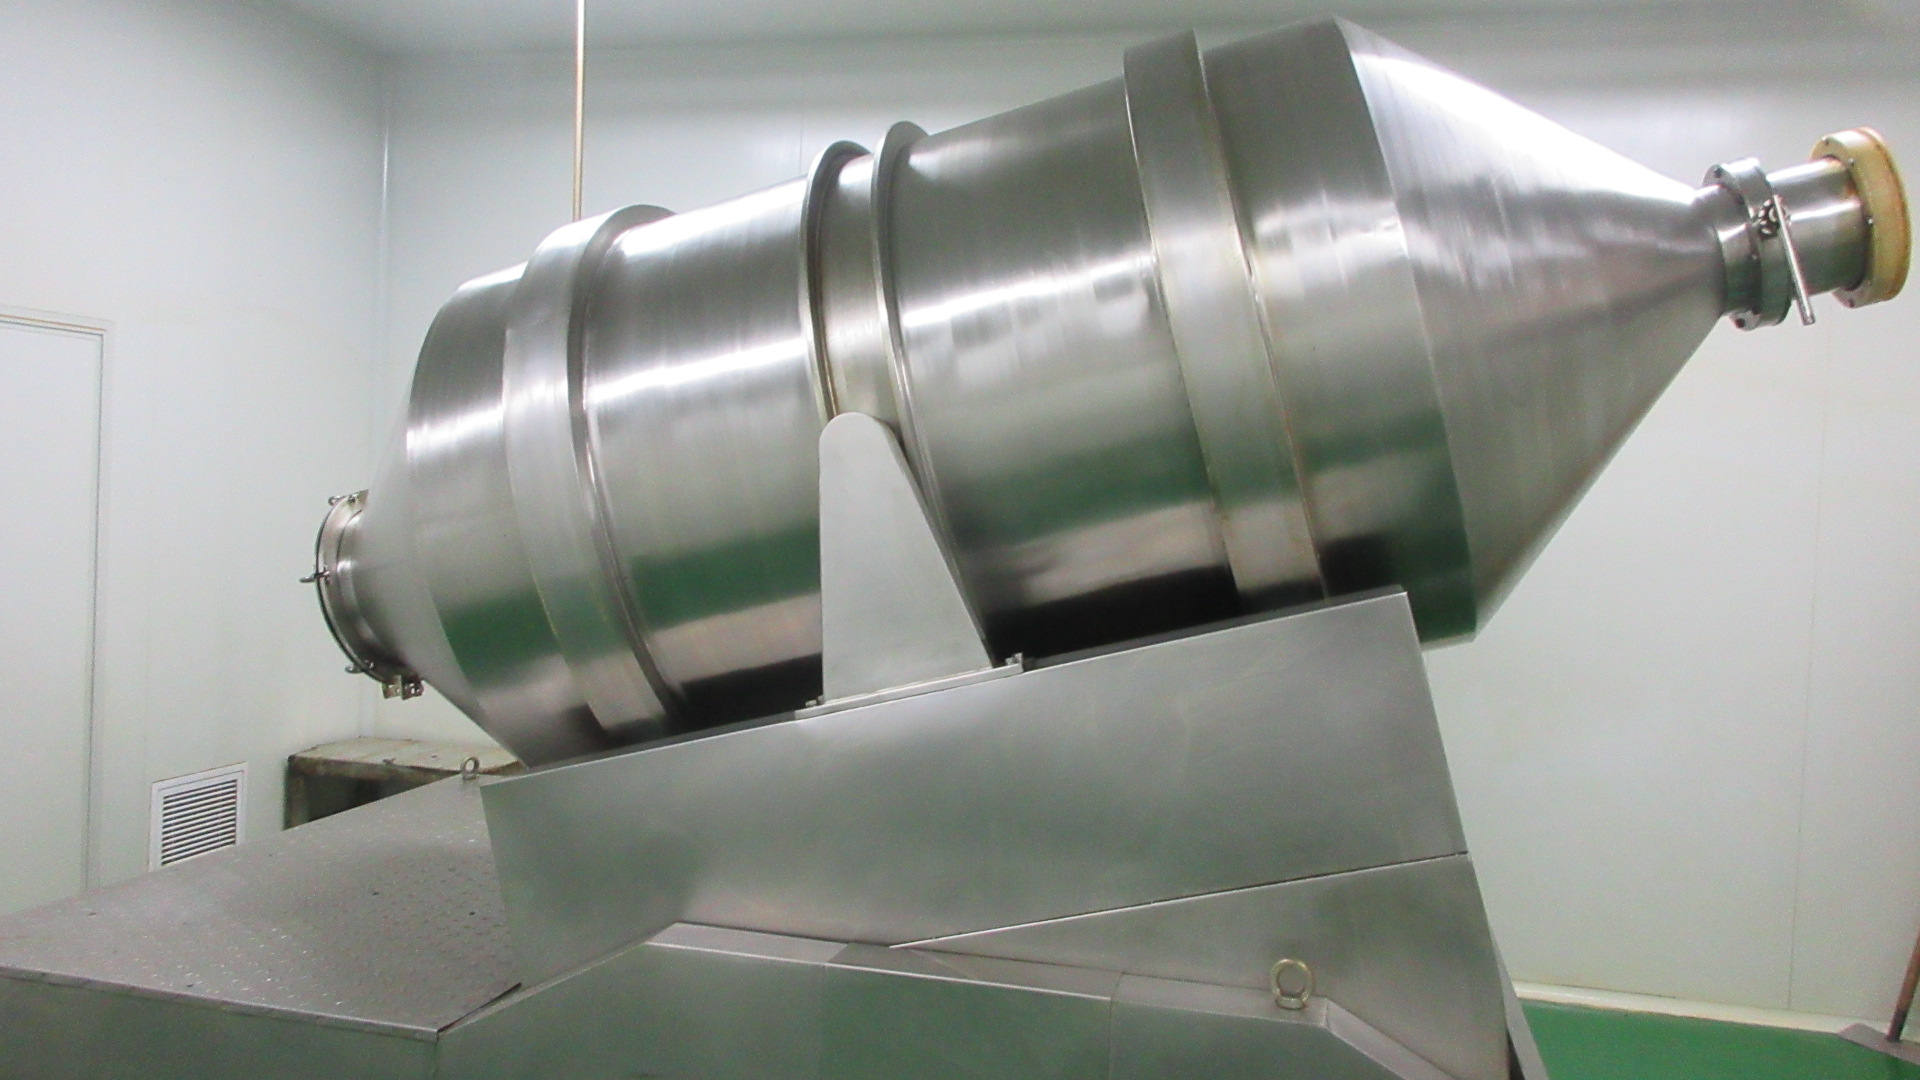
8. Mixing
3D homogeneous powder blending to guarantee uniform active ratios across batch lots.
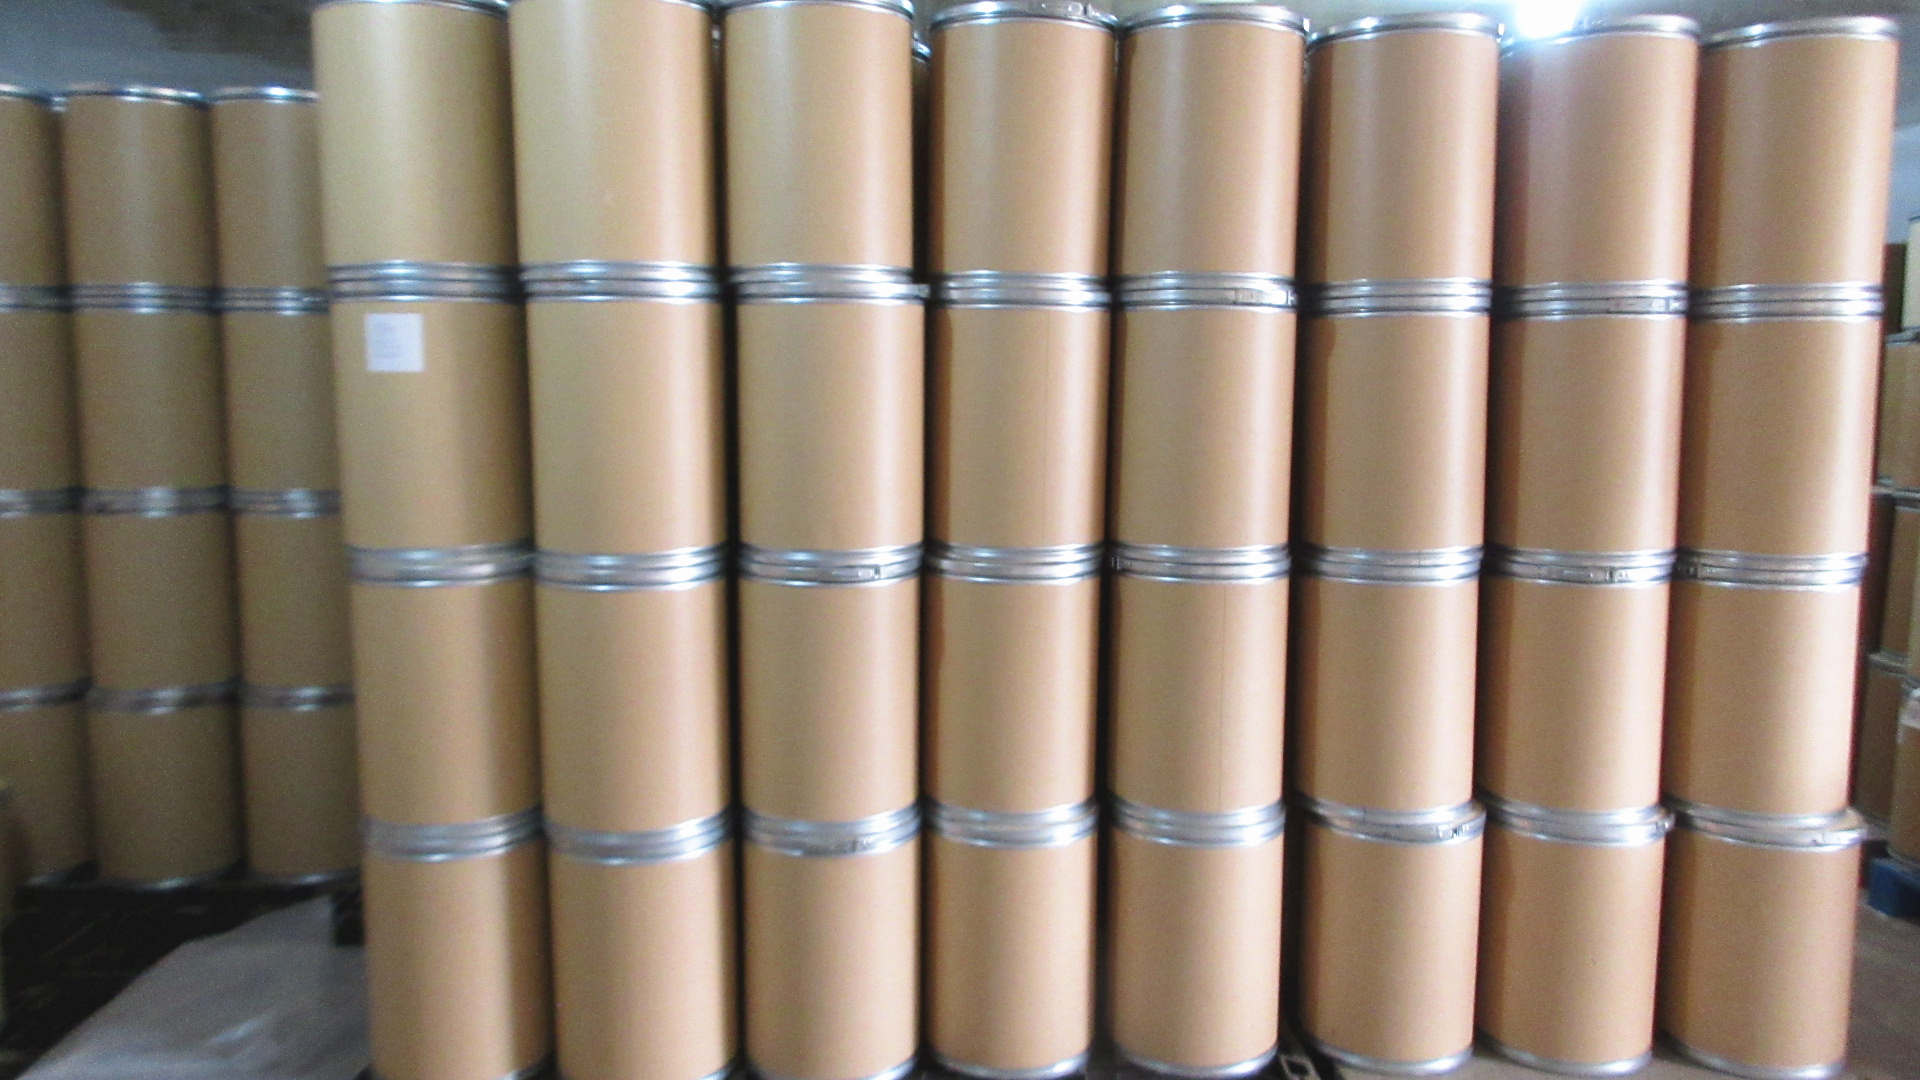
9. Finished Product
Final QC approval, pharmaceutical-grade drum packing, retained sampling, and COA release.
Core Processing Equipment
Modern stainless steel hardware supporting reliable industrial-scale production.
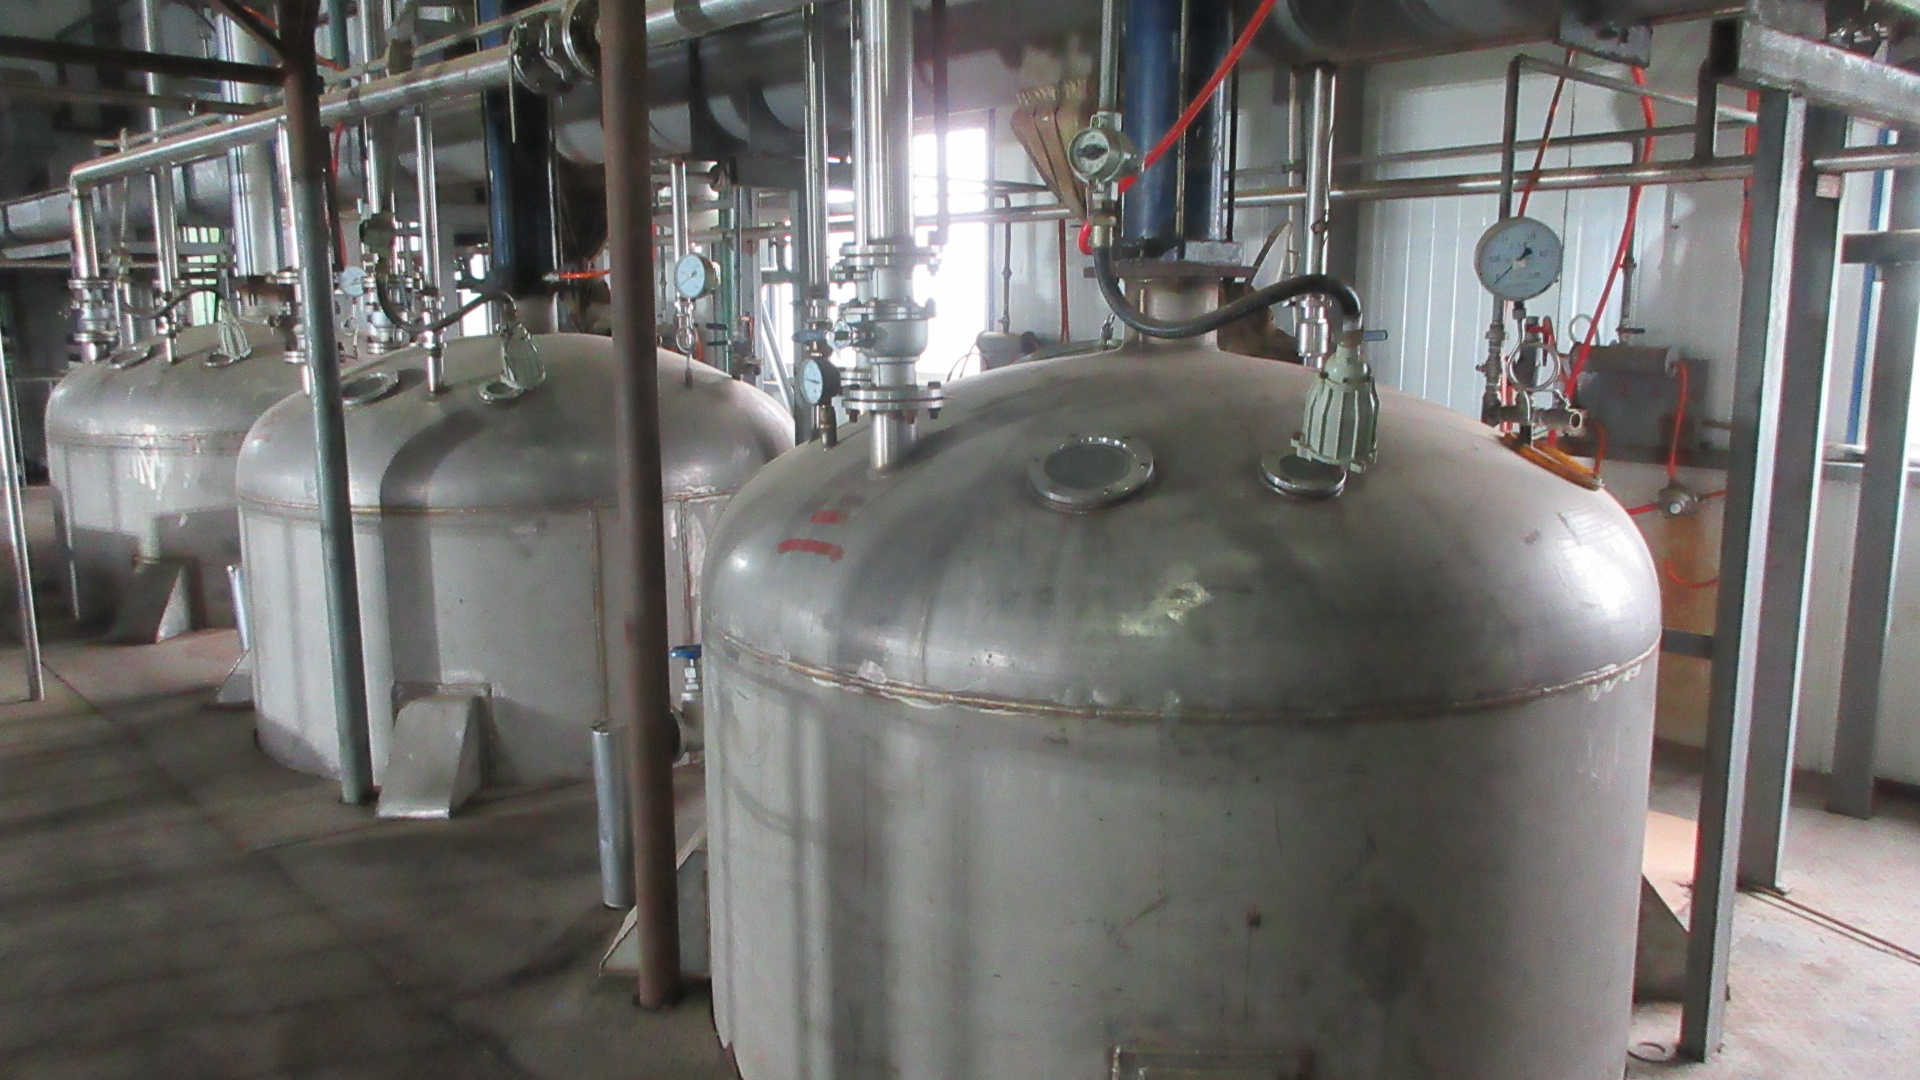
Extracting Tank
Multi-functional dynamic extraction tank for botanical active recovery.
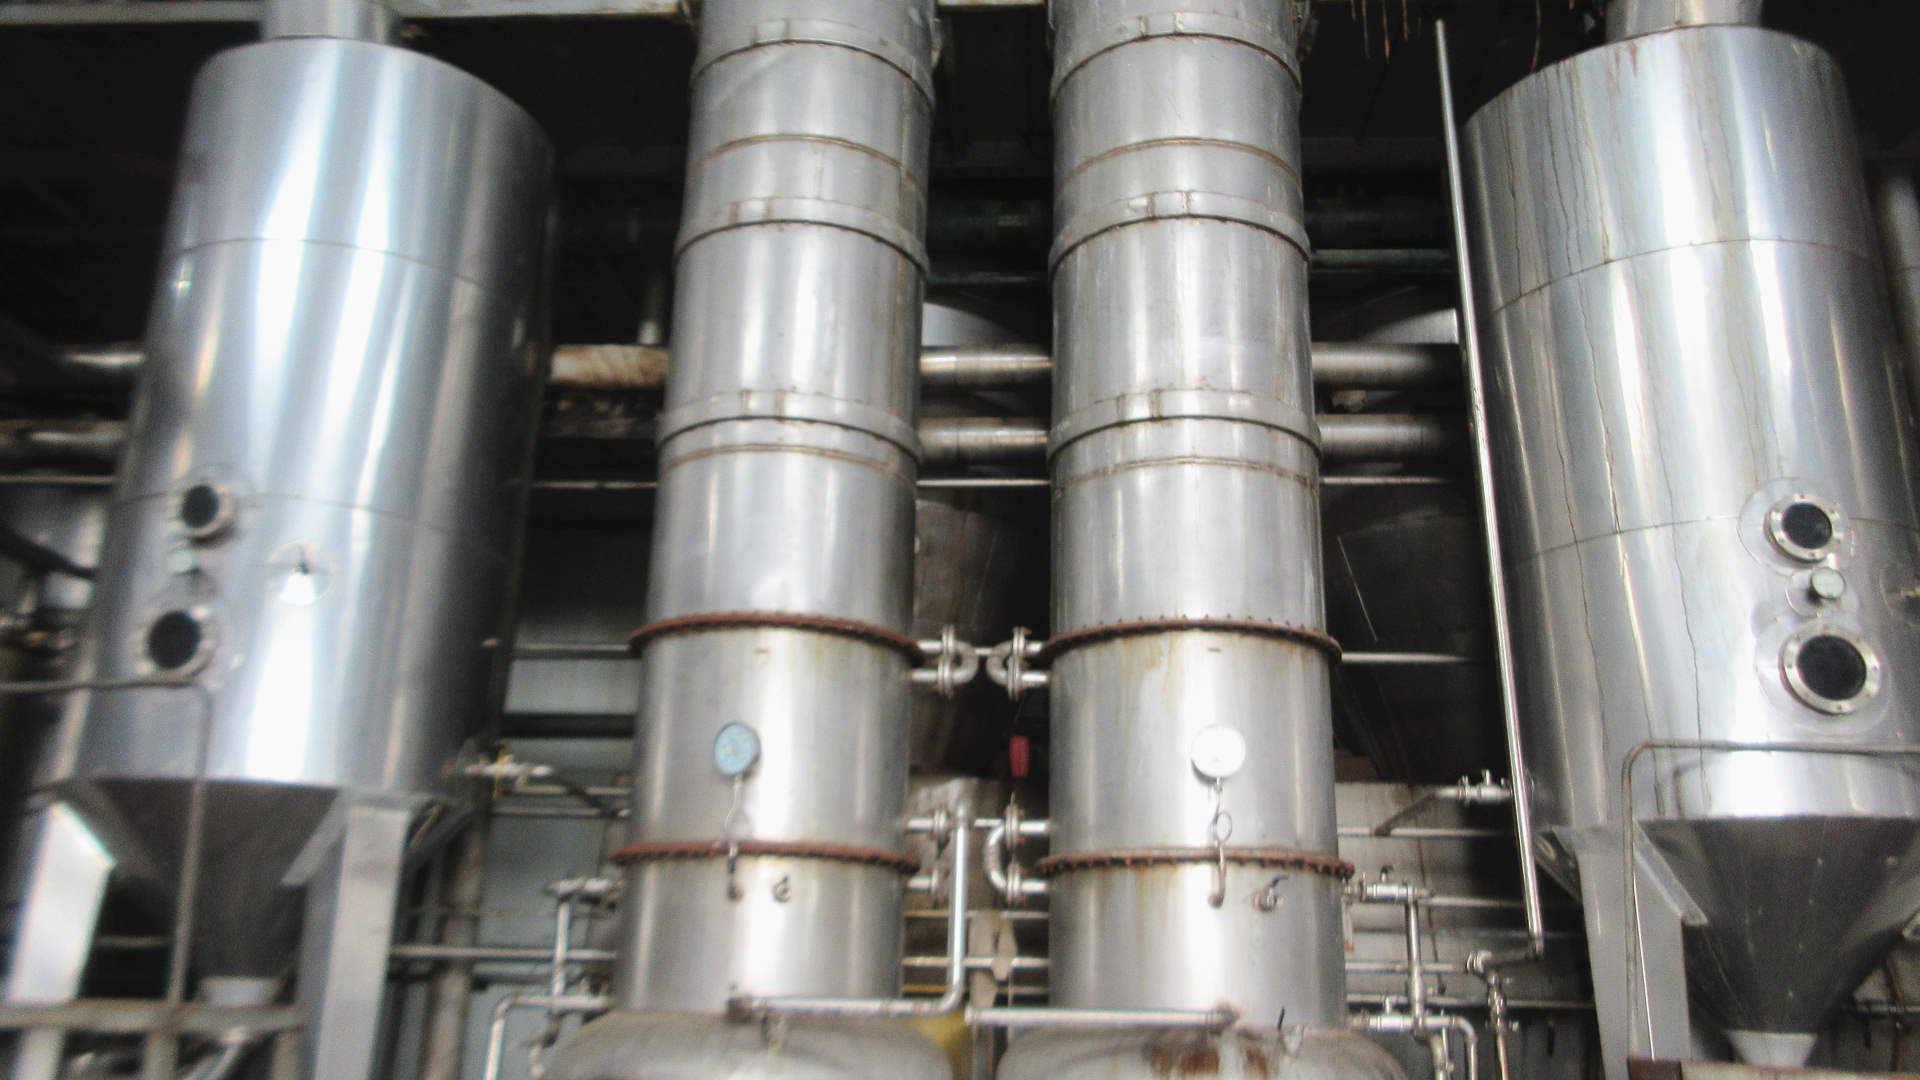
Concentrator
Low-temperature vacuum evaporator maintaining heat-sensitive compounds.
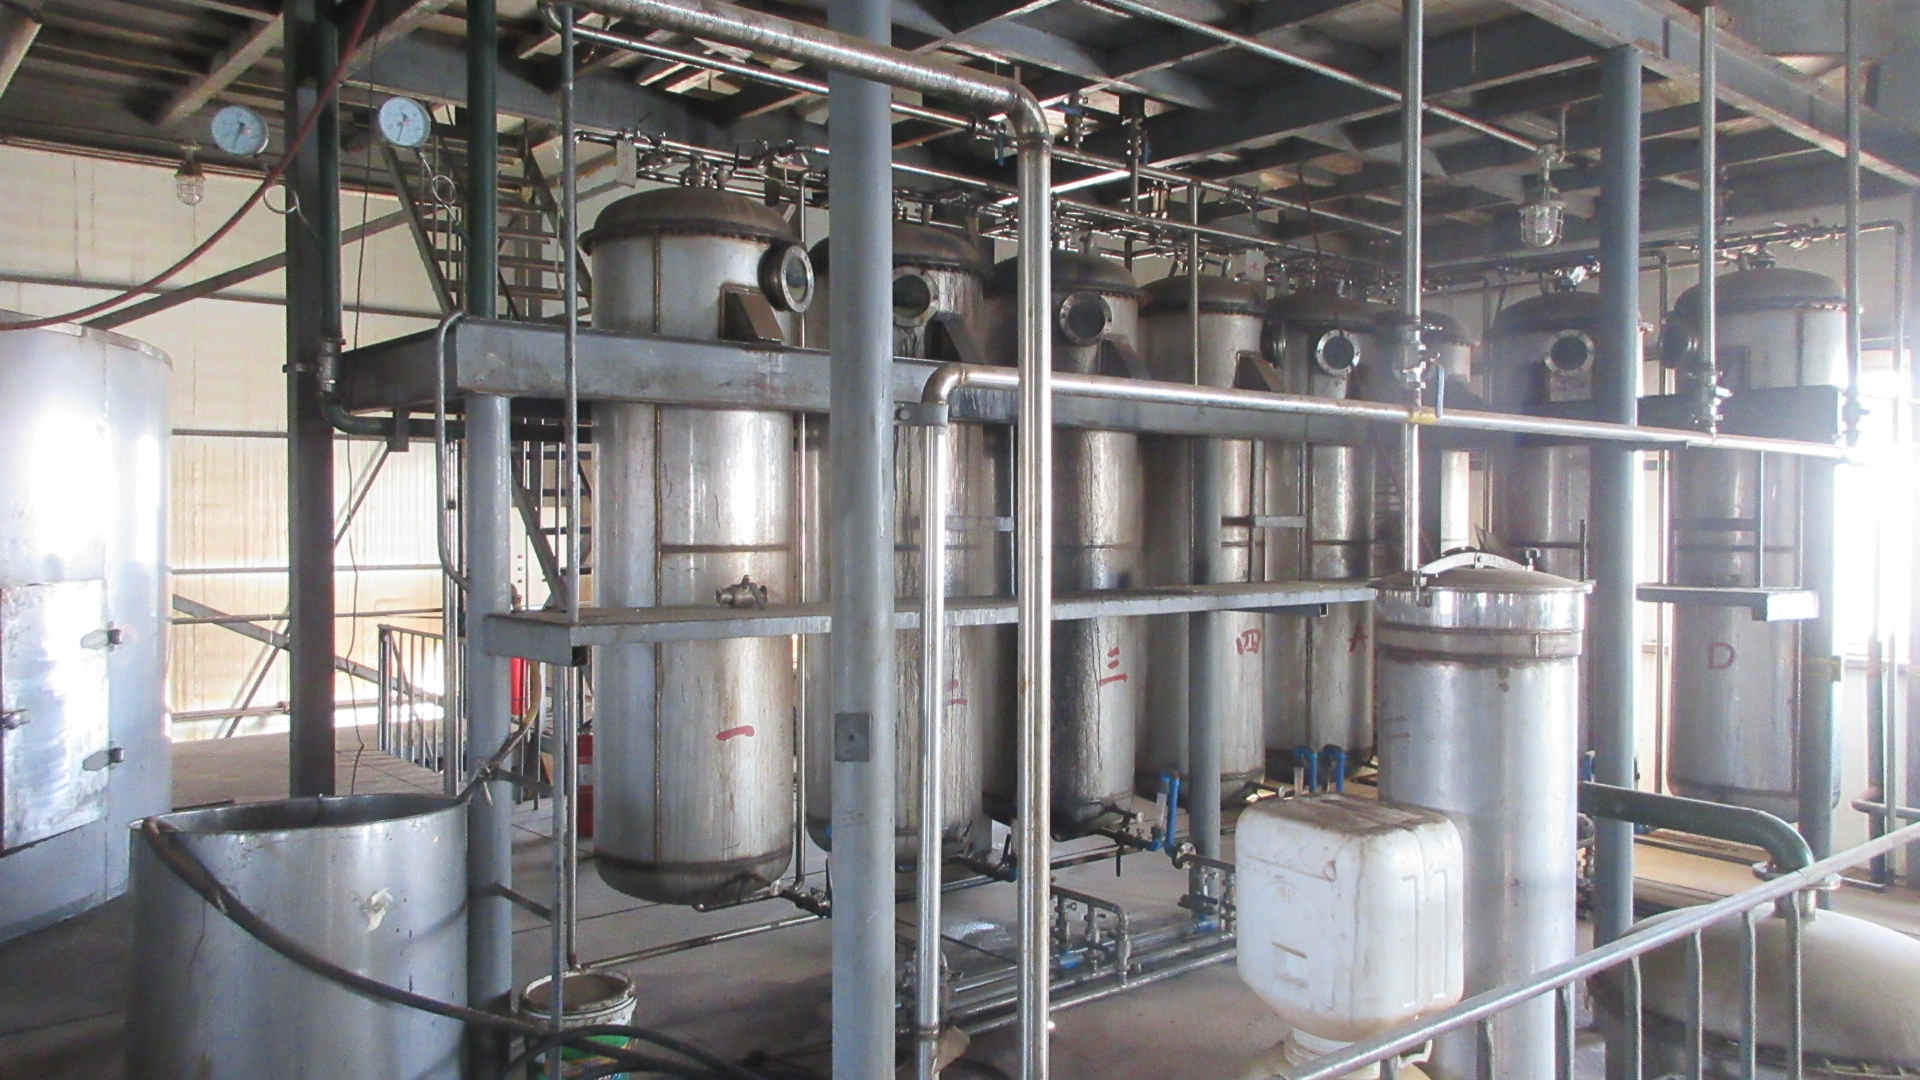
Purification Equipment
Column separation and resin purification for high-assay extract fractions.
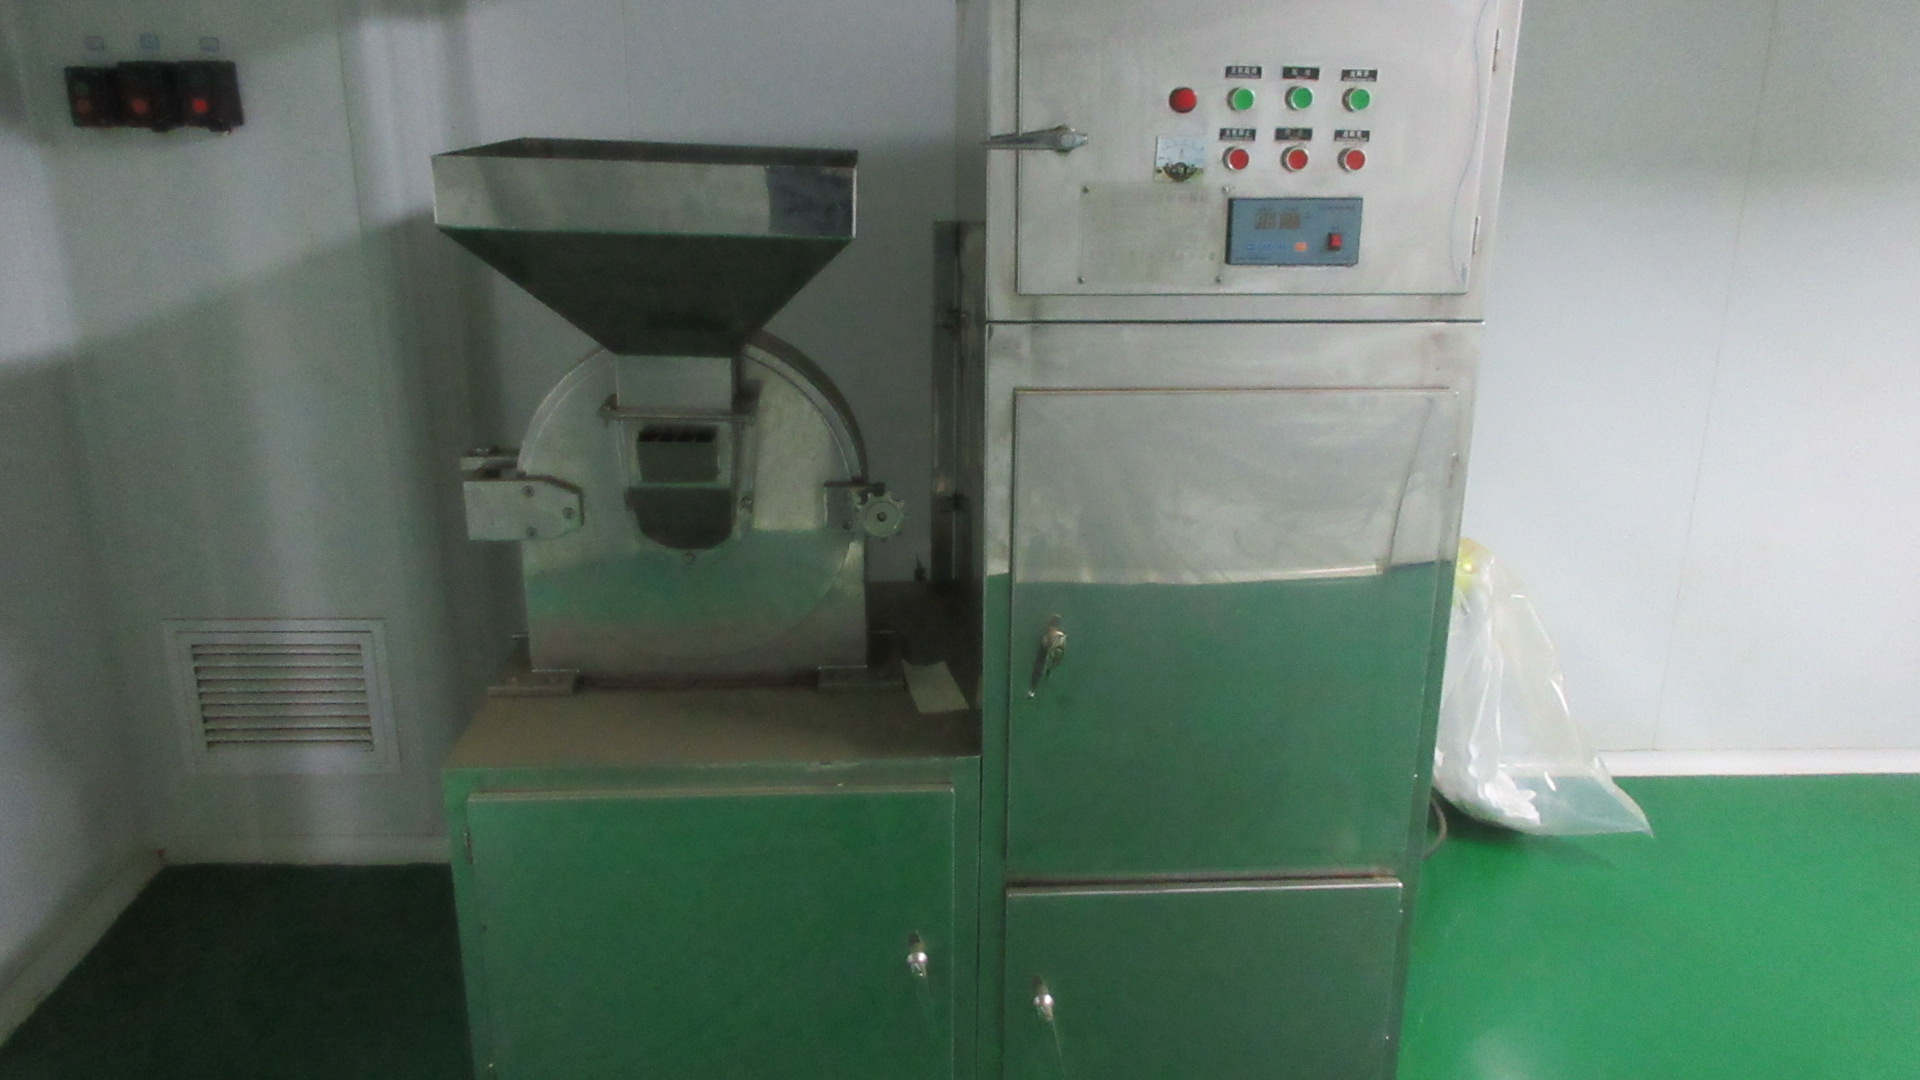
Pulverizer
Controlled particle milling system for uniform powder density.
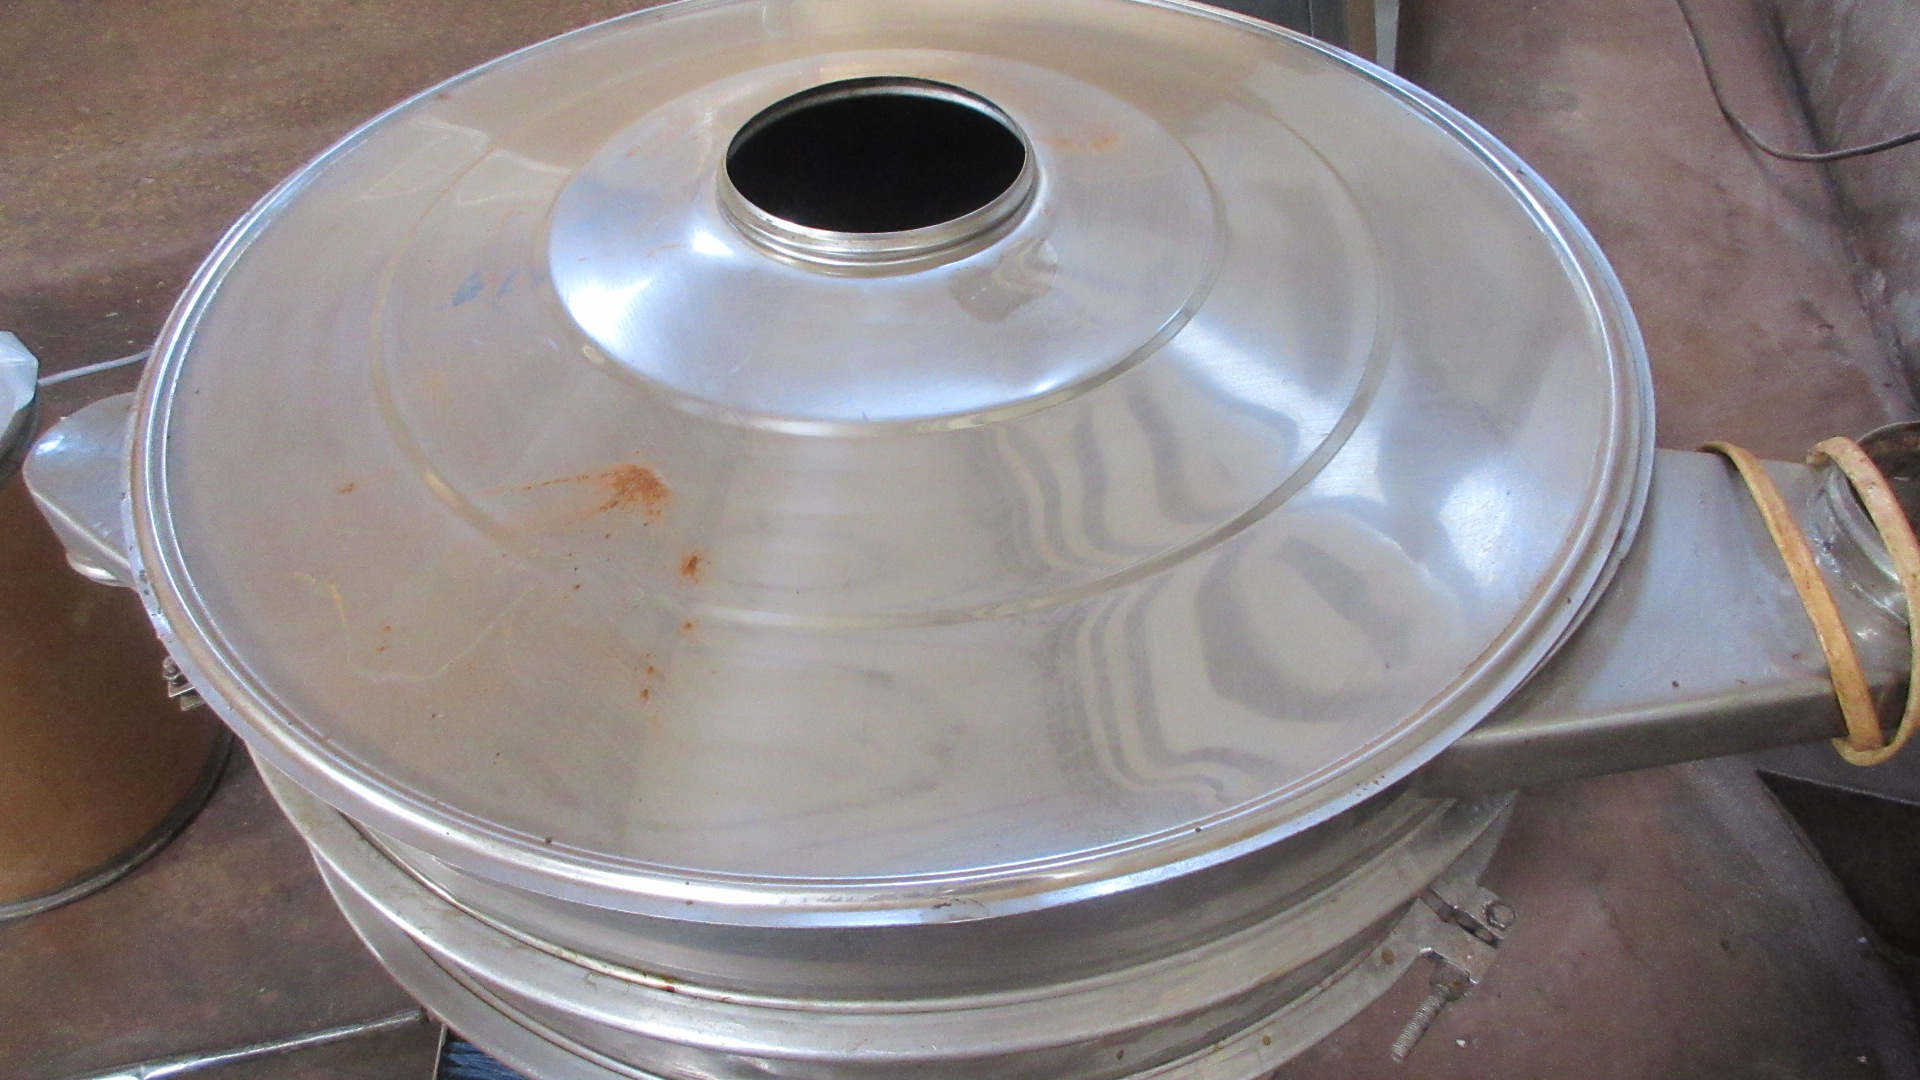
Sieving Machine
Automated mesh grading to meet strict particle size specifications.
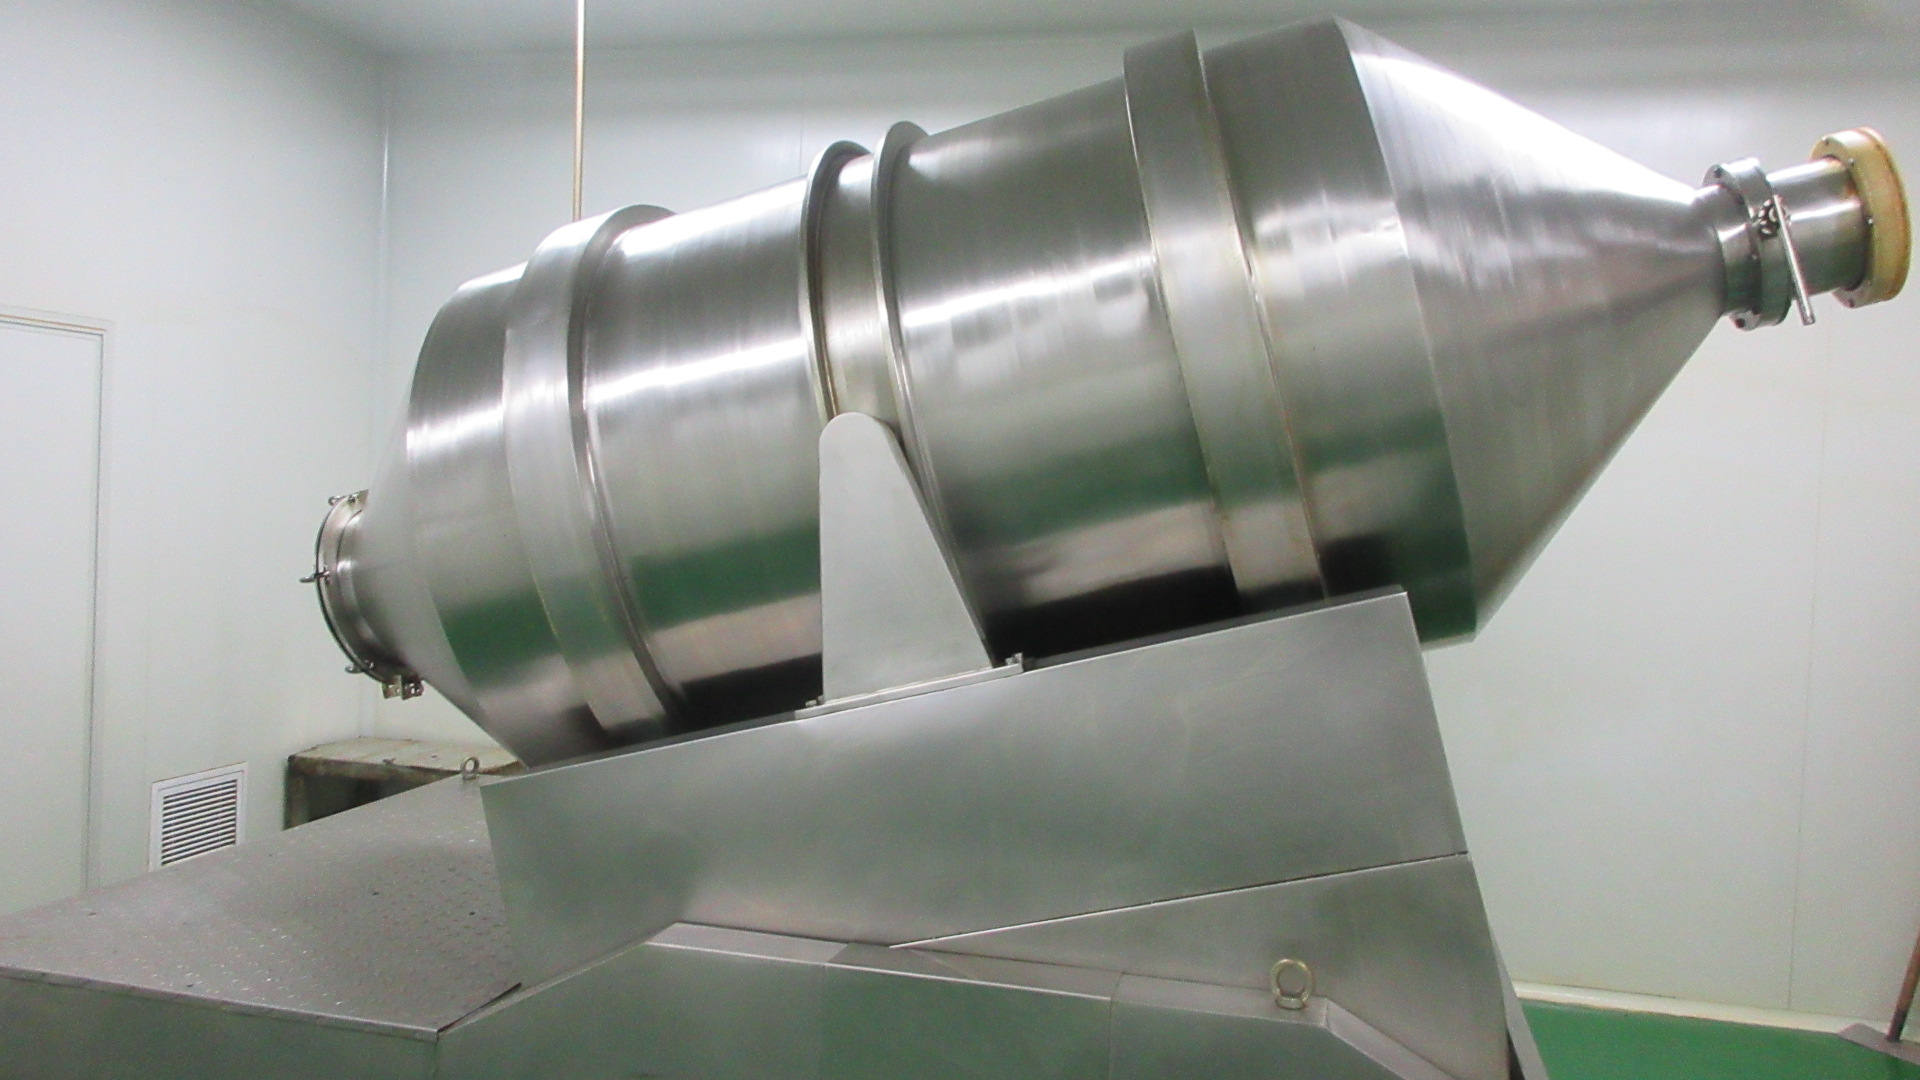
Mixer
High-efficiency blender ensuring uniform lot-to-lot consistency.
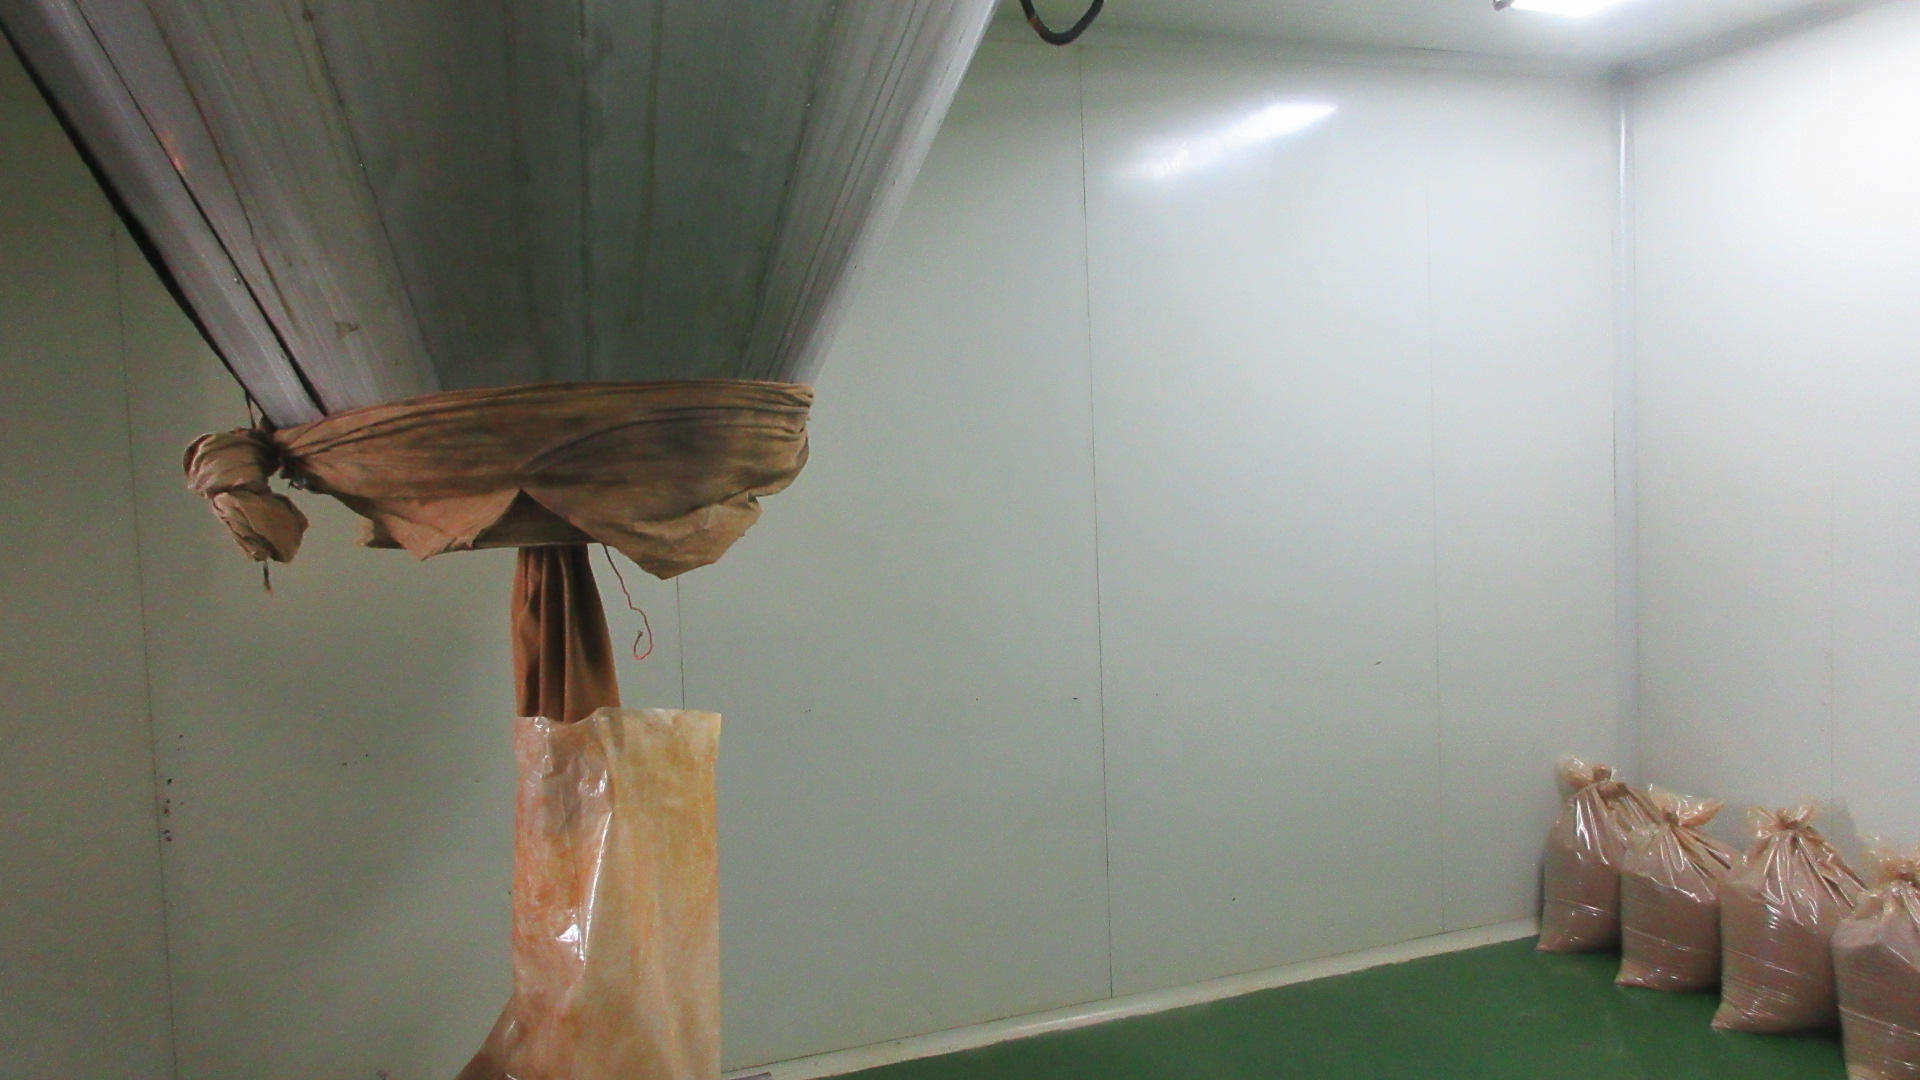
Spraying Tower
Instant spray-drying for excellent water solubility and flow properties.
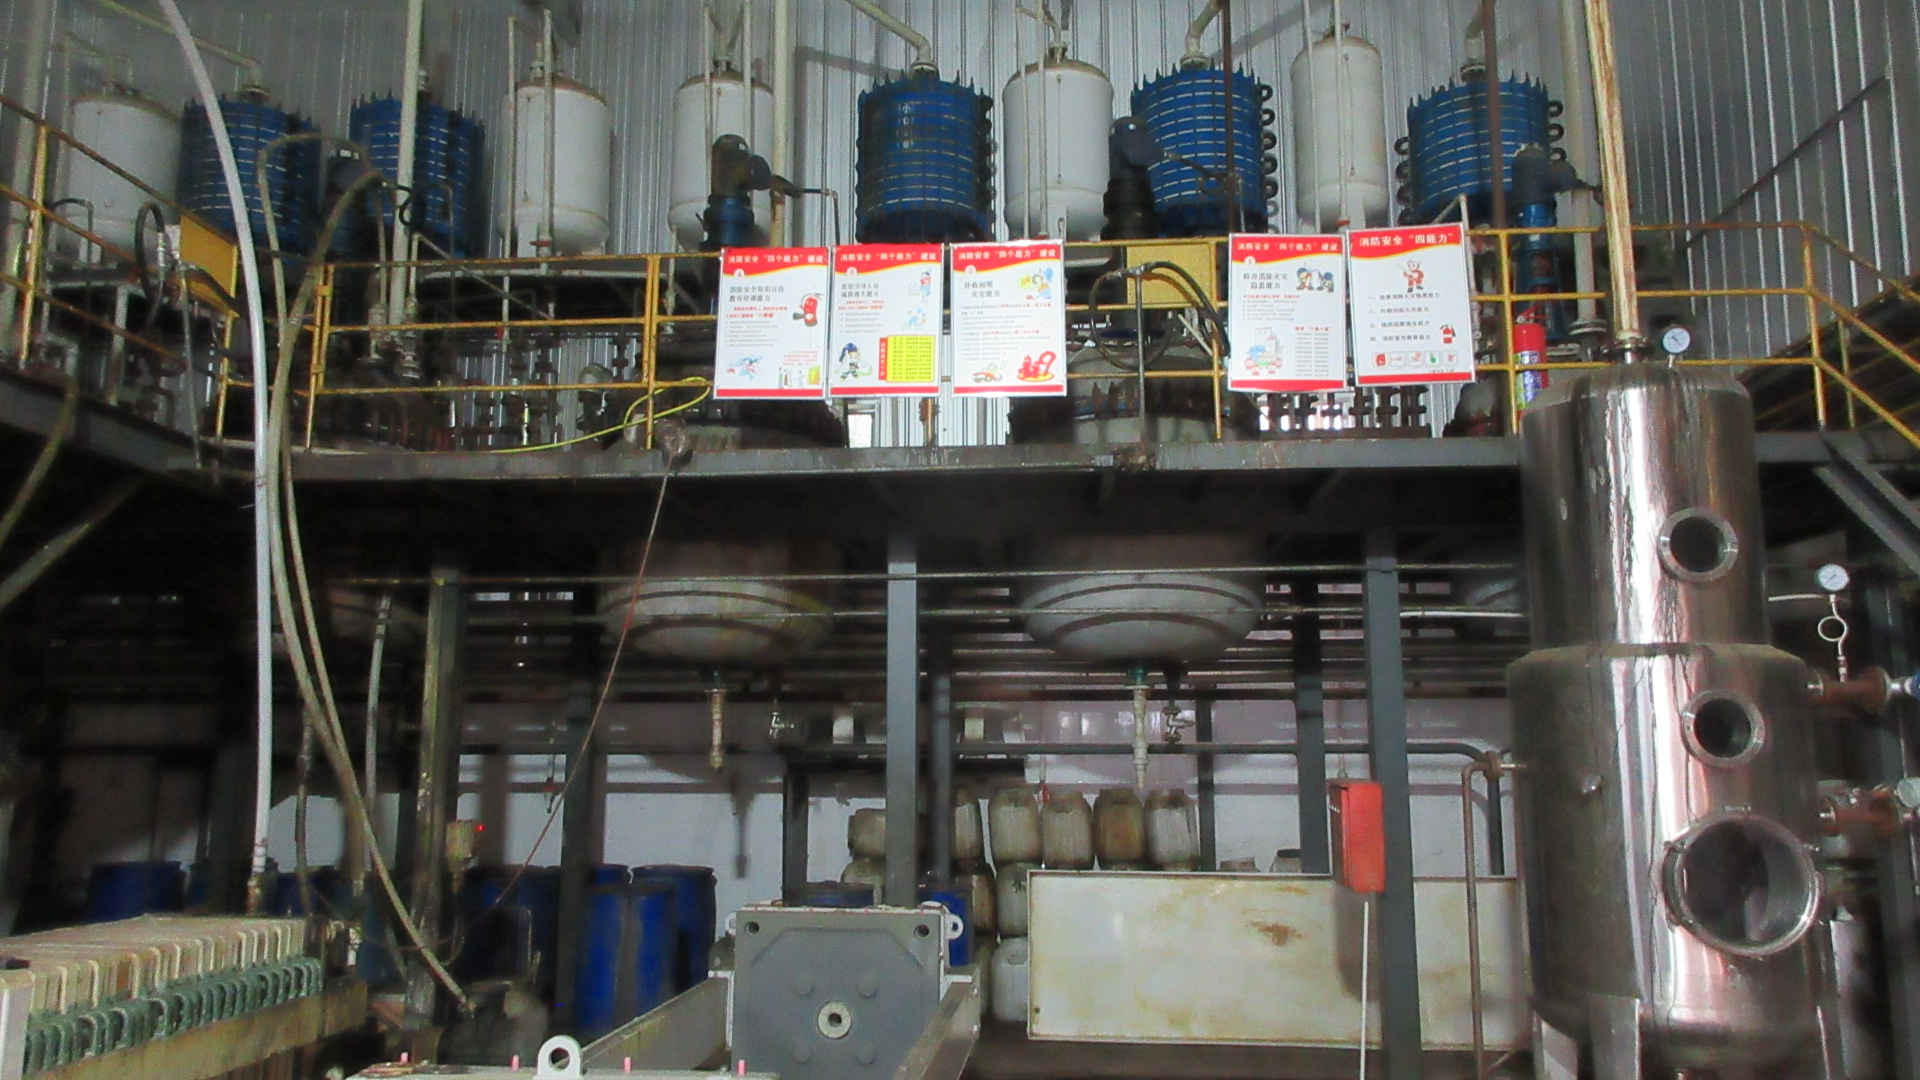
Enamel Reactor
Corrosion-resistant reactor vessel for high-purity chemical reactions.
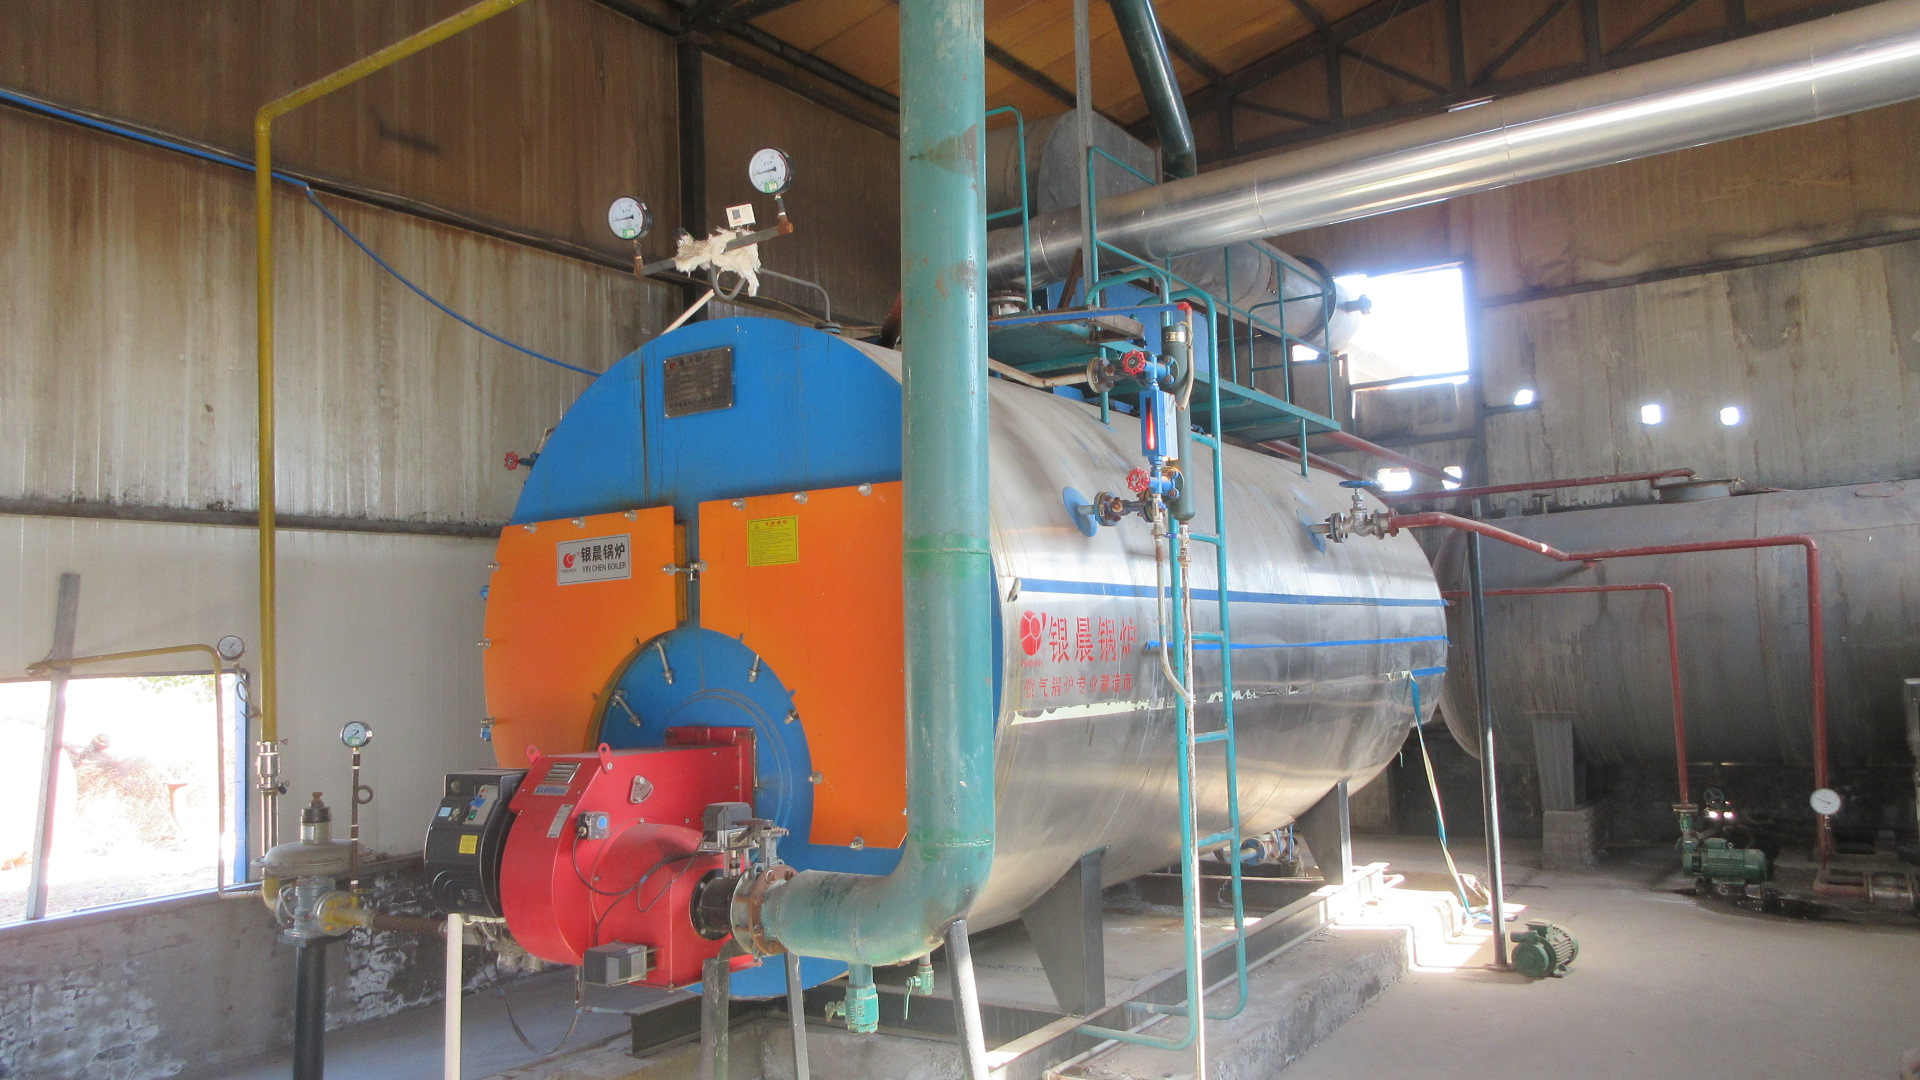
Heating Furnace
Thermal supply system ensuring consistent extraction temperatures.
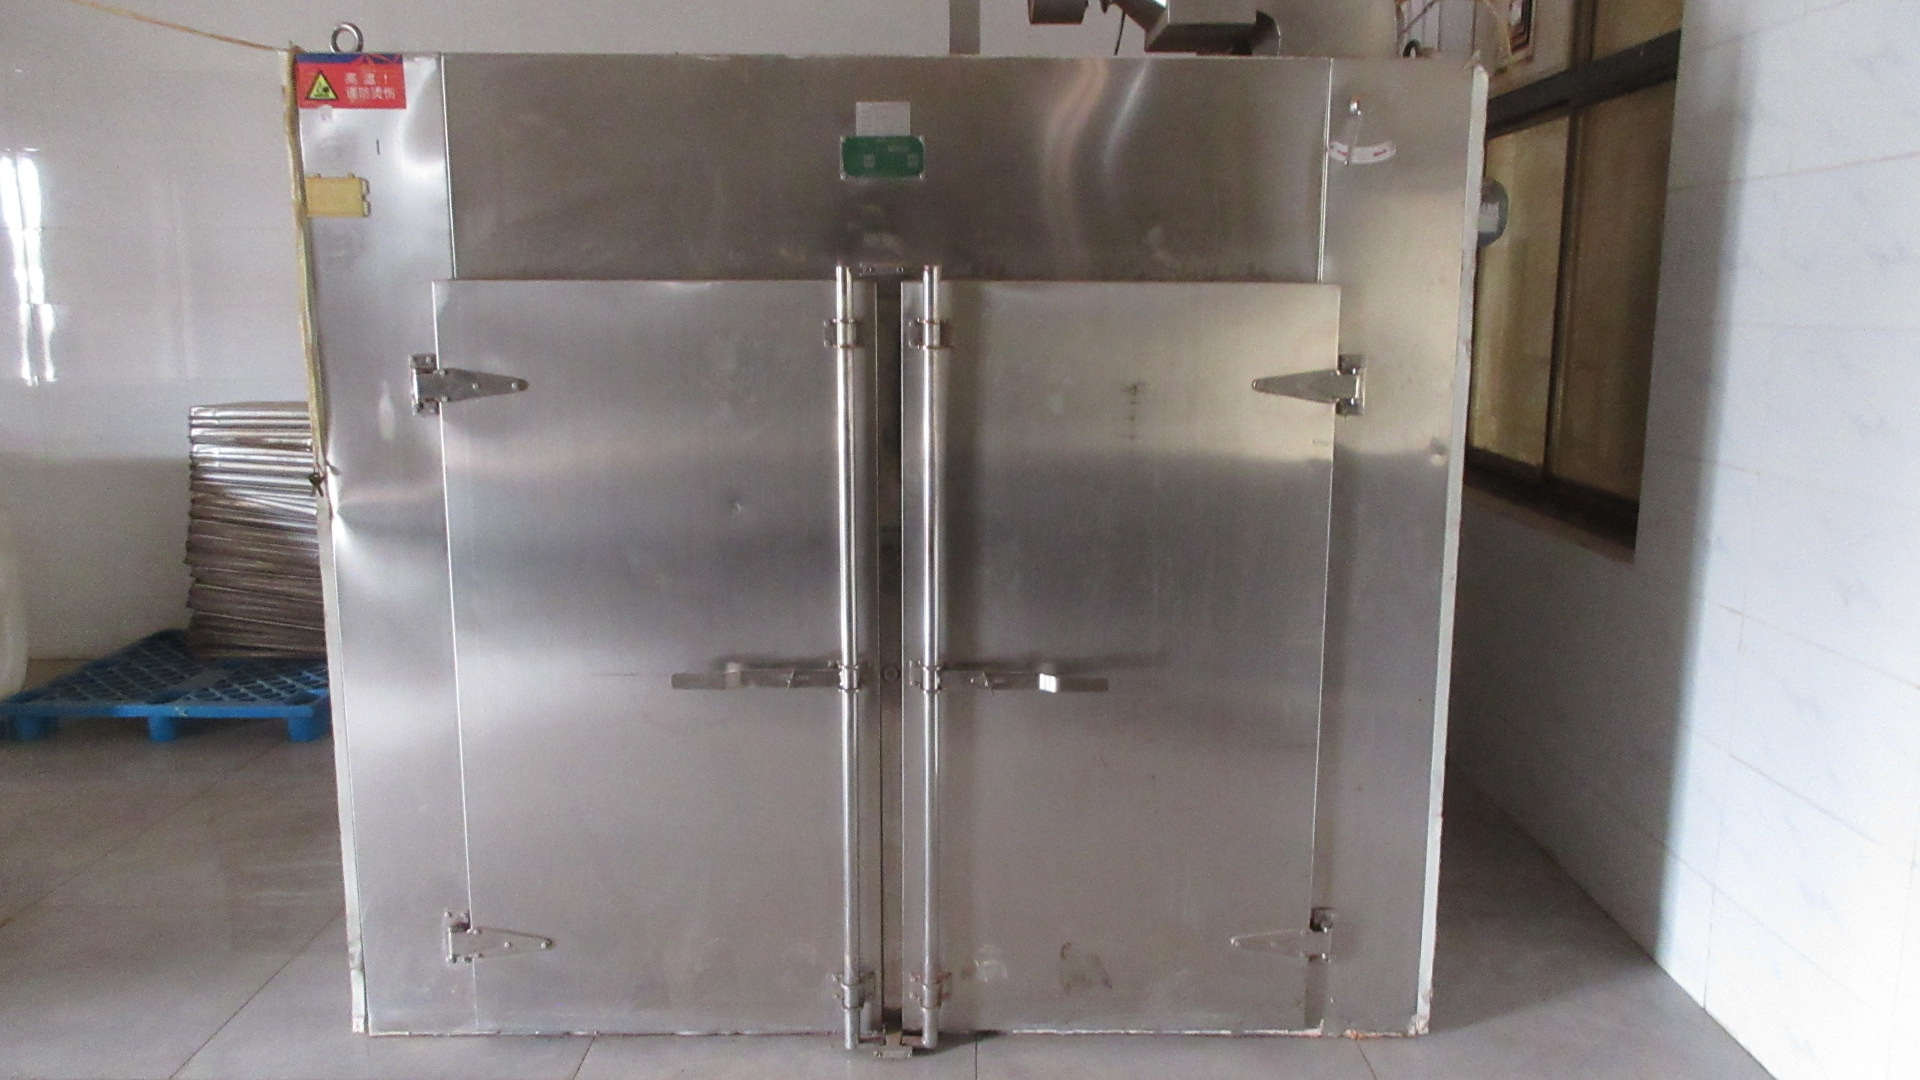
Dryer
Precision temperature drying chamber for moisture-sensitive active powders.
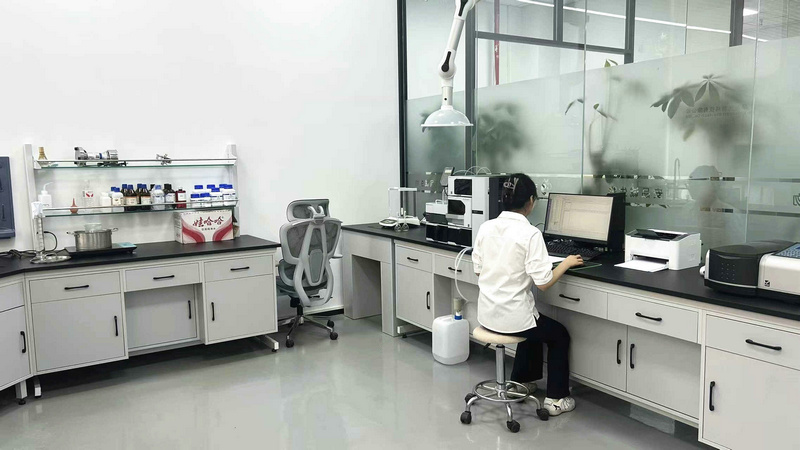
In-House Laboratory & Testing Instrumentation
Every lot is analyzed for purity, heavy metals, microbial safety, and active compound assays.
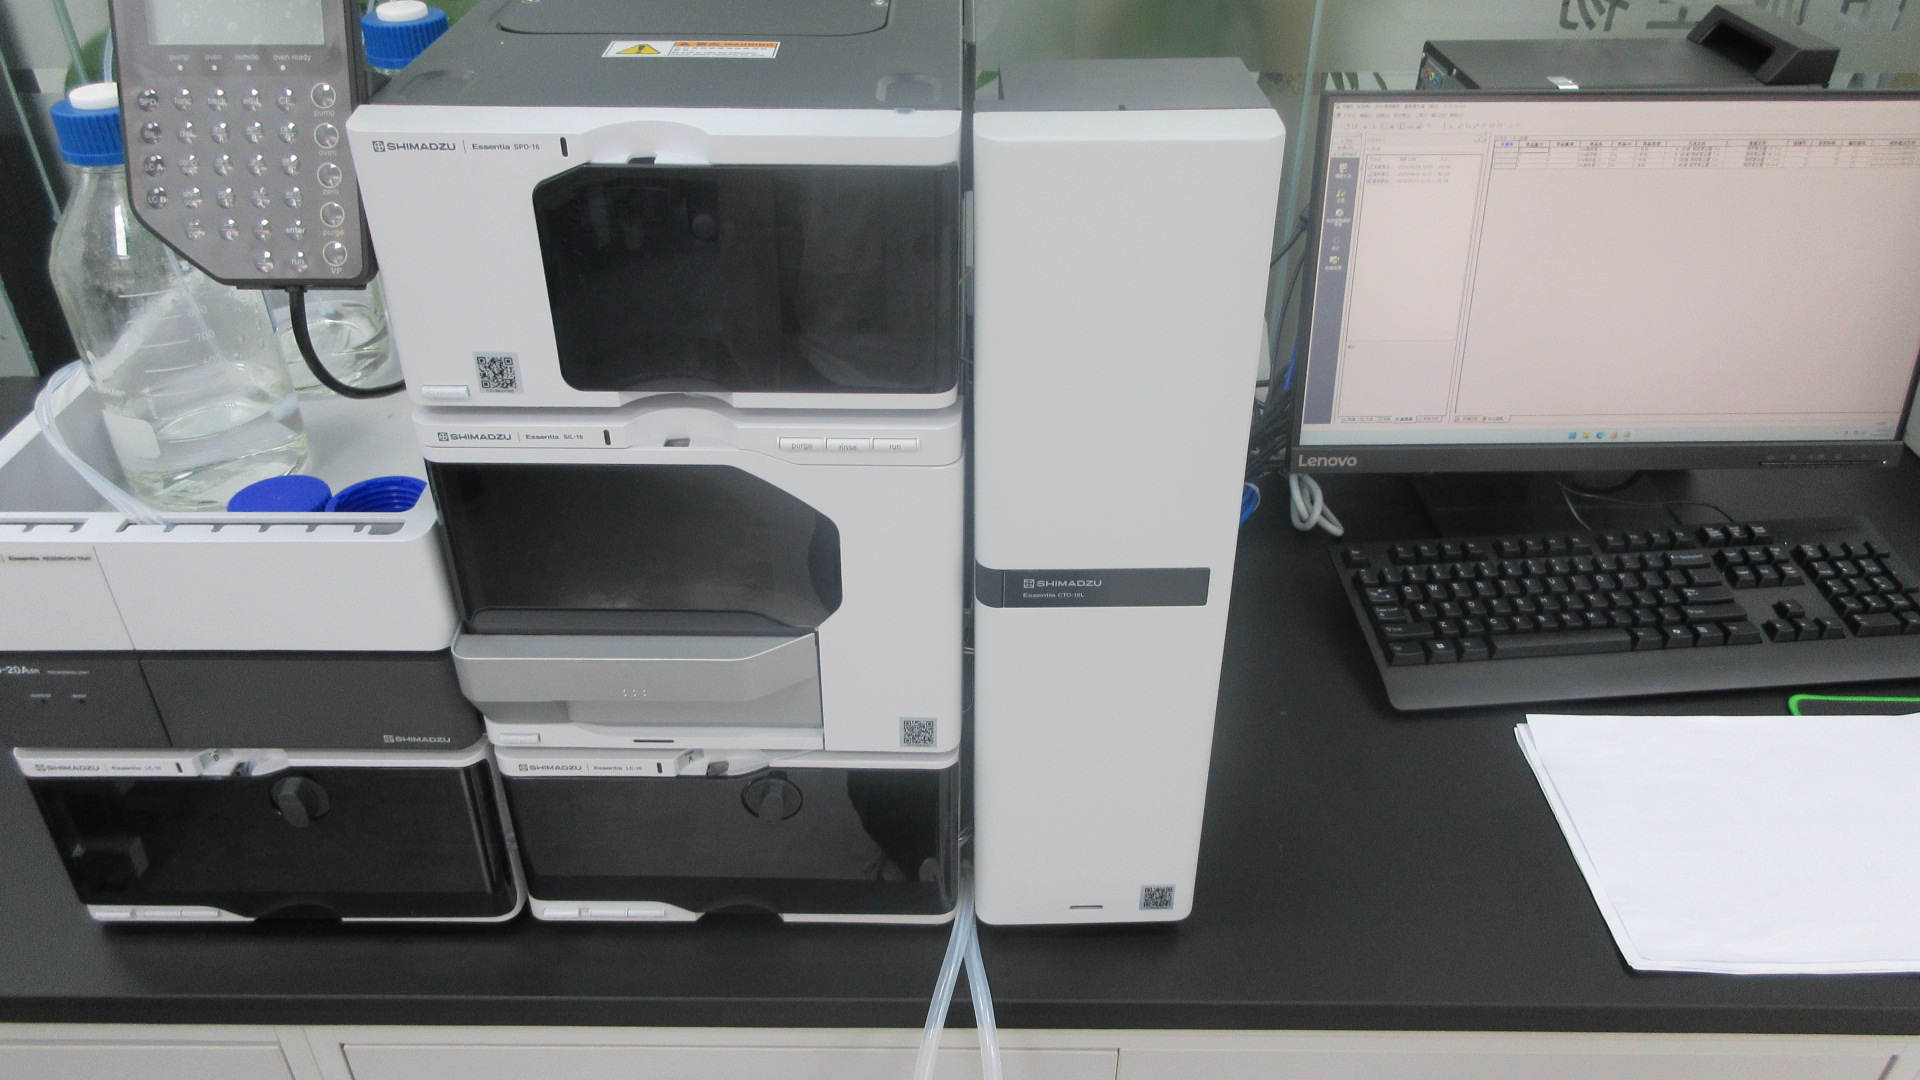
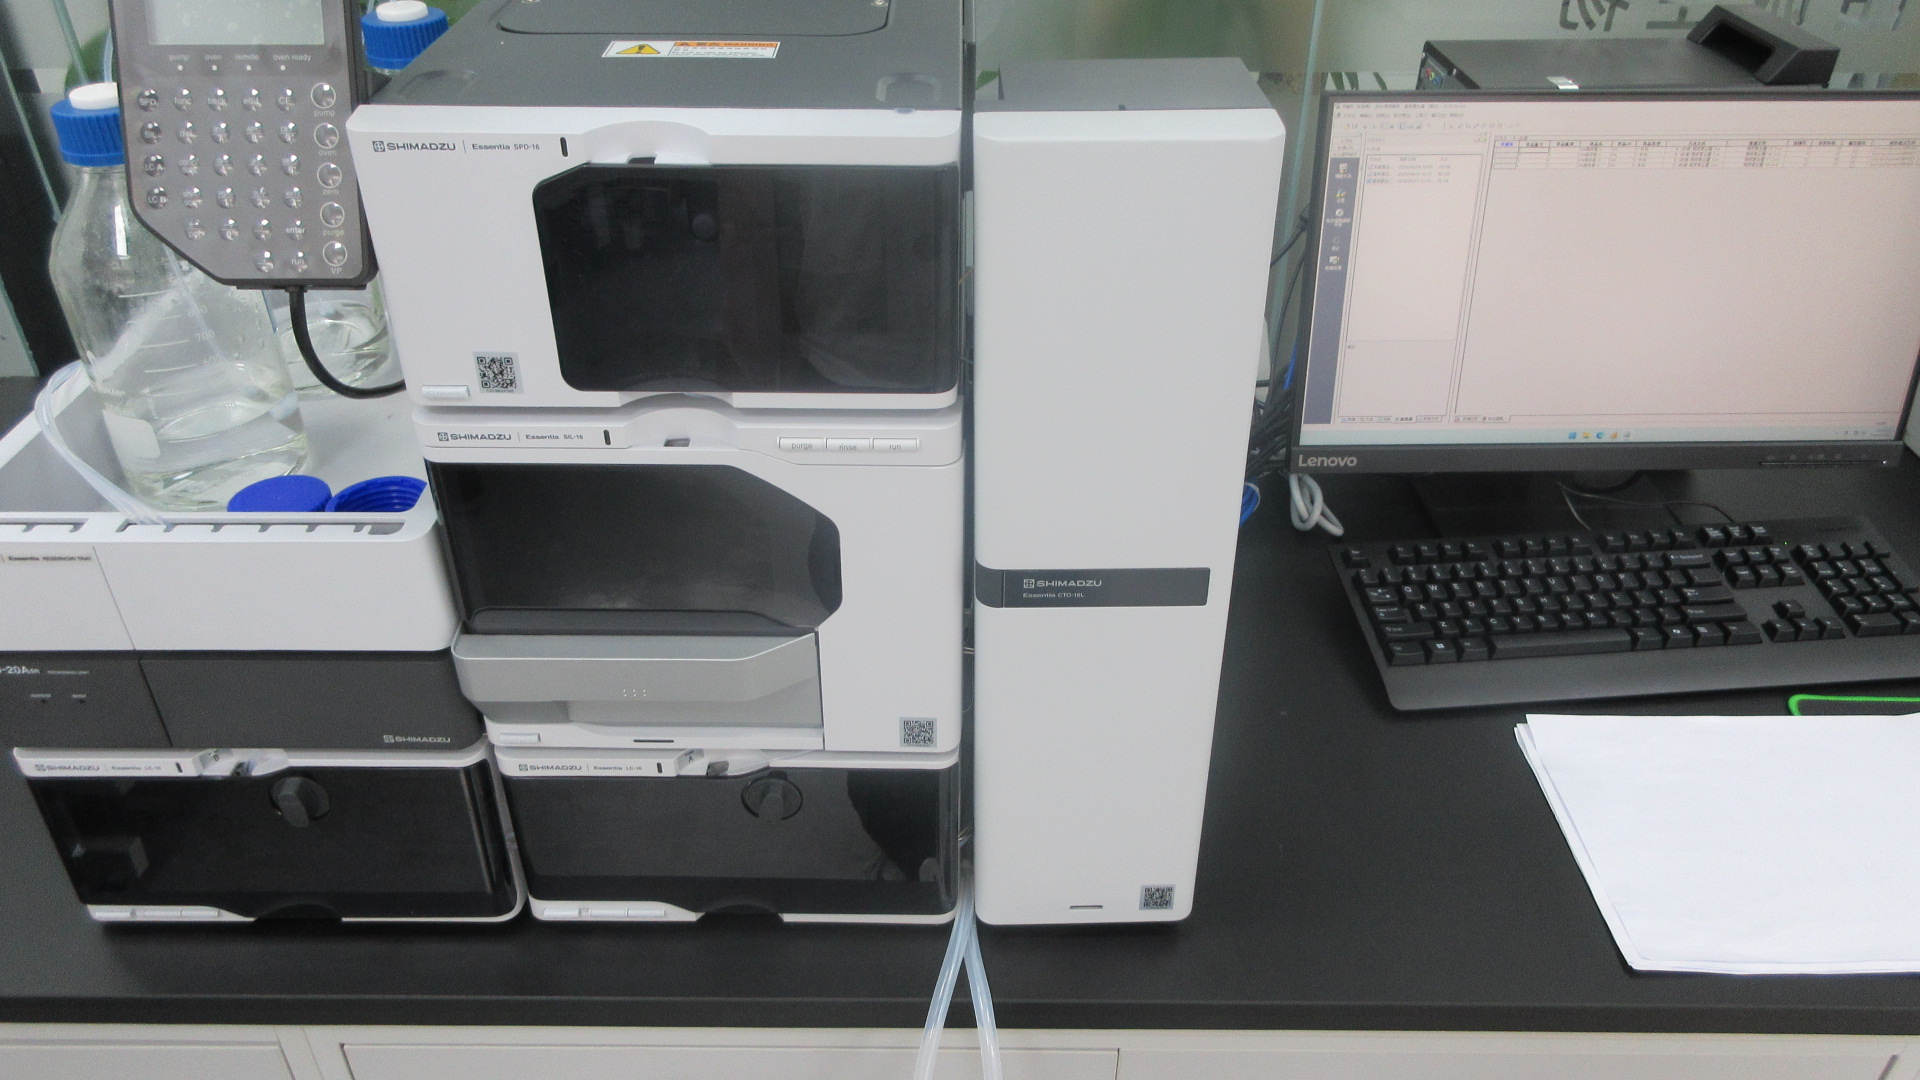
HPLC Analysis
Precise quantification of active compounds (NMN, NAD+, Glutathione, Mogrosides).
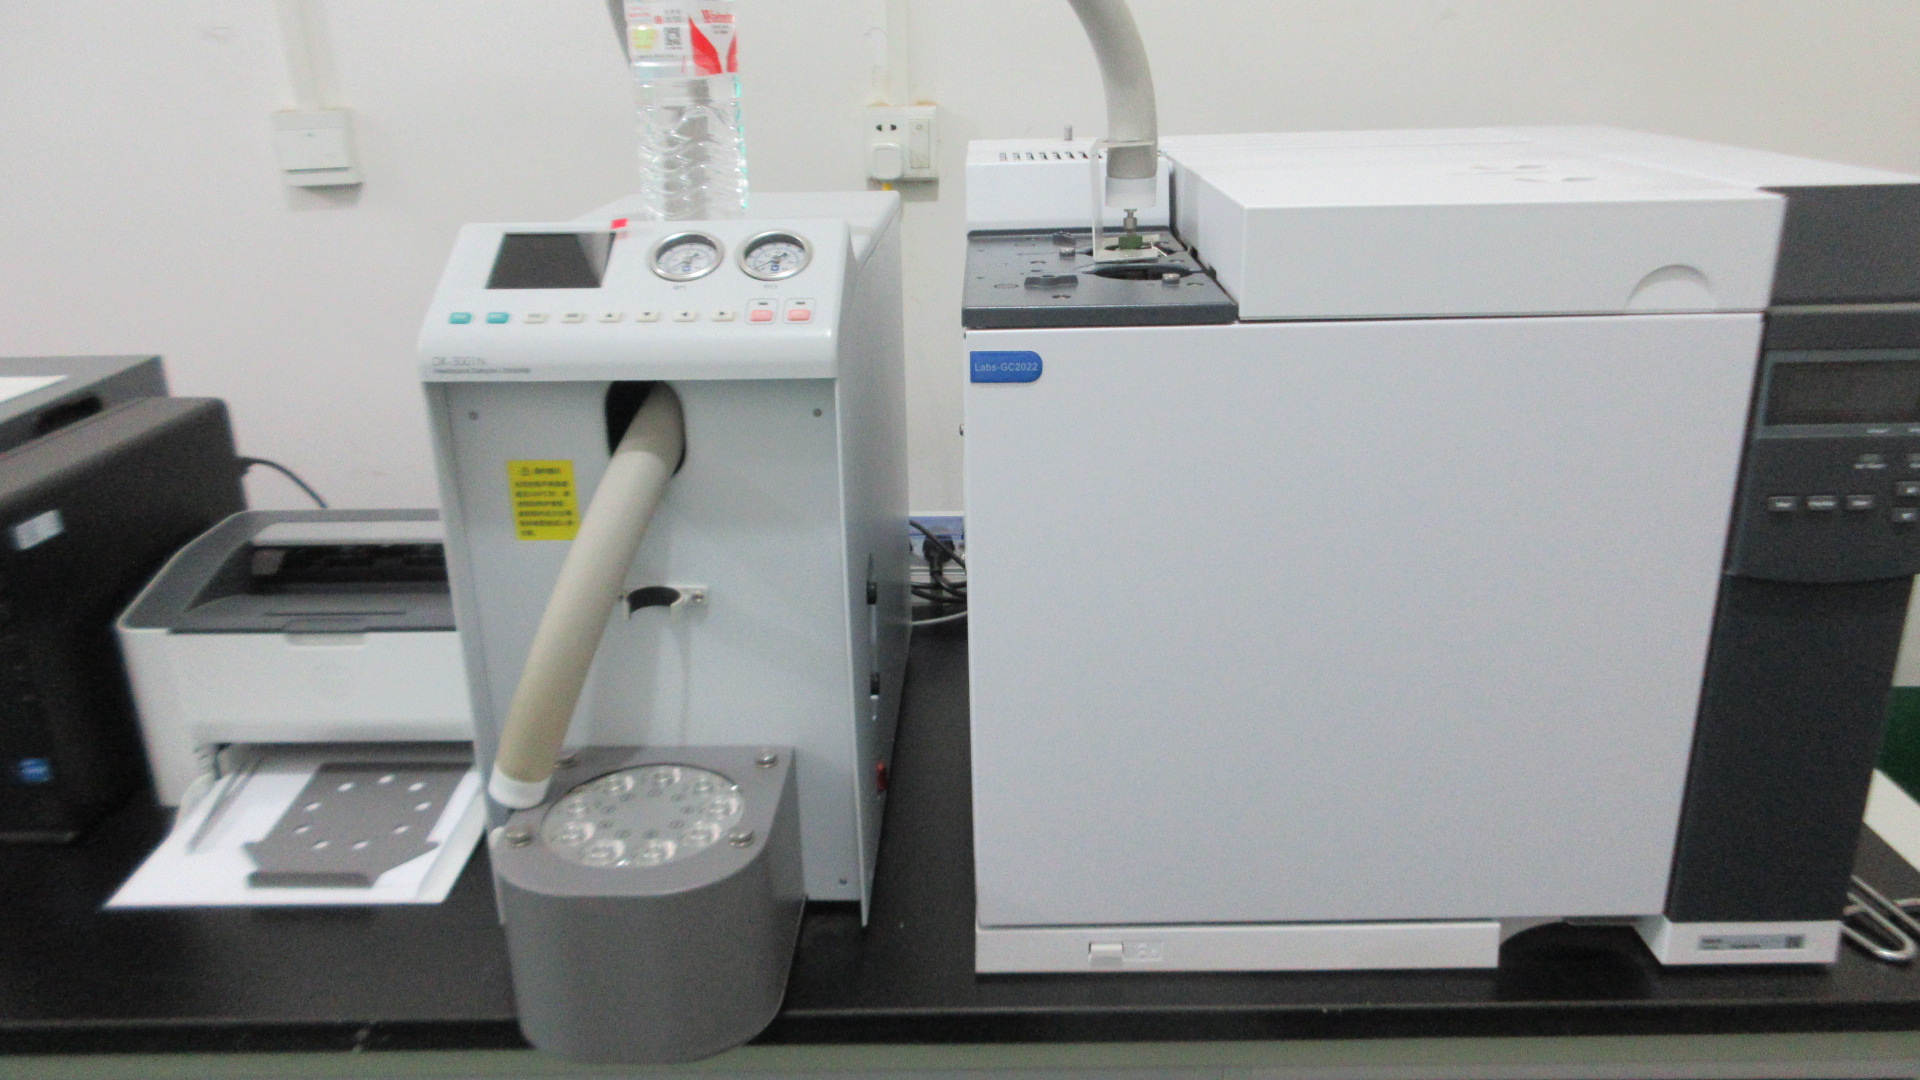
Gas Chromatography (GC)
Screening for residual solvents and volatile trace impurities.
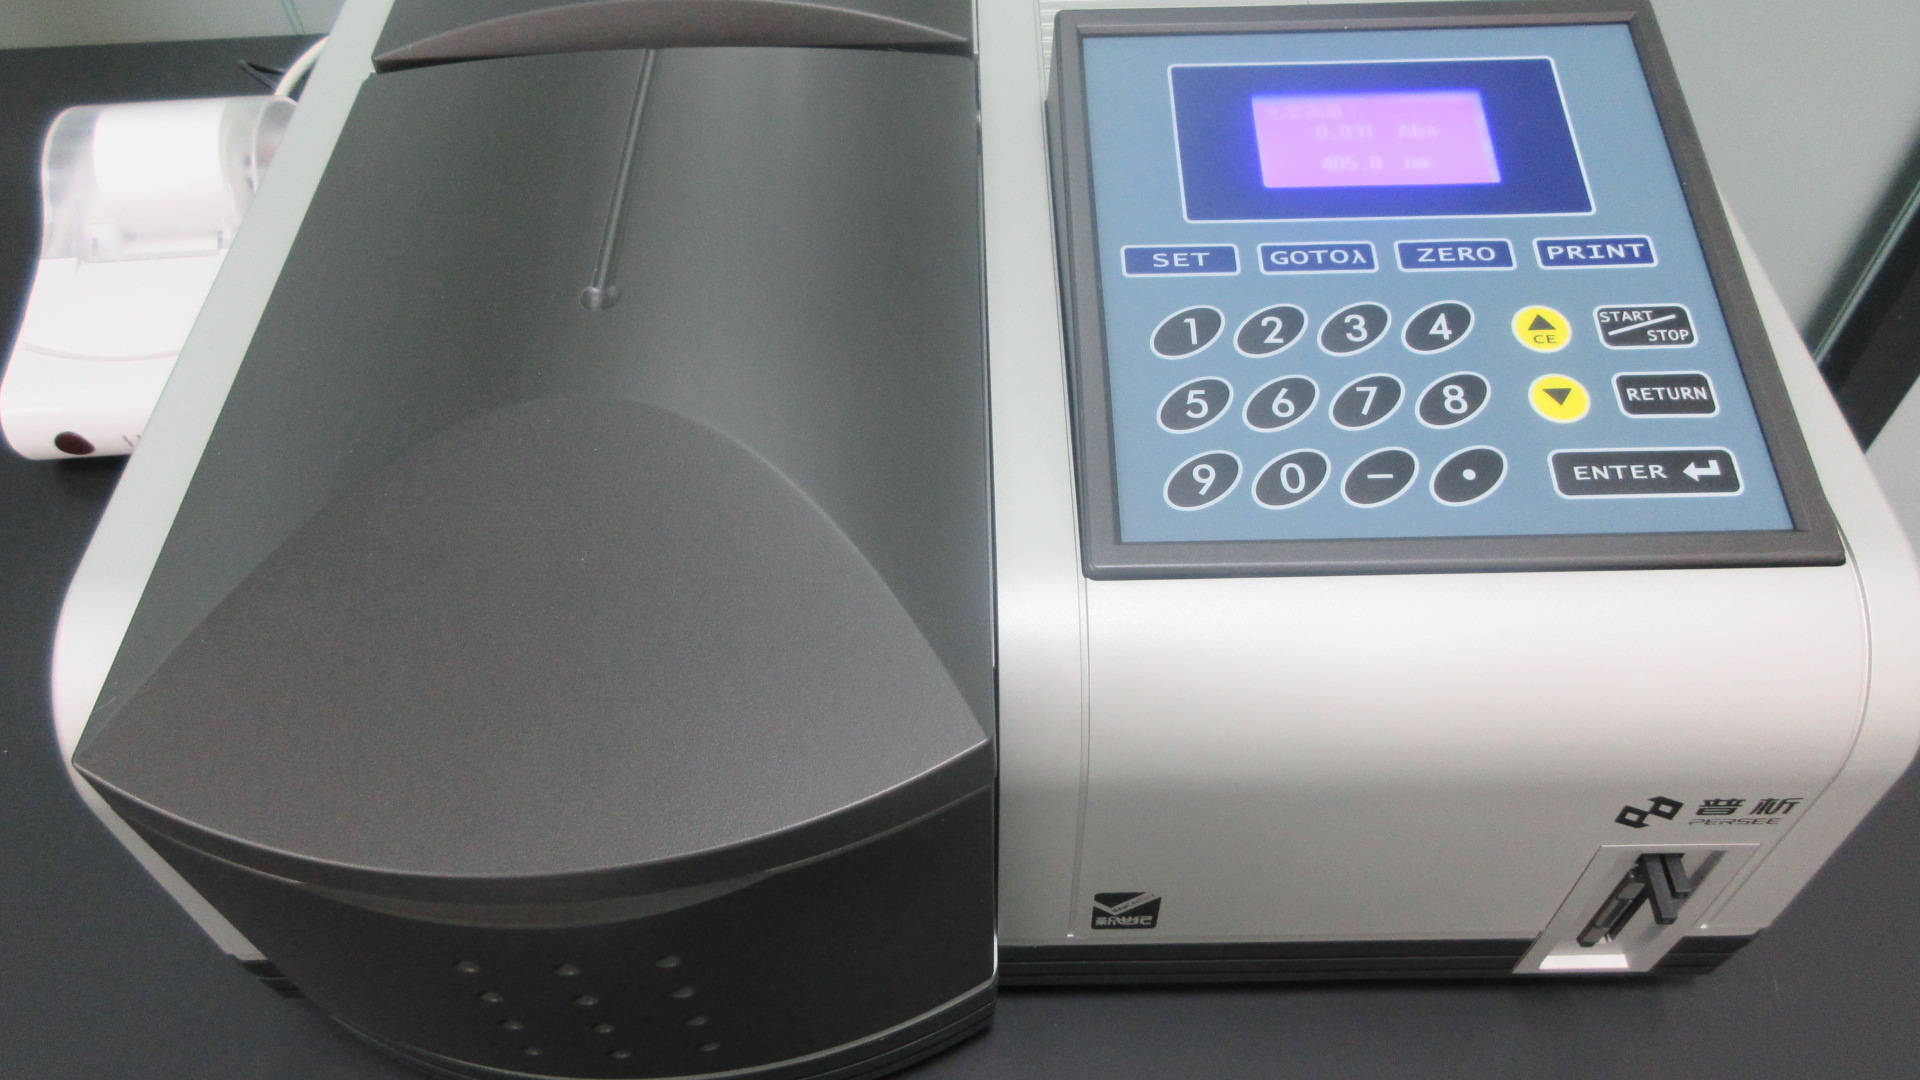
UV Spectrophotometer
Color value measurement (Phycocyanin E18) and total polysaccharide ratios.
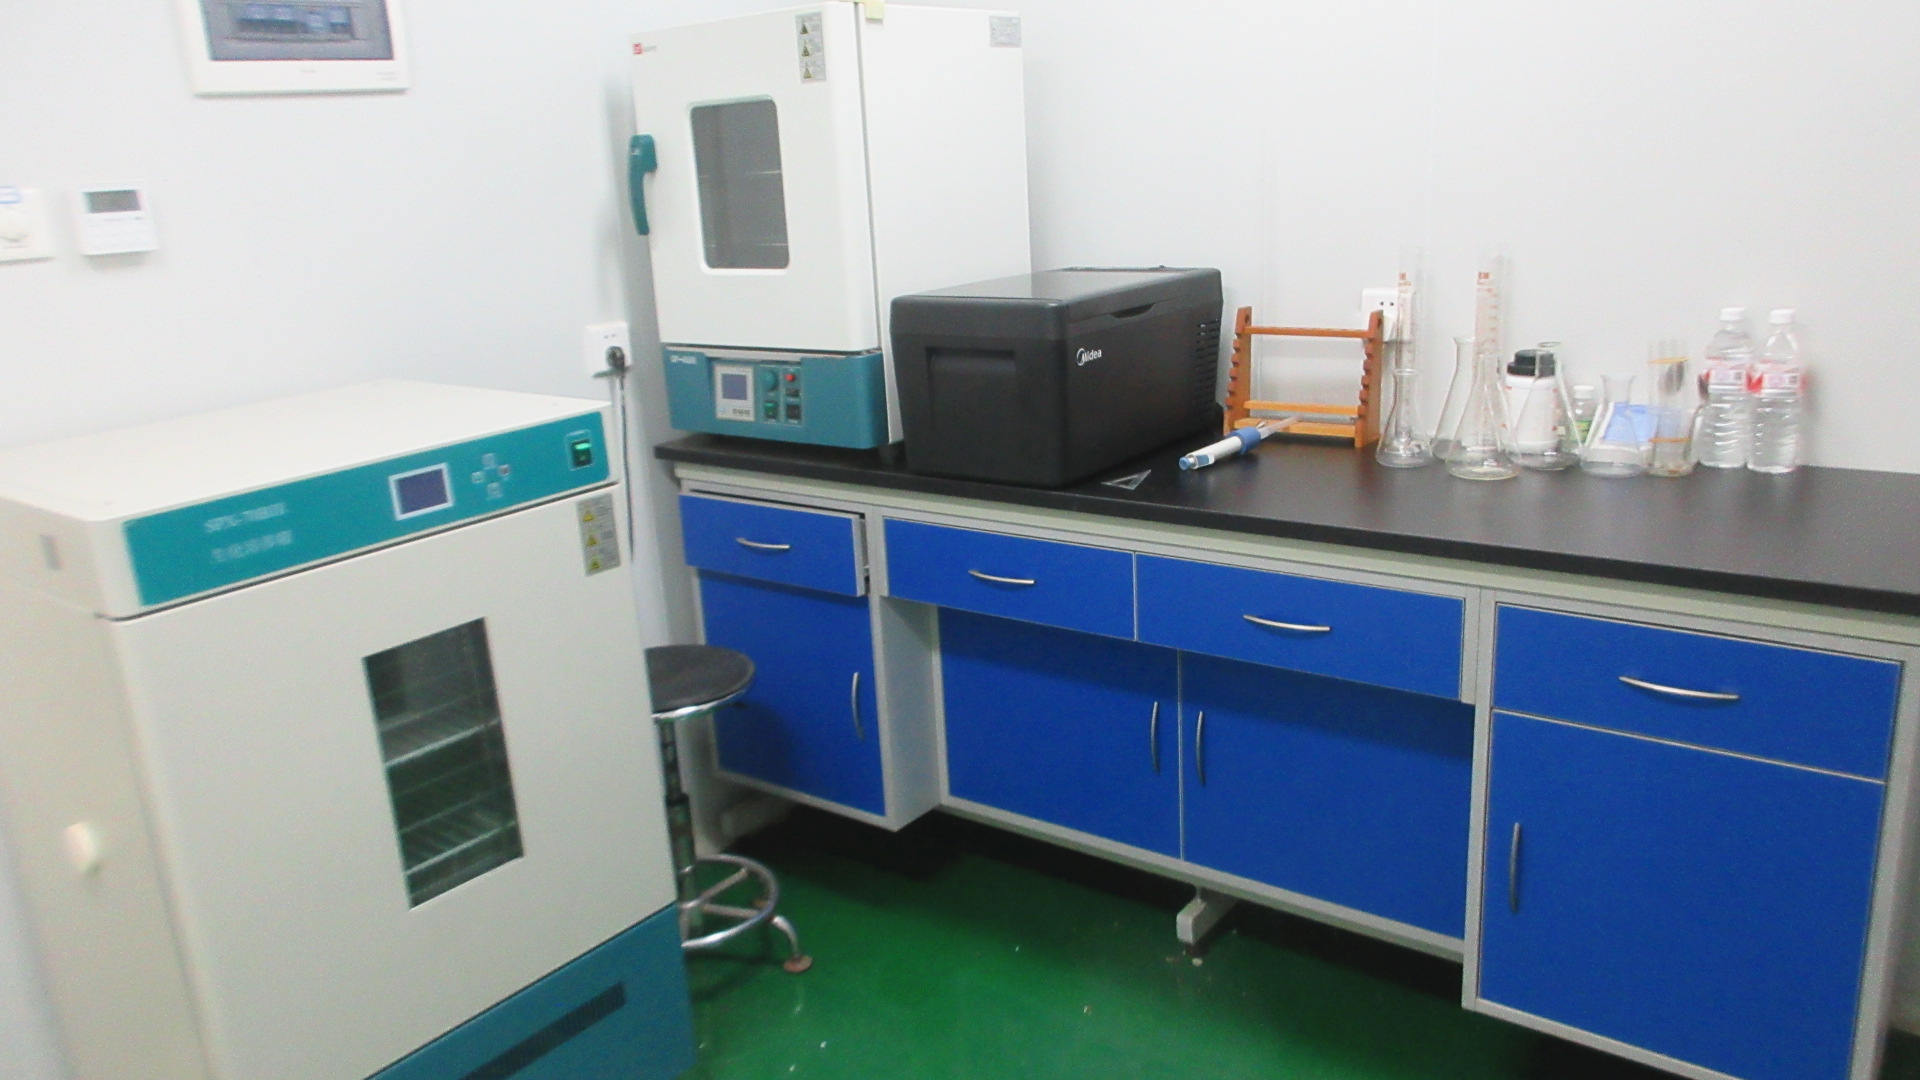
Microbiological Testing
Plate counts for total aerobic bacteria, yeast, mold, E. coli, and Salmonella.
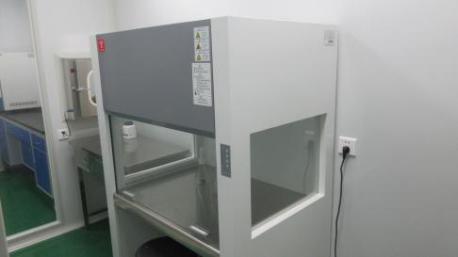
Clean Station
Laminar flow cabinet preventing cross-contamination during sampling.
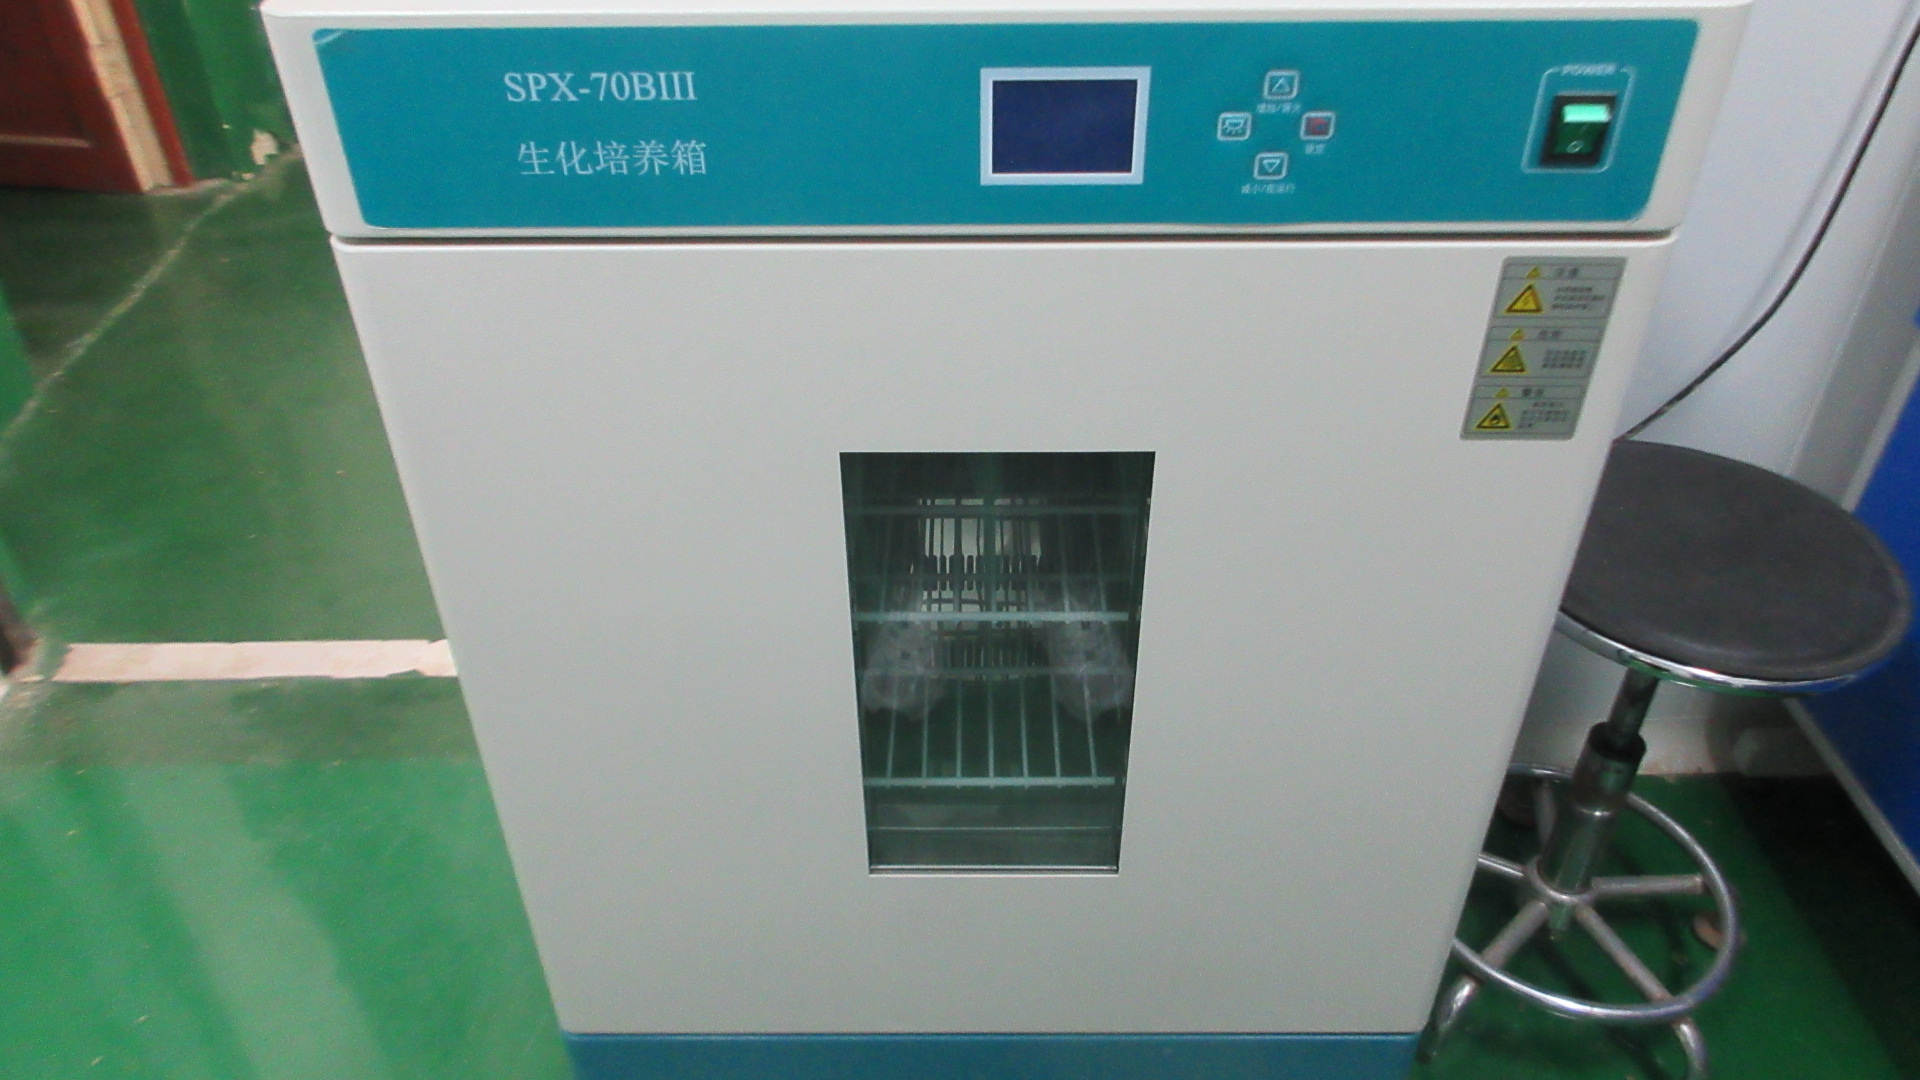
Incubator
Constant-temperature culture testing for strict hygiene verification.
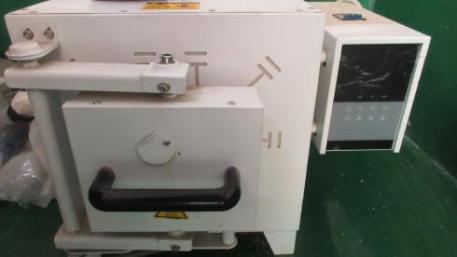
Muffle Furnace
Ash content analysis confirming botanical extract purity.
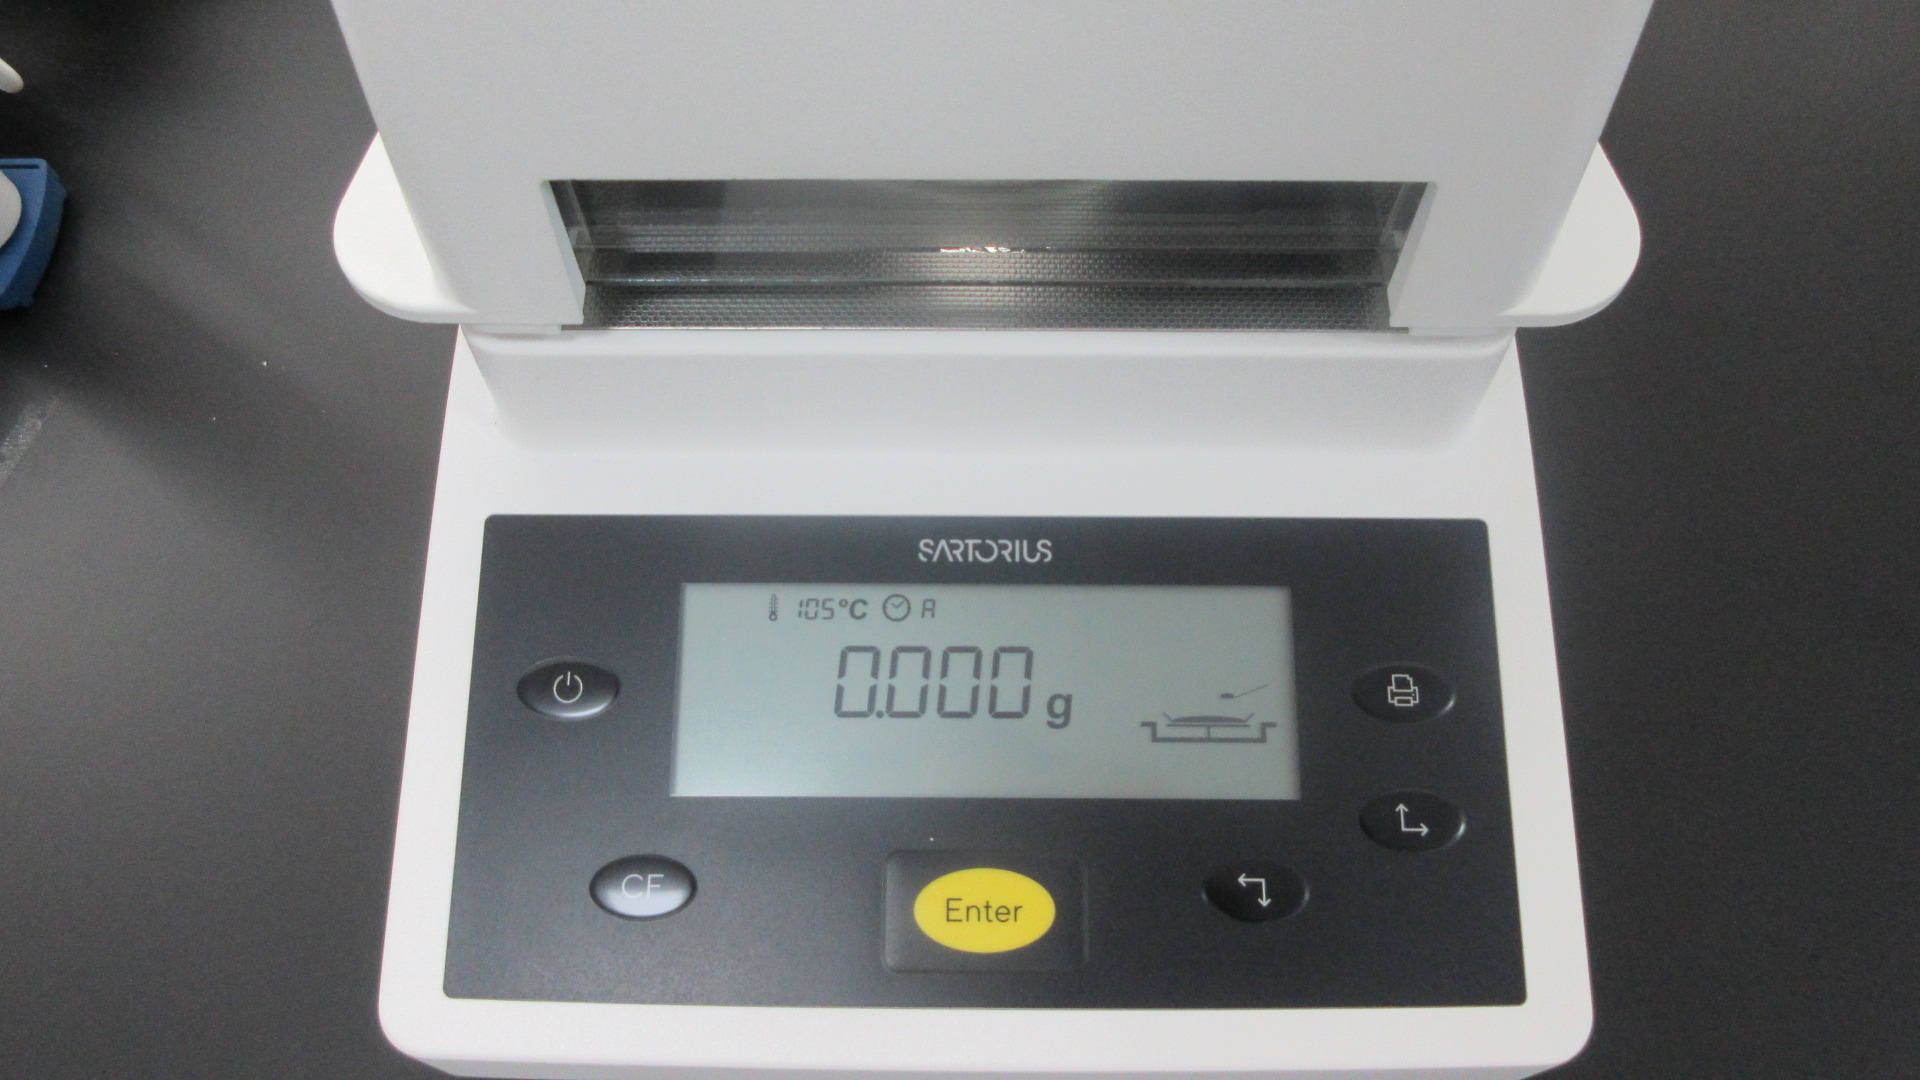
Moisture Meter
Loss on drying (LOD) testing to protect product stability and shelf-life.
R&D Center & Patent Portfolio
4 full-time R&D engineers supporting minor adjustments, full custom formulas, and method optimization.
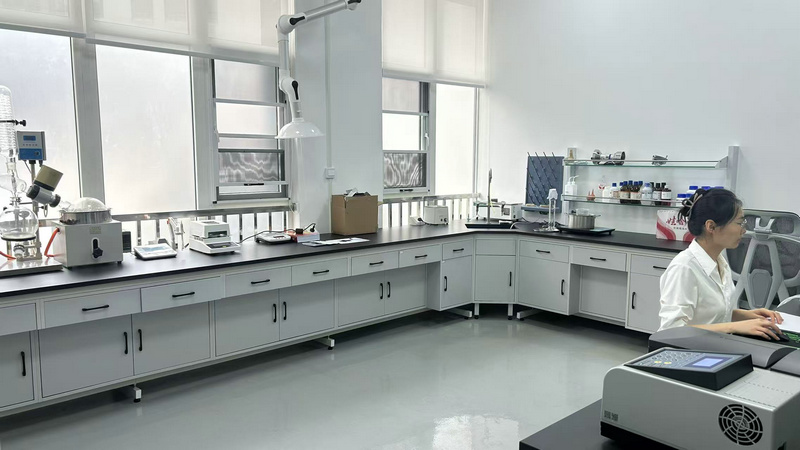
R&D Facility
Dedicated bench space for bench-scale formulation and extraction trials.
Formulation Bench
Tailored blend developments for sweeteners, instant beverages, and dietary mixes.
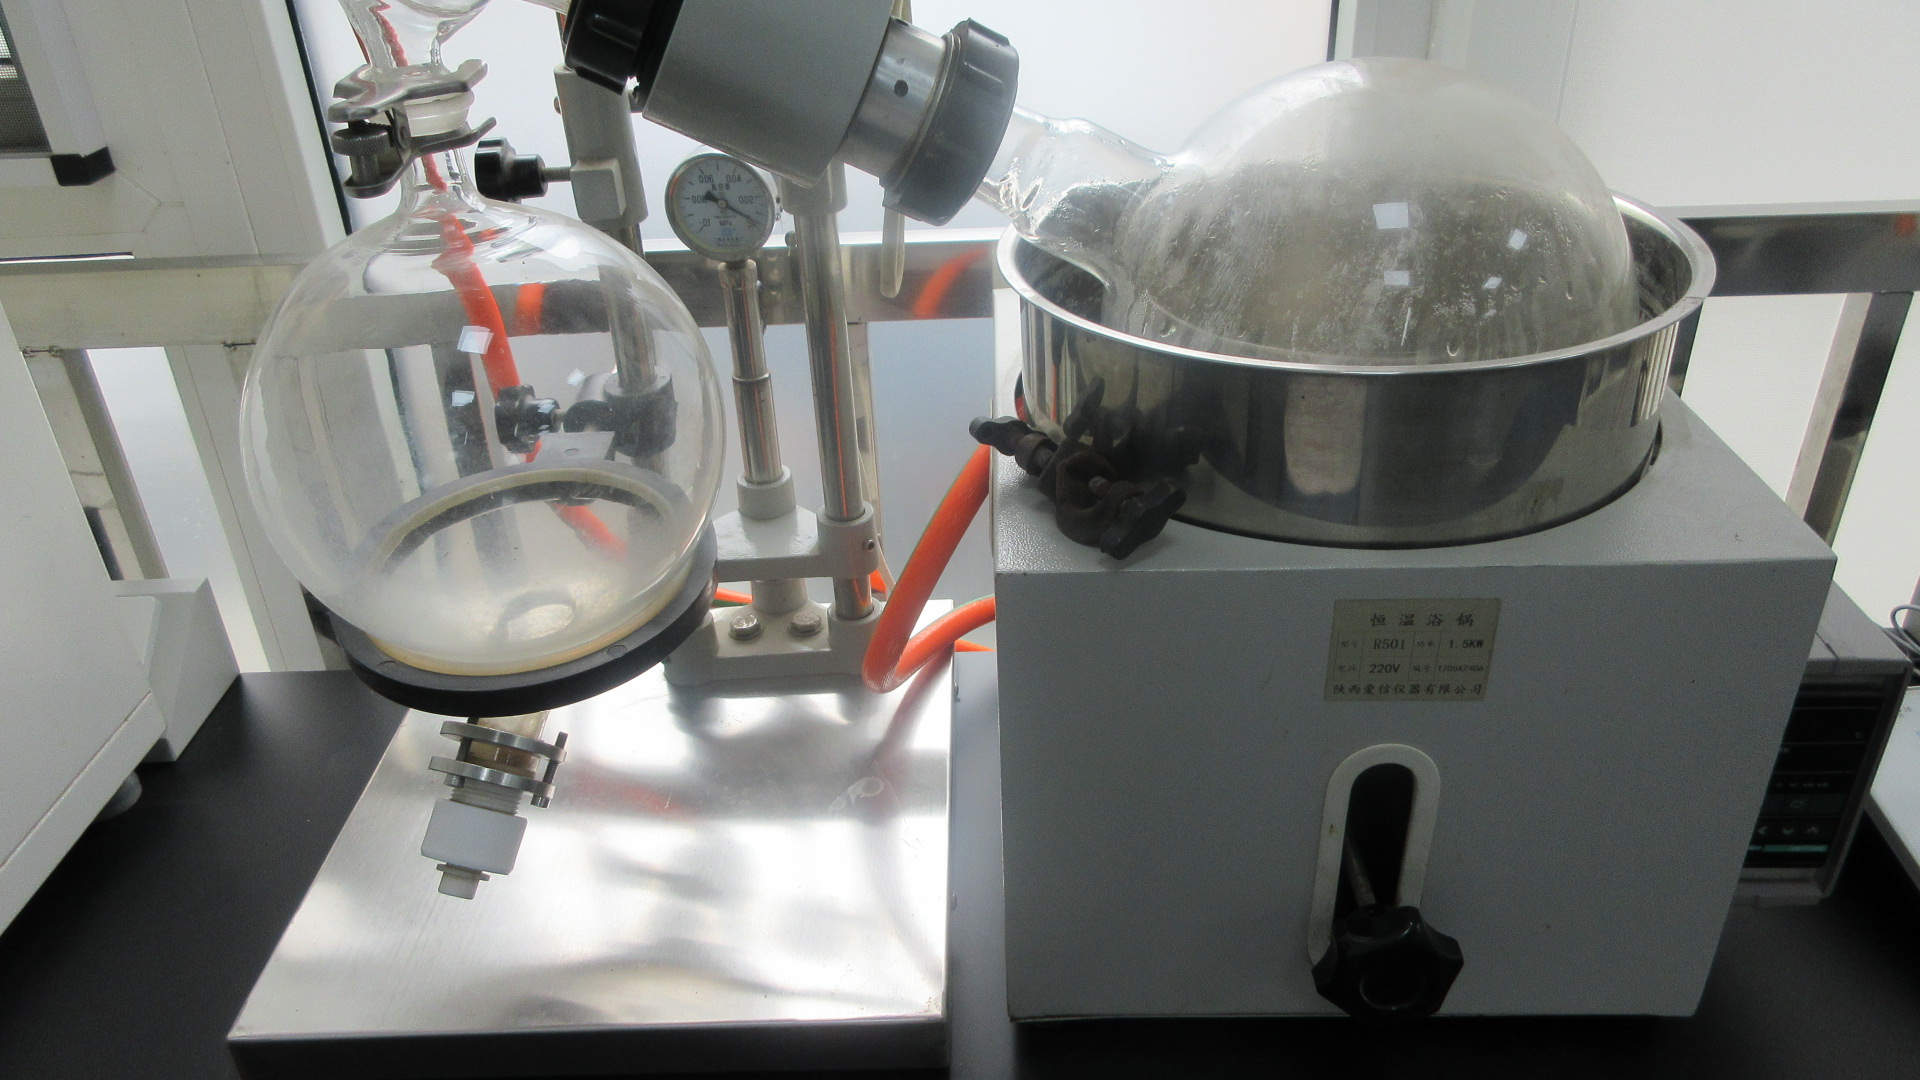
Rotary Evaporator
Pilot solvent removal and concentrate recovery for experimental botanical batches.
Method Validation
Developing accurate assay identification protocols for novel plant markers.
Invention Patent ZL 2014 1 0464649.9
Patented method for extracting and purifying high-purity protocatechuic aldehyde from Salvia miltiorrhiza (Danshen).
Utility Model Patent No. 14520048
Patented botanical extraction device designed to optimize extraction yields and ensure batch-to-batch consistency.
Full-Service Manufacturing Capabilities
Customization Services
Flexible manufacturing options tailored to client specification sheets.
- Custom active assay ratios
- Mesh size adjustments (80 - 450 mesh)
- Custom formula blending
- Private label retail packaging
Comprehensive Certifications
Meeting religious, organic, and international food safety regulations.
- ISO 22000 & HACCP Certified
- USDA Organic & EU Organic
- Halal & Kosher Verified
- SGS Pesticide Multi-Residue Reports
International Shipping
Seamless export handling to over 30 countries and regions worldwide.
- FOB, CIF, CFR, EXW, DDP, Express
- IATA DGR & IMDG Transport Reports
- Air & Sea transport safety compliance
- T/T, L/C, Credit Card, PayPal, Escrow
Request Technical Specs, COA, or Custom Blends
Share your target active content, application, and destination market. Our technical engineering team will reply with specification sheets and batch COAs within 24 hours.