
Multispecialty Manufacturer
Direct Herbal Sourcing, Standardized Extraction & Global Supply
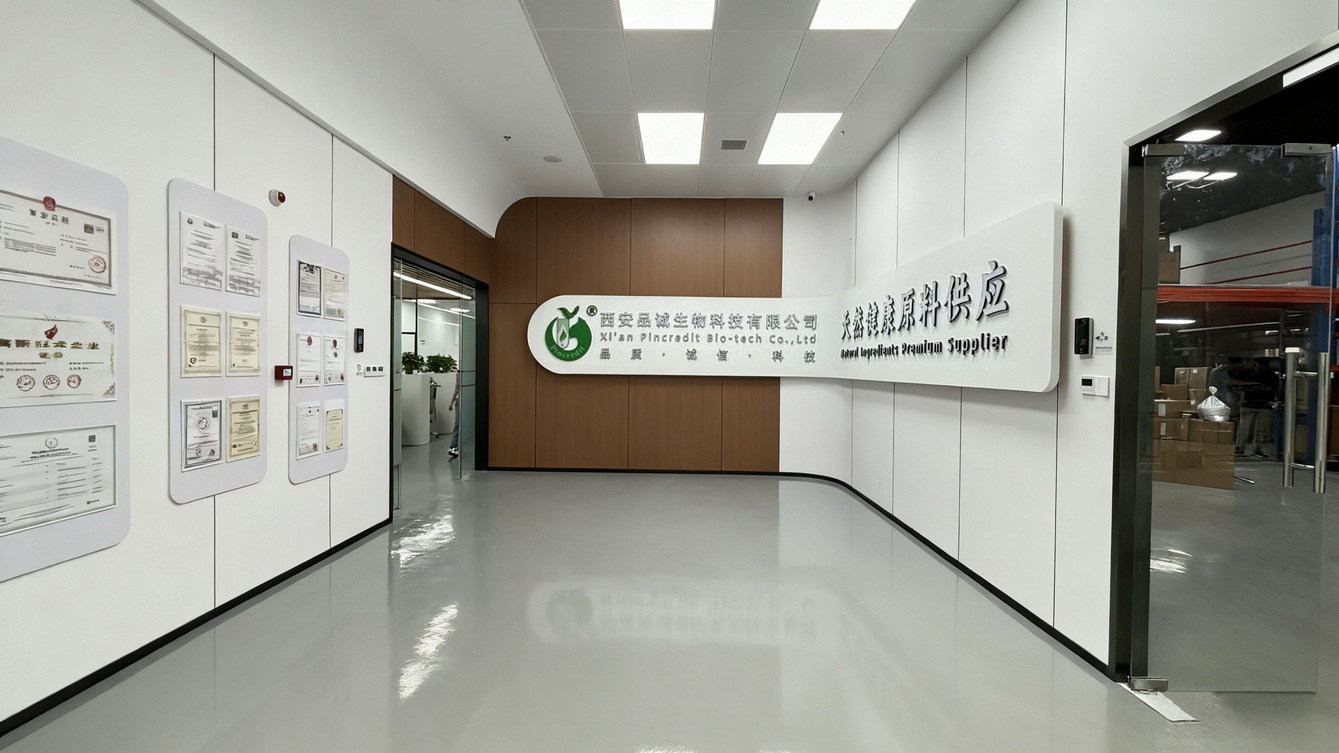
Headquartered in Xi'an, Shaanxi Province — China's historic hub for Qinba mountain botanical herbs — Xi'an Vexli Bio-Tech Co., Ltd. has been dedicated to the research, production, and worldwide export of premium plant extracts, certified organic superfoods, natural colorants, and dietary supplement actives since 2014.
Combining modern industrial extraction lines with an audited network of 25 standardized partner manufacturing facilities, we eliminate intermediary speculation by purchasing botanical raw crops directly at origin. Every production campaign is governed by strict ISO 22000 and HACCP safety standards, providing international brands with batch-to-batch chemical stability, heavy metal control, pesticide traceability, and low minimum order quantities (MOQs from 1 kg).
Verified Data Backed by Independent Inspection
Metrics assessed and validated during our annual on-site audit by SGS Group and certified export records.
Integrated Production, Testing & Customization Capabilities
From cultivation origins to micron-mesh precision, our technical departments support rigorous QA and private label demands.
OEM / ODM Customization
Formulate bespoke botanical and dietary active products built precisely to your regional regulatory thresholds.
- Customization ModelsDesign-Based & Full Custom
- Particle Size Control80 Mesh to 450 Mesh
- Packaging OptionsFoil Pouches, Cans, Drums
- Sample ValidationAvailable for QA Testing
Quality Control & QA
In-house laboratory paired with certified third-party testing guarantees potency, purity, and microbial integrity.
- Dedicated QA/QC Inspectors7 Full-Time Specialists
- QM Process Inspection2-Stage Gate (Intake + Release)
- Pesticide ScreeningBS EN 15662 Standard (SGS)
- TraceabilityRetained Lot Samples for 2 Yrs
R&D & Innovation
Continuous extraction method development, natural color preservation, and proprietary purification processes.
- R&D Technical Engineers4 Senior Specialists
- New Products / Year8+ Validated Formulations
- Invention PatentZL 2014 1 0464649.9
- Utility Model PatentPatent No. 14520048
Standardized 9-Step Extraction & Processing Workflow
Every botanical lot is processed through automated stainless-steel lines under strict critical control points.
 Step 01
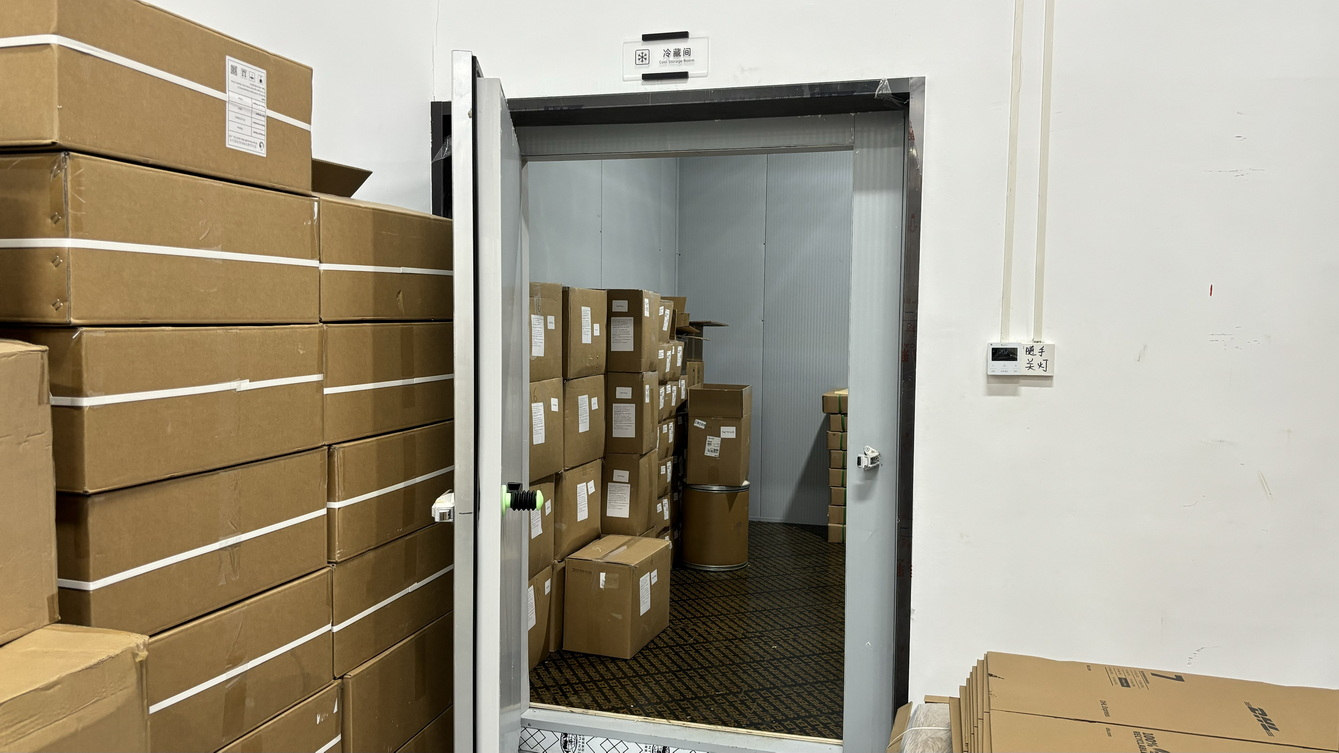
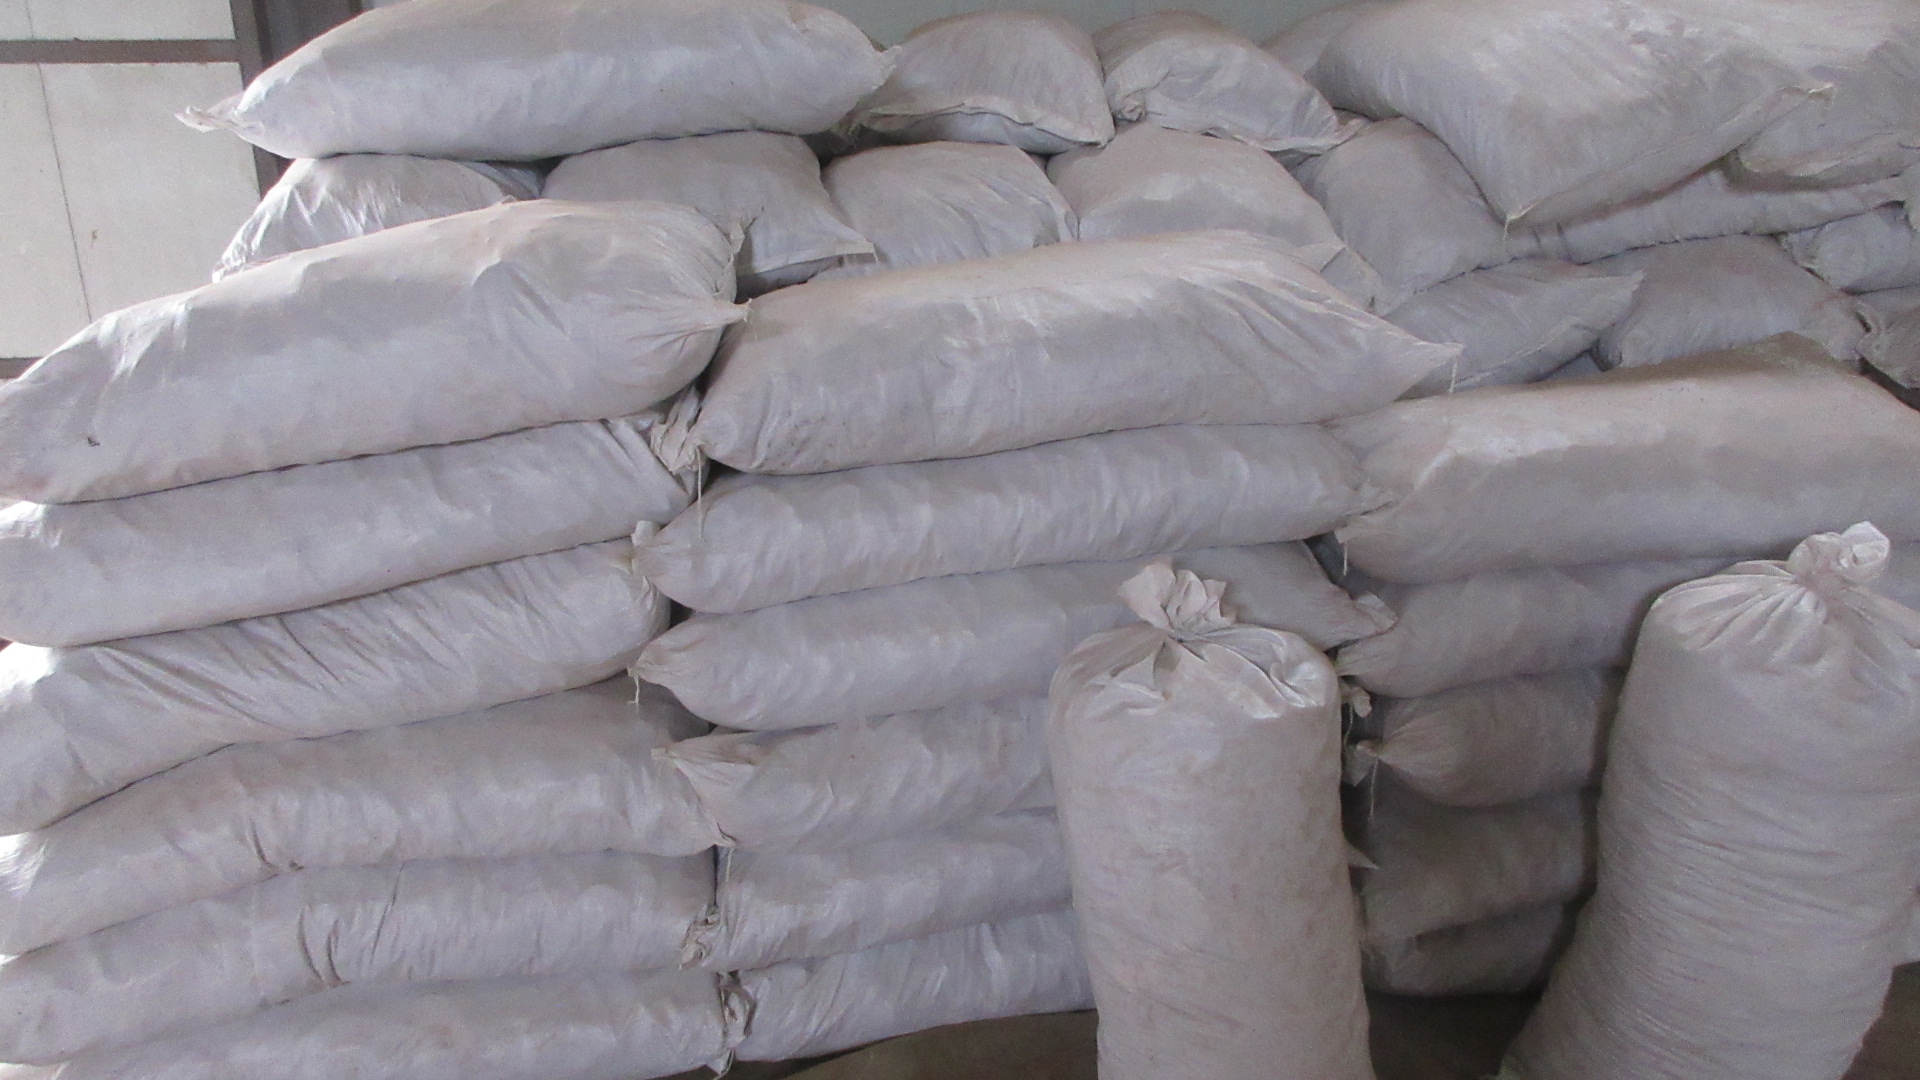
Raw Material Quarantine
Origin-sourced botanicals verified for botanical identity, moisture content, visual cleanliness, and pesticide pre-screening upon arrival.
 Step 02
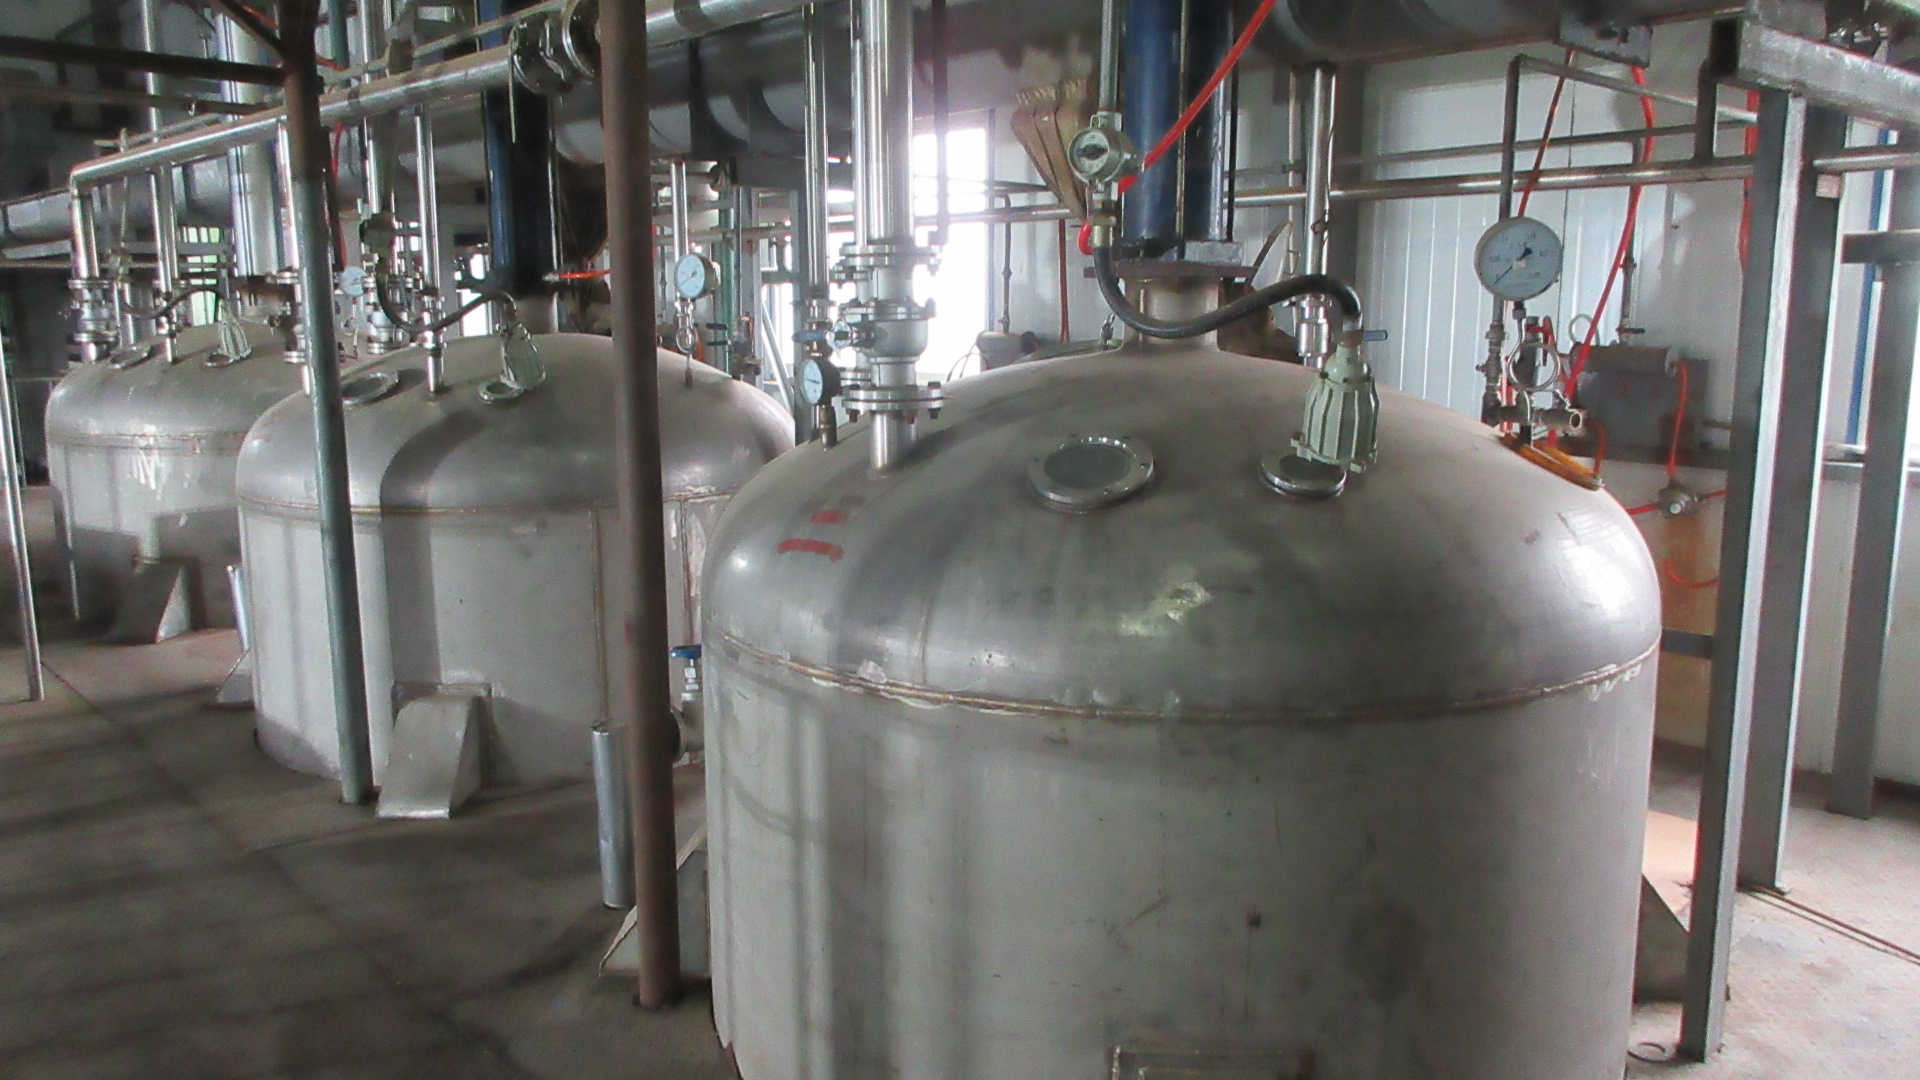
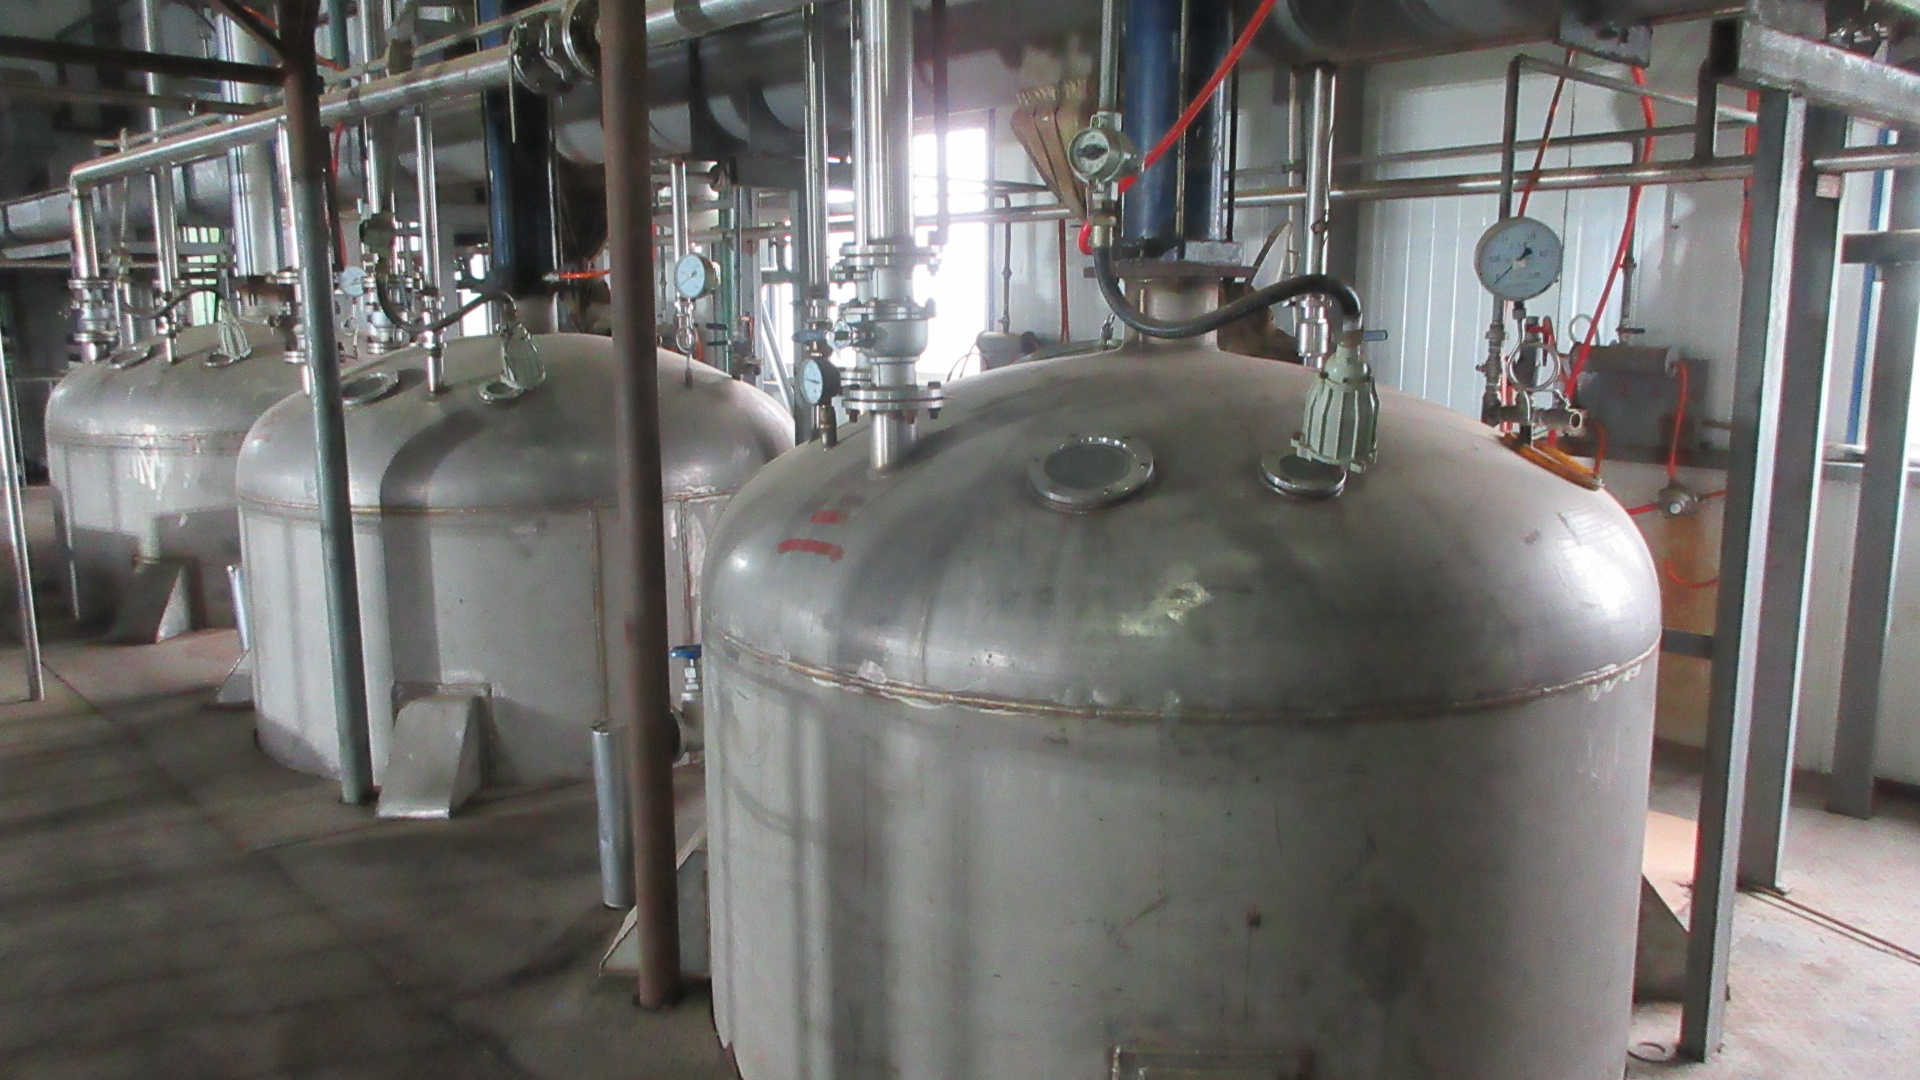
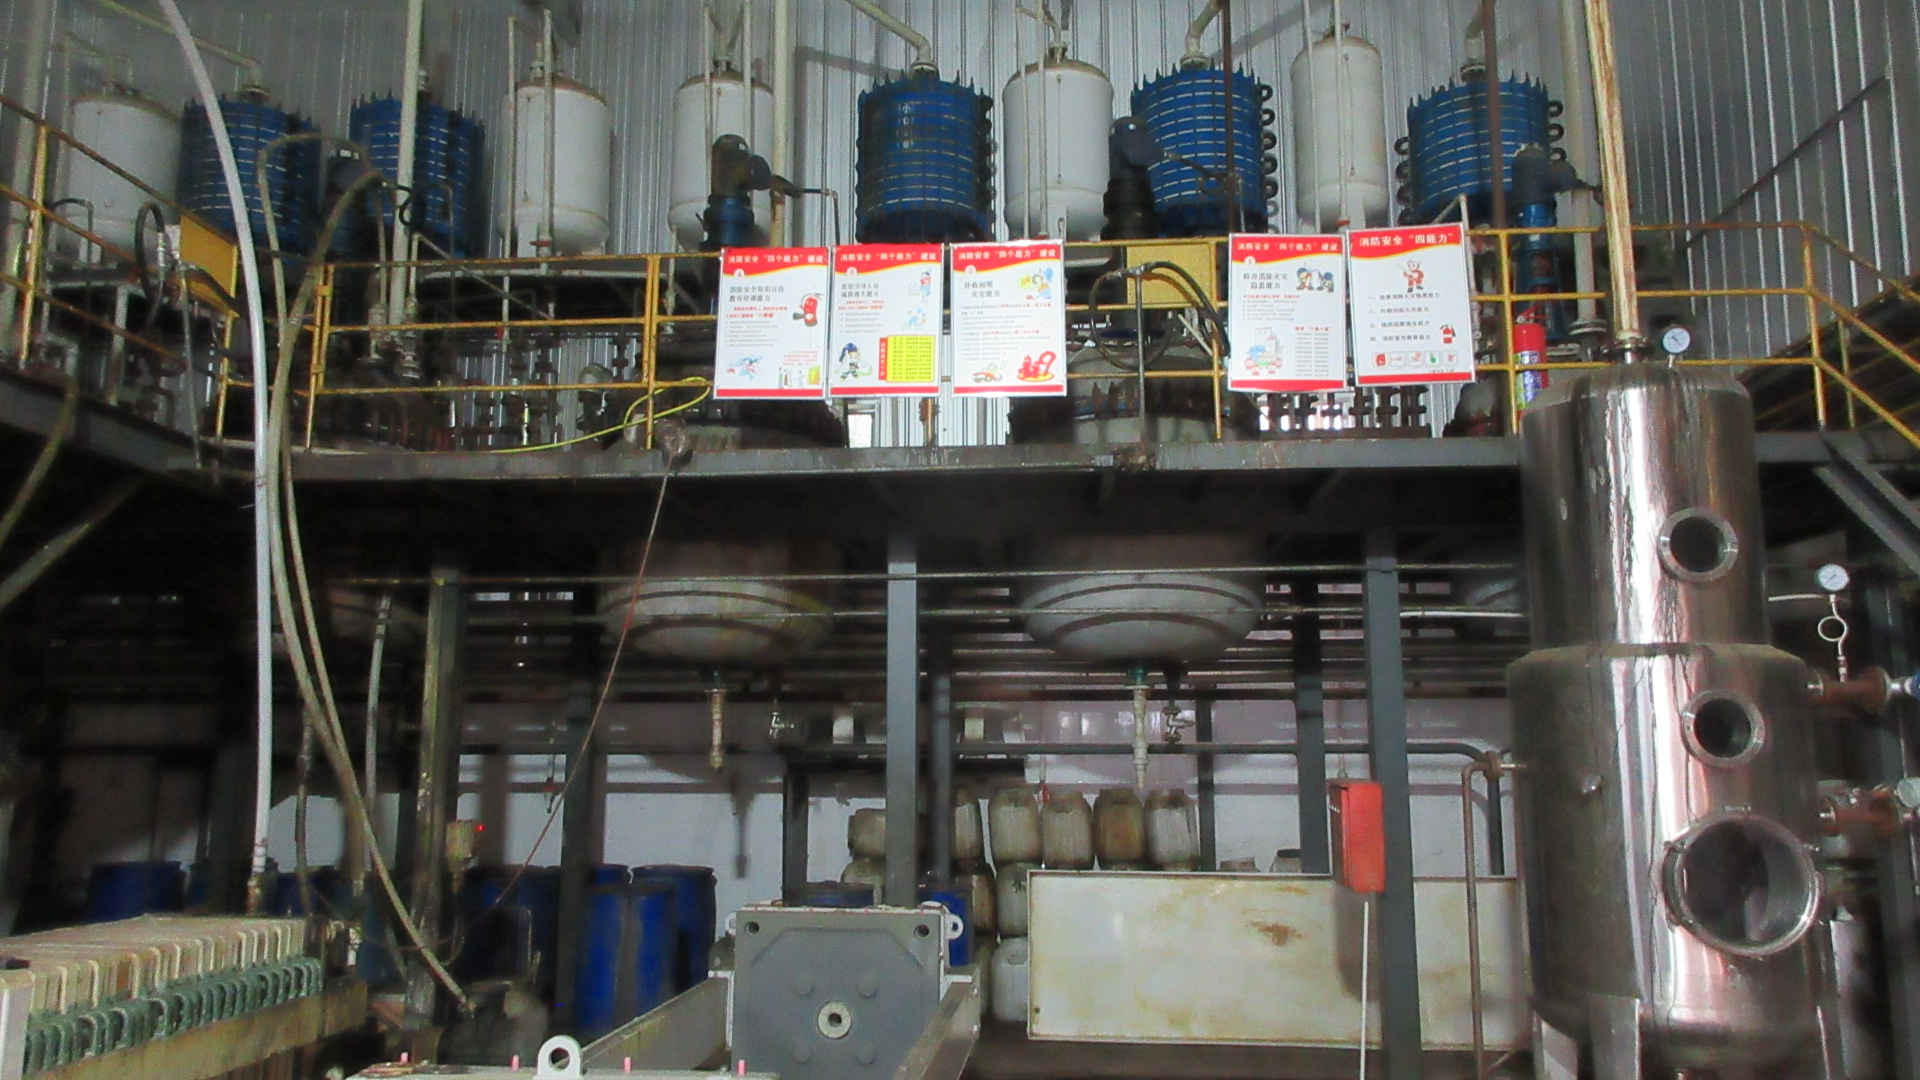
Solvent Extraction
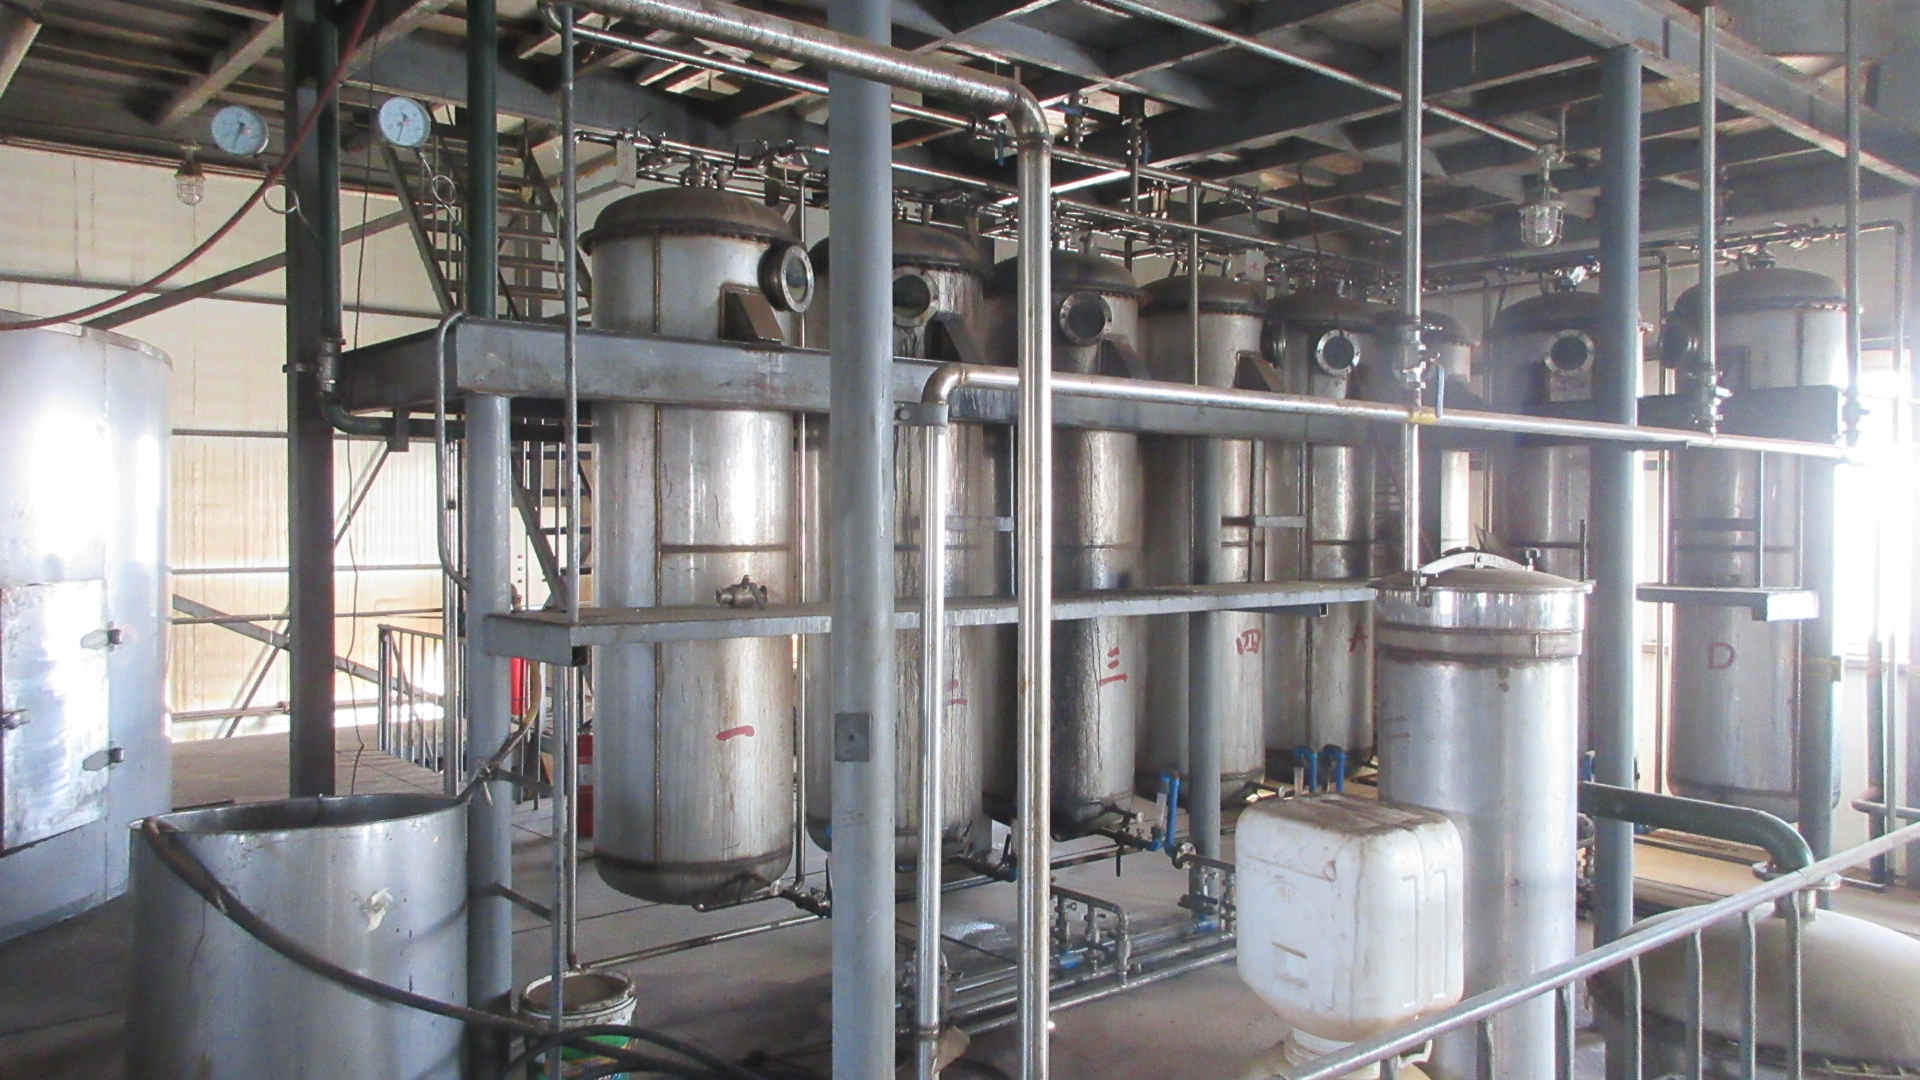
Optimized hydro-ethanolic or pure water extraction in stainless-steel tanks with exact control over solvent ratio, temperature, and residence time.
 Step 03
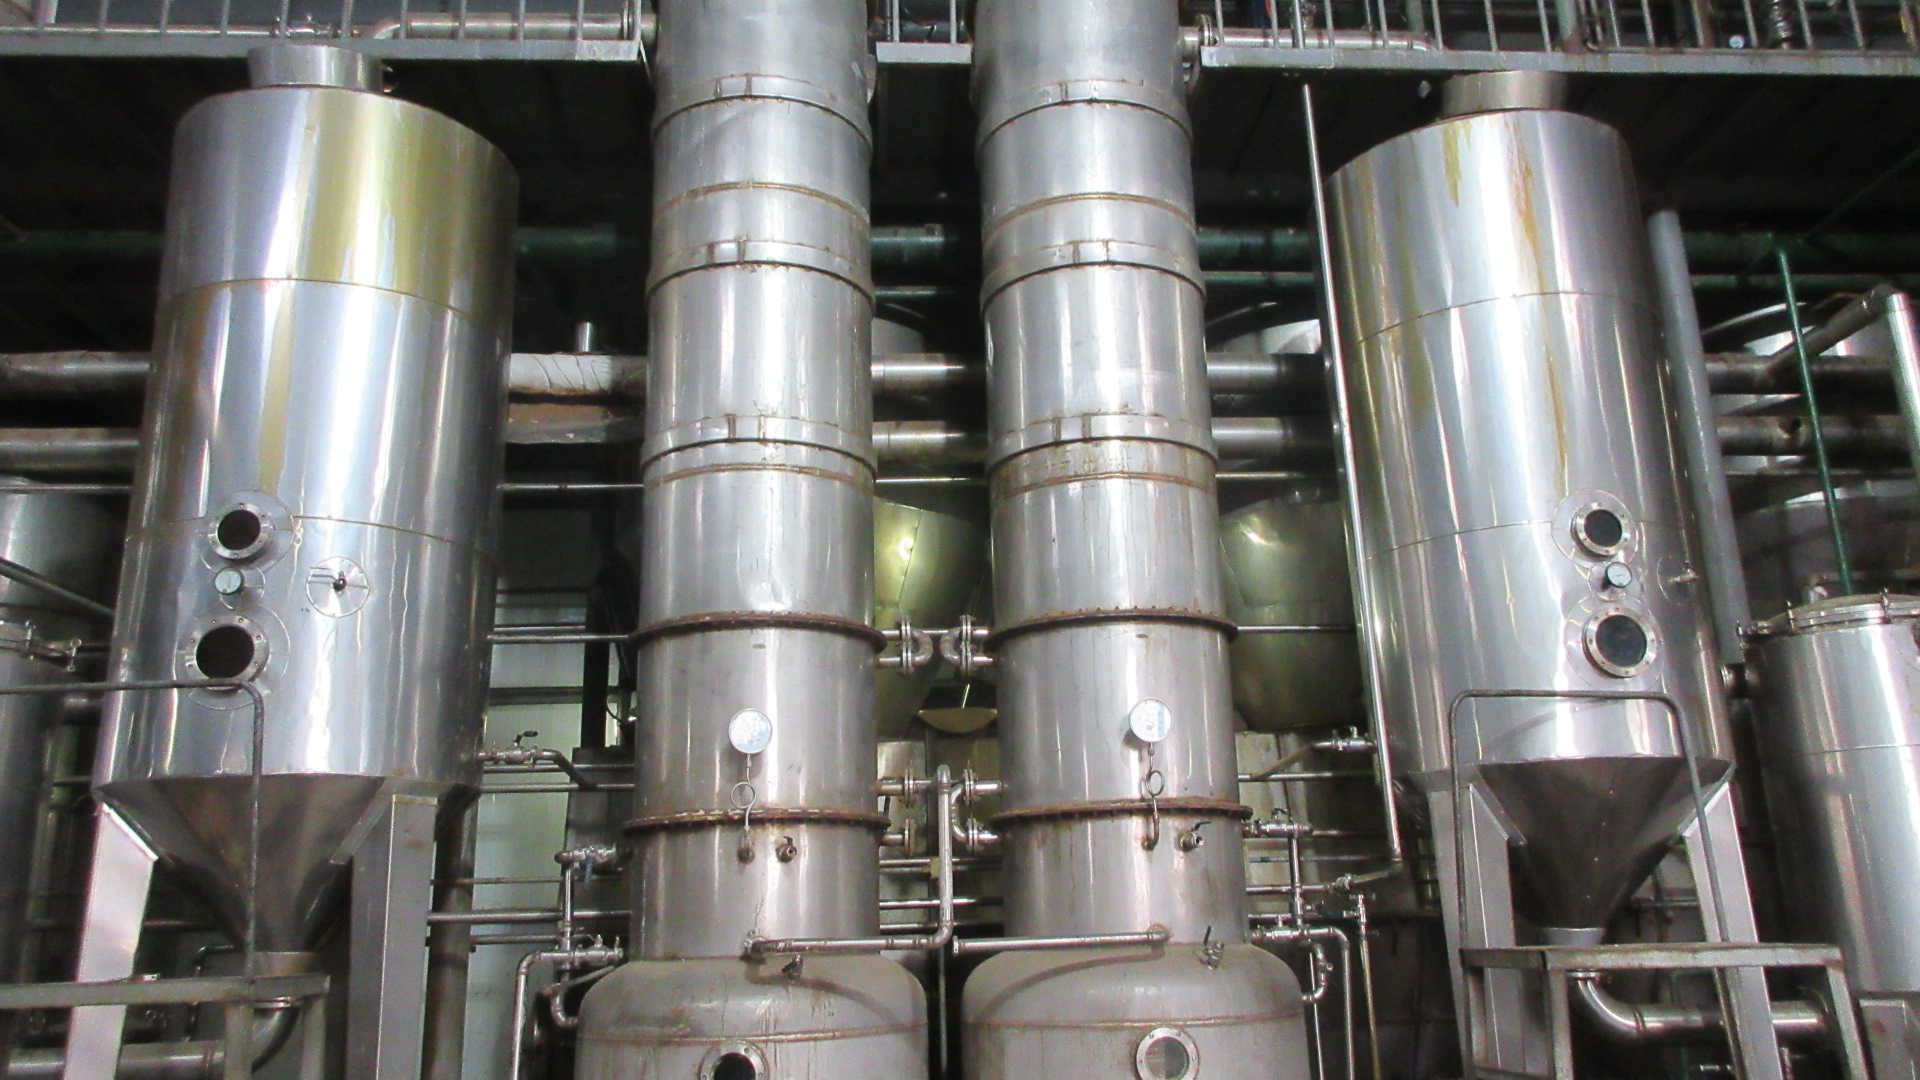
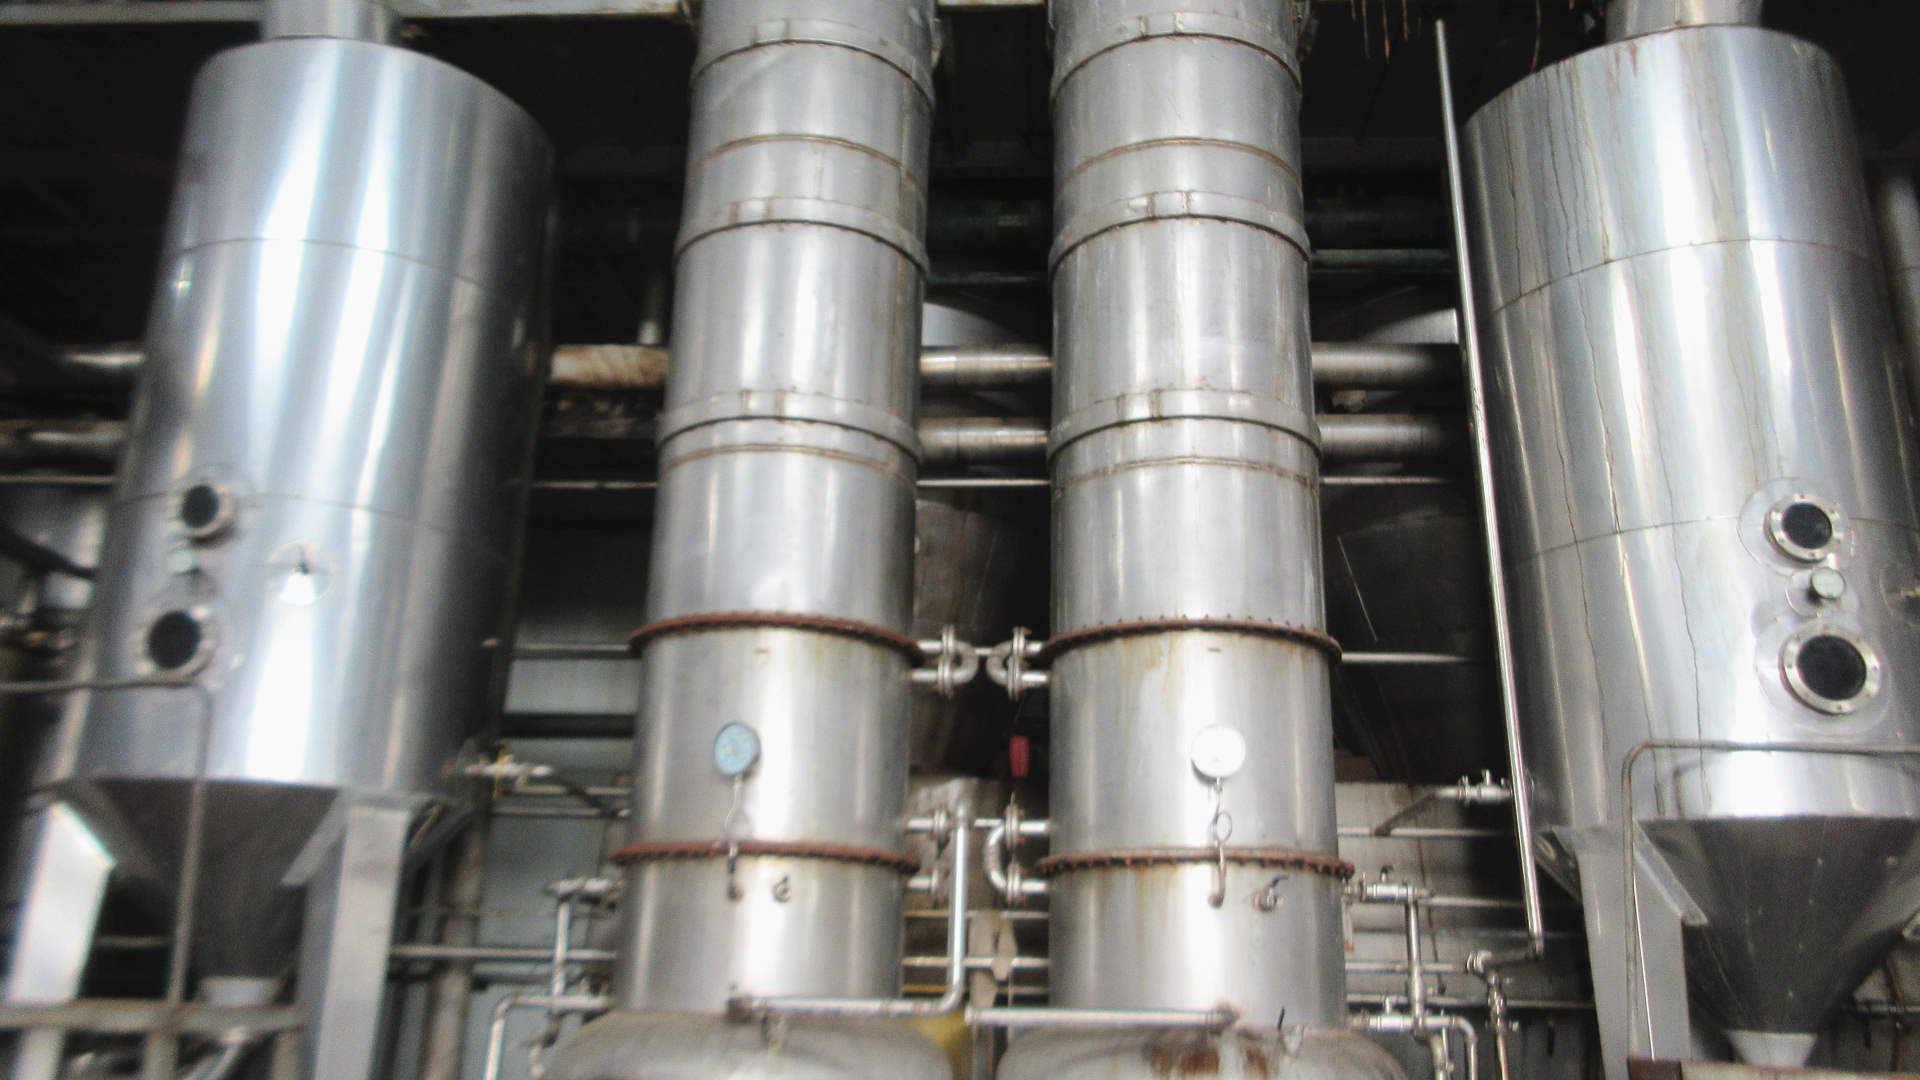
Vacuum Concentration
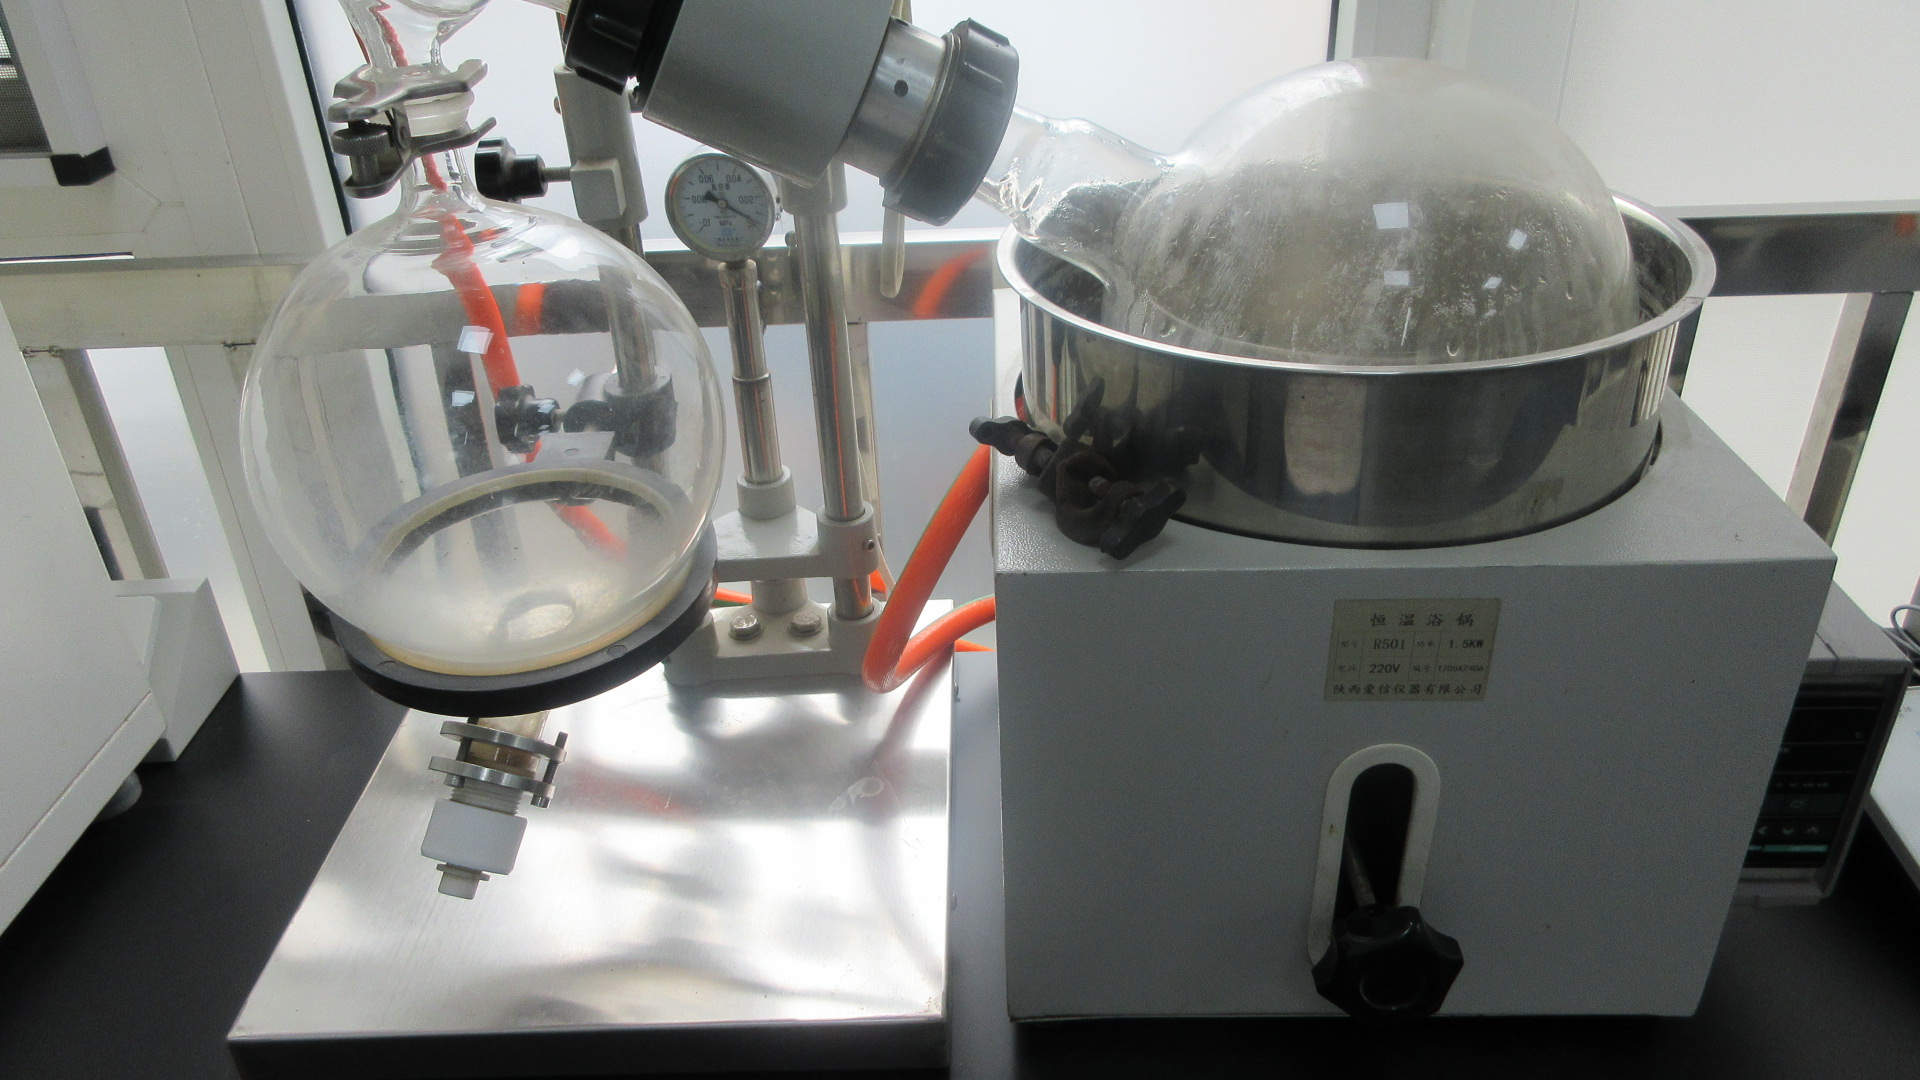
Low-temperature vacuum evaporators concentrate botanical liquor while preserving thermosensitive polyphenols, pigments, and bioactive fractions.
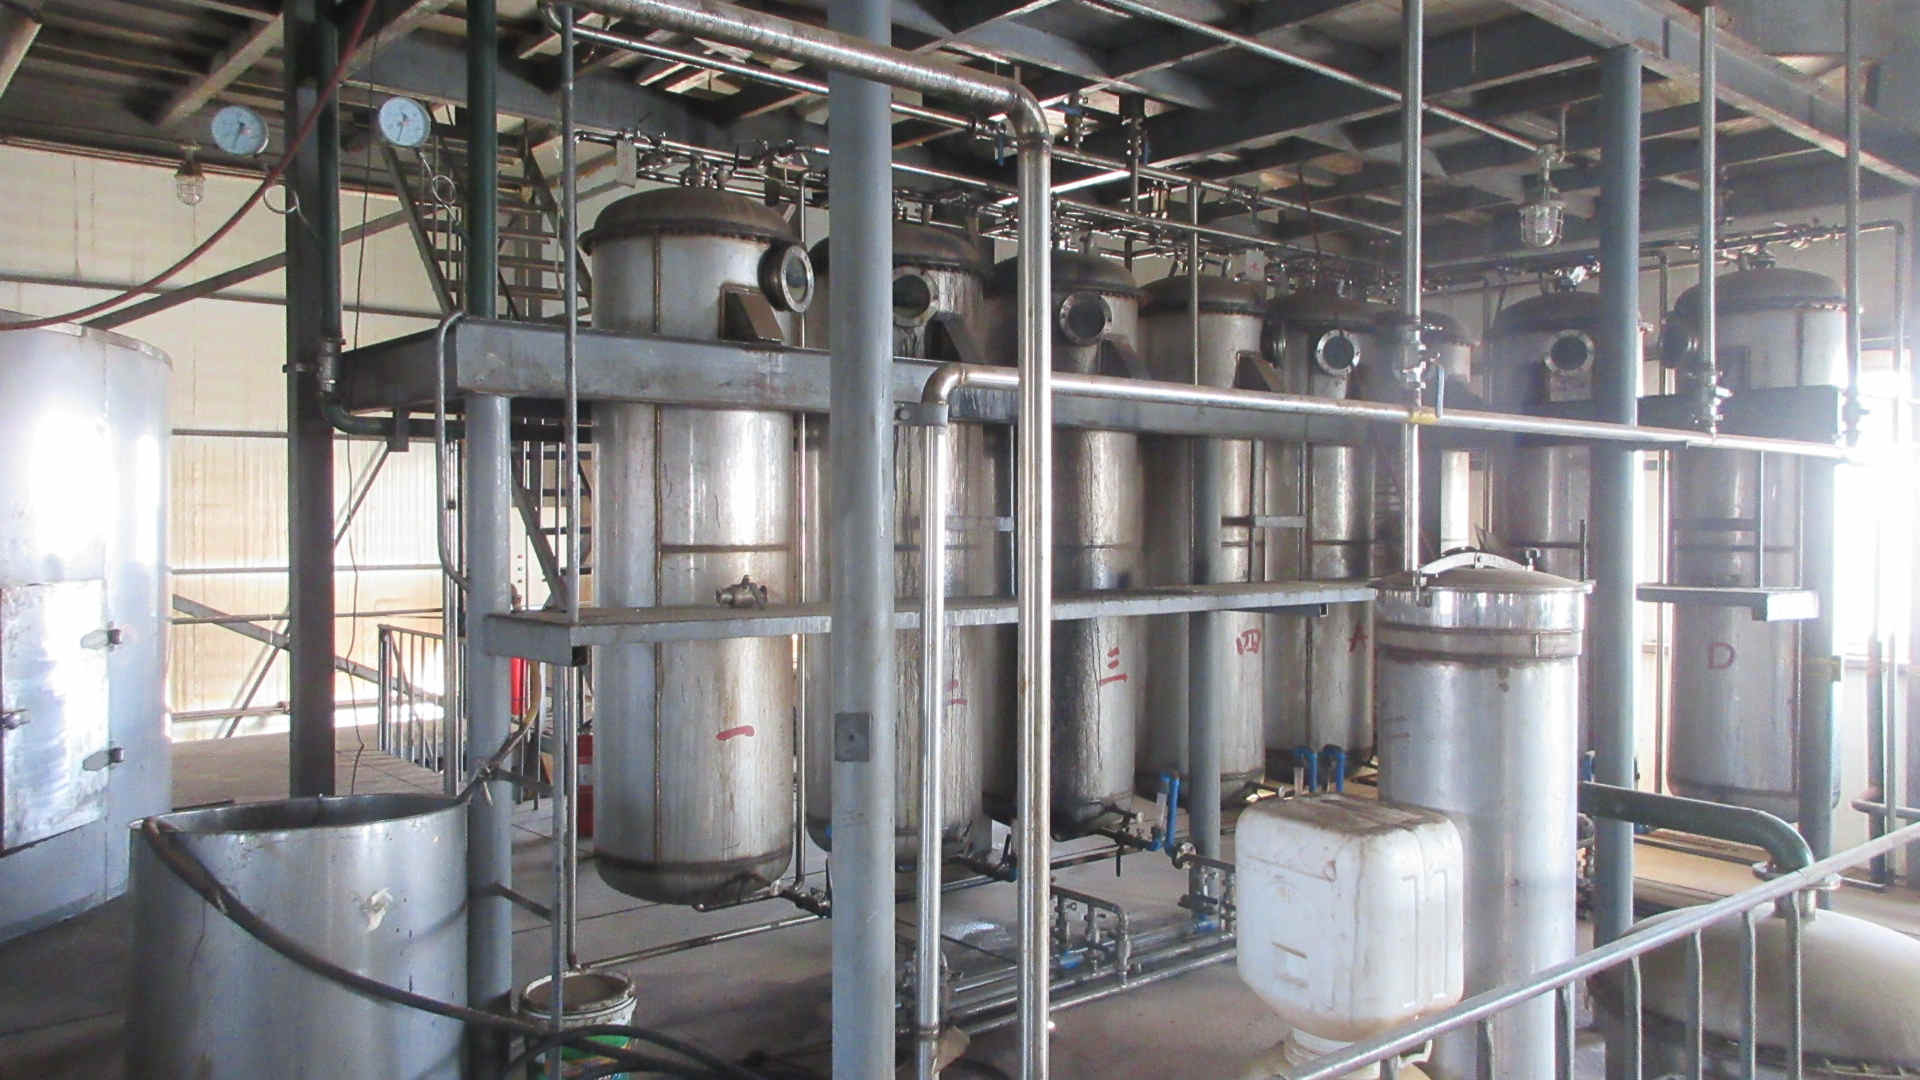 Step 04
Column Purification
Macroporous adsorption resins and ultrafiltration membrane modules isolate target chemical markers and strip undesirable tannins or heavy impurities.
 Step 05
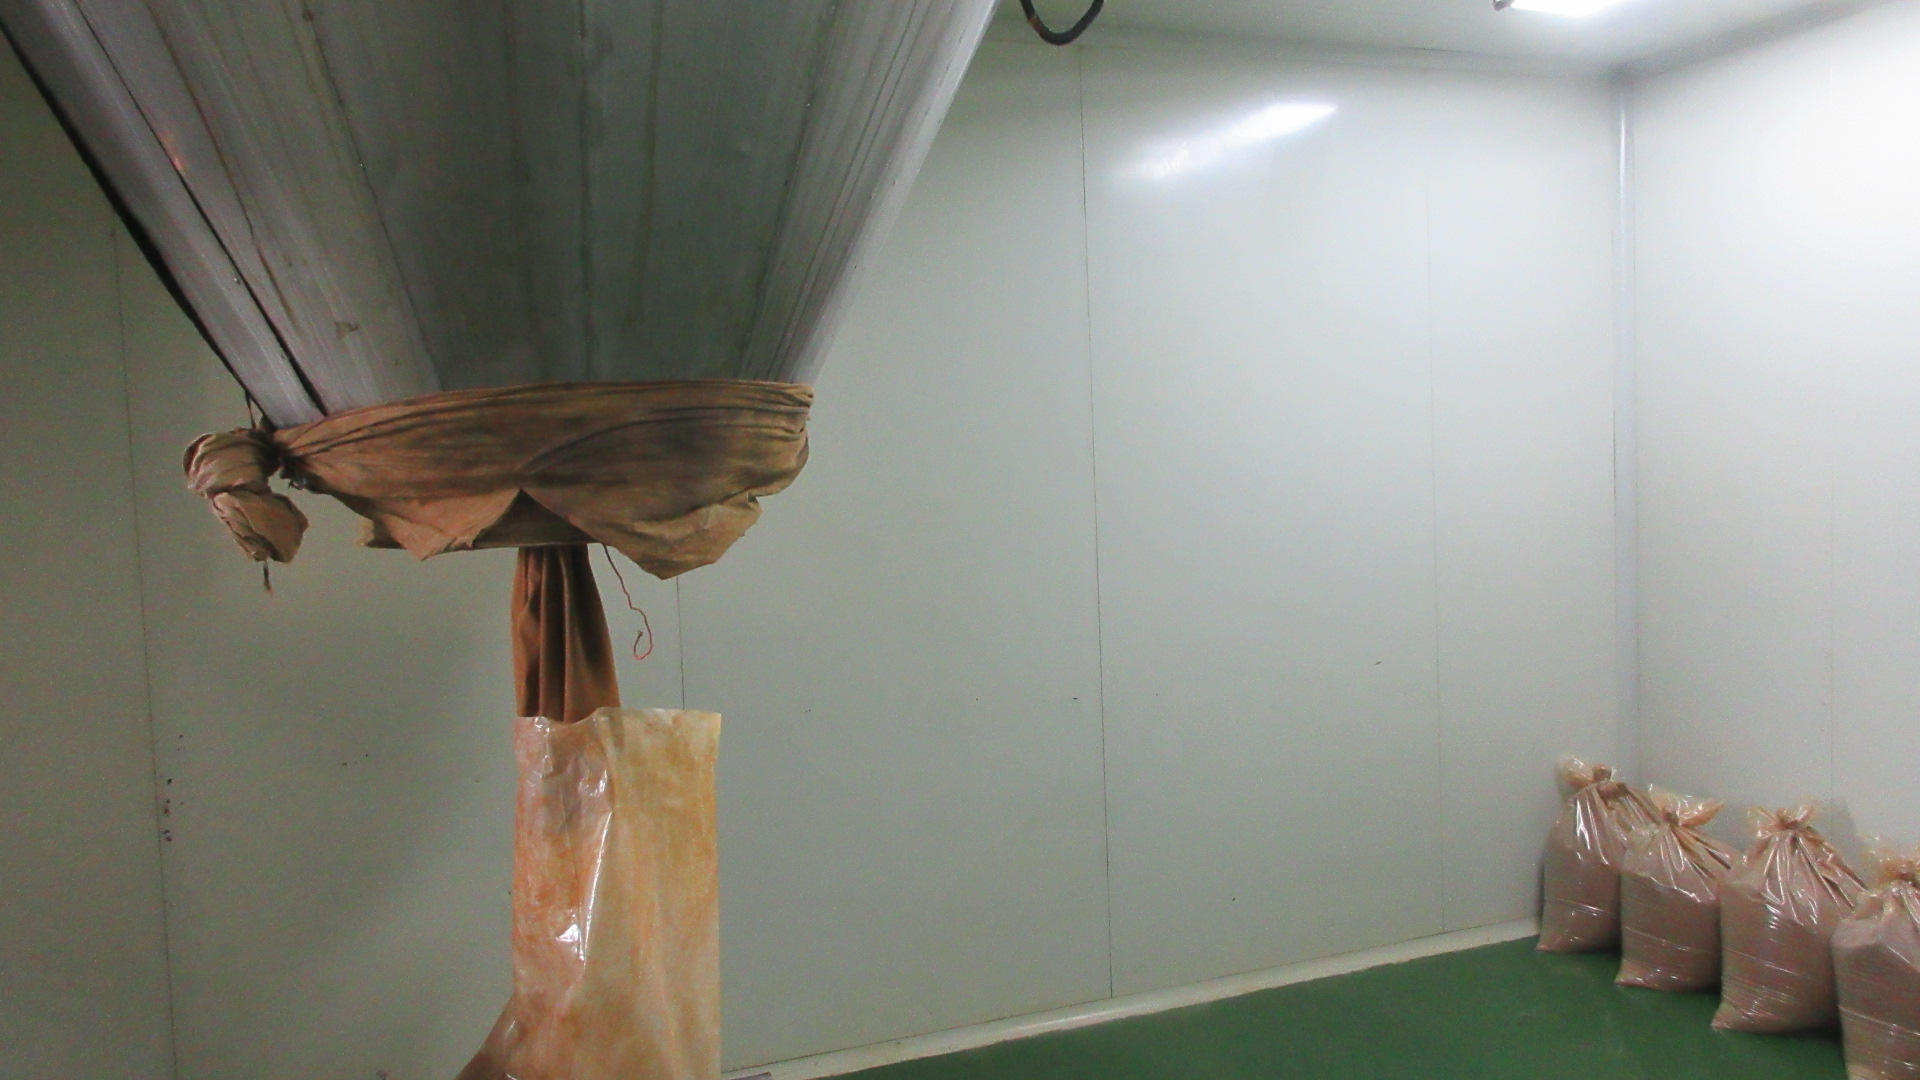
Drying & Spraying
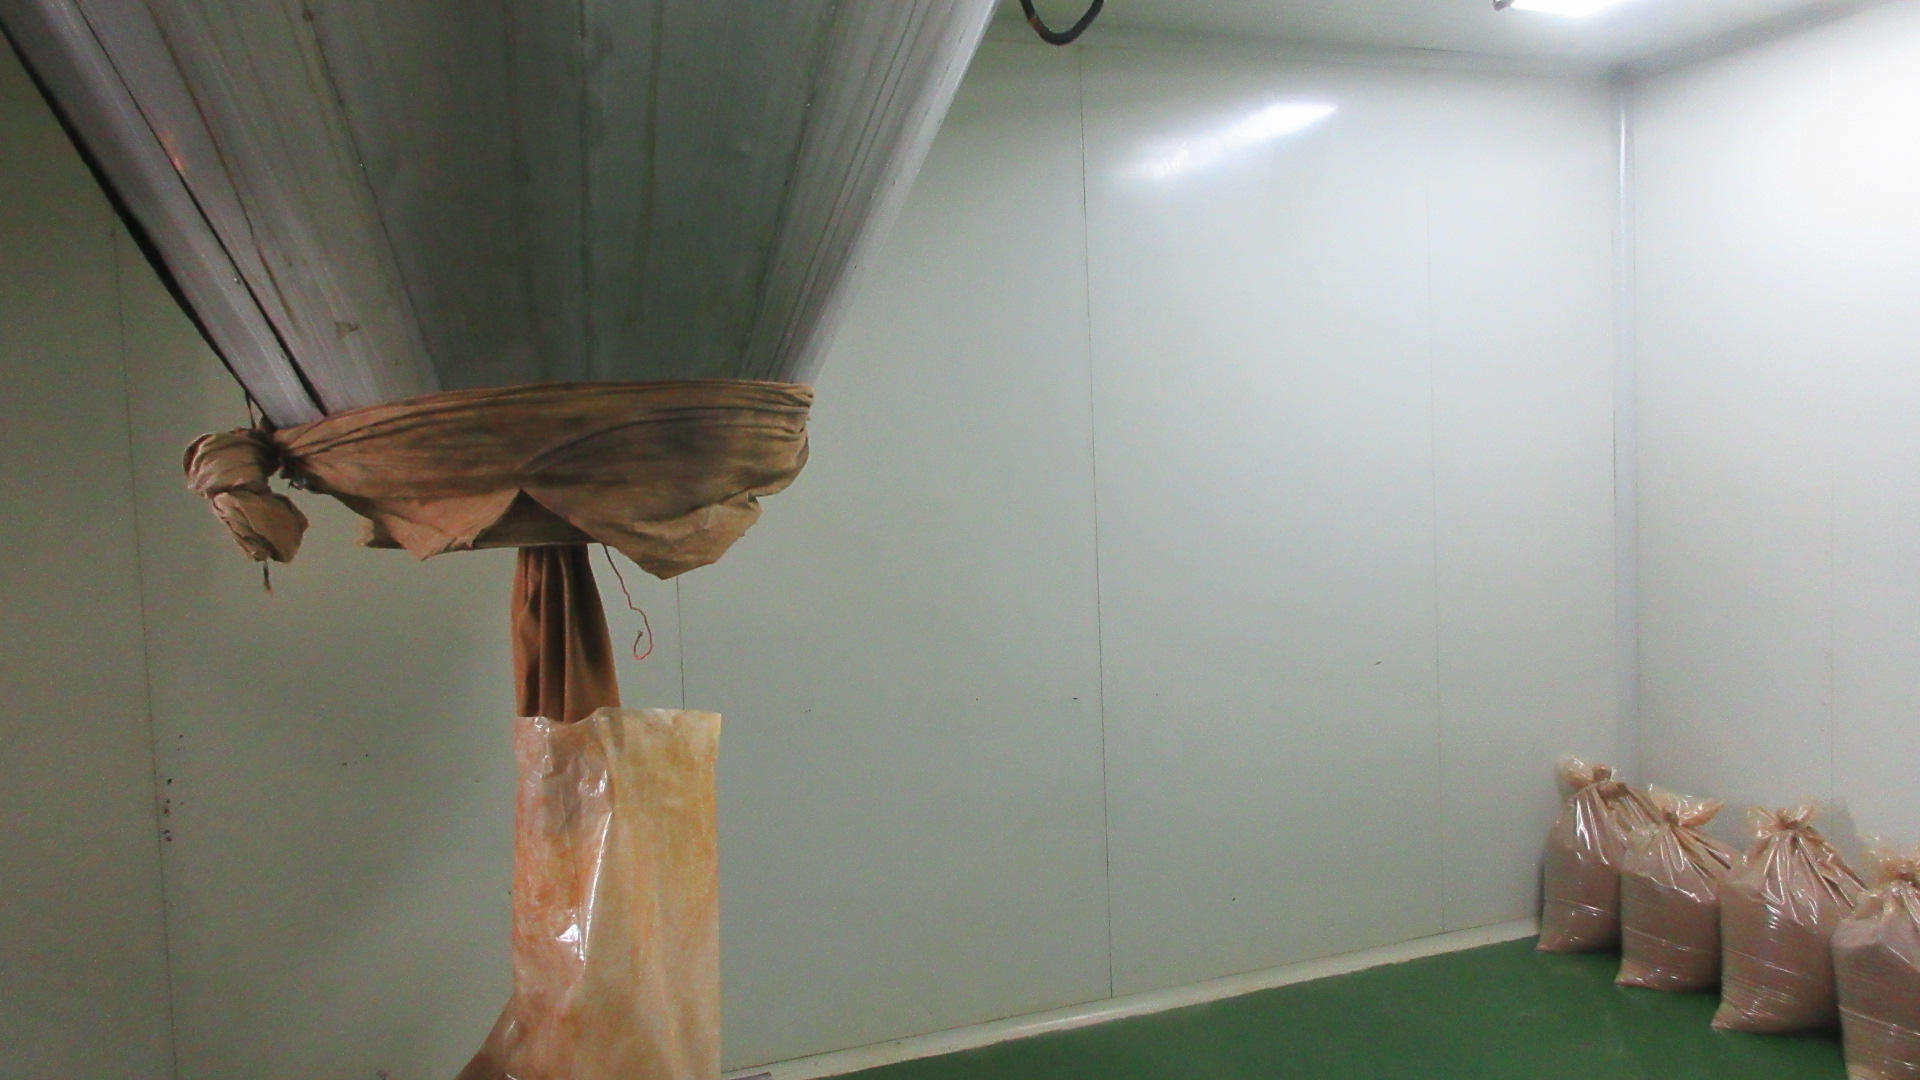
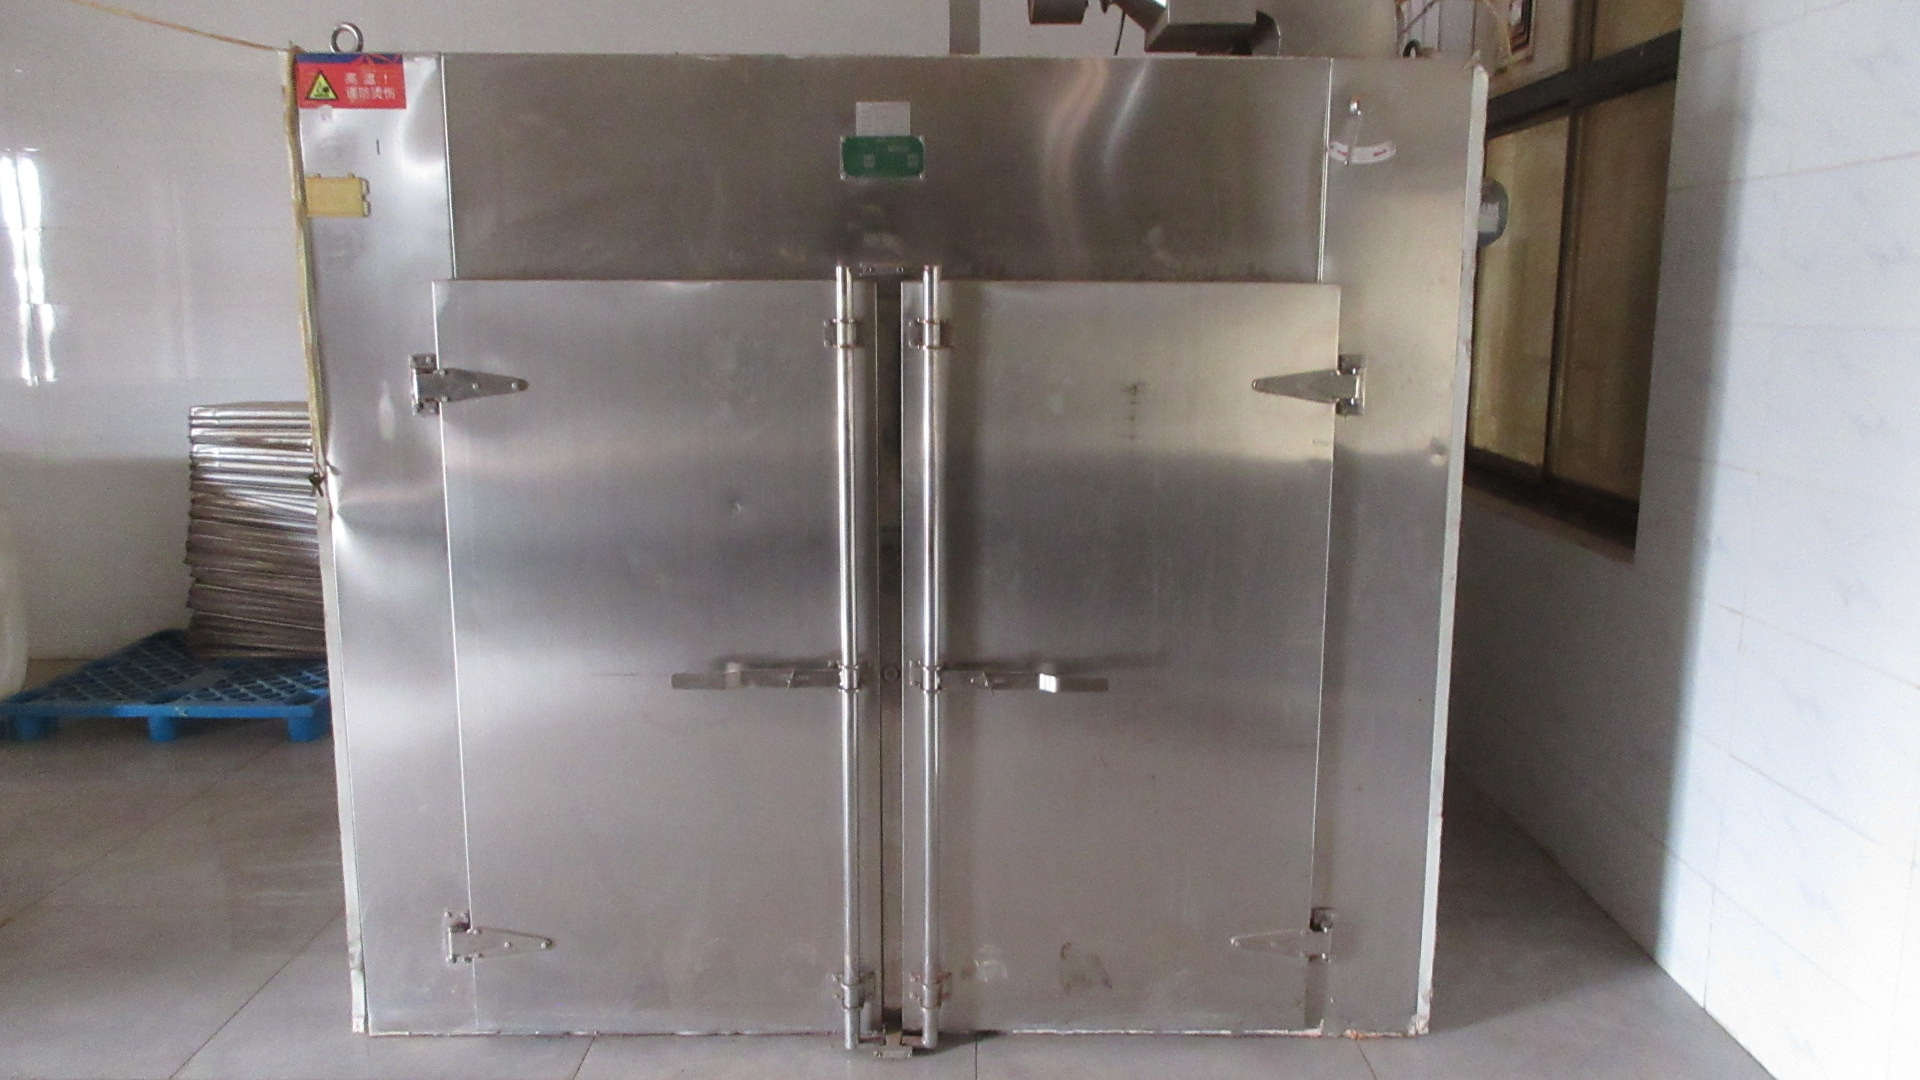
High-capacity centrifugal spray towers convert liquid concentrate into free-flowing, instantly soluble micro-granules with strictly regulated water activity.
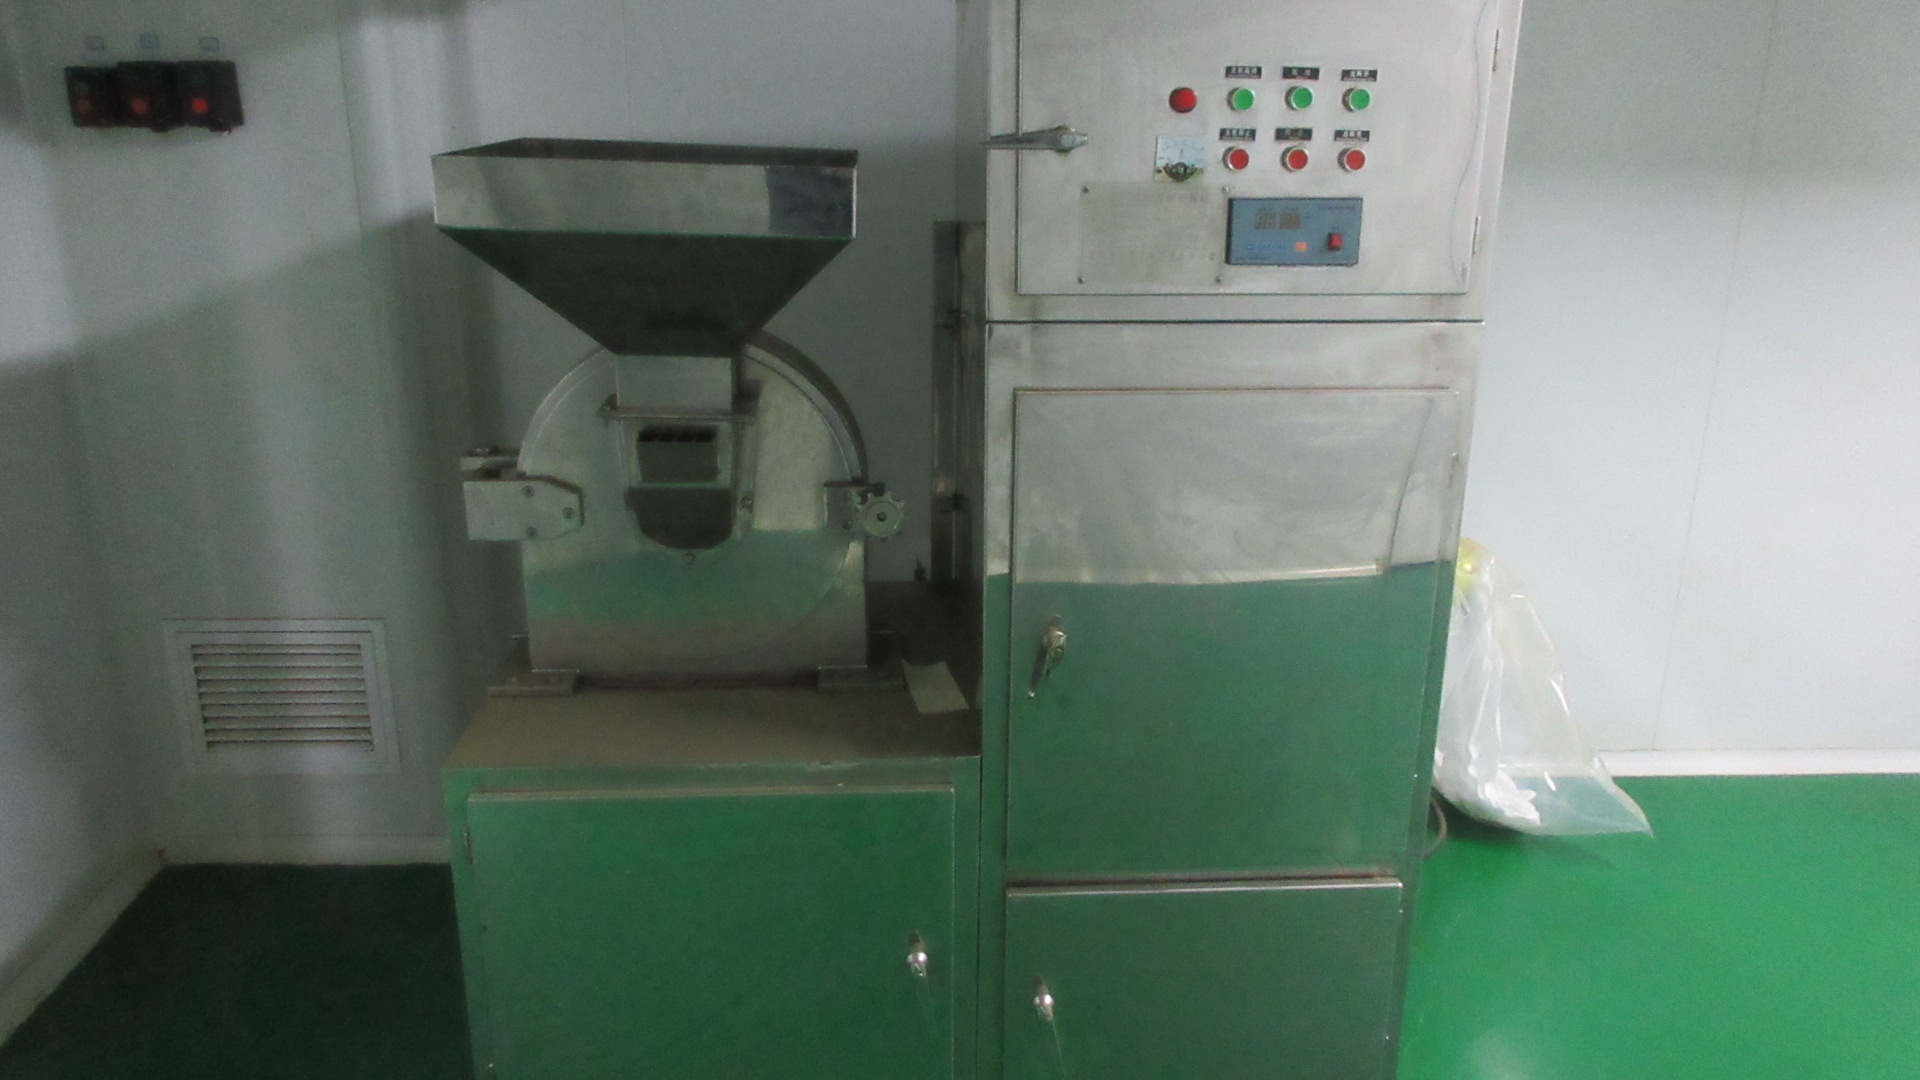 Step 06
Precision Pulverizing
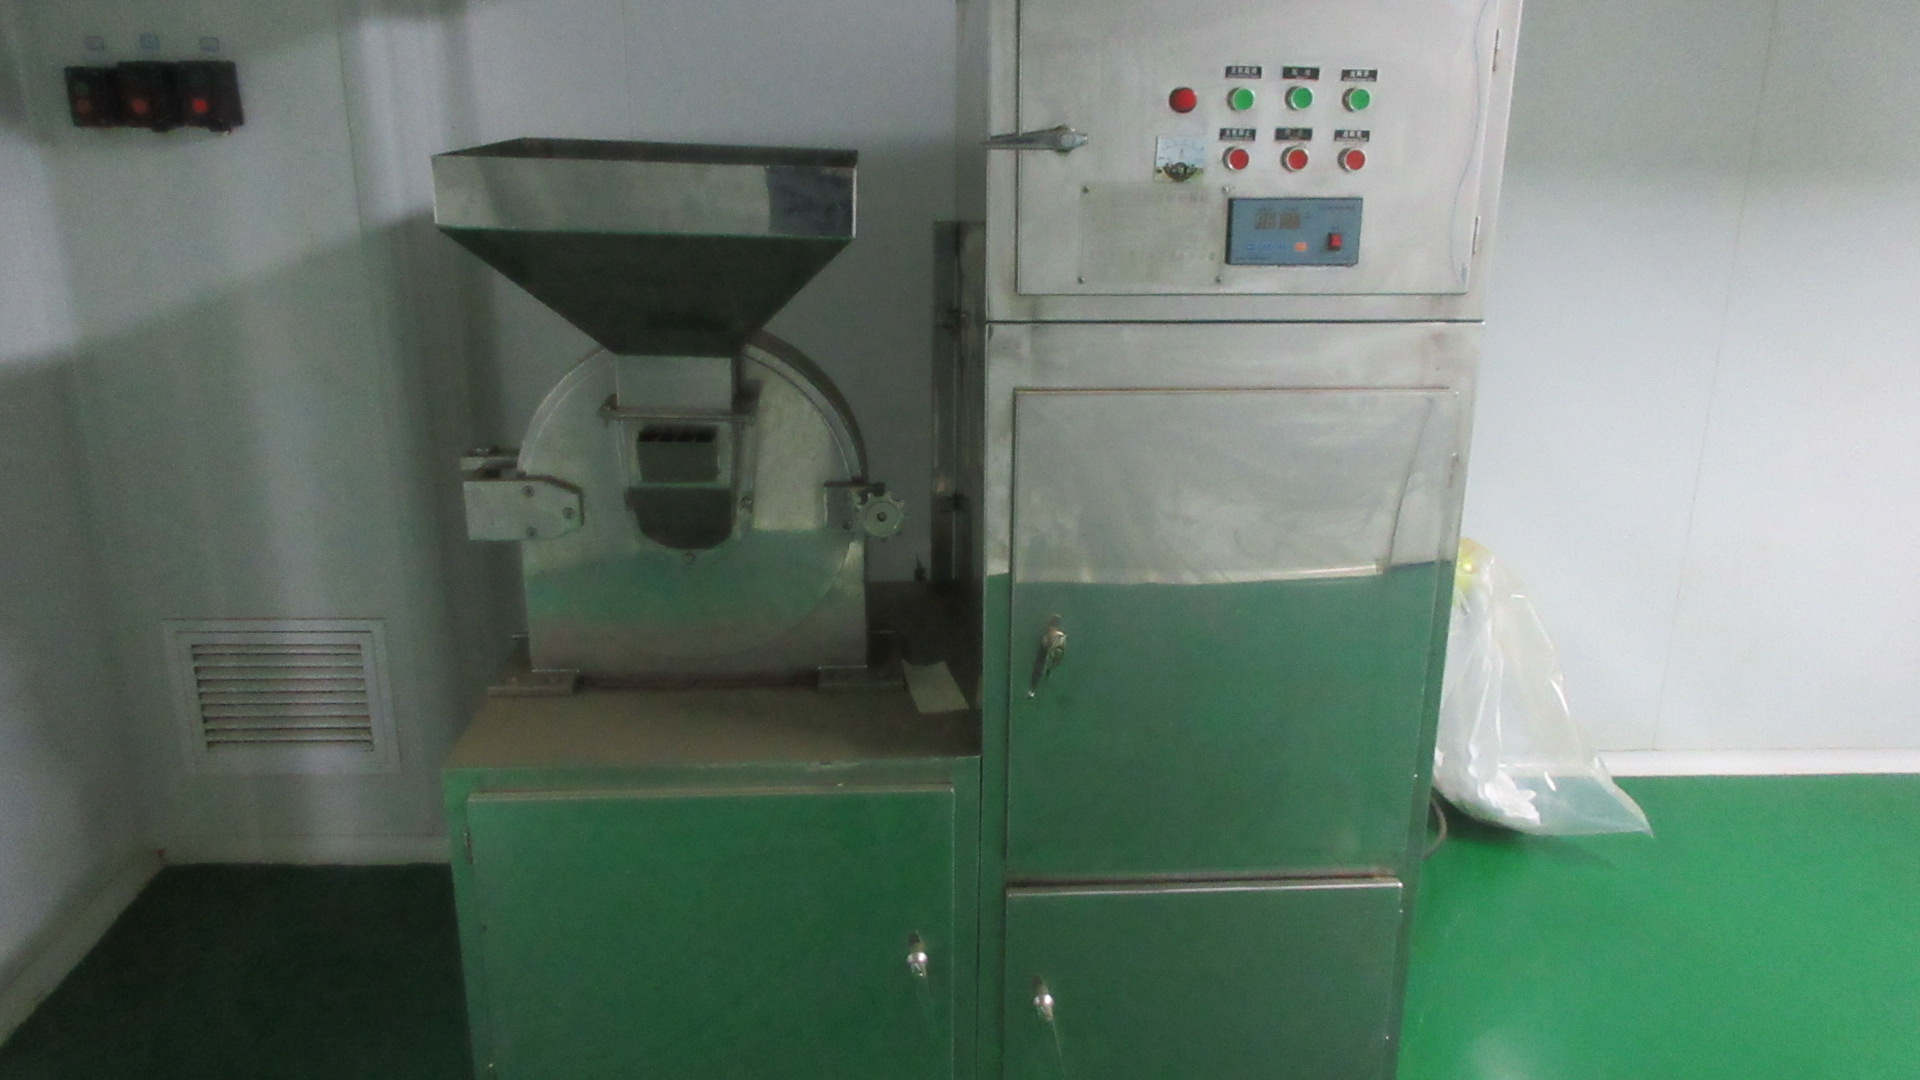
Industrial impact and air-classifier mills grind dry materials into homogeneous powders suited for capsules, tablets, or instant beverage dispersions.
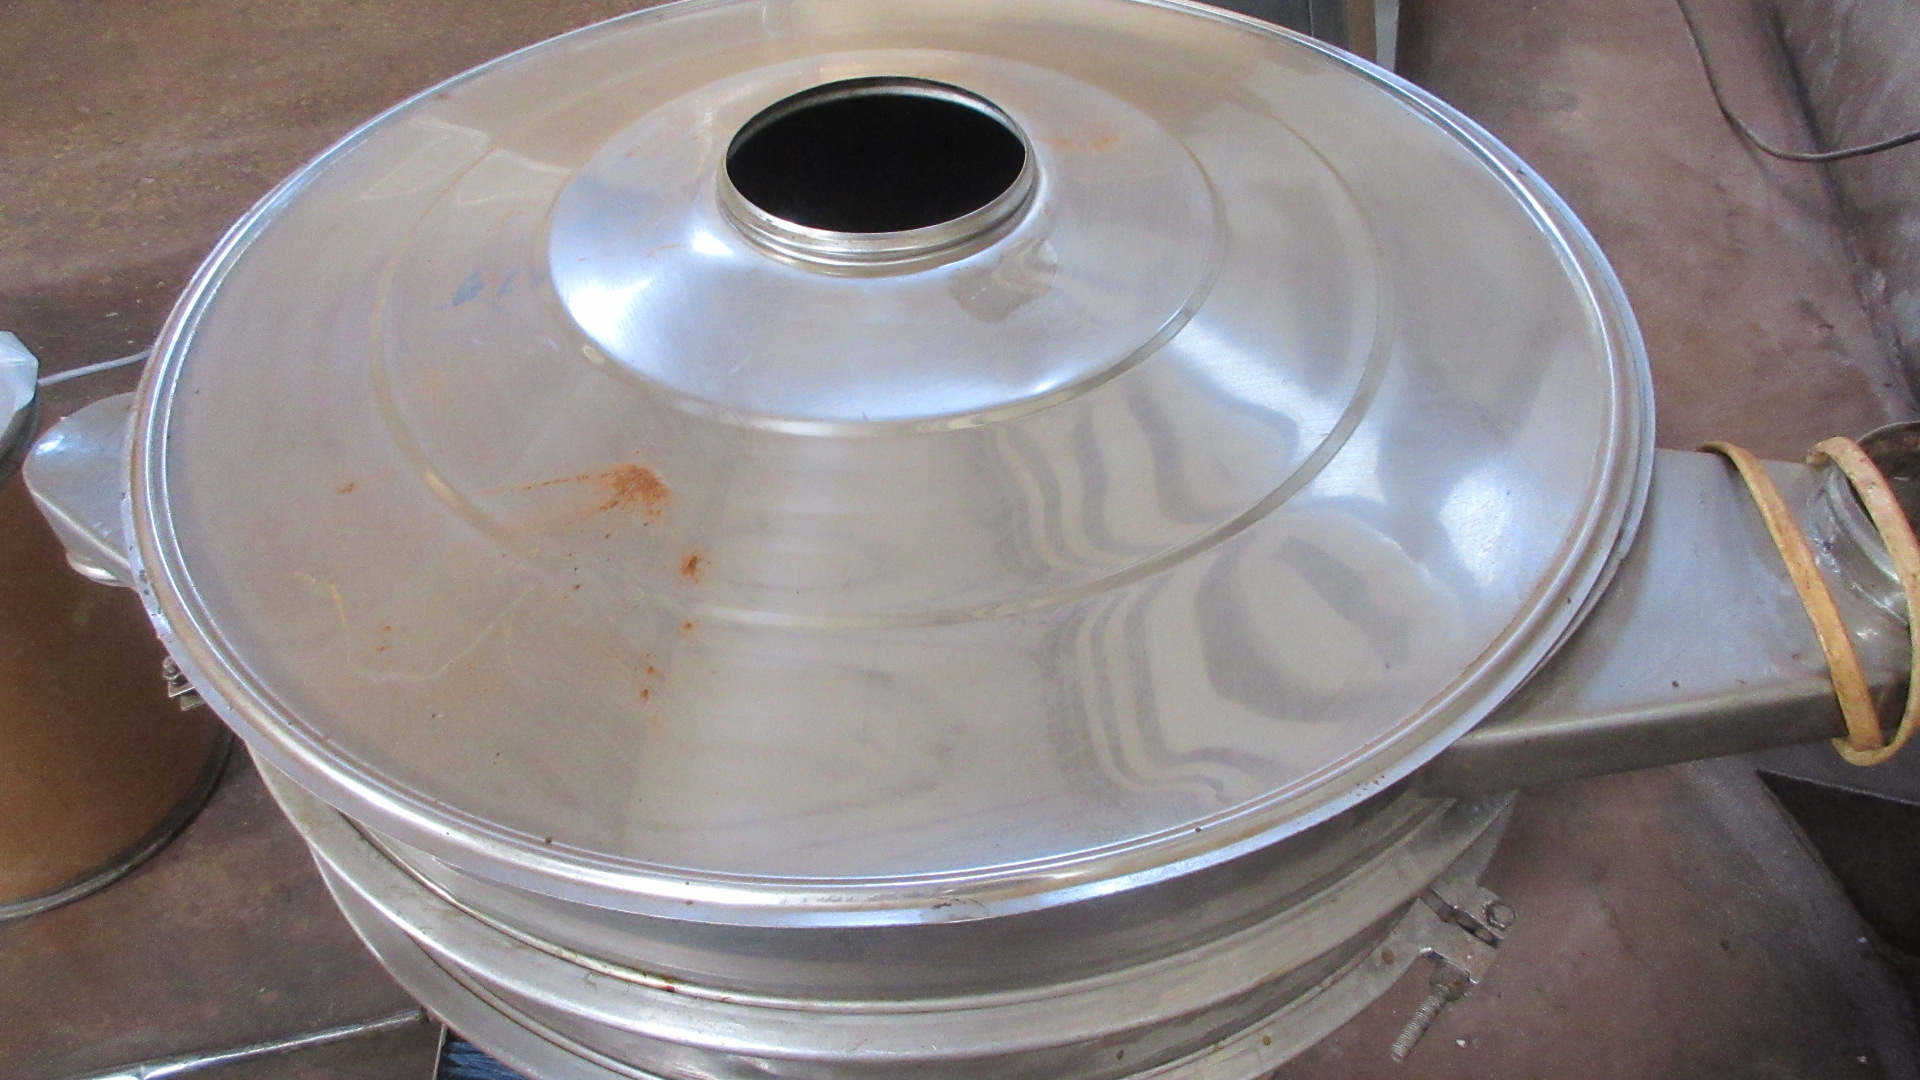 Step 07
Graded Sieving
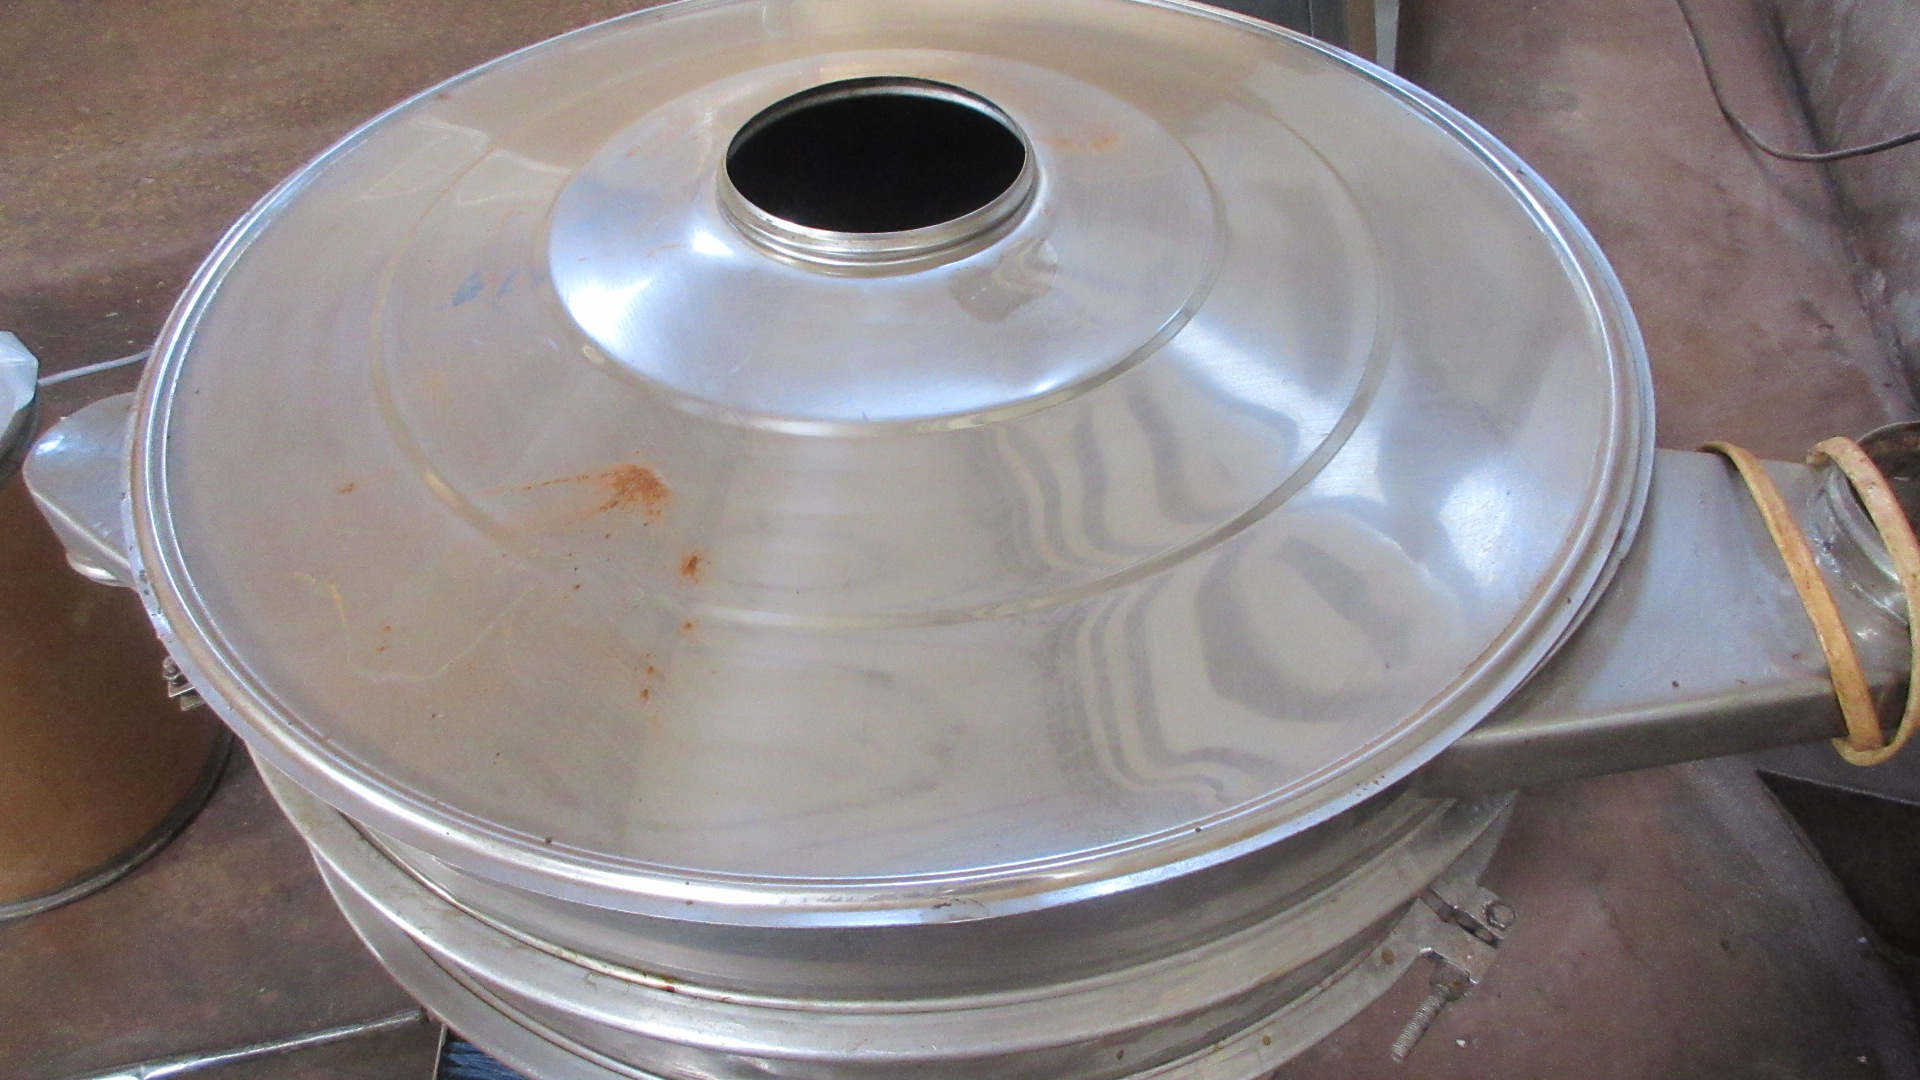
Multi-deck vibratory screens classify powder mesh sizes (80 mesh up to 450 mesh) coupled with in-line neodymium rare-earth magnet separators.
 Step 08
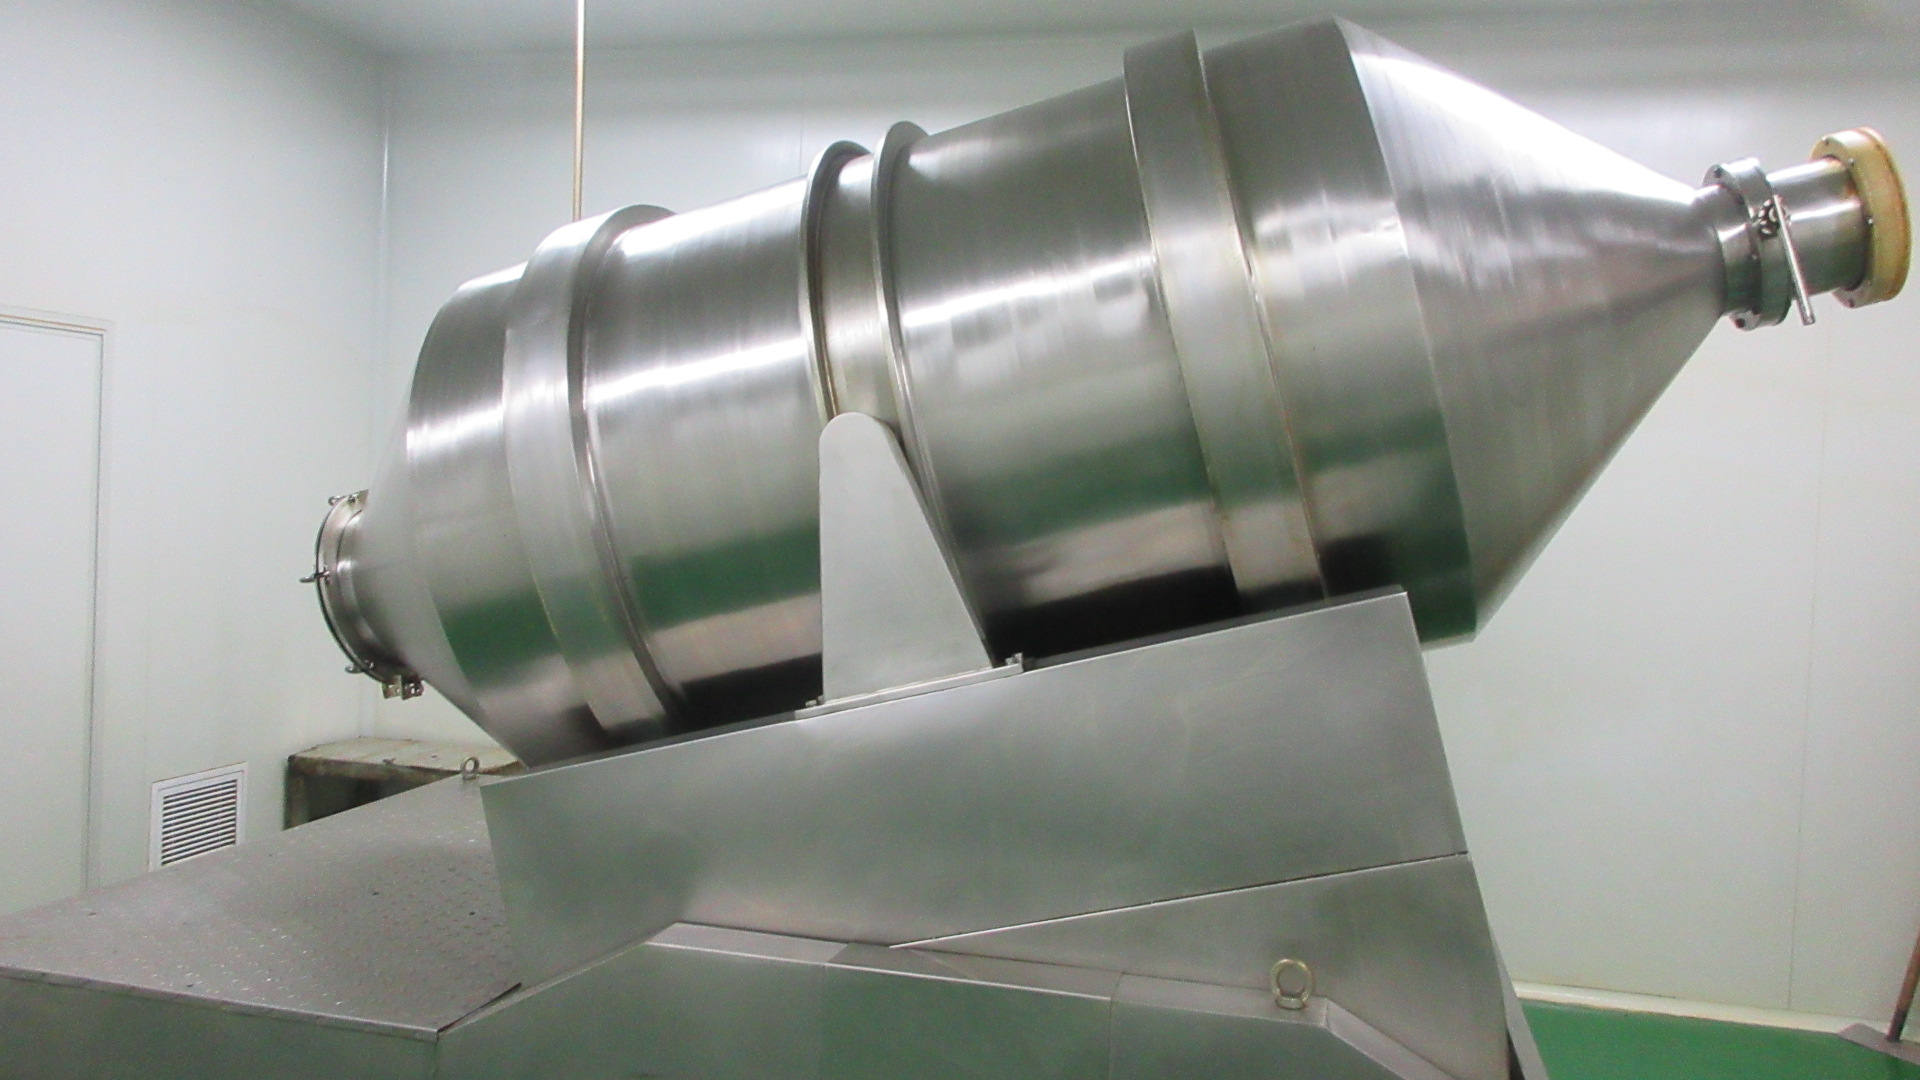
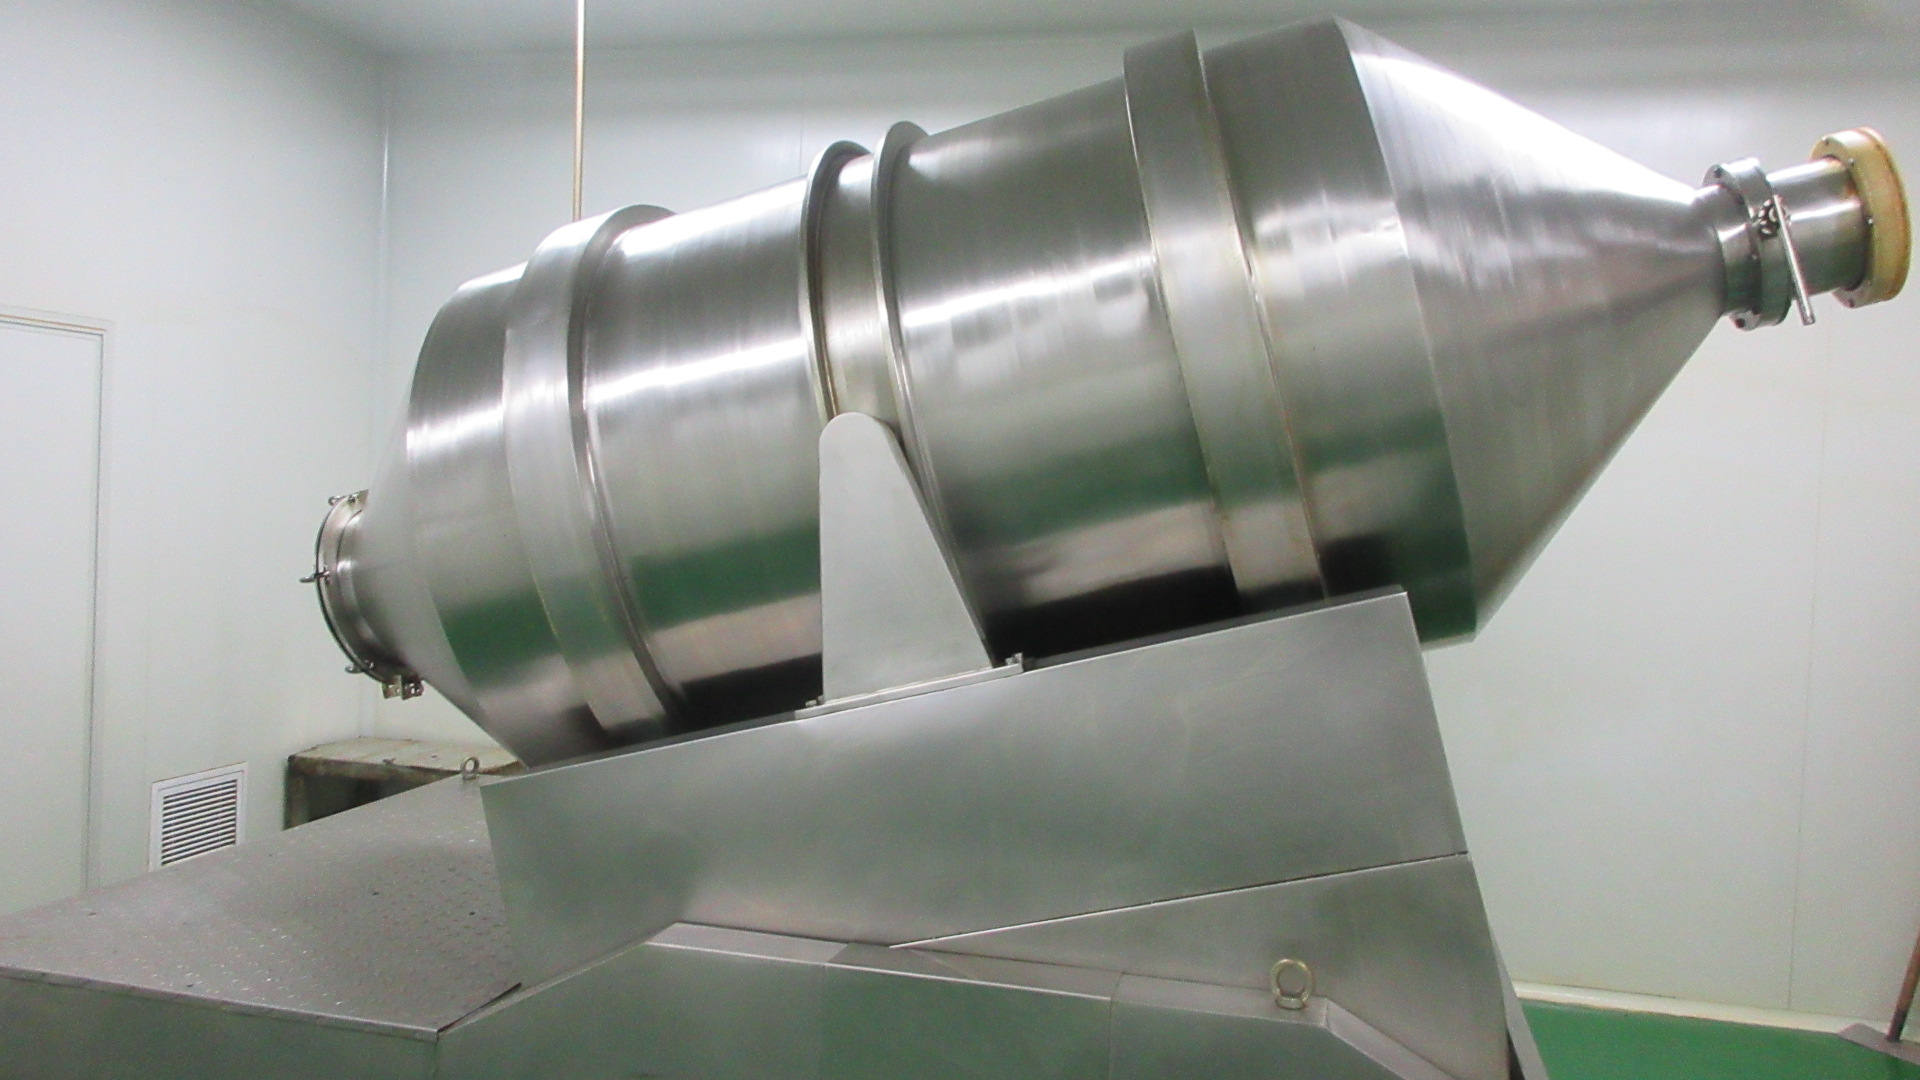
Homogeneous Mixing
Three-dimensional and ribbon mixers thoroughly standardize active compound percentages across multi-ton production batches or custom formulation blends.
 Step 09
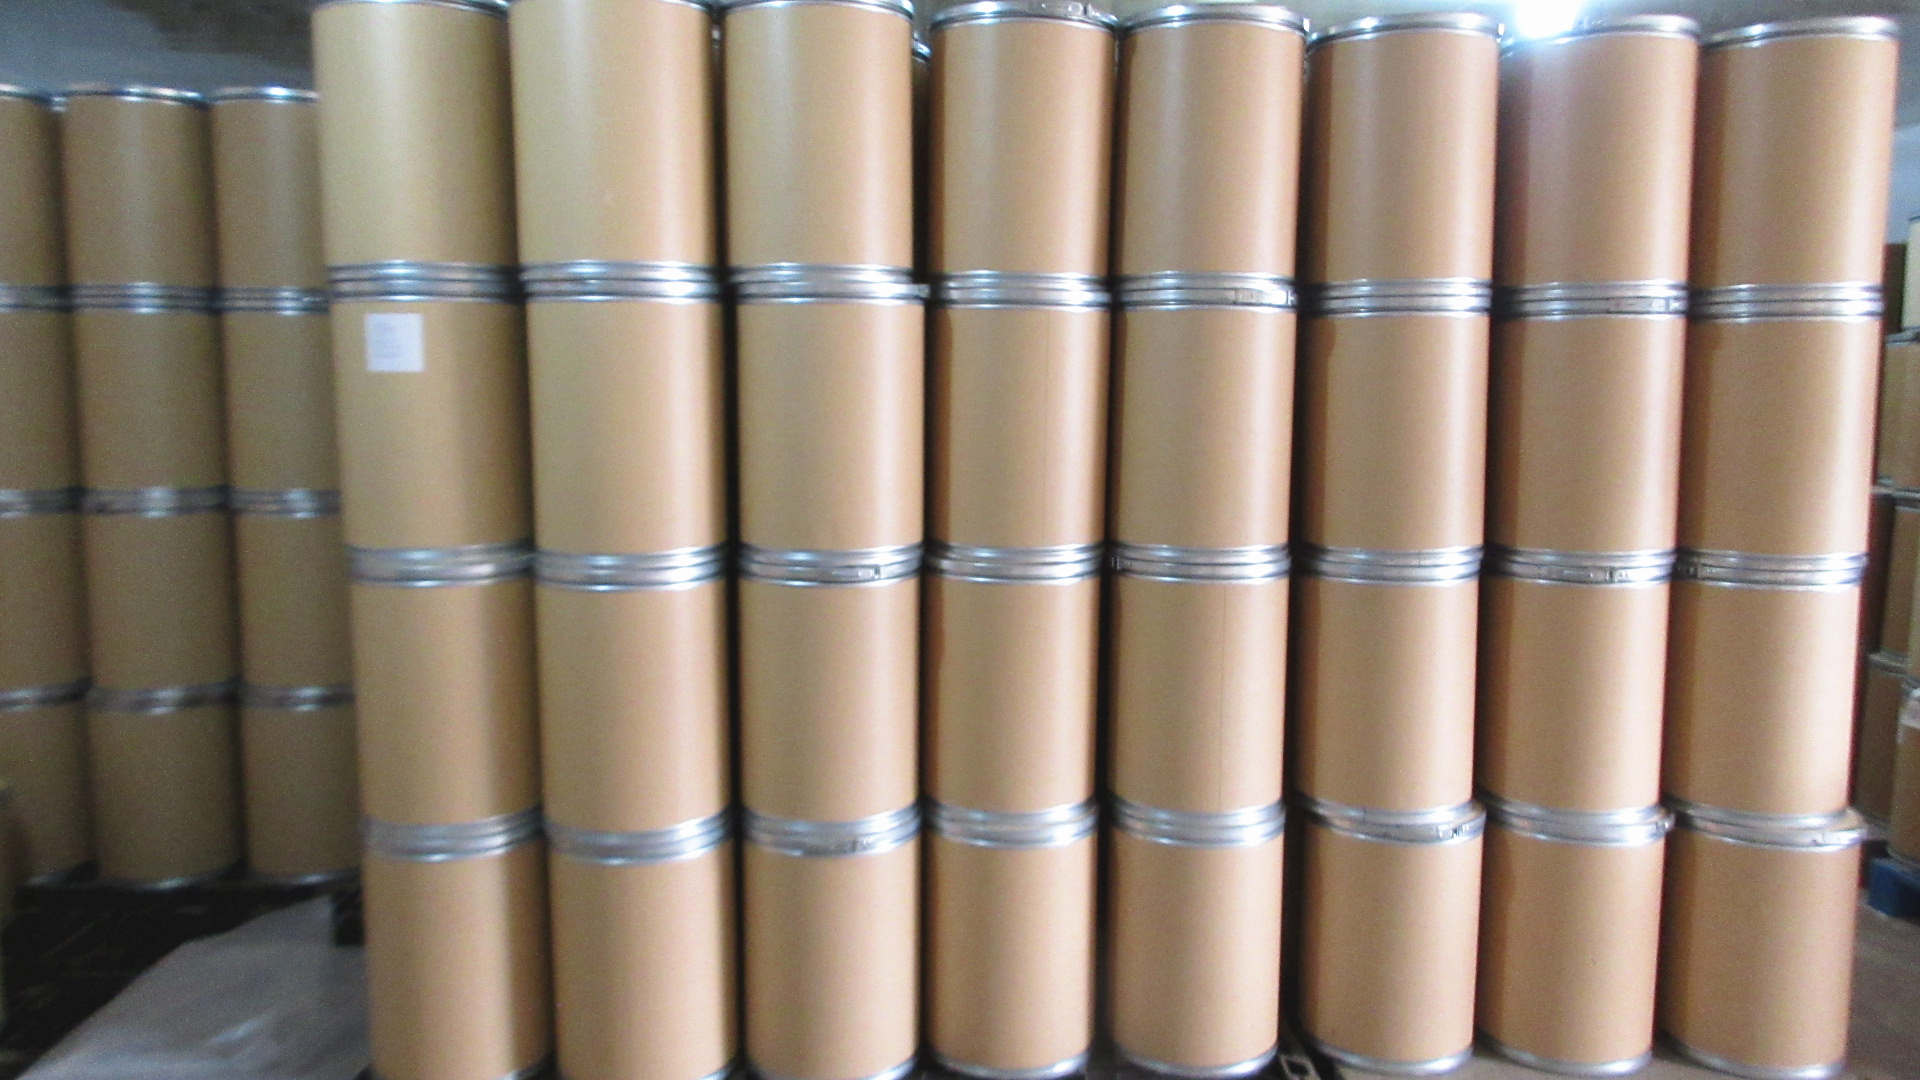
Packaging & Final QC
Cleanroom packaging in double food-grade polyethylene lined vacuum foil bags and fiber drums, followed by QA release verification and batch COA signing.
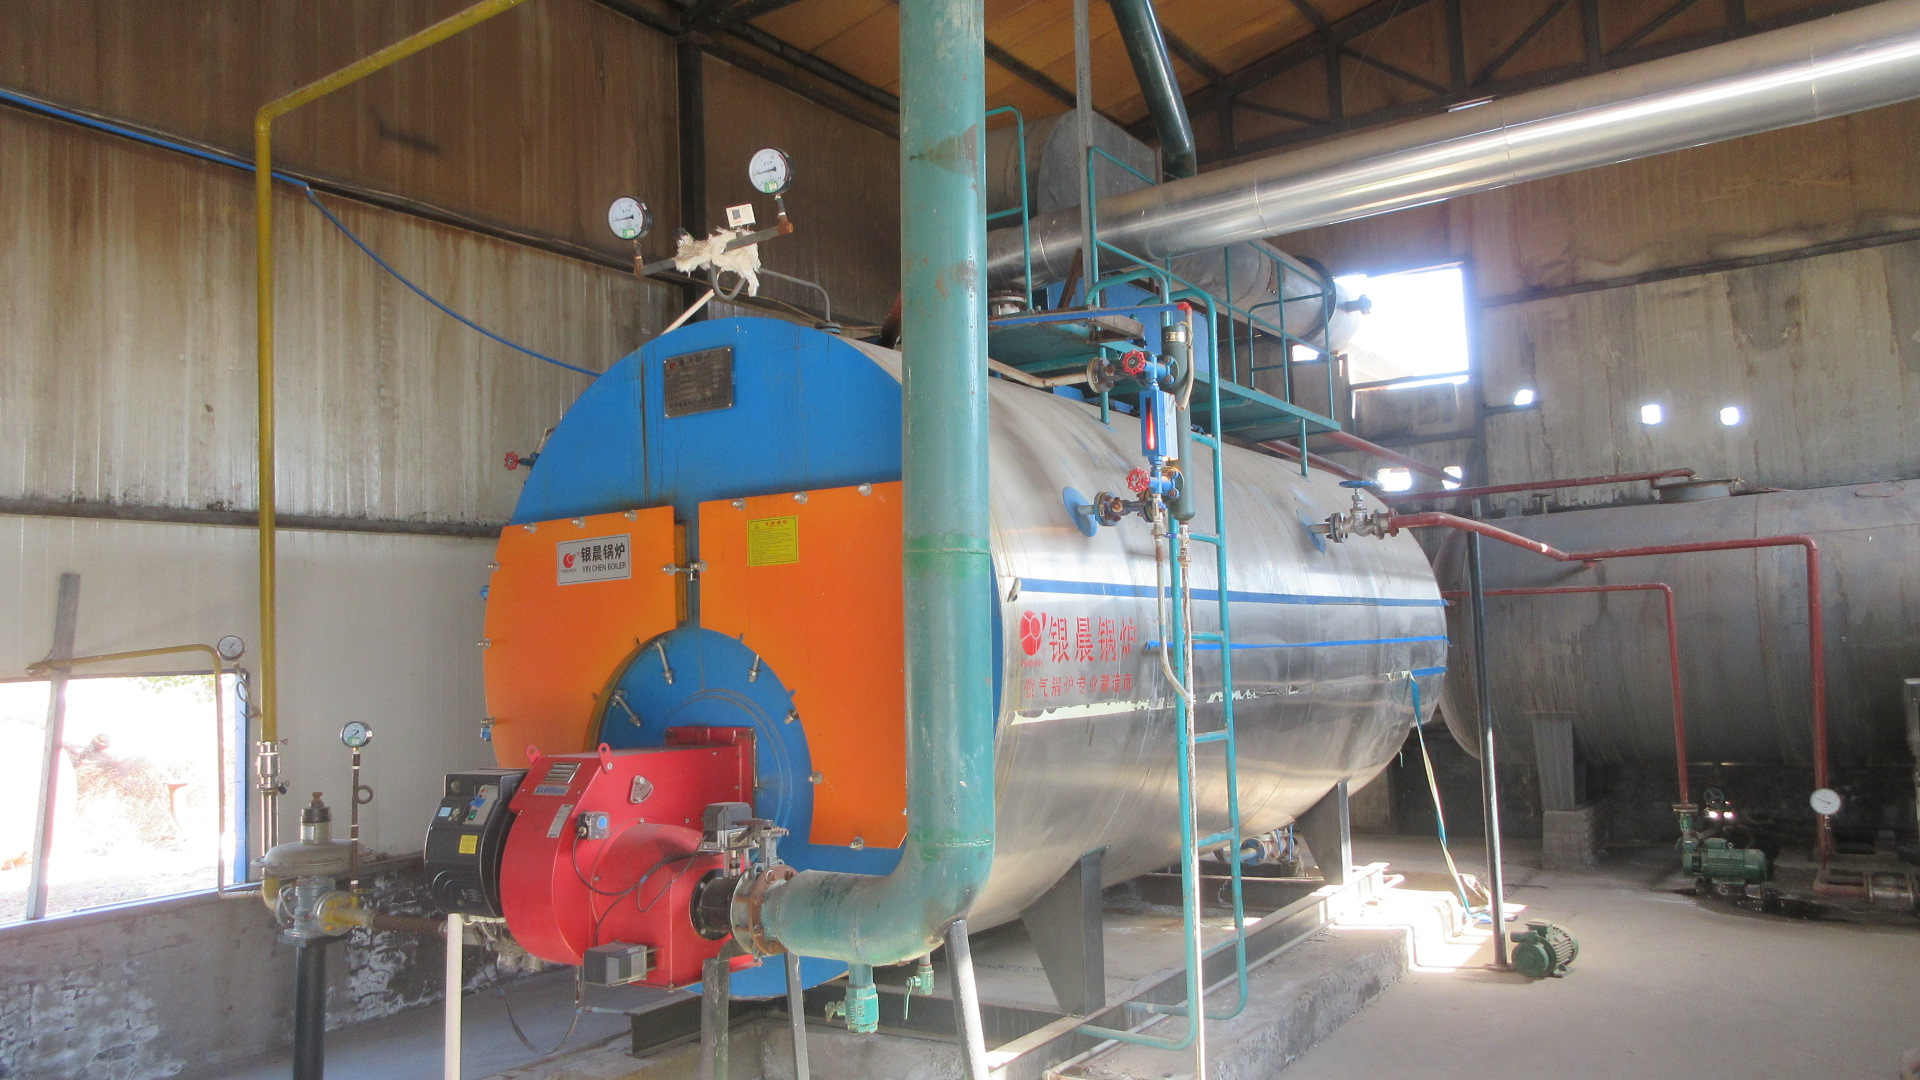
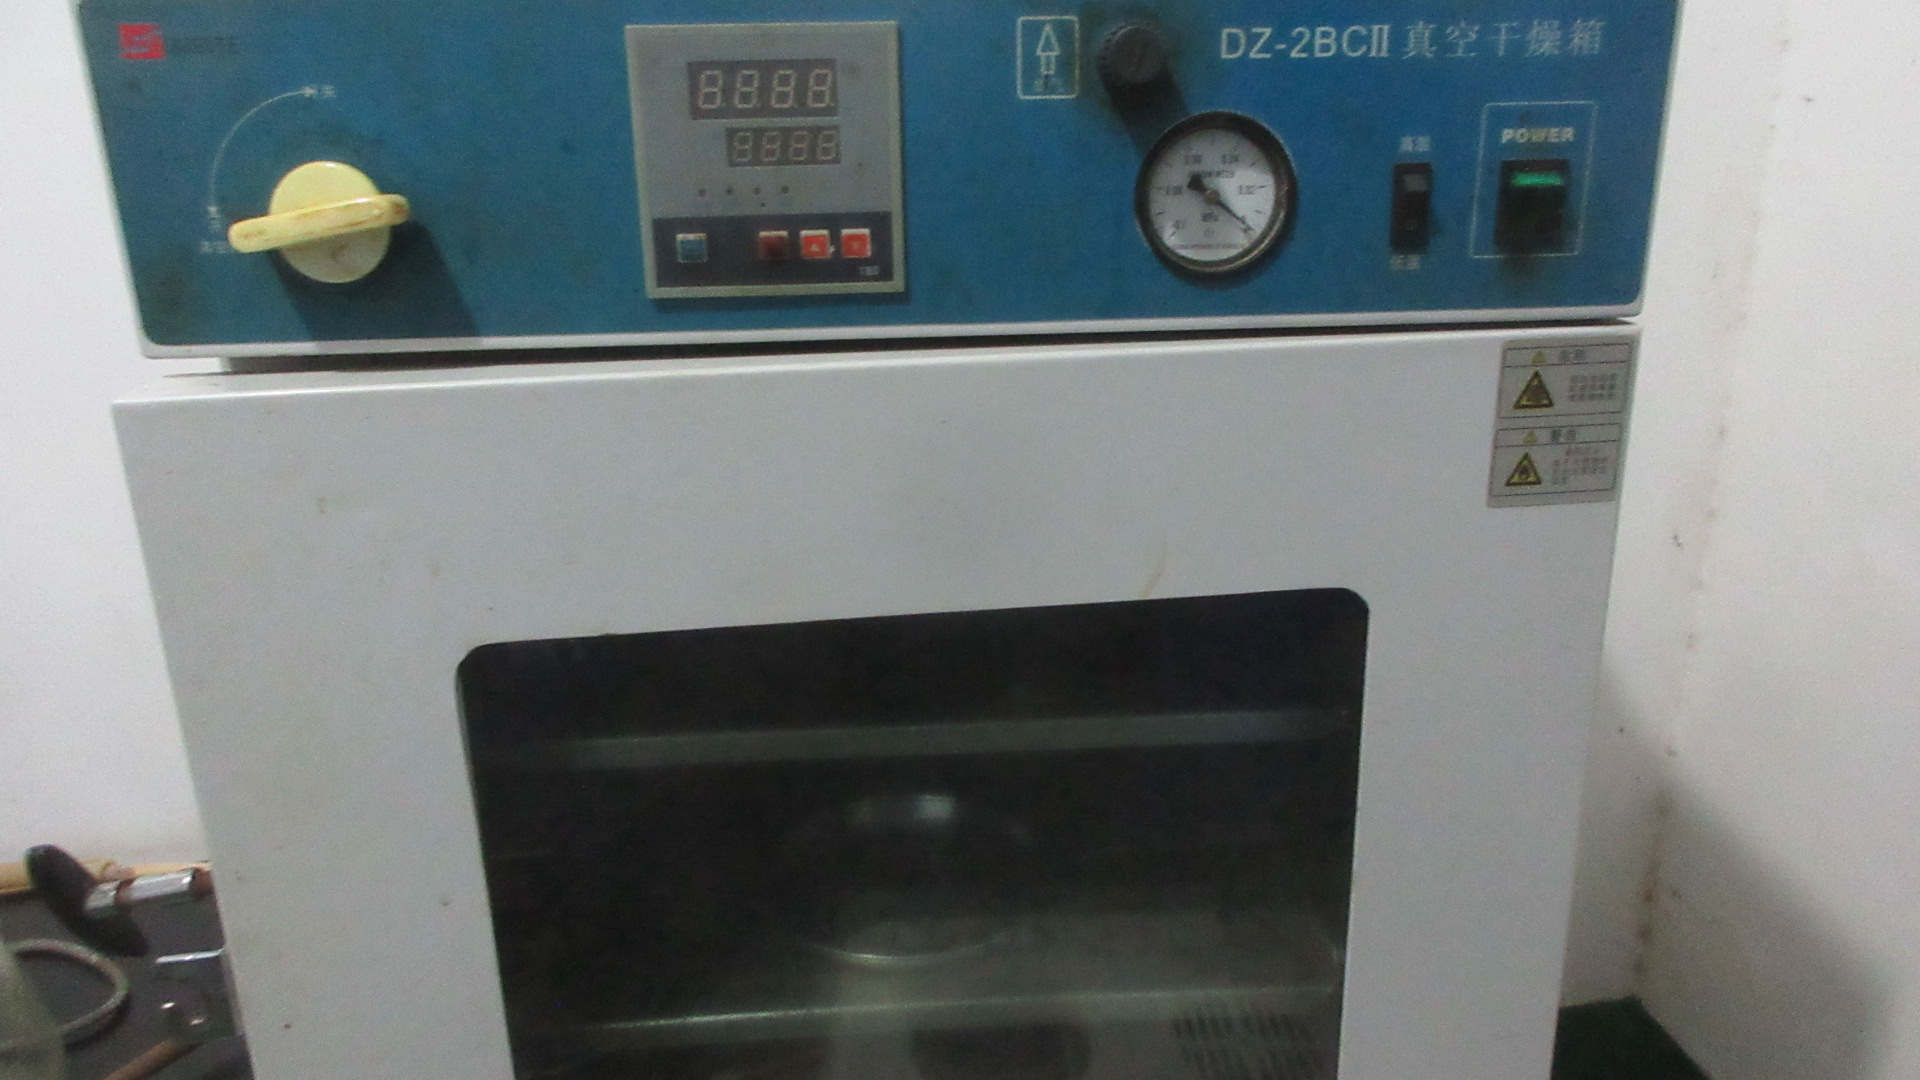
Industrial Equipment & Processing Machinery
Built with 304/316L sanitary stainless steel to ensure absolute purity and compliance with food-grade sanitary standards.
In-House Analytical Laboratory & Instruments
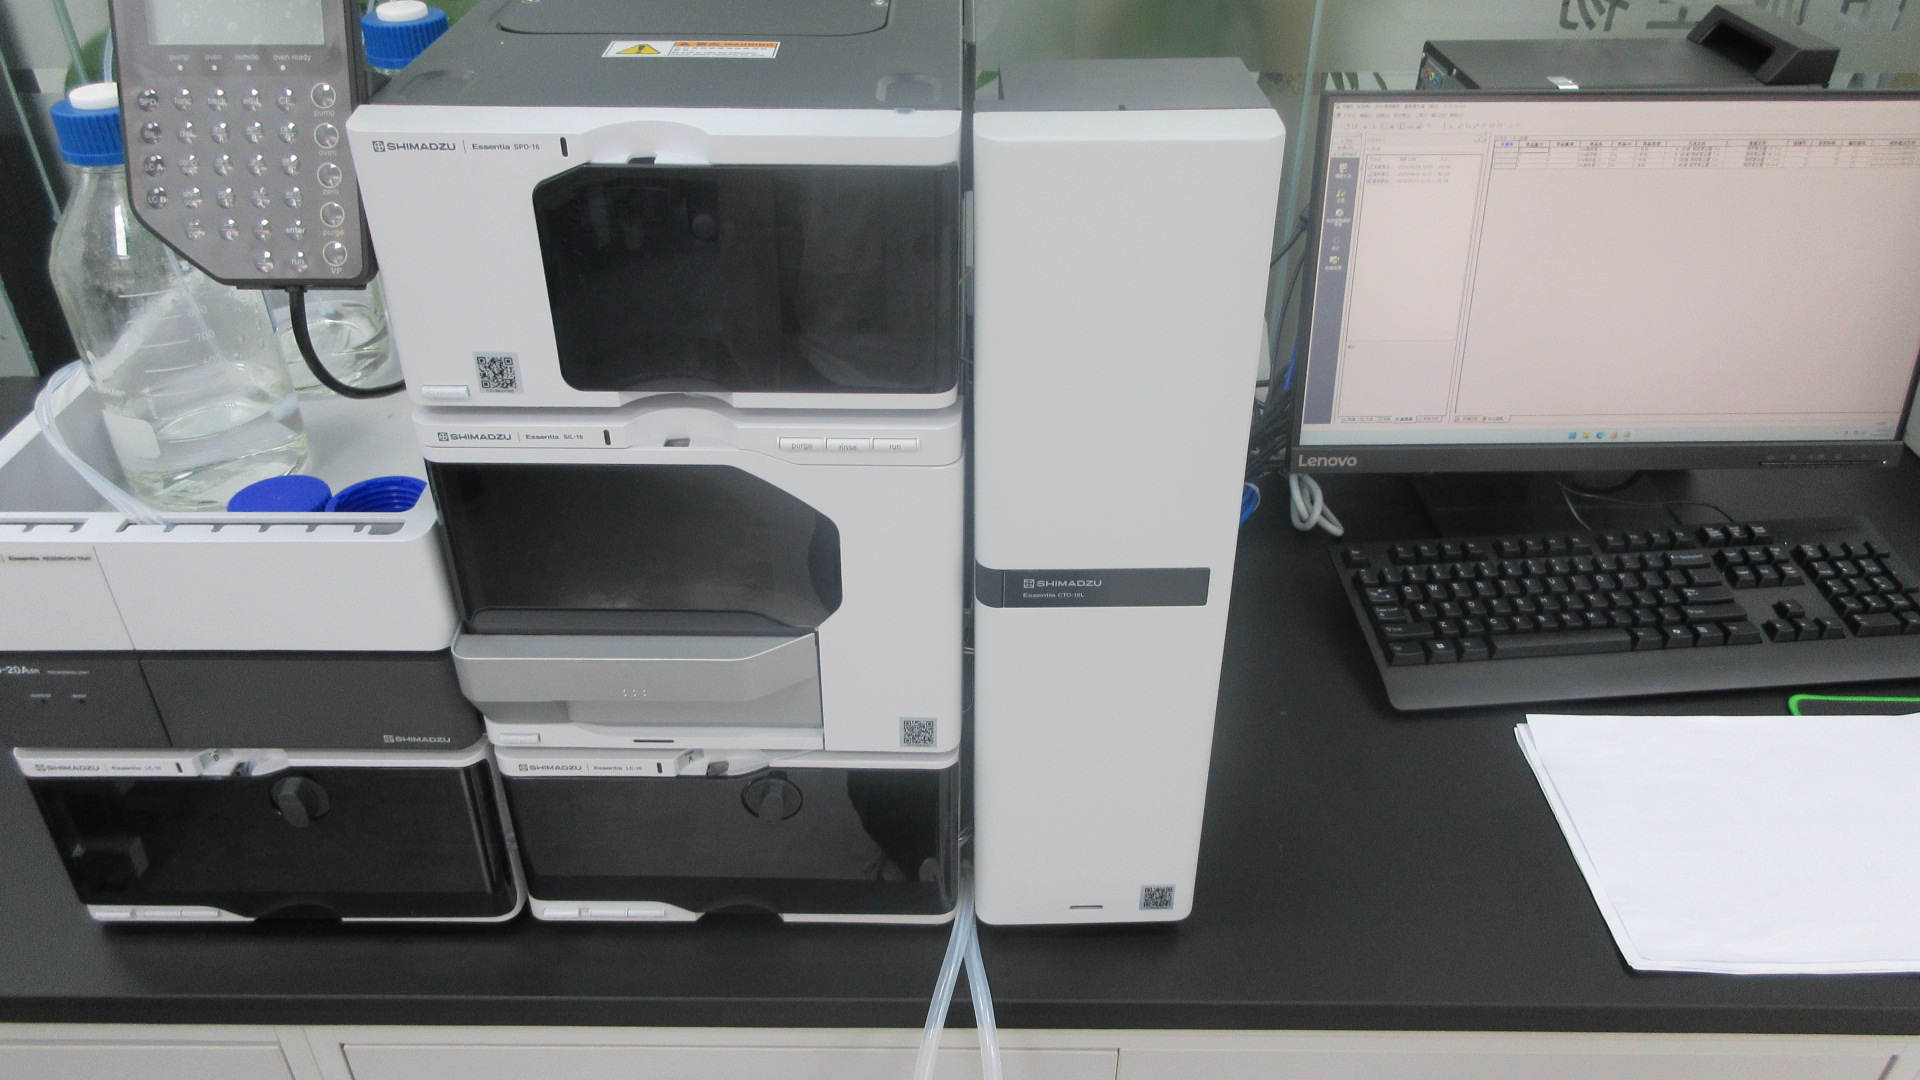
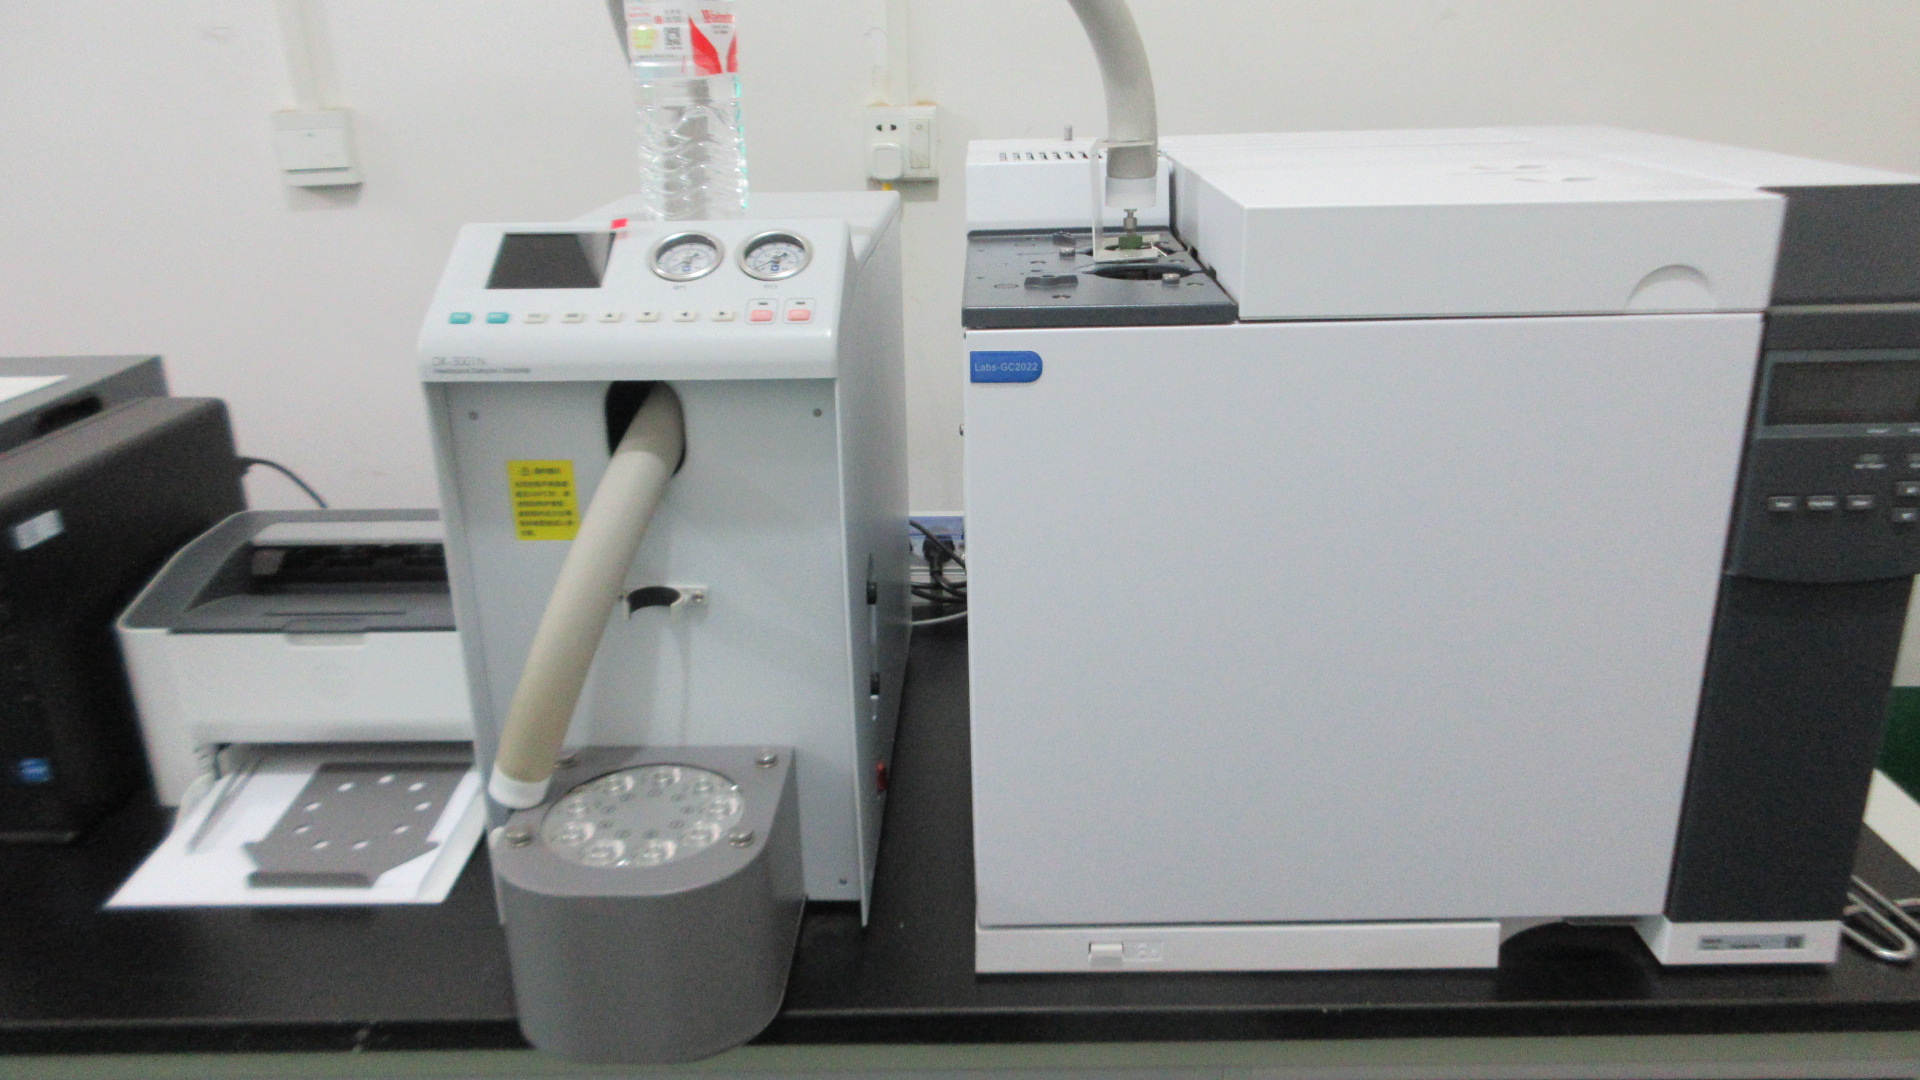
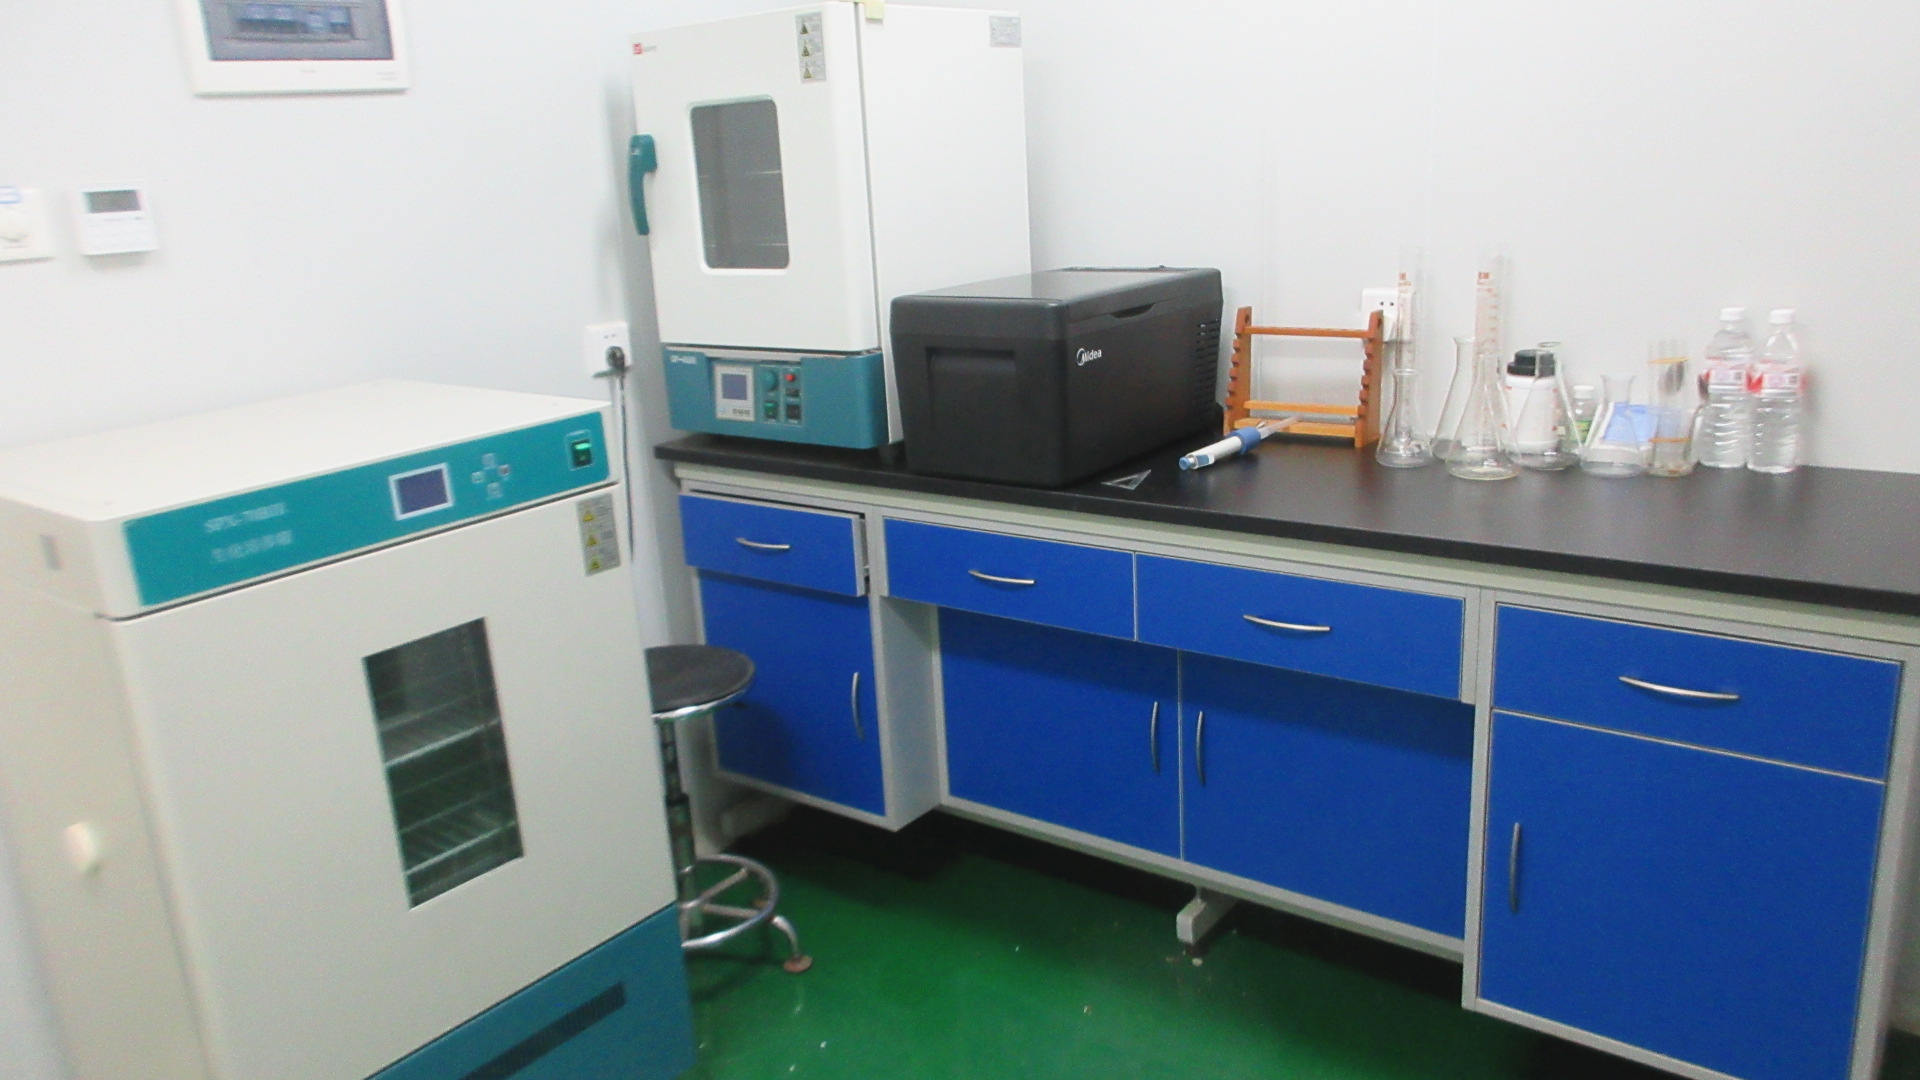
Staffed by 7 dedicated QA/QC chemists and 4 R&D engineers, our testing facility verifies molecular purity, residual solvents, heavy metals, and microbiology.
| Testing Parameter | Analytical Instrument | Verification Purpose |
|---|---|---|
| Assay & Marker Identification | High-Performance Liquid Chromatography (HPLC) | Quantifies active percentages (NMN ≥99%, Chlorophyllin, Arbutin, Mogrosides). |
| Residual Solvents Screening | Gas Chromatography (GC) with FID | Ensures ethanol, methanol, ethyl acetate comply with USP/EP monographs. |
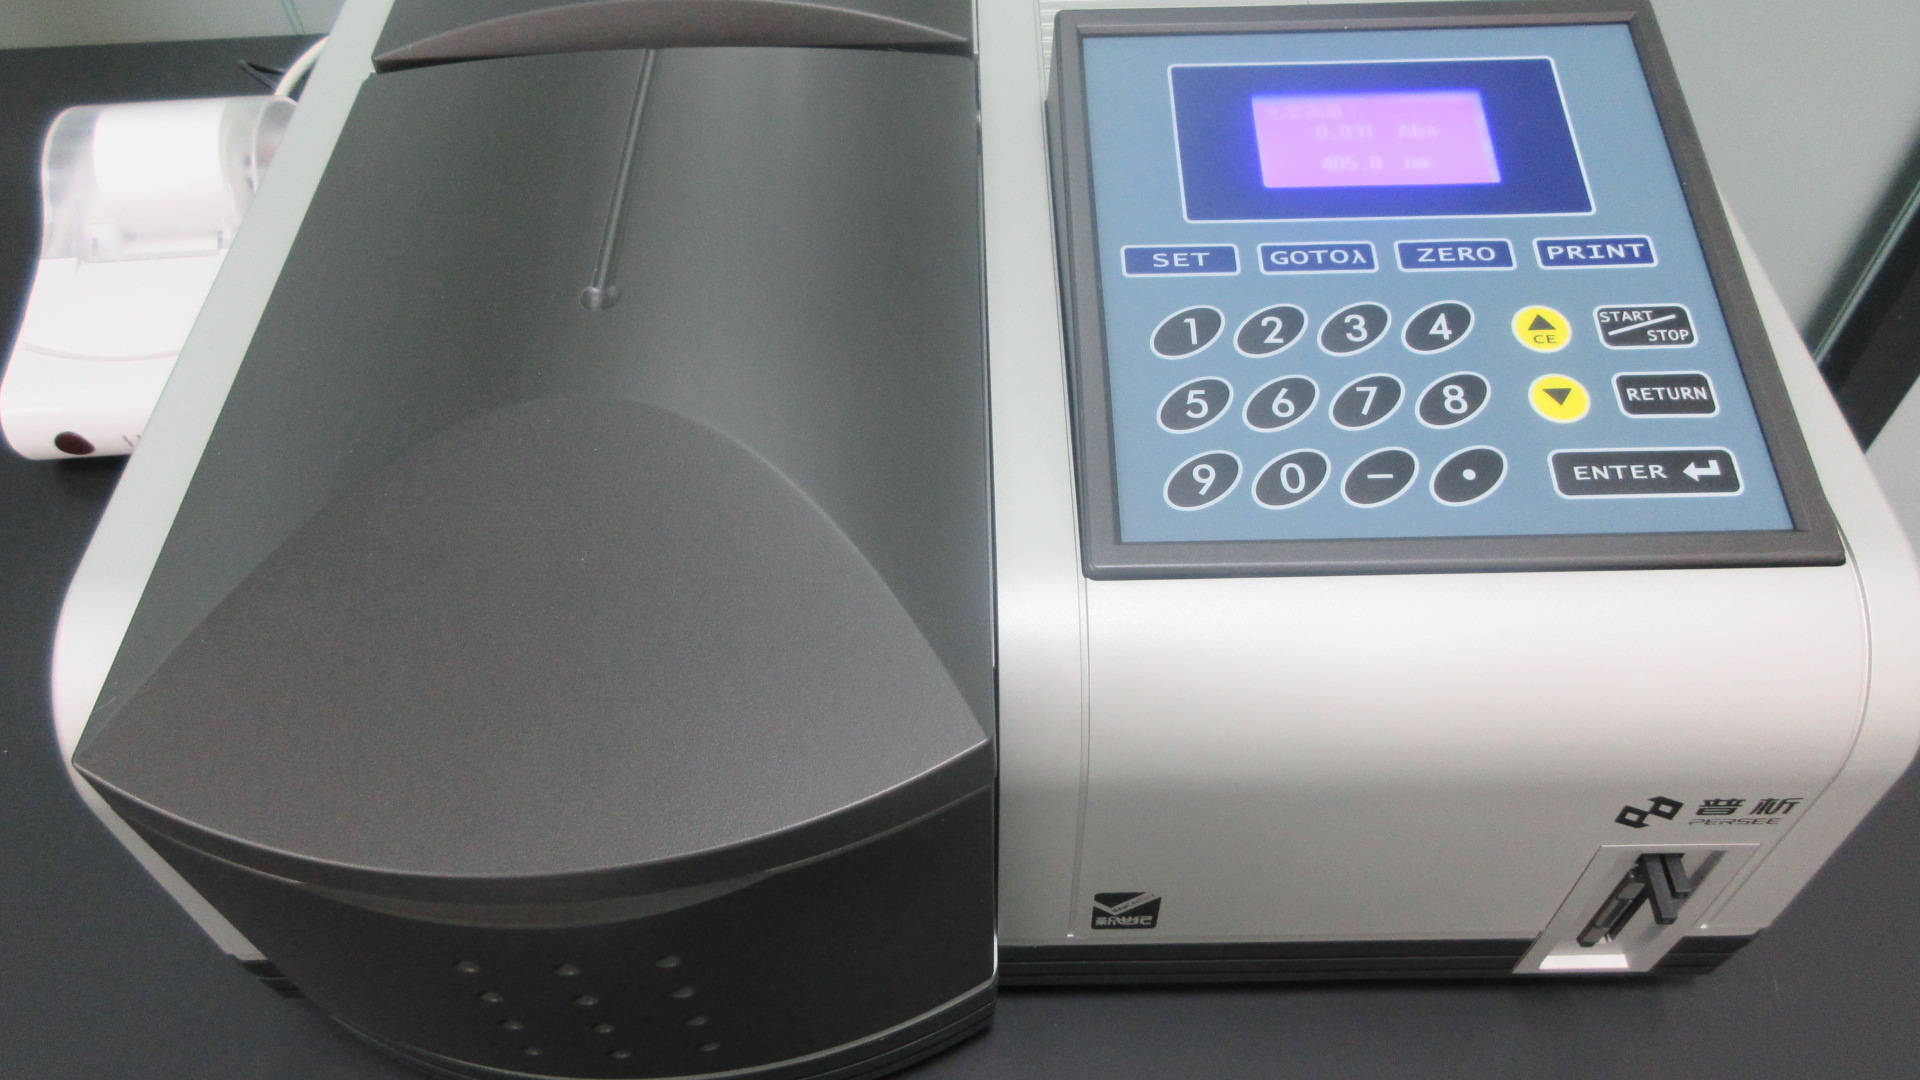
| Total Polysaccharide & Color | UV-Vis Spectrophotometer | Measures mushroom glucans, phycocyanin E-value, and plant pigment absorption. |
| Heavy Metals (Pb, As, Cd, Hg) | Atomic Absorption / ICP-MS (Partner) | Enforces strict EU regulation 2023/915 and US FDA food contact thresholds. |
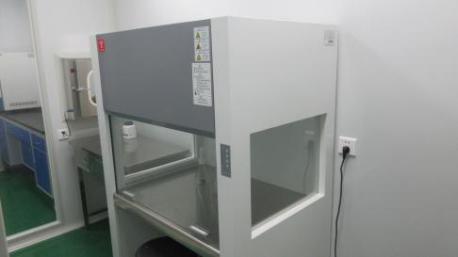
| Microbiological Safety | Class 10,000 Clean Bench & Incubators | Plate count, Yeast & Mold, Salmonella, E. coli, and Staphylococcus aureus. |
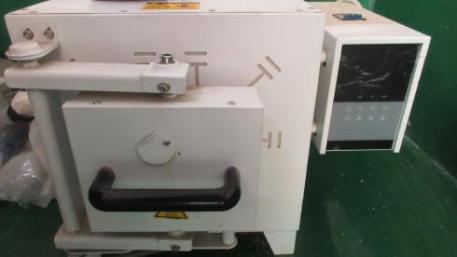
| Moisture & Ash Content | Halogen Moisture Meter & Muffle Furnace | Validates Loss on Drying (≤5%) and Total Ash residue (≤5%–9%). |
| Pesticide Multi-Residue | BS EN 15662 Standard (via SGS) | Multi-residue screening validating Organic and conventional tea/herb compliance. |
International Certifications & Test Qualifications
Certified by international auditing bodies to give food manufacturers, supplement brands, and cosmetic formulators total confidence.
ISO 22000:2018
Food Safety Management System covering botanical extracts, natural colorants, zero-calorie sweeteners & dietary supplements.
HACCP Certified
Hazard Analysis and Critical Control Points system eliminating biological, chemical, and physical food safety hazards.
USDA Organic
Compliant with NOP standards for Organic Matcha, Spirulina, Chlorella, Mushroom Powders and D-Allulose.
EU Organic
Certified organic green tea, functional mushroom extracts, plant powders, and erythritol under strict European regulations.
Halal Certified
Compliant with Islamic dietary laws for Phycocyanin, Matcha, Butterfly Pea Flower, Stevia, and Mushroom Extracts.
Kosher Certified
Certified Kosher Parve across natural fruit powders, herbal actives, coenzyme Q10, collagen and sweetening ingredients.
BS EN 15662 (SGS)
Pesticide multi-residue test reports by SGS confirming compliance for Matcha, Ube Powder, and Phycocyanin shipments.
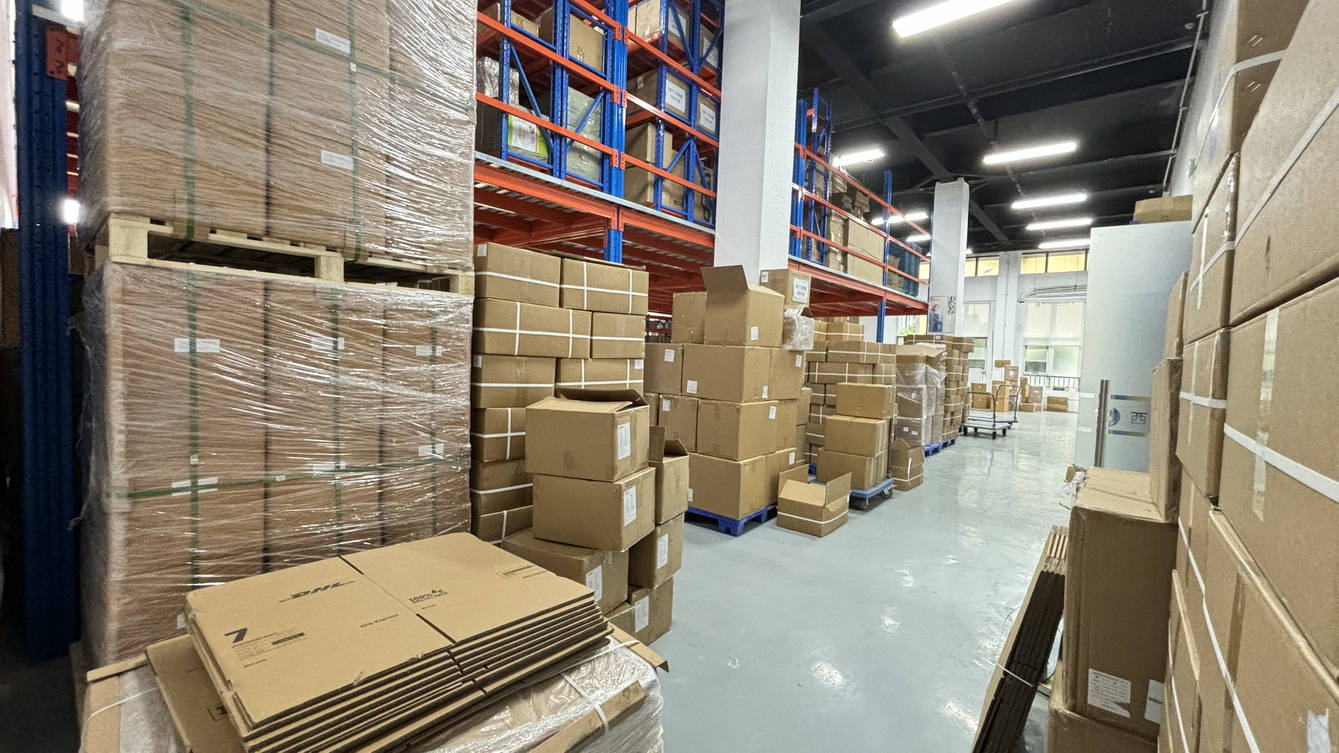
IATA DGR & IMDG
Official air transport dangerous goods certification and sea container classification reports for smooth global customs transit.
Export Operations Serving B2B Brands in 30+ Countries
From spot trial quantities to multi-container shipments, we handle cross-border logistics smoothly with full shipping documentation.
North America 30%
Serving nutritional brand formulators, private label contract packers, and food manufacturers across the United States and Canada.
Western Europe 15%
Supplying certified organic extracts, EU-compliant pesticide-free matcha, and functional mushroom extracts to the UK, Germany, and France.
Oceania 10%
Providing high-purity longevity molecules (NMN, NAD+), collagen peptides, and superfood blends to Australia and New Zealand.
Middle East 8%
Regular Halal-certified shipments of natural food colorants, plant sweeteners, and botanical beverage powders to UAE and Saudi Arabia.
South America 5%
Delivering active cosmetic raw materials, functional extracts, and bulk food ingredients with complete legal and phytosanitary certificates.
Southeast Asia & Others 27%
Serving beverage, confectionery, and functional wellness producers across Japan, South Korea, Thailand, Singapore, and beyond.
Nearest Departure Ports
Shanghai Port, Ningbo Port, Tianjin Port, Qingdao Port & Xi'an International Air Cargo
Accepted Trade Incoterms
FOB, CFR, CIF, EXW, FCA, CPT, CIP, DDP & Express Door-to-Door Delivery
Accepted Settlement Currencies
USD, EUR, GBP, CAD, AUD, JPY, CHF, HKD, CNY
Payment Settlement Methods
T/T (Wire Transfer), L/C (Letter of Credit), D/P, D/A, Credit Card, PayPal, Escrow
Request Specification Sheets, Batch COA & Factory Quote
Whether you require standard 1 kg trial validation samples or full container custom contracted lots, our technical procurement engineers respond within 4 hours with comprehensive documentation.