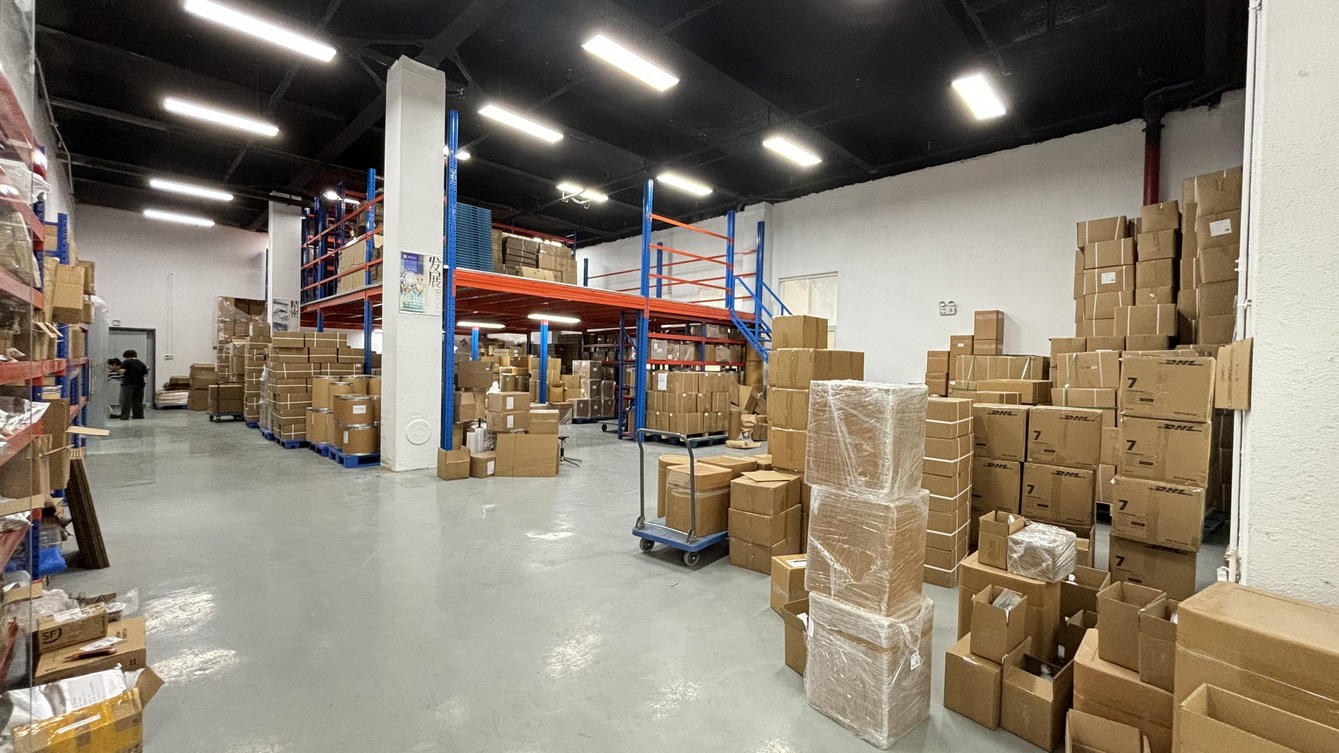
Modern Production Facility
Our facility in Xi'an features dedicated workshops for extraction, concentration, refining, and clean packaging designed for scalable bulk ingredient manufacturing.
Xi'an Vexli Bio-Tech Co., Ltd. operates standardized extraction lines, cleanrooms, and testing facilities engineered to comply with ISO 22000, HACCP, USDA Organic, EU Organic, Halal, and Kosher regulatory benchmarks.
Our facility in Xi'an features dedicated workshops for extraction, concentration, refining, and clean packaging designed for scalable bulk ingredient manufacturing.
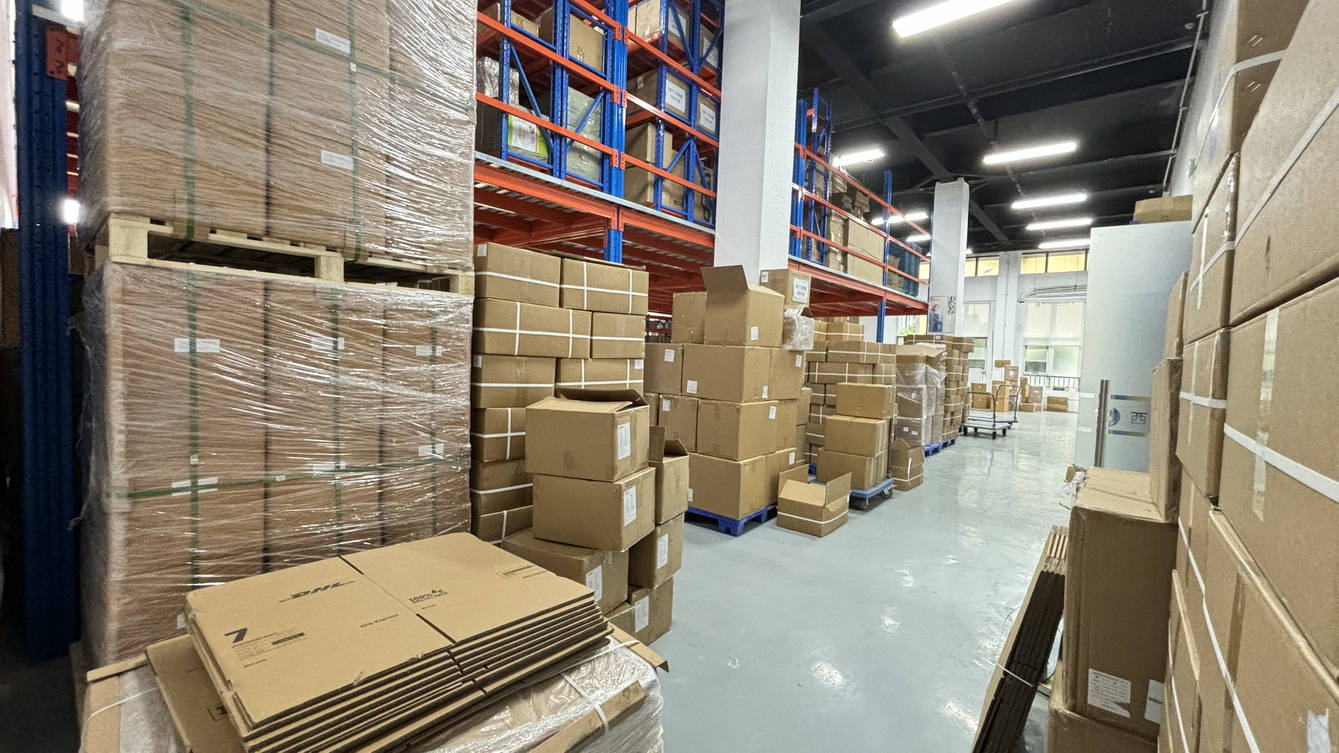
Equipped with high-capacity stainless steel extraction reactors, multi-stage filtration units, and low-temperature vacuum concentrators to safeguard bio-actives.
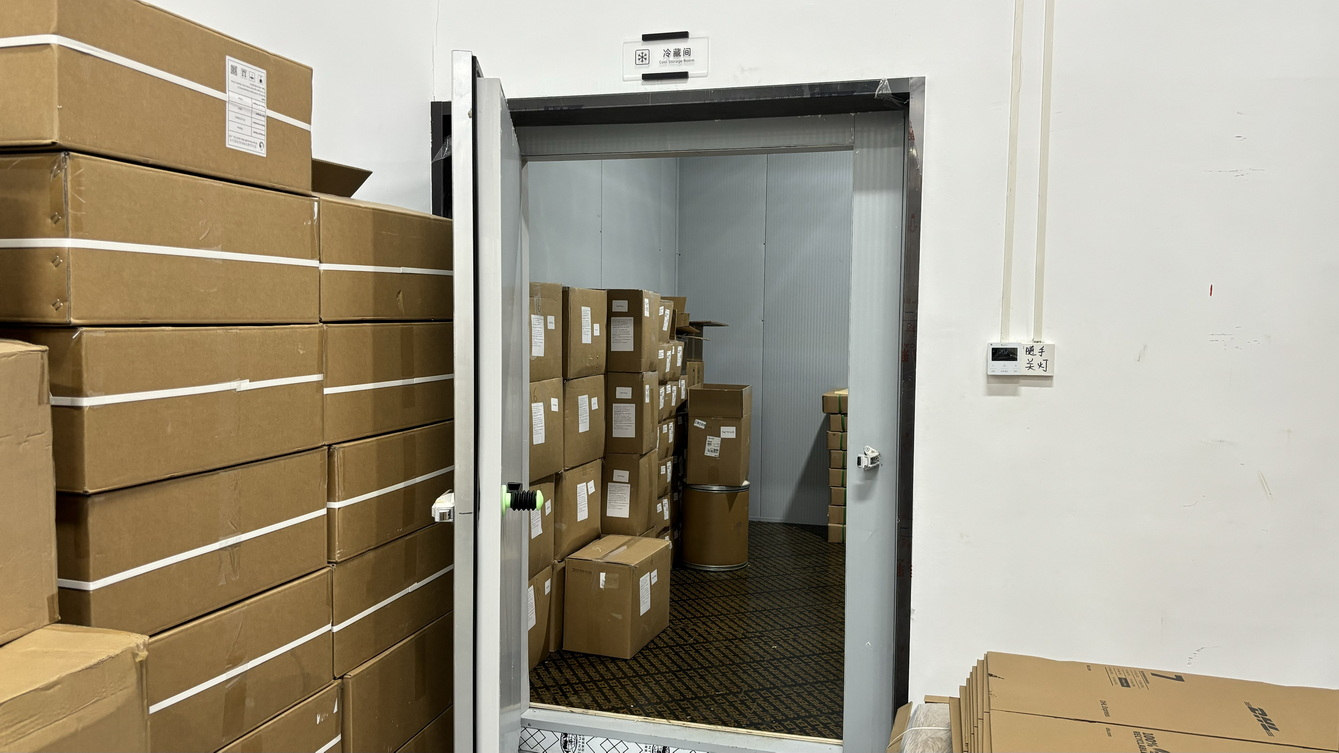
Temperature- and humidity-monitored storage preserving the potency of sensitive powders, extracts, natural pigments, and clean-label sweeteners.
Every lot manufactured by Xi'an Vexli Bio-Tech Co., Ltd. follows a strictly controlled workflow to ensure batch-to-batch consistency and international compliance.
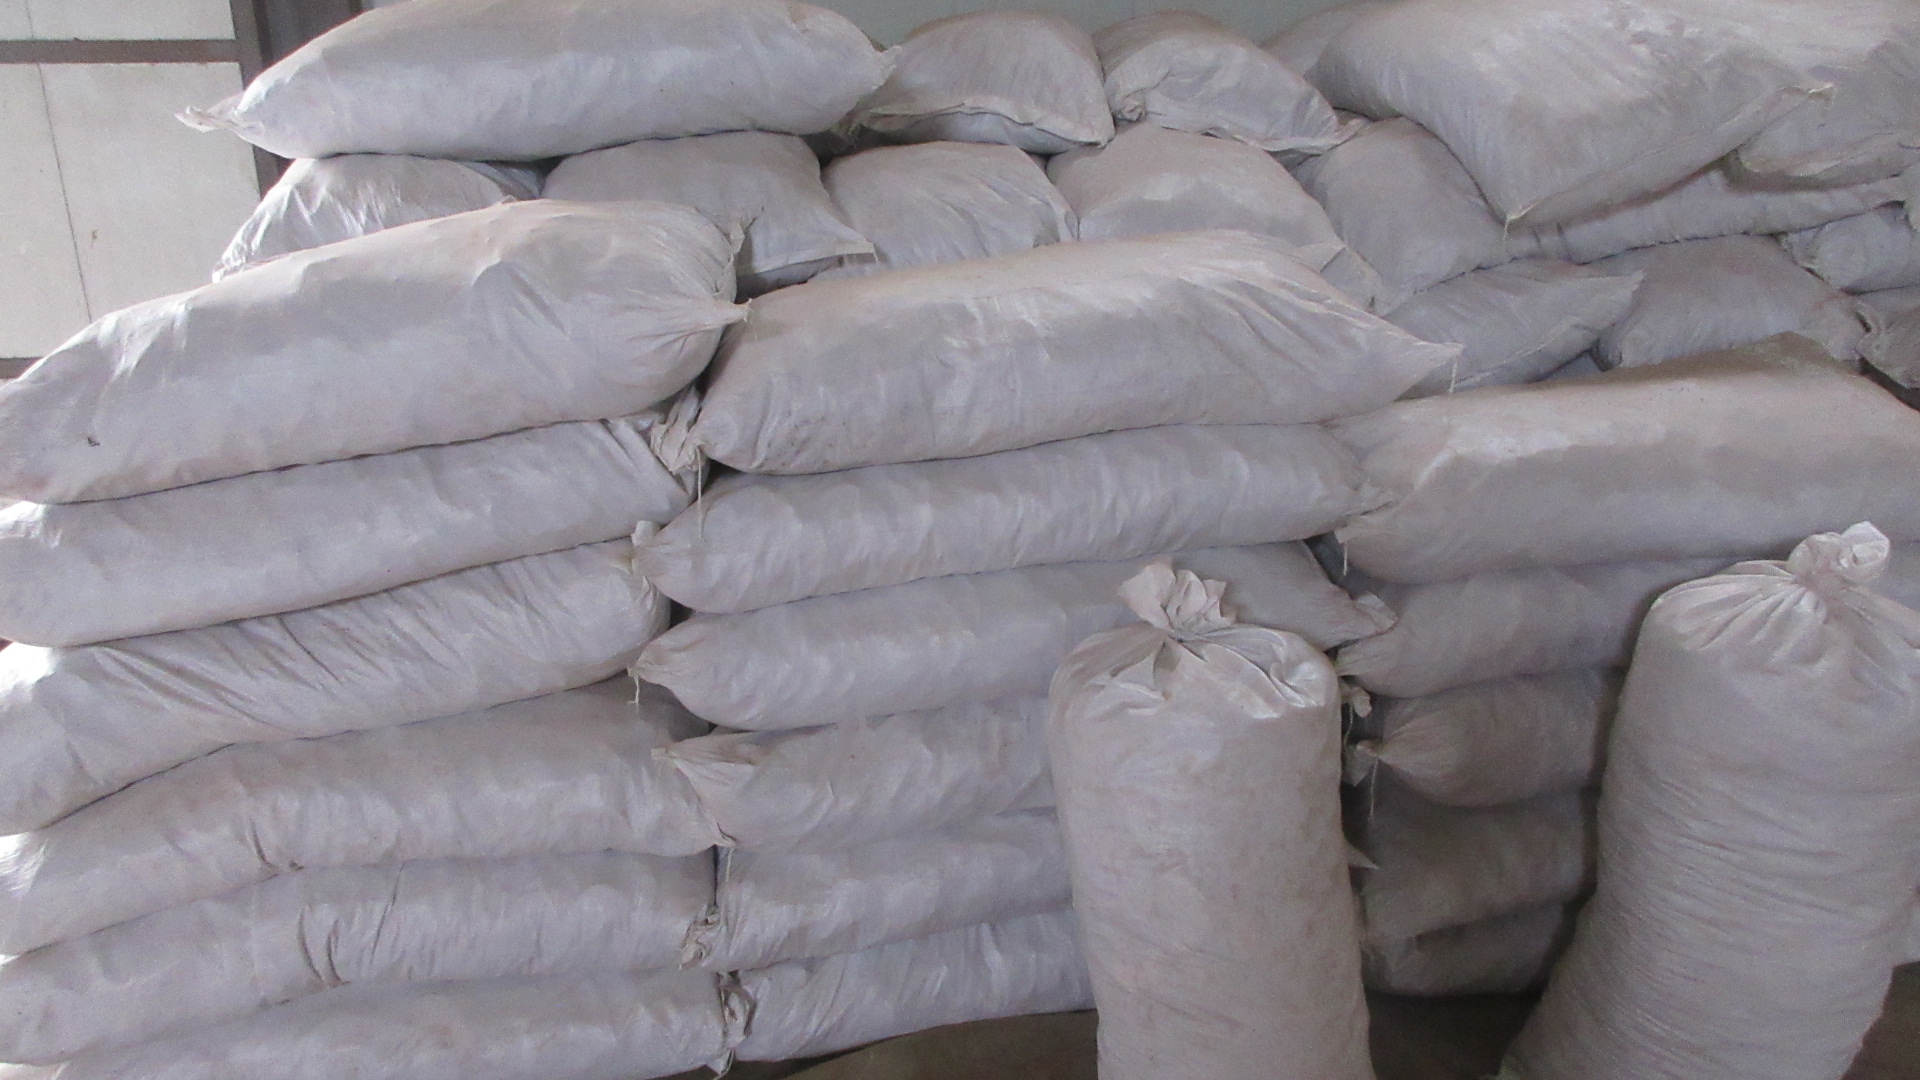
Herbarium species validation, pesticide residue pre-screening, moisture check, and heavy metal baseline assays.
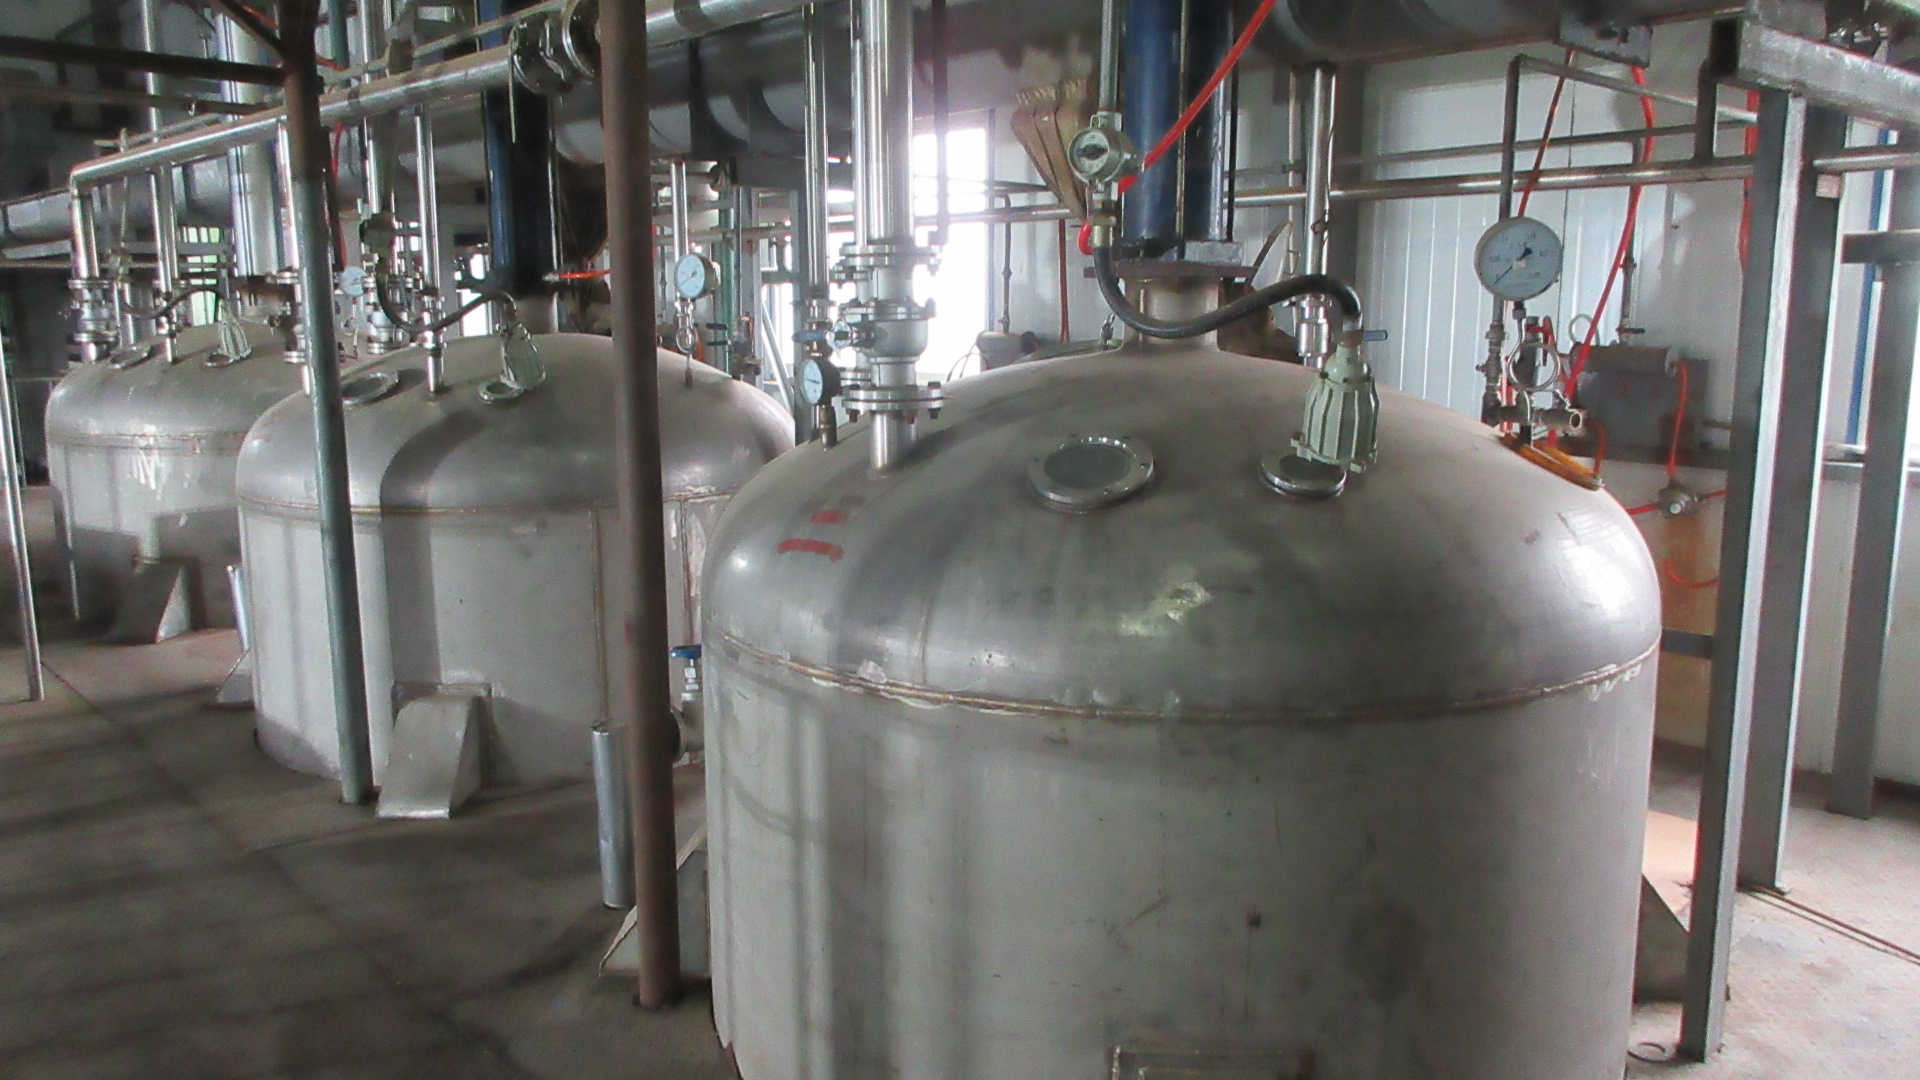
Optimized solid-to-liquid ratio extraction using purified deionized water or food-grade ethanol at monitored temperatures.
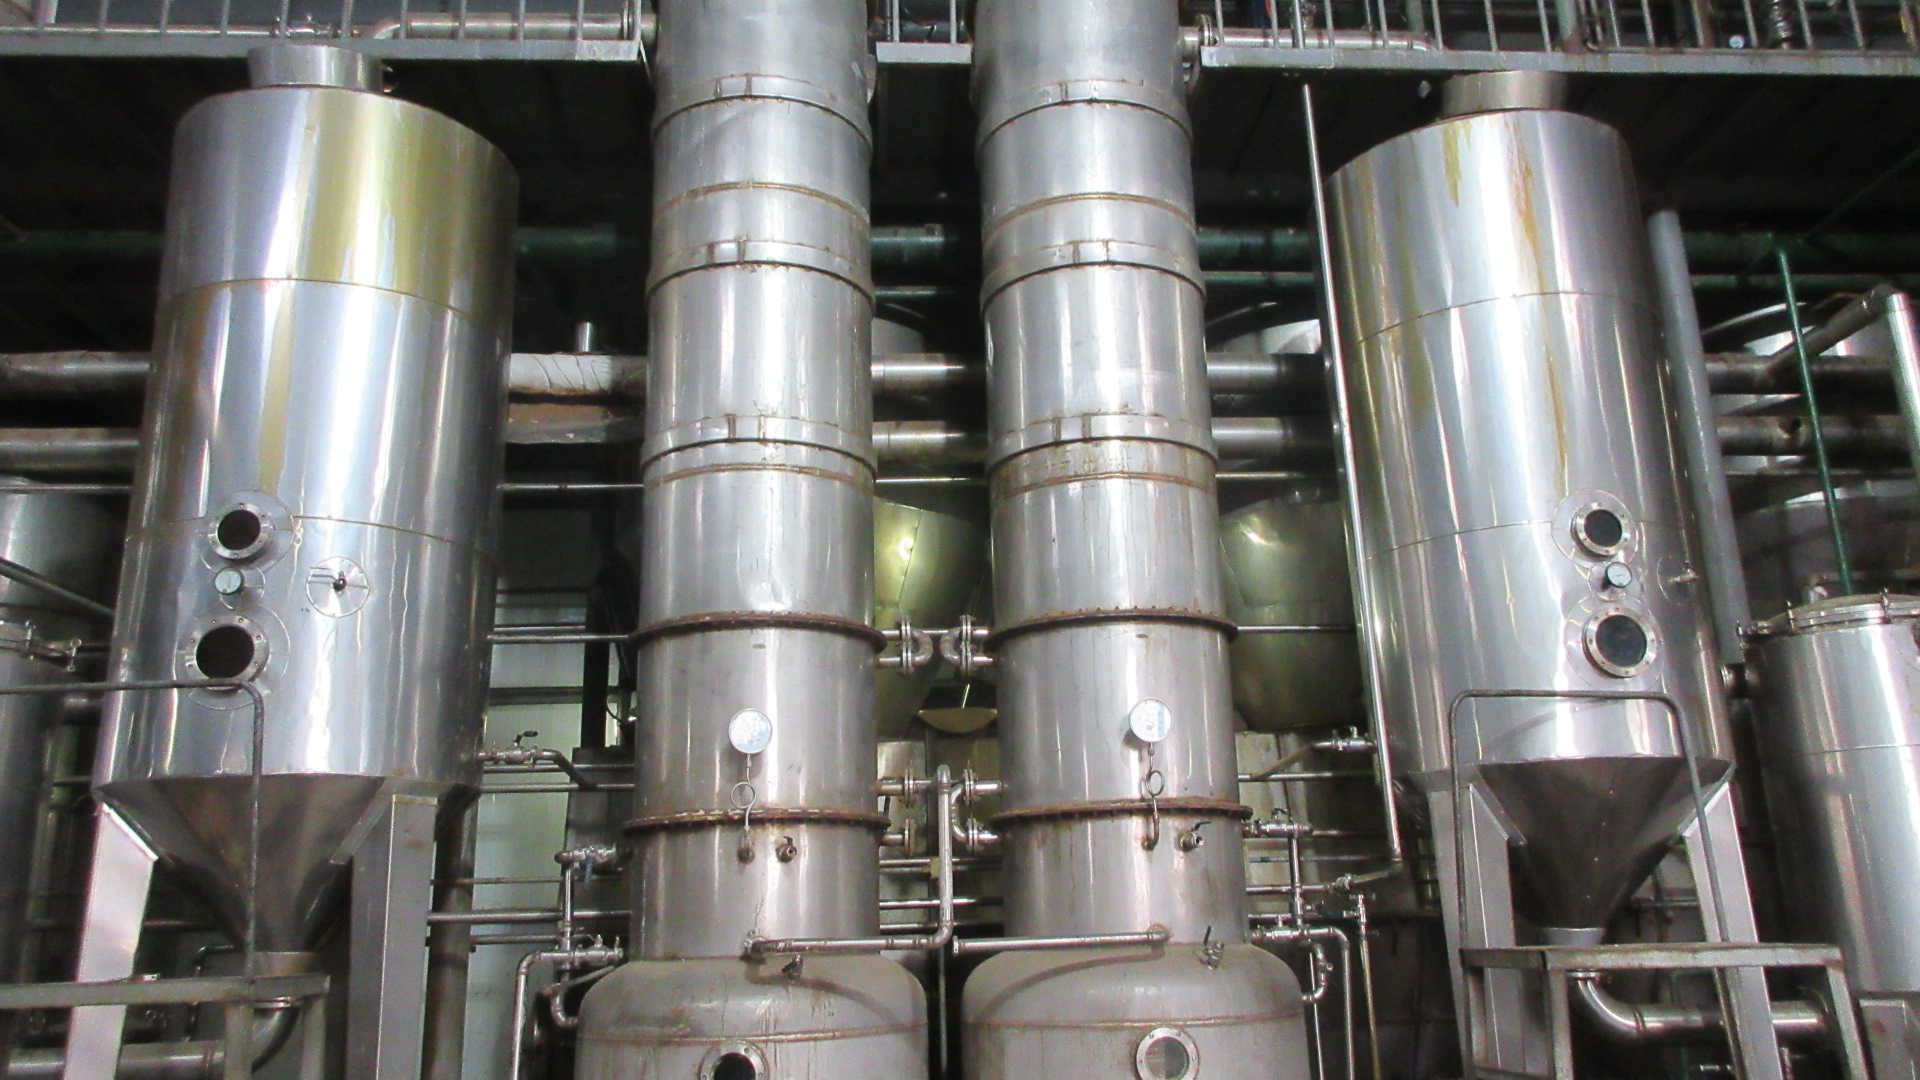
Gentle low-temperature falling-film concentration preventing thermal degradation of delicate flavonoids and phytochemicals.
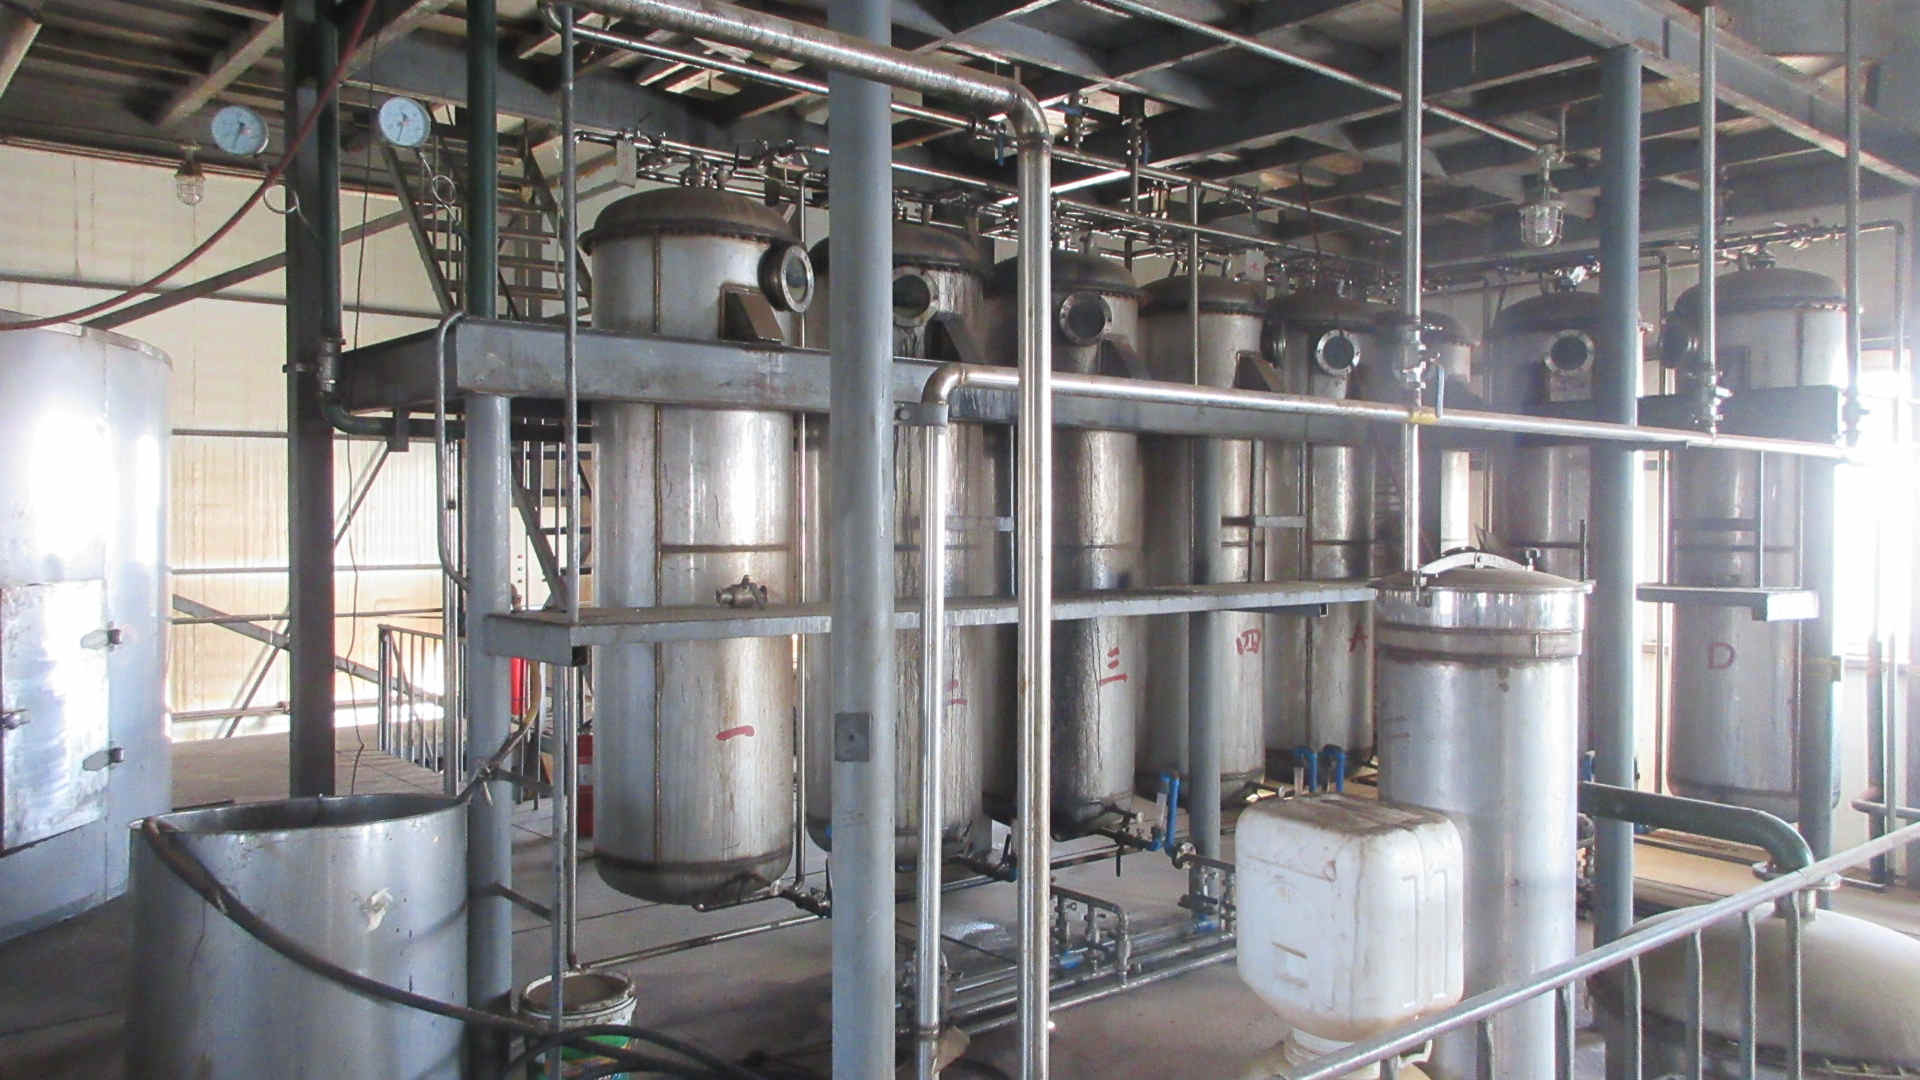
Macroporous resin separation and ceramic membrane filtration targeting specific active assays while removing ballast.
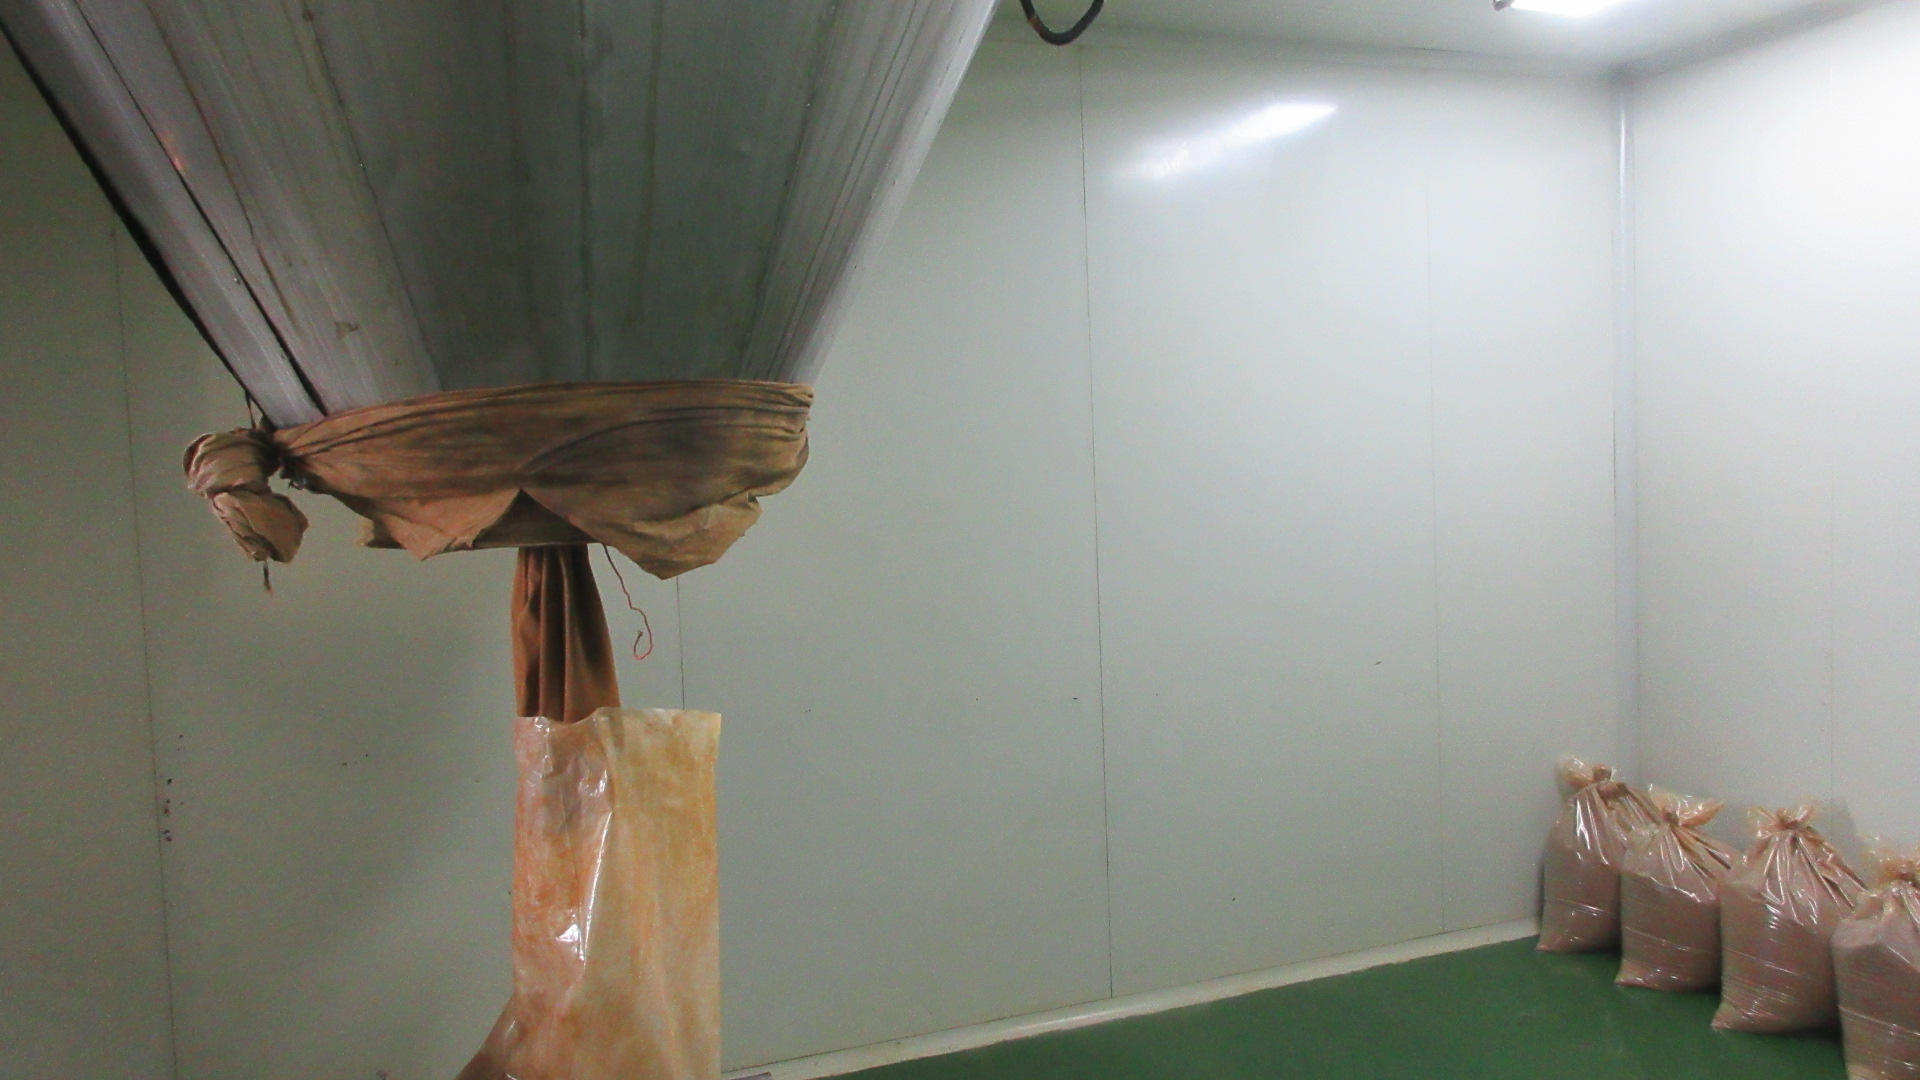
Instant atomized spray drying producing free-flowing, instantly soluble micro-granules with strictly regulated residual moisture.
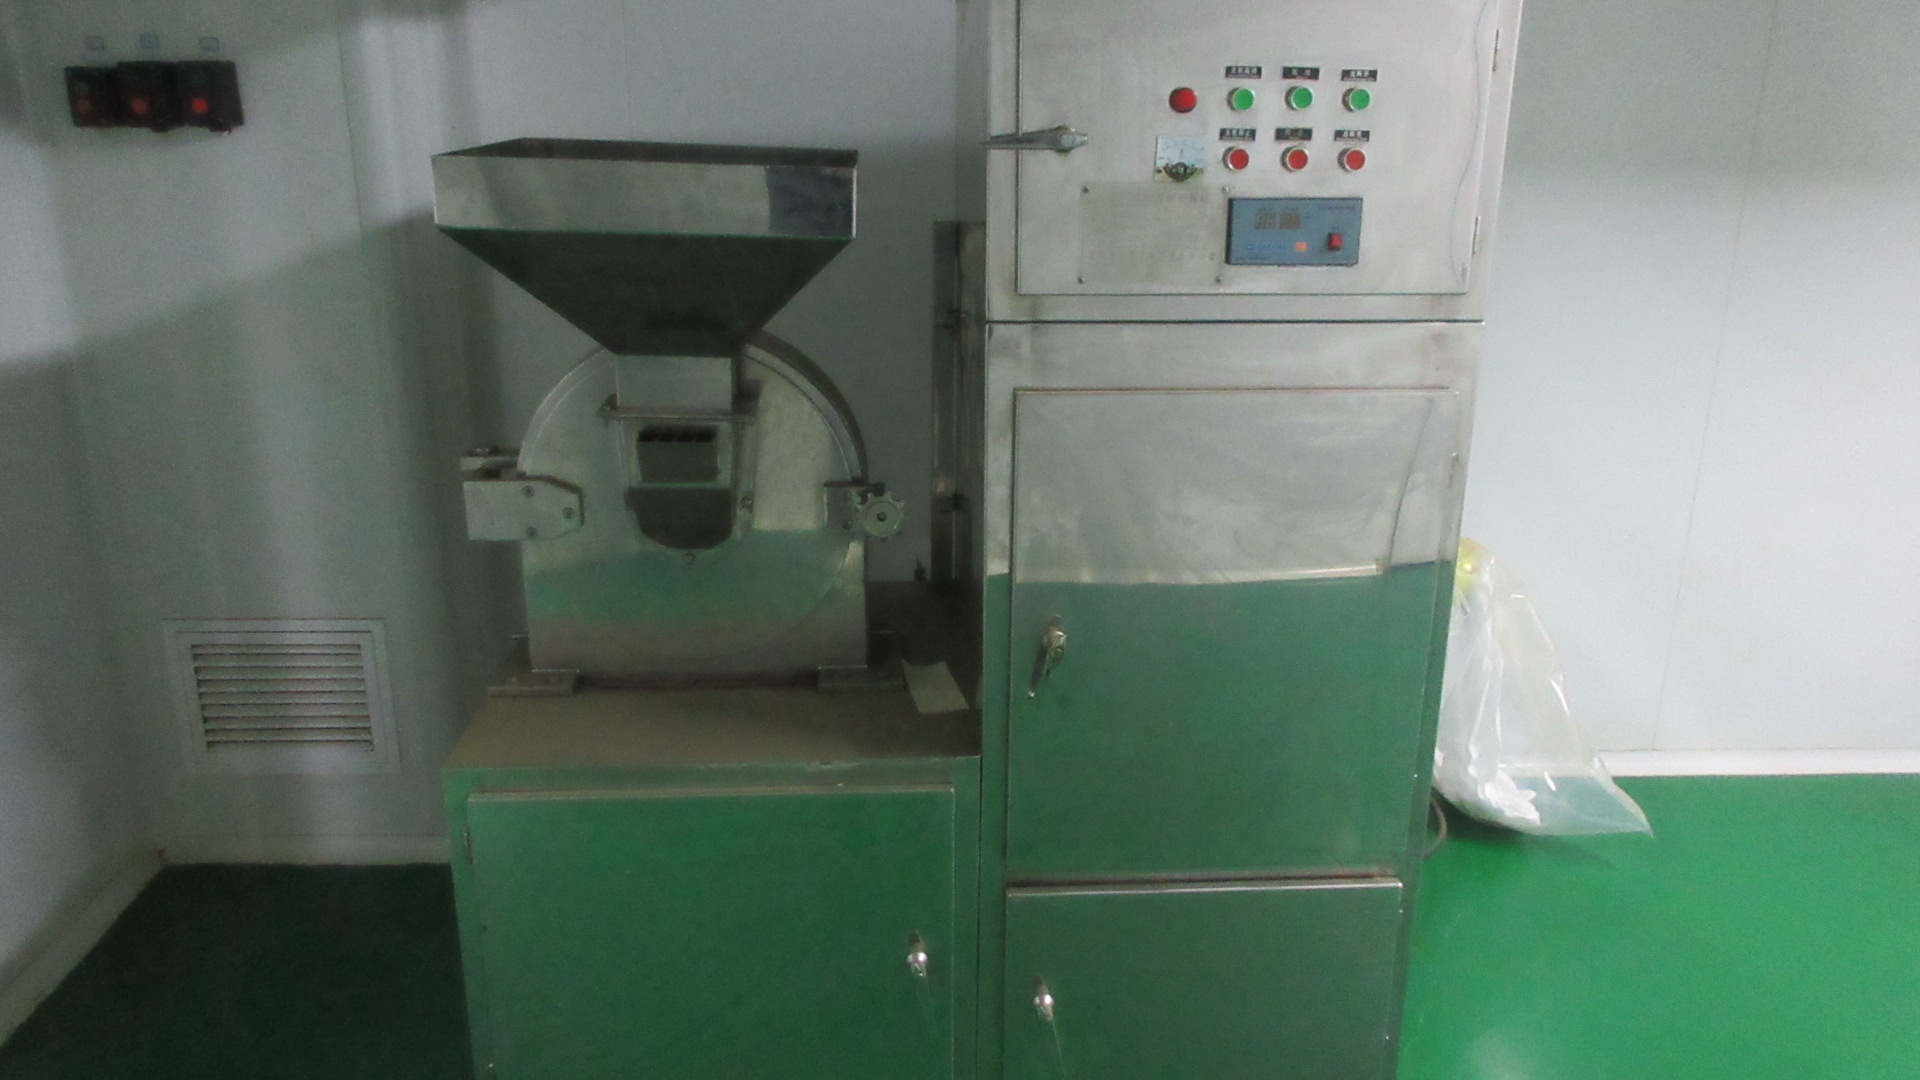
Ultrafine micro-milling calibrated to client-specified bulk densities and particle dimensions suited for tablets or drink blends.
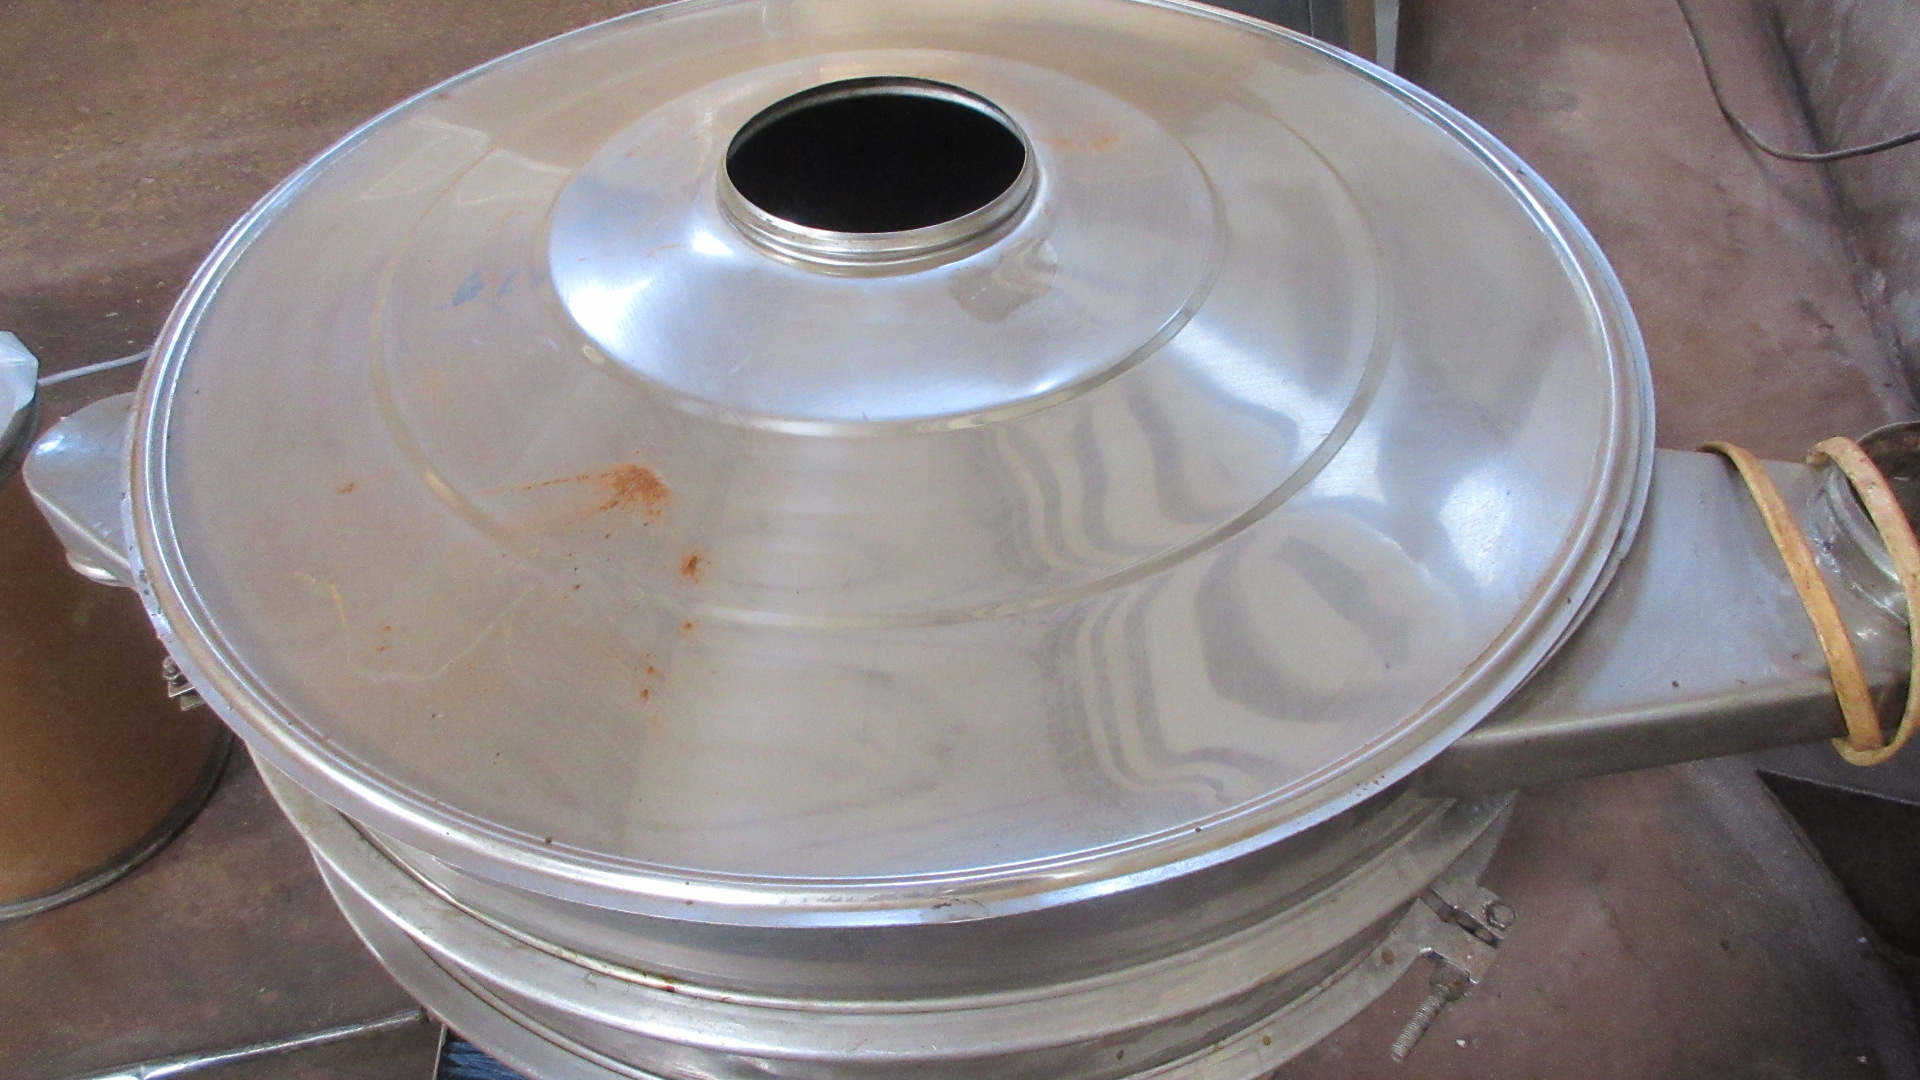
Screening through 80 to 450 mesh specifications coupled with rare-earth magnetic separation and dual-aperture metal detectors.
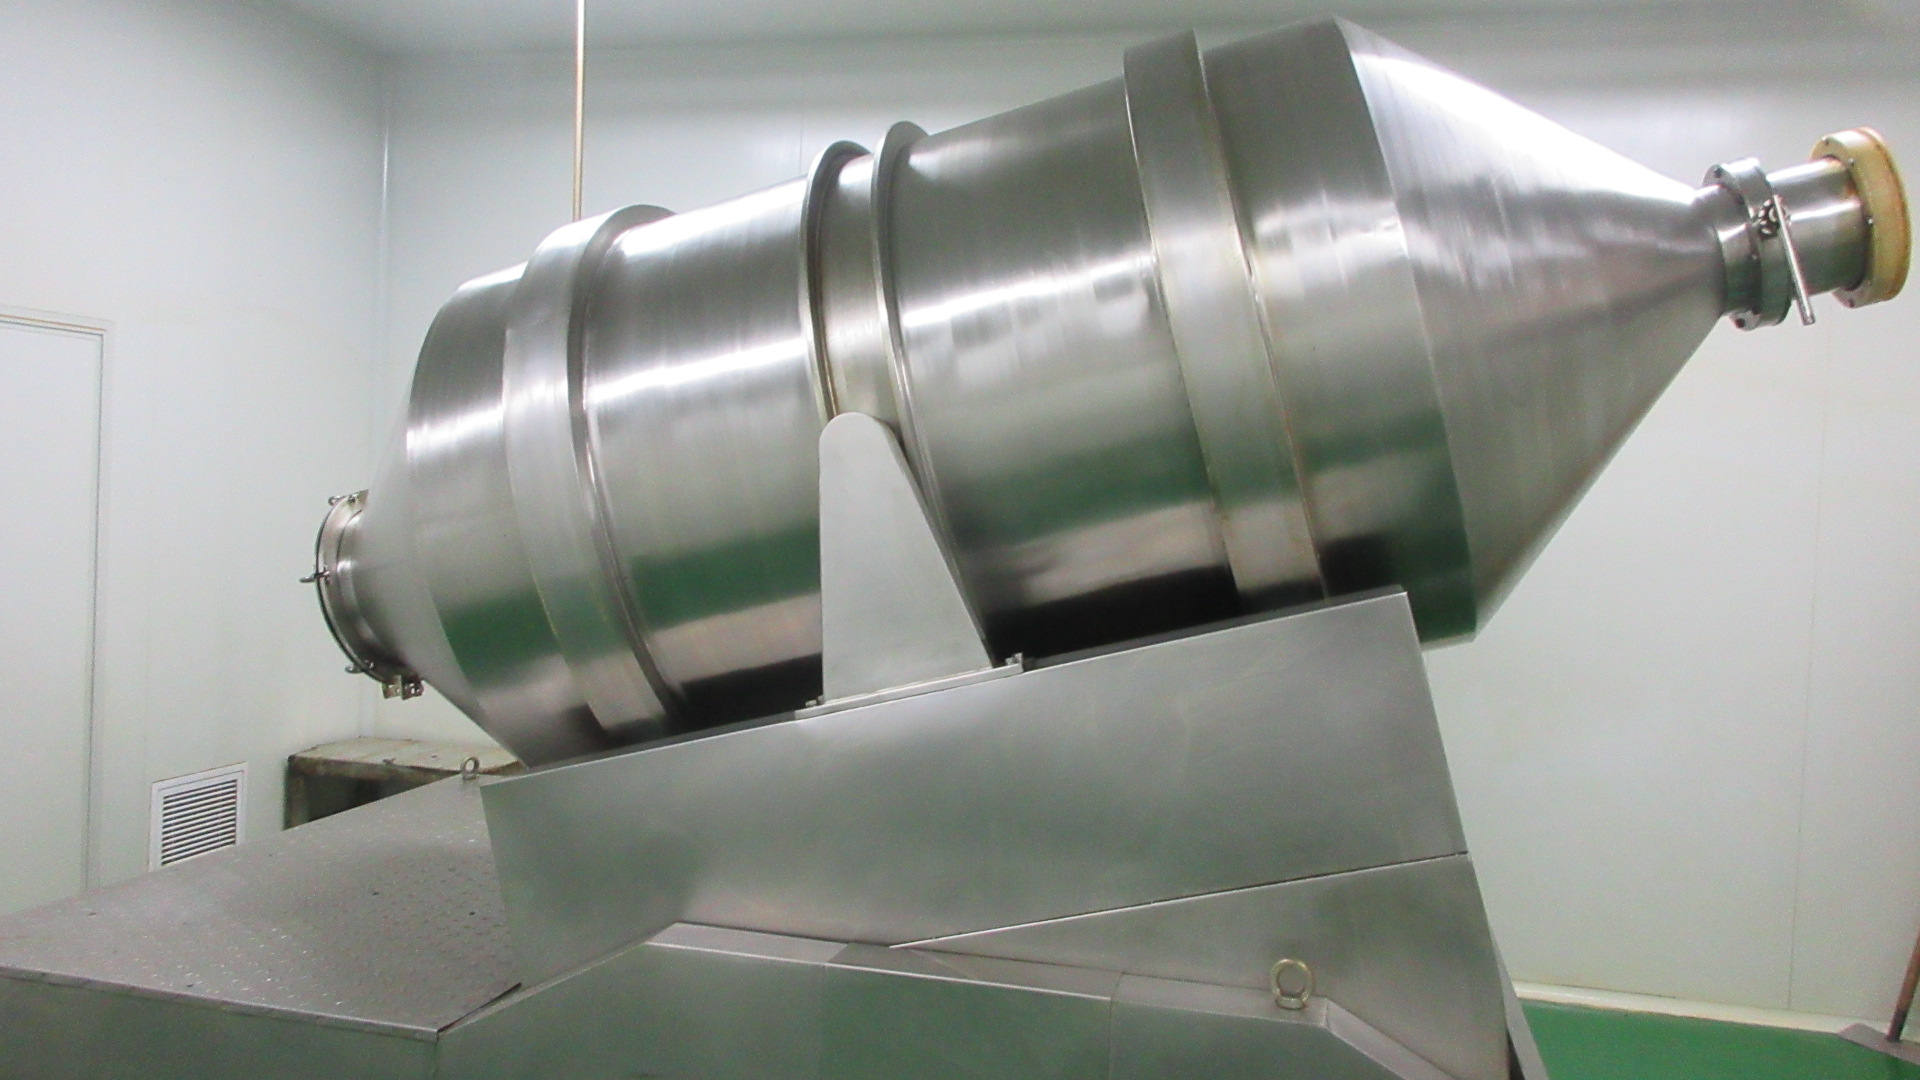
High-efficiency ribbon blending guaranteeing uniform active dispersion across commercial batch sizes up to multiple tons.
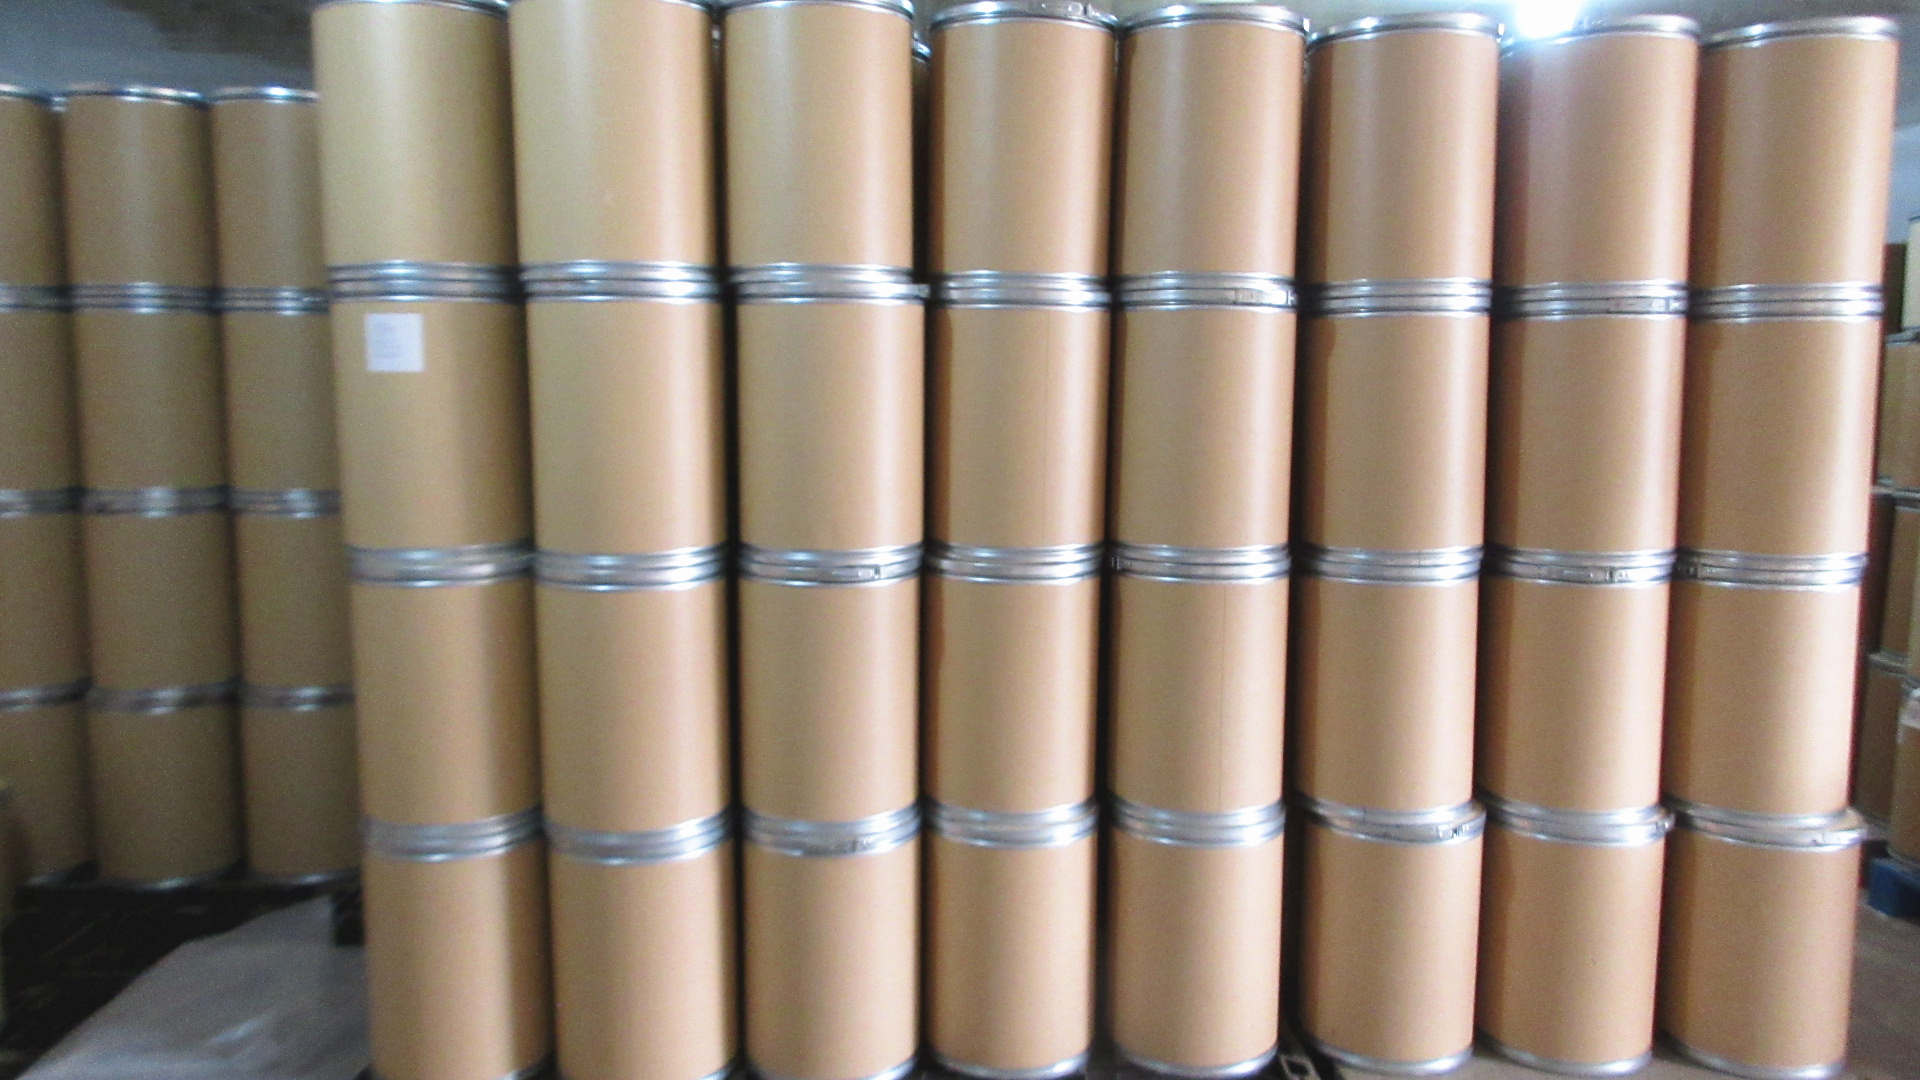
Double-layer food-grade polyethylene lined drums, nitrogen flushed bags, or custom private-label containers with full lot traceability.
Precision-machined stainless steel reactors and drying towers designed for sanitary continuous processing.
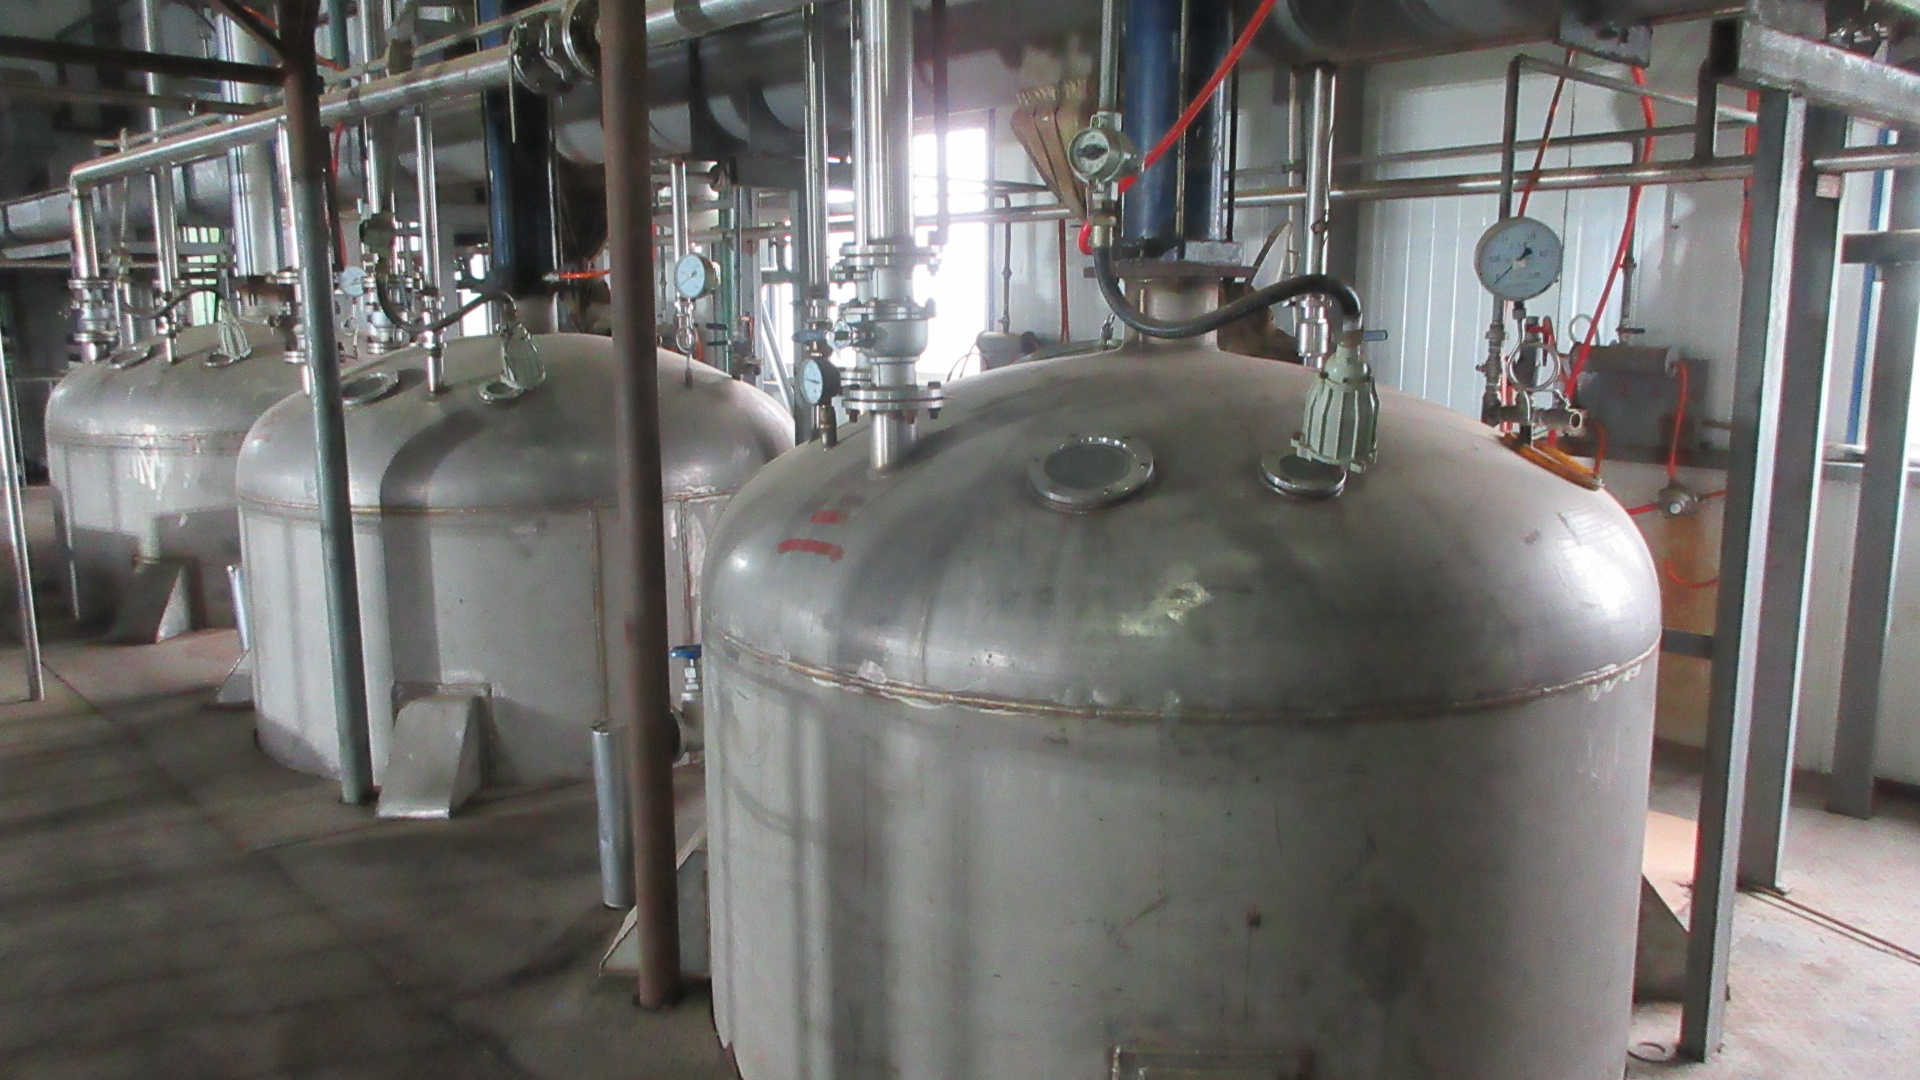
Multi-functional stainless unit
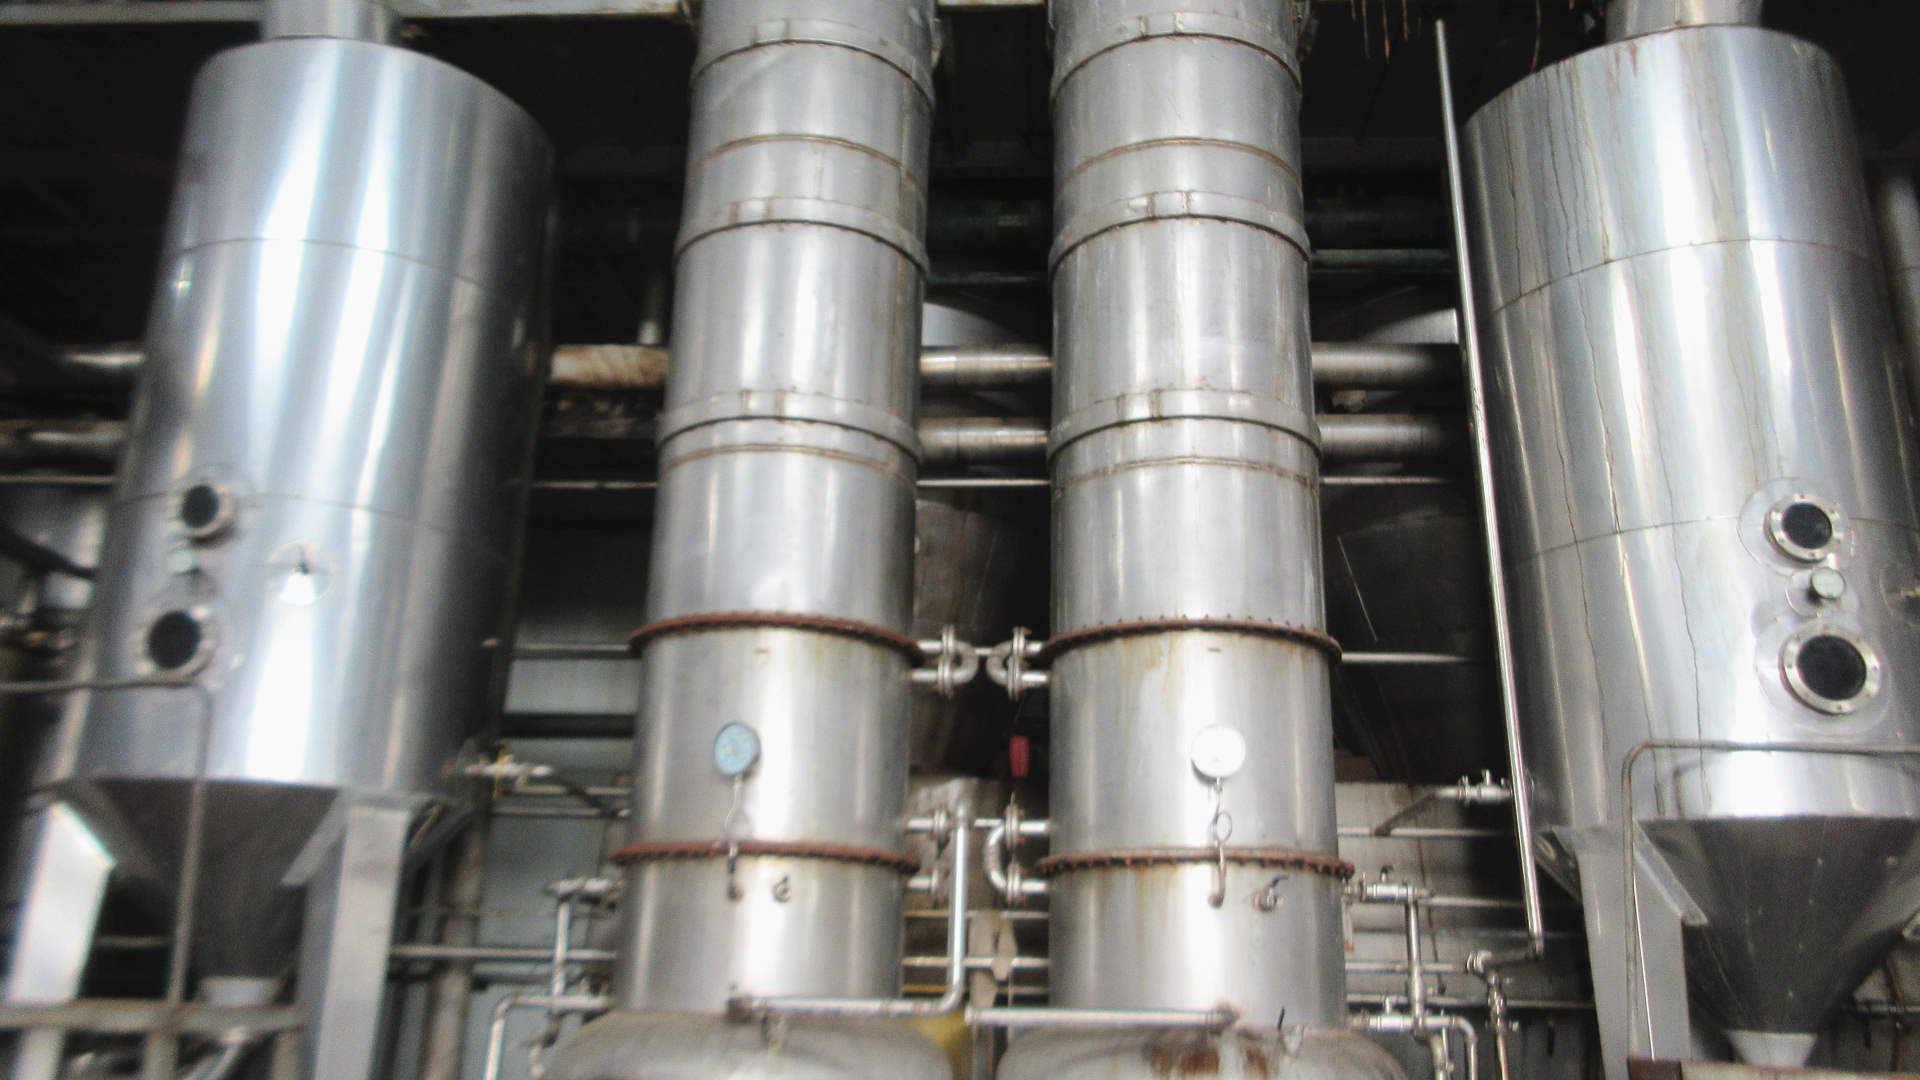
Energy-saving vacuum unit
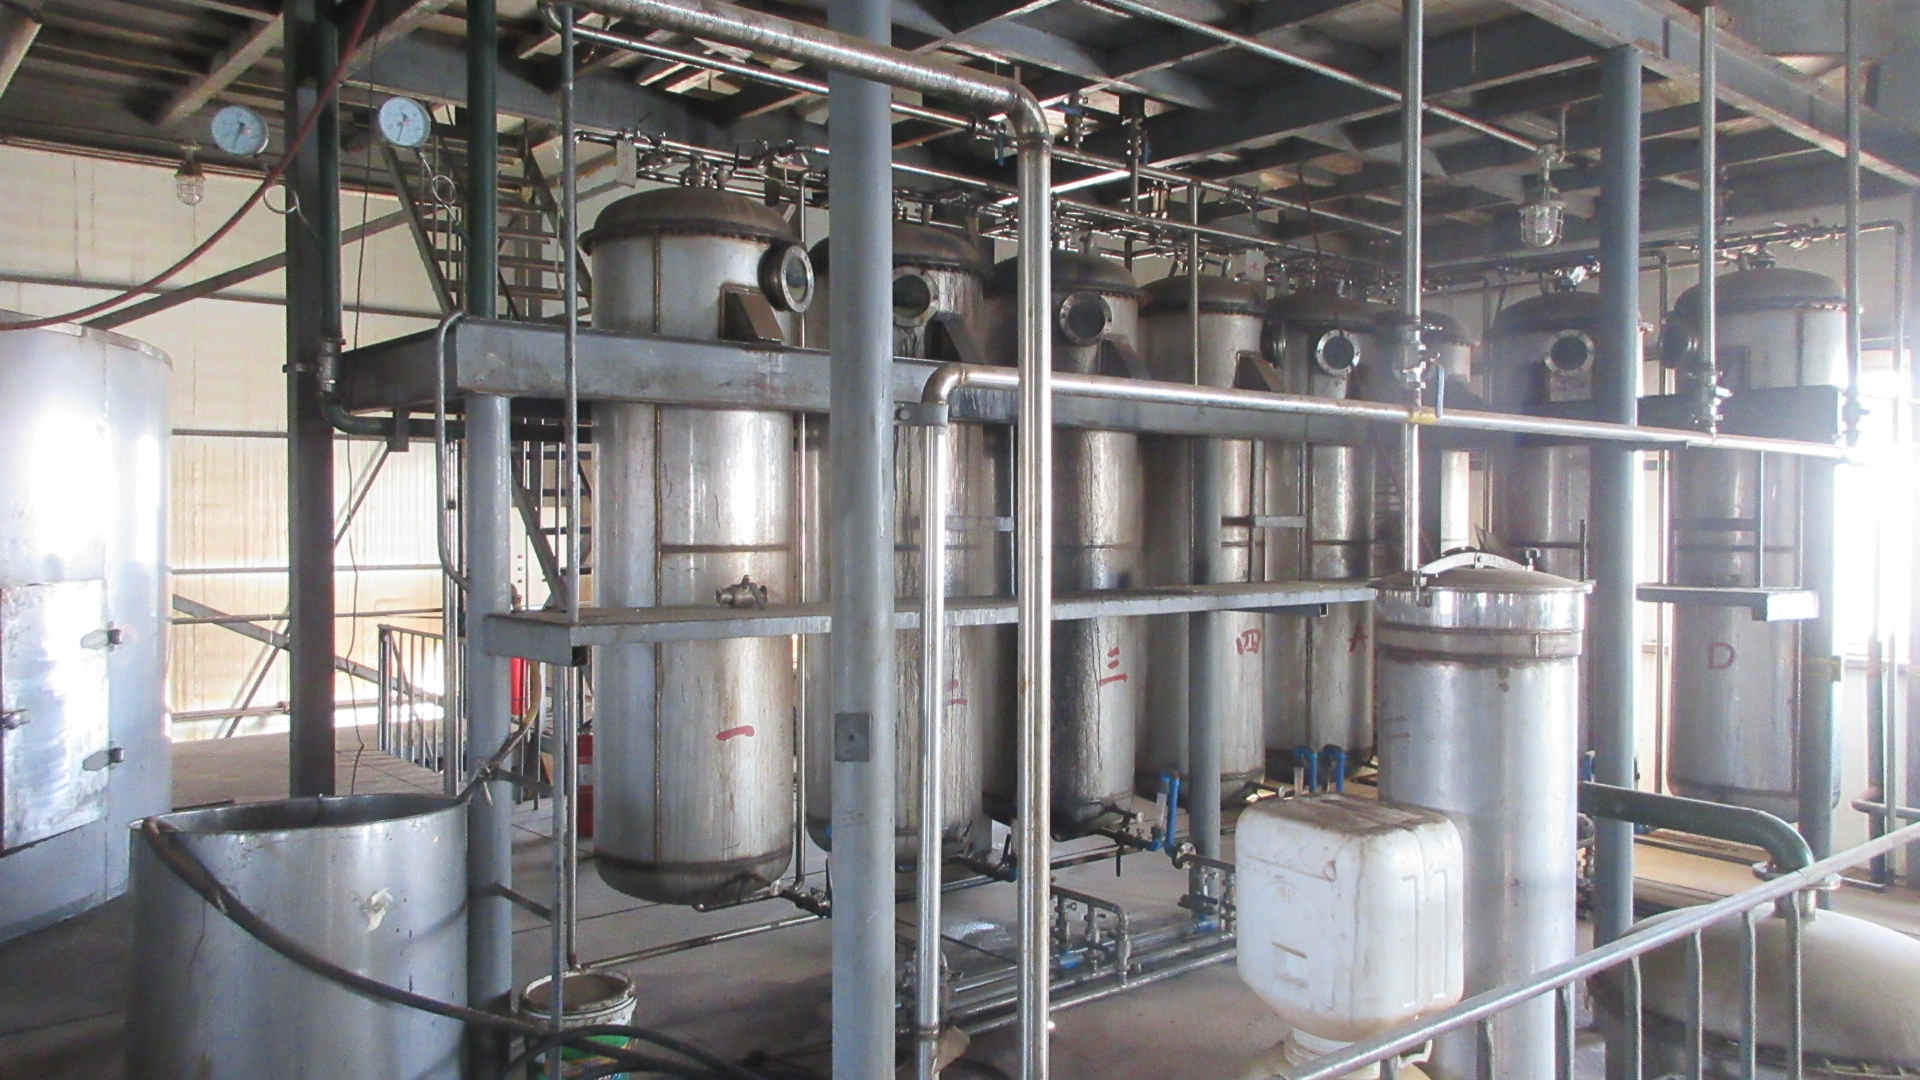
Resin adsorption technology
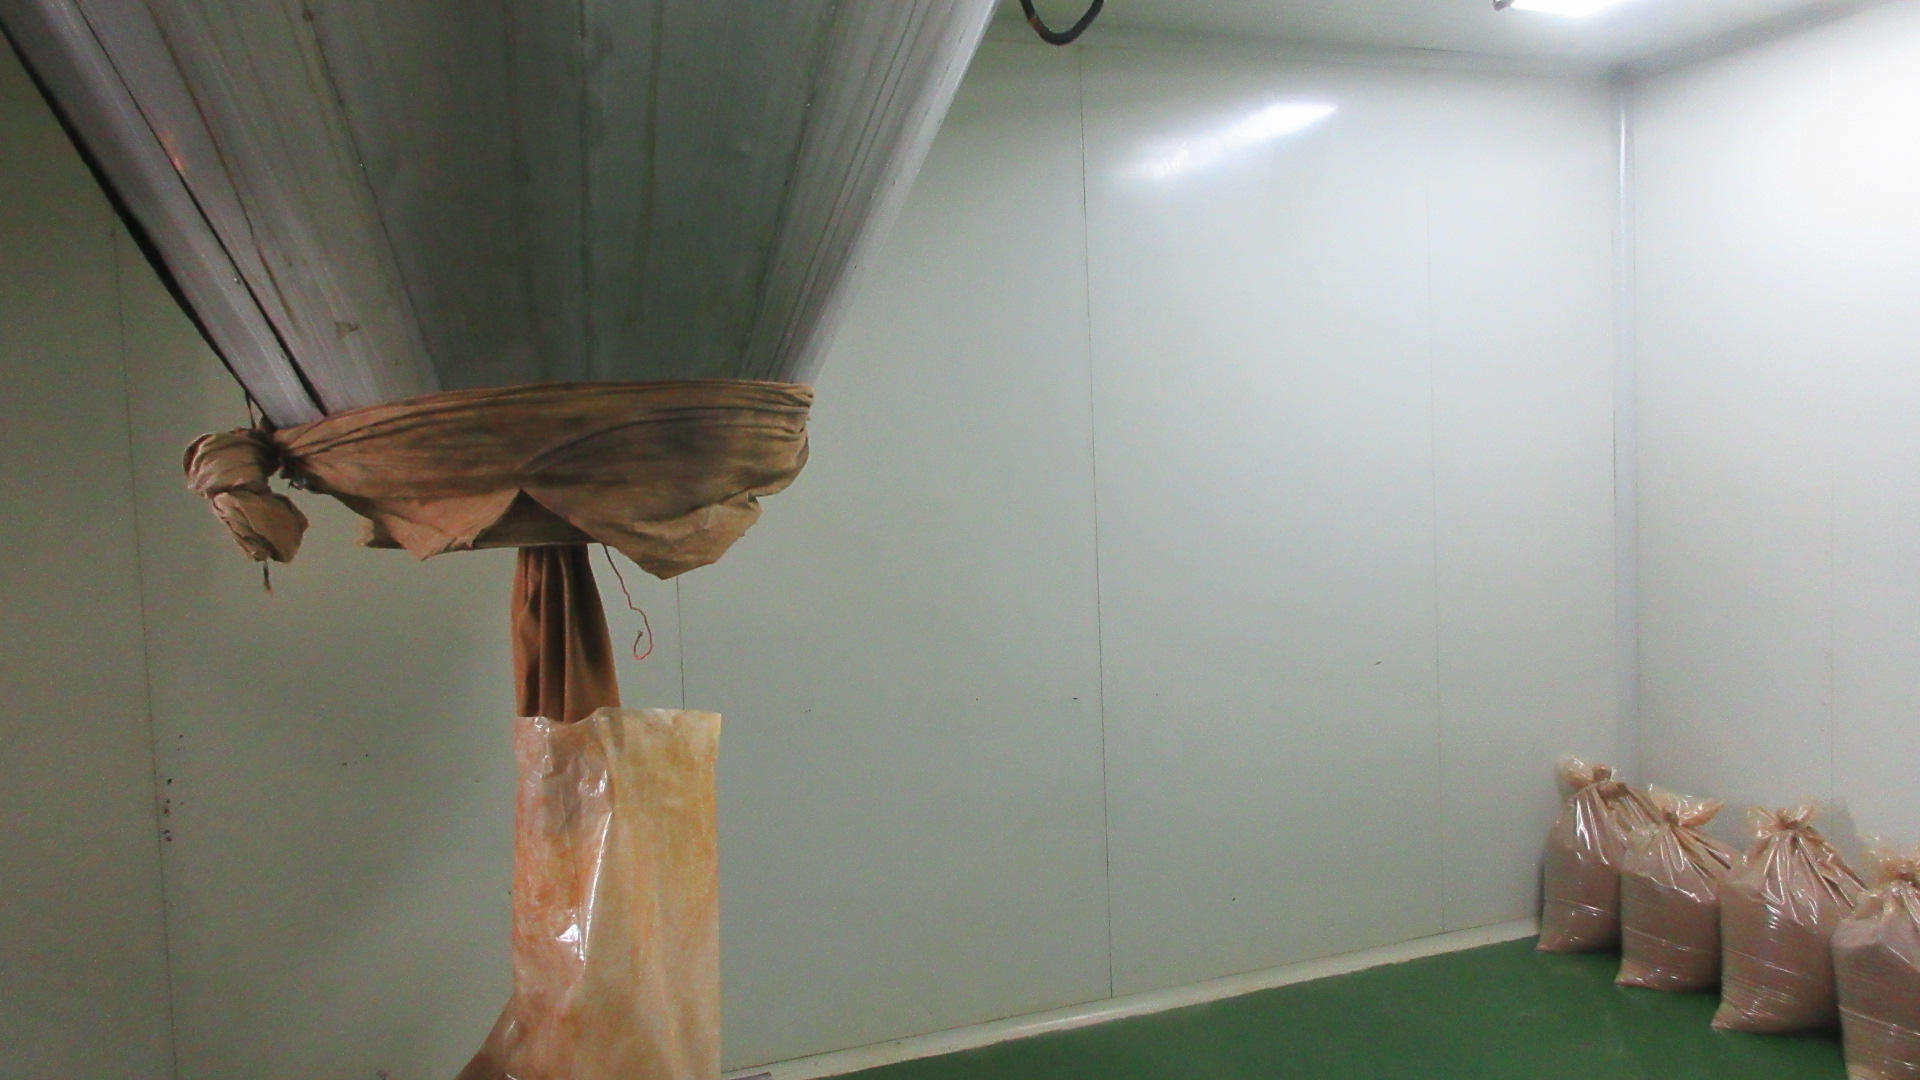
Centrifugal spray drying
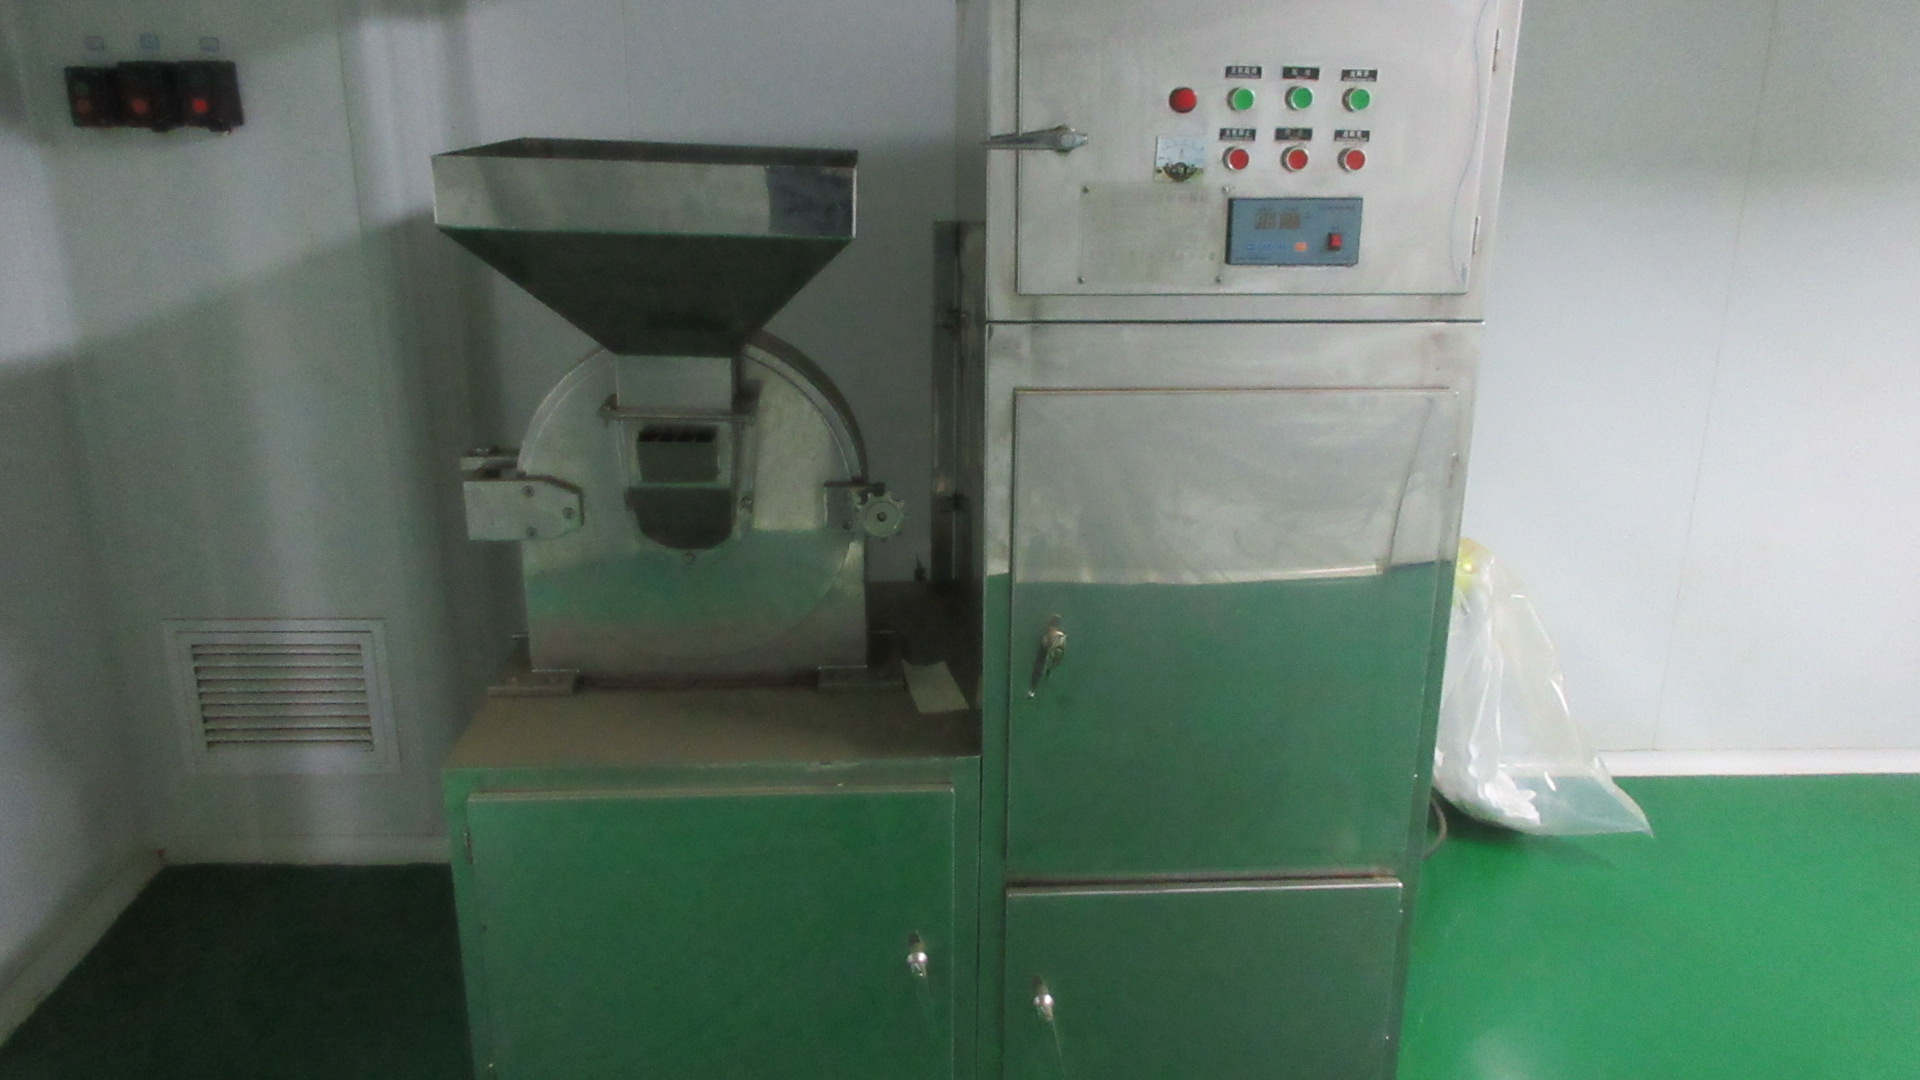
High-speed mechanical milling
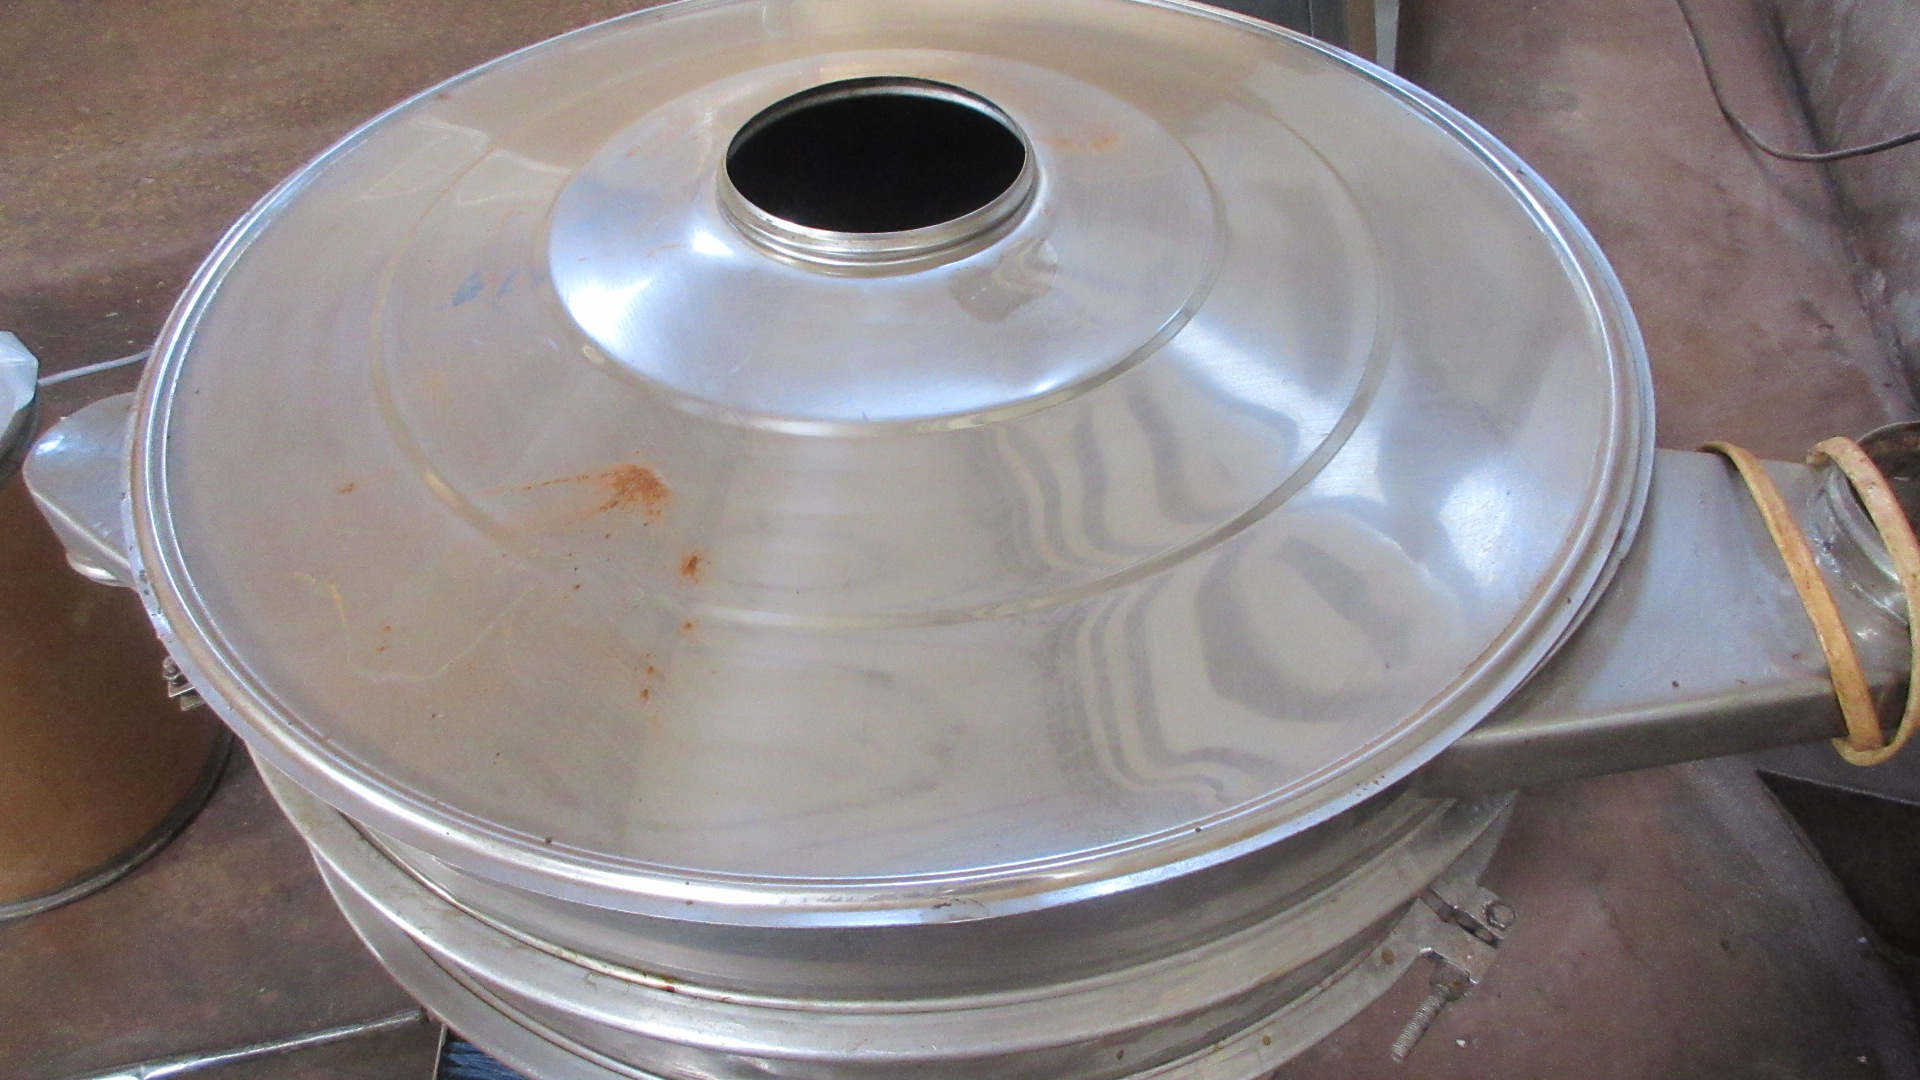
Vibratory grading screens
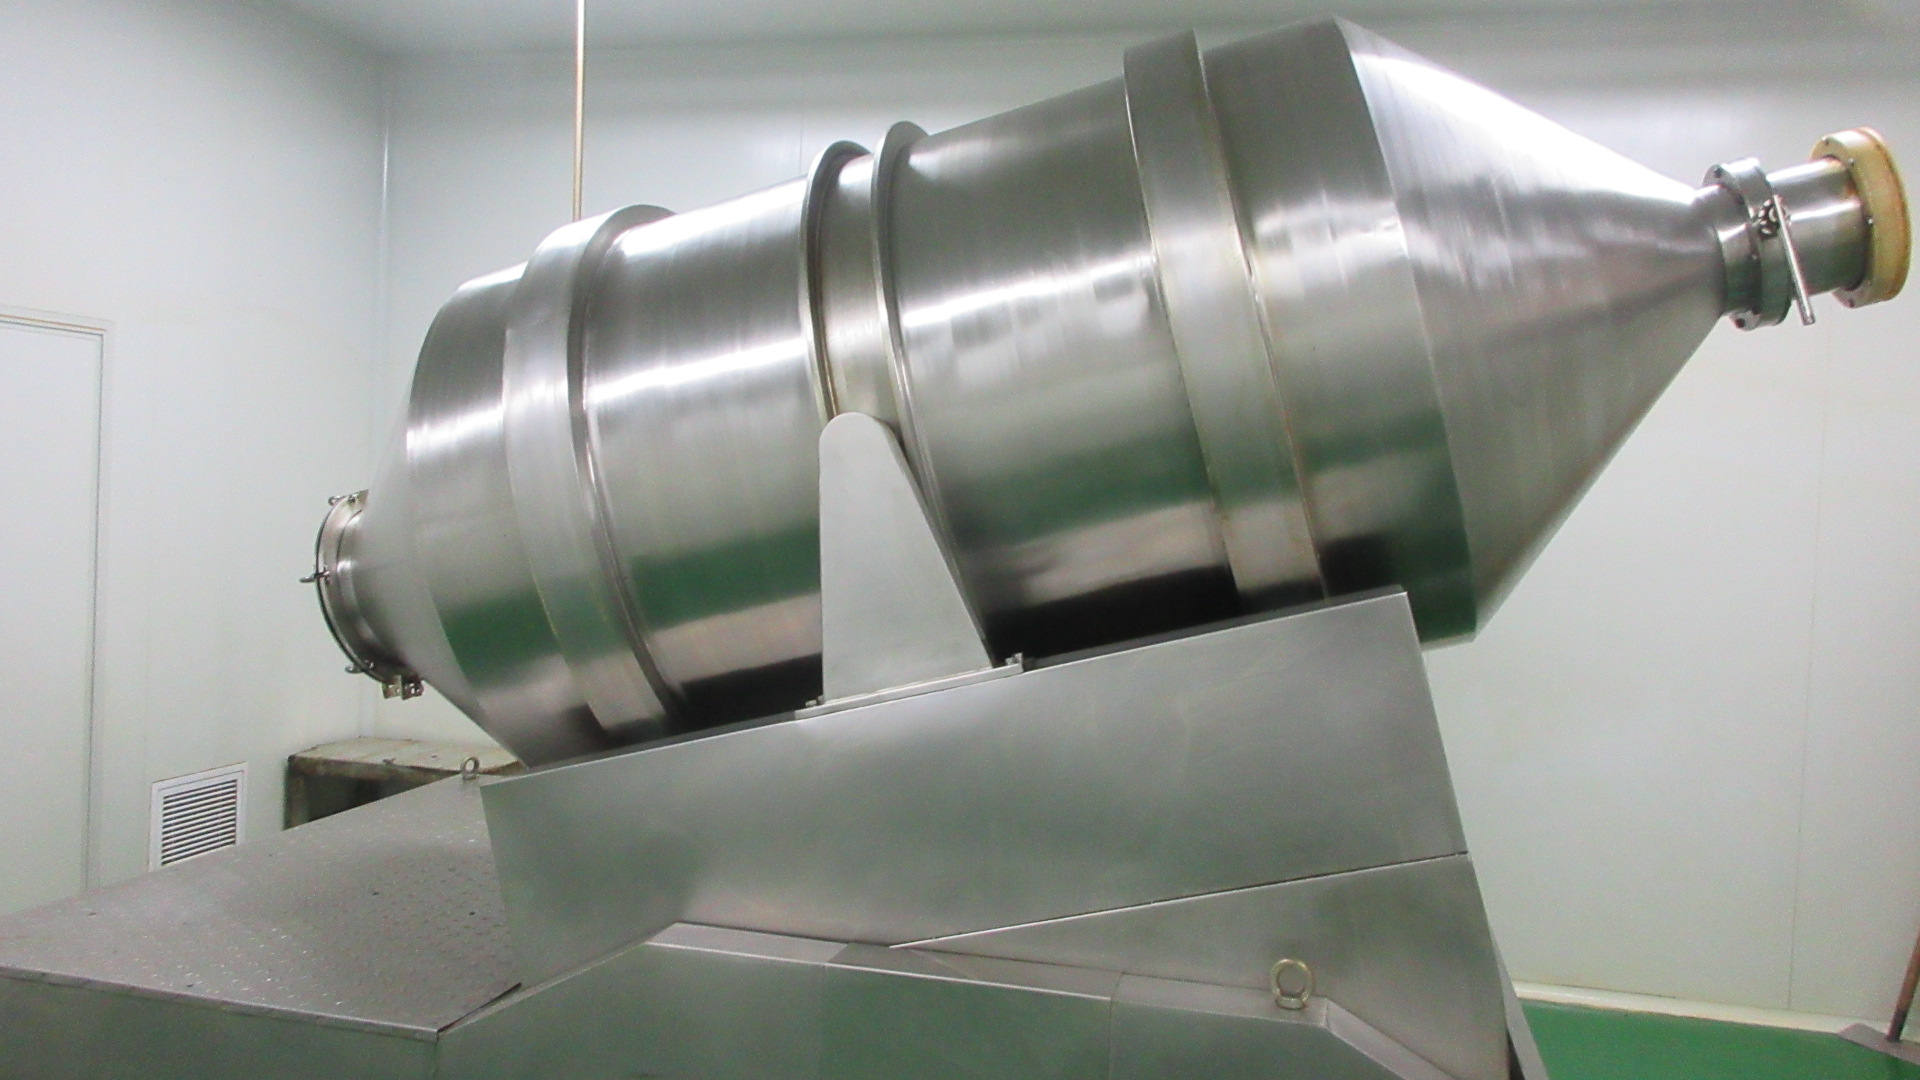
Dual-cone homogeneous blender
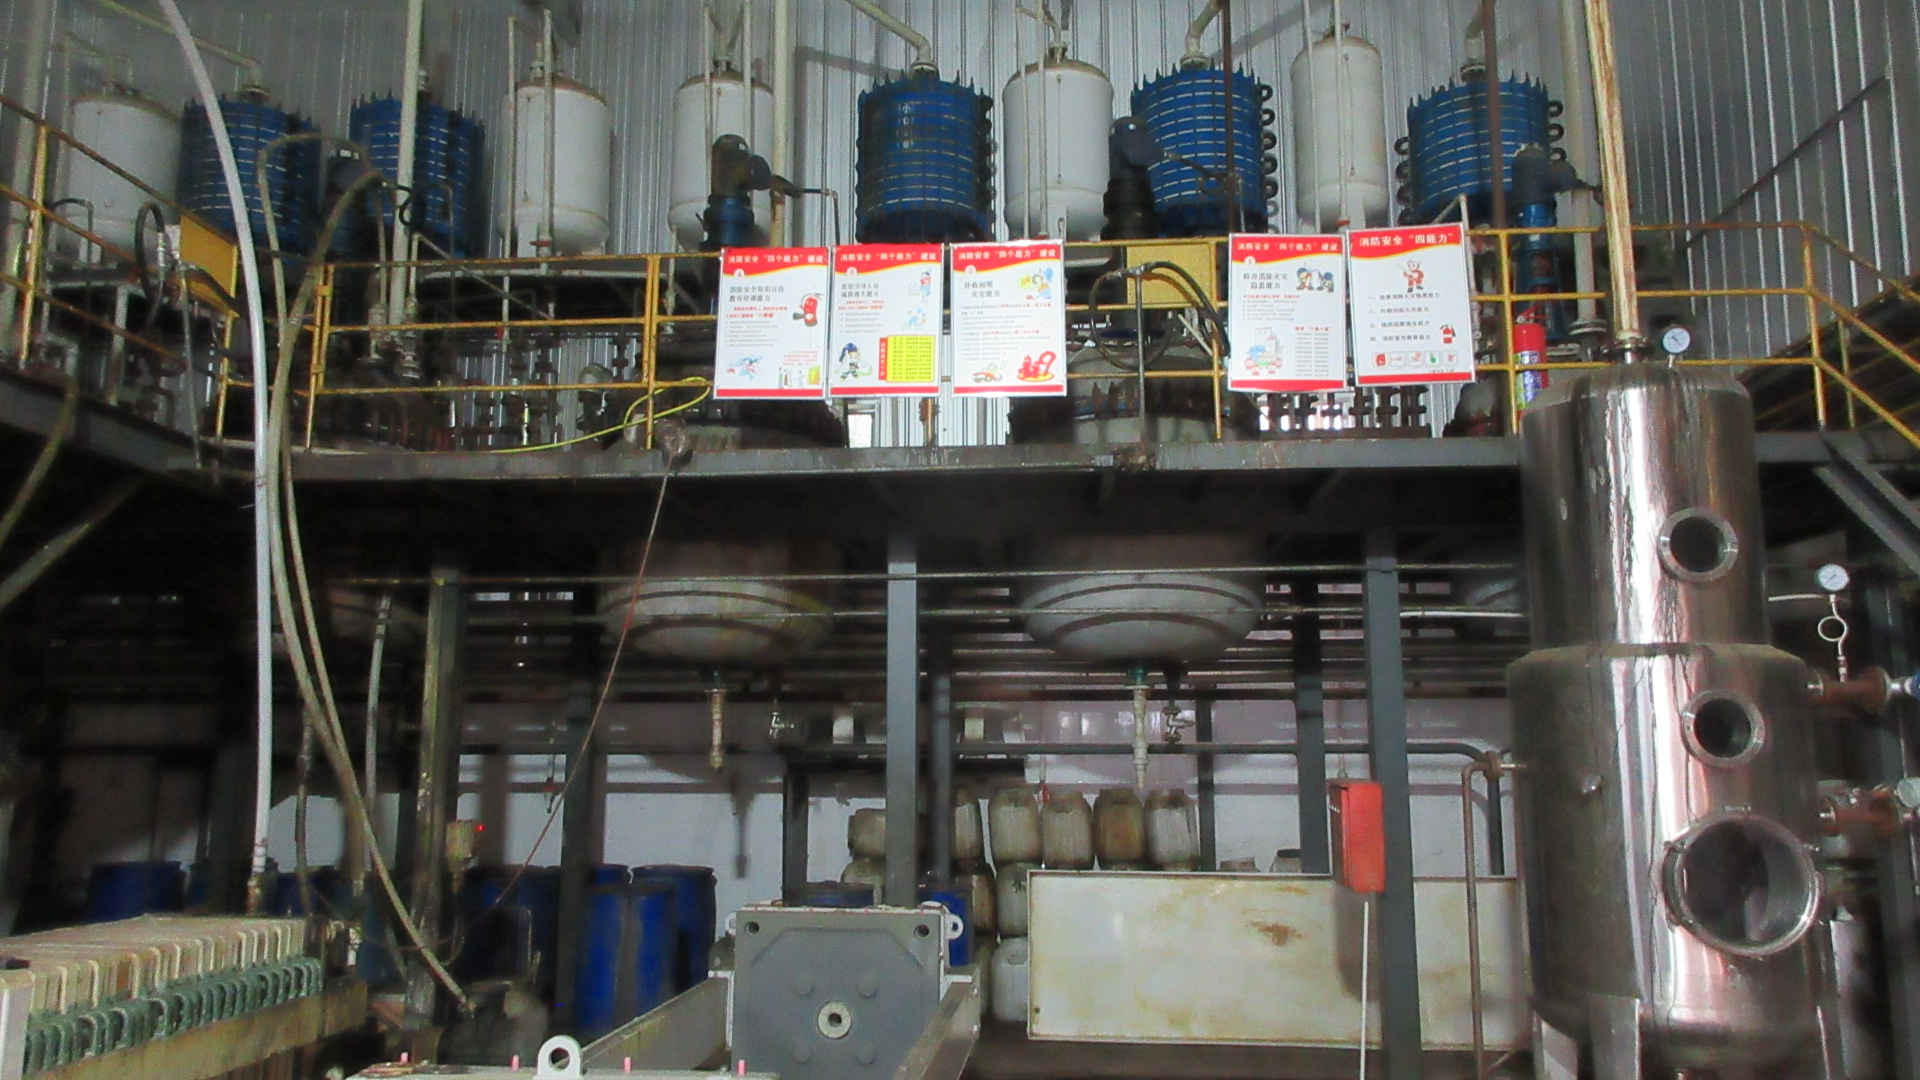
Acid & alkaline corrosion proof
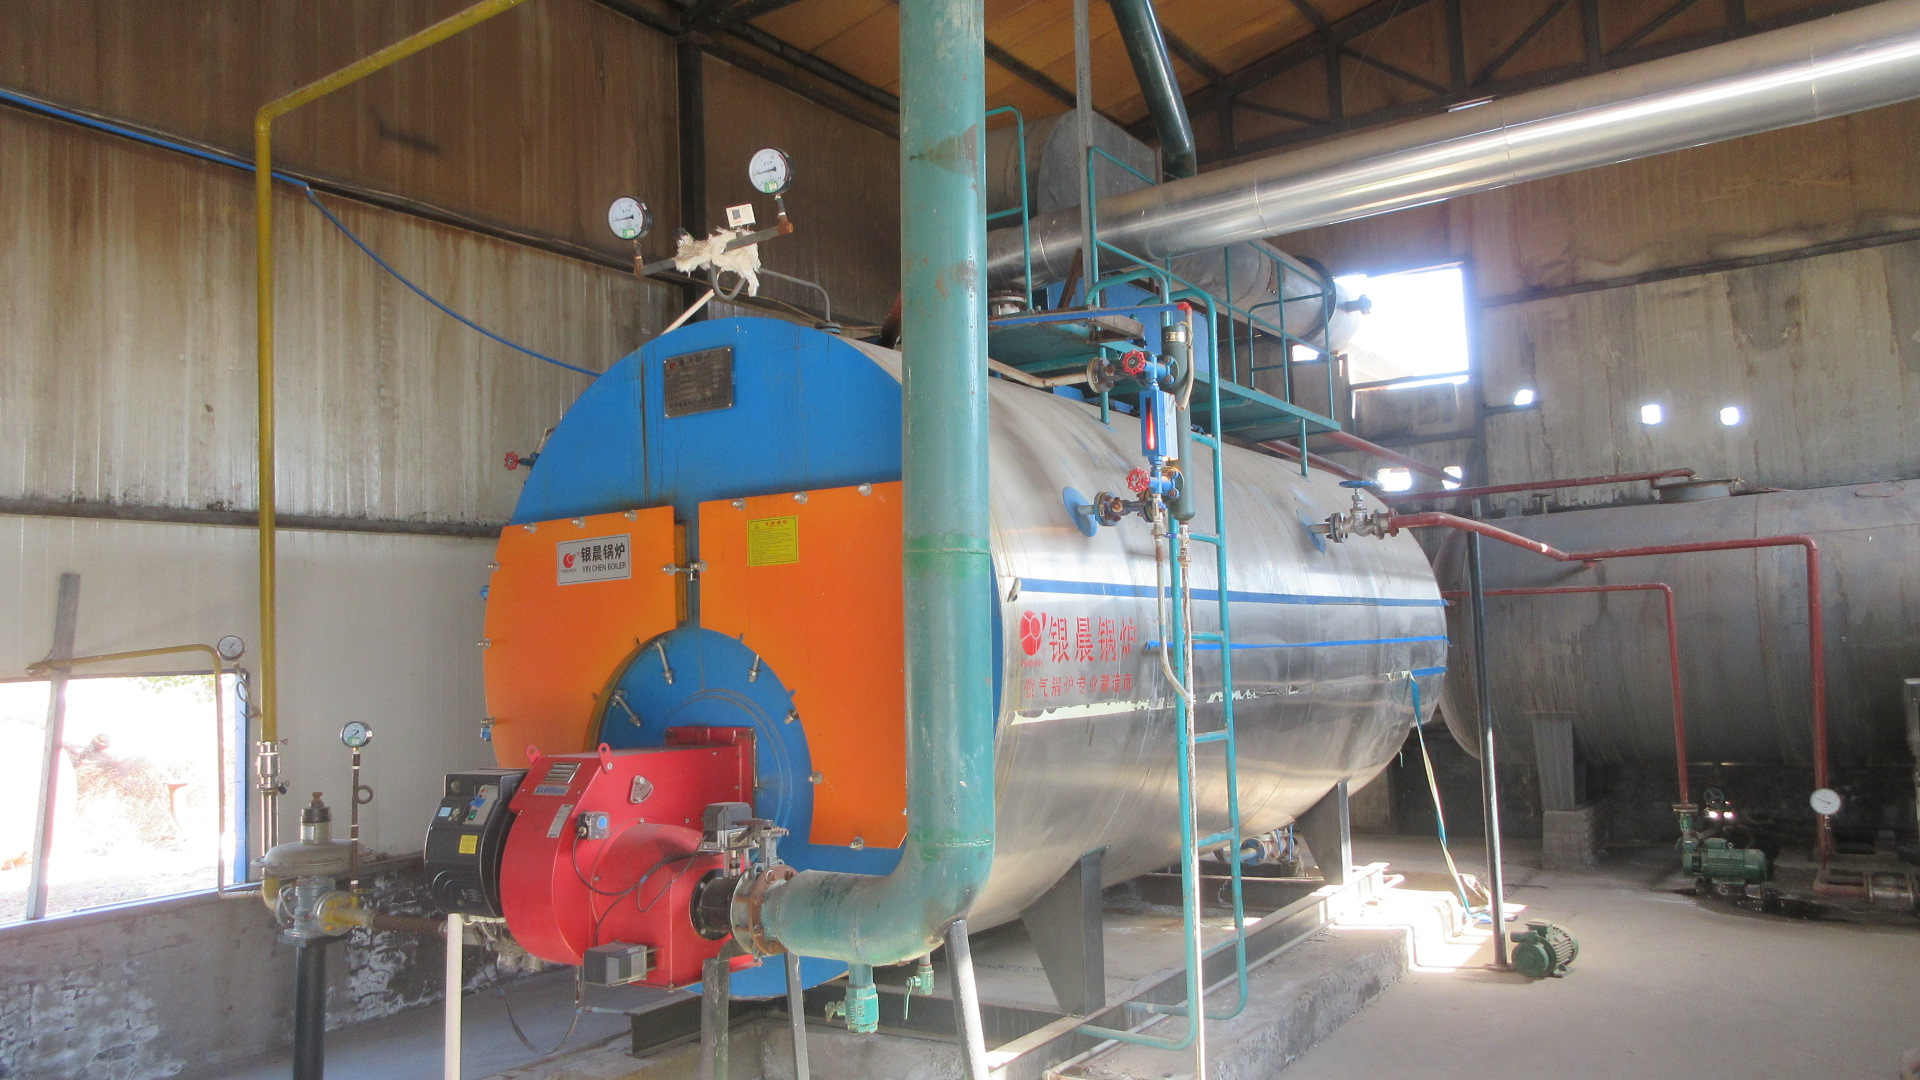
Clean thermal fluid delivery
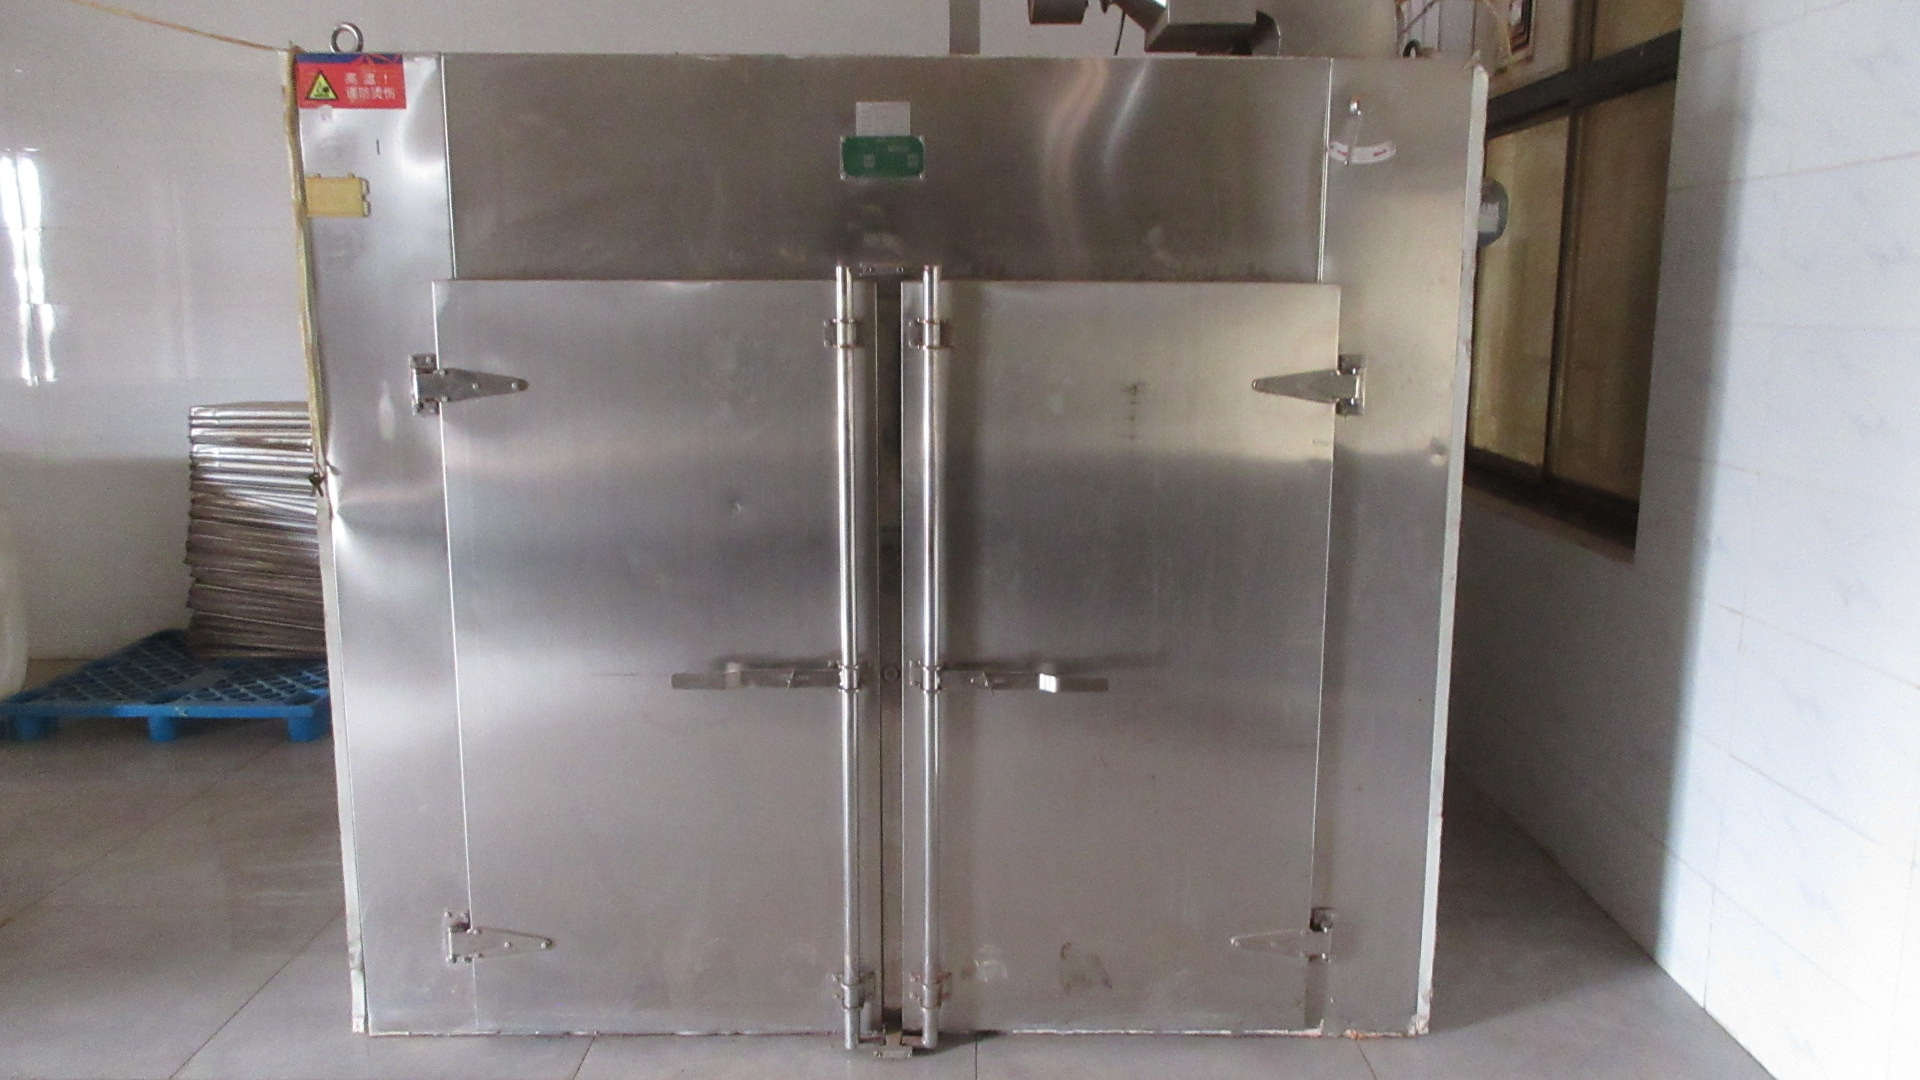
Controlled thermal processing
Every commercial batch undergoes multi-stage physicochemical and microbiological testing prior to Certificate of Analysis (COA) release.
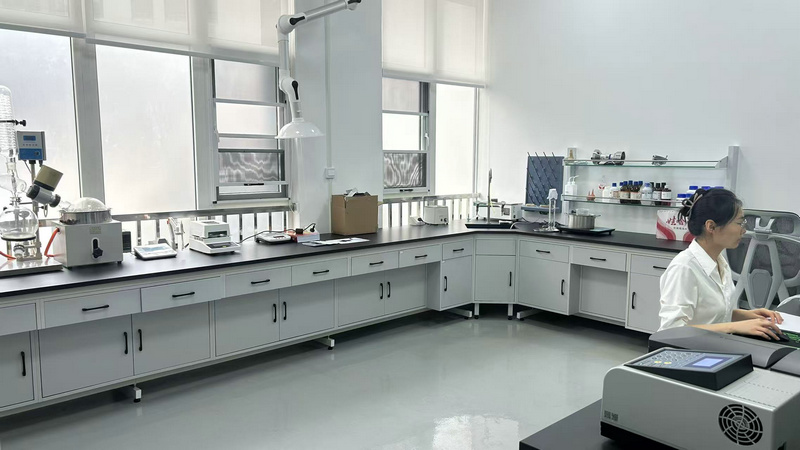
Routine QC testing bench
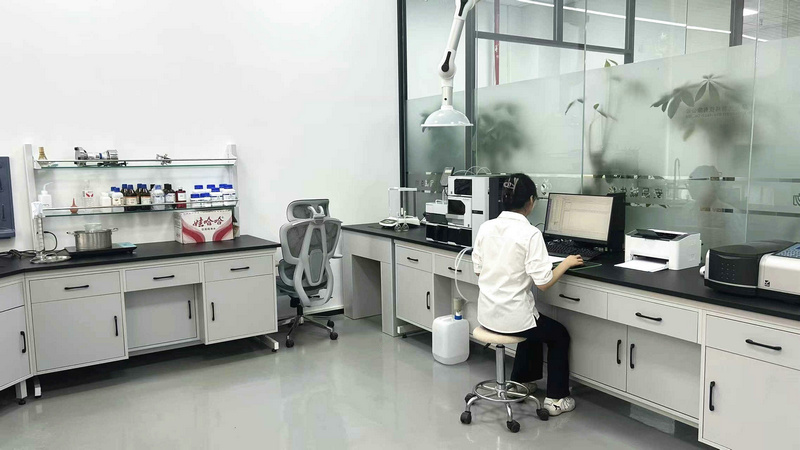
Standardized pharmacopeia assays
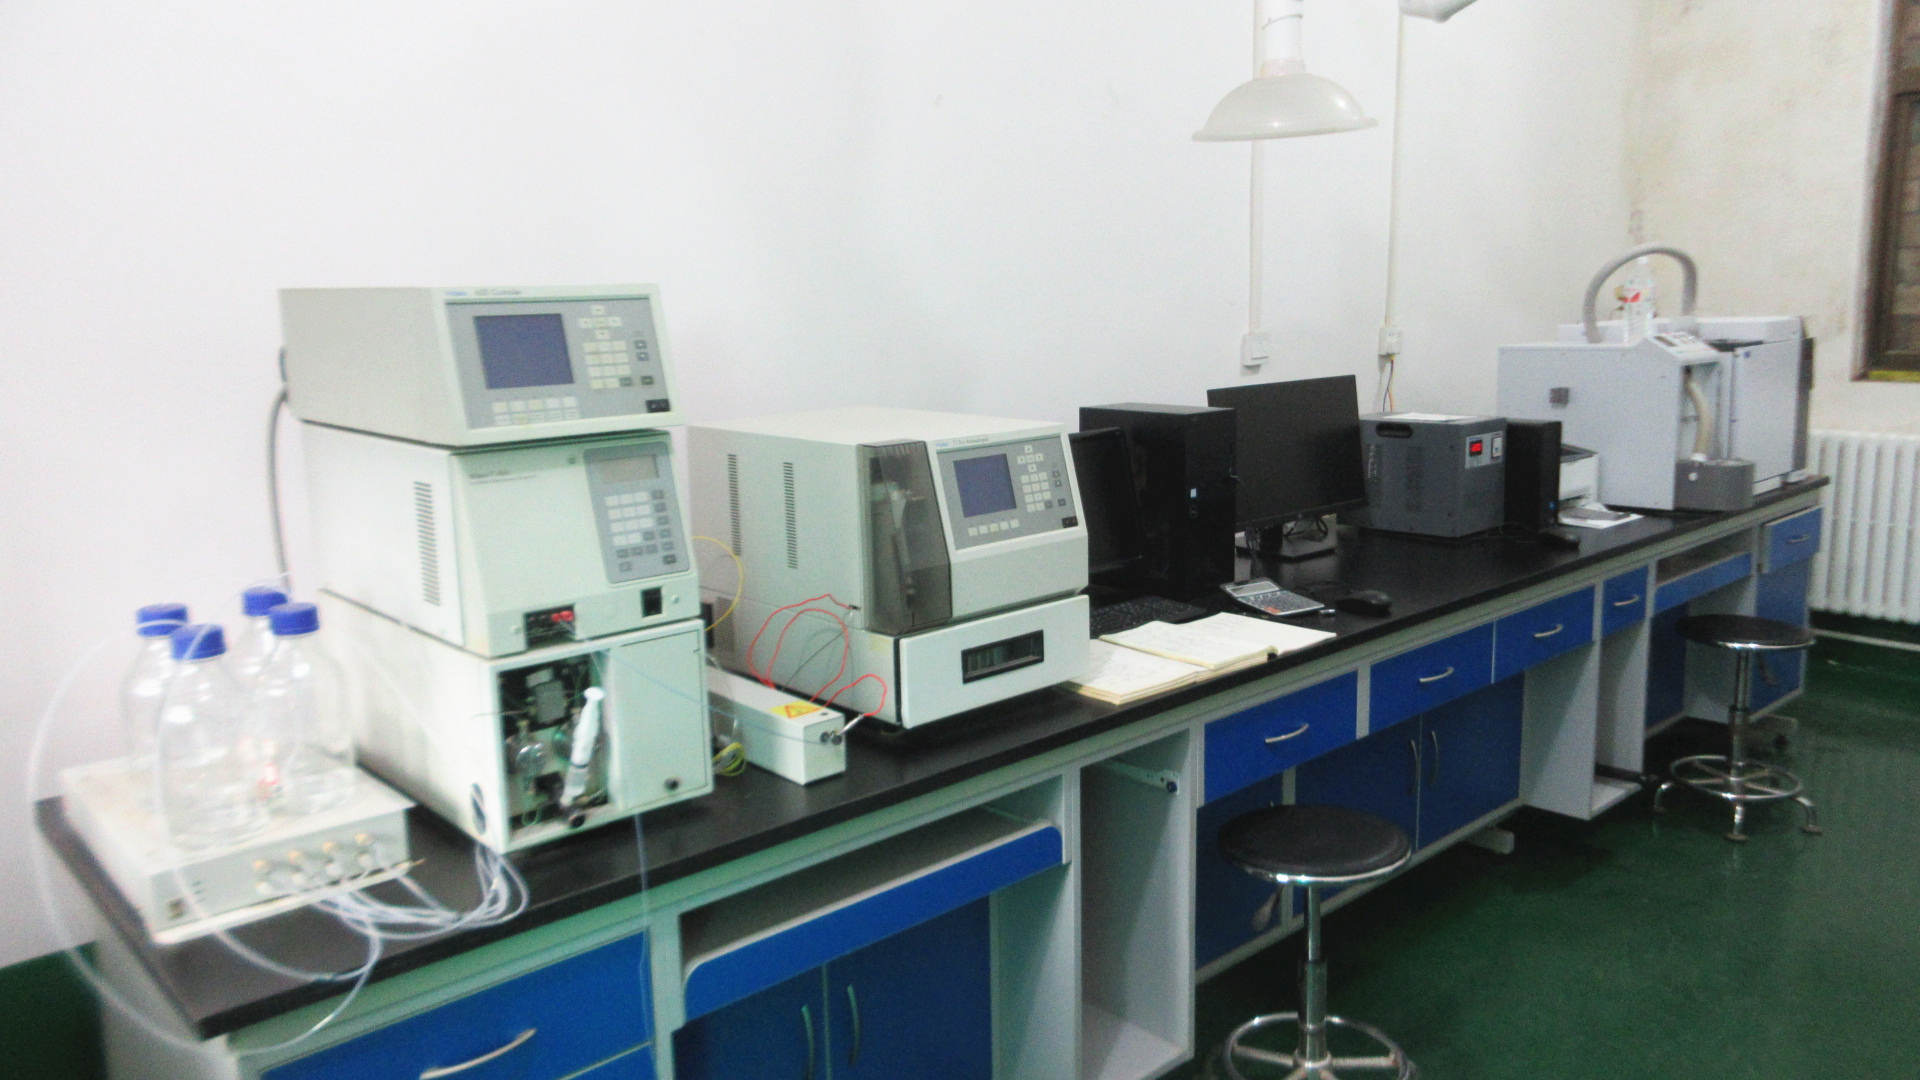
Active compound profiling
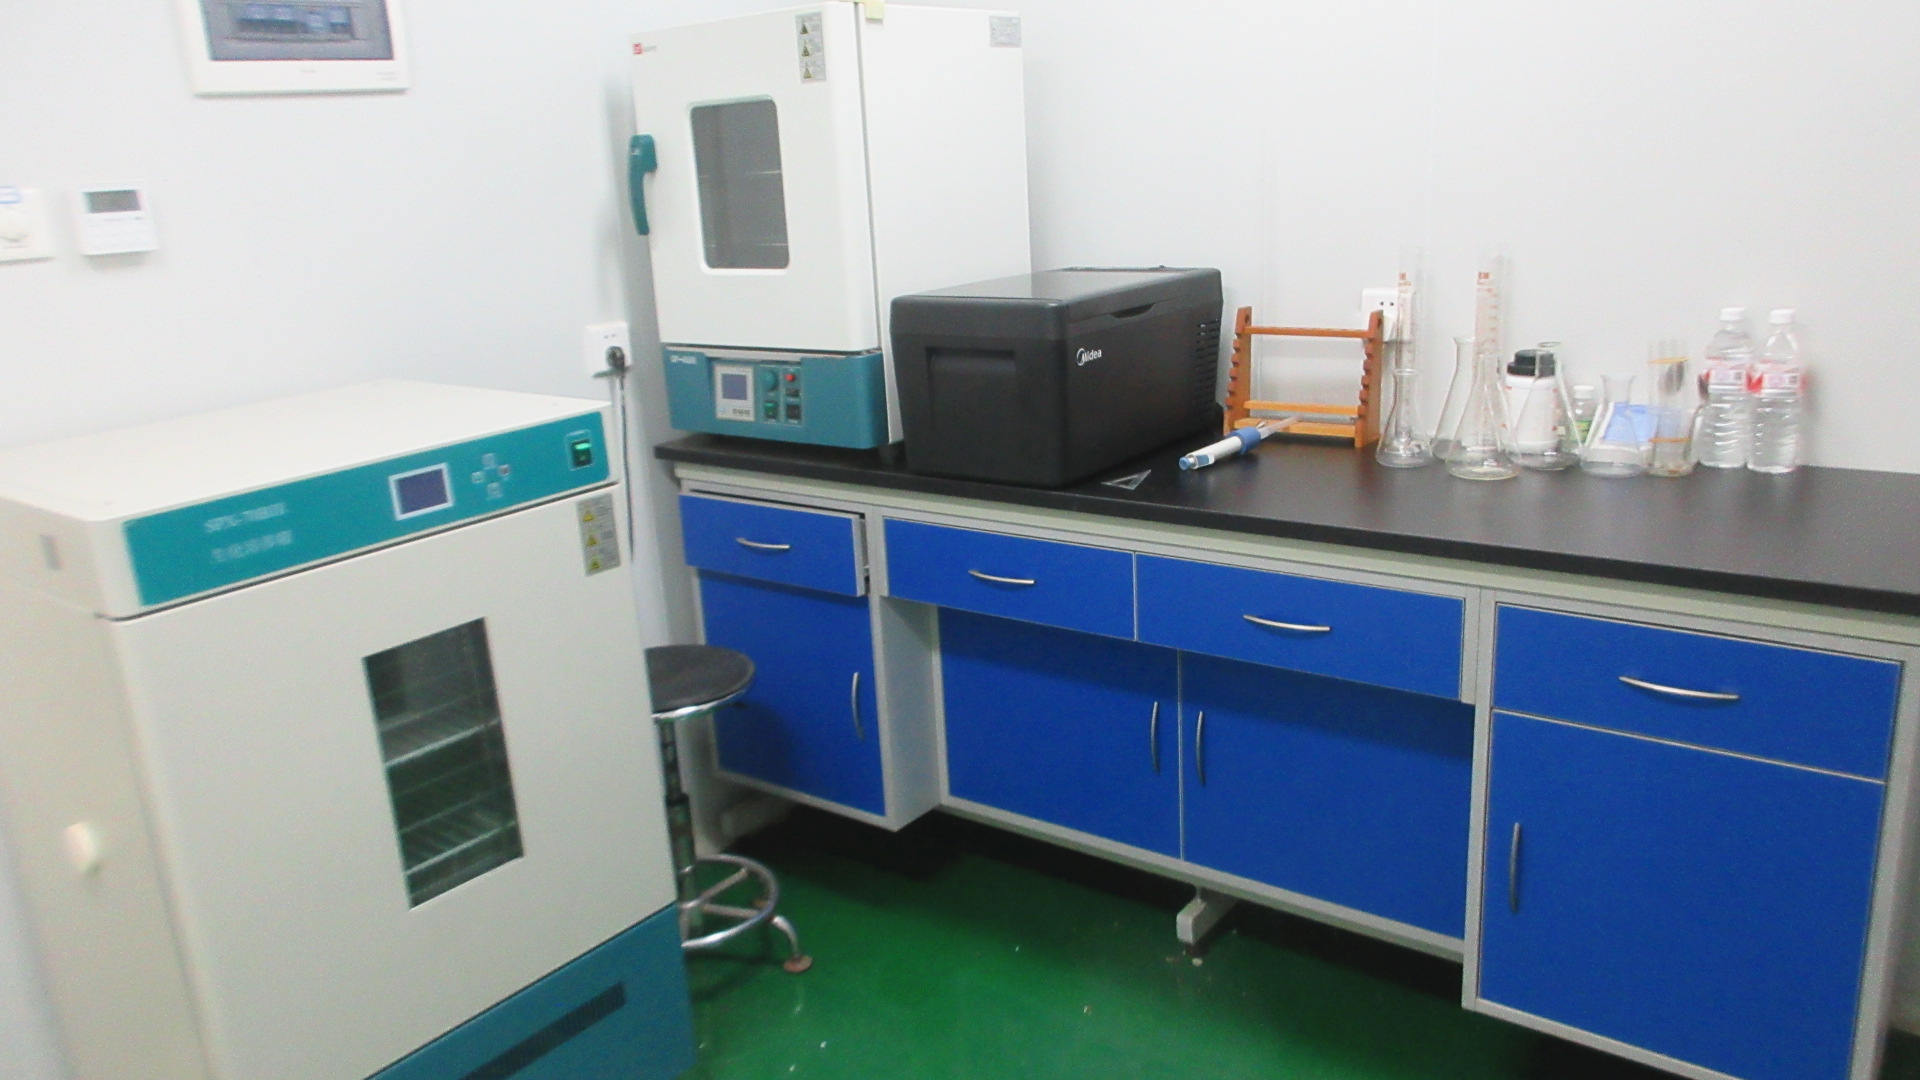
TPC, Salmonella, E. Coli, Yeast
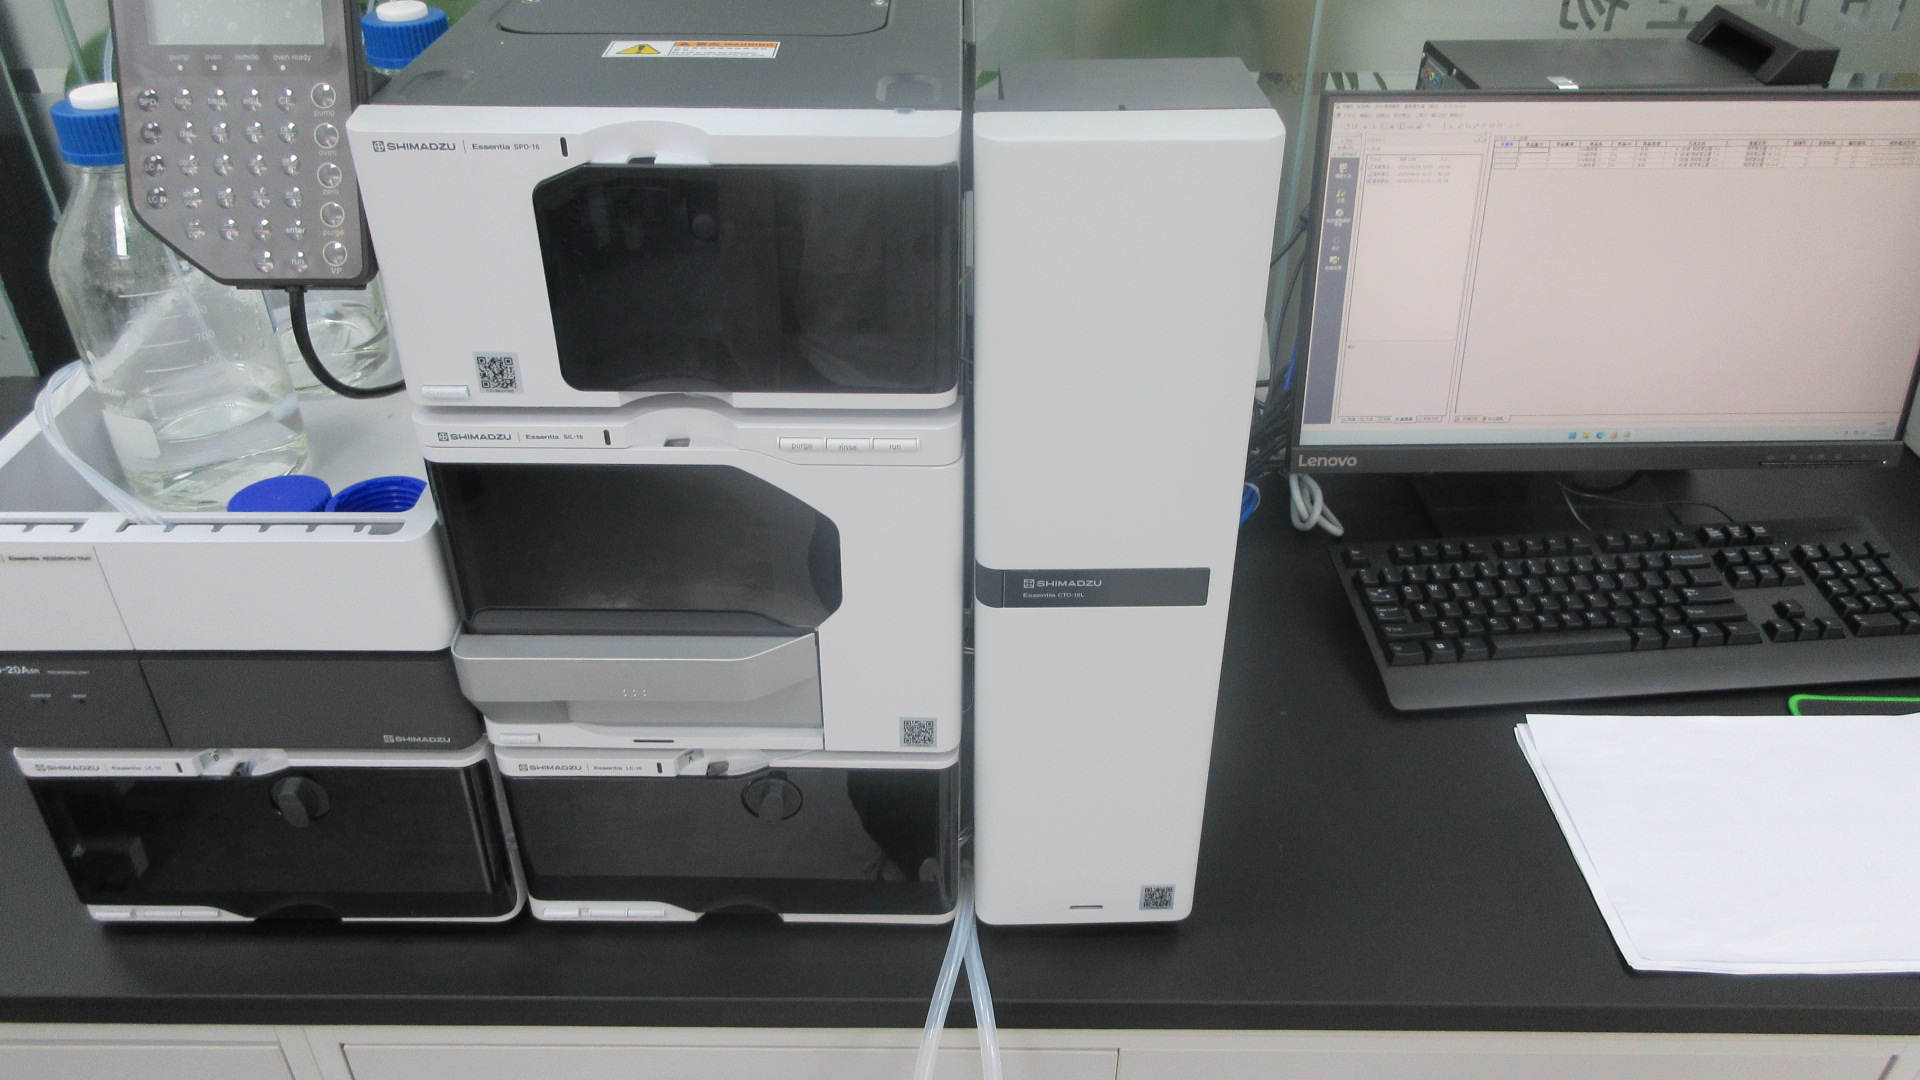
High performance chromatography
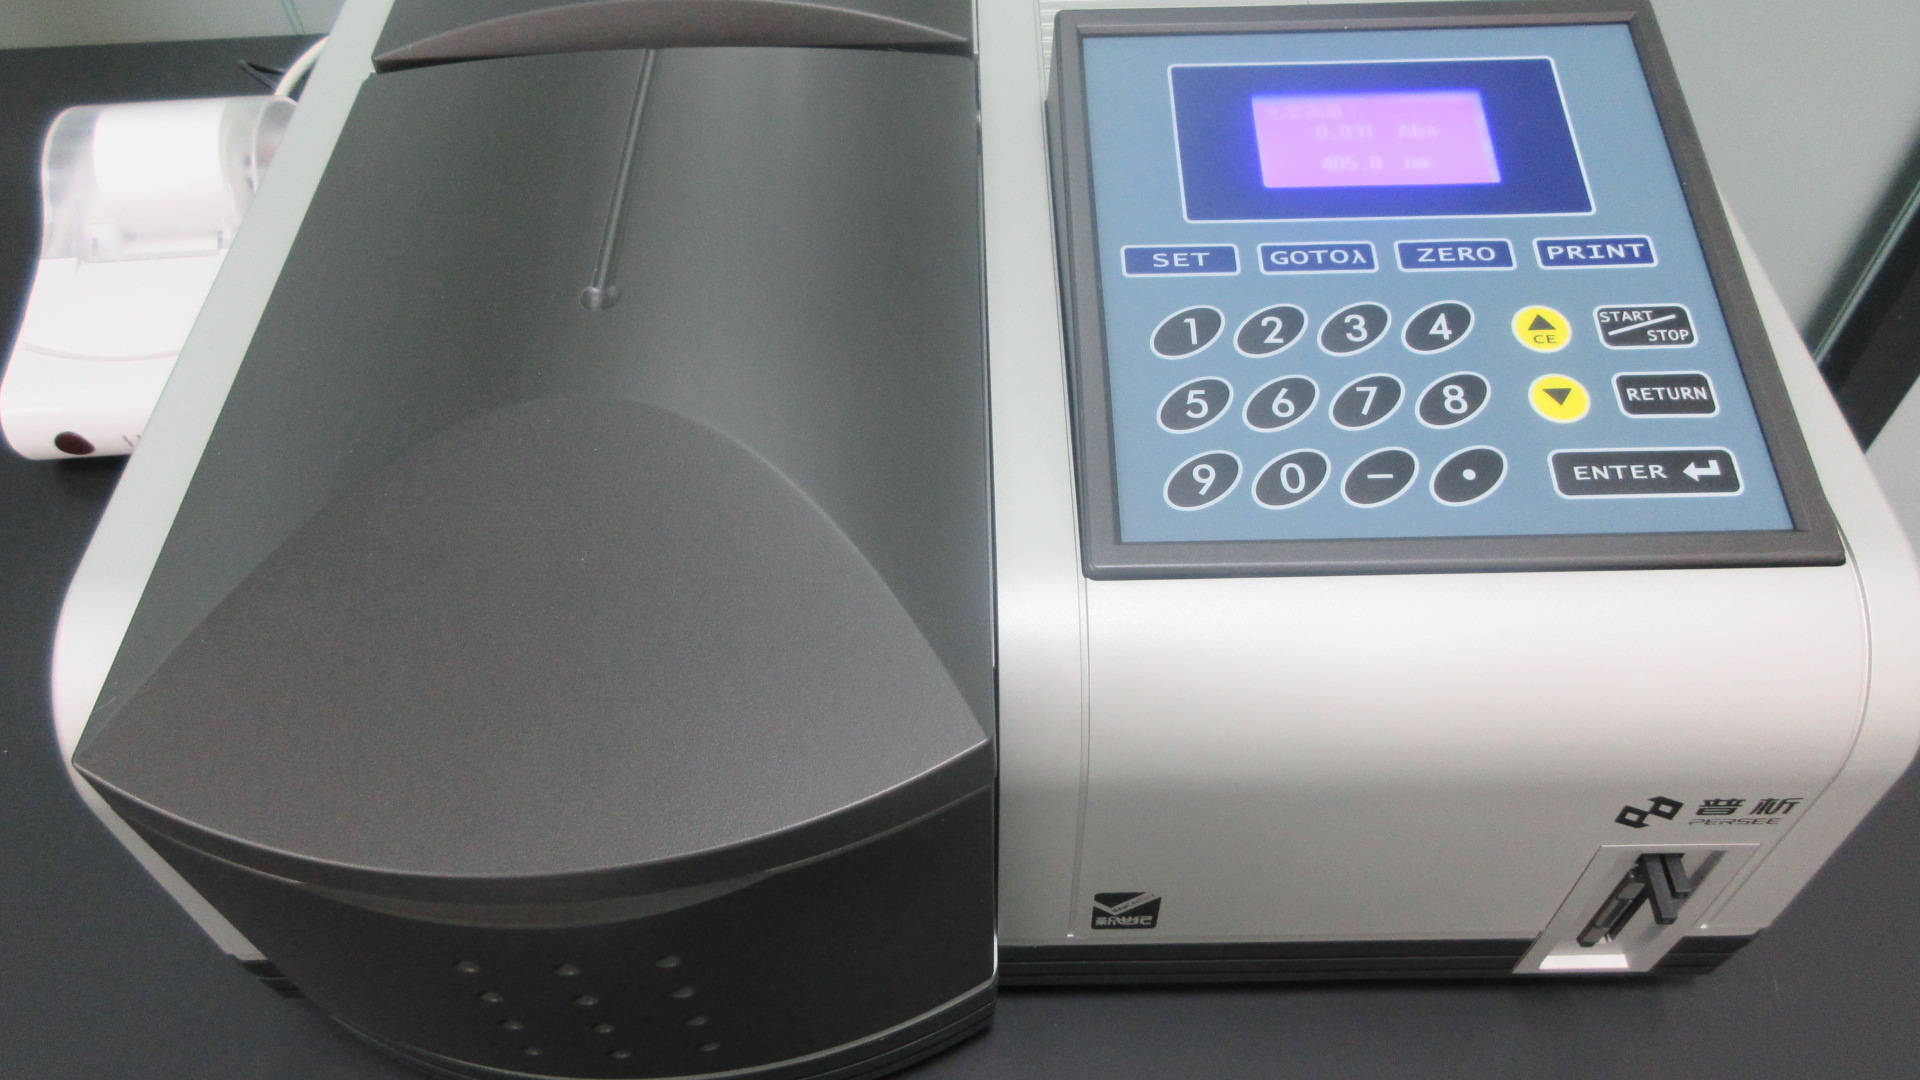
Spectroscopic assay quantification
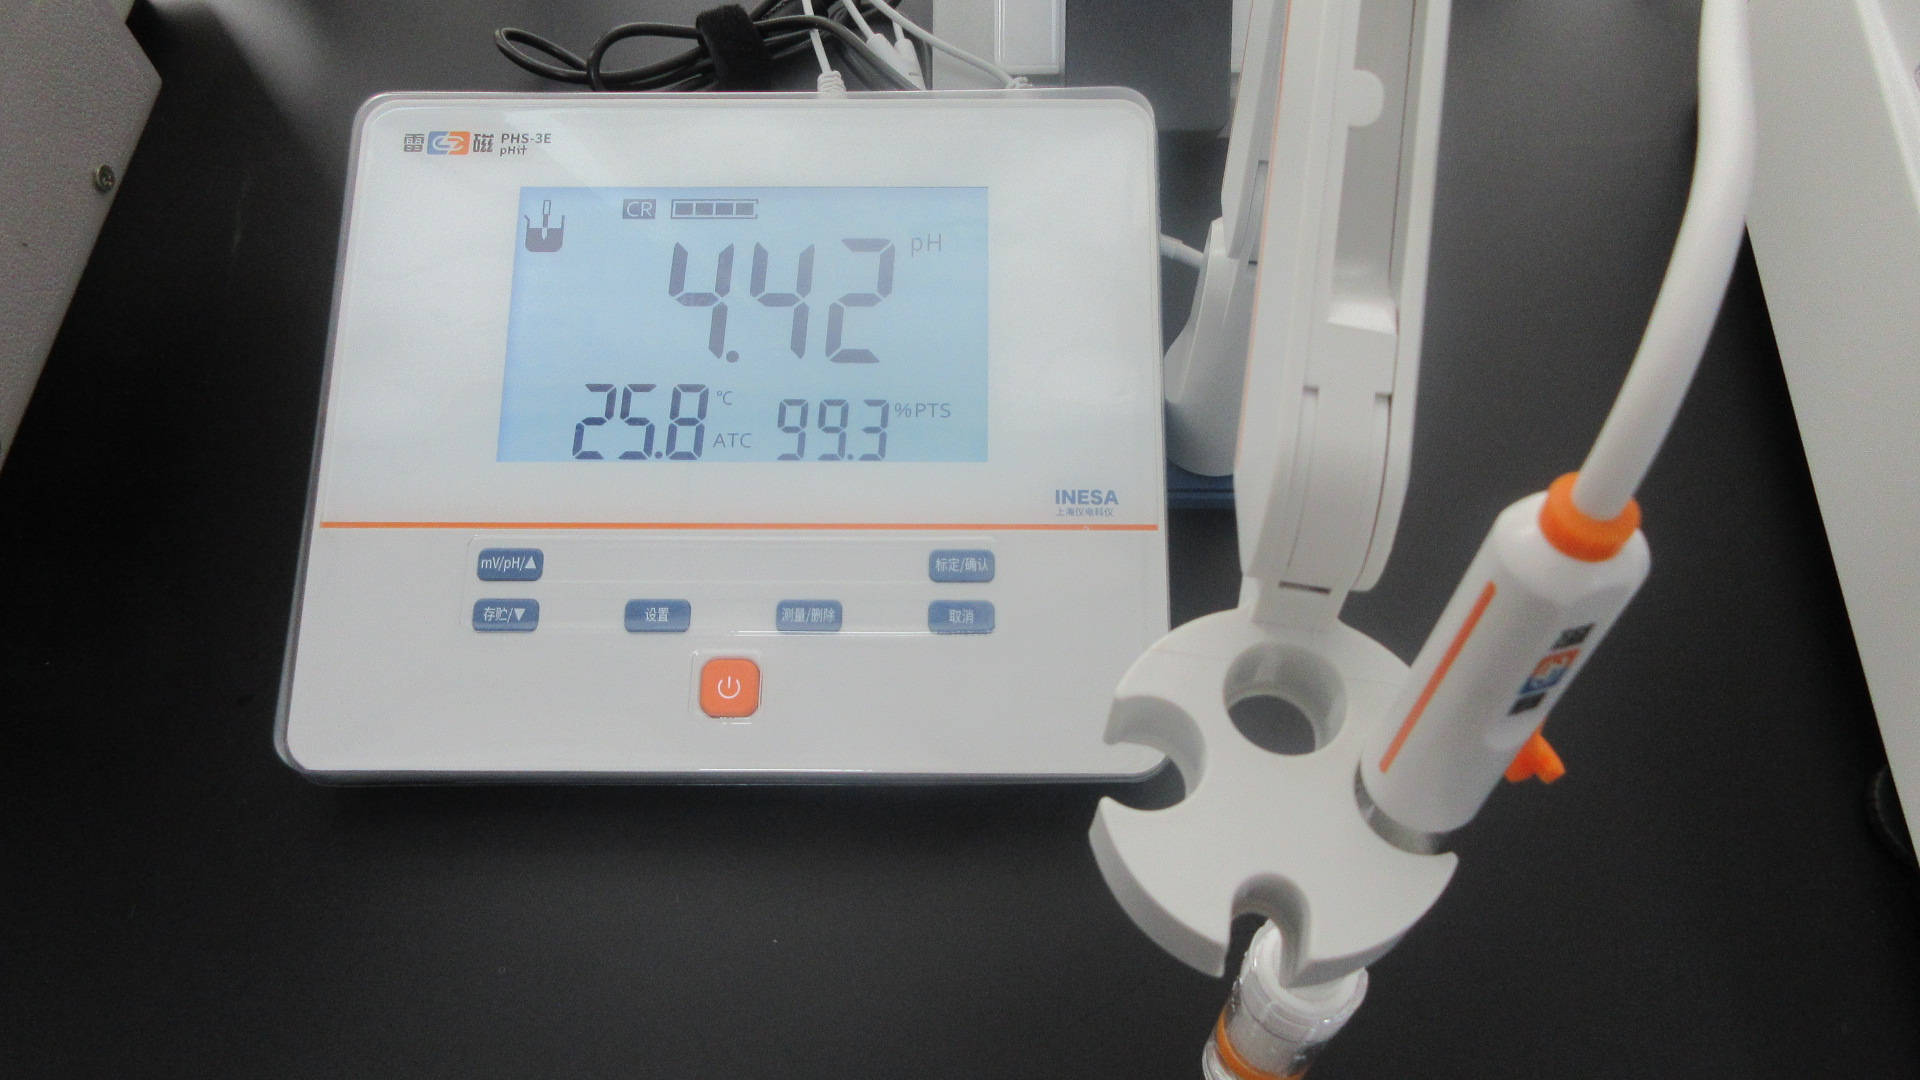
Electrochemical buffer analysis
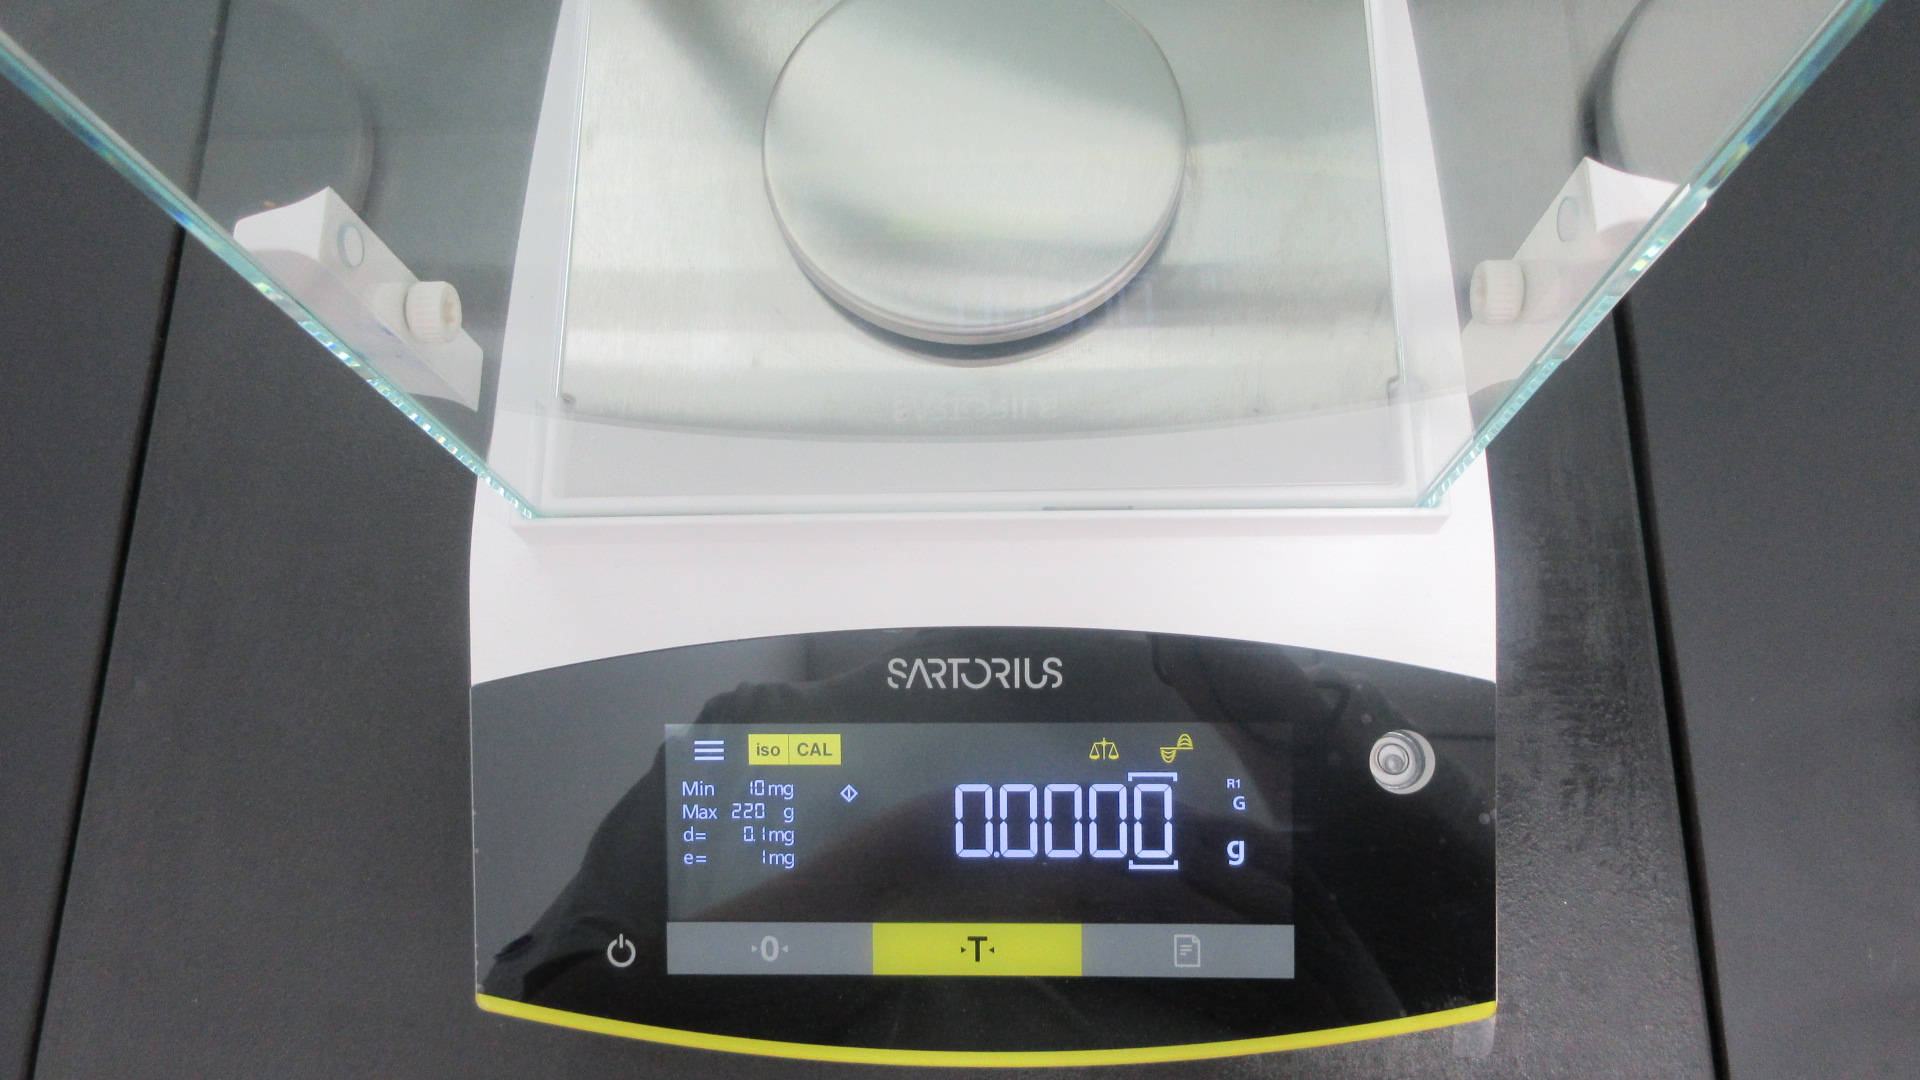
Four-decimal high precision
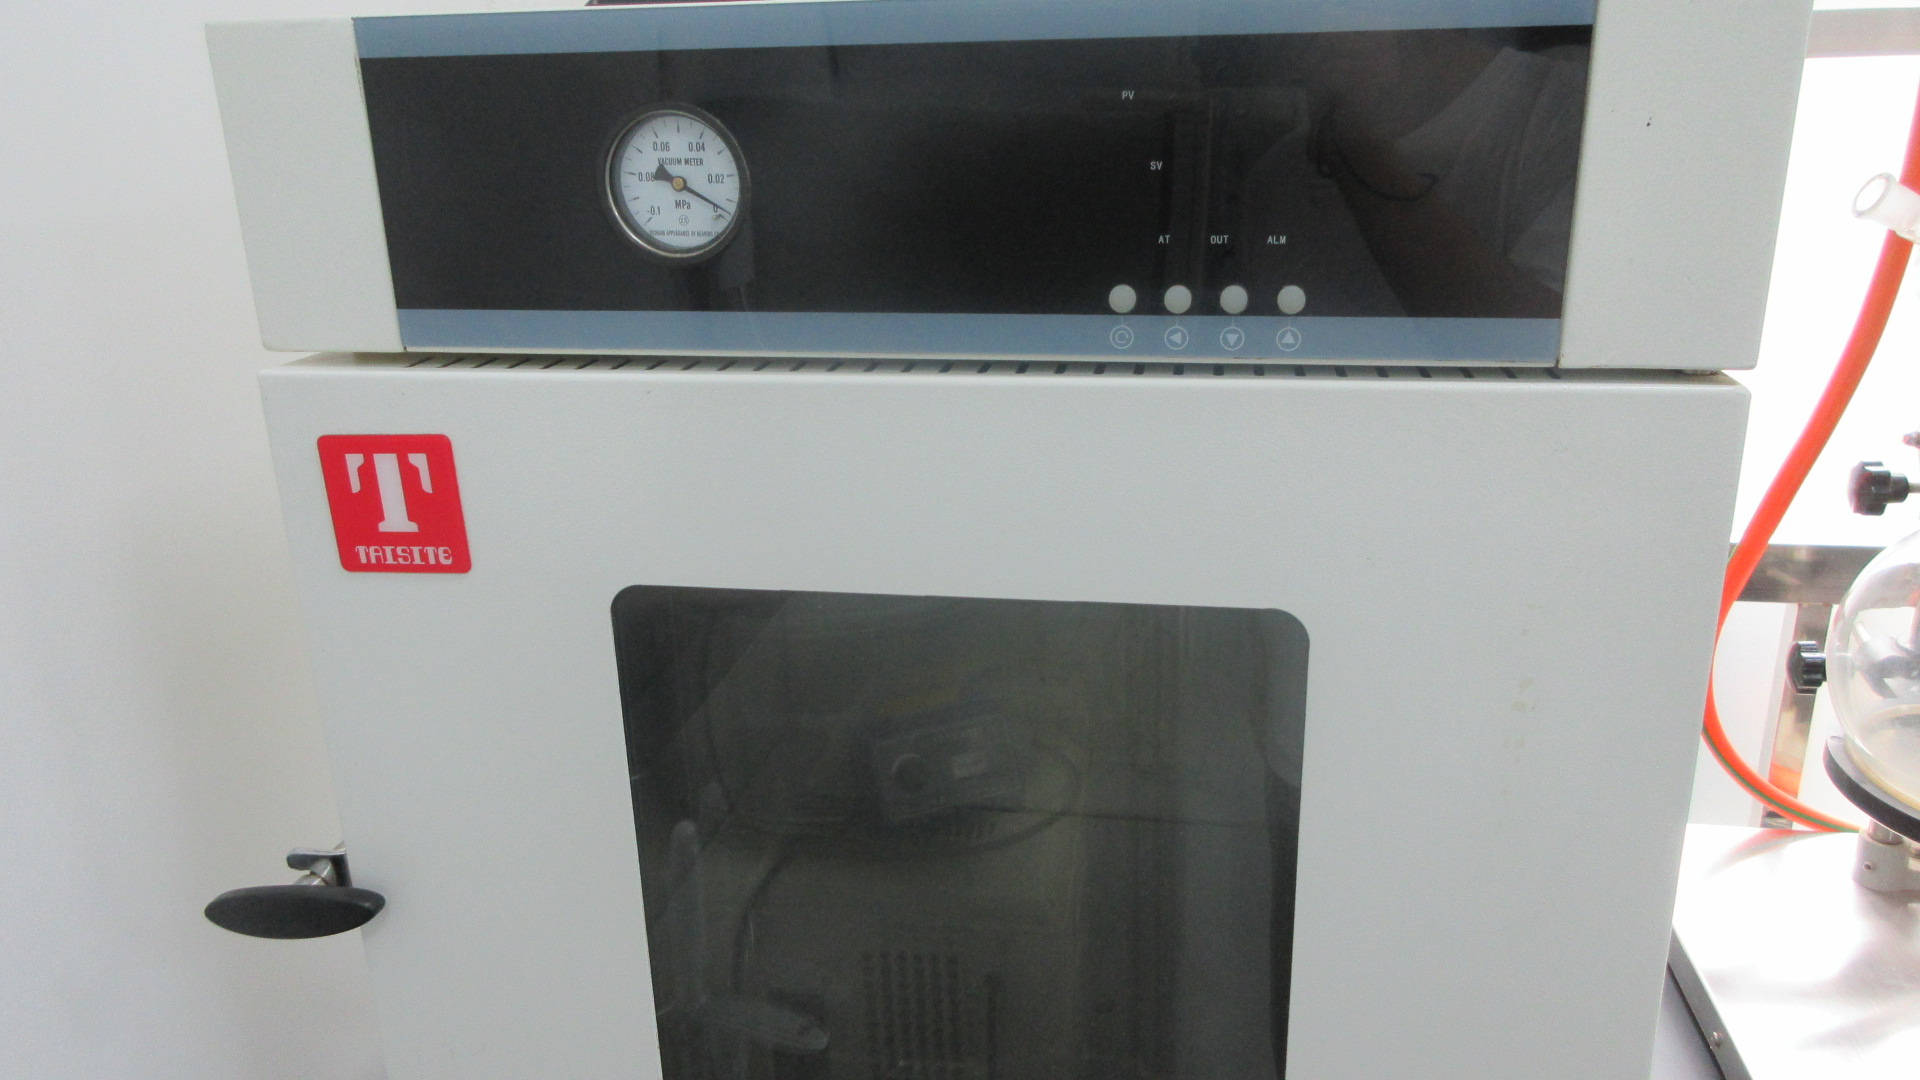
Low-temperature moisture testing
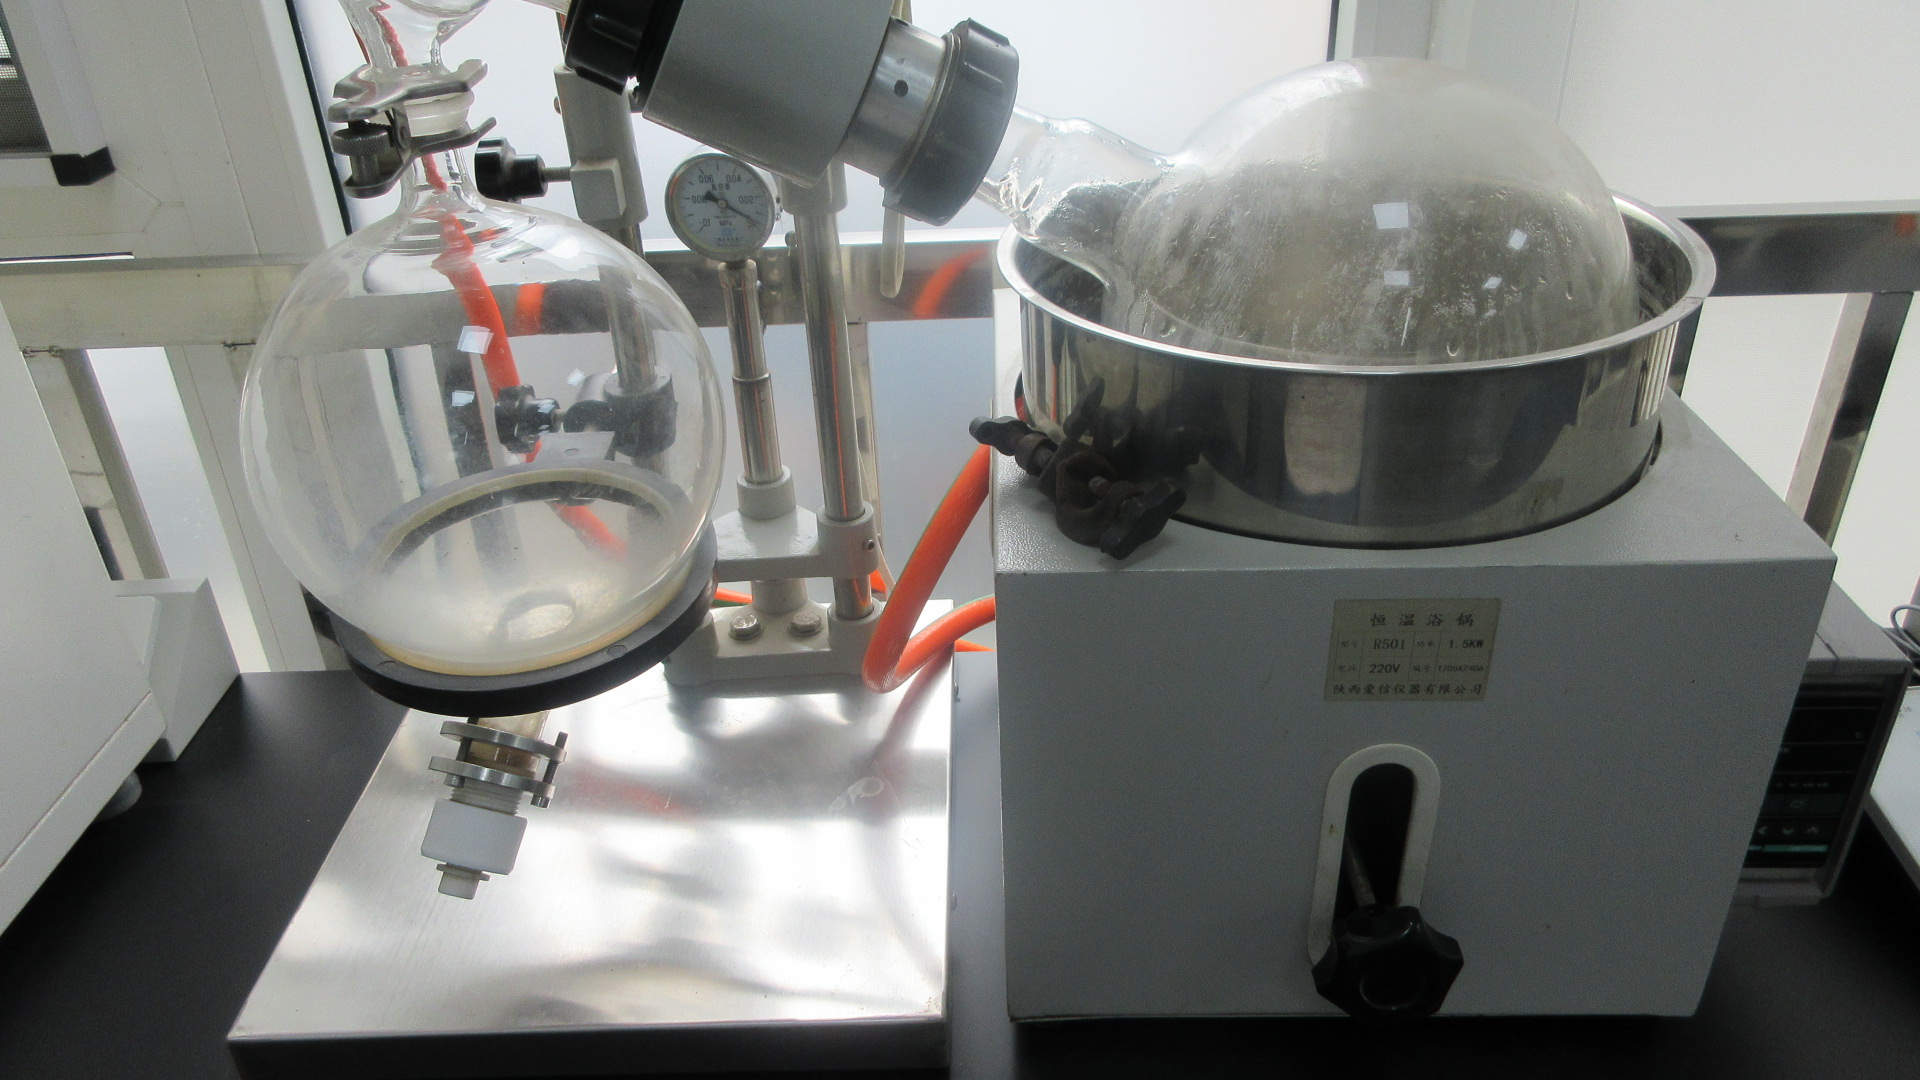
Solvent recovery & assay trials
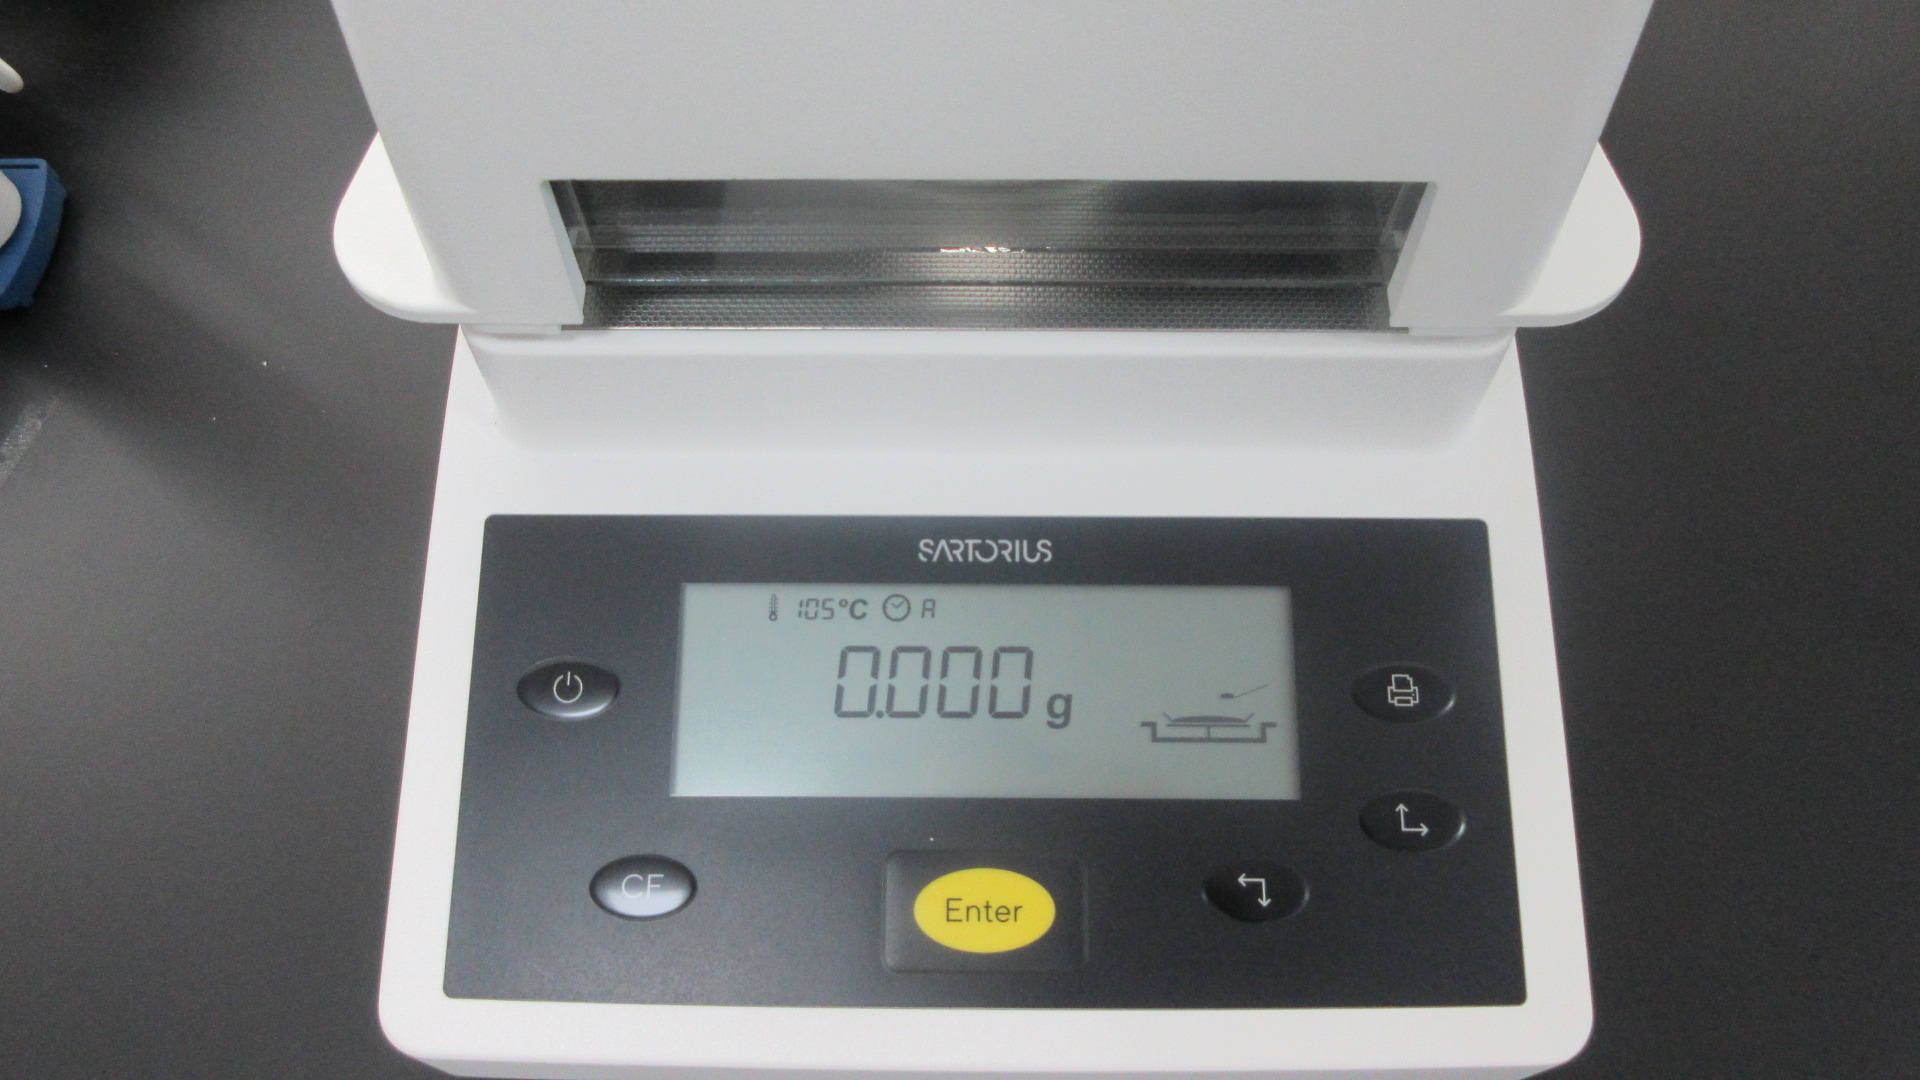
Loss on drying (LOD) check
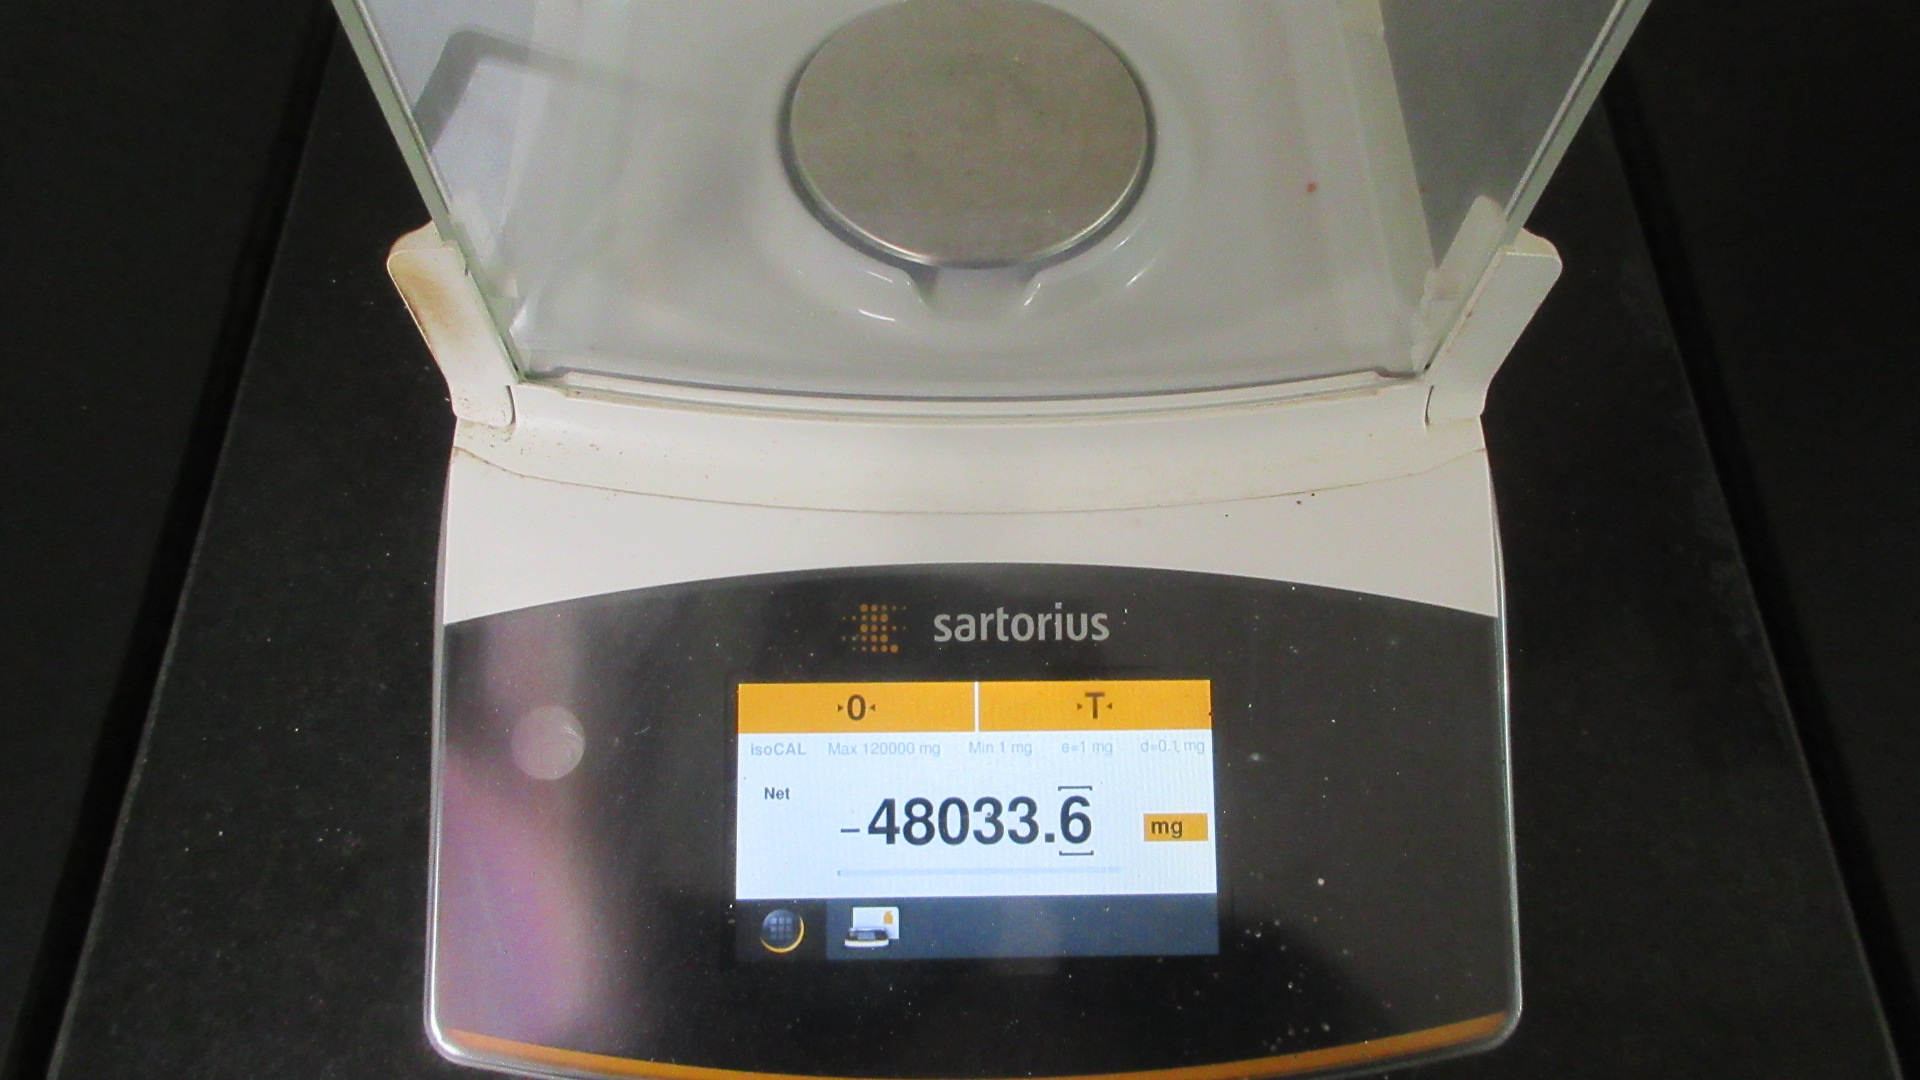
Micro-gram gravimetric checks
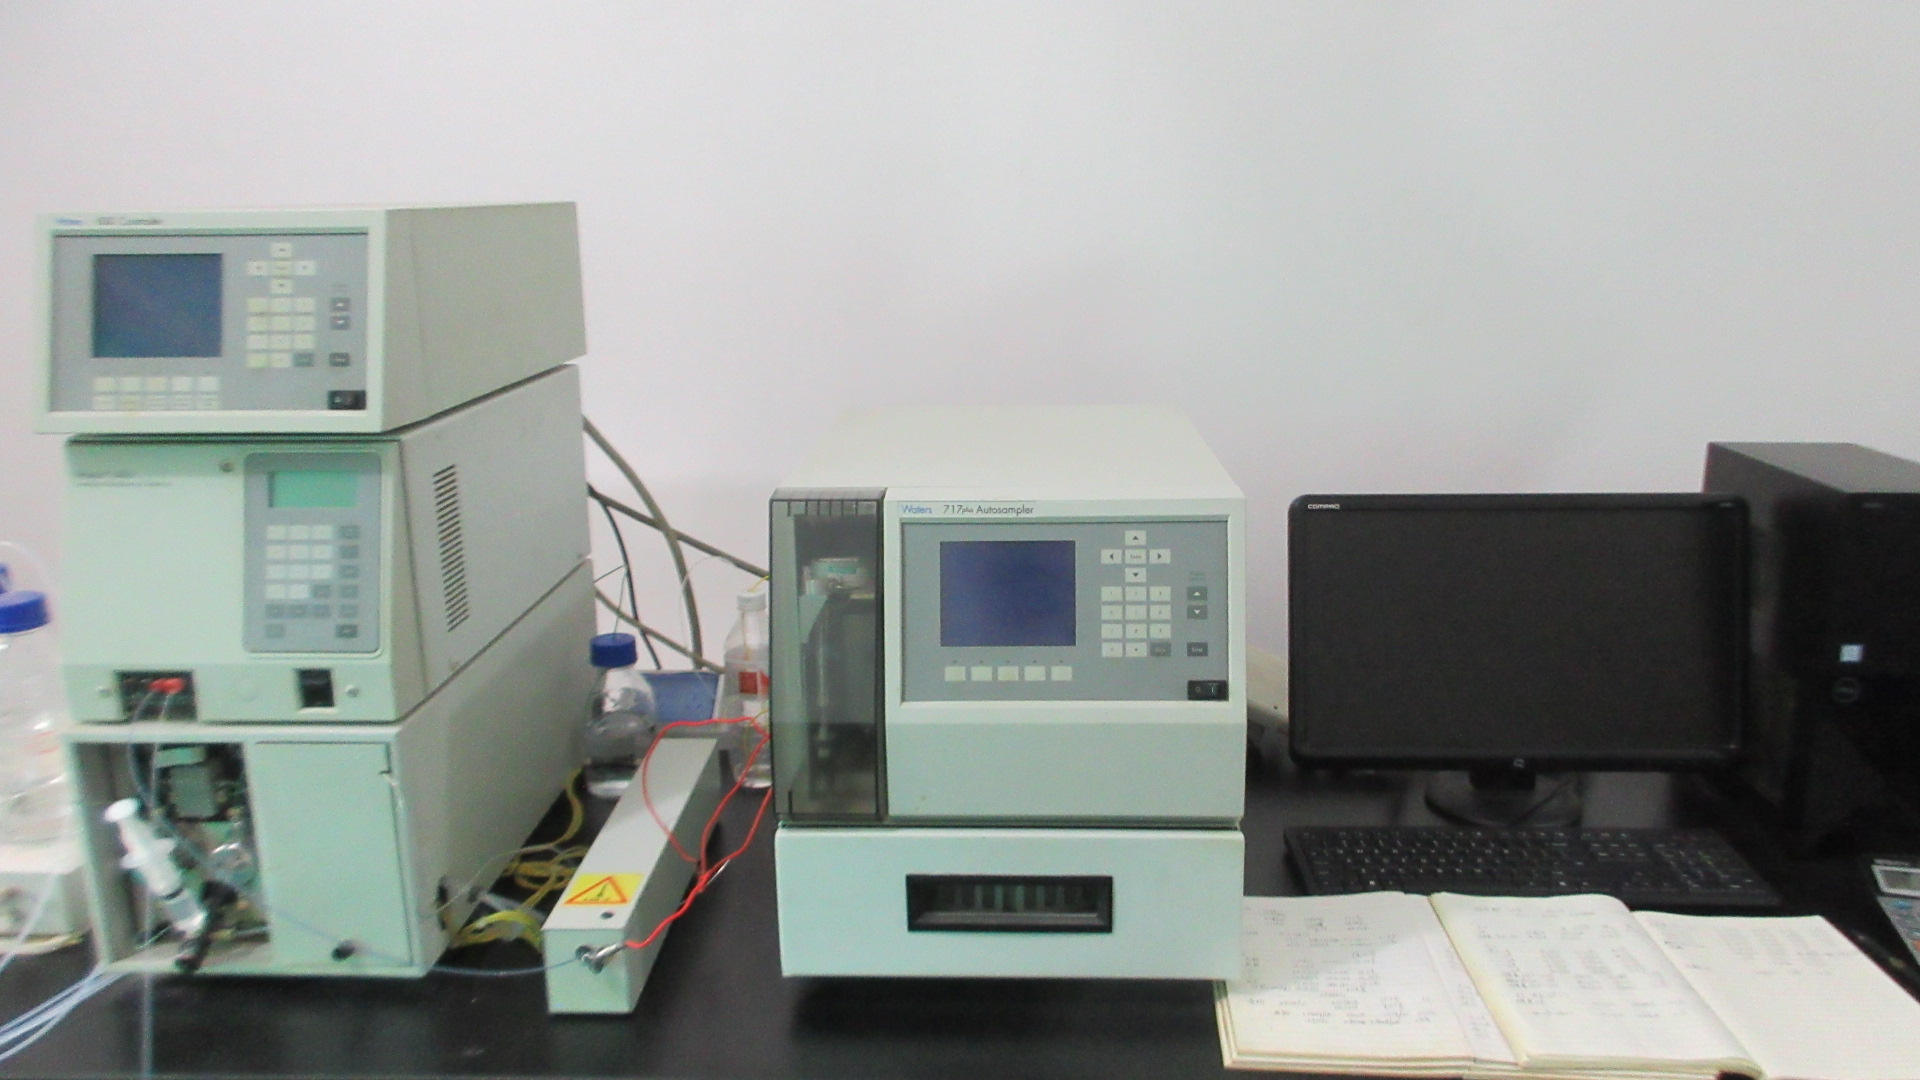
Active compound separation
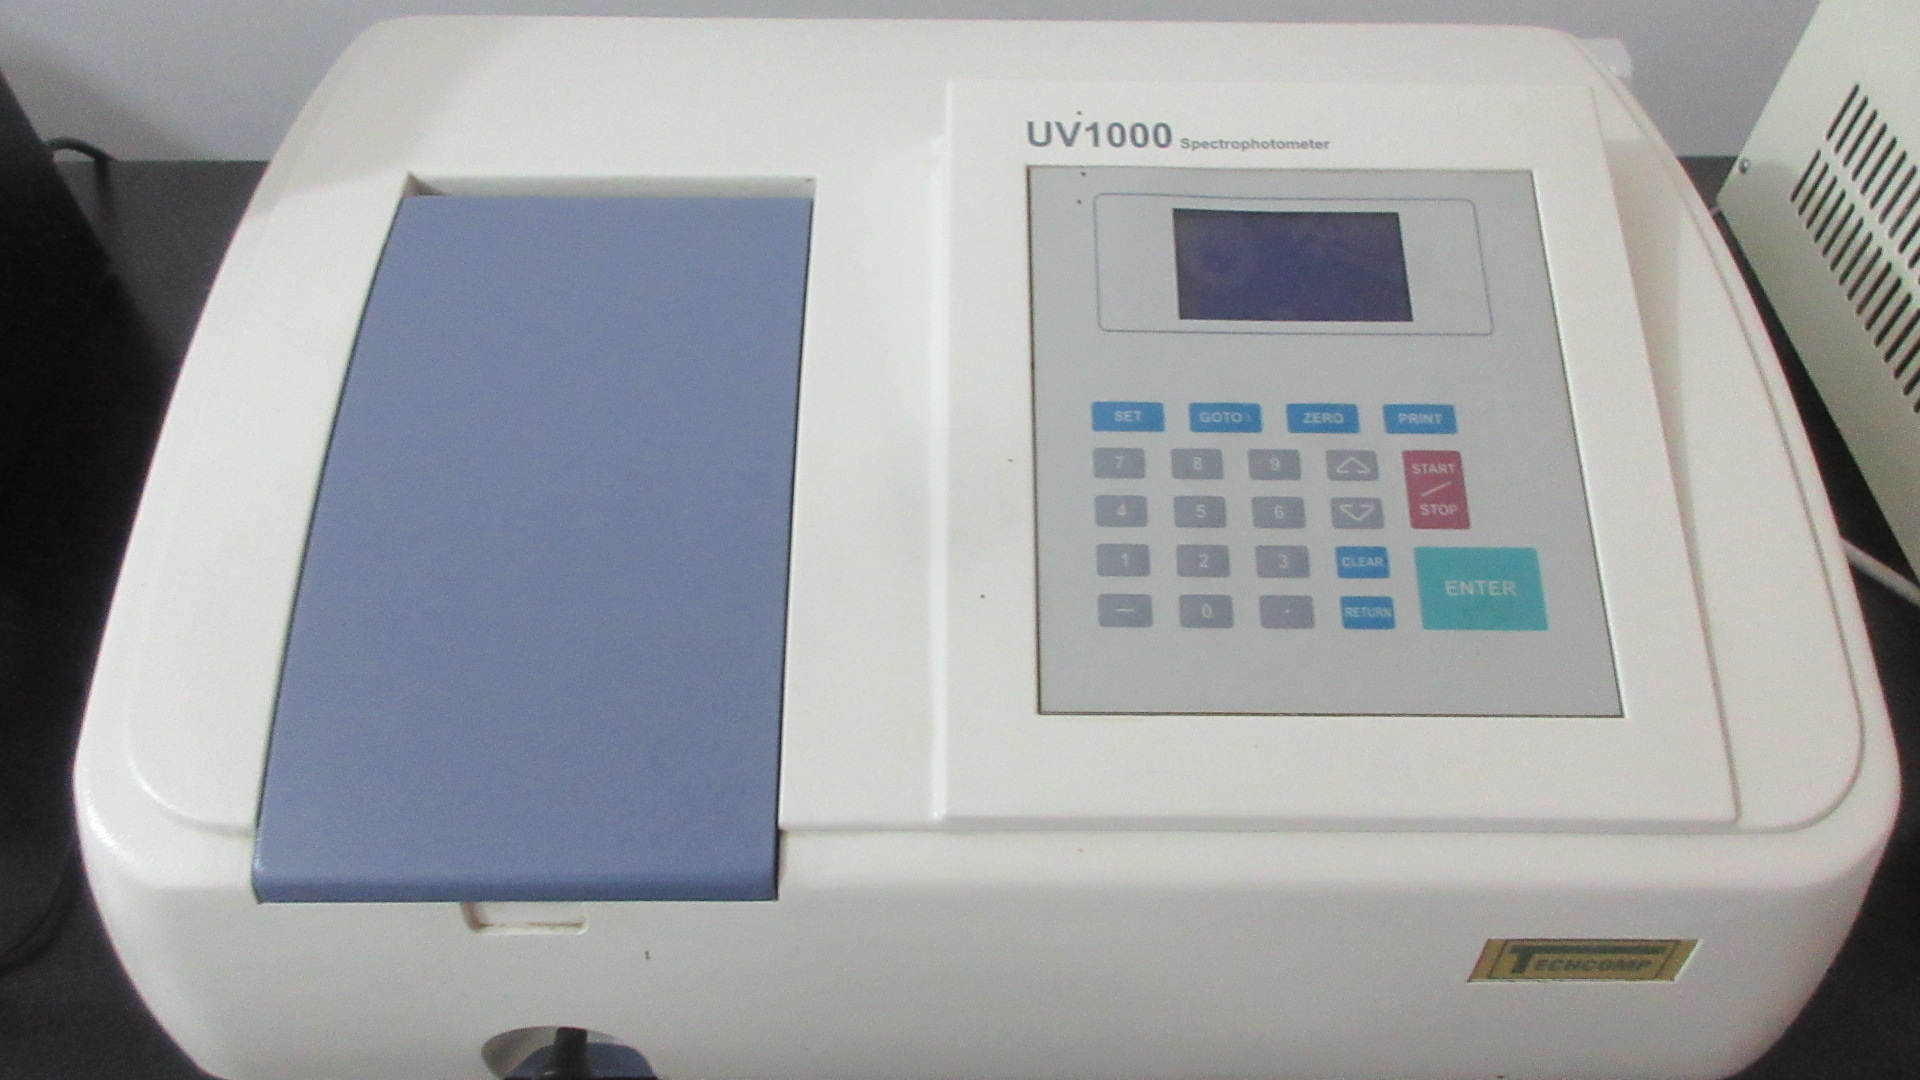
Color value & polysaccharide analysis
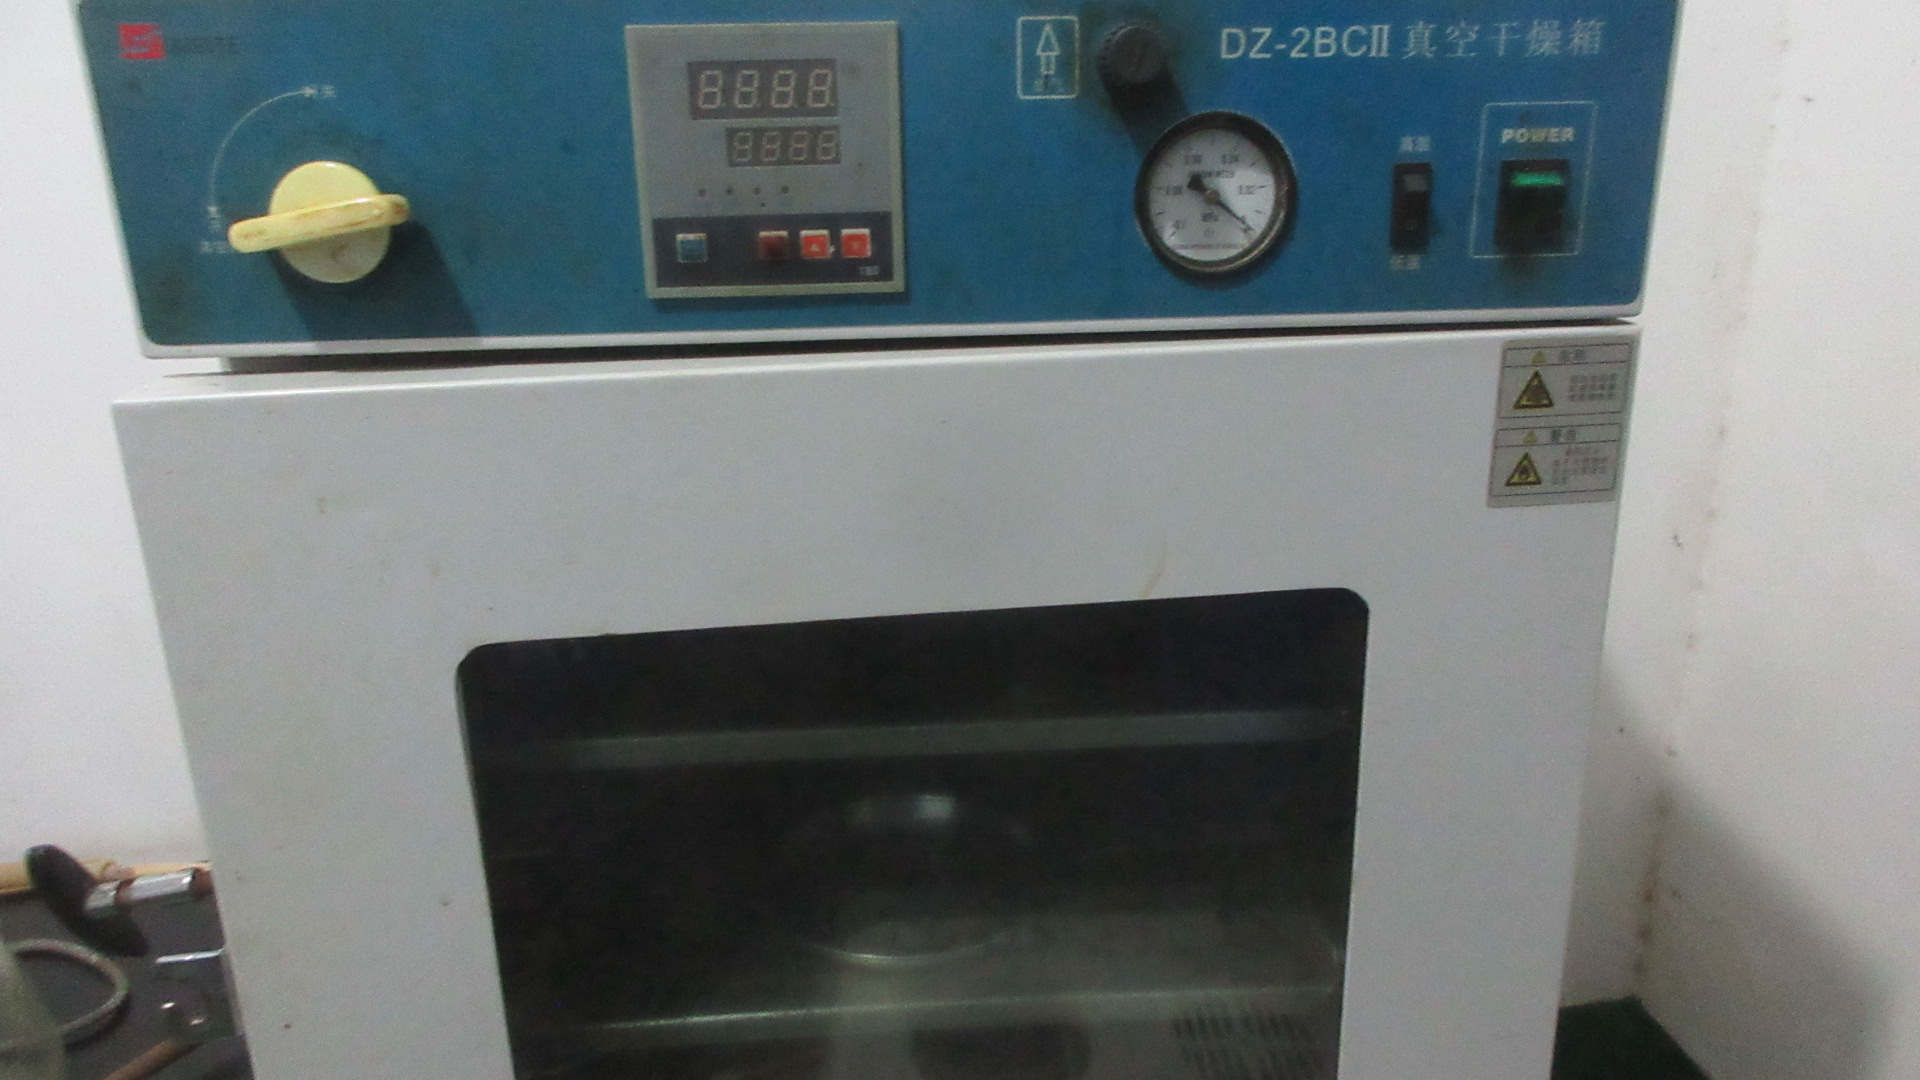
Constant temperature thermal dry
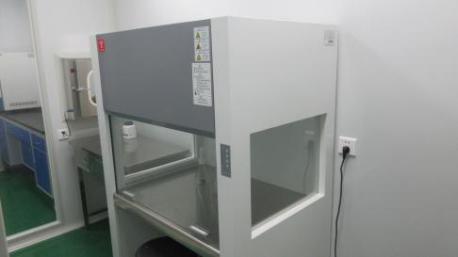
Laminar flow aseptic enclosure
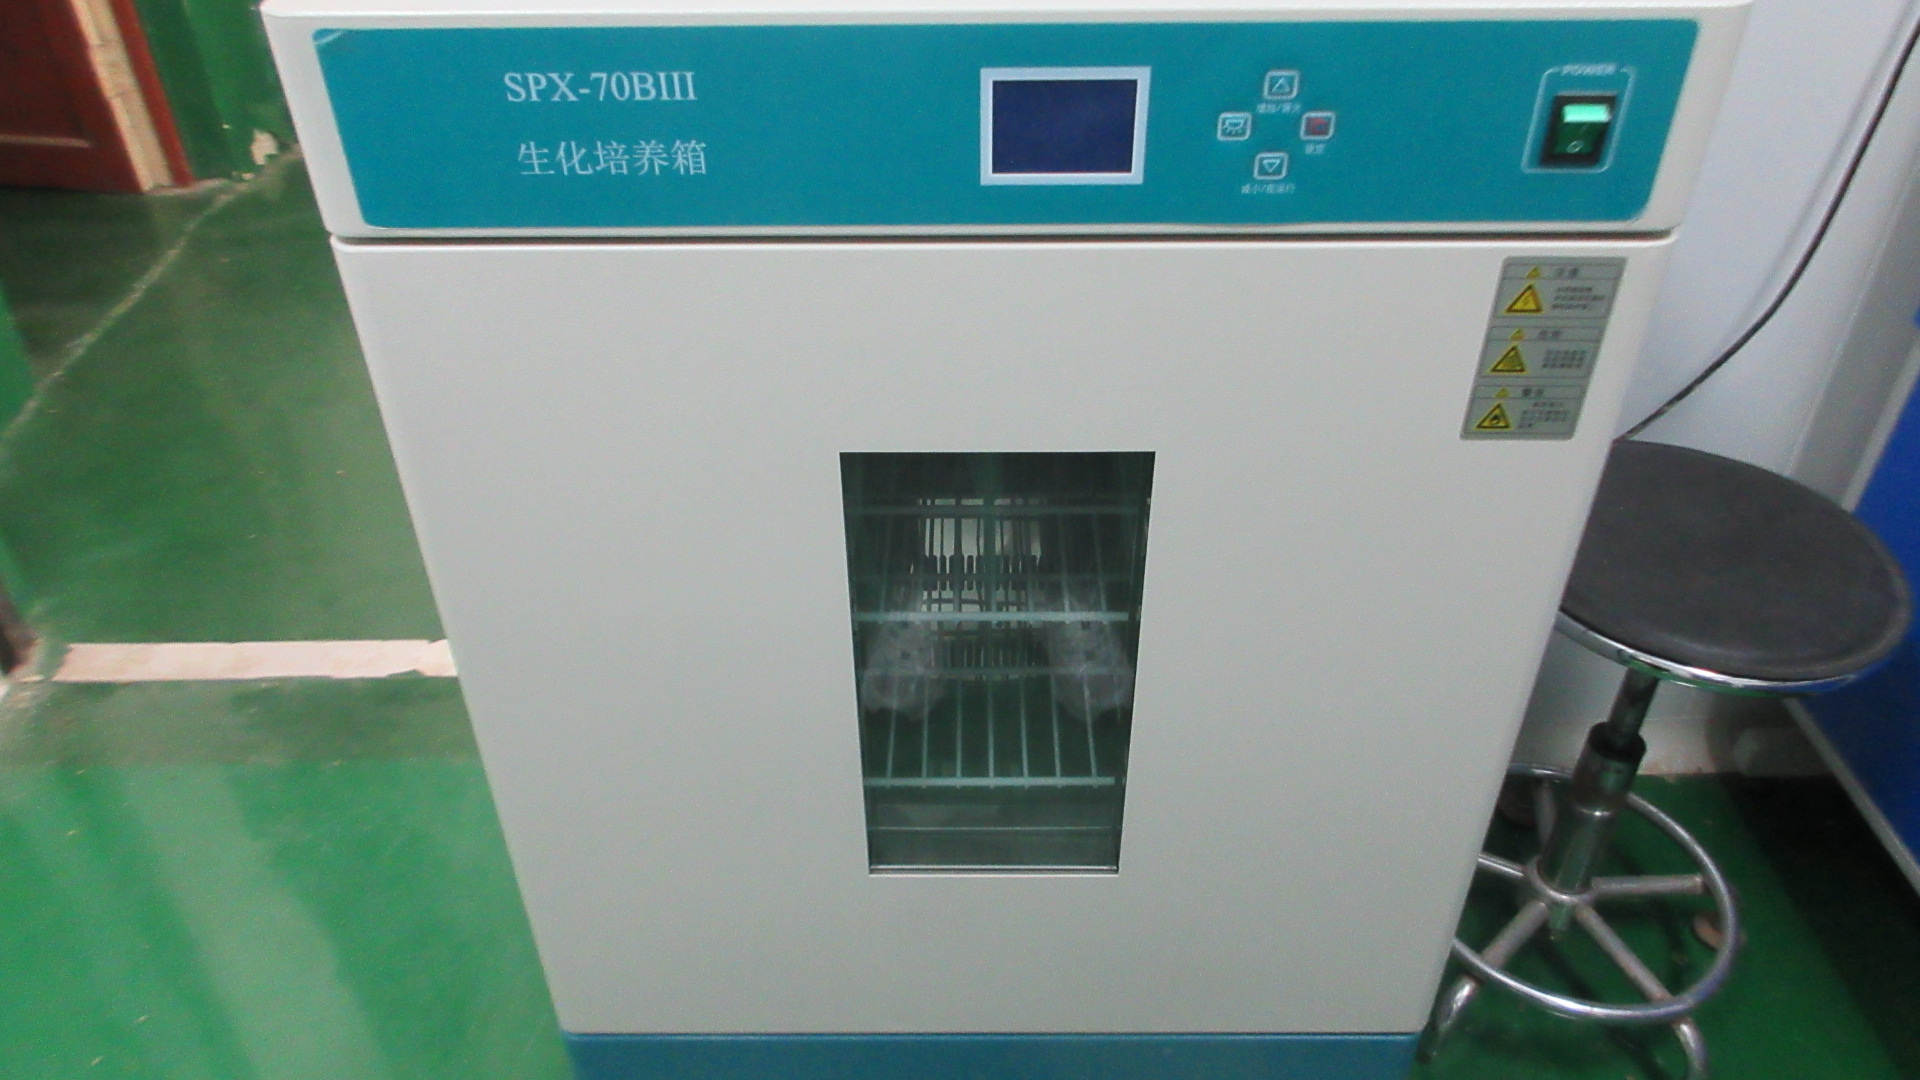
Constant temperature culture
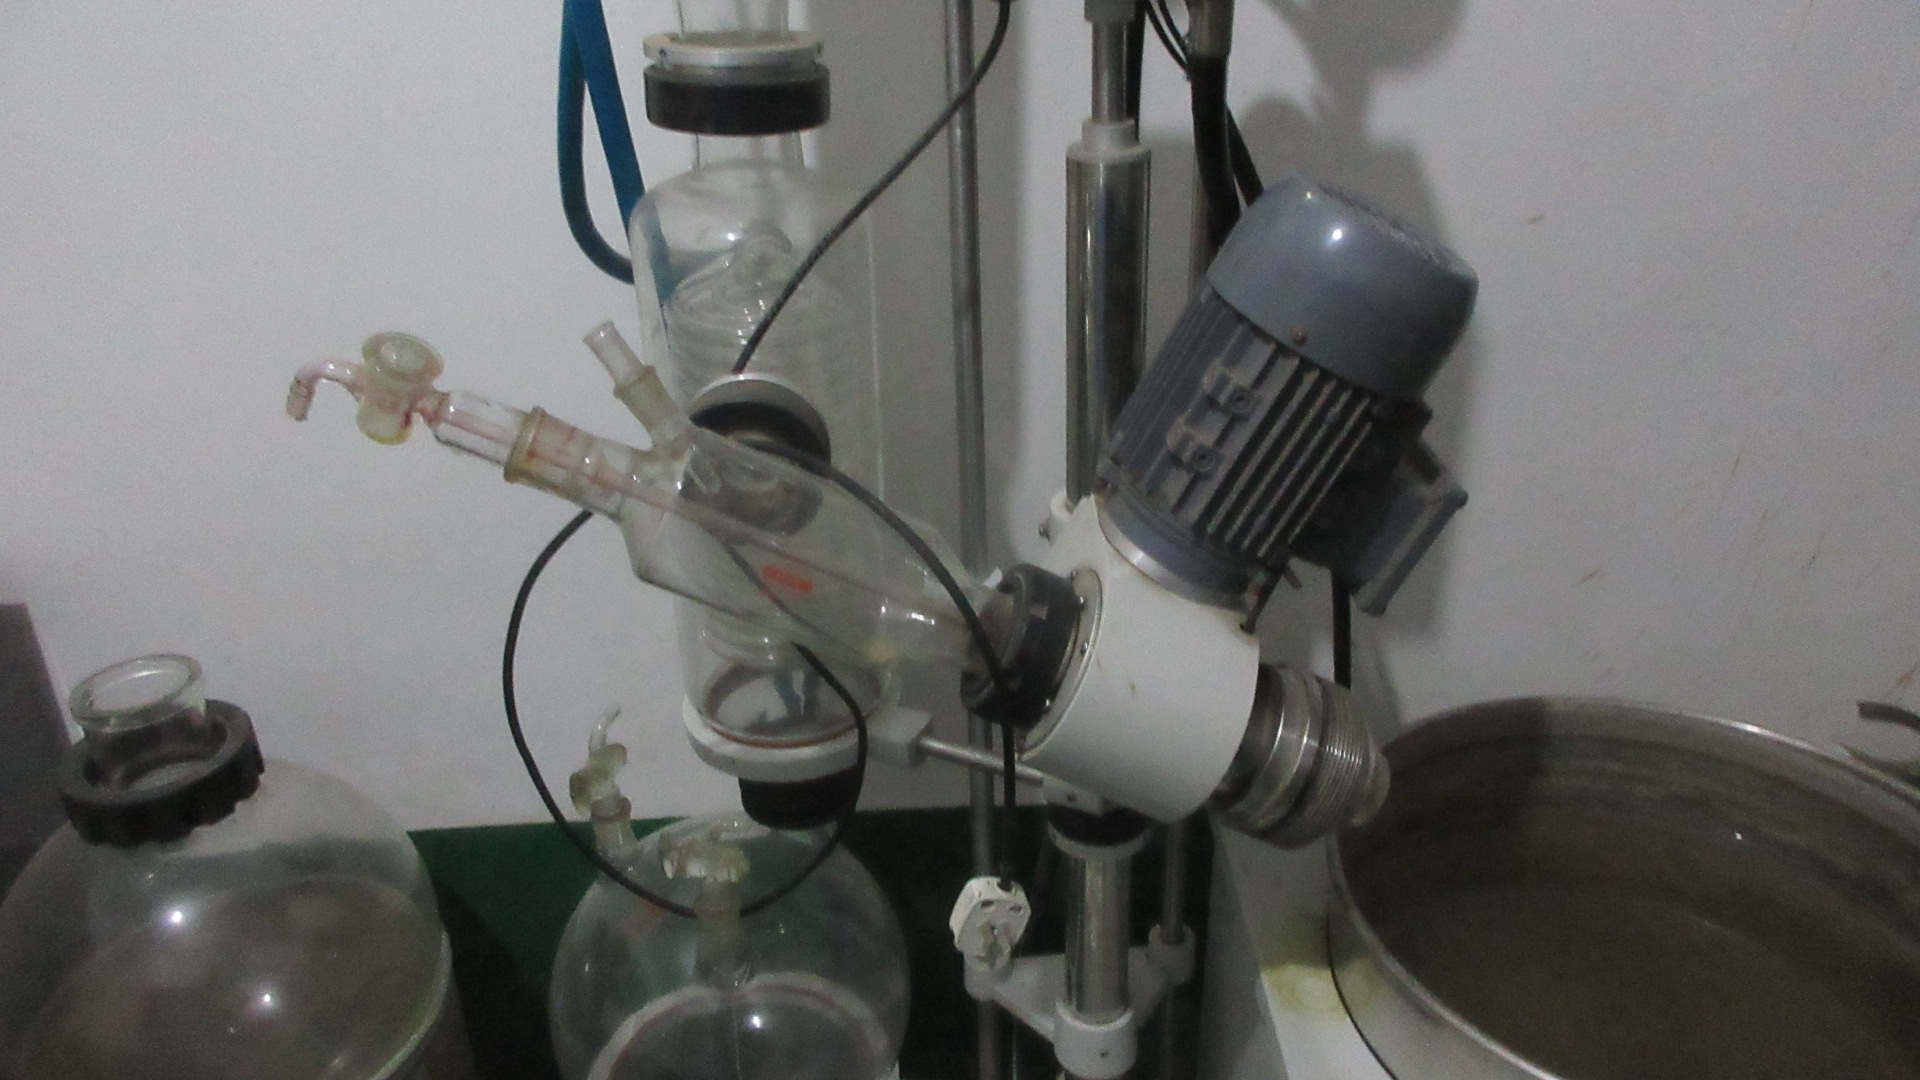
Pilot laboratory distillations
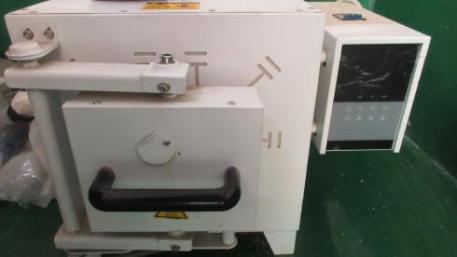
High-temp total ash determination
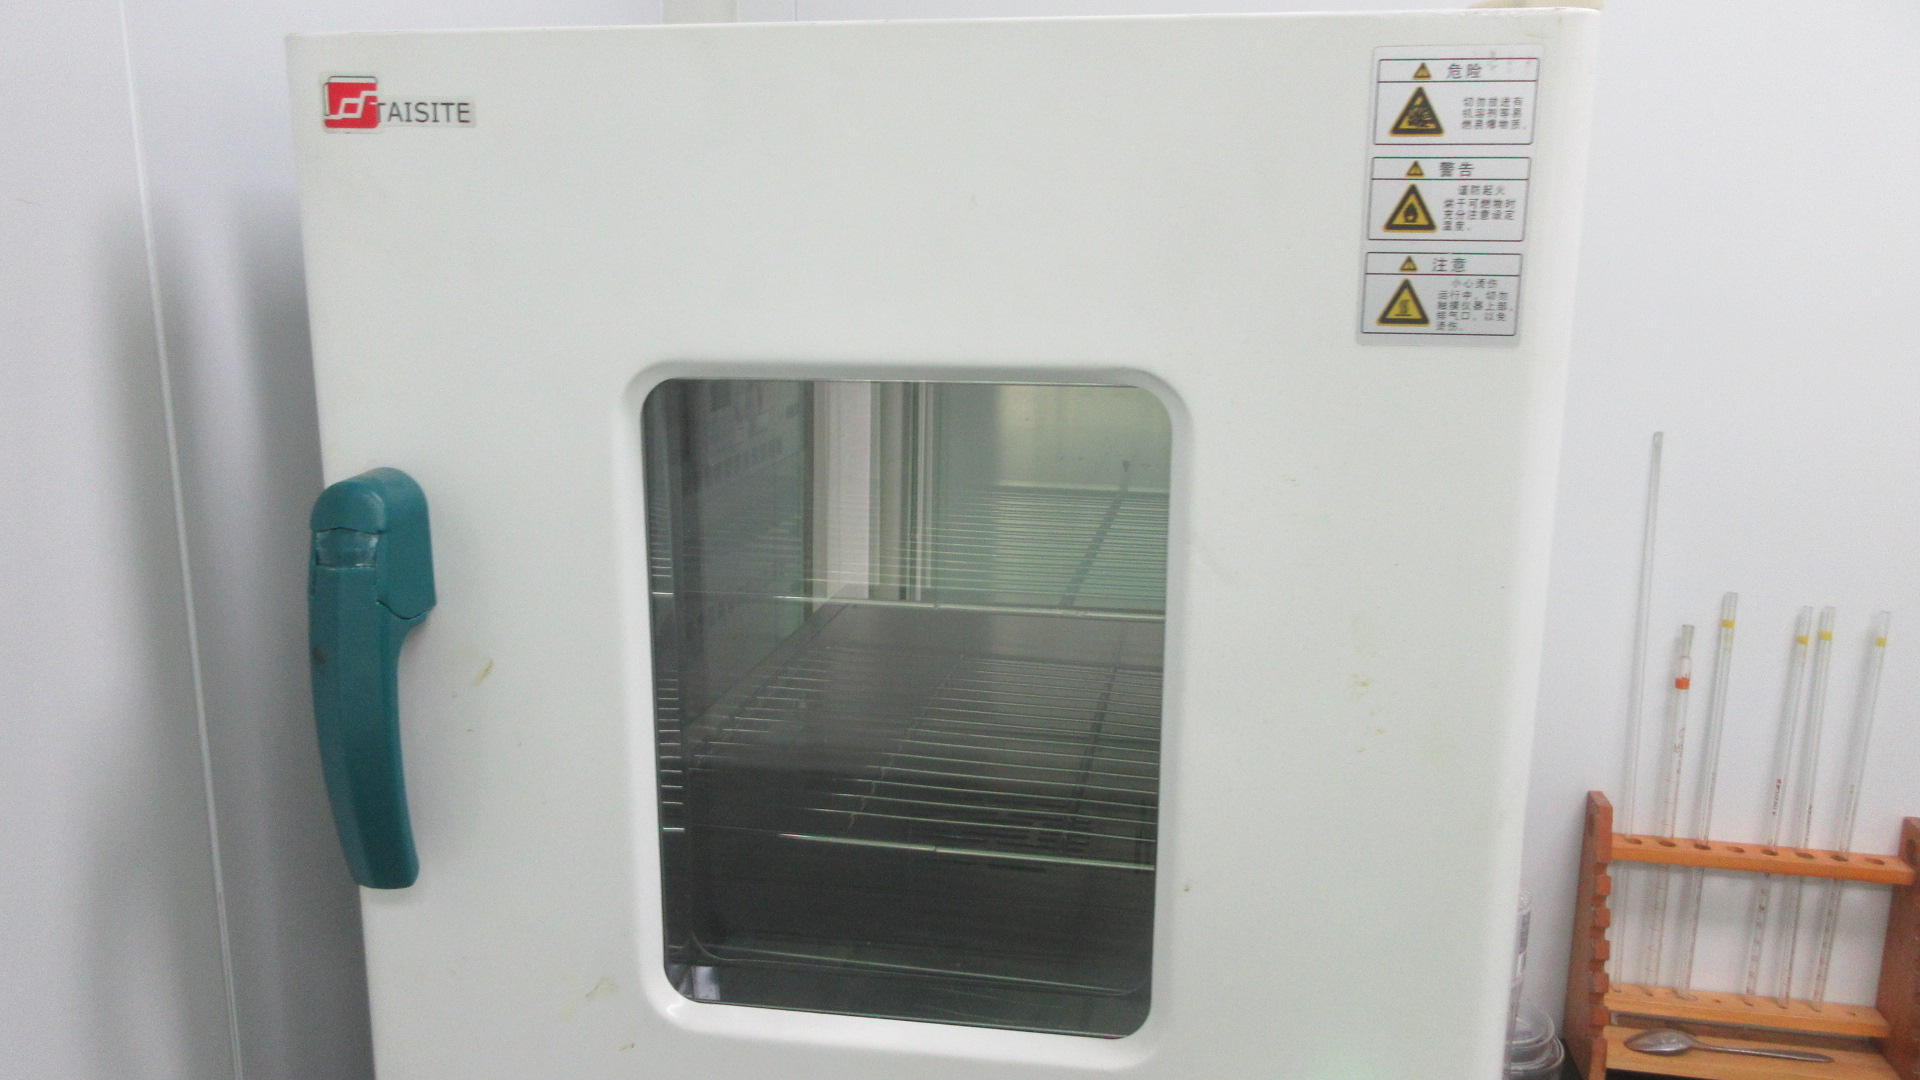
Forced convection drying cabinet
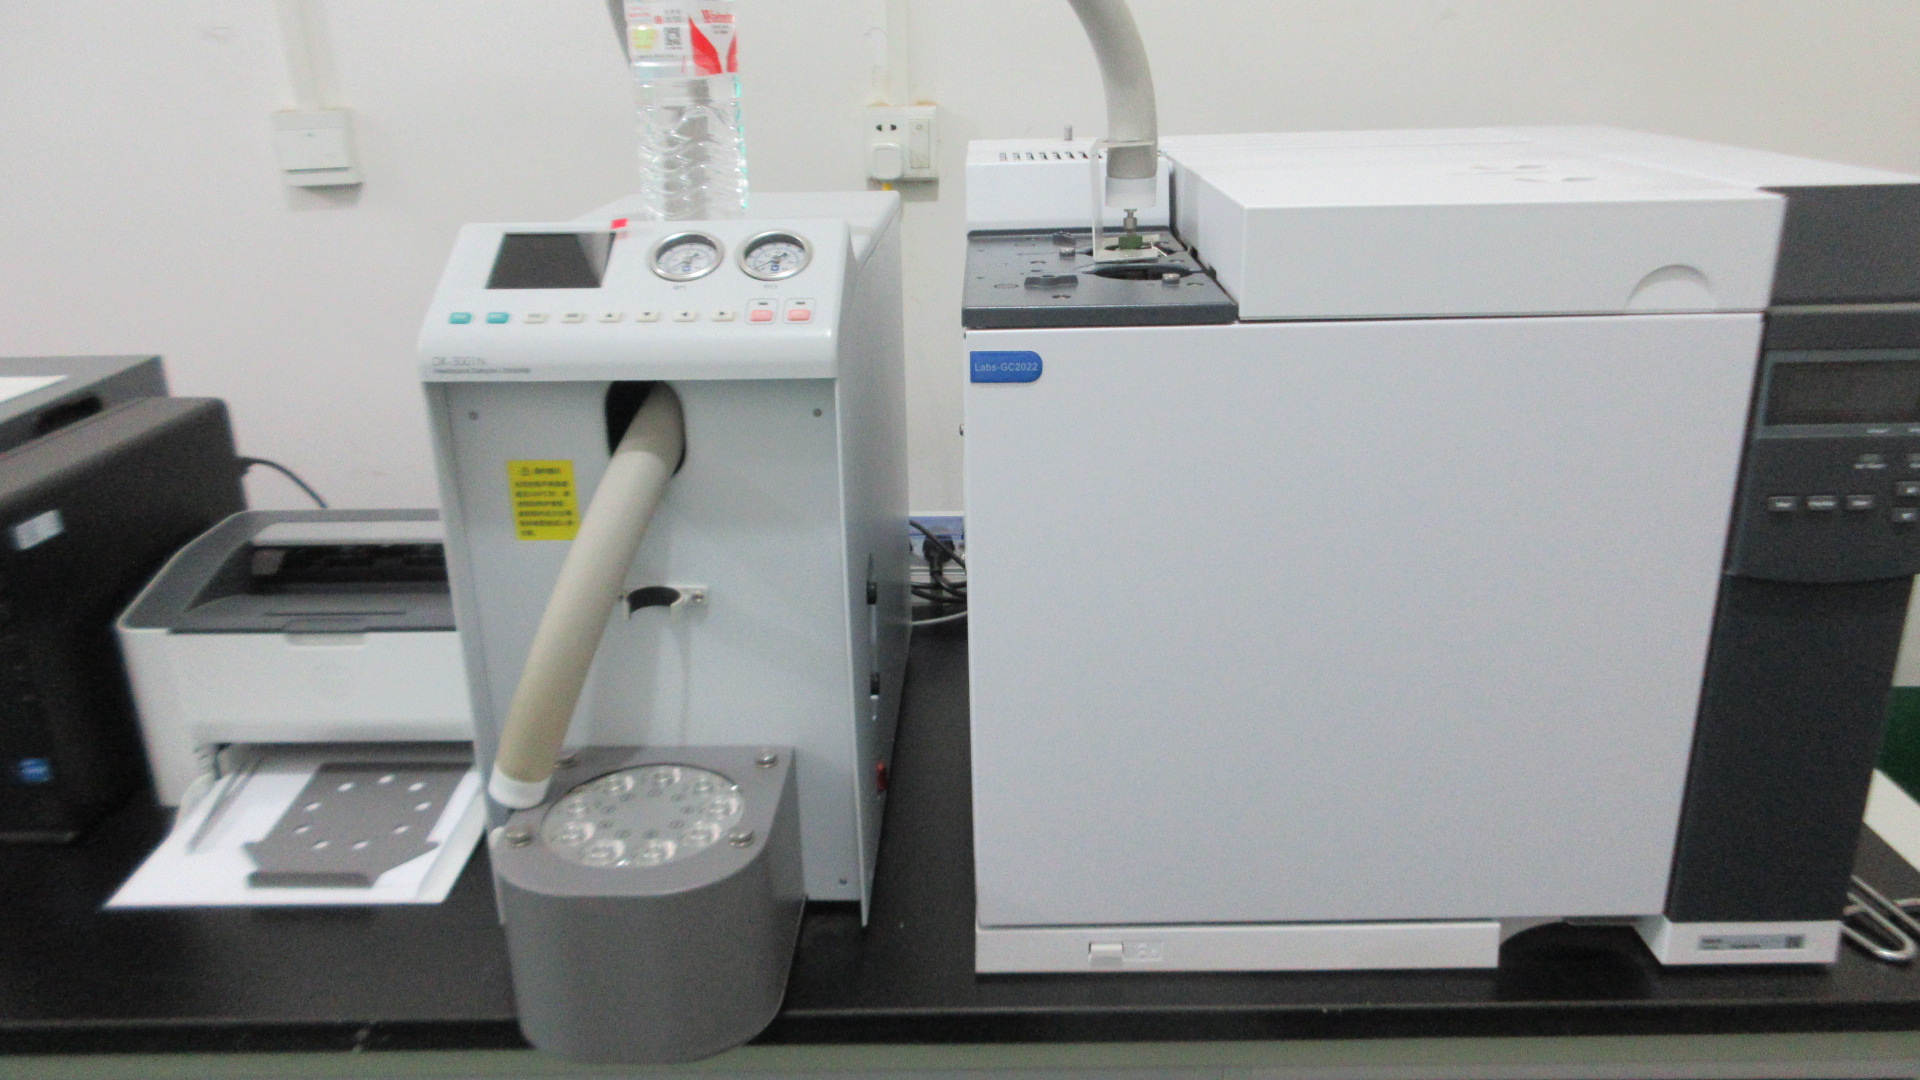
Residual solvent detection
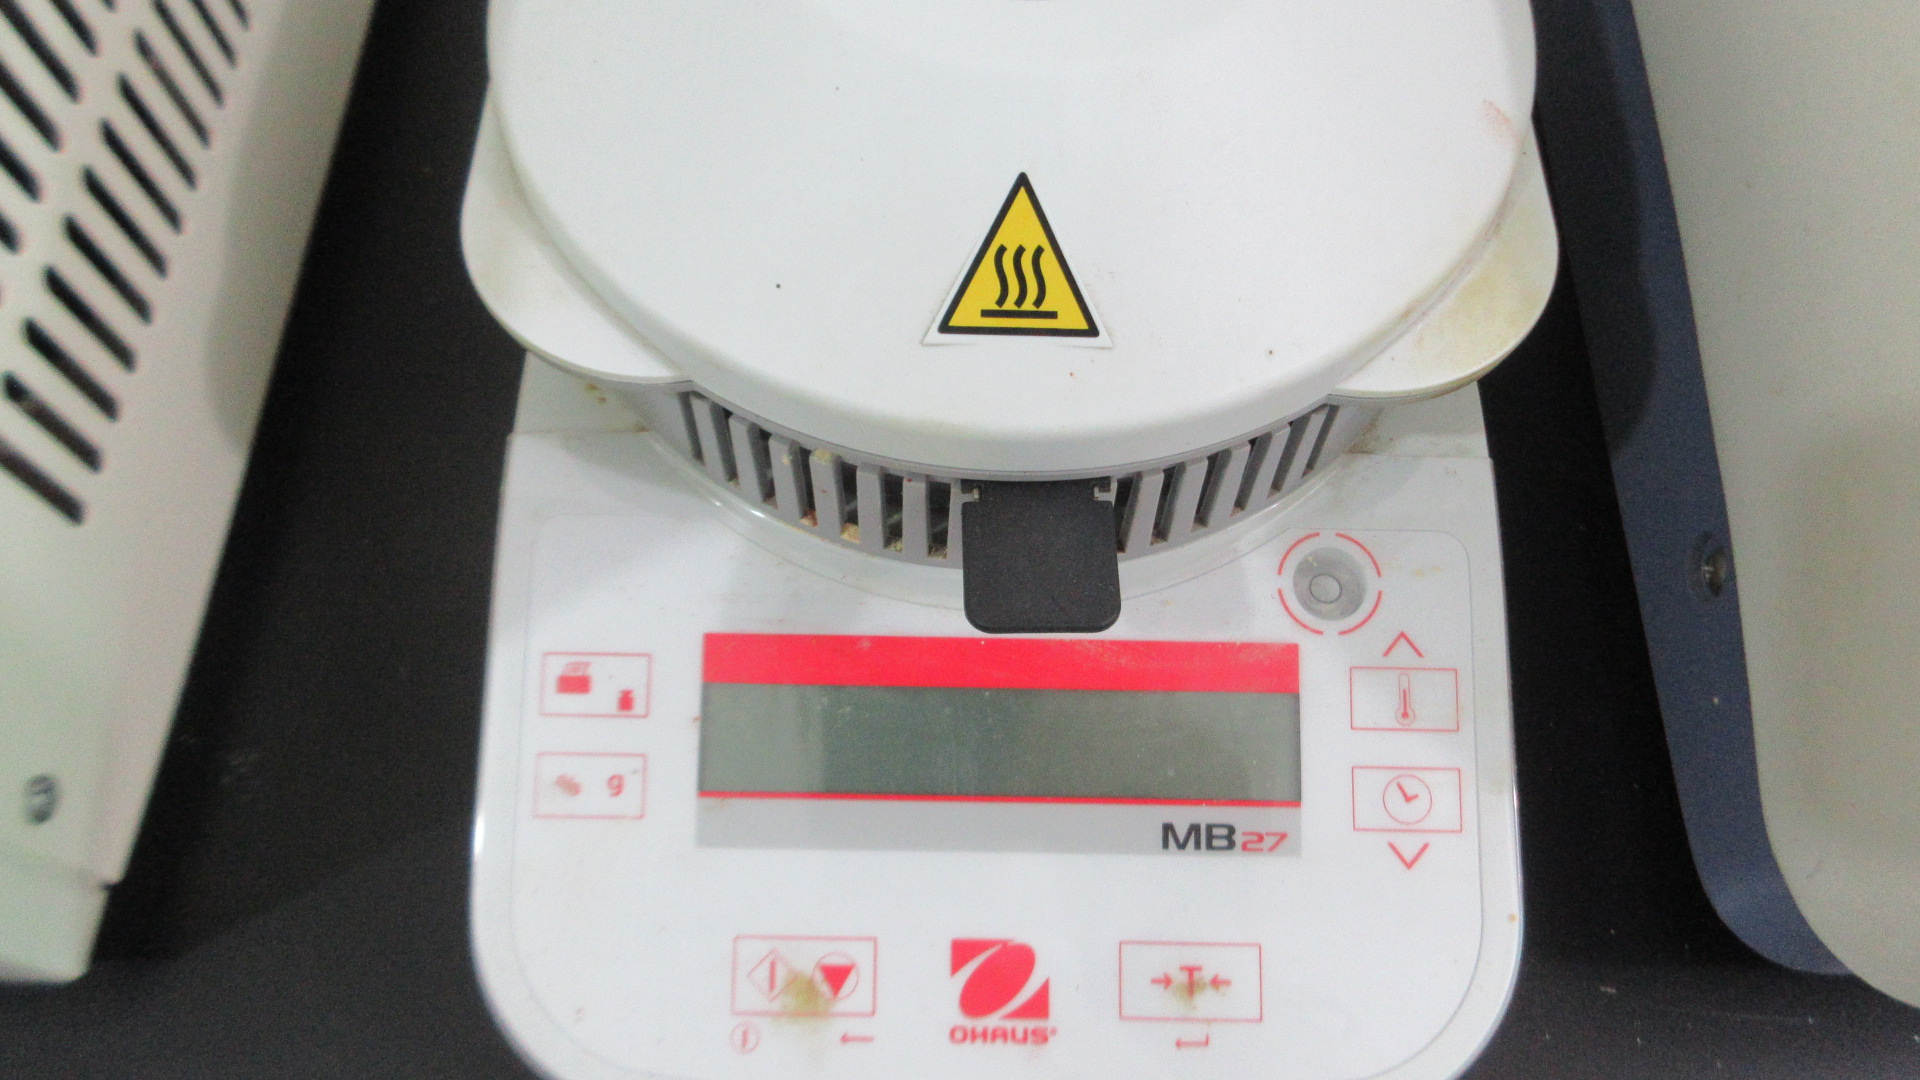
Halogen rapid moisture analysis
Our specialized laboratory team customizes particle sizing, active assays, natural coloring stability, and zero-calorie sweetness profiles for leading brands.
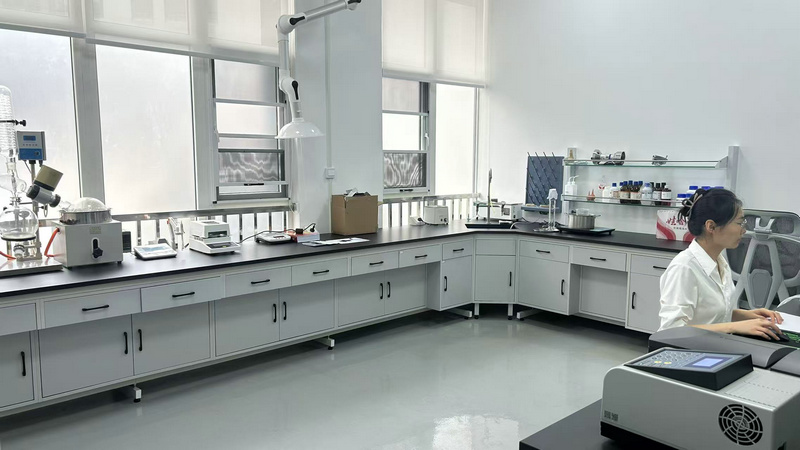
Formula development bench
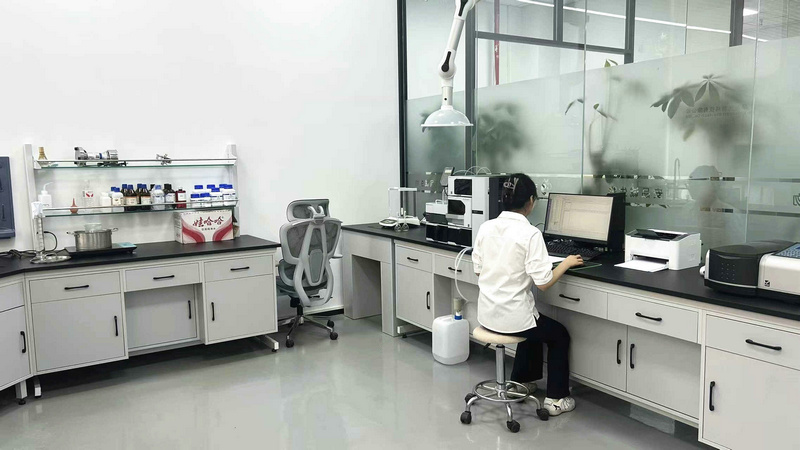
Solubility and stability trials
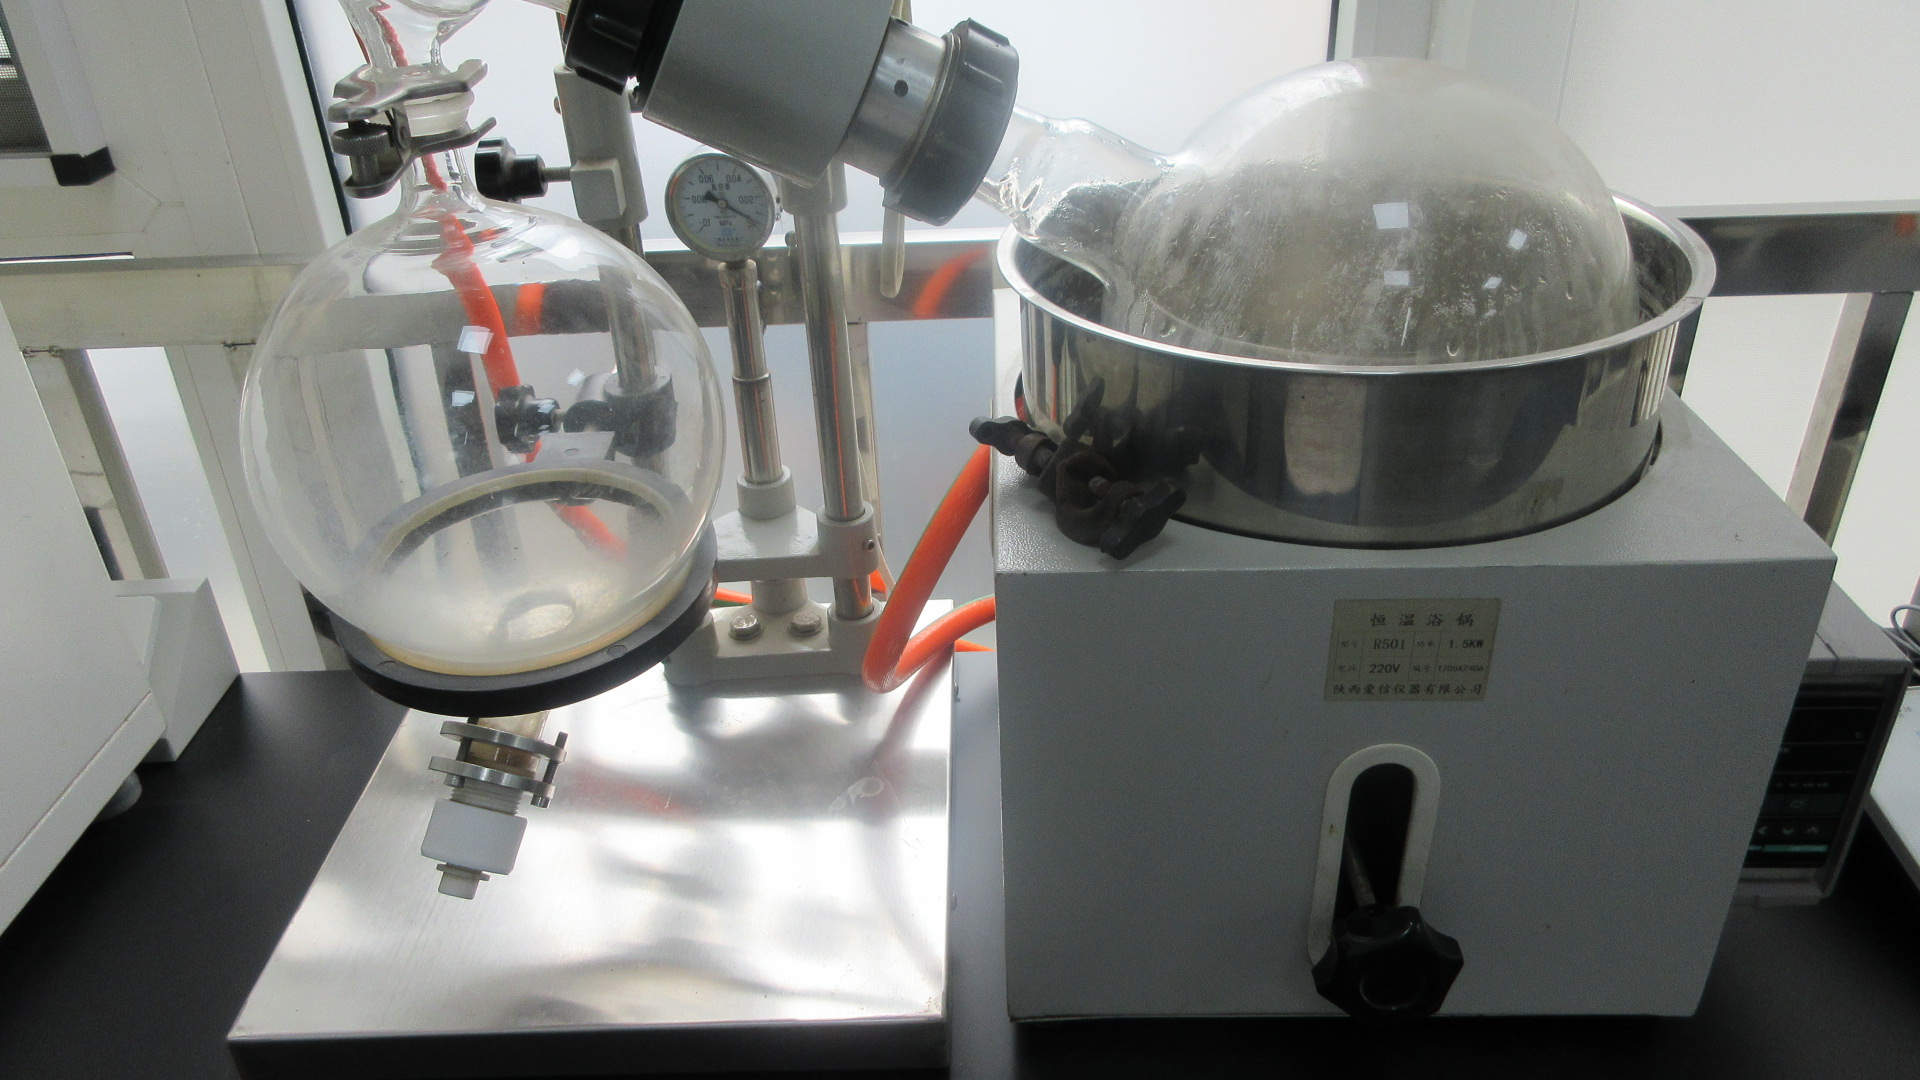
Small-batch process refinement
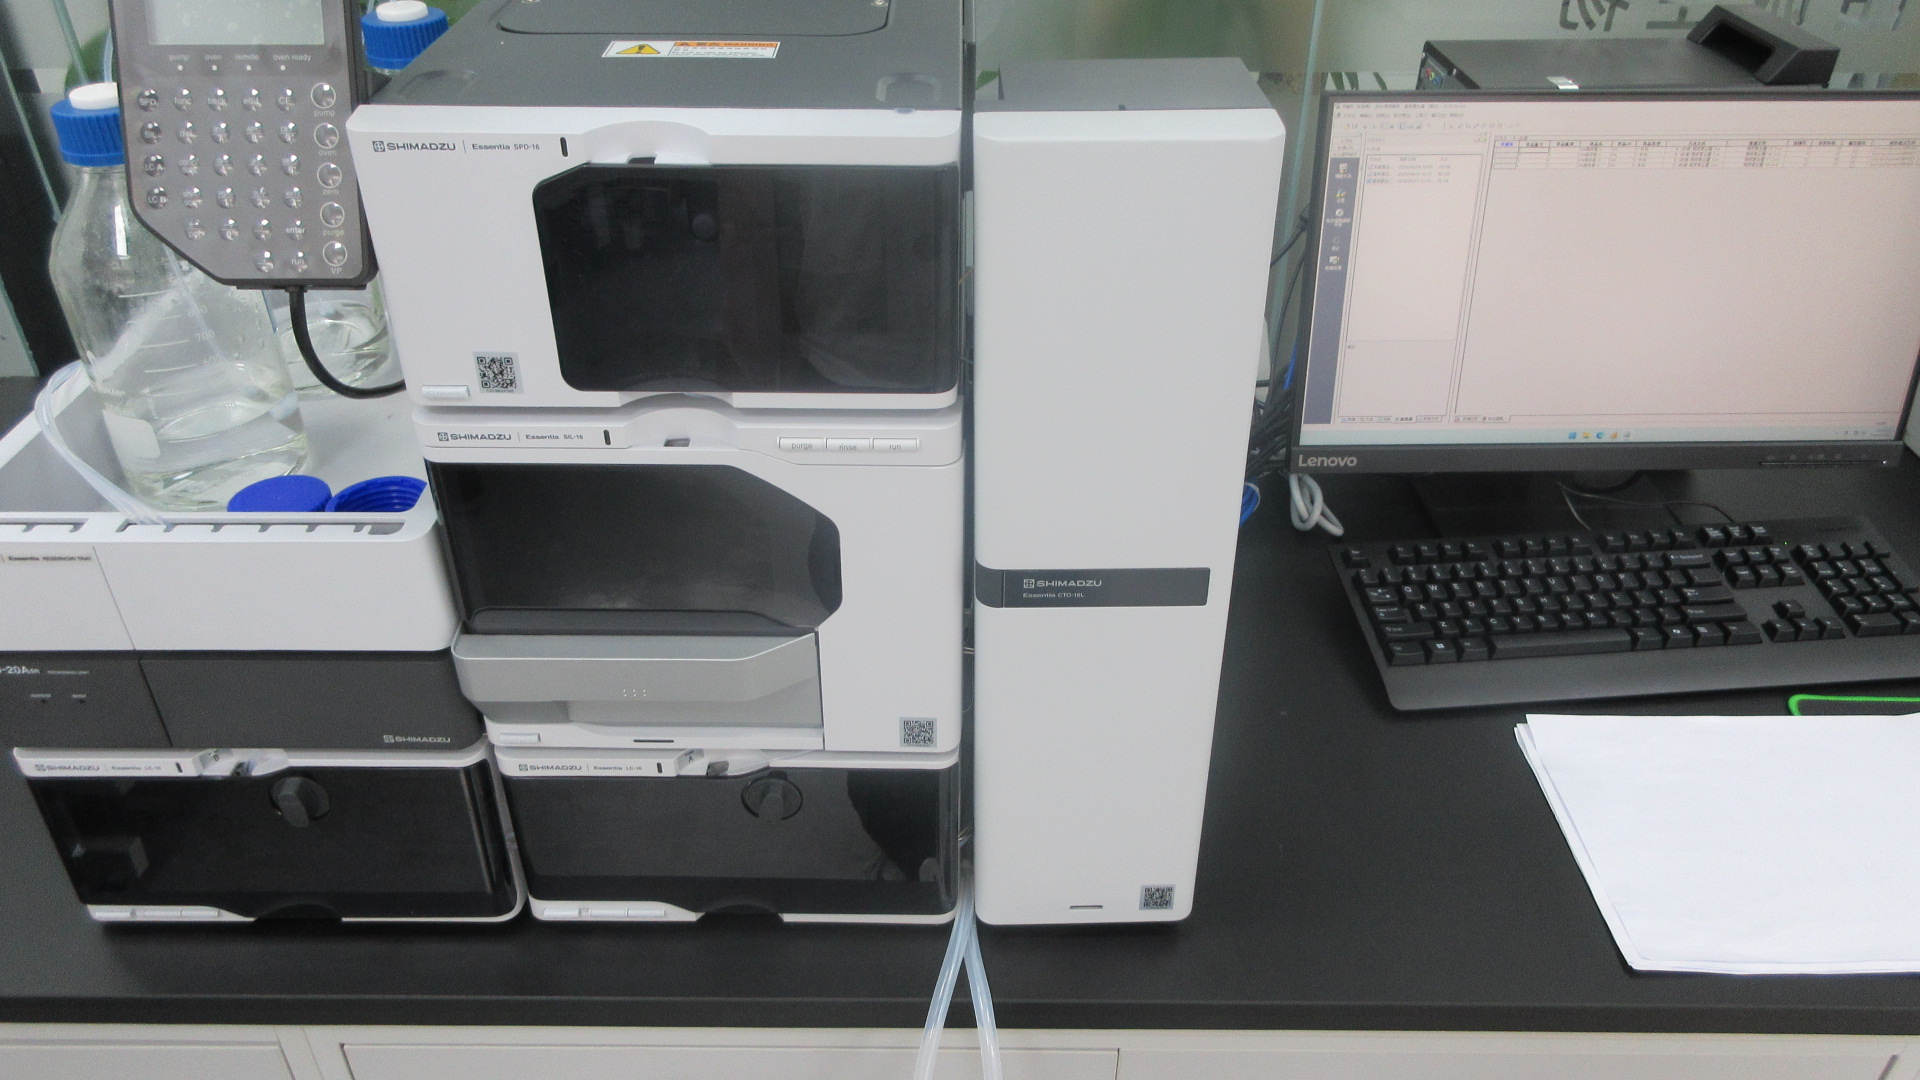
Marker identification & validation
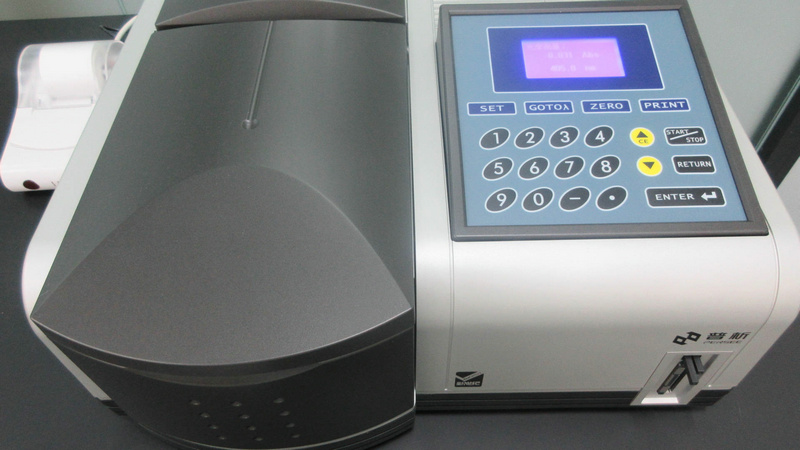
Colorimetric assay testing
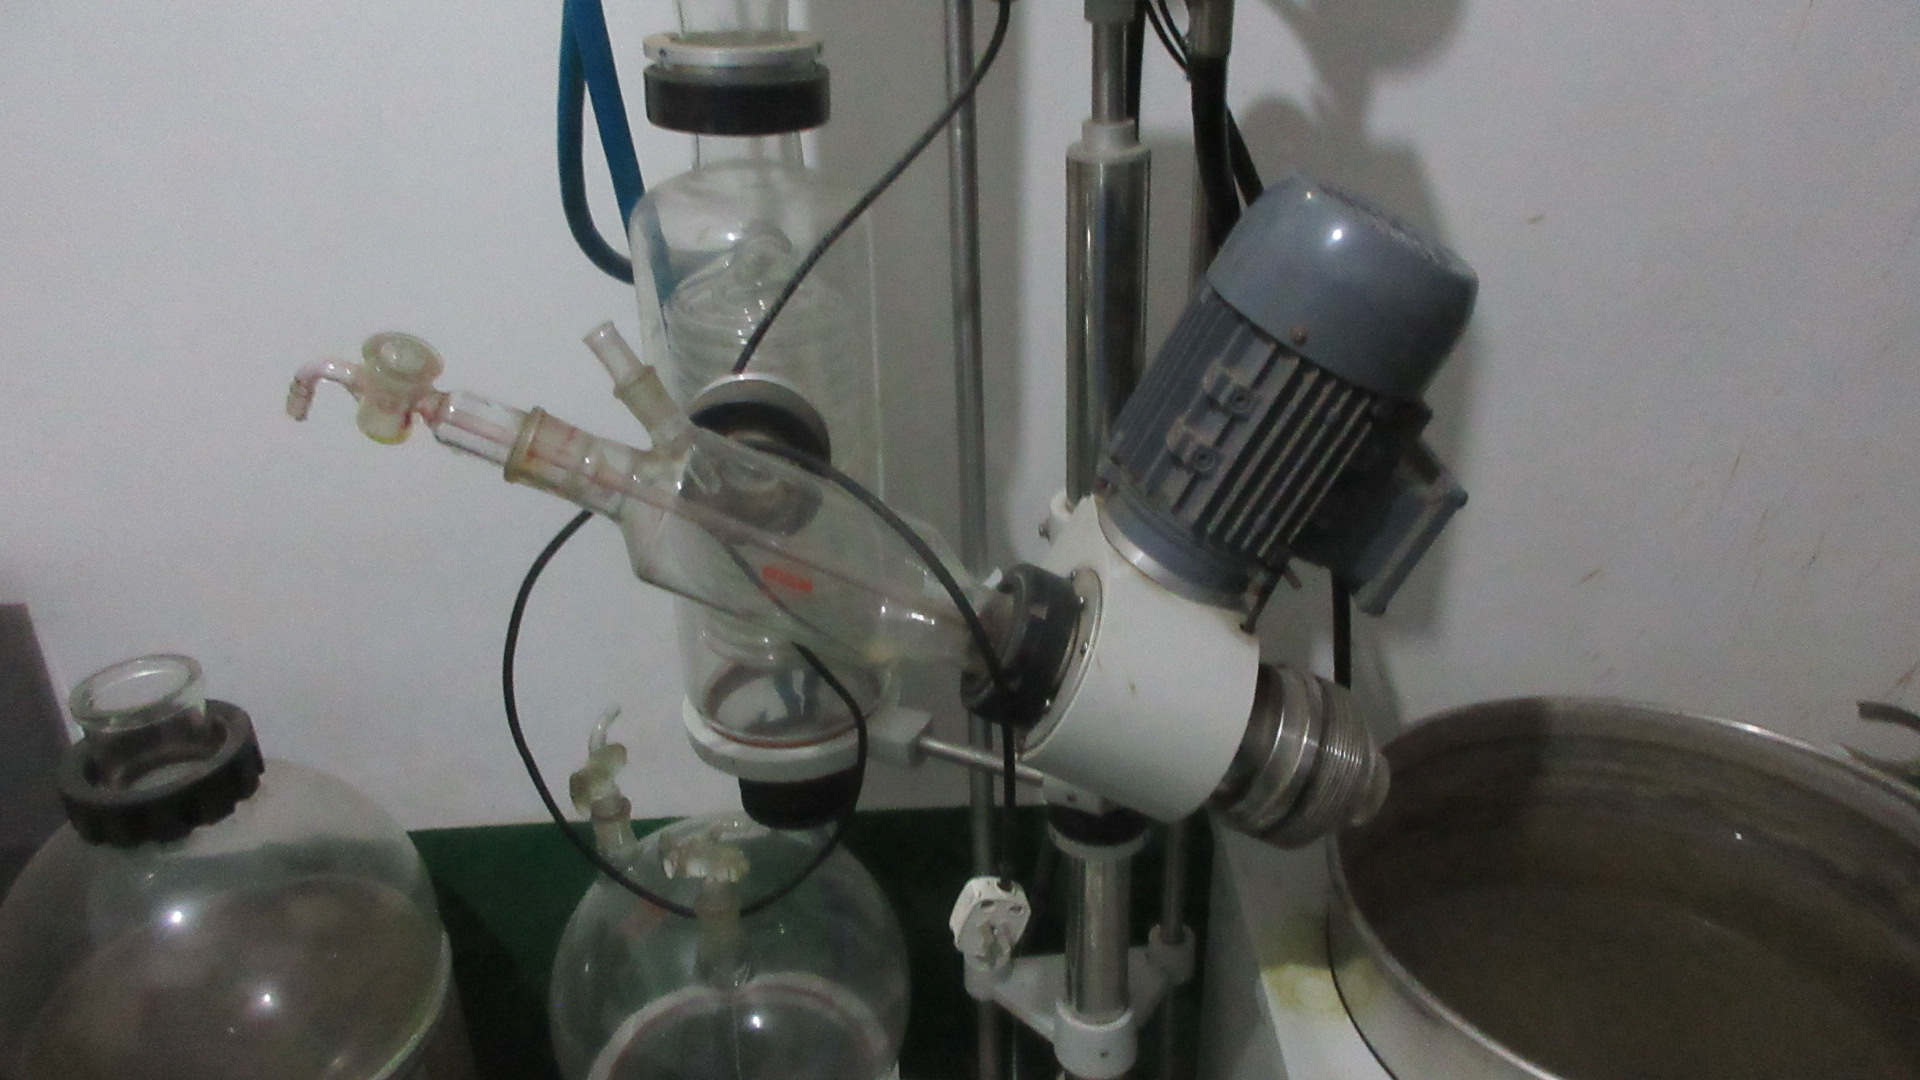
Thermal stability evaluation
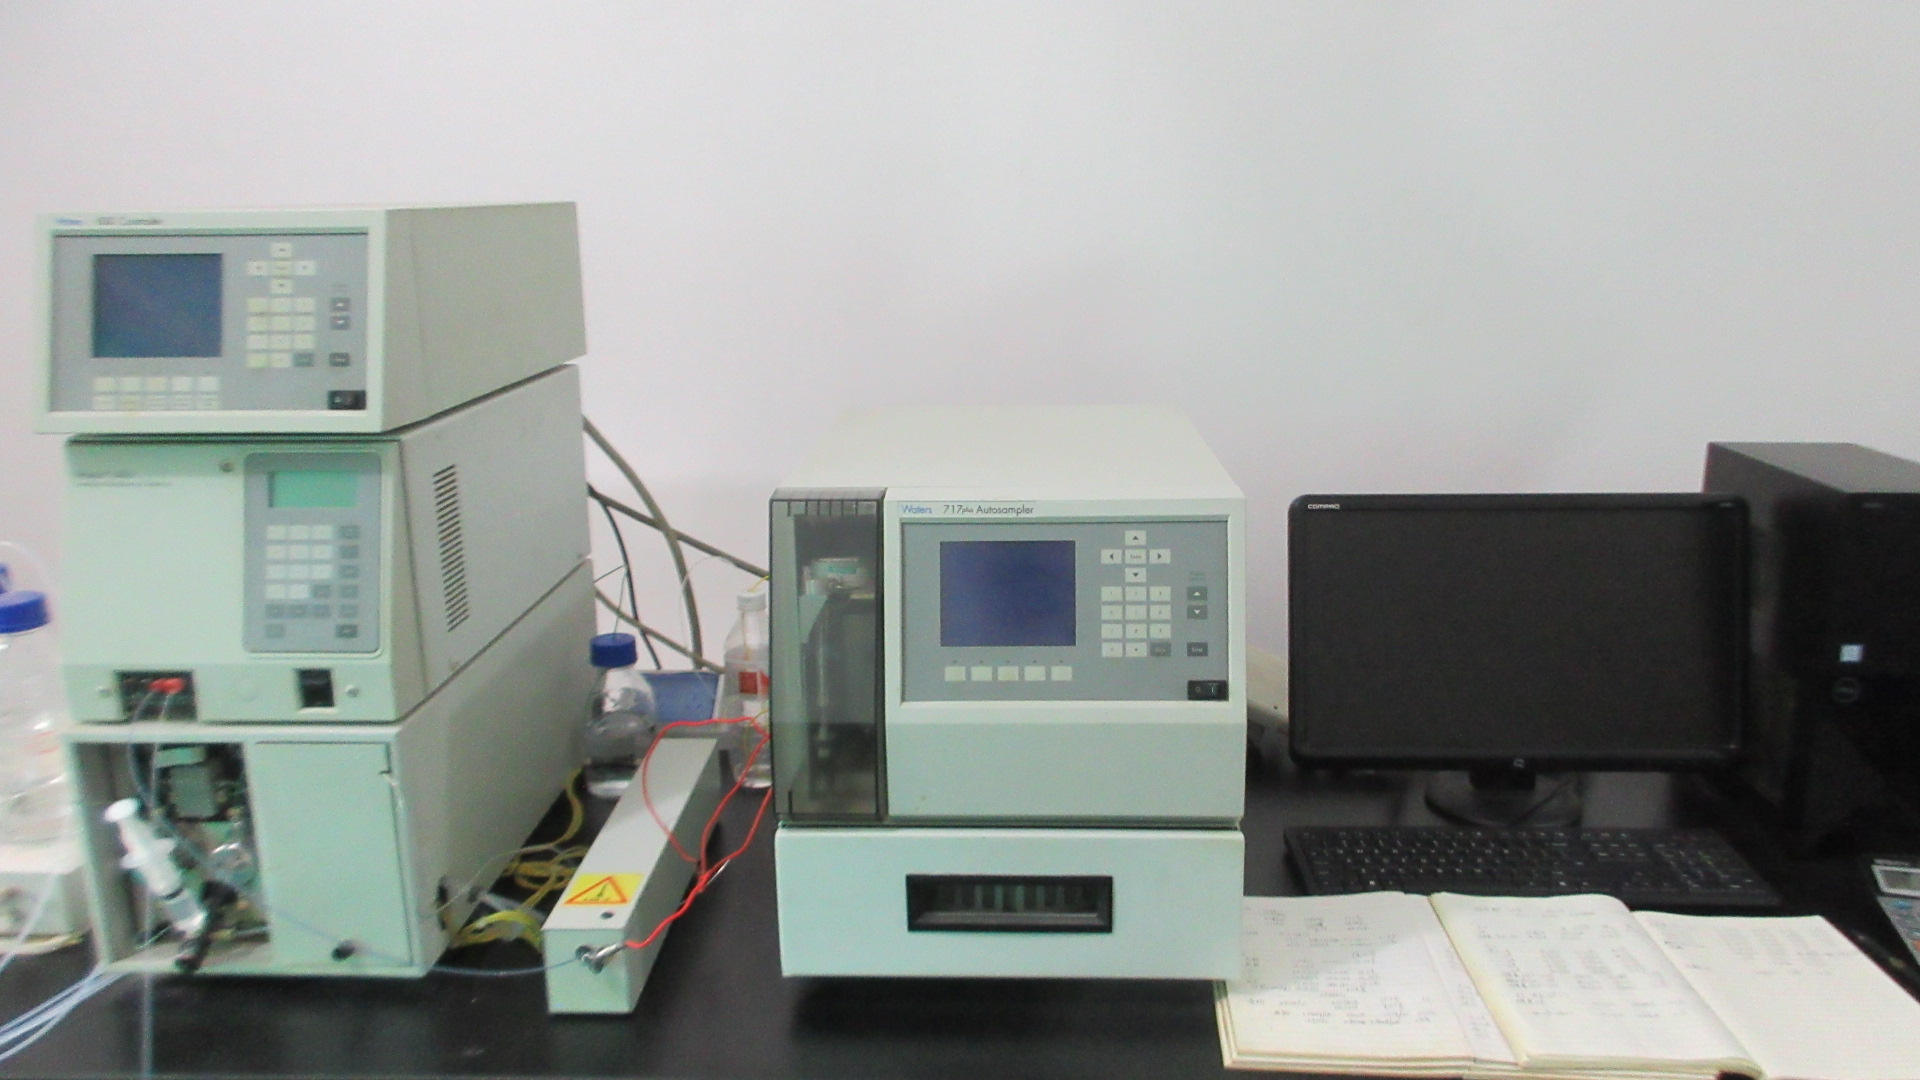
Quantitative purity verification
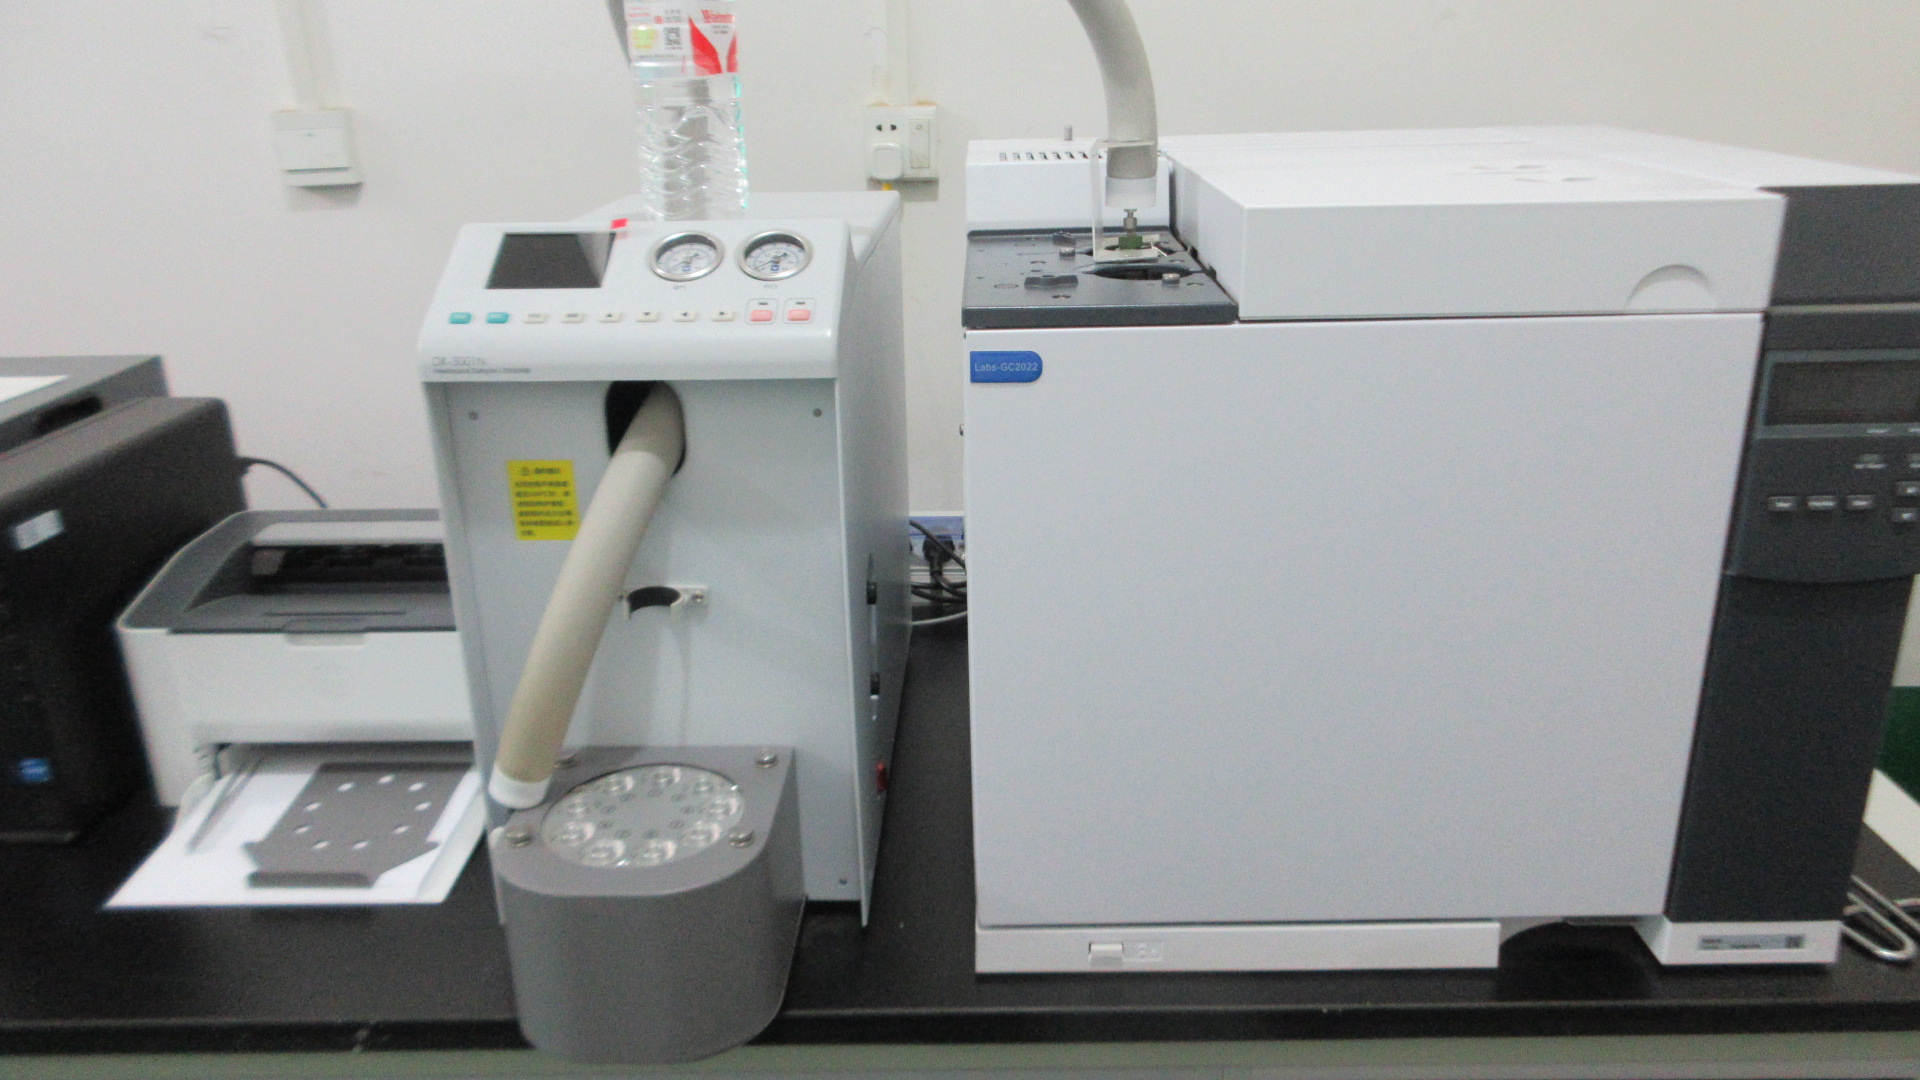
Precision residual solvent assays