
Scientific Botanical Processing Built on Traceability and Global Regulatory Alignment
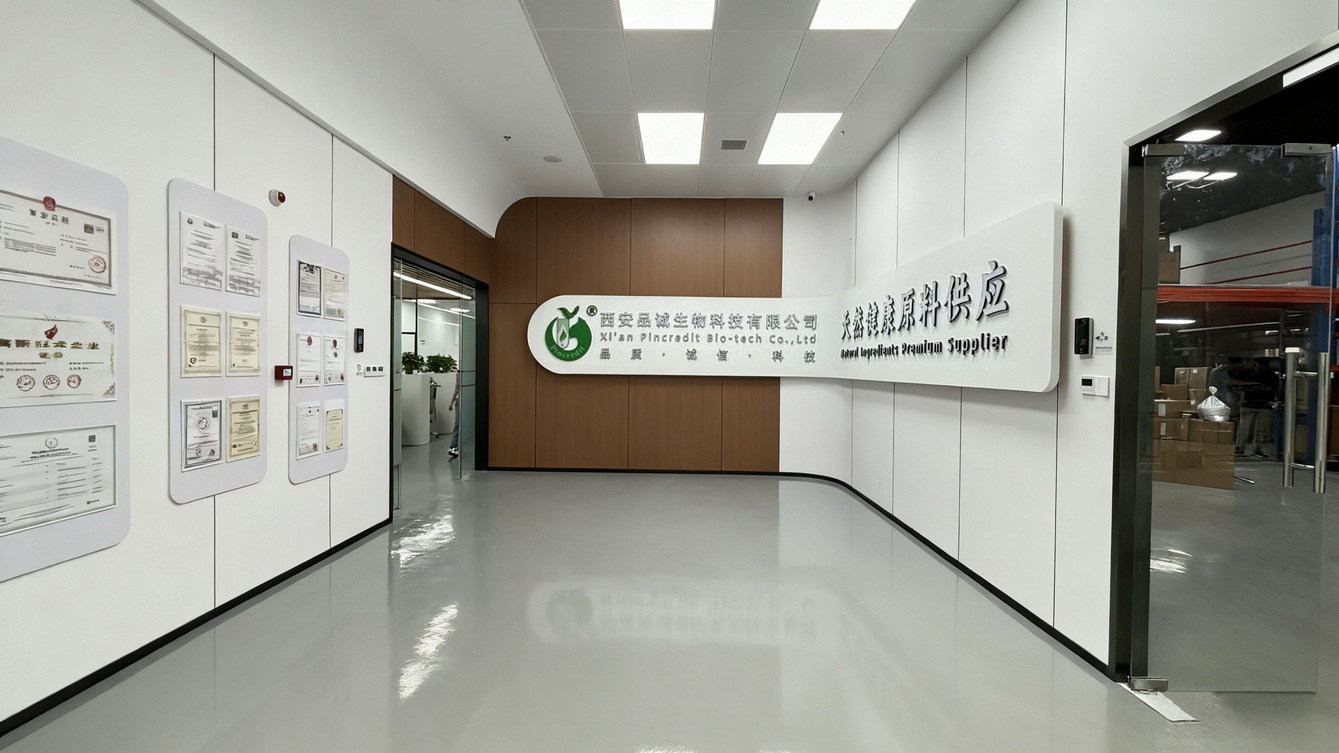
Xi'an Vexli Bio-Tech Co., Ltd. is based in Xi'an, Shaanxi Province, China's core botanical science and herbal cultivation hub. With over 12 years of specialized export experience, we operate modern plant extraction, purification, vacuum concentration, and aseptic spray drying workshops along with independent quality verification laboratories.
We serve pharmaceutical research partners, functional food formulators, beverage innovators, and premium cosmetic brand owners across more than 30 nations. Our integrated supply chain merges origin-direct wildcrafted and GAP-compliant raw materials with precision analytical validation, ensuring batch-to-batch consistency from pilot development to multi-ton container shipments.
Audited Supplier Benchmark
Assessed by SGS & International Trade RecordsFull-Cycle Botanical Processing, Formulating & Delivery
Engineered to streamline international procurement with certified ingredient integrity, technical documentation, and flexible batch configurations.
Tailored to precise customer requirements from initial formula conception through pilot test batches to private retail packaging.
- Sample-based replication and customized assay targets
- Particle sizing adjustment from 80 mesh up to 450 mesh
- Full private label packaging: pouches, sachets, tubs, drums
Internal laboratory managed by 7 full-time analytical chemists, utilizing verified pharmacopeial and international standard methods.
- HPLC and UV assay confirmation for active compounds
- Gas chromatography (GC) residual solvent determination
- BS EN 15662 pesticide multi-residue & heavy metal monitoring
Comprehensive commercial export support with audited hazardous/non-hazardous transport safety documents.
- IATA DGR air cargo & IMDG maritime certification
- Flexible trade terms: FOB, CIF, CFR, FCA, EXW, and DDP
- Rapid dispatch through Shanghai, Ningbo, and Tianjin ports
Standardized Manufacturing, Advanced Machinery & Testing Apparatus
Explore our complete botanical workflow: from raw material harvesting, pressurized extraction, and column purification, to laboratory instrument release.
1. Raw Materials Inspection
Direct sourcing with origin verification, physical screening, moisture limits, and preliminary identity confirmation.
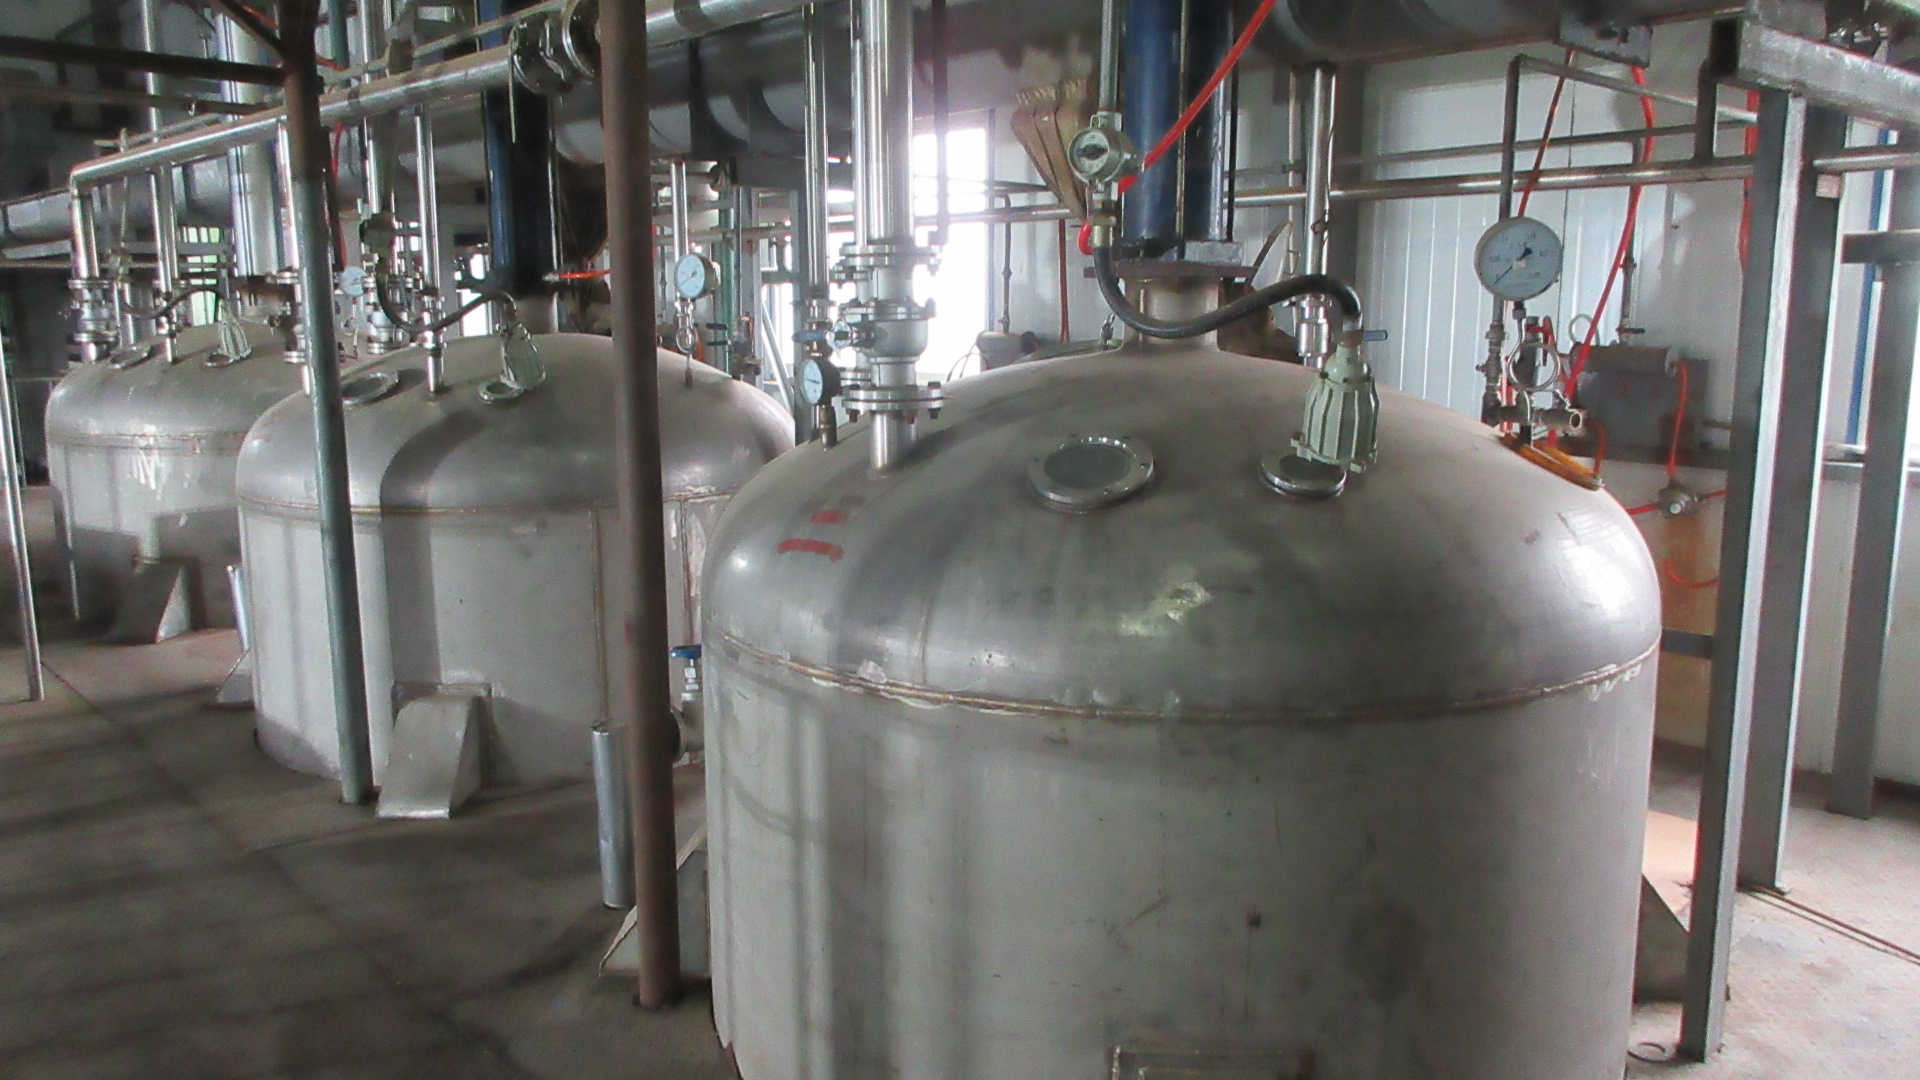
2. Solid-Liquid Extracting
Purified water or food-grade ethanol extraction with automated thermal control to preserve fragile botanical active fractions.
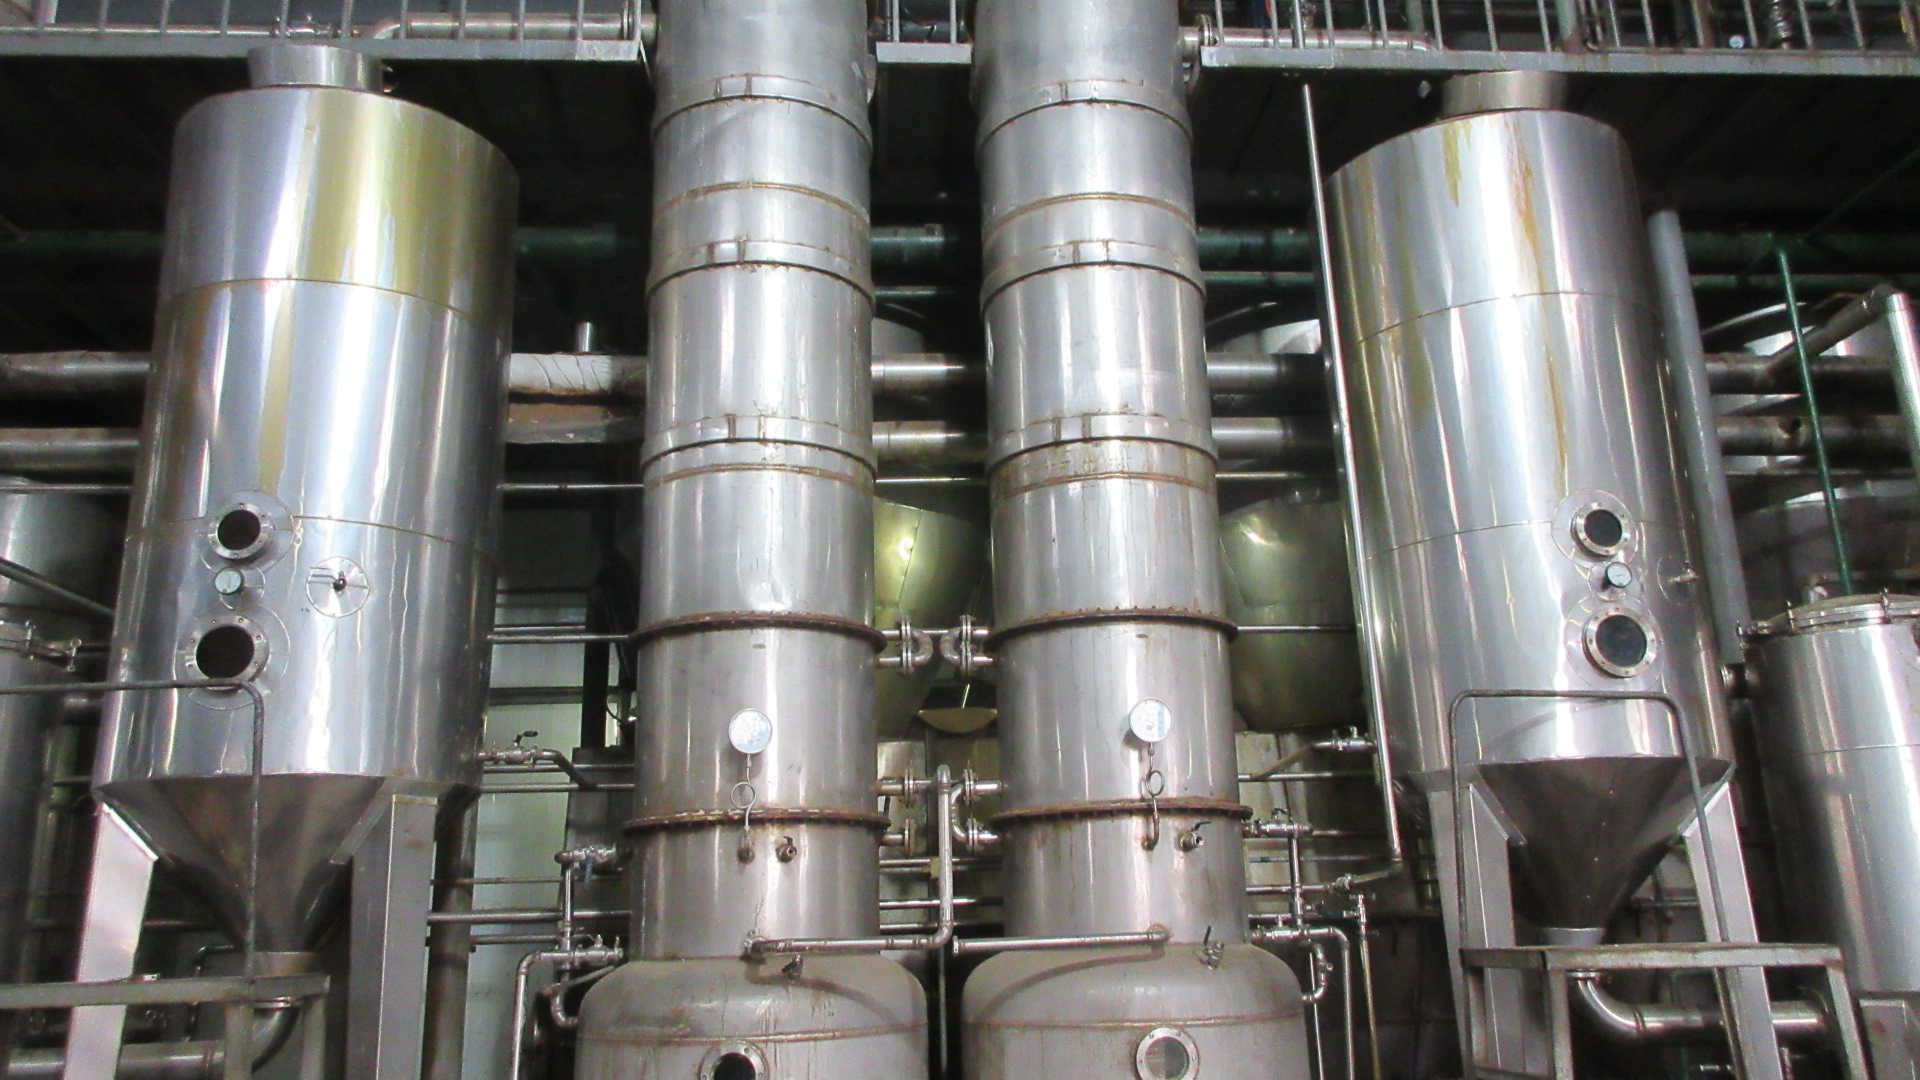
3. Vacuum Concentration
Continuous low-temperature vacuum evaporation concentrates active compounds while safeguarding thermolabile constituents.
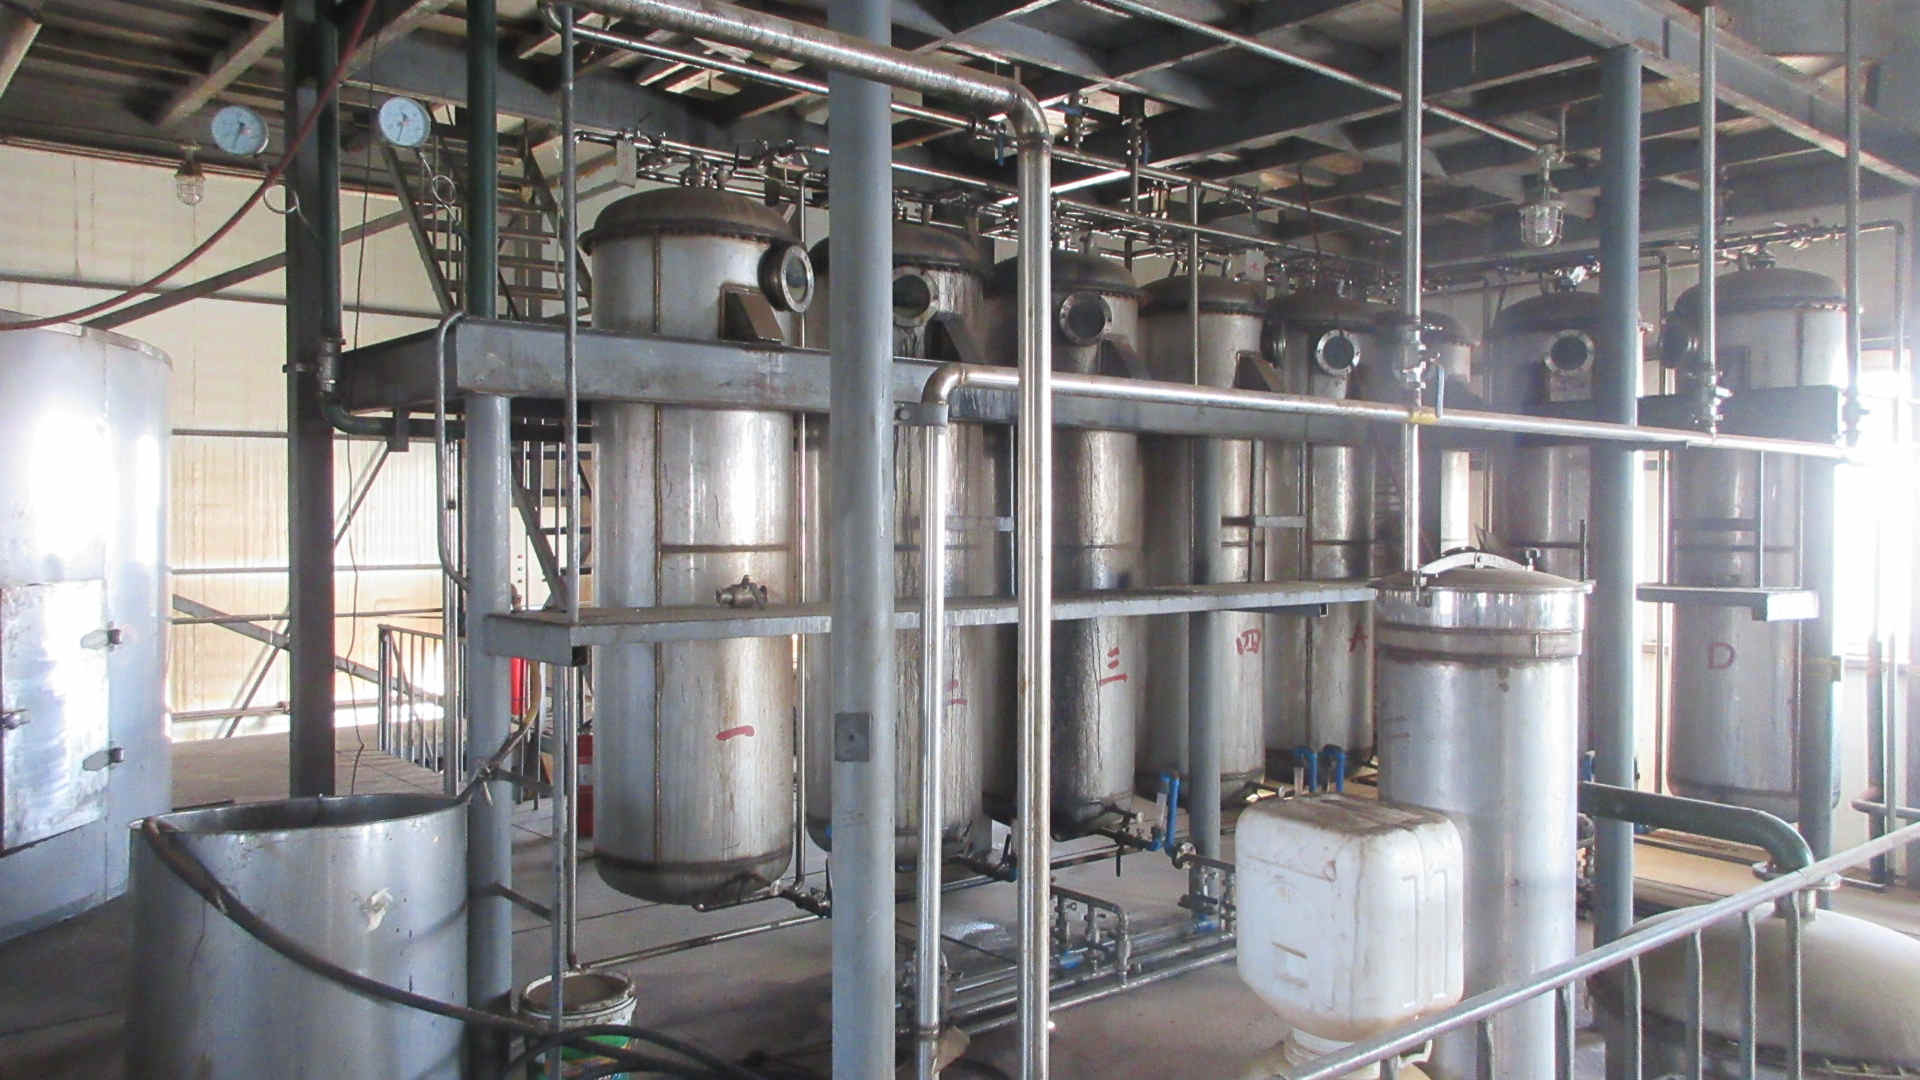
4. Column Purification
Macroporous adsorption resins and filtration systems isolate target molecules and eliminate inactive organic residues.
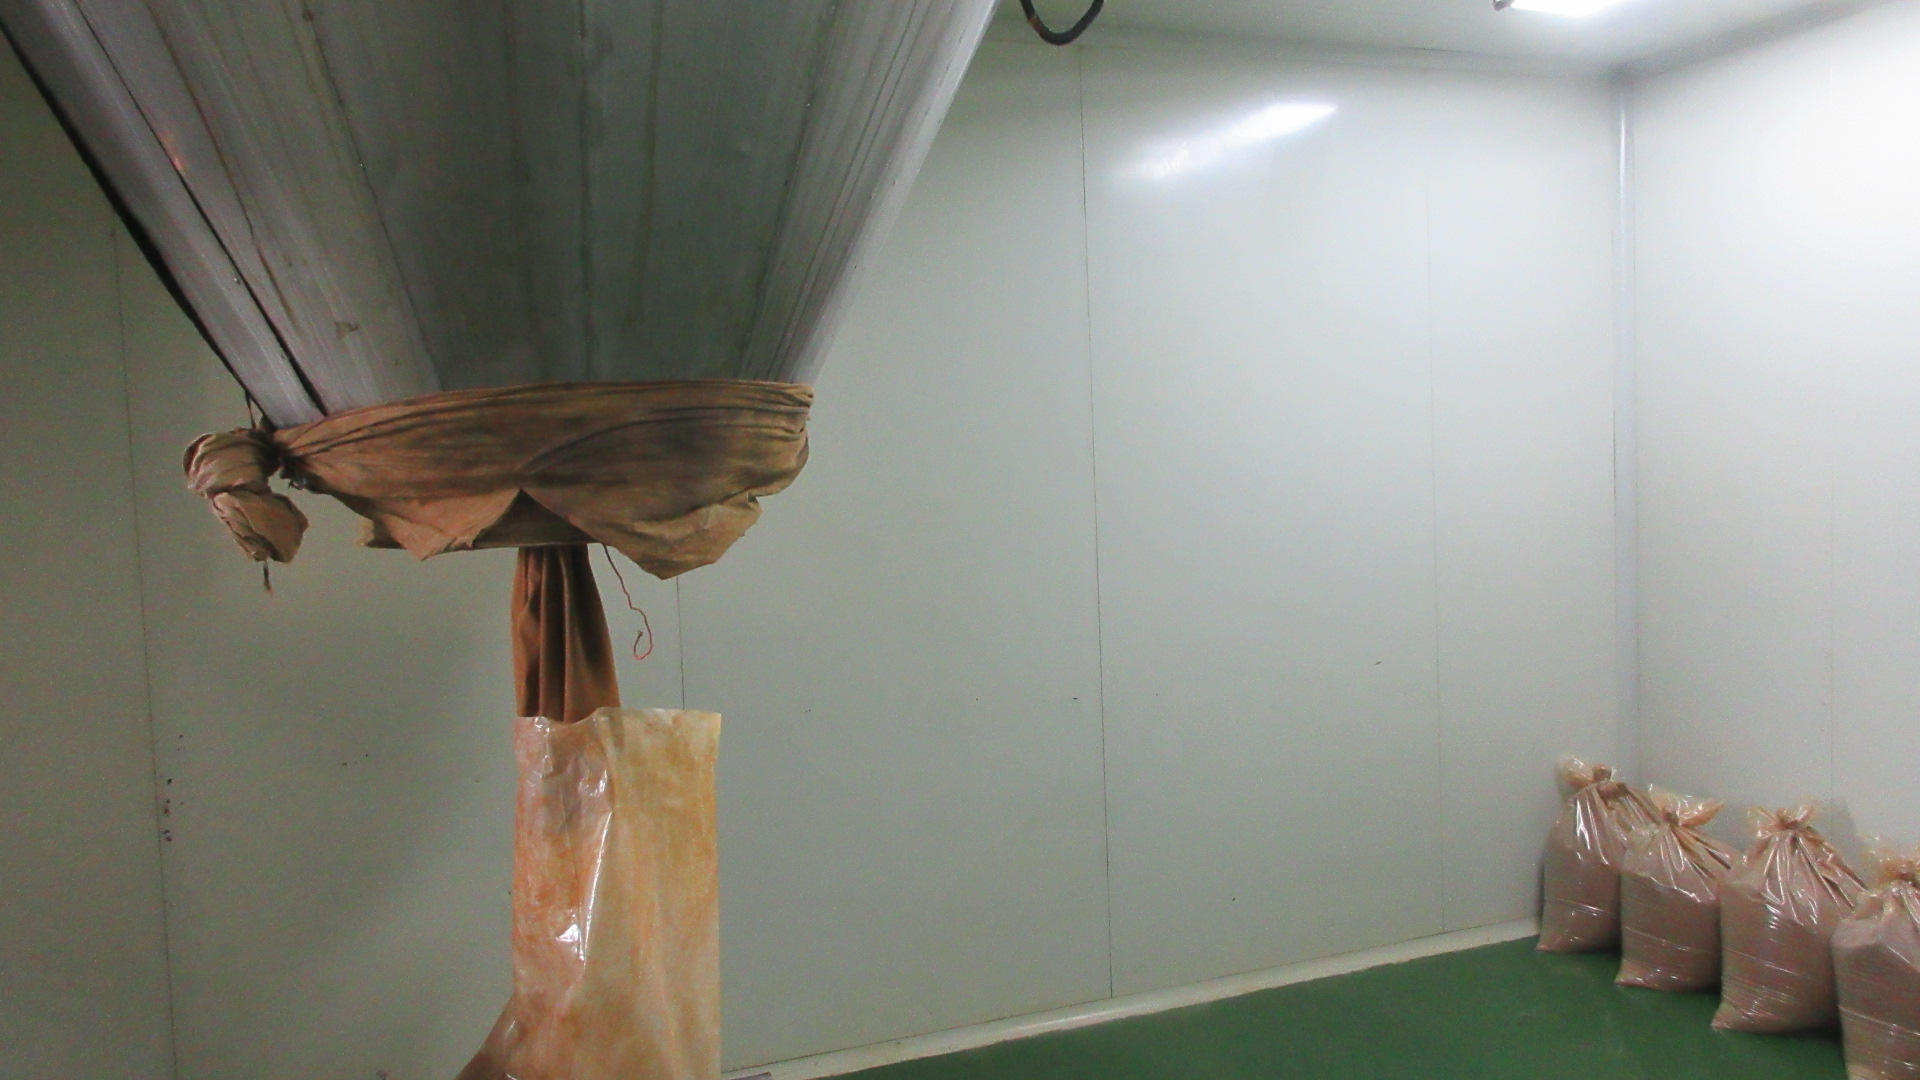
5. Spray & Vacuum Drying
Centrifugal atomization in filtered positive-pressure chambers yields instant-dissolve, free-flowing micro-powders.
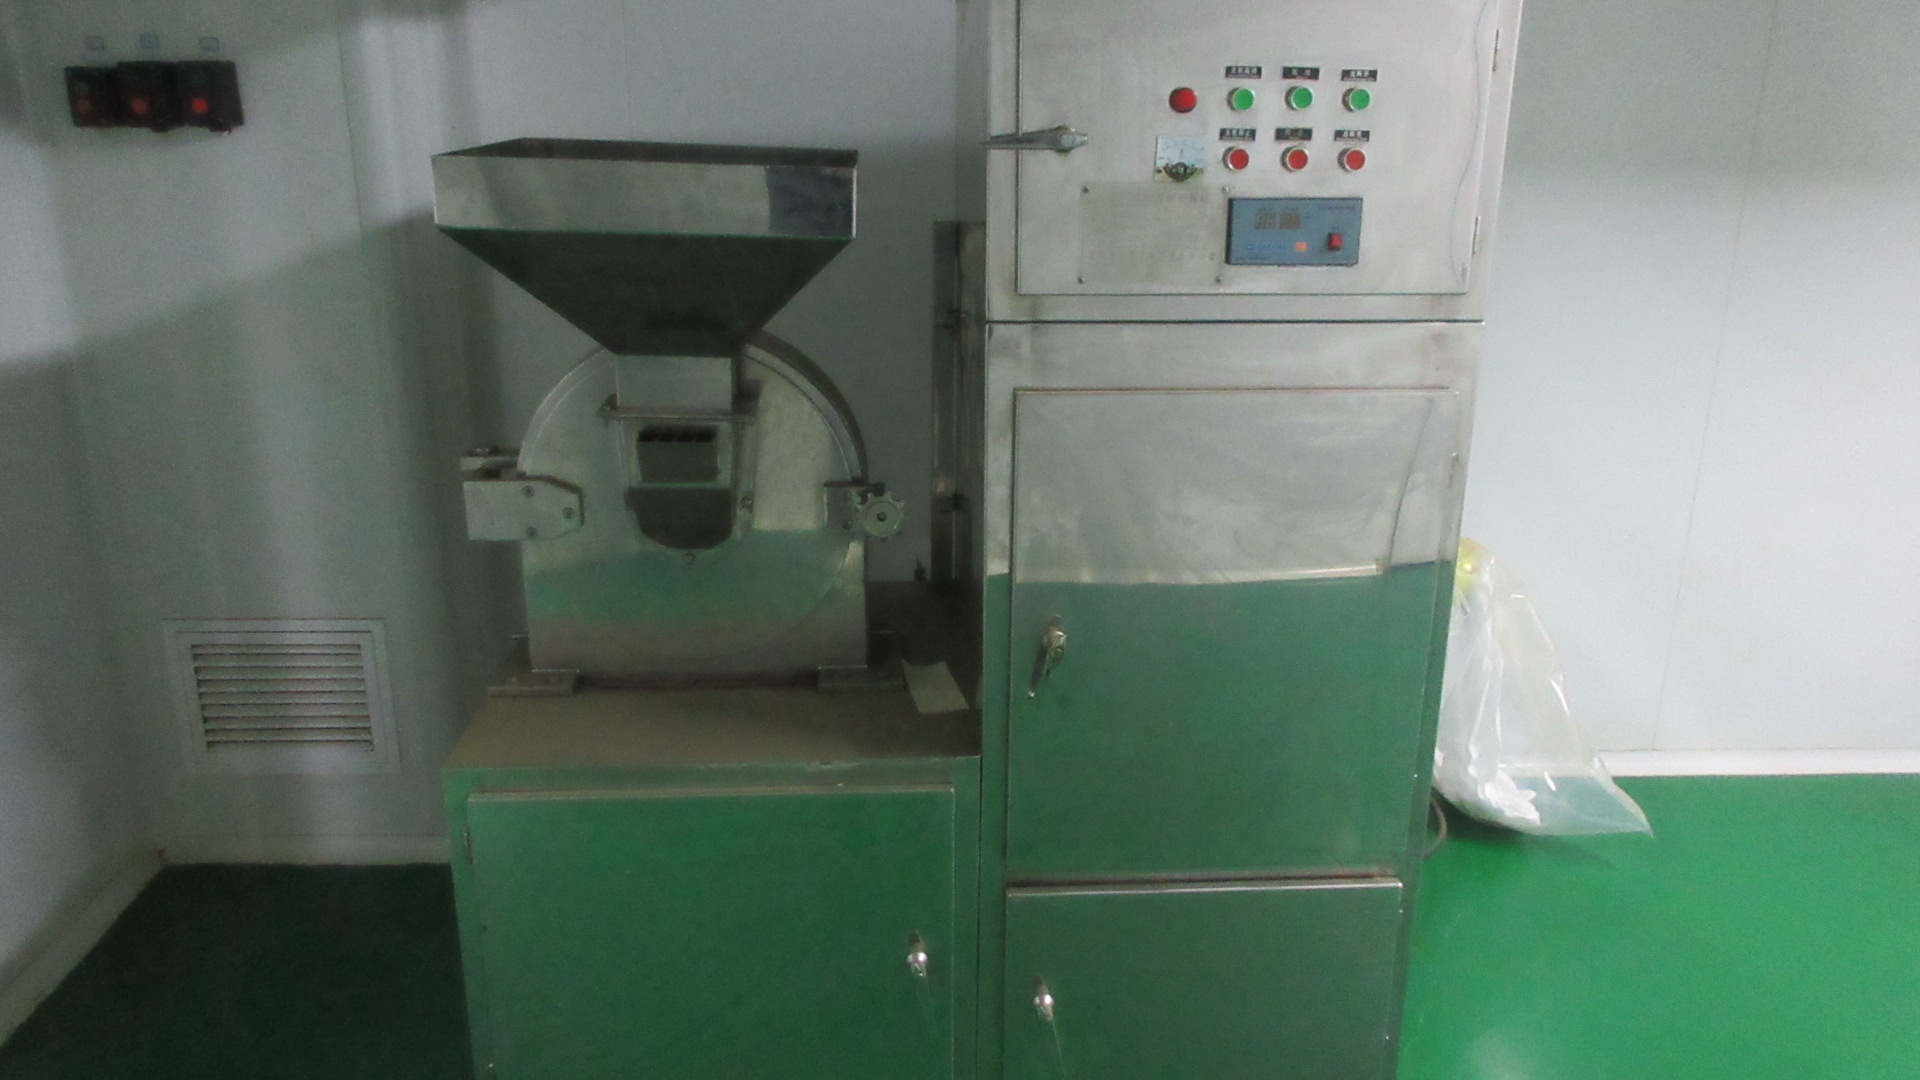
6. Precision Pulverizing
Ultra-fine impact milling controls particle size distribution suited for capsules, tableting, or ready-to-drink beverage mixes.
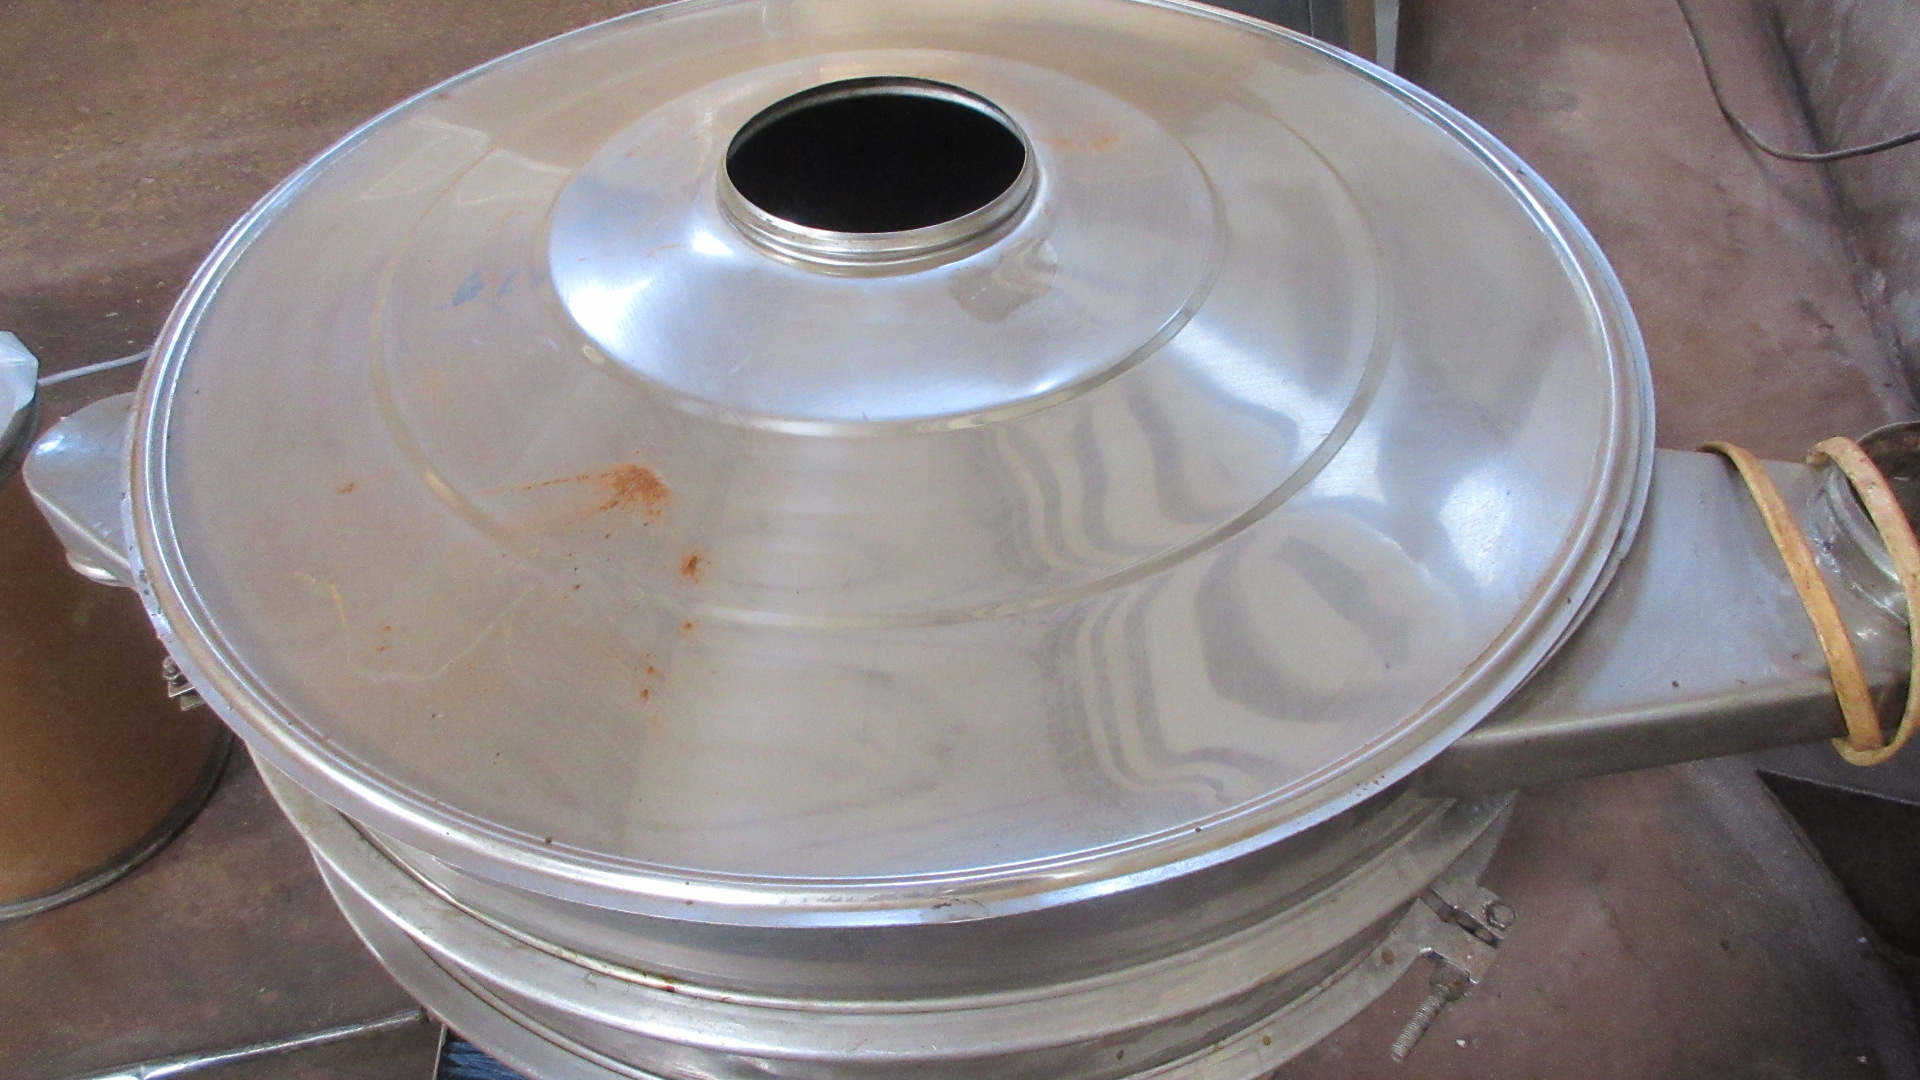
7. Vibrating Mesh Sieving
High-frequency grading screens ensure uniform granularity (80 to 450 mesh) coupled with in-line rare-earth magnetic separation.
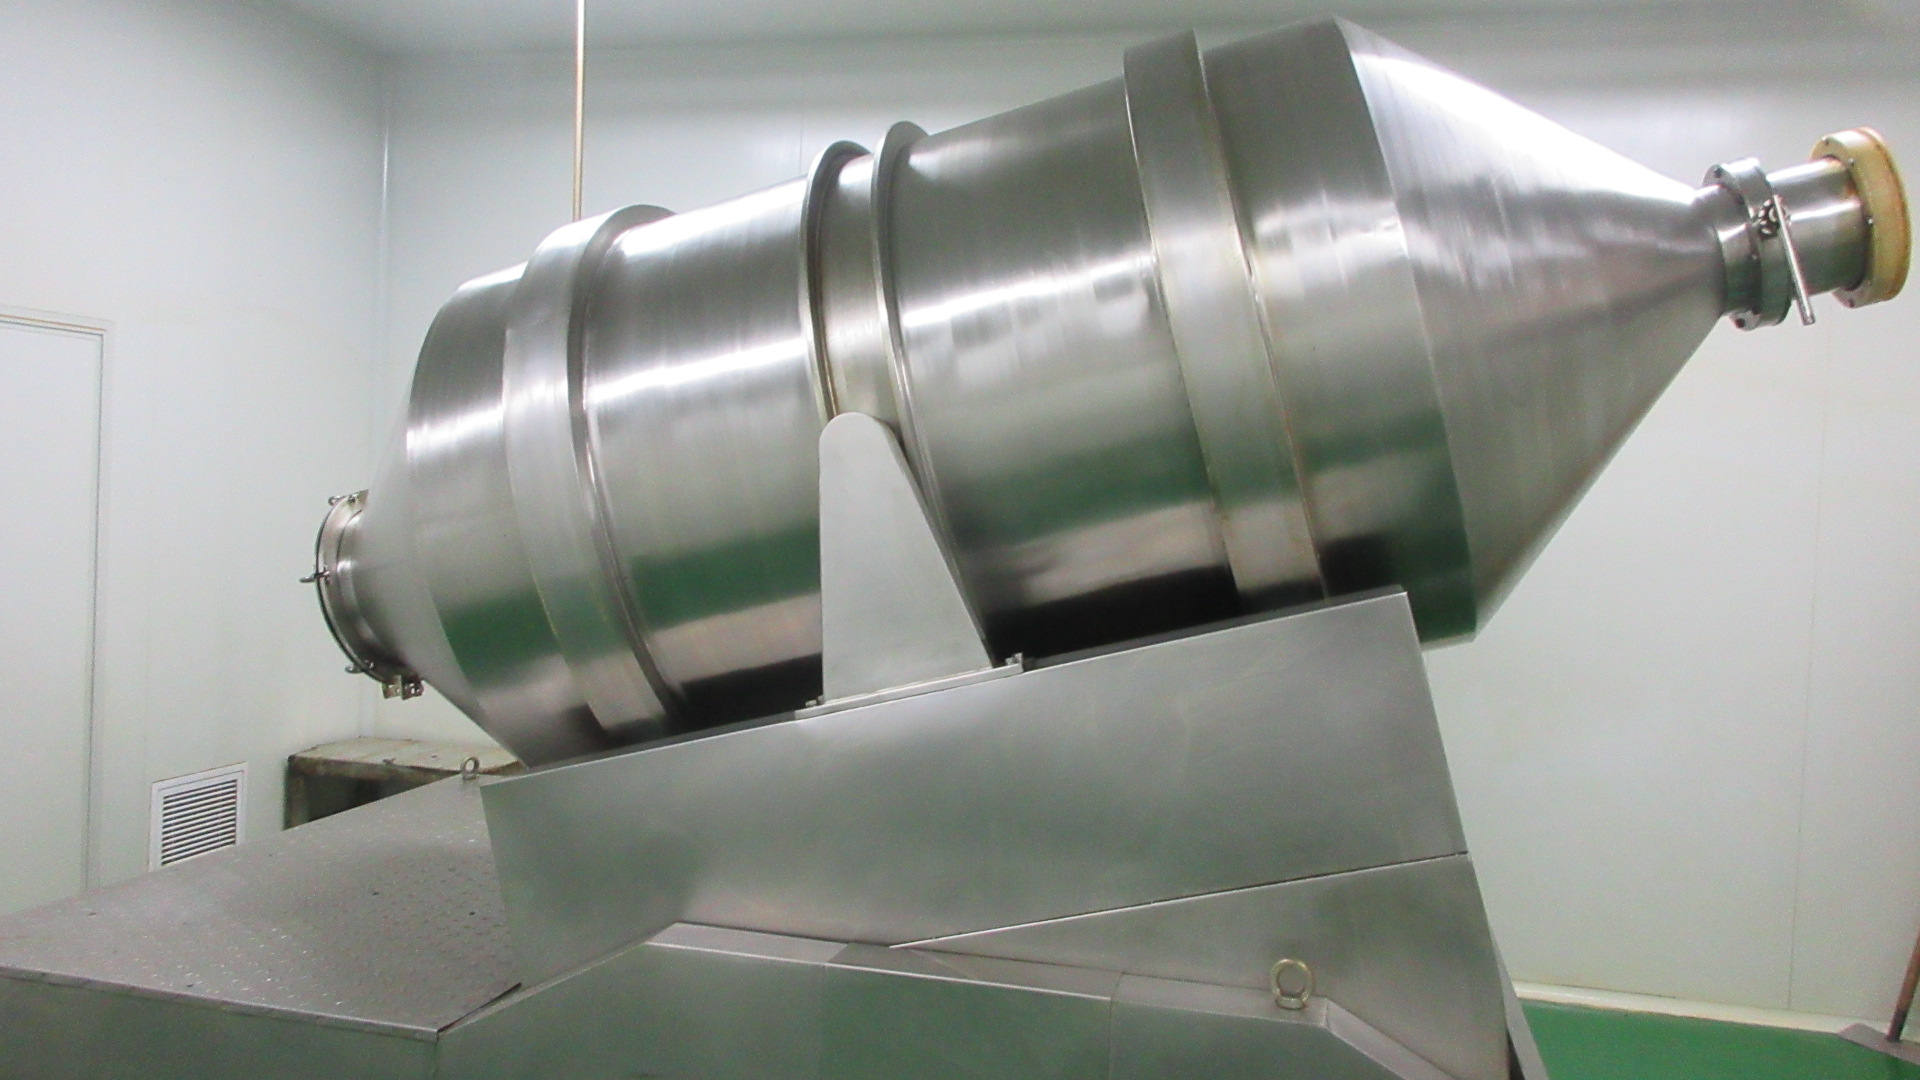
8. Homogeneous Mixing
Three-dimensional powder blenders guarantee homogeneous active content across multi-thousand kilogram production batches.
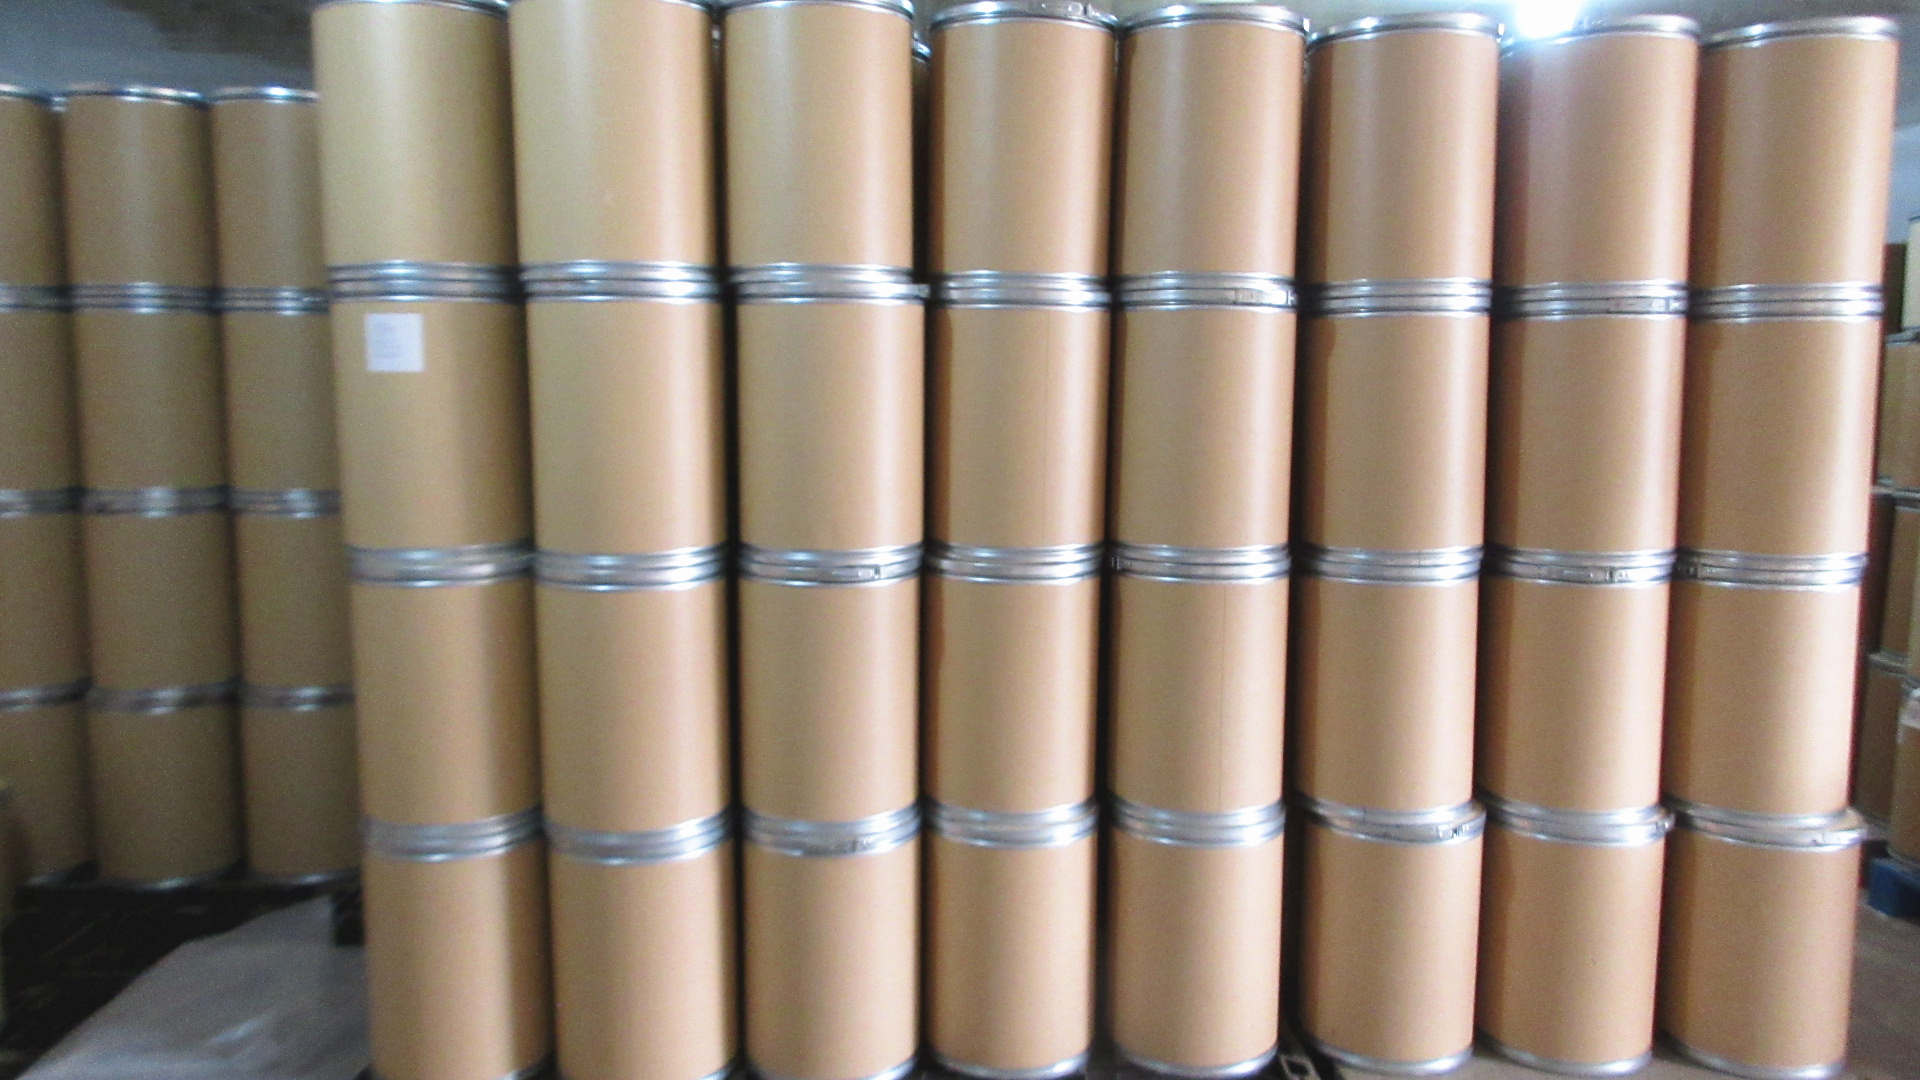
9. Finished Product Pack
Double food-grade inner aseptic PE bags sealed in tamper-evident fiber drums or custom retail barrier pouches with batch lot COAs.
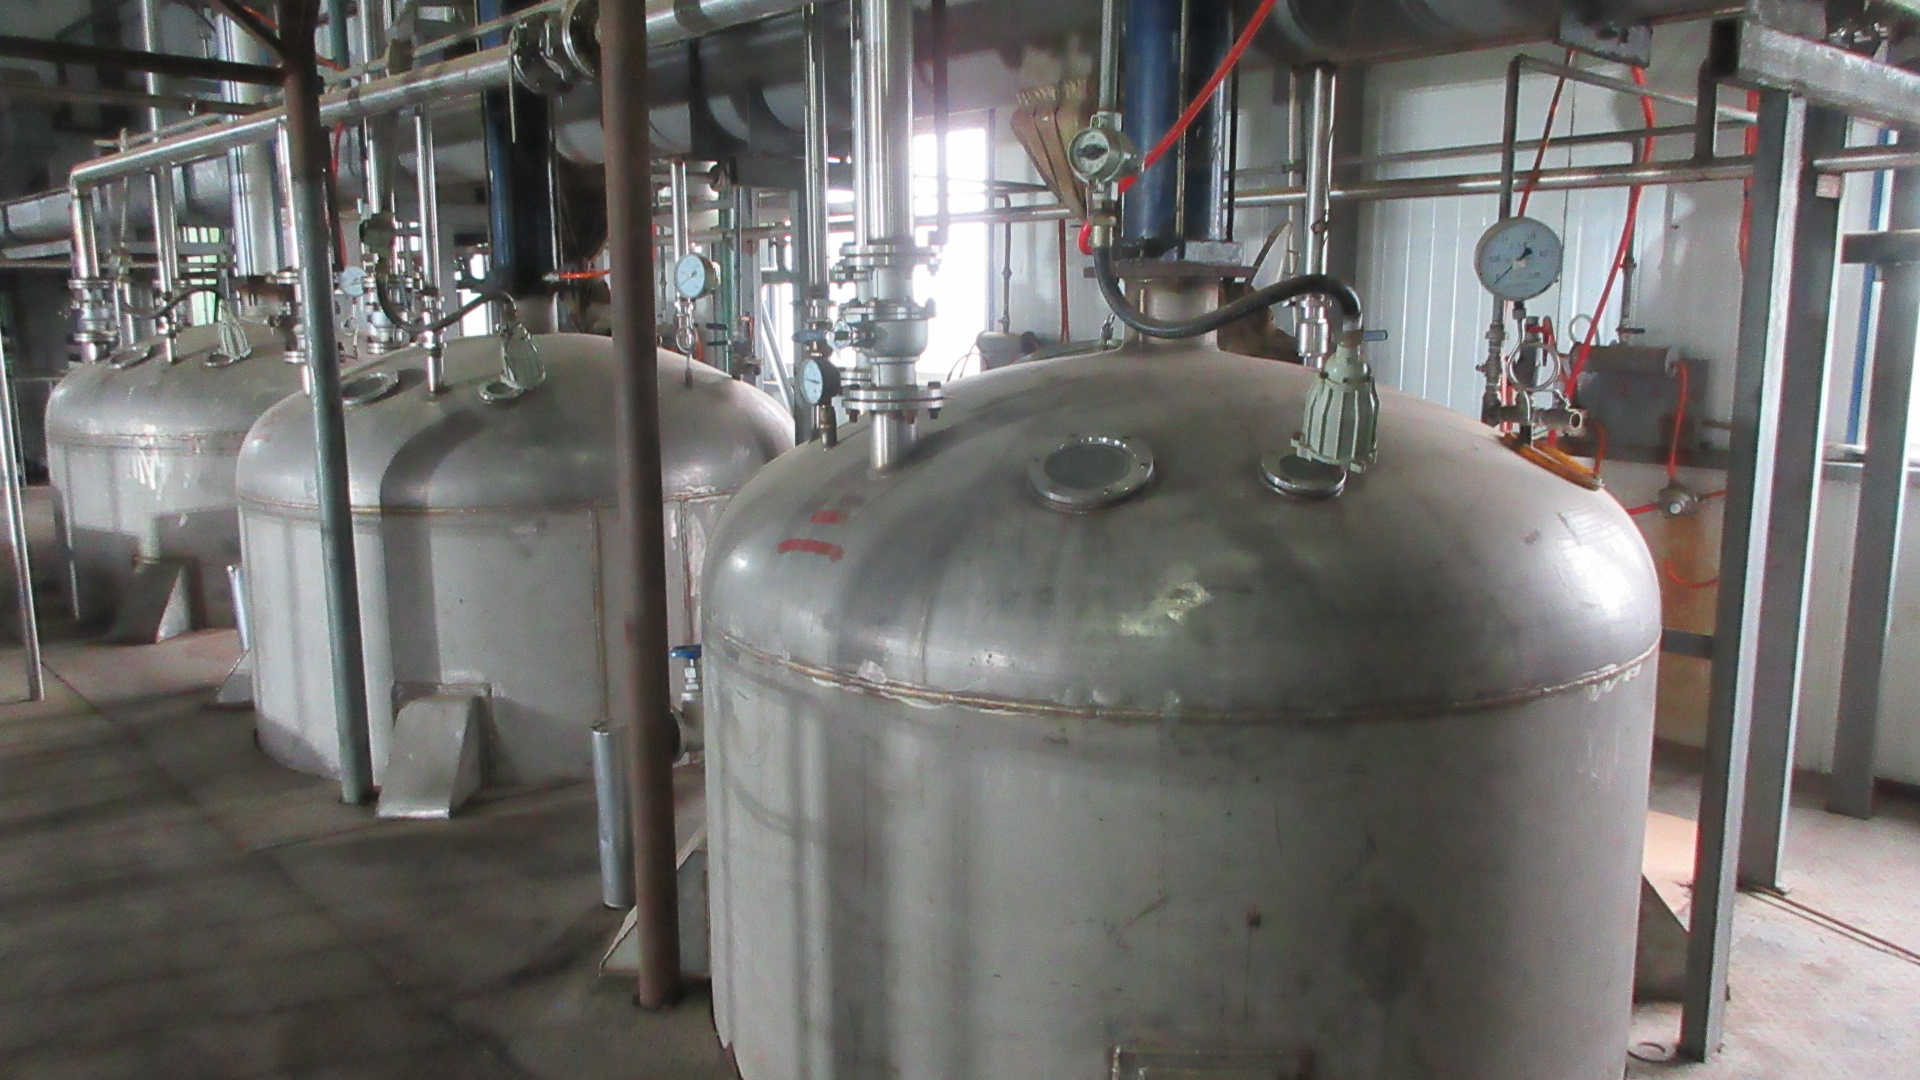
Extracting Tank
Sanitary SUS304/SUS316 stainless multi-functional dynamic extractors with reflux condensers and automated temperature controls.
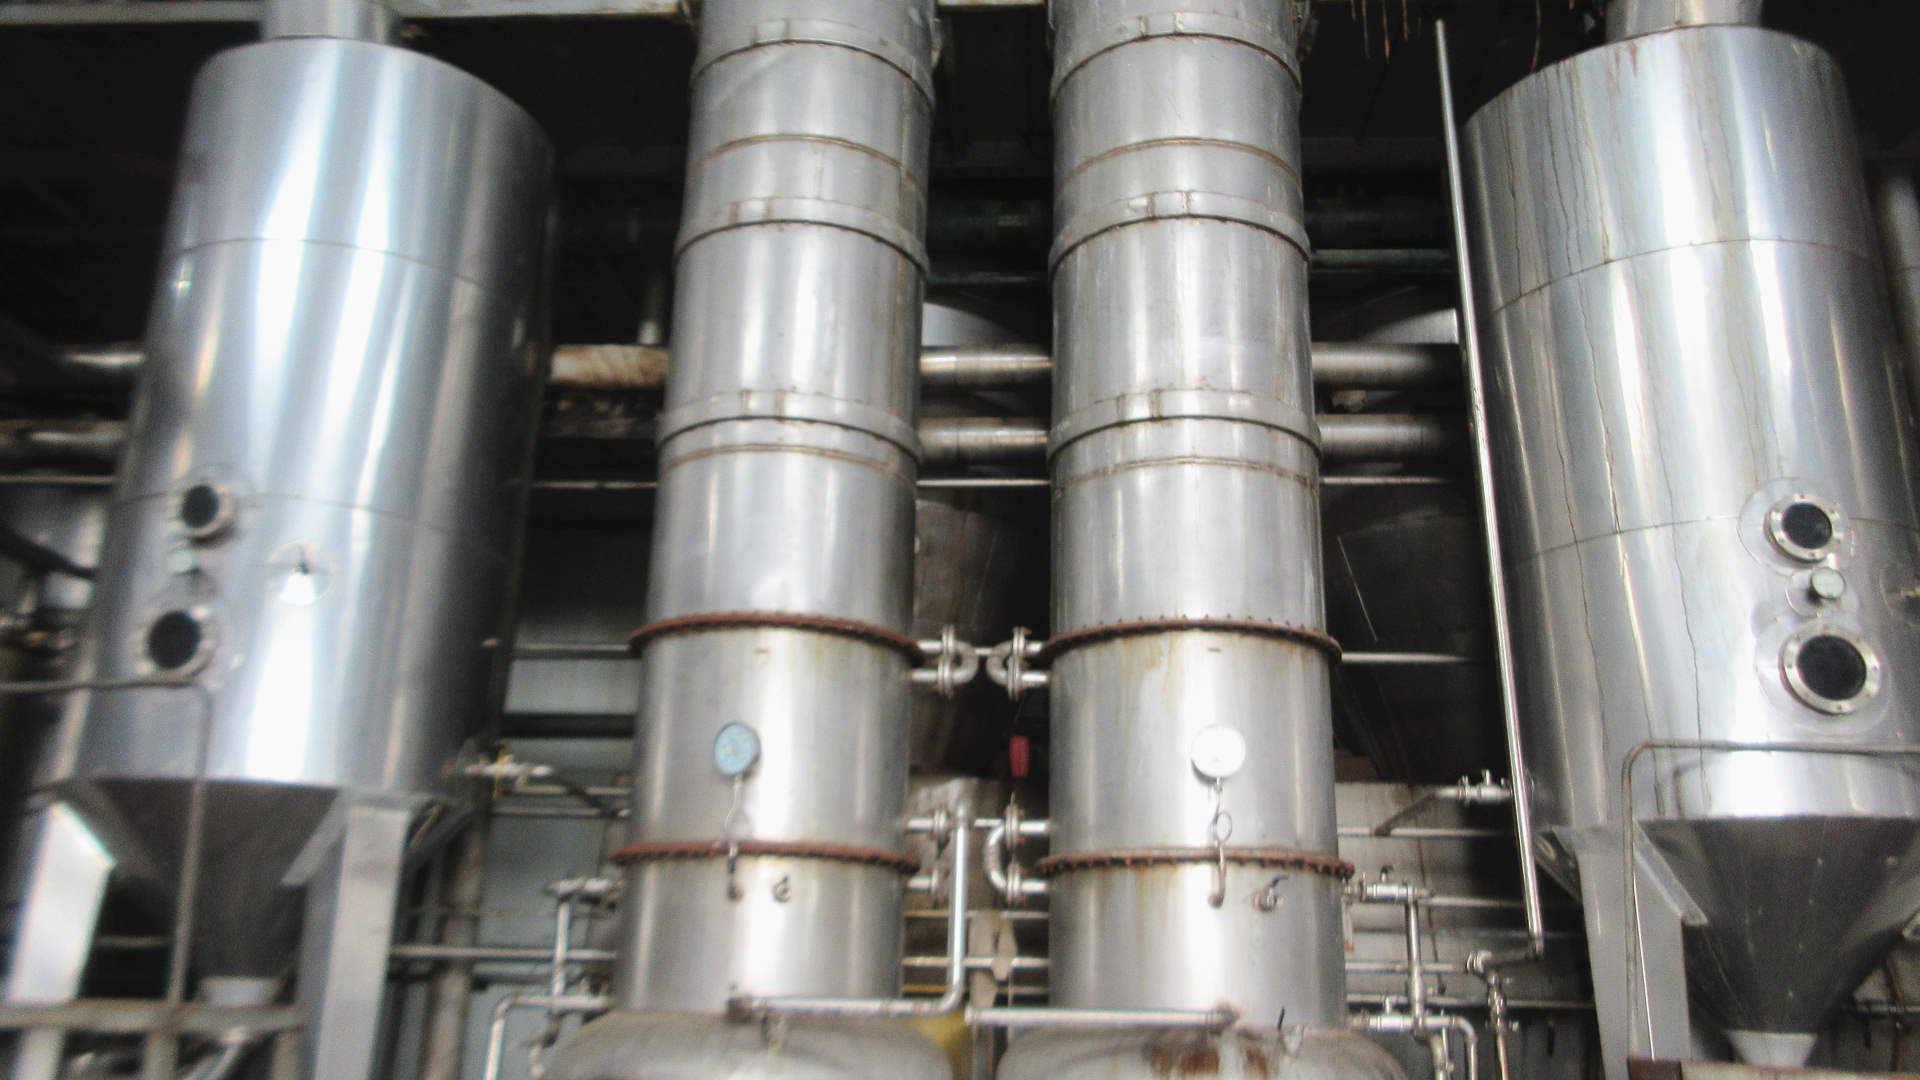
Concentrator
Energy-efficient falling film and external circulation vacuum evaporators operating at optimal low thermal thresholds.
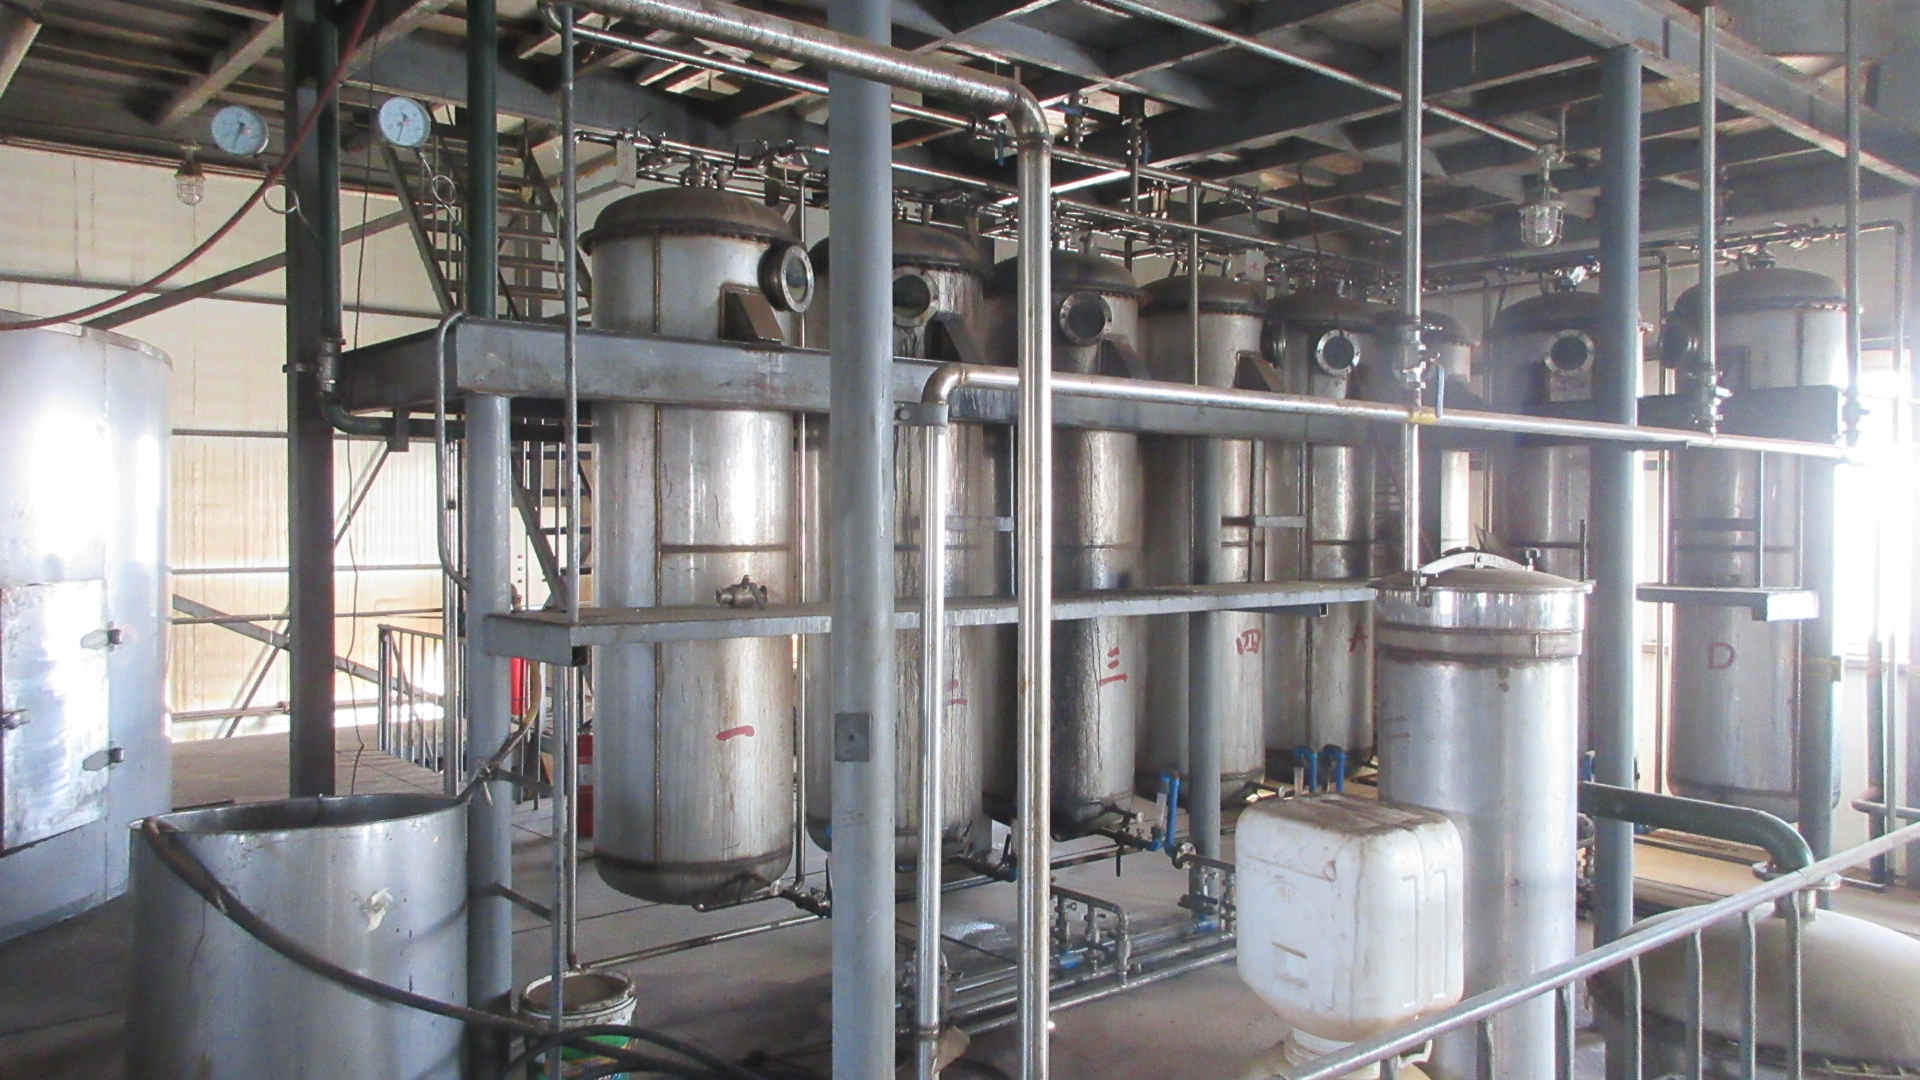
Purification Equipment
Multi-stage chromatography columns and membrane ultrafiltration skids for high-enrichment active isolation.
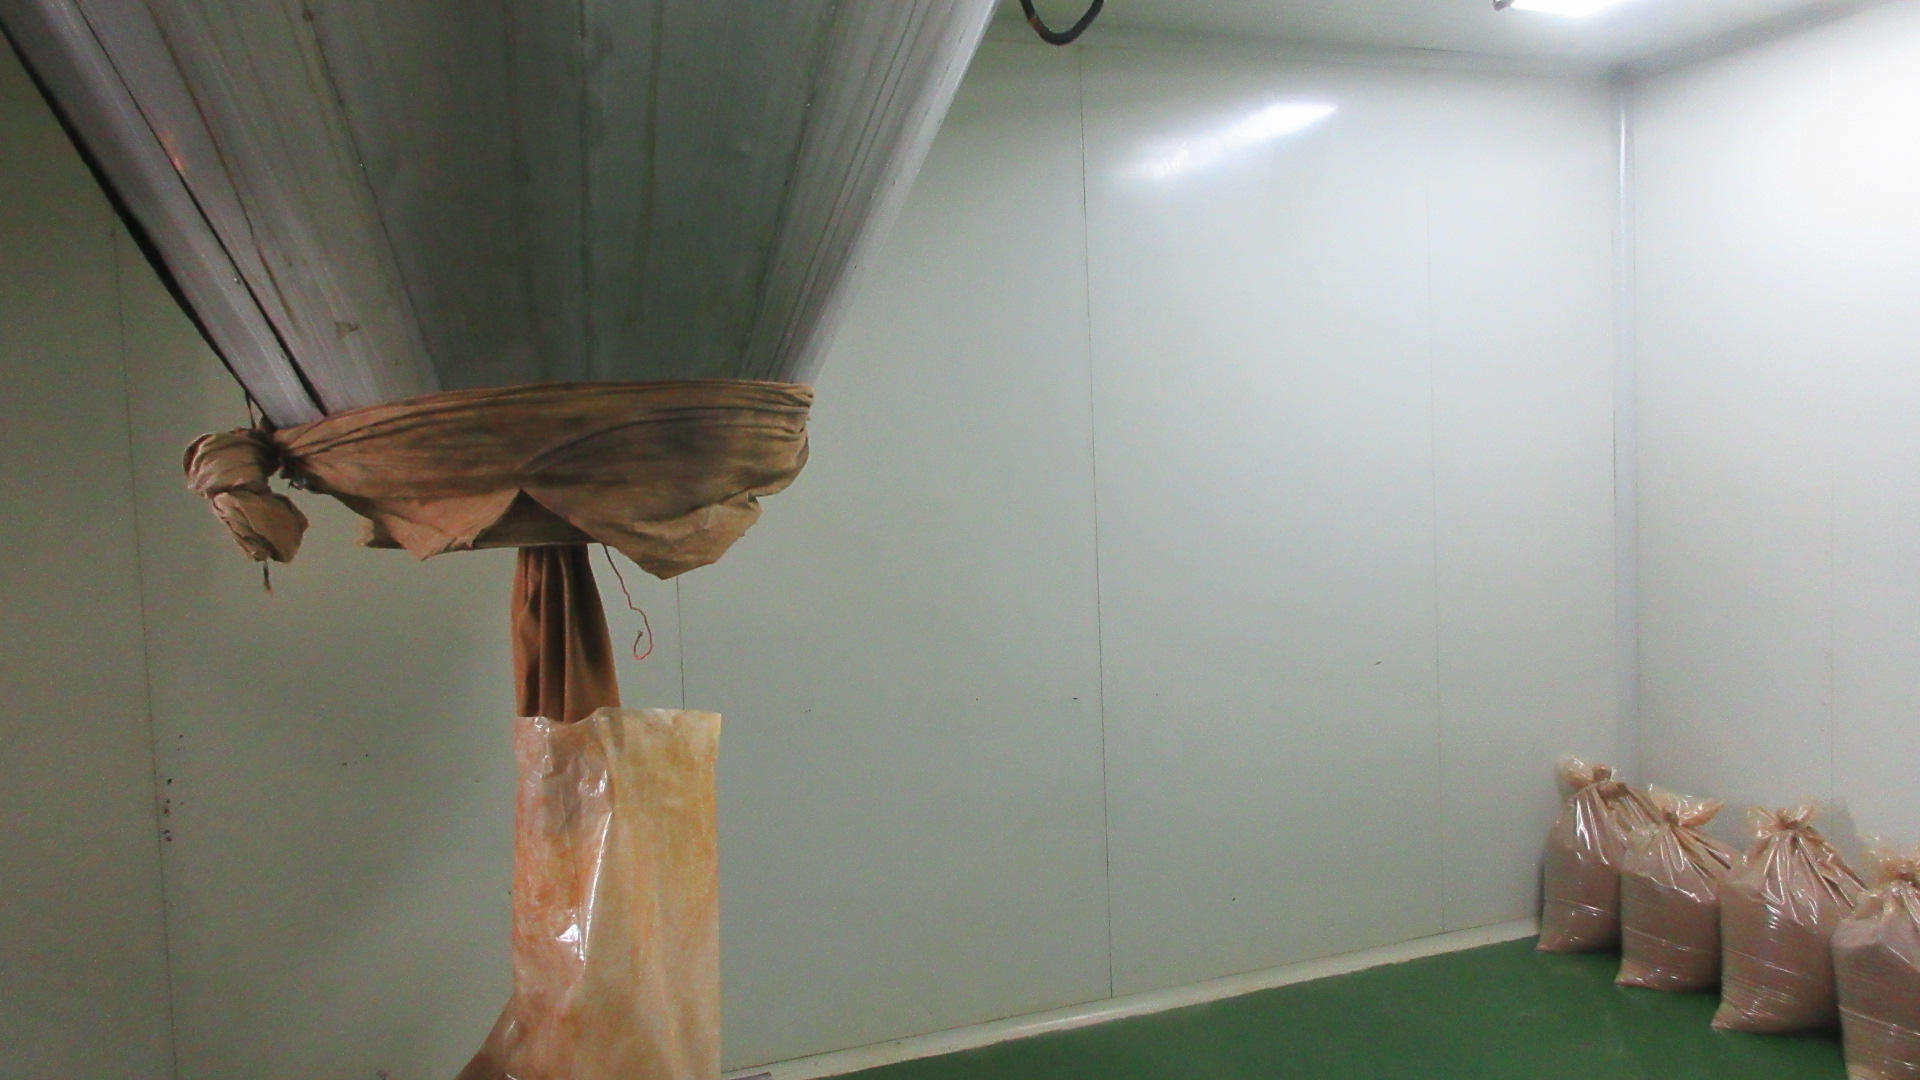
Spraying Tower
Sanitary high-speed centrifugal spray dryers with clean air HEPA filtration, dehumidification, and rapid cooling collectors.
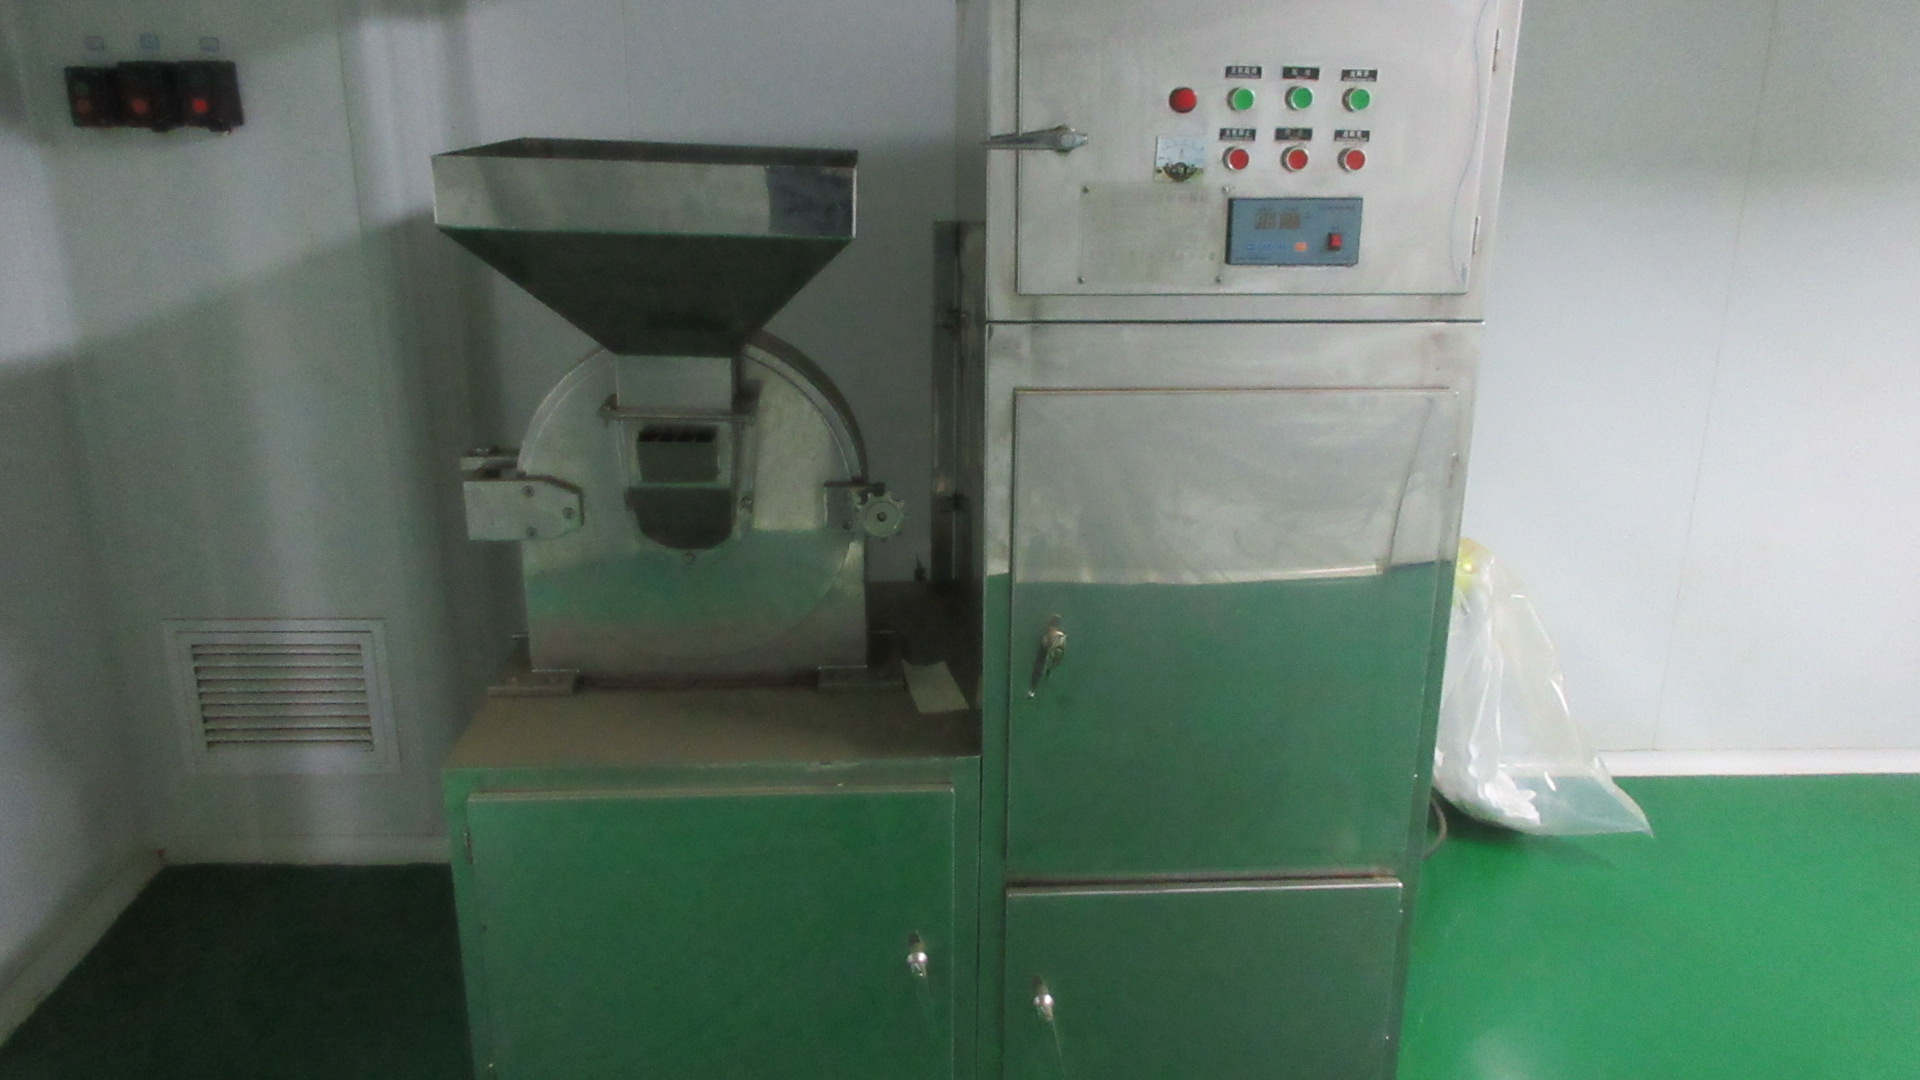
Pulverizer
Water-cooled fine mechanical grinder units preventing heat-induced degradation during continuous pulverization.
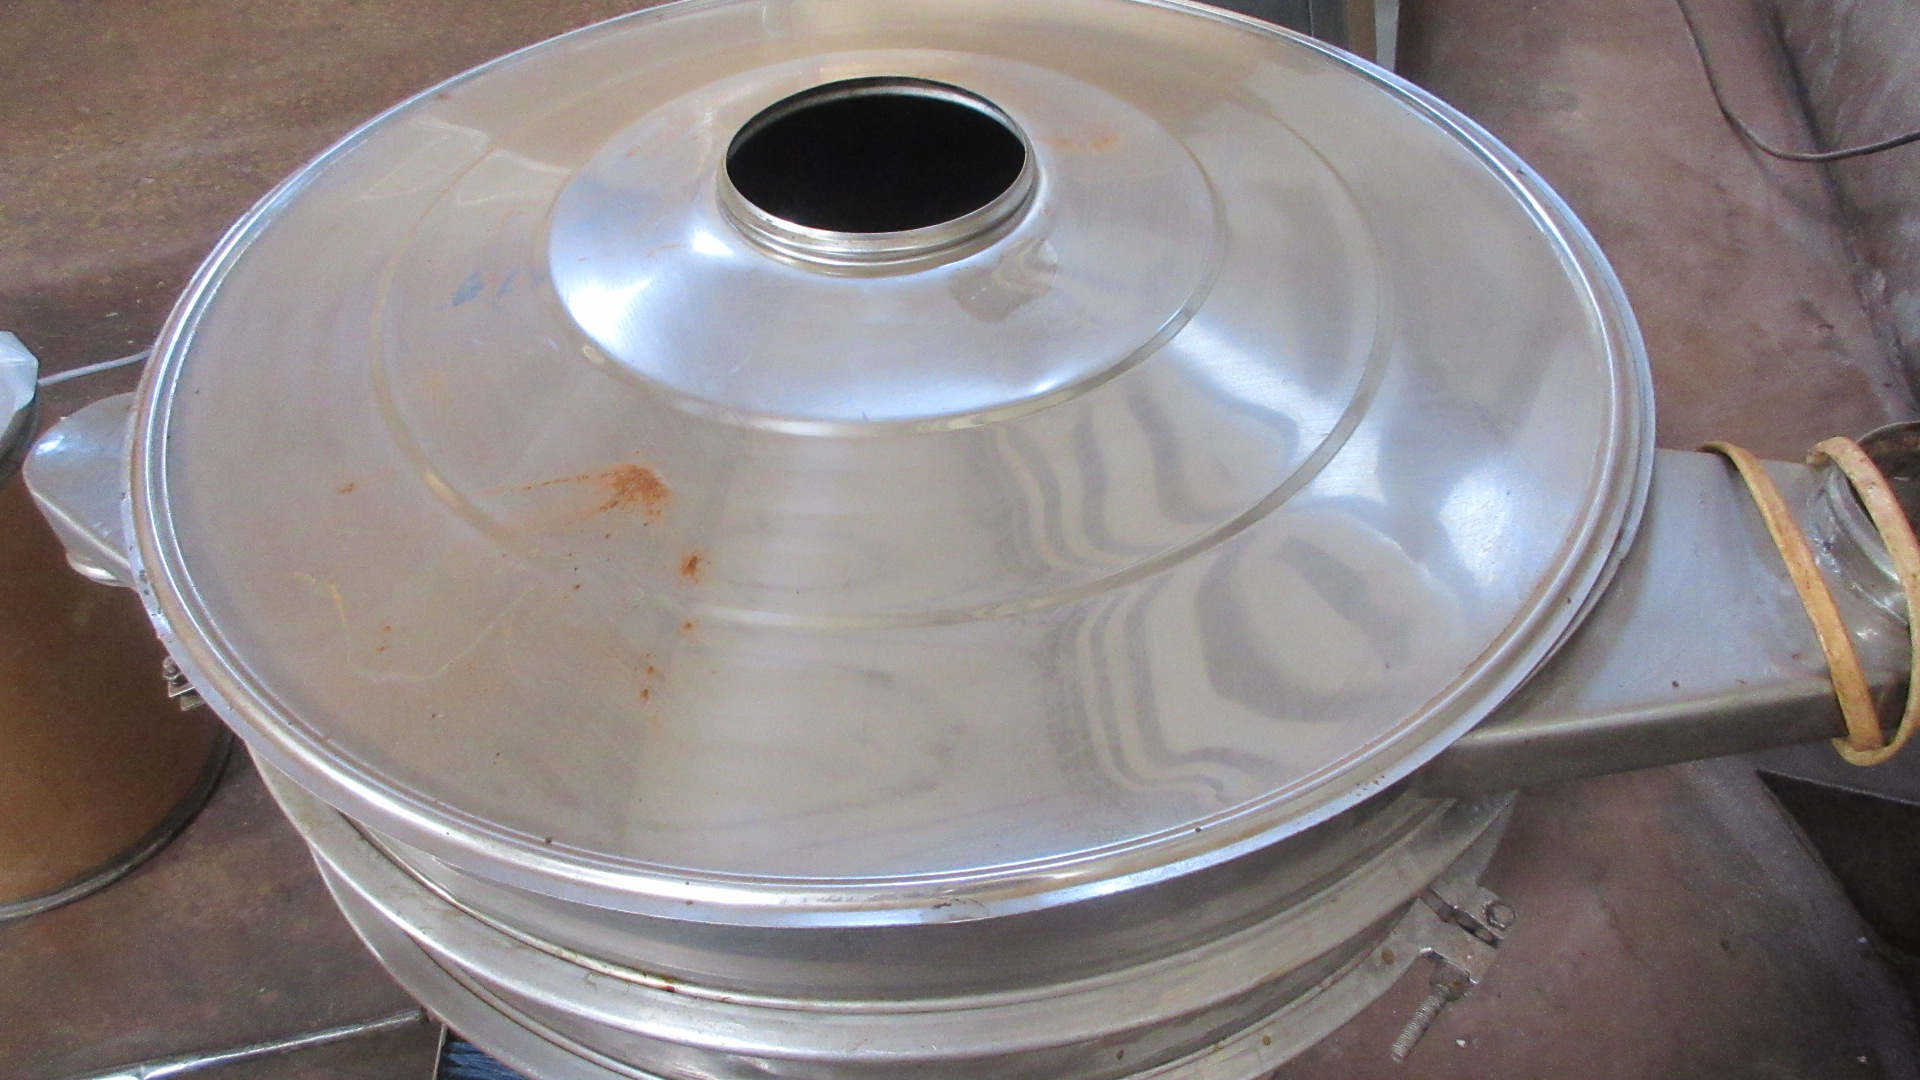
Sieving Machine
Aseptic multi-deck vibratory screens isolating exact target particle dimensions while eliminating fines and agglomerates.
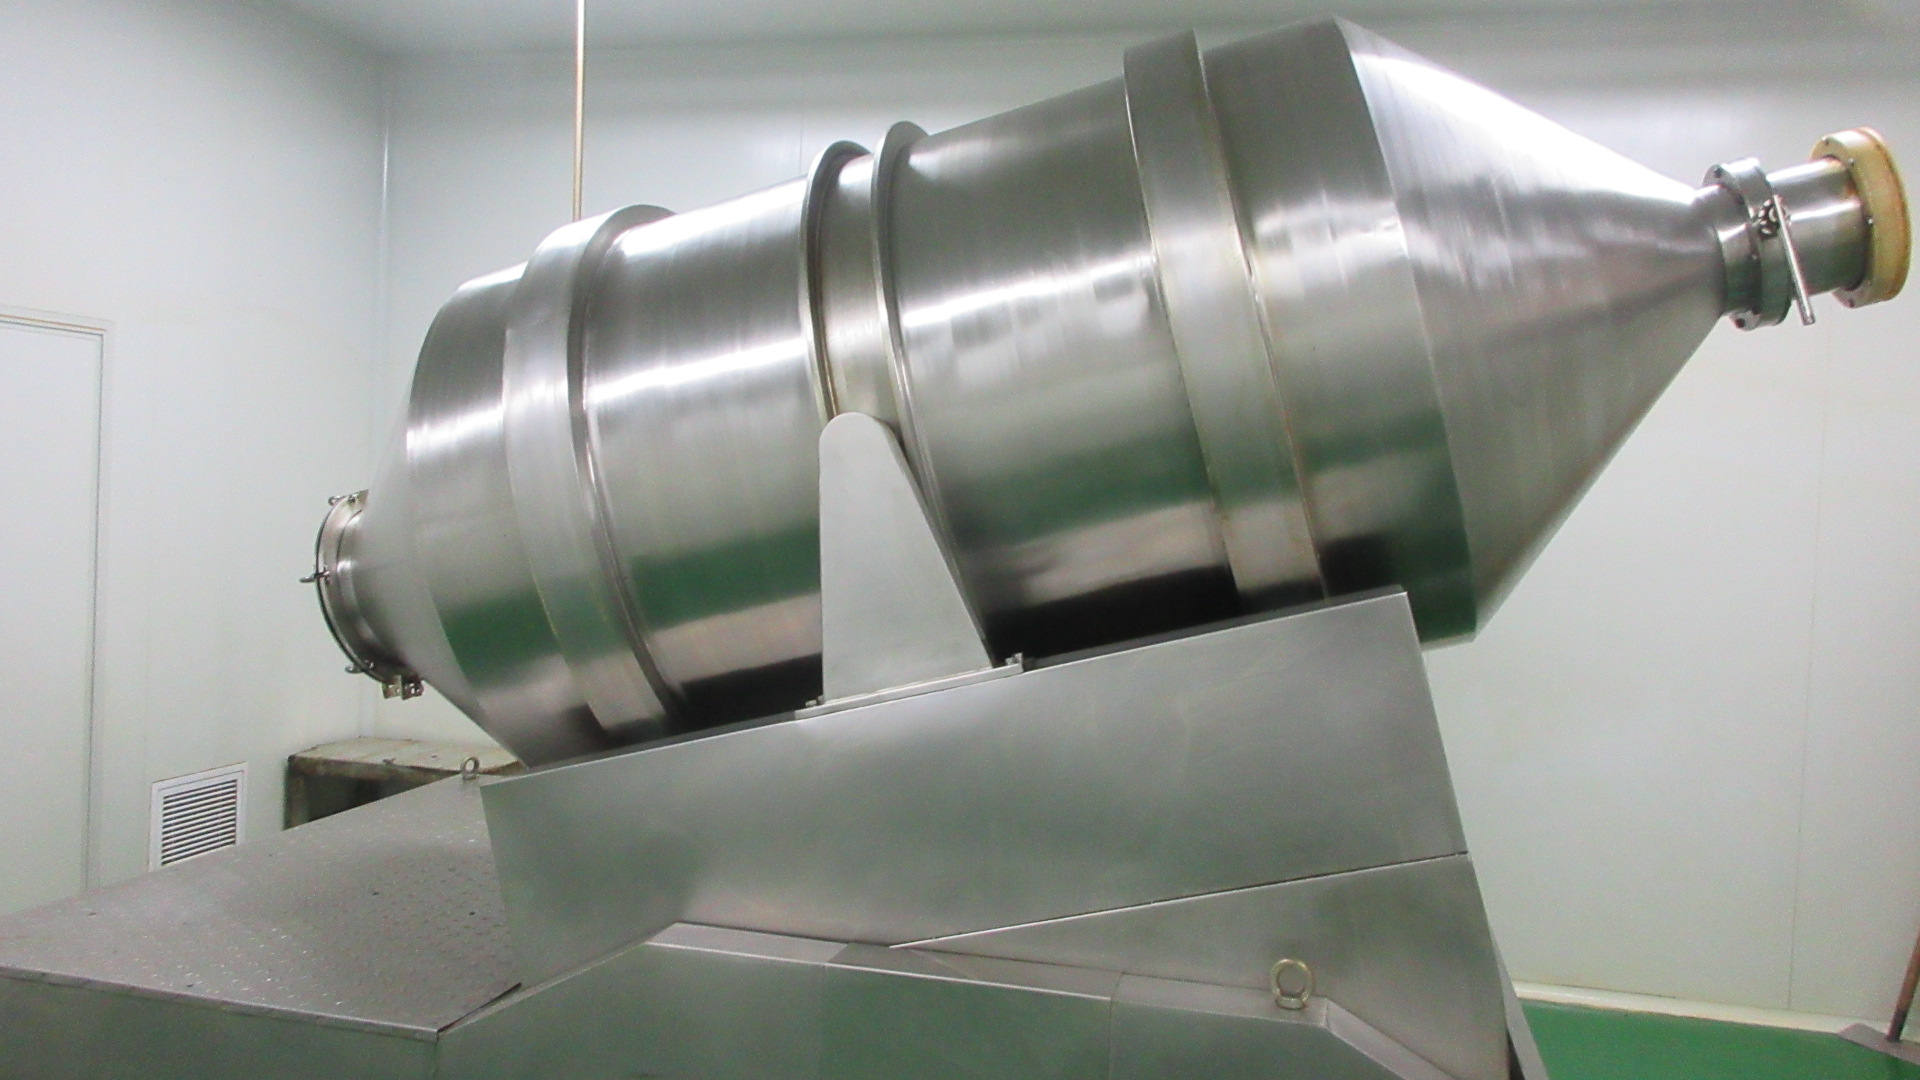
Powder Mixer
Double-cone and ribbon mechanical blenders engineered for zero-shear, completely consistent homogeneous botanical mixes.
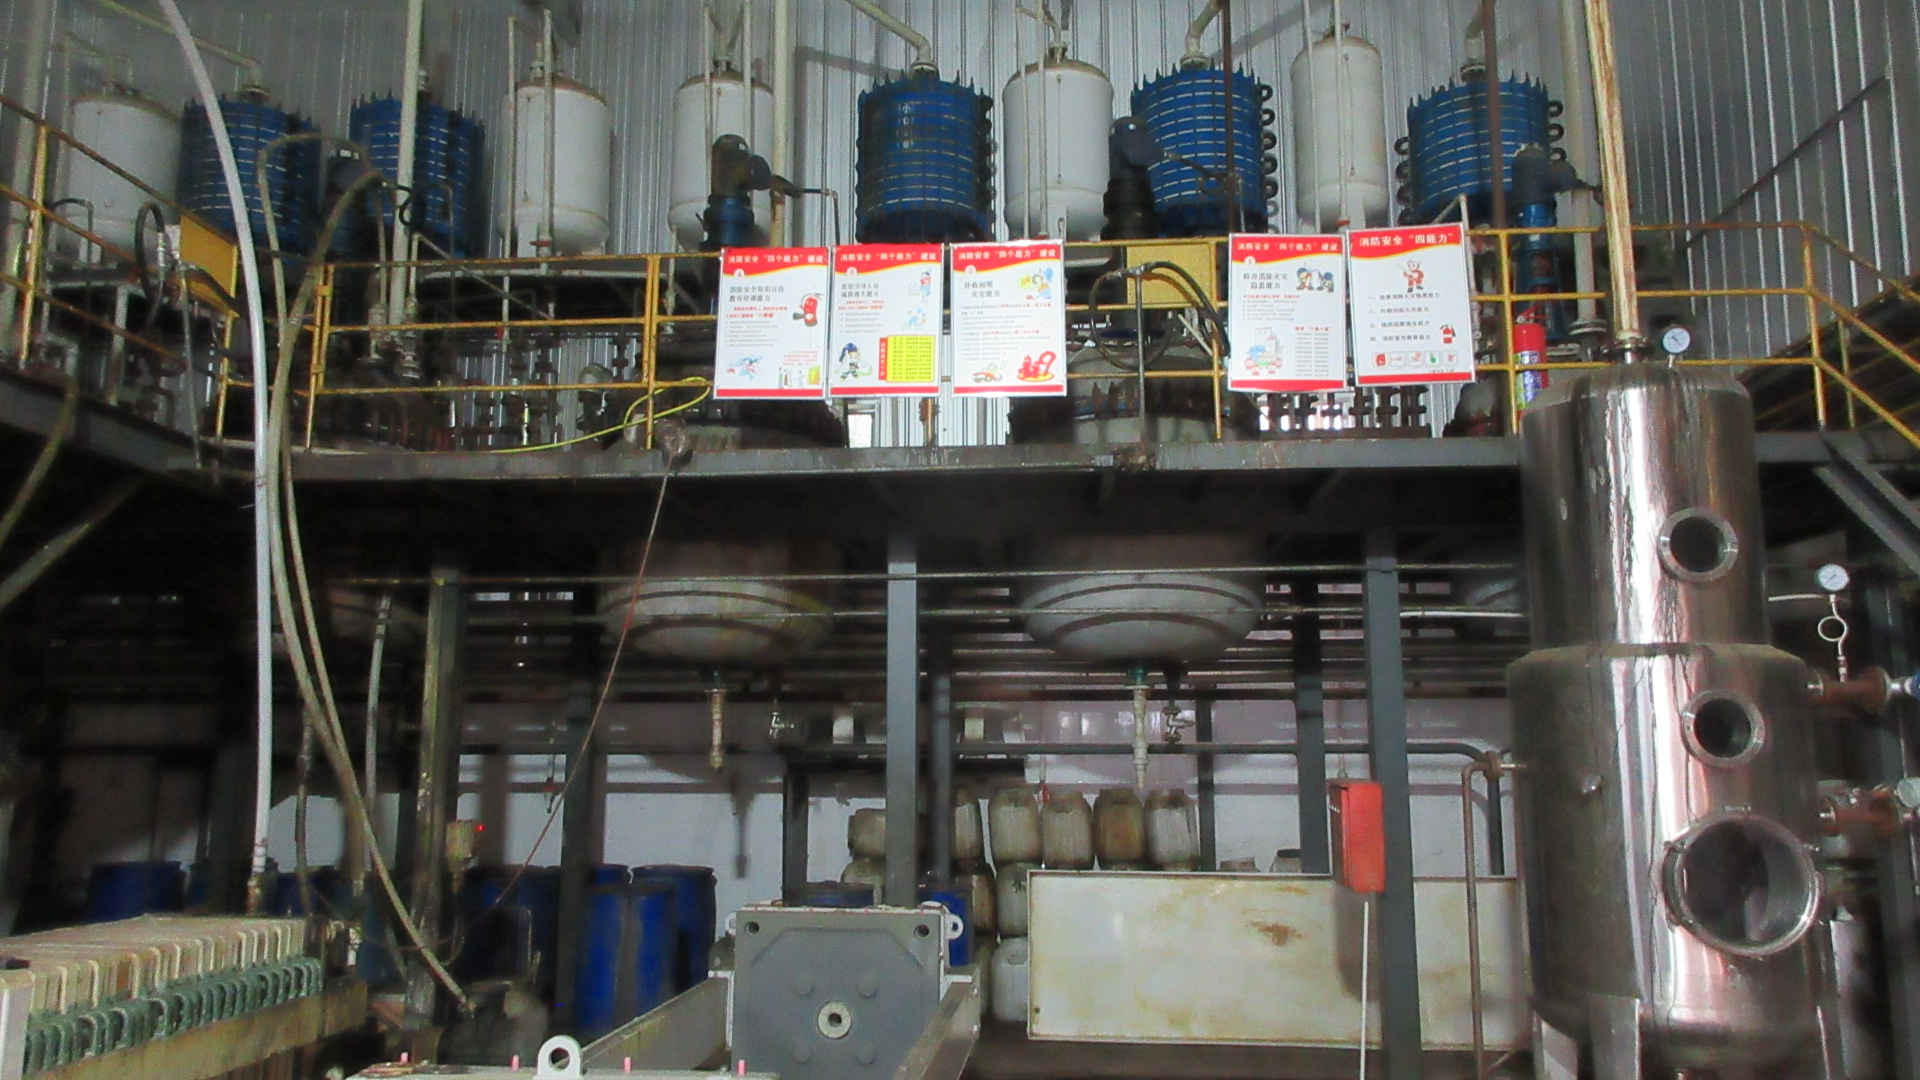
Enamel Reactor
Heavy-duty corrosion-resistant glass-lined vessels for specialized active crystallization and organic synthesis steps.
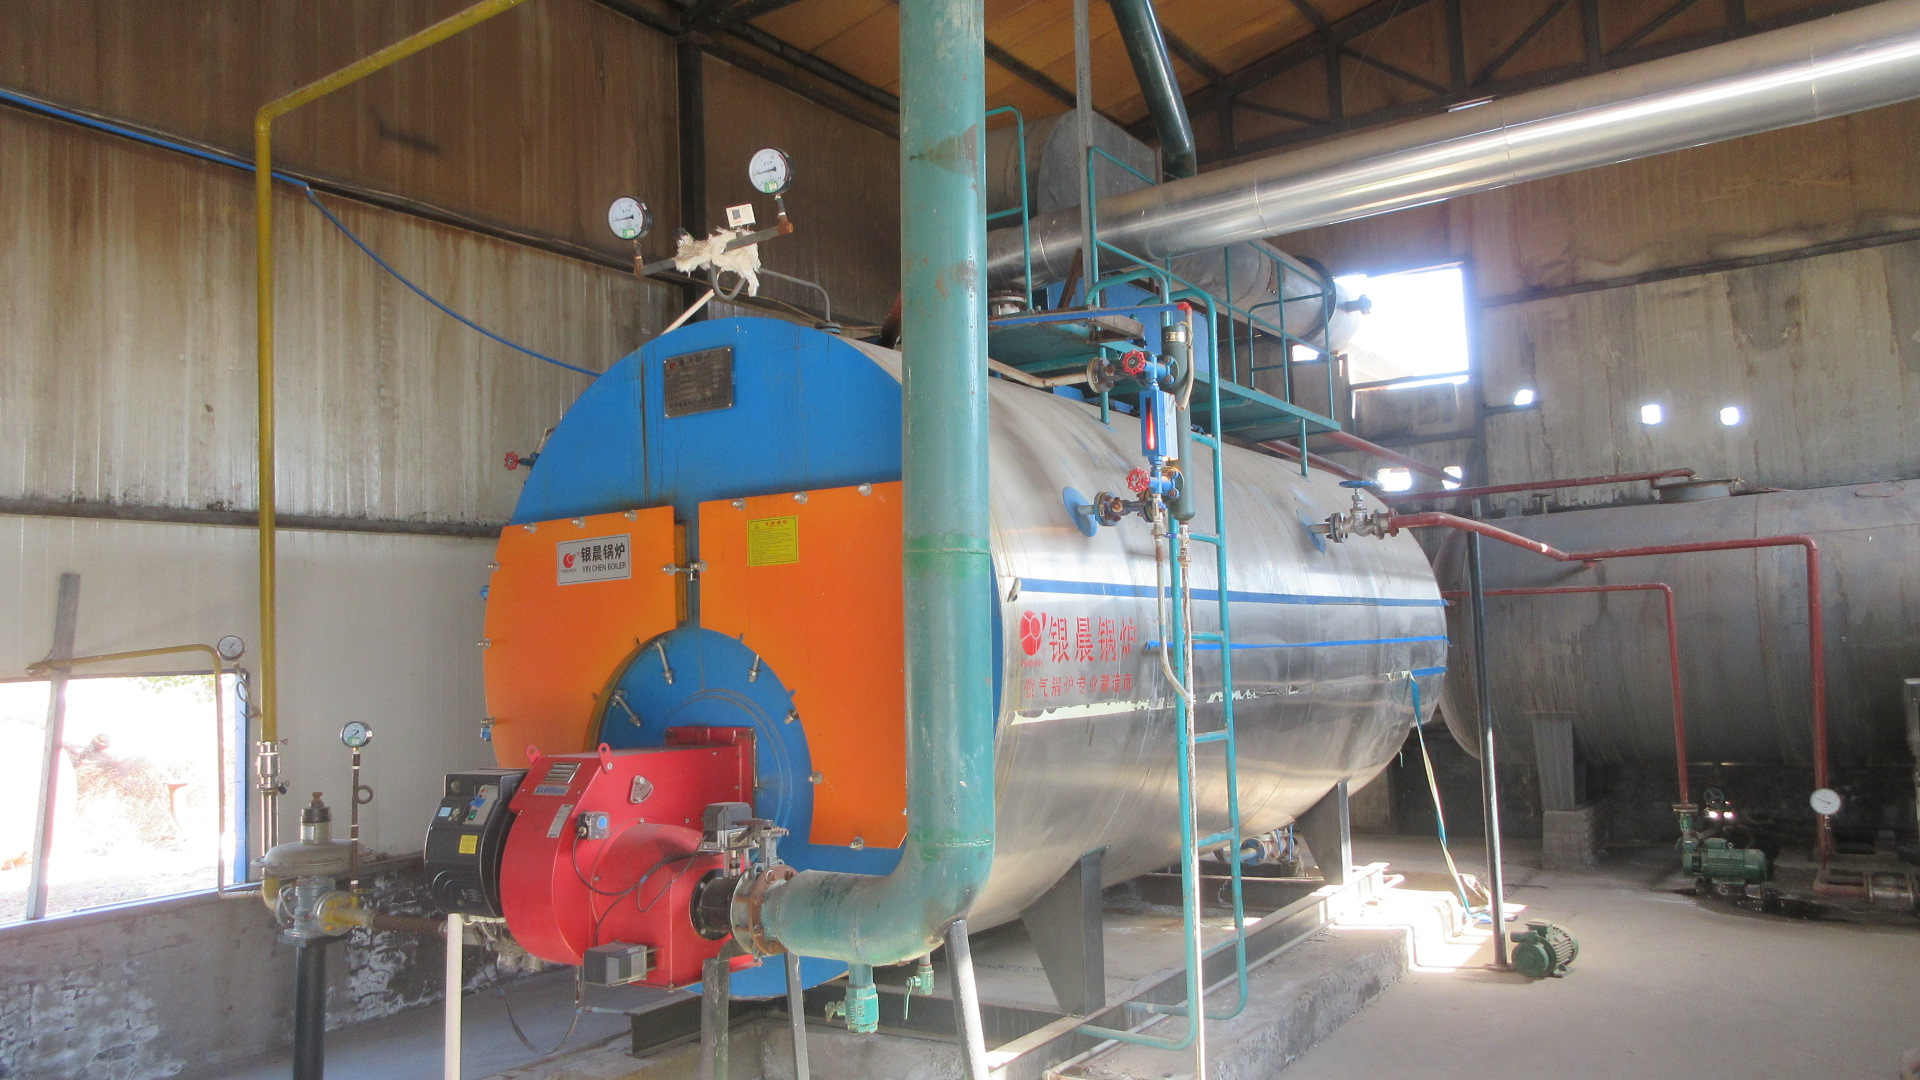
Heating Furnace
High-efficiency thermal control unit providing stable, constant pressure steam to our extraction and evaporation pipelines.
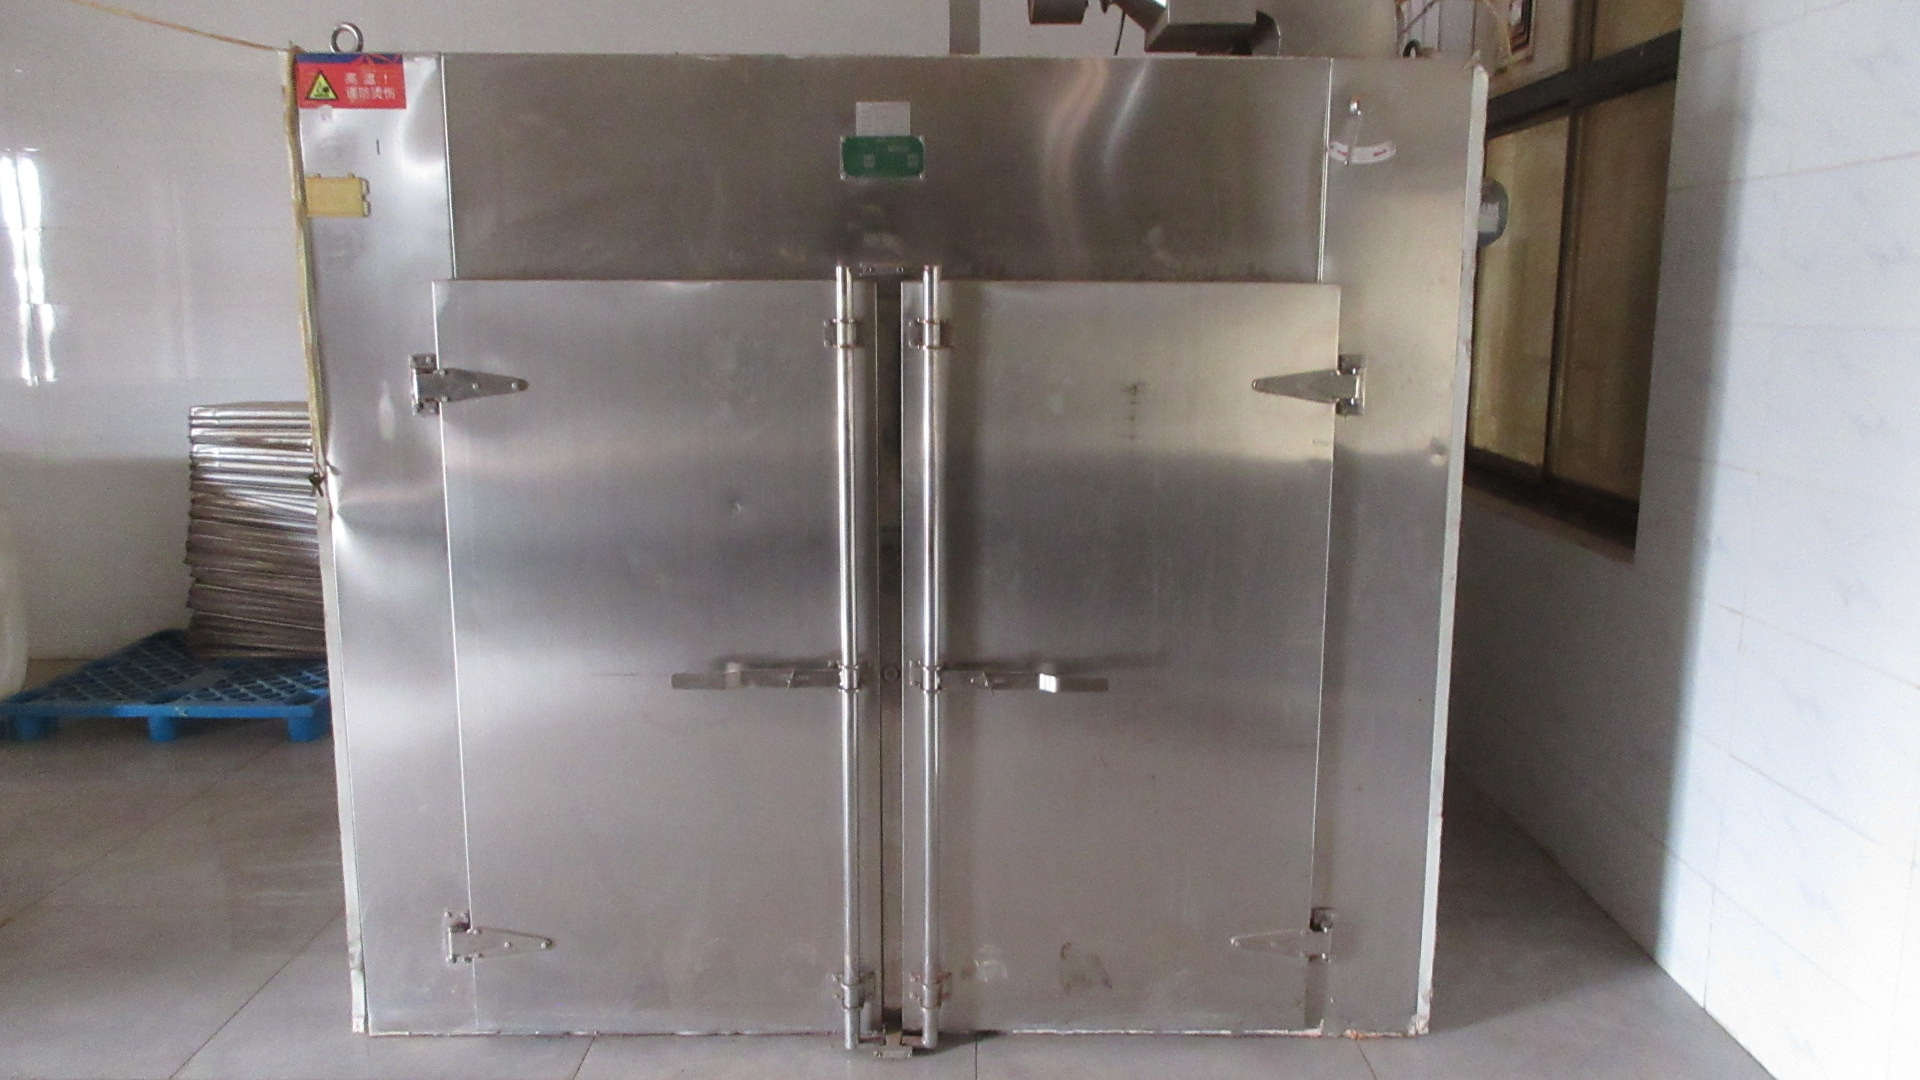
Industrial Dryer
Static vacuum oven drying units specially calibrated for heat-sensitive active ingredients like polyphenols and antioxidants.
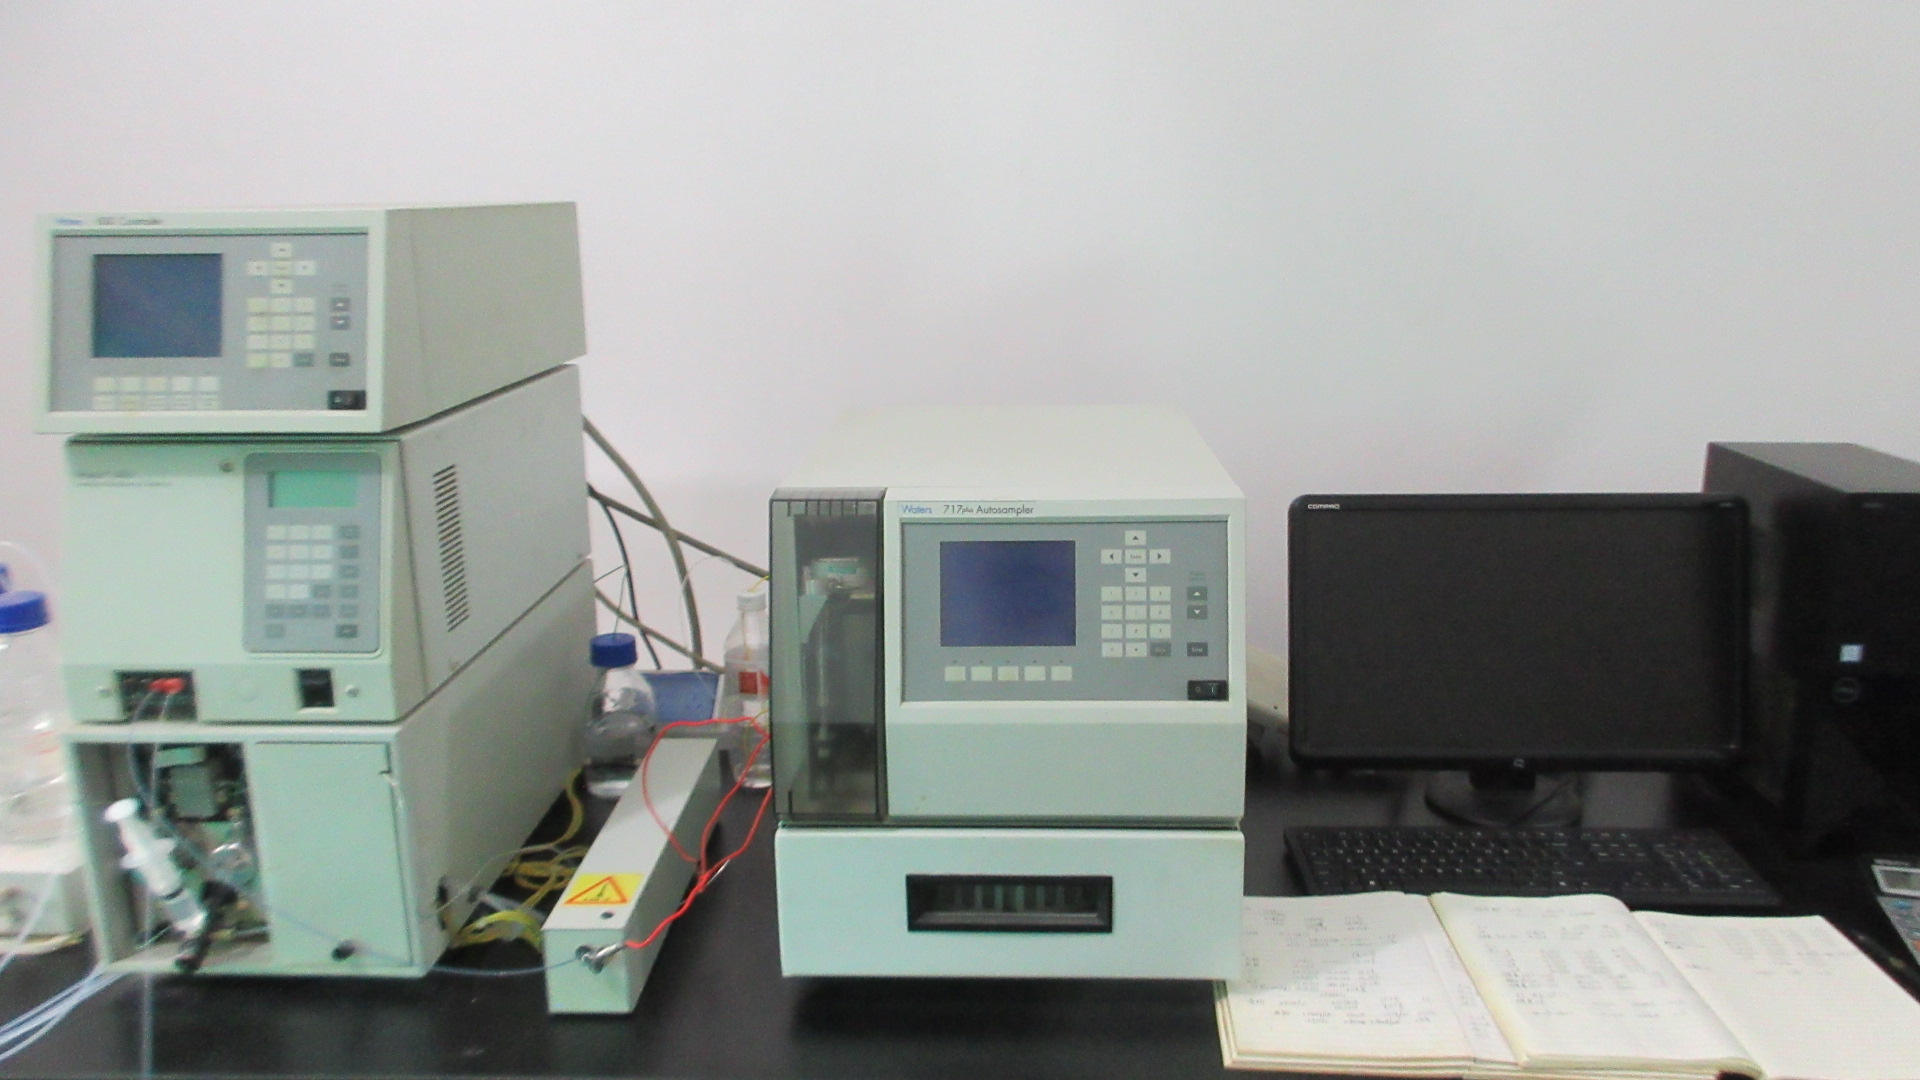
HPLC Chromatography
Quantitative analysis verifying precise percentages of actives including NMN, NAD+, resveratrol, and arbutin.
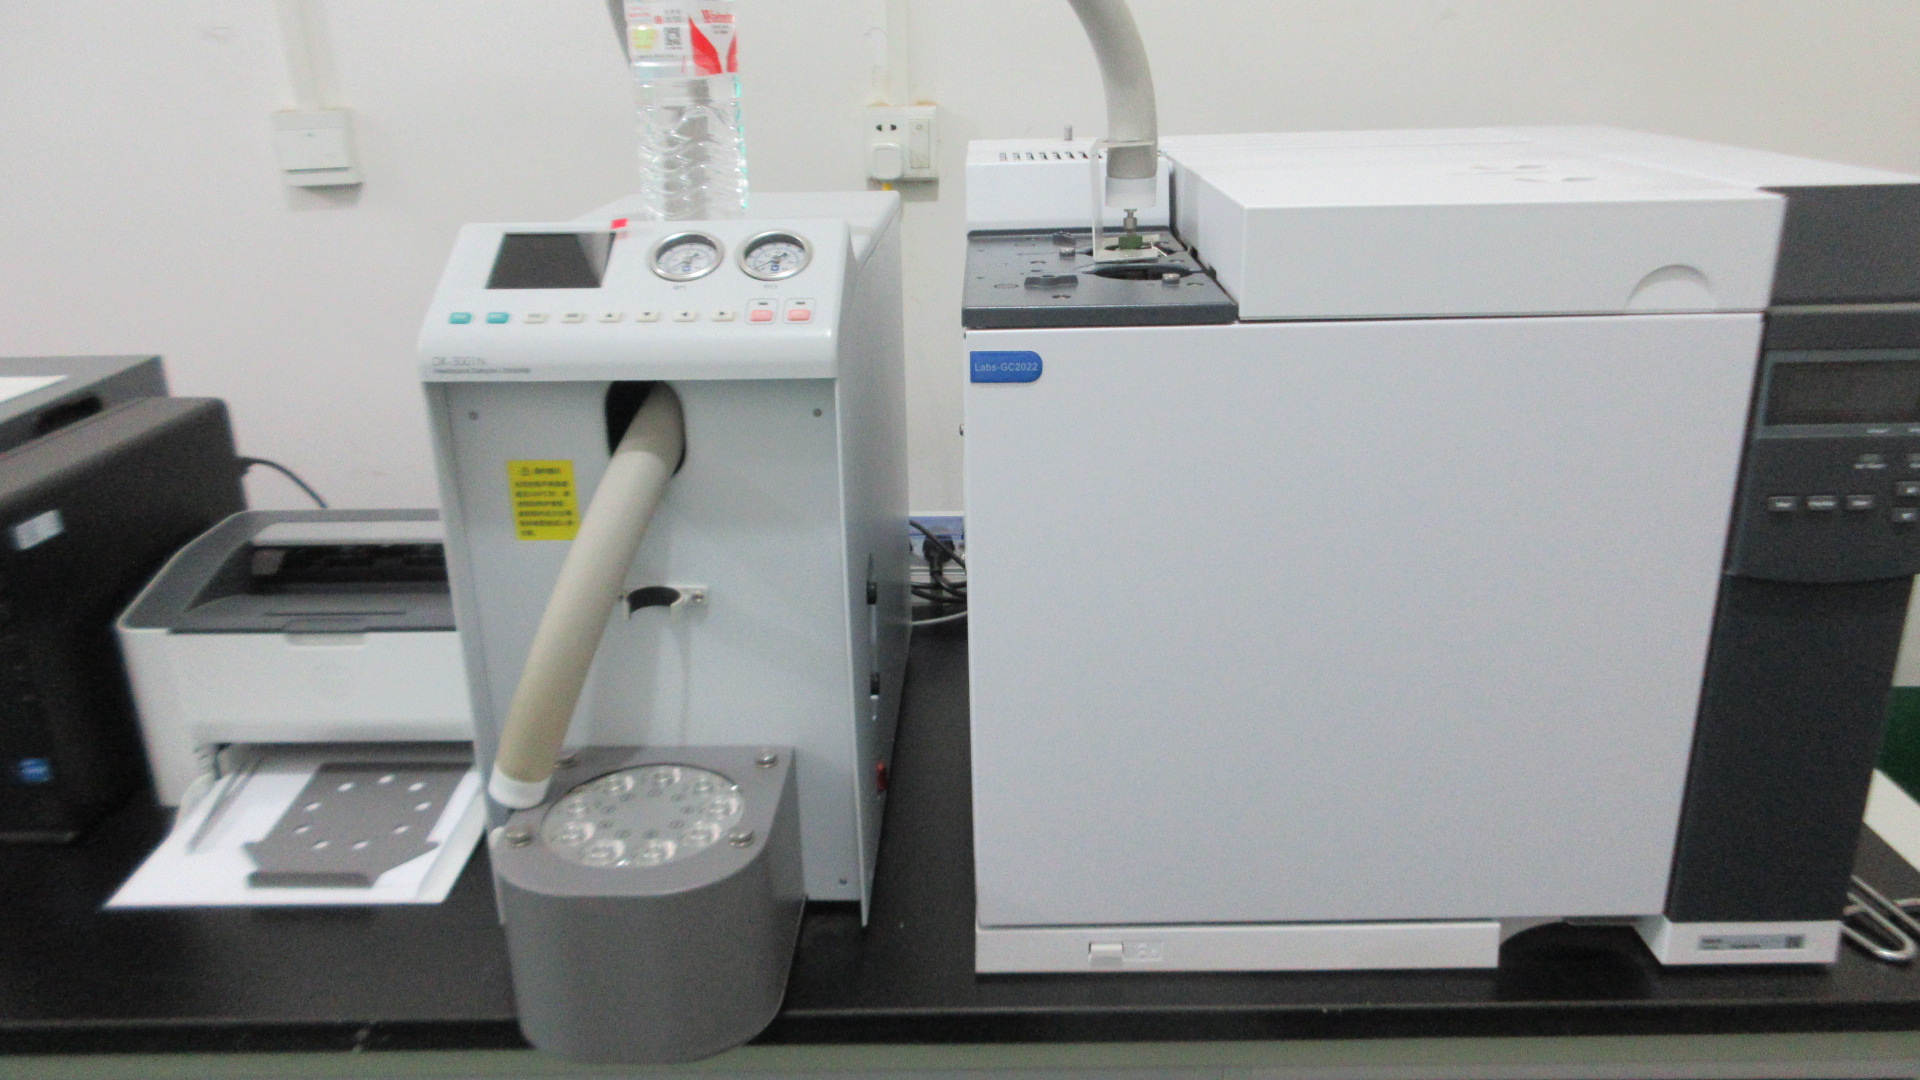
Gas Chromatography (GC)
Trace residual solvent monitoring complying with stringent USP, EP, and CP international safety limits.
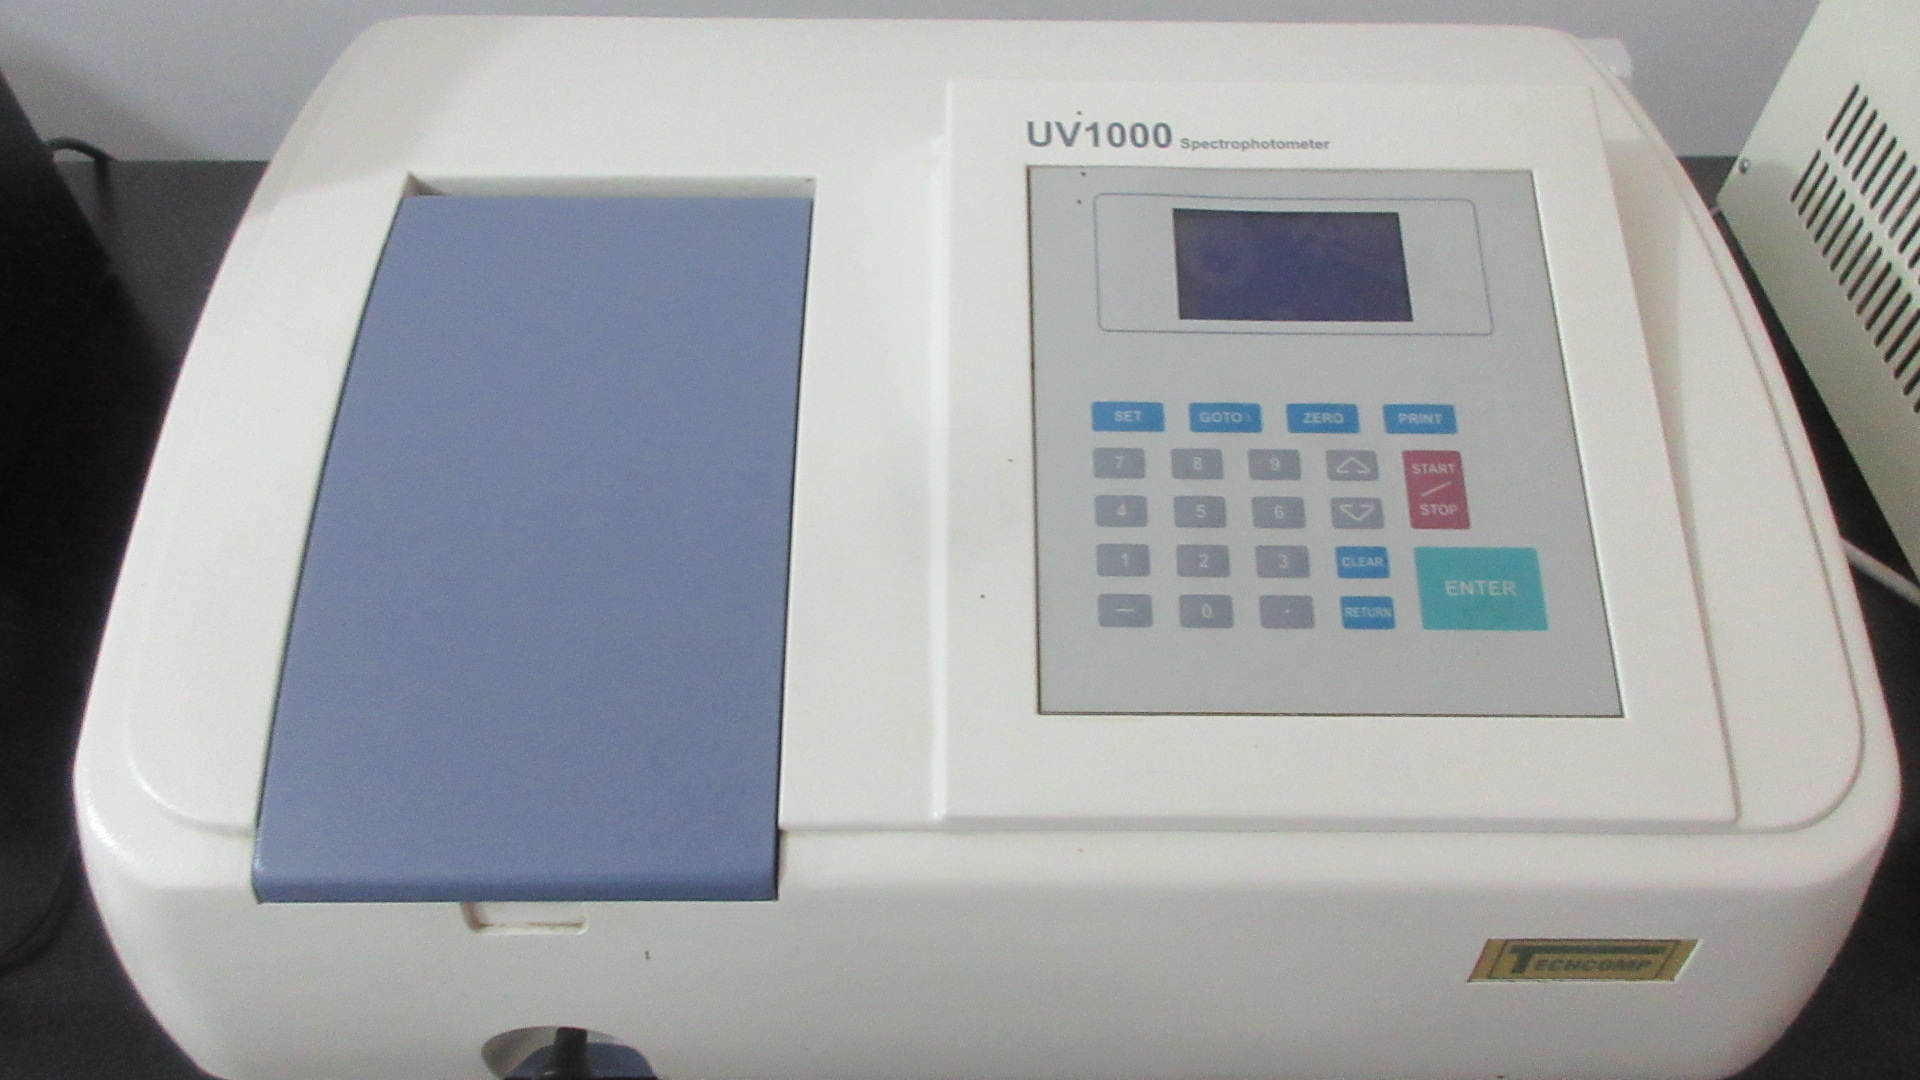
UV Spectrophotometer
Optical density quantification of mushroom beta-glucan polysaccharides, color absorption, and pigment assay values.
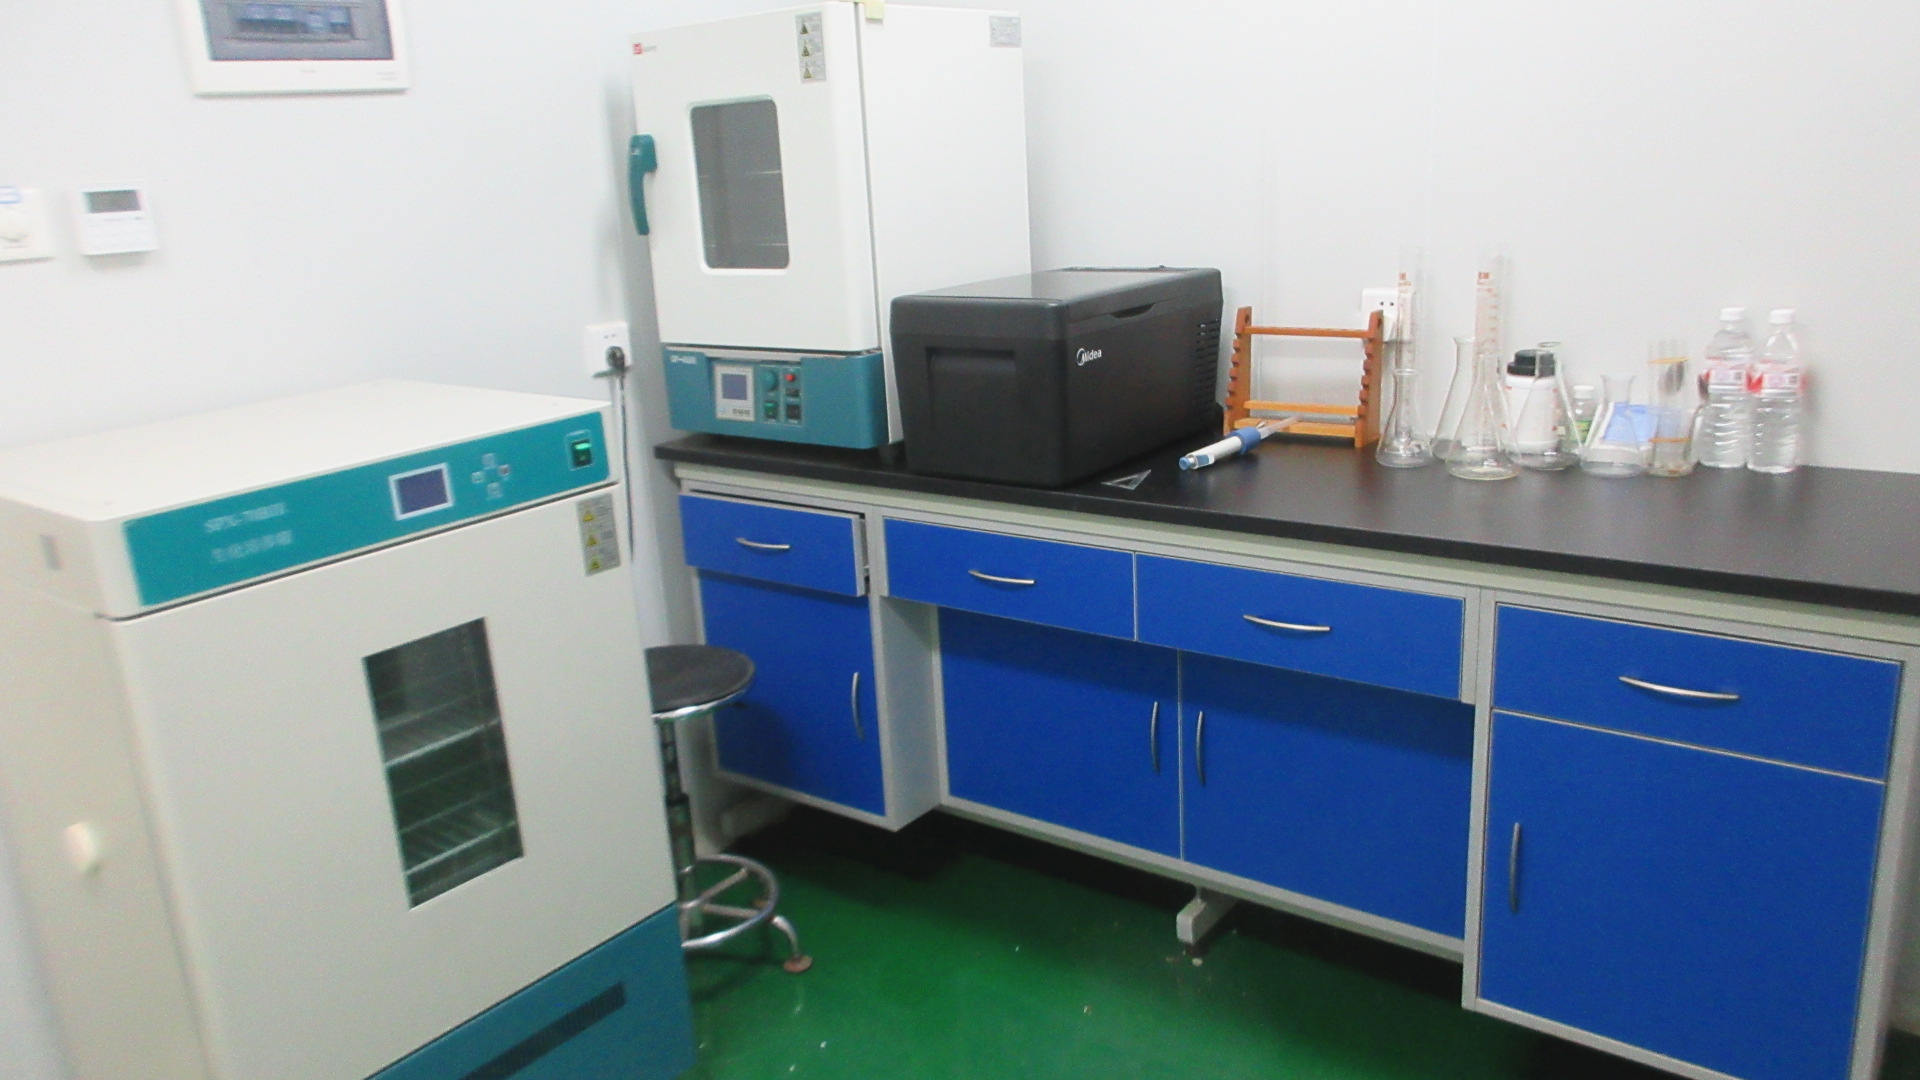
Microbiology Suite
Testing total plate count, yeast & mold, Coliforms, Salmonella, and E. coli in strict Class 10,000 biological isolation.
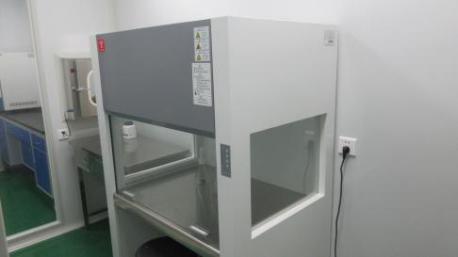
Clean Station
Class 100 laminar airflow containment cabinets ensure zero microbial cross-contamination during sample preparation.
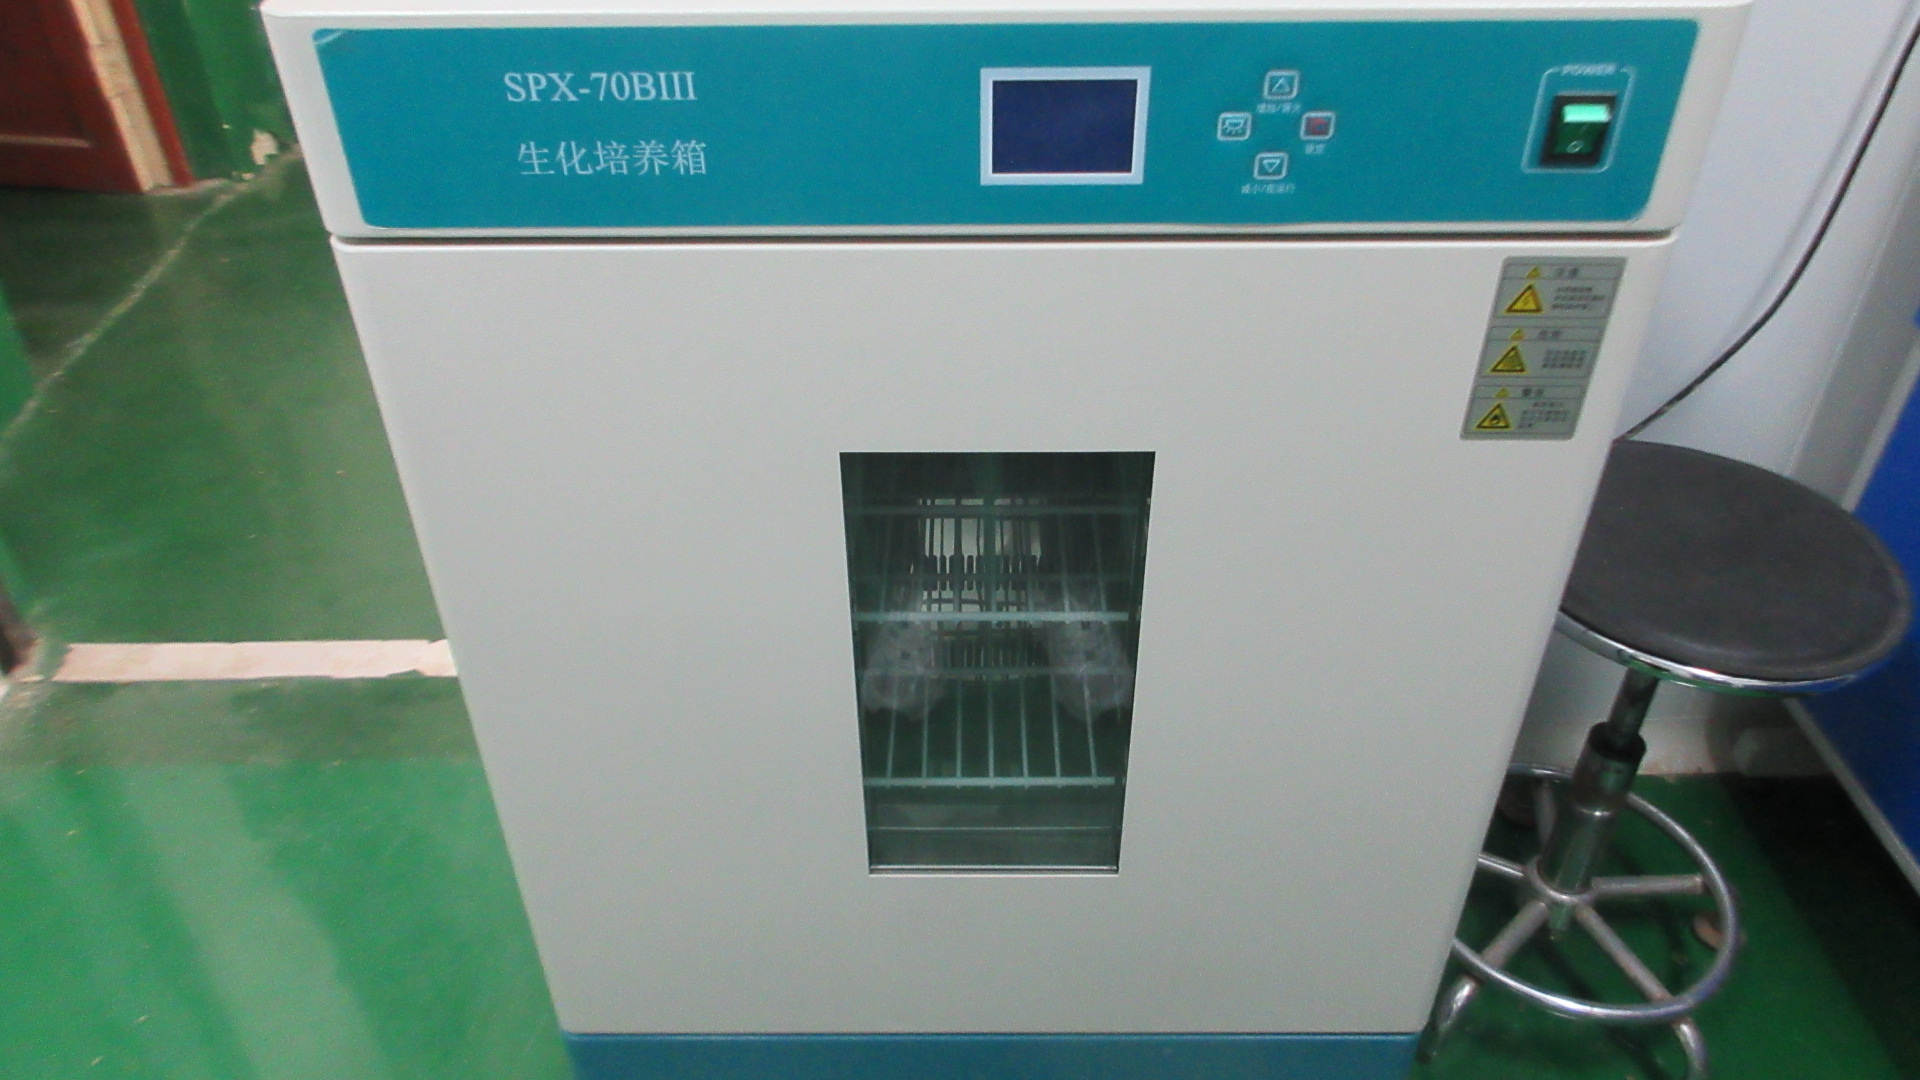
Incubator
Constant temperature and humidity chambers dedicated to rigorous microbiological culture incubation protocols.
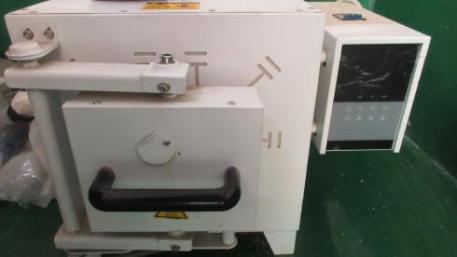
Muffle Furnace
High-temperature incineration chambers calibrated up to 1000°C for accurate total ash and sulfated ash measurements.
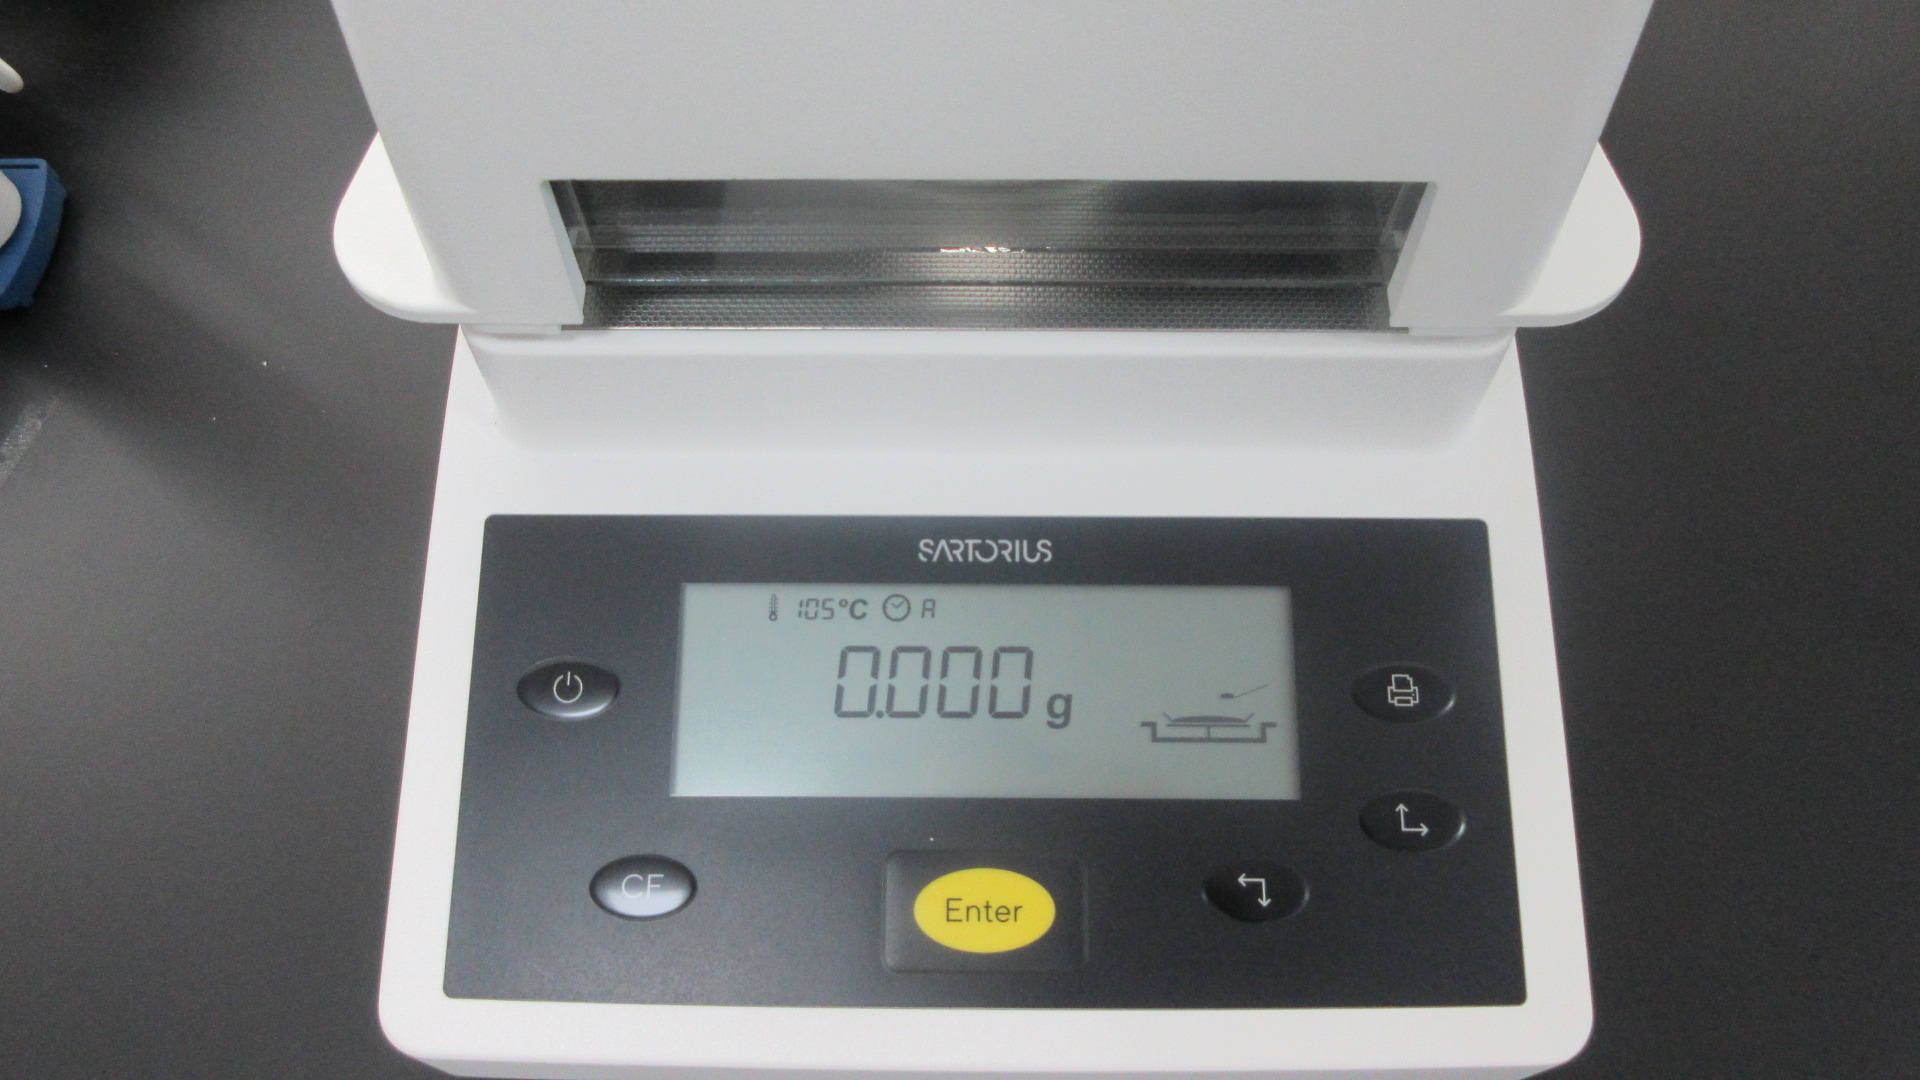
Moisture Meter
High-sensitivity halogen moisture analyzers determining loss on drying to prevent powder agglomeration and degradation.
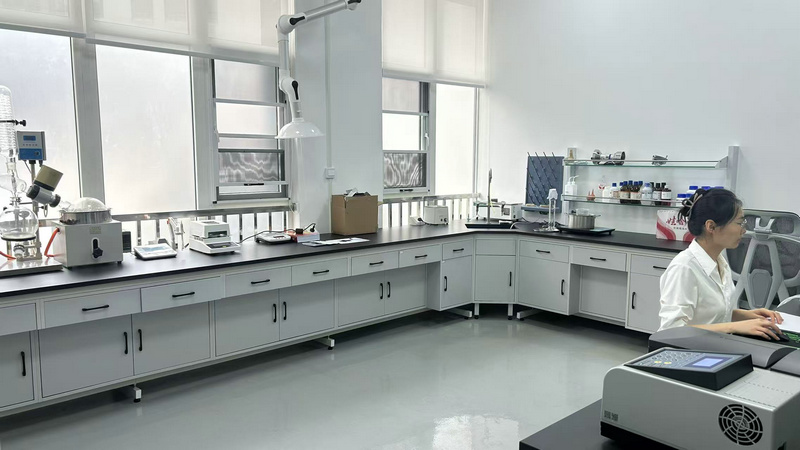
R&D Research Facility
Our 4 dedicated formulation engineers formulate tailored botanical active compounds, water-soluble matrixes, and premixes.
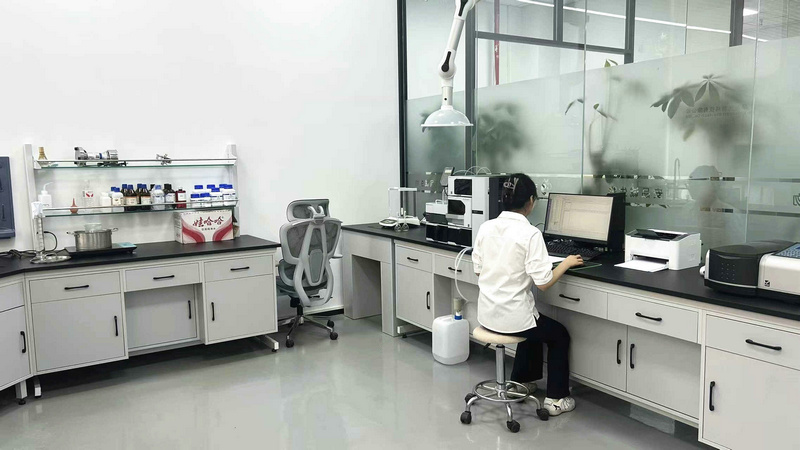
Formulation Bench
Small-batch trial formulation bench dedicated to client-specific solubility, natural color matching, and sweetness blending.
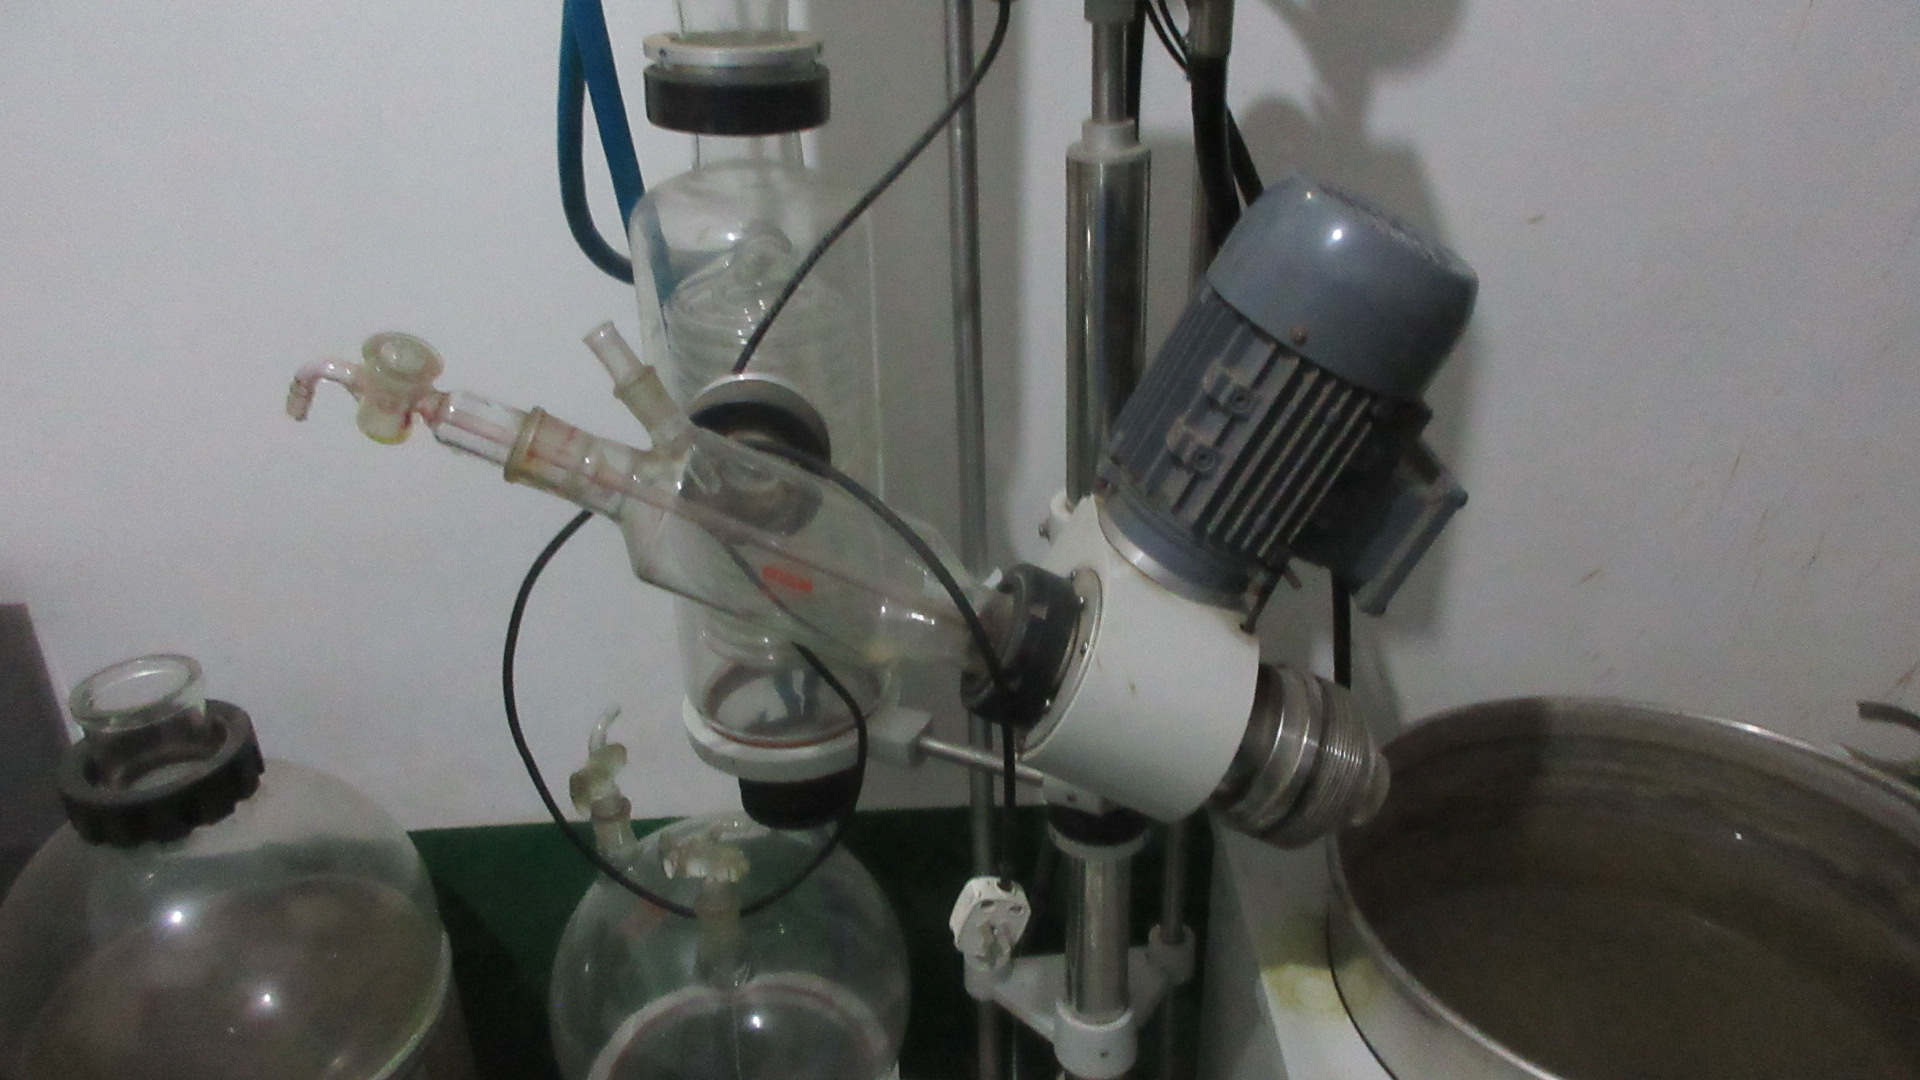
Pilot Rotary Evaporators
Bench-scale rotary evaporation setup allowing rapid extraction solvent testing before mass production scaling.
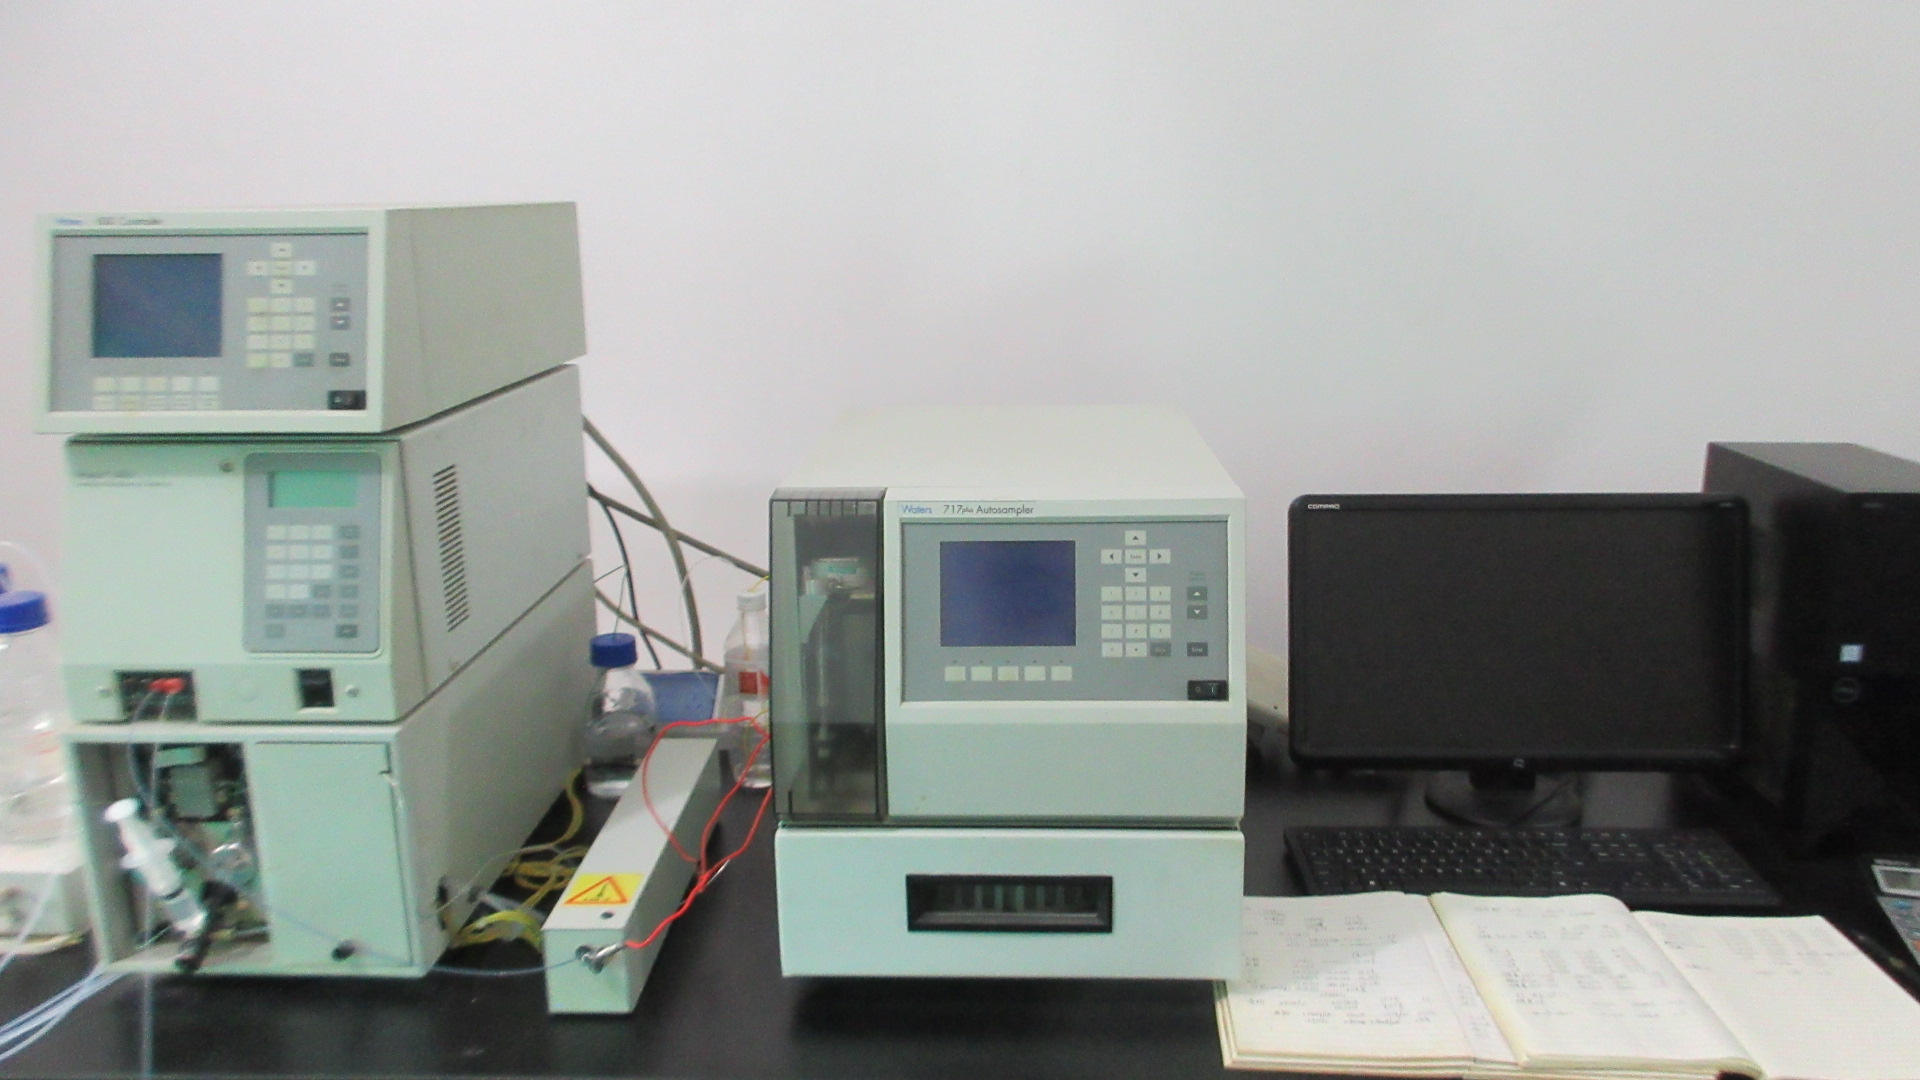
Method Development HPLC
Developing validated chromatographic retention time profiles and calibration curves for emerging active phytochemicals.
Supplying Verified Ingredients Across Global Continents
With multi-currency payment clearing and localized logistics handling, Xi'an Vexli Bio-Tech Co., Ltd. supplies verified ingredient solutions directly to brand manufacturers, contract packagers, and compounding facilities worldwide.
We work smoothly with regional compliance guidelines across North America, the European Union, Australia, Latin America, and Southeast Asia. Every single lot is accompanied by a batch COA, Allergen statement, Non-GMO declaration, and origin paperwork.
Core Logistics & Shipping Gateways
Seamless clearance and palletized dispatch through major international hub ports including Shanghai Port, Ningbo Port, and Tianjin Port. Air express options available via DHL, FedEx, and door-to-door DDP air freight for urgent production batches.
| Destination Region | Market Share | Primary Supplied Categories |
|---|---|---|
| North America | 30.0% | Organic Matcha, Phycocyanin, NMN, Sweetener Blends |
| Western Europe | 15.0% | EU Organic Mushroom Extracts, Chlorophyllin, Butterfly Pea |
| Oceania (AU / NZ) | 10.0% | Ceremonial Matcha, Marine Collagen, Superfood Powders |
| Middle East | 8.0% | Halal Certified Natural Colorants & Plant Extracts |
| South America | 5.0% | Nutraceutical Raw Ingredients & Food Colorants |
| Other Global Markets | 27.0% | Custom Active Formulations & Bulk Botanical Powders |
Request Specifications, Batch COAs, or Custom Quotations
Connect directly with our technical sales engineers. We provide comprehensive ingredient dossiers, sample dispatch within 48 hours, and transparent B2B contract terms.