Core Functional Botanicals & Standardized Extracts
High-yield, HPLC-quantified compounds manufactured under strict ISO22000, HACCP, Halal, and Kosher quality controls.
US $29.5M
Annual Global Export Volume
30+
Export Nations (US, EU, APAC)
25
Audited Partner Extraction Plants
1,250 m²
Dedicated Testing & Warehousing
1. Defining Industrial Excellence: The Terpenoid and Botanical Extract Matrix
Terpenoids represent one of the most structurally diverse classes of plant secondary metabolites. Formed from fundamental isoprene units (C5H8), their molecular architecture encompasses hemiterpenes, monoterpenes, sesquiterpenes, diterpenes, triterpenes, and tetraterpenes. In high-performance nutraceutical, cosmeceutical, and pharmaceutical formulation, isolating pure terpenoids without thermal degradation demands severe control parameters. When evaluating global manufacturing tiers, formulators must delineate between standard broad-spectrum botanical processing and isolated terpene fractions.
Xi'an Vexli Bio-Tech Co., Ltd., situated in Shaanxi Province—the historical and logistical nucleus of Chinese botanical extraction—operates with deep vertical integration. Rather than operating purely on open-market spot material, our raw botanicals are sourced at origin, monitored for geographic phytochemistry, and processed across 25 verified partner facilities. The table below provides an analytical comparison of manufacturing protocols deployed across tier-one terpenoid and functional botanical production:
| Terpenoid / Phytochemical Class | Typical Botanical Origin | Extraction & Isolation Pathway | Primary Quality Control Indicator | Target Regulatory Limits |
|---|---|---|---|---|
| Monoterpenoids & Volatiles | Mentha, Citrus, Pinus spp. | Fractional steam distillation, Supercritical CO2 (scCO2) | GC-MS Fingerprinting & Chiral GC | Residual Solvents < USP <467> Class 3 |
| Diterpenoids (e.g., Ginkgolides, Steviol) | Ginkgo biloba, Stevia rebaudiana | Hydro-ethanolic extraction, Macroporous resin separation | HPLC-ELSD / HPLC-DAD quantification | Ginkgolic acids < 5 ppm (EP/USP compliant) |
| Triterpenoids (e.g., Ursolic Acid, Betulin) | Rosmarinus officinalis, Betula alba | Solvent-assisted thermal extraction, Multi-stage crystallization | HPLC-UV Assay ≥ 98% | Heavy Metals: Pb ≤ 1.0 ppm, As ≤ 1.0 ppm |
| Tetraterpenoids & Carotenoids | Haematococcus pluvialis, Tagetes erecta | Low-temperature physical cell-rupture, Ethyl acetate / scCO2 | Spectrophotometry & HPLC cis/trans isomer ratio | Loss on Drying ≤ 5.0%, Peroxide value control |
| Polyphenolic & Complex Actives | Camellia sinensis, Mulberry Leaf | Low-temperature membrane concentration & vacuum spray drying | UV-Vis Polysaccharide & Phenolic assay | Multi-residue screen (BS EN 15662: 500+ compounds) |
For research and development procurement specialists, understanding this analytical divergence is critical. A crude 10:1 ratio extract cannot provide the pharmacokinetic predictability of an isolated, HPLC-standardized single entity or targeted active group. Our analytical laboratories deploy high-performance liquid chromatography (HPLC), gas chromatography (GC), and UV-Vis spectrophotometers to guarantee batch-to-batch chemical congruity.
Benchmark: Selecting a Top 10 Terpenoid & Botanical Exporter
Comprehensive qualification criteria established by international regulatory frameworks (FDA 21 CFR Part 111, EU 2023/915).
01
Chromatographic Transparency
A leading exporter must provide authentic HPLC/GC-MS traces displaying peak purity, baseline resolution, and unambiguous retention times rather than non-specific gravimetric assertions.
02
Origin-Direct Botanical Tracing
Phytochemical density depends heavily on altitude, climate, and soil geochemistry. Direct sourcing at Chinese origins eliminates seasonal potency variations and prevents species substitution.
03
Clean Extraction Engineering
Leading suppliers avoid Class 1 and Class 2 solvents, standardizing exclusively on subcritical water, food-grade ethanol, or green supercritical CO2 extraction methods to prevent residual halogenated hydrocarbons.
04
Cross-Border Regulatory Compliance
Validation against destination laws—such as BS EN 15662 pesticide multi-residue panels for the European Union and heavy metal limits for California Proposition 65—is mandatory for every batch.
05
Flexible Batch Scaling (1kg to FCL)
True Tier 1 partners accommodate rapid pilot bench testing with 1 kg minimum order quantities while possessing the capacity to deliver multi-ton container shipments seamlessly.
06
Comprehensive Transport Clearance
Full integration of IATA DGR and IMDG non-hazardous certification reports prevents expensive maritime or airfreight custom clearance impounds at international distribution hubs.
Future Sourcing & Industrial Trends (2025–2030)
Key supply chain transitions shaping formulation parameters, sustainability audits, and extraction technology.
TR
Targeted Terpene Tailoring
Industrial demand is migrating from whole-herb extracts to precise terpene-cannabinoid and terpene-polyphenol synergies. Reconstituted, designer botanical fractions engineered for specific neuroprotective, adaptogenic, or sensory profiles are dominating functional beverage innovation.
CF
Carbon-Neutral Extraction Tech
Energy-intensive vacuum evaporation is yielding to continuous membrane nano-filtration and enclosed cryogenic ethanol cycles. Global buyers are factoring Scope 1 and Scope 2 carbon indices directly into their annual vendor performance scorecards.
AI
Phytochemical Fingerprint AI
Near-infrared (NIR) spectroscopy combined with machine learning models allows real-time raw material identification at receipt docks, instantly flagging adulterations, synthetics, or off-harvest variations before batches proceed to industrial extraction columns.
Why Partner with Xi'an Vexli Bio-Tech?
Industrial-scale production backed by rigorous third-party auditing and intellectual property.
SGS On-Site Audited Facilities
Our extraction facilities and warehouses have undergone exhaustive on-site evaluation by SGS, confirming world-class standards across personnel hygiene, storage controls, and raw material handling.
Proprietary Extraction Patents
Holding Chinese Invention Patent ZL 2014 1 0464649.9 (advanced isolation of protocatechuic aldehyde) and Utility Model Patent No. 14520048 for high-efficiency plant extraction apparatus.
Tier-1 Quality Assurance
Serving multinational brands and Fortune 500 downstream clients with dedicated batch Certificate of Analysis (COA), specification dossiers, allergen control declarations, and MSDS documentation.
Multi-Category Consolidation
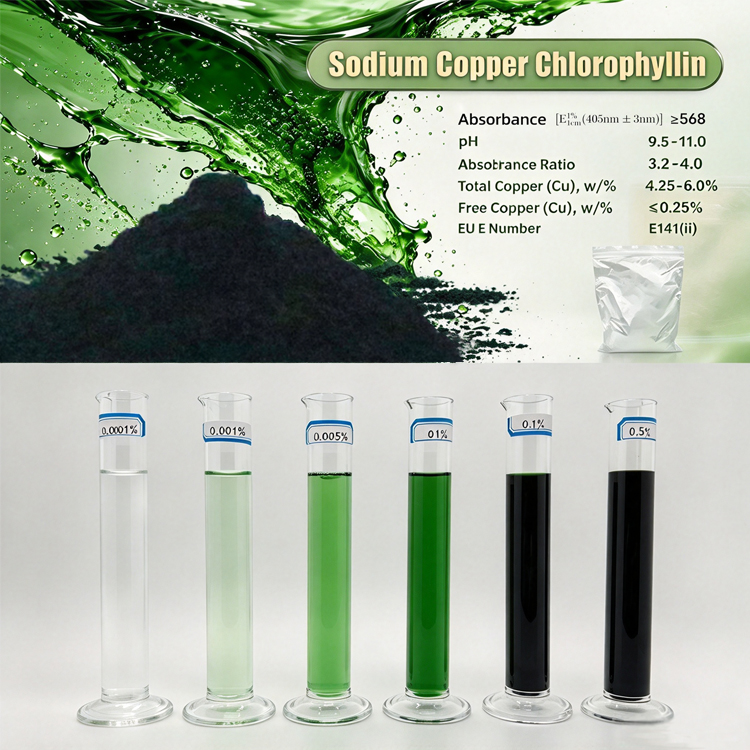
Consolidate clean-label sweeteners (Allulose, Monk Fruit, Stevia), functional pigments (Phycocyanin, Chlorophyll), and high-assay longevity actives (NMN, NAD+) into a single ocean consignment.
Full OEM & Particle Engineering
Complete custom formulation, micronization (80 to 450 mesh), custom microencapsulation for unstable volatile terpenes, and end-to-end private labeling delivered ready for distribution.
Multi-Currency & Global Logistics
Flexible commercial settlements across USD, EUR, GBP, CAD, AUD, JPY, CHF, HKD, and CNY, under standard Incoterms from EXW and FOB to seamless direct-to-warehouse DDP delivery.
Frequently Asked Questions for B2B Sourcing
Clear, direct answers to common queries from global sourcing directors, analytical chemists, and supply managers.
What are the standard Minimum Order Quantities (MOQ)?
For the majority of our standardized active extracts, botanical powders, and terpenoid isolates, our minimum order quantity starts at just 1 kg. Bulk commodities and specialty sugars, such as D-Allulose or marine collagen, operate under custom commercial batch tiers (25 kg to 500 kg).
What analytical documentation accompanies each export shipment?
Every commercial lot is accompanied by a batch-specific Certificate of Analysis (COA) detailing physical appearance, particle size, assay percentage (via HPLC/UV), heavy metal metrics (ICP-MS), residual solvents, and full microbiological testing. Third-party SGS pesticide screening is provided upon agreement.
How do you manage batch stability and heat-sensitive degradation?
Thermal degradation of delicate aromatic terpenes and polyphenols is mitigated using low-temperature falling-film vacuum concentration, nitrogen flushing during milling, and vacuum-sealed aluminum moisture-barrier inner packaging stored in temperature-controlled warehouses.
Are samples available for pre-shipment laboratory validation?
Yes. We routinely provide 20g to 100g verification samples to qualified industrial buyers. This enables your internal R&D and analytical laboratories to cross-reference HPLC retention times, solubility, sensory characteristics, and bulk density before formal commercial release.
Can you match customized particle sizes for tableting or beverages?
Yes. Our processing lines utilize multi-stage air-classifier mills and vibrating sieves capable of targeting particle distributions from free-flowing coarse granular specifications (40–80 mesh for capsules) to ultra-fine dispersions (300–450 mesh for instant beverage lattes).
What Incoterms and international payment options are supported?
We routinely execute freight under EXW, FOB, CFR, CIF, CIP, and door-to-door DDP arrangements via sea, air, and international express couriers. Commercial settlements can be processed via T/T, L/C at sight, PayPal, or escrow across multiple major currencies including USD, EUR, and GBP.
Request Technical Dossiers, Batch COAs & Commercial Quotations
Submit your target chemical specification, purity requirements, particle mesh, and projected purchase volumes. Our chemical engineering team replies within 12 working hours.
Inquire Now